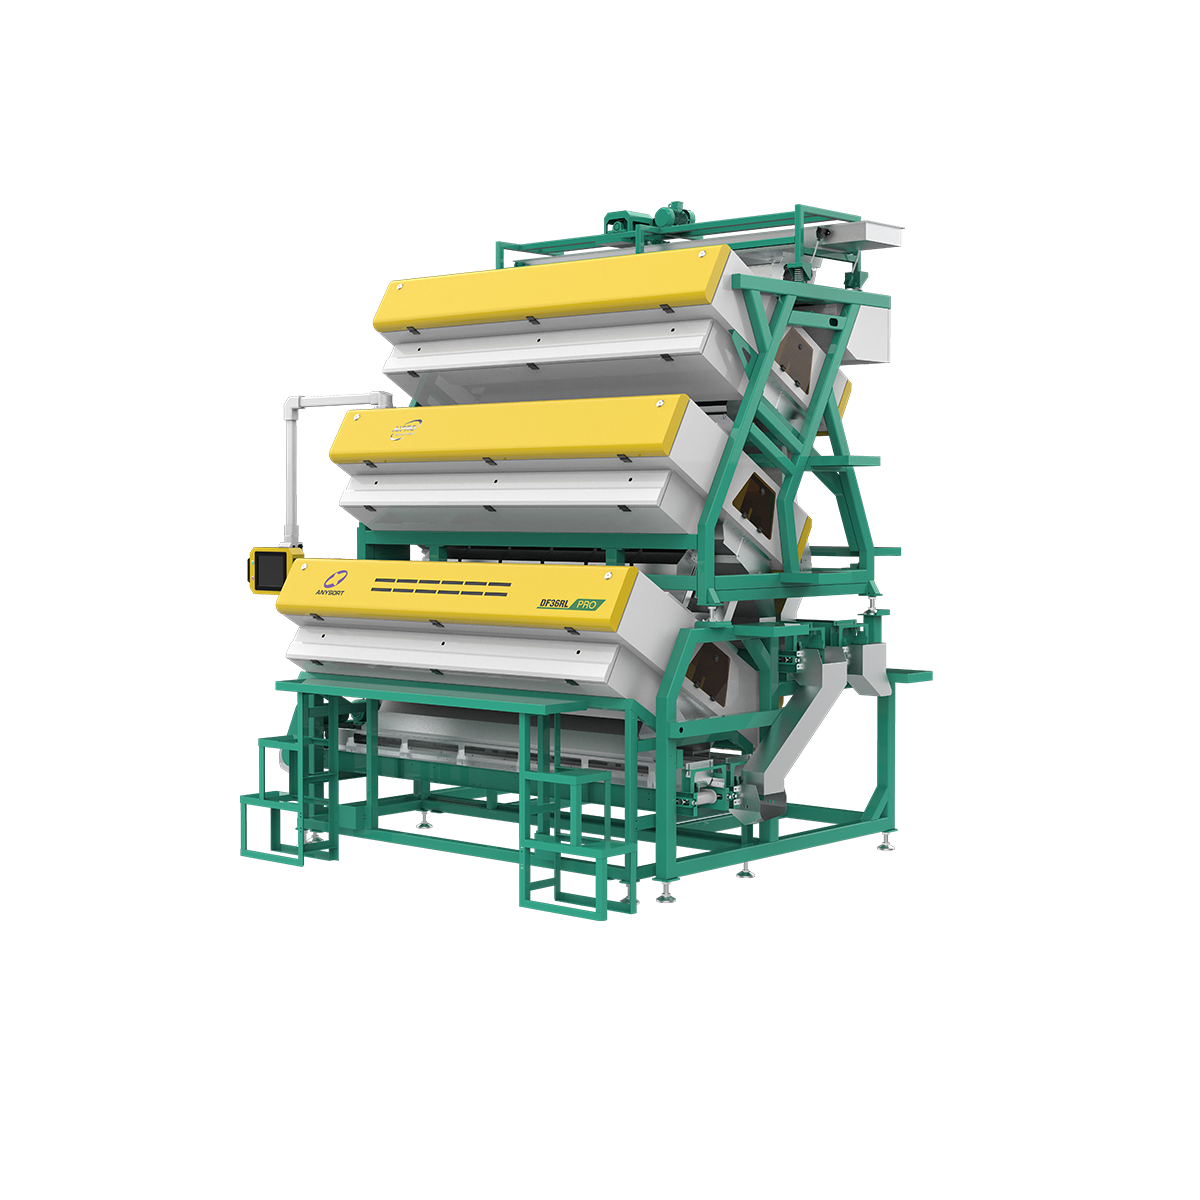
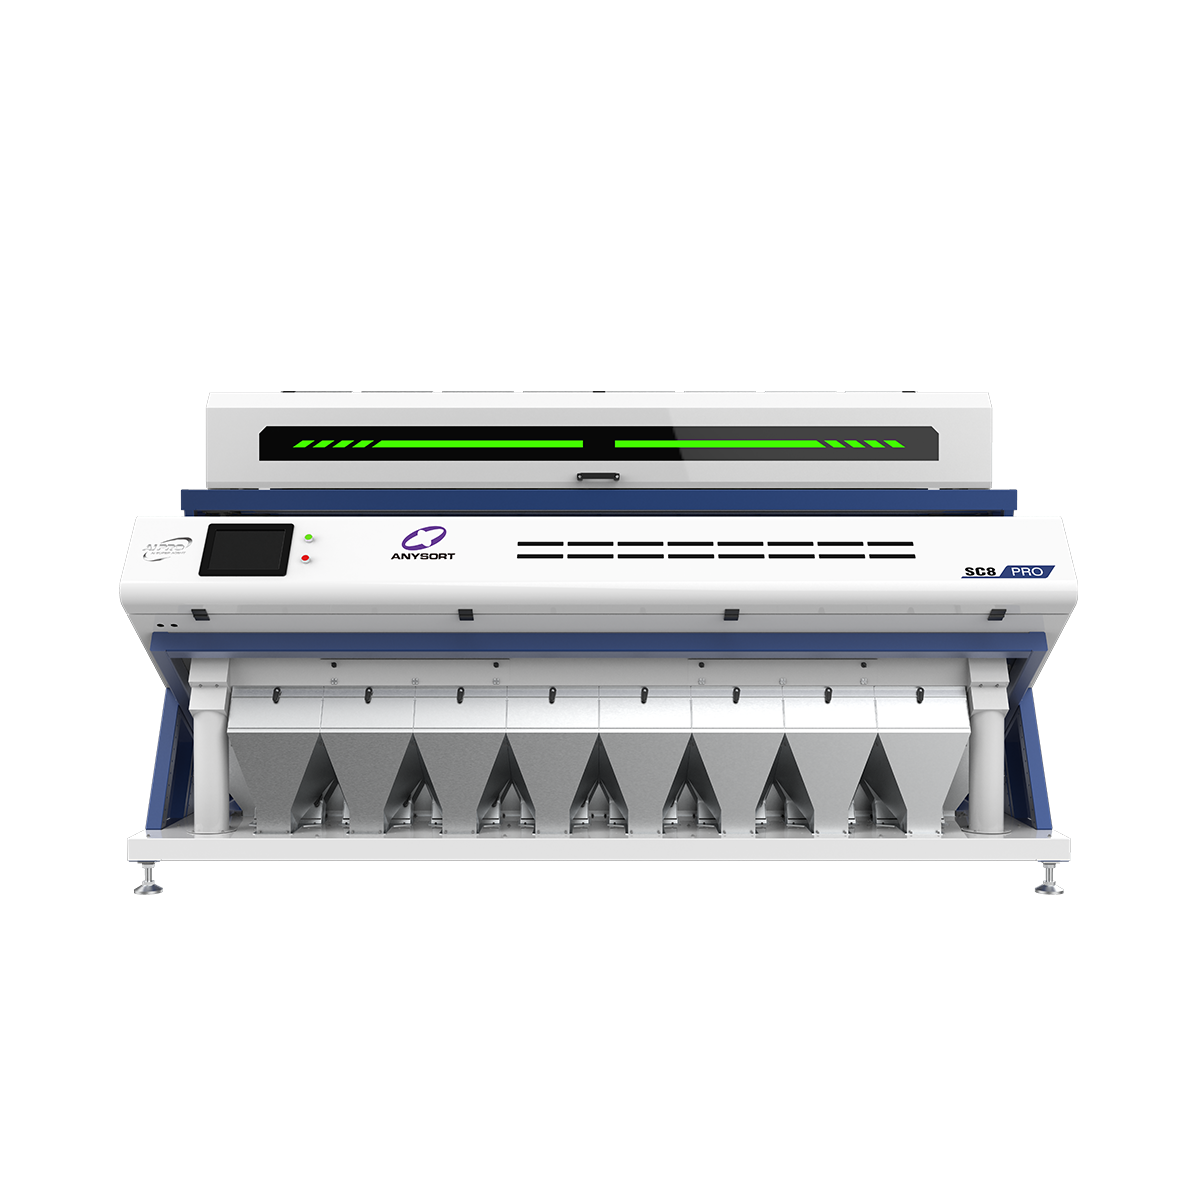
cashew kernel grading machine
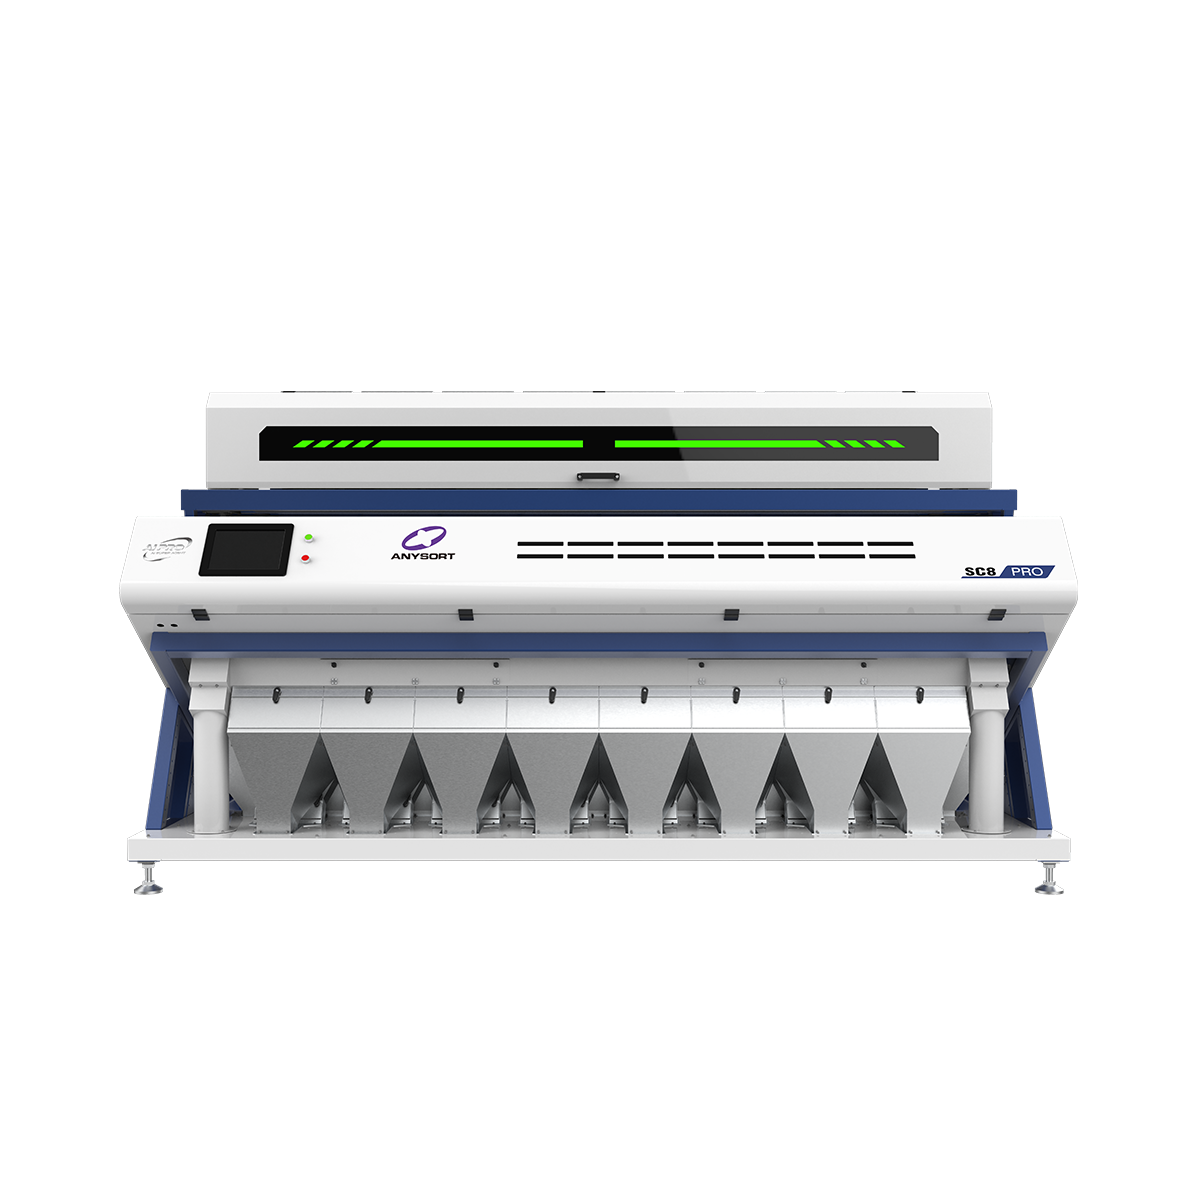
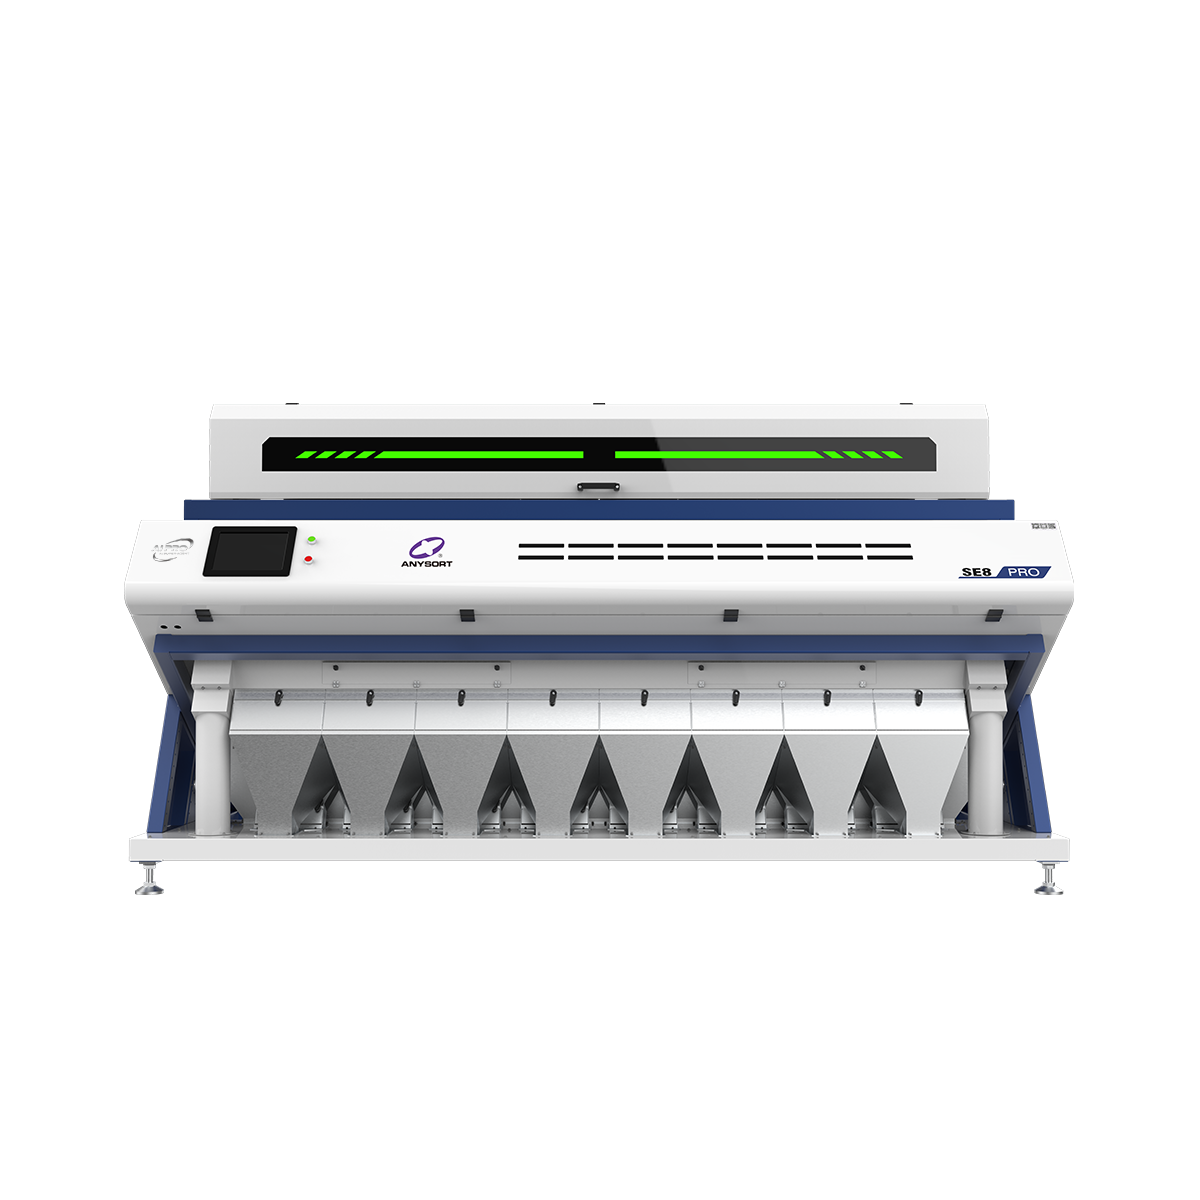
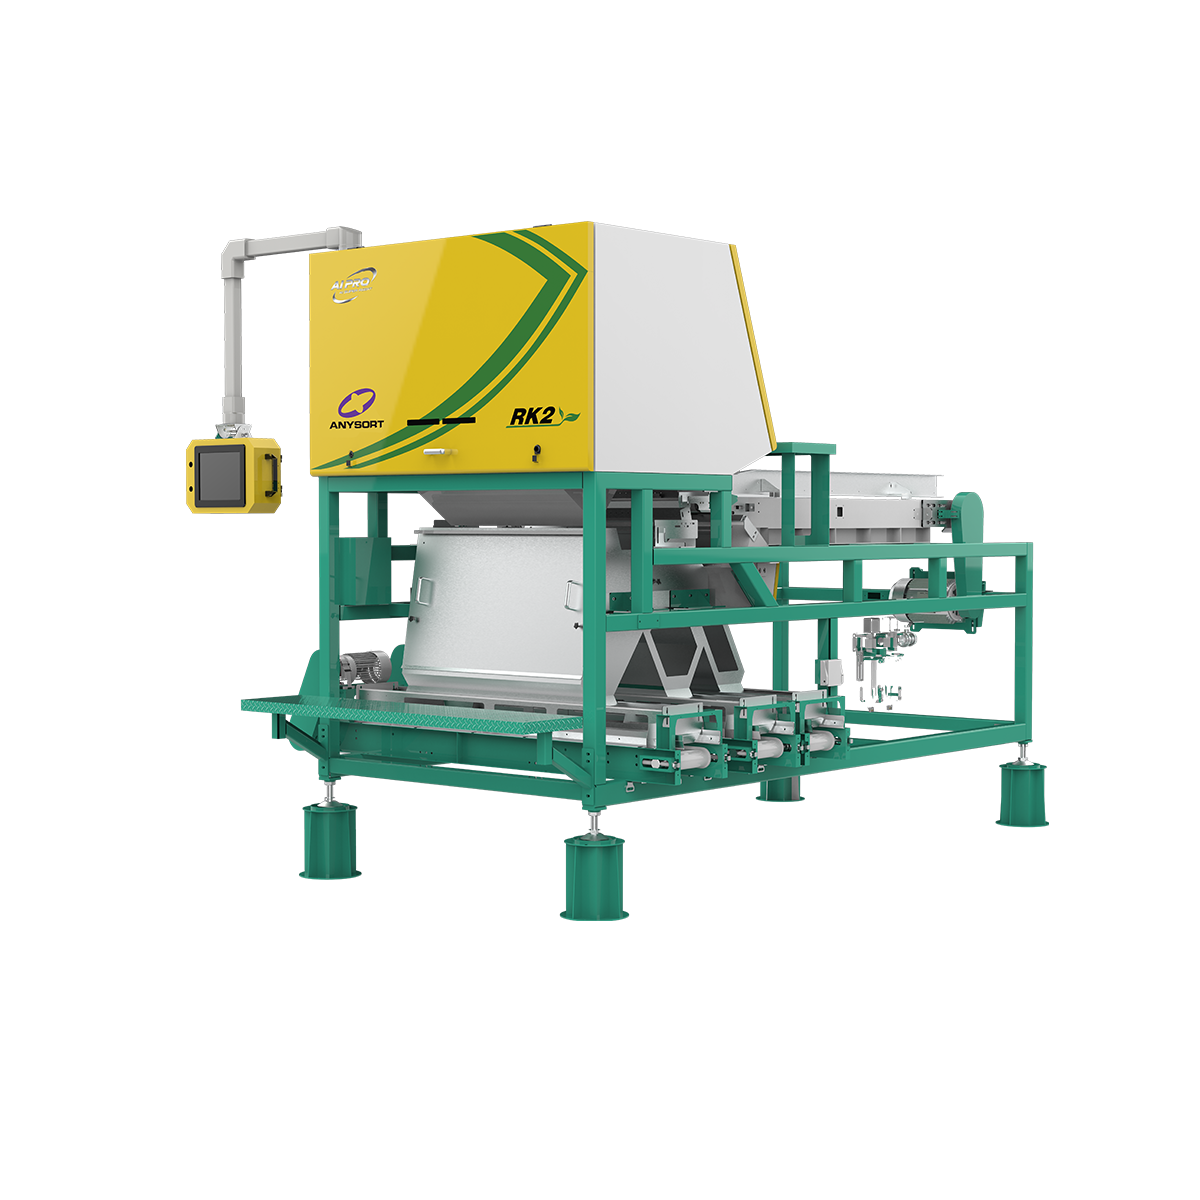
A cashew kernel grading machine is an advanced automated system designed to sort and classify cashew kernels based on size, quality, and condition. This specialized equipment plays a crucial role in cashew processing facilities worldwide, ensuring consistent product standards and maximizing yield efficiency. The cashew kernel grading machine utilizes sophisticated optical sensors and precise mechanical mechanisms to evaluate each kernel individually, separating them into distinct categories for different market demands.
The primary function of a cashew kernel grading machine is to eliminate defective, discolored, or undersized kernels while organizing acceptable products into uniform grades. Modern cashew kernel grading machines employ multi-dimensional scanning technology that detects surface imperfections, moisture content variations, and dimensional inconsistencies with remarkable accuracy. These machines can process hundreds of kilograms per hour, significantly reducing manual labor requirements and human error in the sorting process.
Technological features of contemporary cashew kernel grading machines include intelligent sorting algorithms, real-time quality monitoring systems, and customizable grading parameters. The equipment integrates seamlessly with existing production lines, featuring user-friendly control panels and automated data logging capabilities. Applications span commercial cashew processing operations, export-oriented facilities, and large-scale agricultural enterprises seeking premium product consistency and enhanced market competitiveness through reliable cashew kernel grading machine technology.

 EN