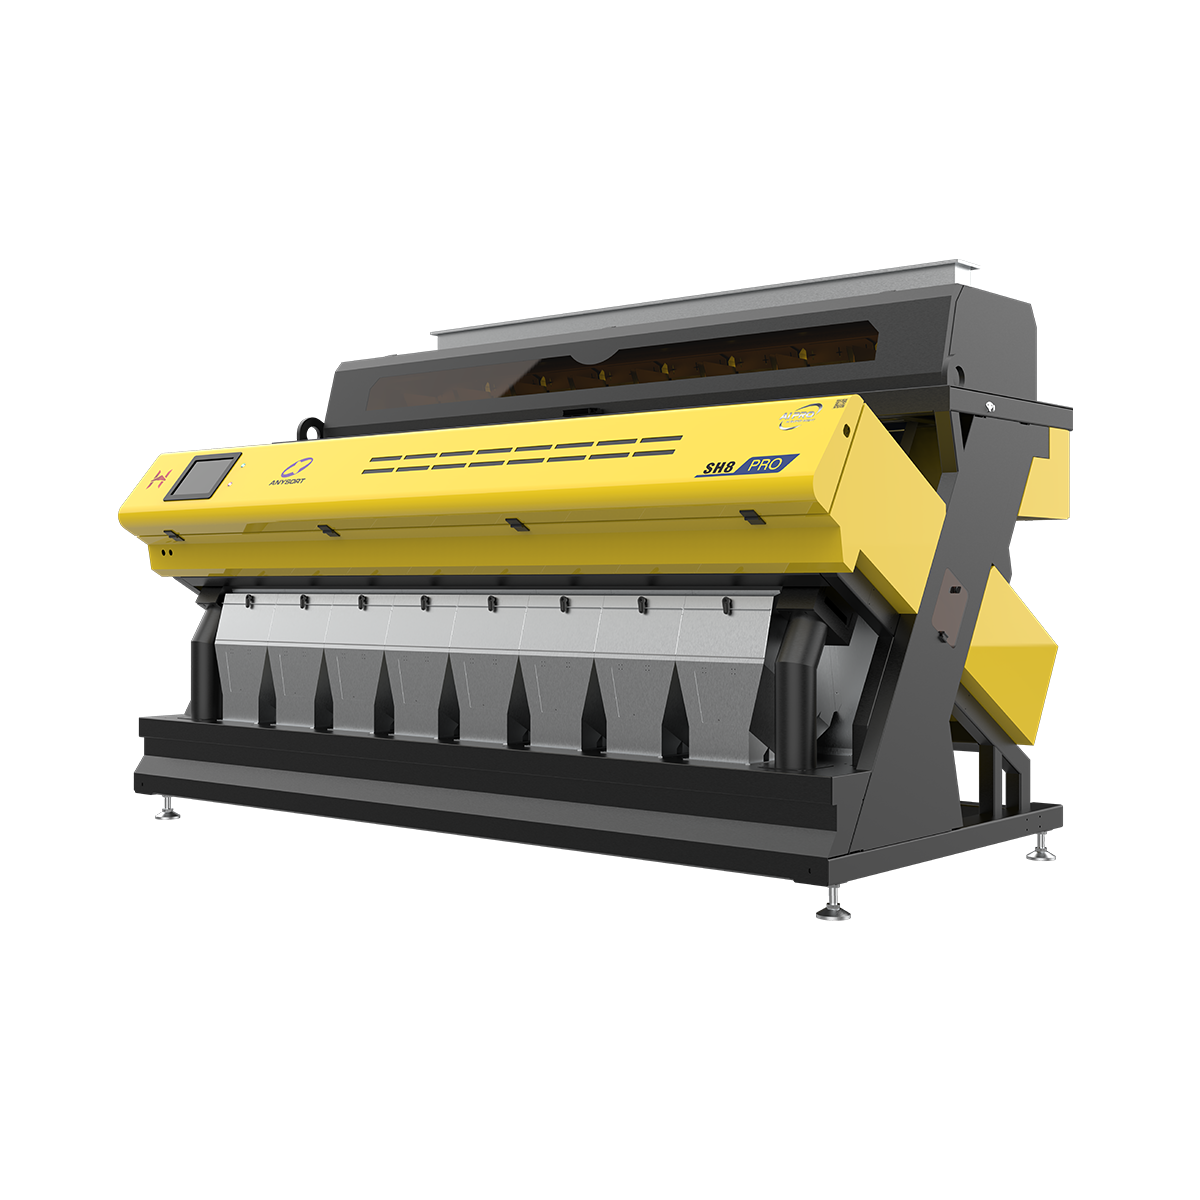
Best Genius Optical Sorter Technology

All Categories

best genius optical sorter

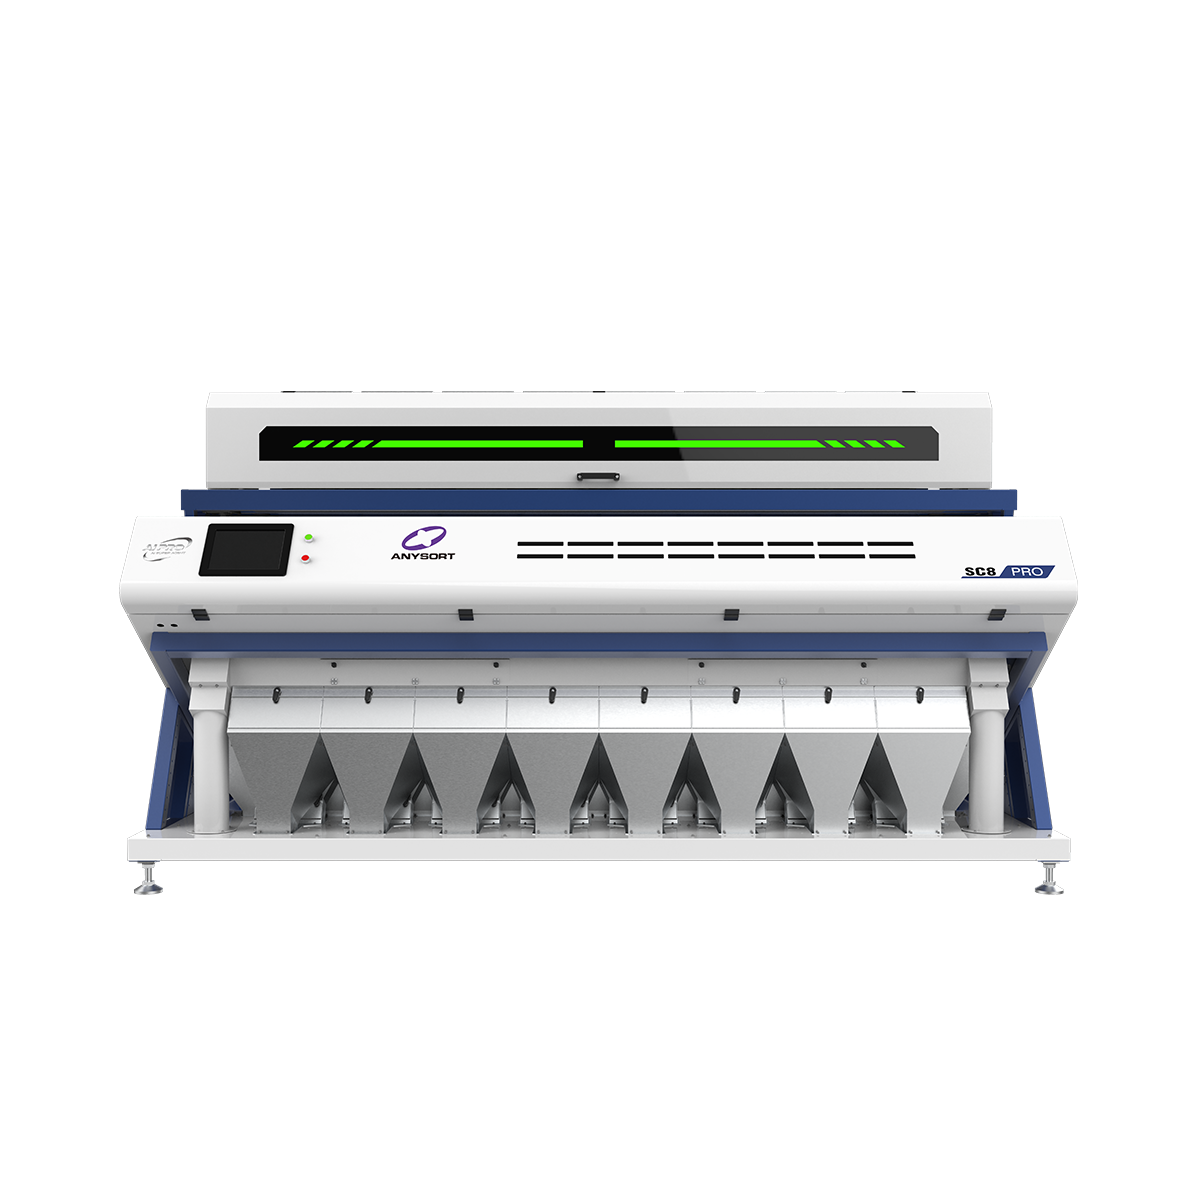
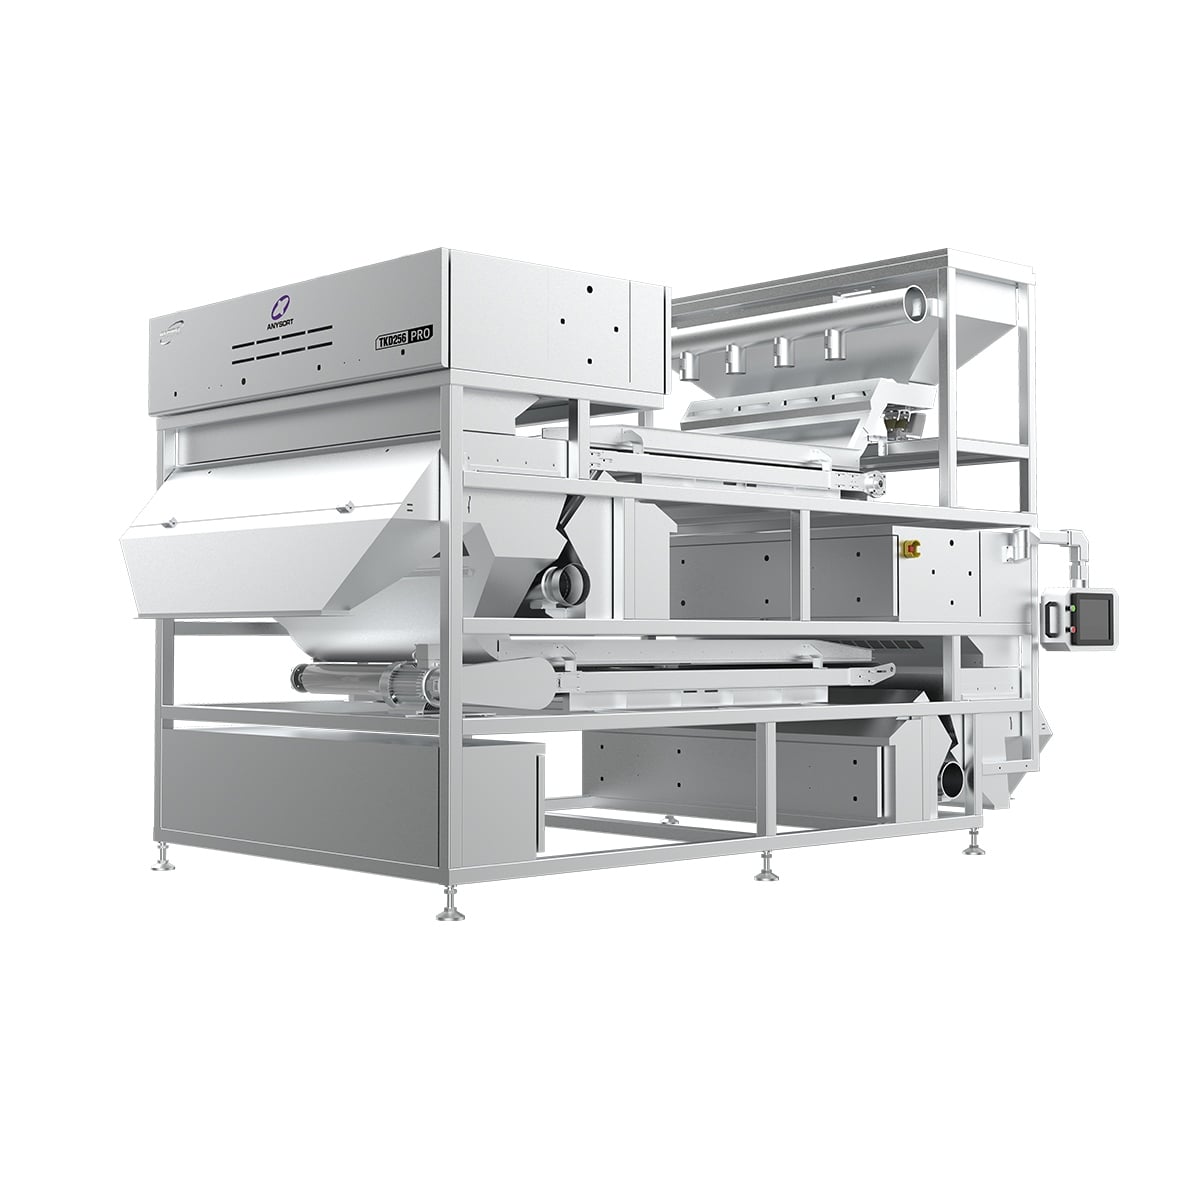
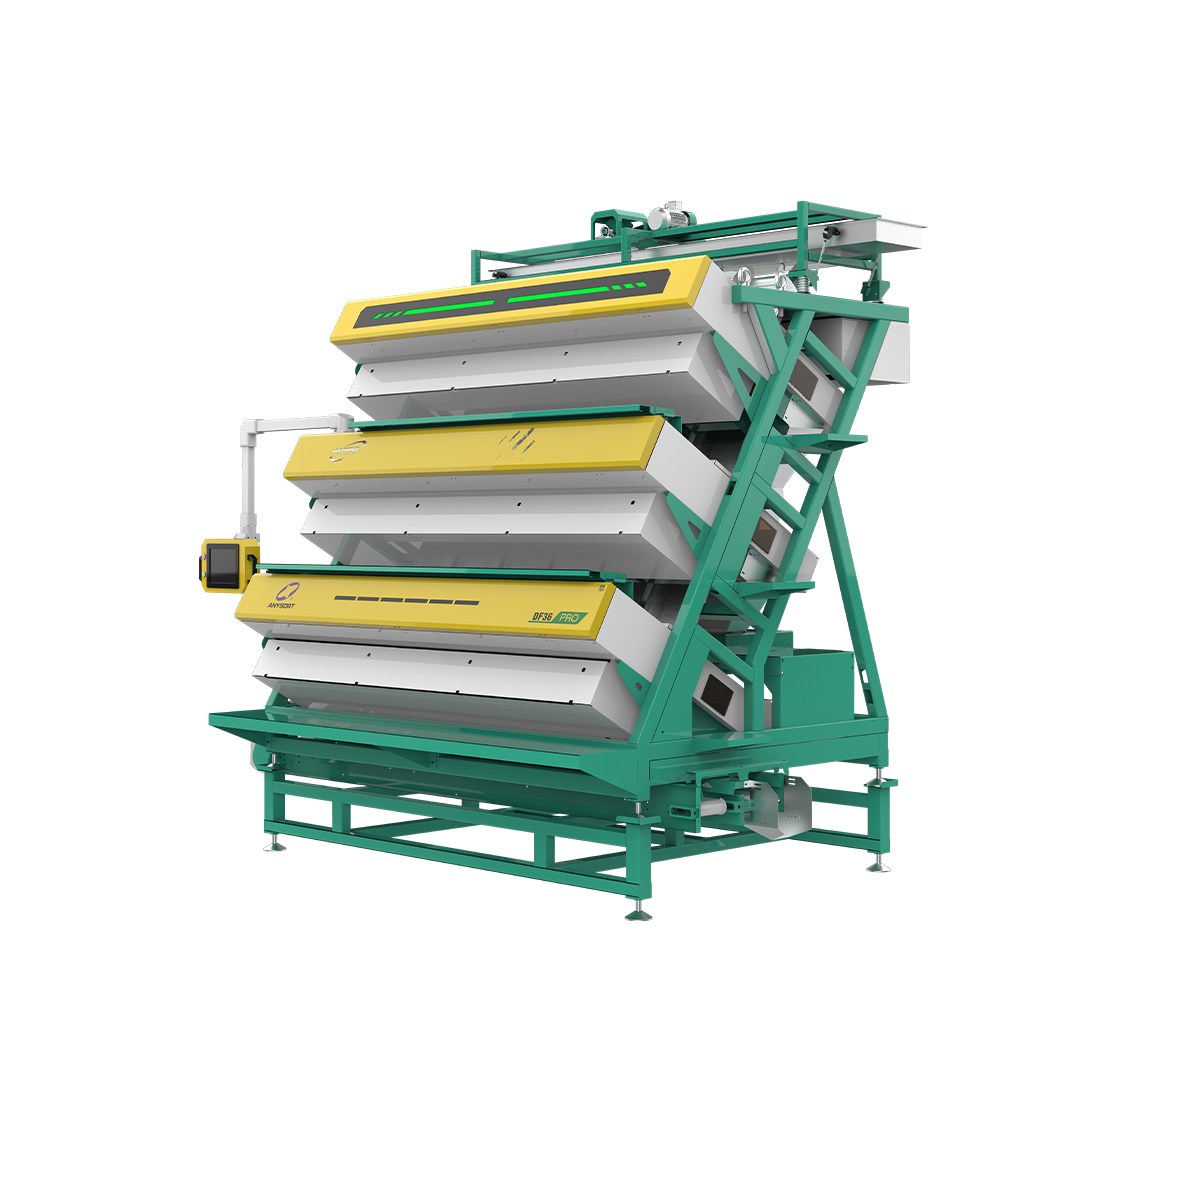
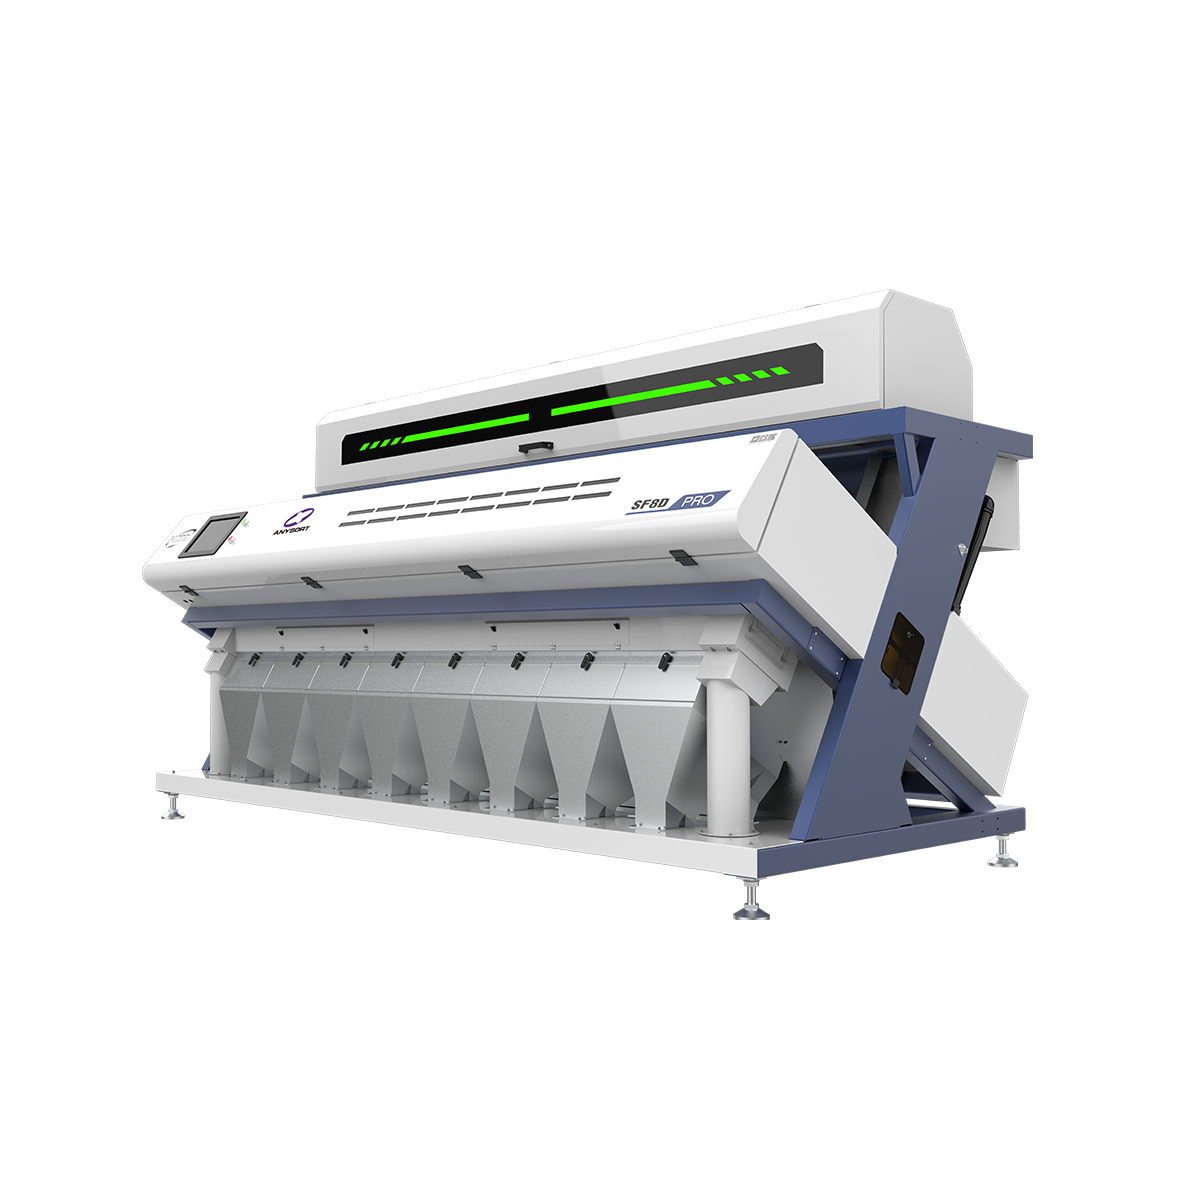
The best genius optical sorter represents cutting-edge technology designed to revolutionize material sorting processes across multiple industries. This advanced sorting system utilizes sophisticated optical sensors and artificial intelligence to identify, classify, and separate materials with exceptional precision and speed. The best genius optical sorter employs high-resolution cameras and spectroscopic analysis to detect subtle differences in color, shape, size, and material composition that human operators might miss. Technologically, the best genius optical sorter integrates machine learning algorithms that continuously improve sorting accuracy through adaptive learning. The system features real-time image processing capabilities, enabling rapid decision-making at processing speeds exceeding several tons per hour. Its modular design allows seamless integration into existing production lines without requiring extensive infrastructure modifications. Applications for the best genius optical sorter span recycling facilities, food processing plants, mining operations, and pharmaceutical manufacturing. In recycling centers, it effectively separates plastics, metals, and paper with remarkable accuracy. Food processors utilize the best genius optical sorter to remove contaminants and ensure product quality consistency. The technology proves invaluable in agricultural operations for grain grading and seed classification, while mining companies rely on it for ore sorting and mineral recovery. Equipped with advanced filtration systems and customizable ejection mechanisms, this solution handles diverse material types efficiently. The best genius optical sorter delivers comprehensive sorting solutions that enhance productivity, reduce waste, and improve product quality across industrial applications.

Popular Products

The best genius optical sorter delivers transformative operational benefits that directly enhance your bottom line and production efficiency. First, this system dramatically increases throughput capacity, processing materials at speeds that exceed traditional manual and outdated mechanical sorting methods. Your facility can handle significantly larger volumes without expanding floor space or adding additional labor, directly reducing per-unit processing costs. Accuracy represents another compelling advantage of the best genius optical sorter. The technology eliminates human error from sorting decisions, achieving consistency rates above 99 percent. This precision dramatically reduces contamination in your final products, minimizes customer complaints, and protects your brand reputation. For quality-sensitive industries like pharmaceuticals and food processing, this reliability proves invaluable. Operational cost reduction stands out as a primary benefit of the best genius optical sorter. By automating repetitive sorting tasks, you reduce labor expenses while improving worker safety by removing employees from hazardous environments. Maintenance requirements remain minimal thanks to robust engineering and durable components designed for continuous operation. Environmental benefits make the best genius optical sorter an eco-conscious choice. Enhanced sorting accuracy maximizes material recovery rates in recycling operations, diverting substantial waste from landfills. Improved sorting efficiency reduces energy consumption compared to manual alternatives, supporting your sustainability initiatives. Flexibility and customization options distinguish the best genius optical sorter from competitors. The system adapts to various material types, sizes, and sorting criteria through simple software adjustments. This adaptability means your investment serves multiple applications, protecting your capital investment across changing business needs and market conditions.

Practical Tips

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

best genius optical sorter

Advanced AI-Powered Recognition Technology

Advanced AI-Powered Recognition Technology

The best genius optical sorter incorporates artificial intelligence that learns and adapts to changing material characteristics and sorting requirements. Using machine vision and spectroscopic analysis, the system identifies materials with unprecedented accuracy, detecting minute variations invisible to human operators. This AI technology continuously improves performance through adaptive algorithms that analyze sorting outcomes and refine detection parameters. The best genius optical sorter's recognition capabilities extend across hundreds of material classifications, making it suitable for diverse industrial applications. Whether sorting recycled plastics by resin type, identifying contaminants in grain shipments, or separating ore minerals, the system delivers consistent, reliable results. This intelligent approach eliminates the need for frequent manual recalibration, reducing downtime and maintenance costs while ensuring your sorting operations remain optimized regardless of material variability or seasonal fluctuations.
Exceptional Speed and Processing Capacity

Exceptional Speed and Processing Capacity

The best genius optical sorter processes materials at extraordinary speeds, handling multiple tons per hour with minimal energy consumption. This exceptional throughput capacity allows facilities to dramatically increase productivity without expanding physical infrastructure or multiplying operational staff. The best genius optical sorter achieves rapid sorting through parallel processing of multiple detection streams and optimized ejection mechanisms that respond in milliseconds. For high-volume operations in recycling, mining, and food processing, this speed translates directly to increased revenue potential and improved return on investment. The system maintains accuracy even at maximum processing speeds, ensuring quality never suffers despite accelerated operations. Facilities implementing the best genius optical sorter report productivity improvements ranging from 200 to 400 percent, fundamentally transforming operational economics and competitive positioning within their respective markets.
Seamless Integration and User-Friendly Operation

Seamless Integration and User-Friendly Operation

The best genius optical sorter installs into existing production lines without requiring extensive facility modifications or production interruptions. Its modular design accommodates various material stream sizes and configurations, adapting to your specific operational needs. The intuitive software interface enables operators to adjust sorting parameters, monitor system performance, and generate comprehensive reports using simple menu-driven commands. Training requirements remain minimal since the best genius optical sorter's controls prioritize usability and accessibility. The system provides real-time feedback and diagnostic information, allowing quick identification and resolution of any operational issues. Remote monitoring capabilities enable technical support teams to assess performance and troubleshoot problems without on-site visits, minimizing downtime and maintenance costs. This user-centric design philosophy makes the best genius optical sorter accessible to facilities of all sizes and technical expertise levels.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy