unique colour sorter
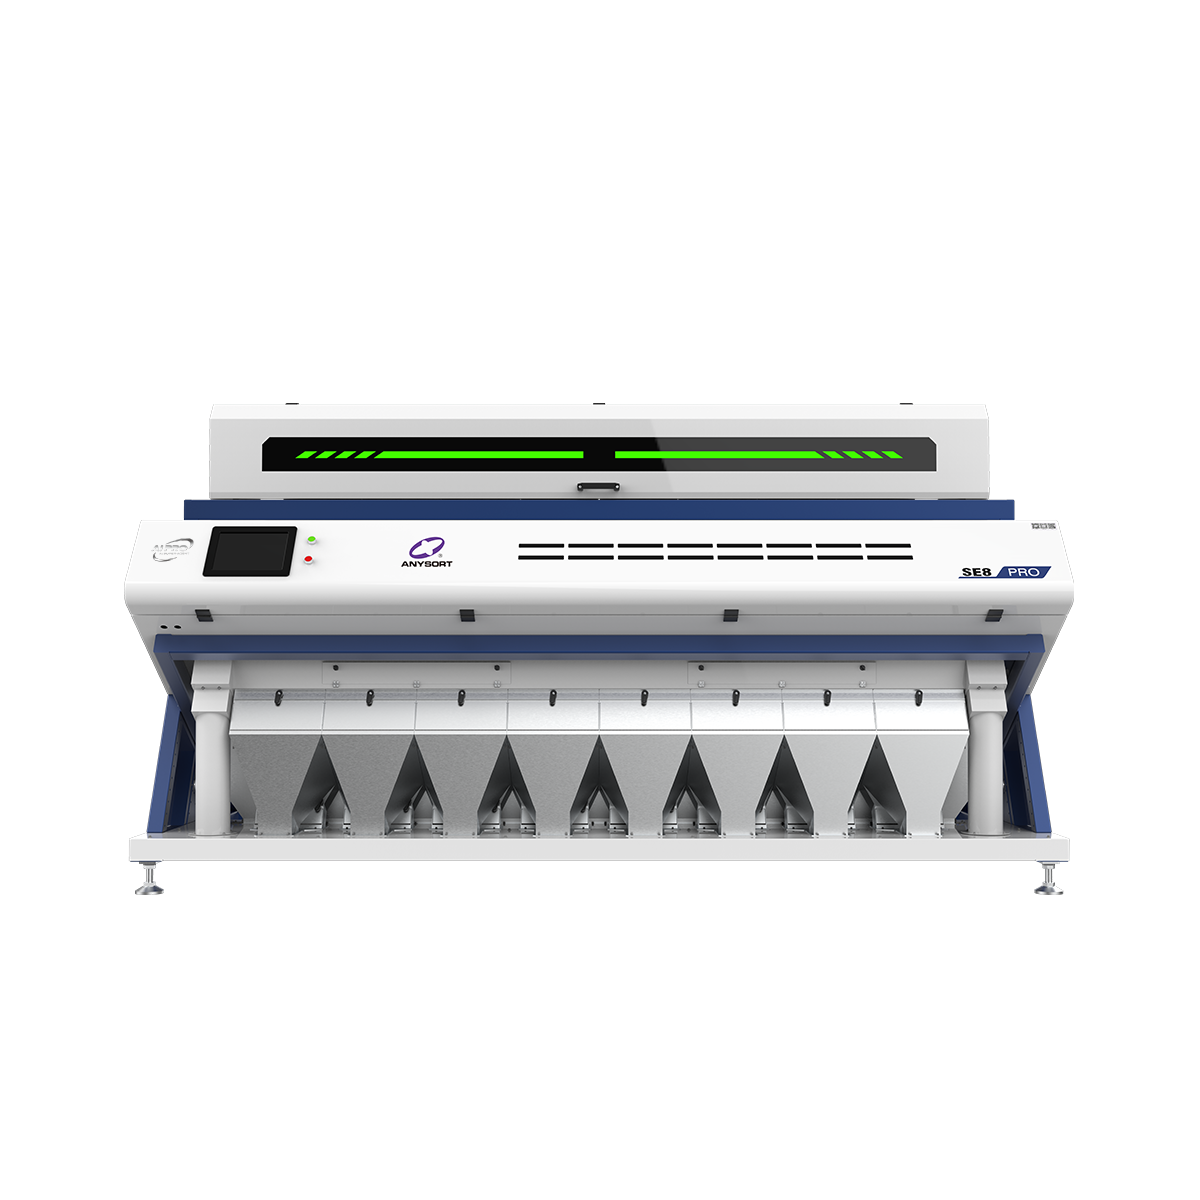
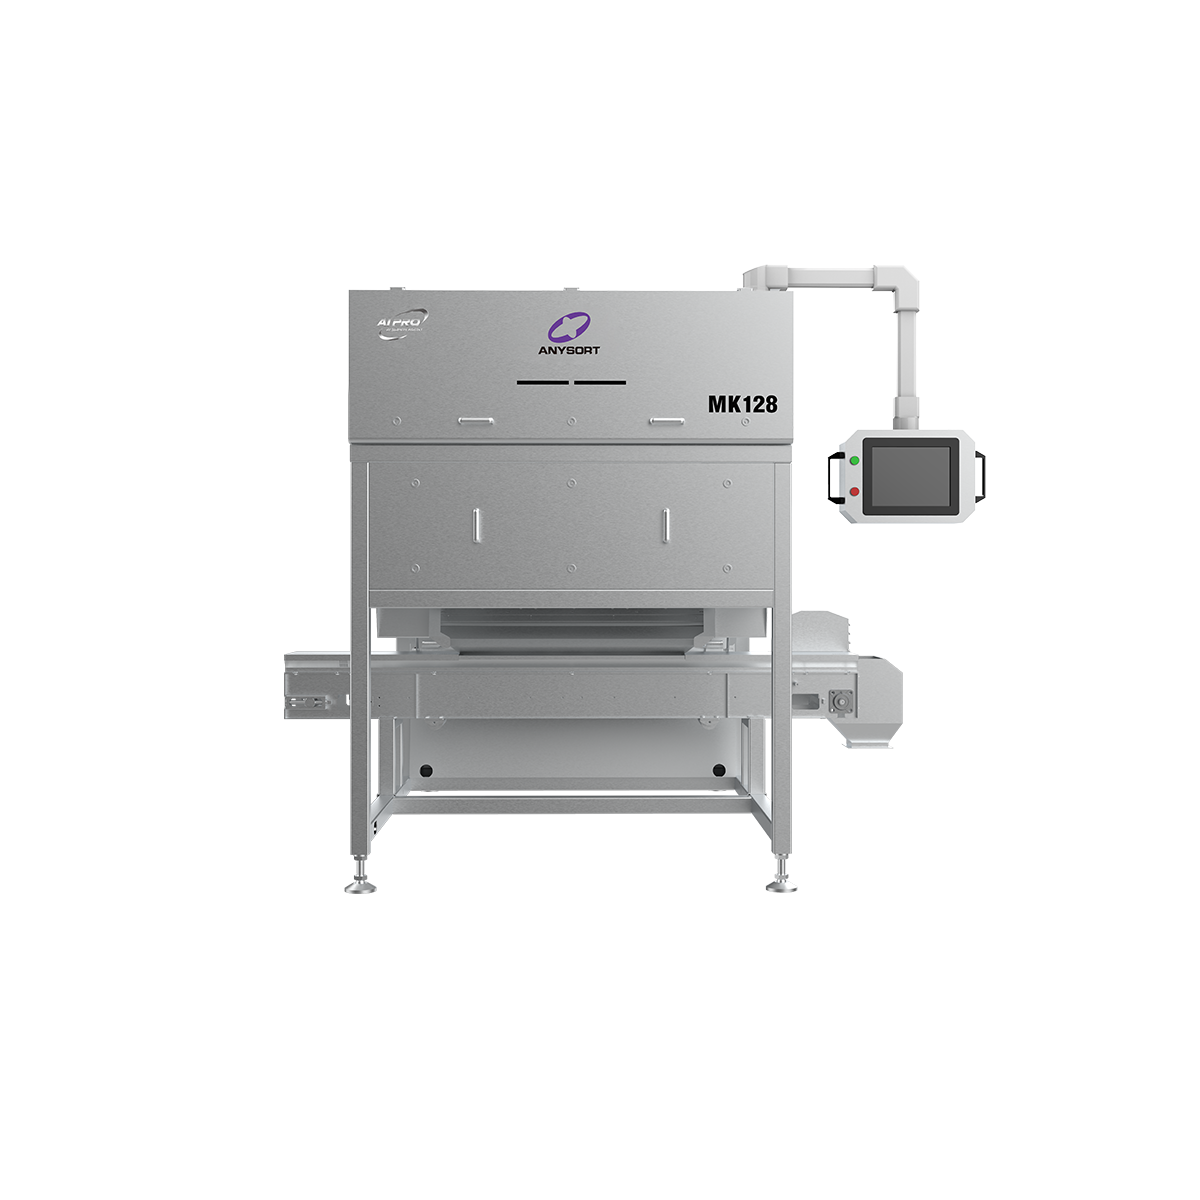
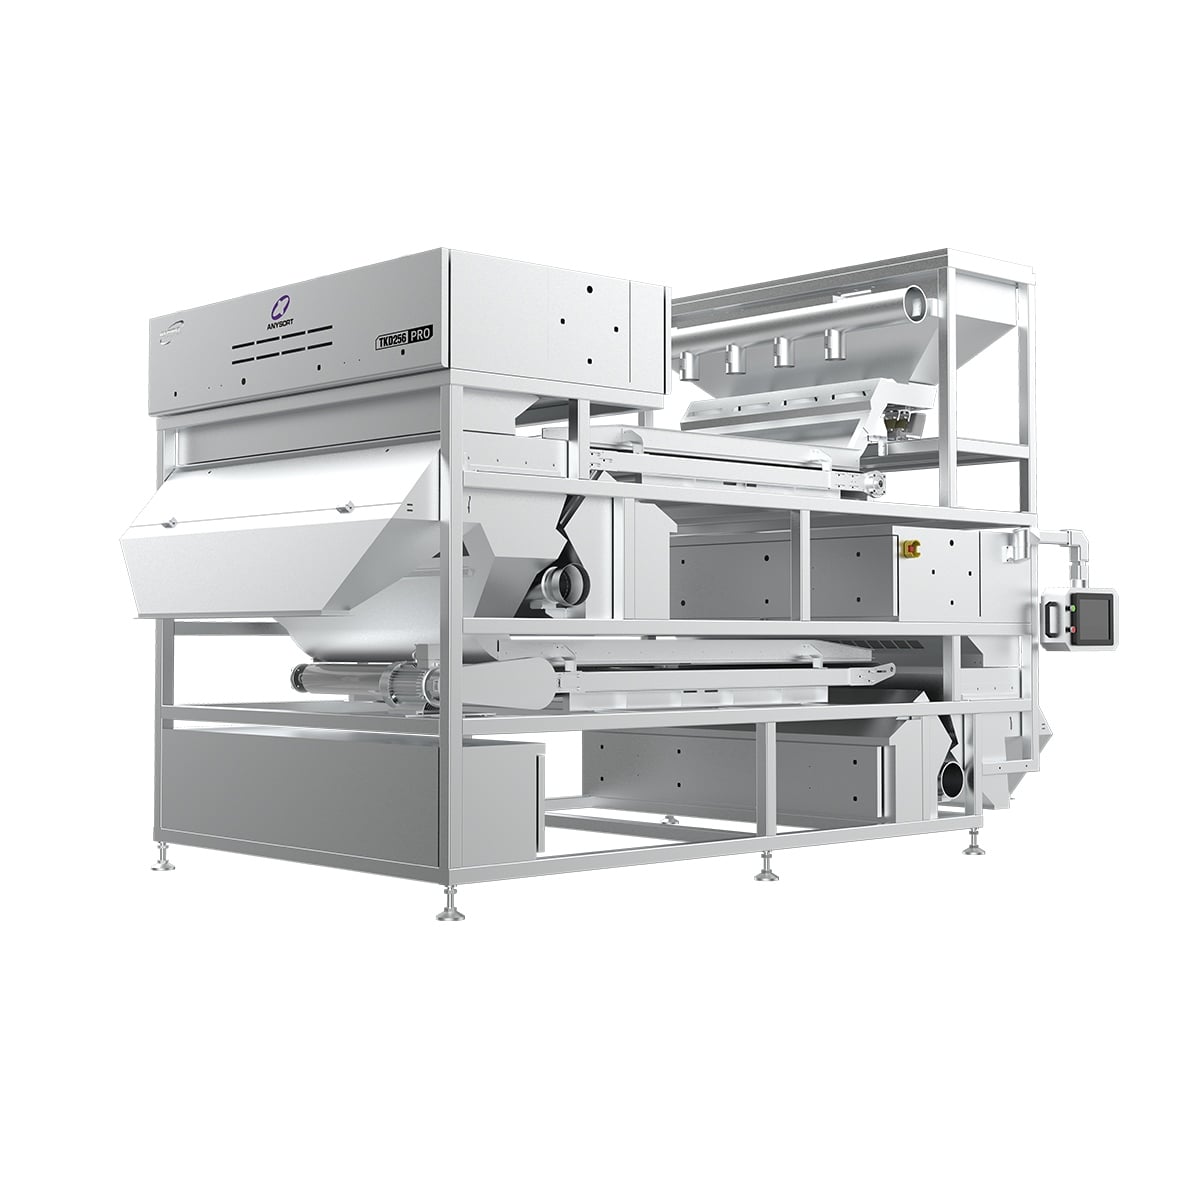
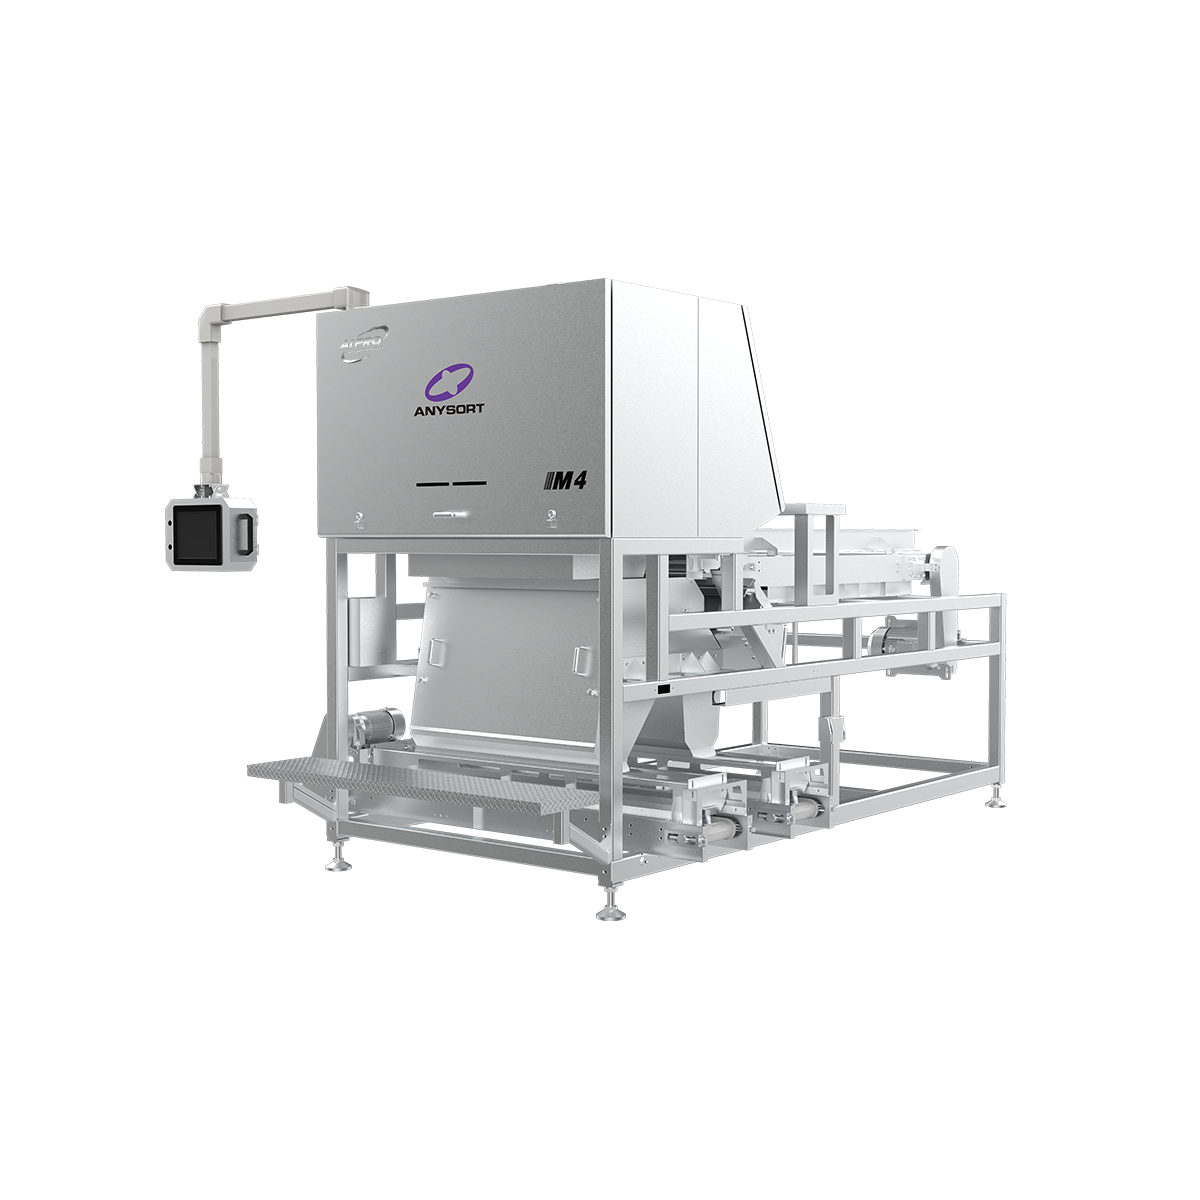
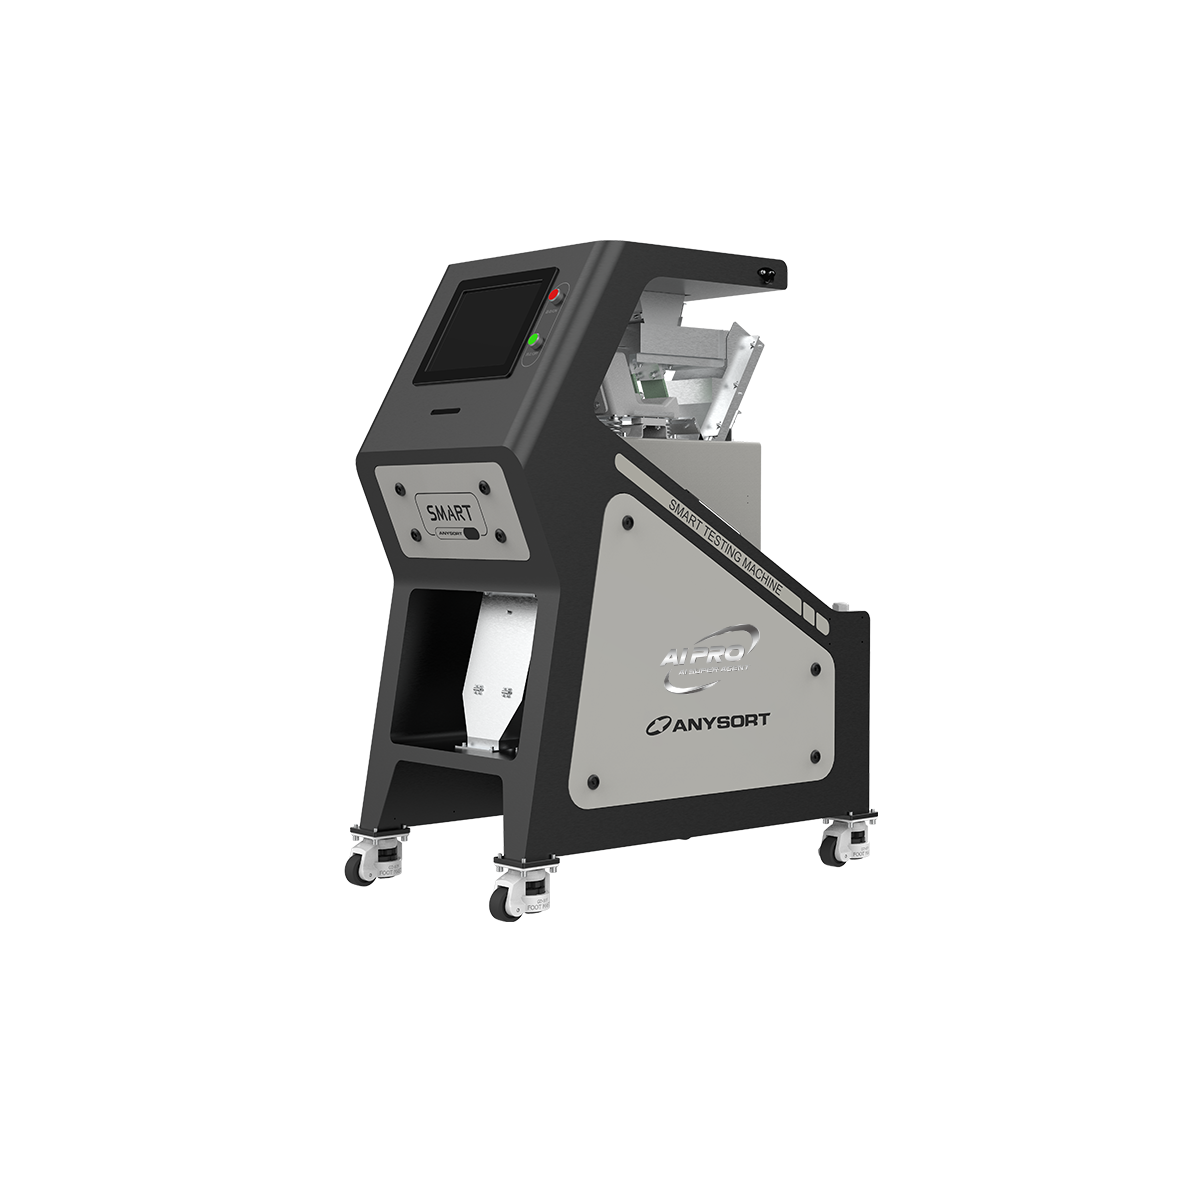
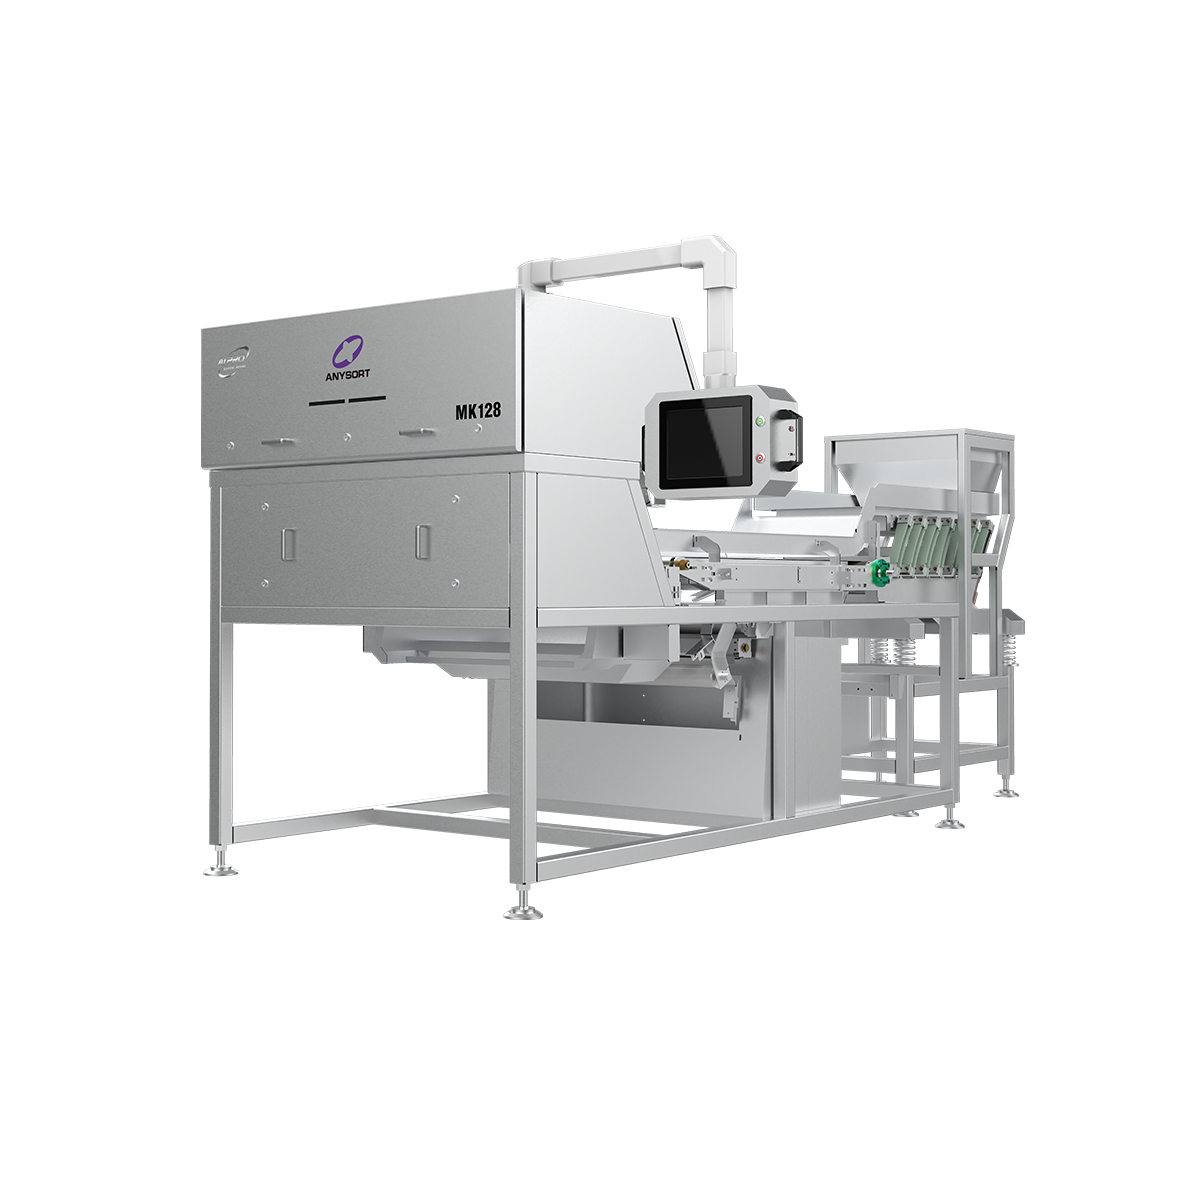
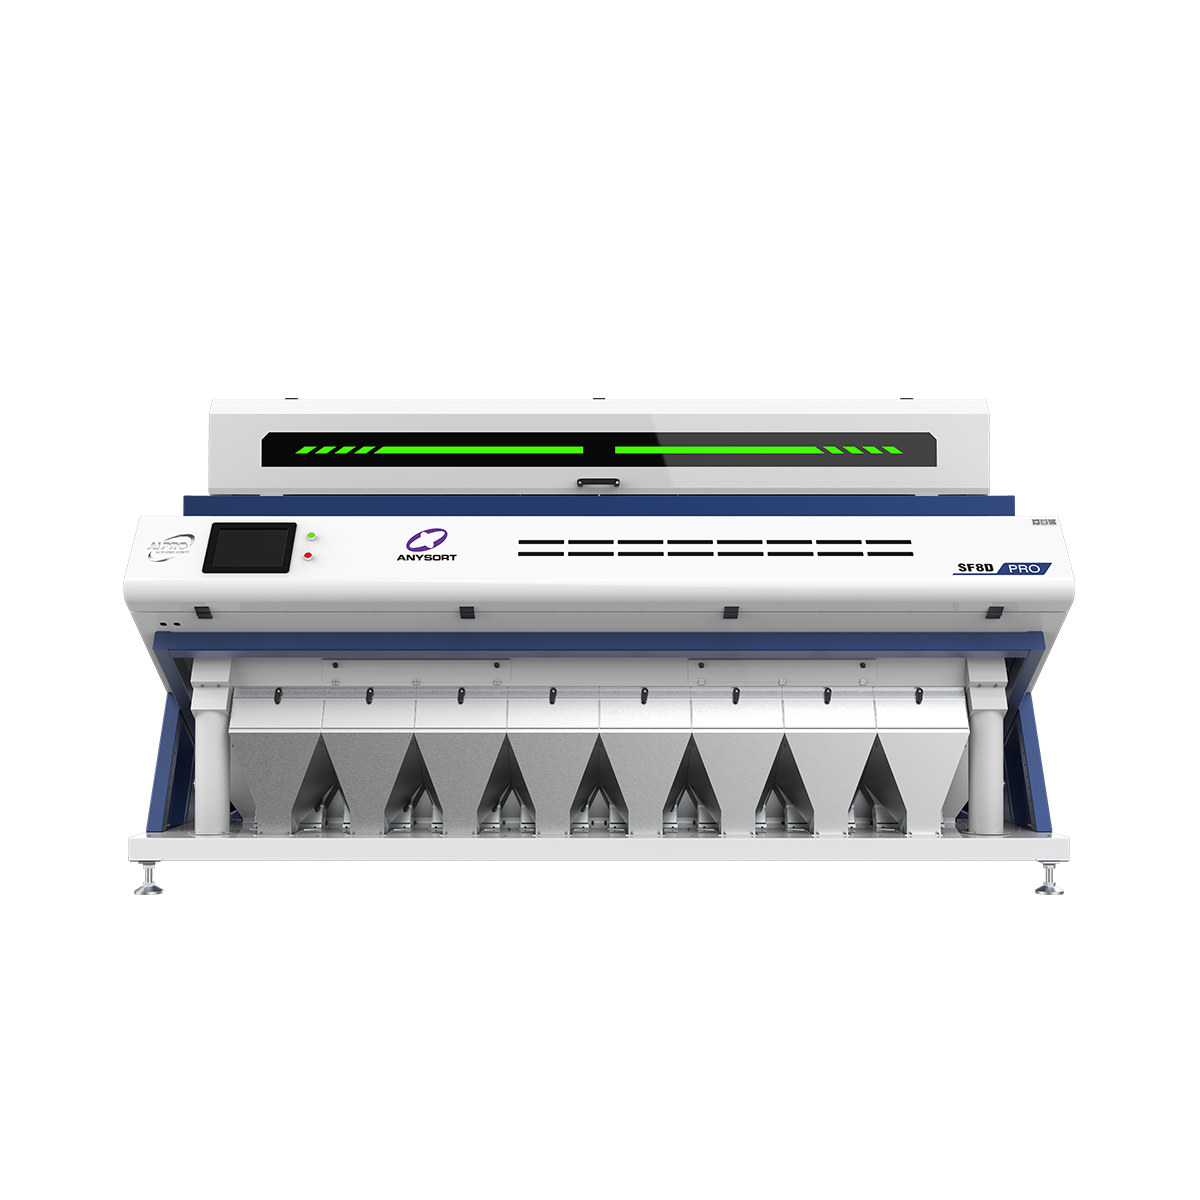
A unique colour sorter represents an advanced optical sorting technology designed to automatically separate and classify materials based on their colour properties. This innovative machine utilizes high-precision cameras, sophisticated lighting systems, and intelligent processing algorithms to identify and sort items with remarkable accuracy. The unique colour sorter operates by capturing detailed colour information from each object as it moves through the sorting chamber, then directing materials to designated collection bins through pneumatic ejection systems.
The technological foundation of a unique colour sorter includes multispectral imaging capabilities that can detect subtle colour variations imperceptible to the human eye. Advanced machine learning algorithms enable the system to continuously improve sorting accuracy while maintaining consistent performance across diverse material types. The unique colour sorter finds extensive applications in food processing, recycling facilities, mineral extraction, and agricultural industries.
In food production, the unique colour sorter efficiently removes discoloured or defective items from grains, nuts, seeds, and dried fruits. Within recycling operations, this technology sorts plastic, glass, and metal materials by colour, significantly enhancing processing efficiency. The unique colour sorter's ability to process hundreds of items per second makes it invaluable for high-volume operations requiring consistent quality control and material separation standards.

 EN