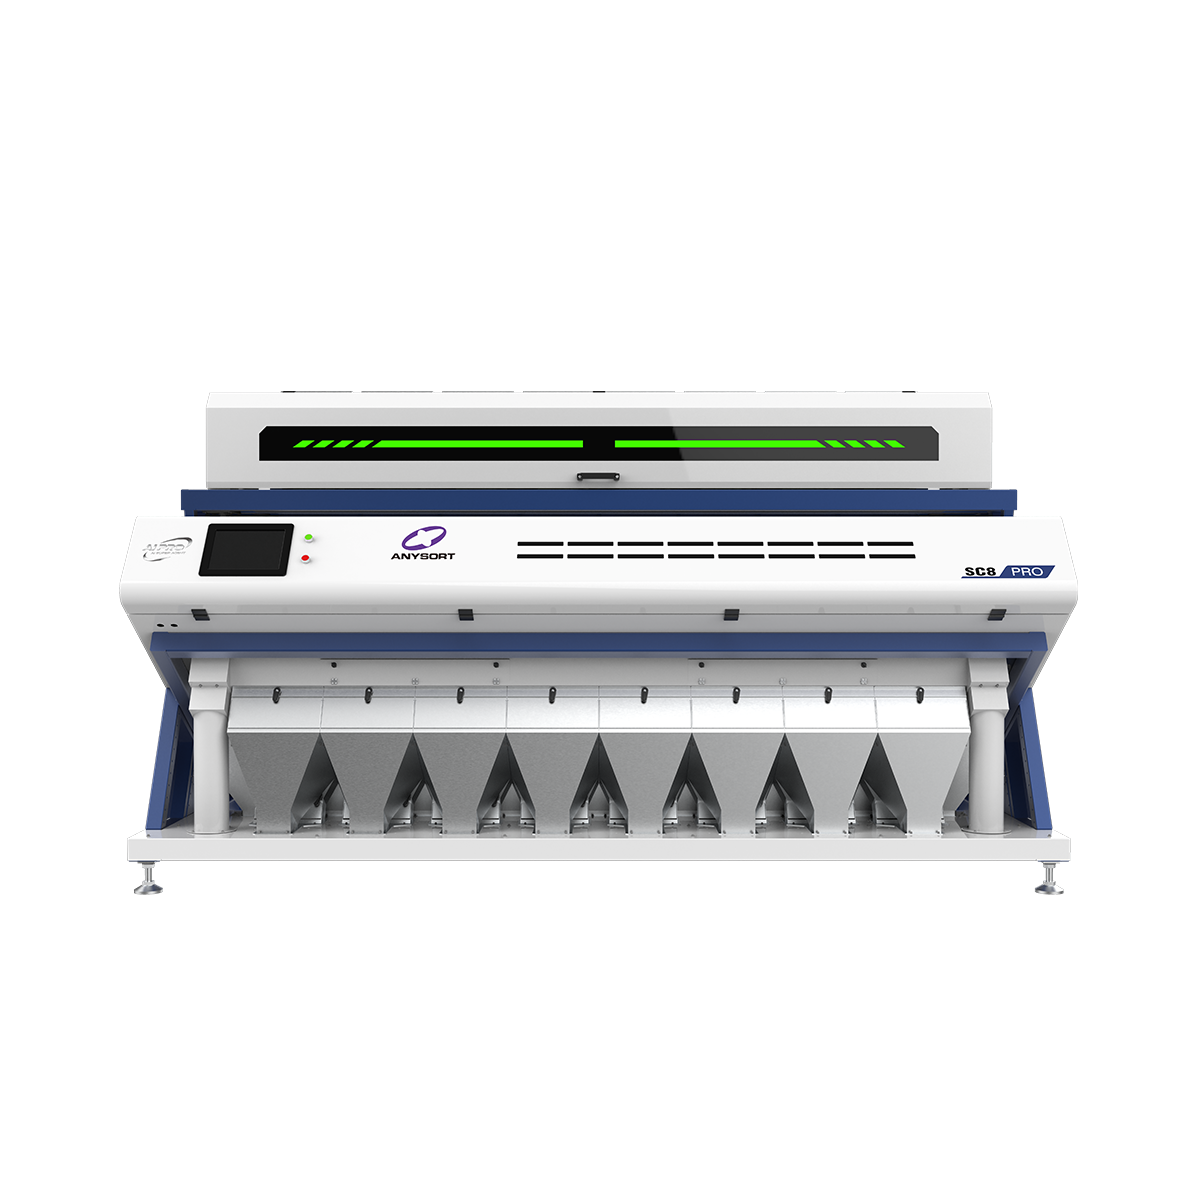
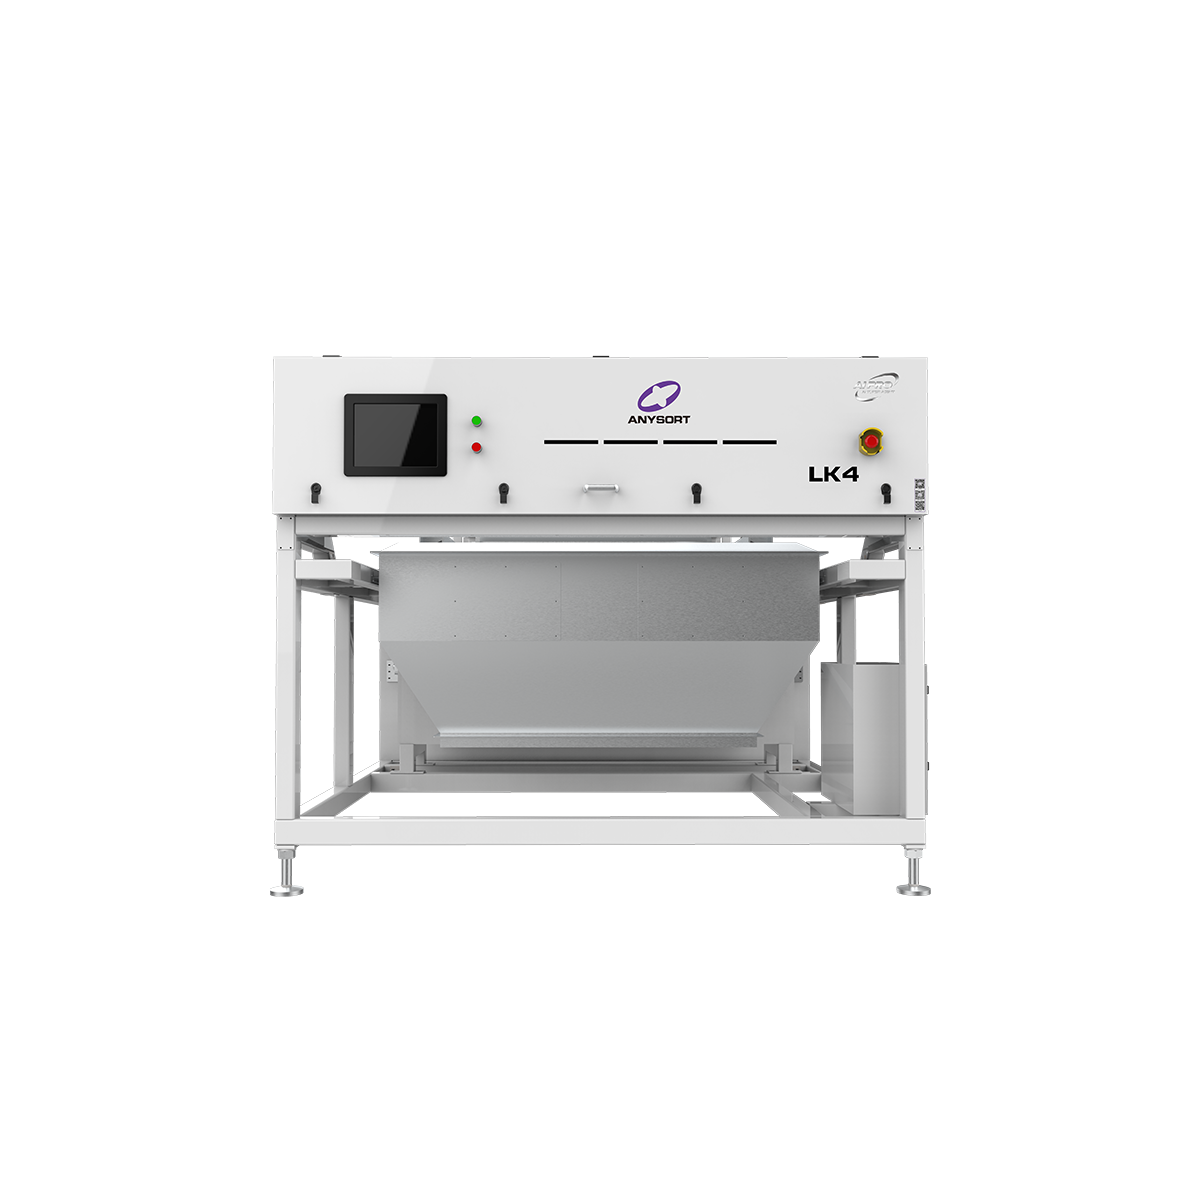
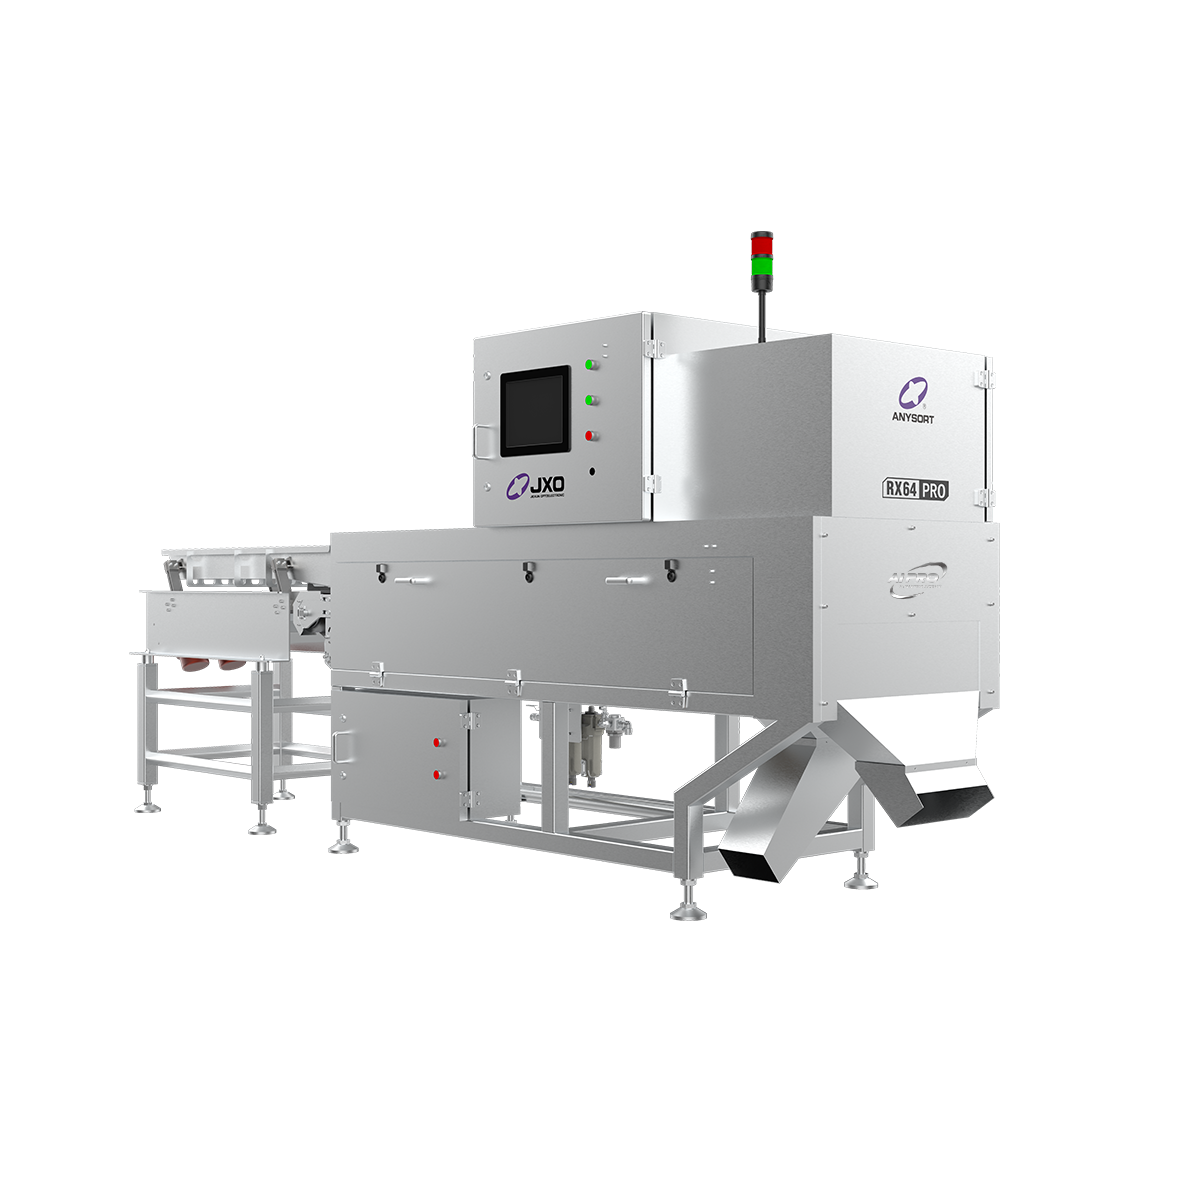
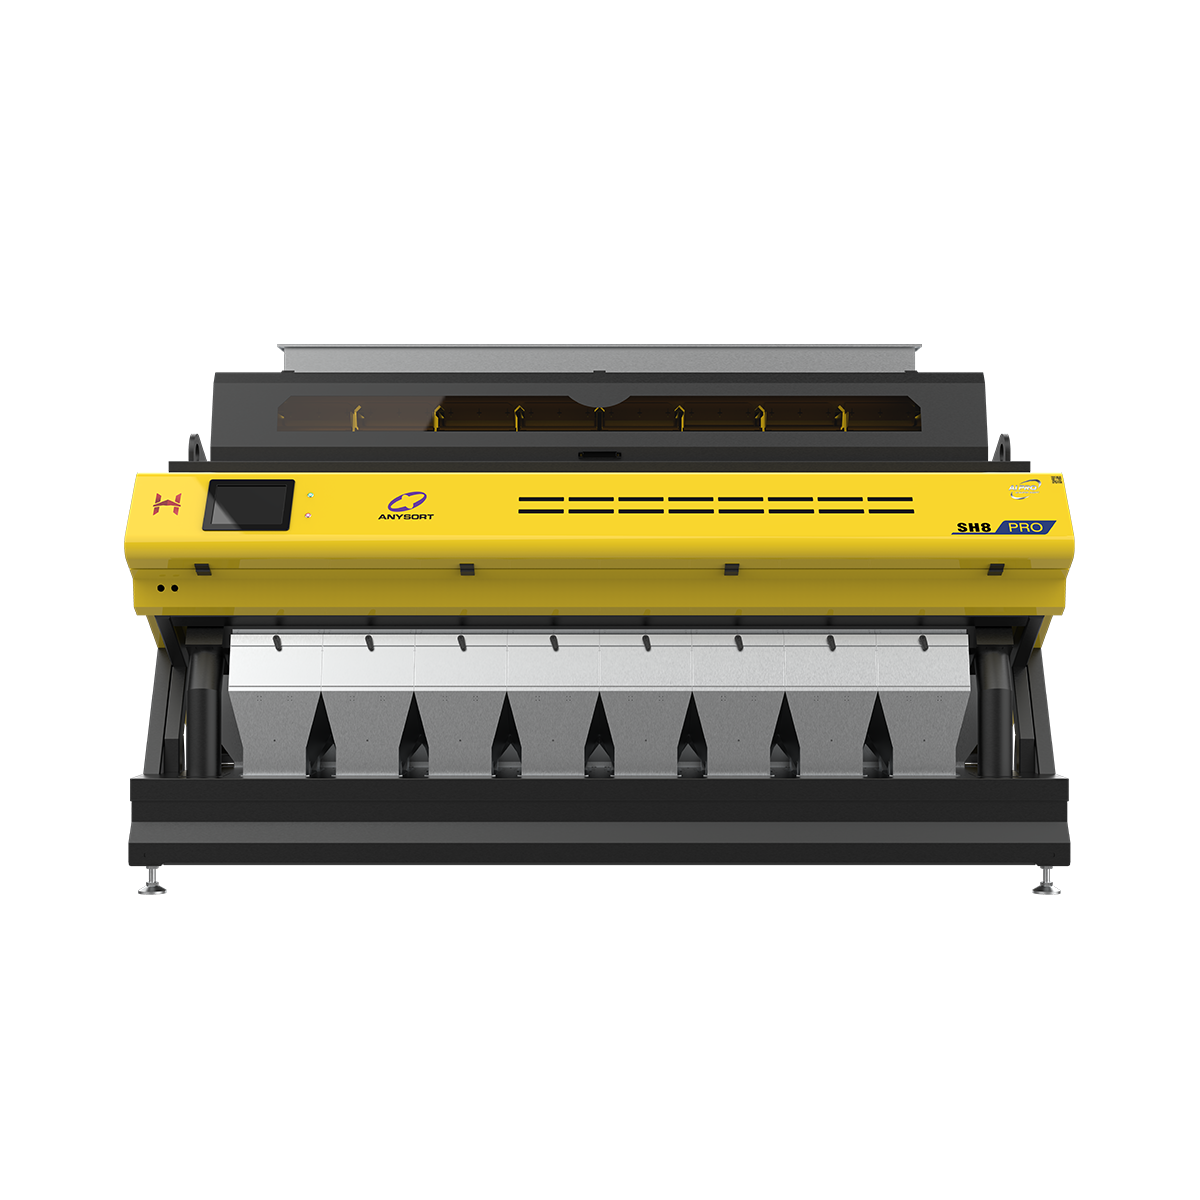
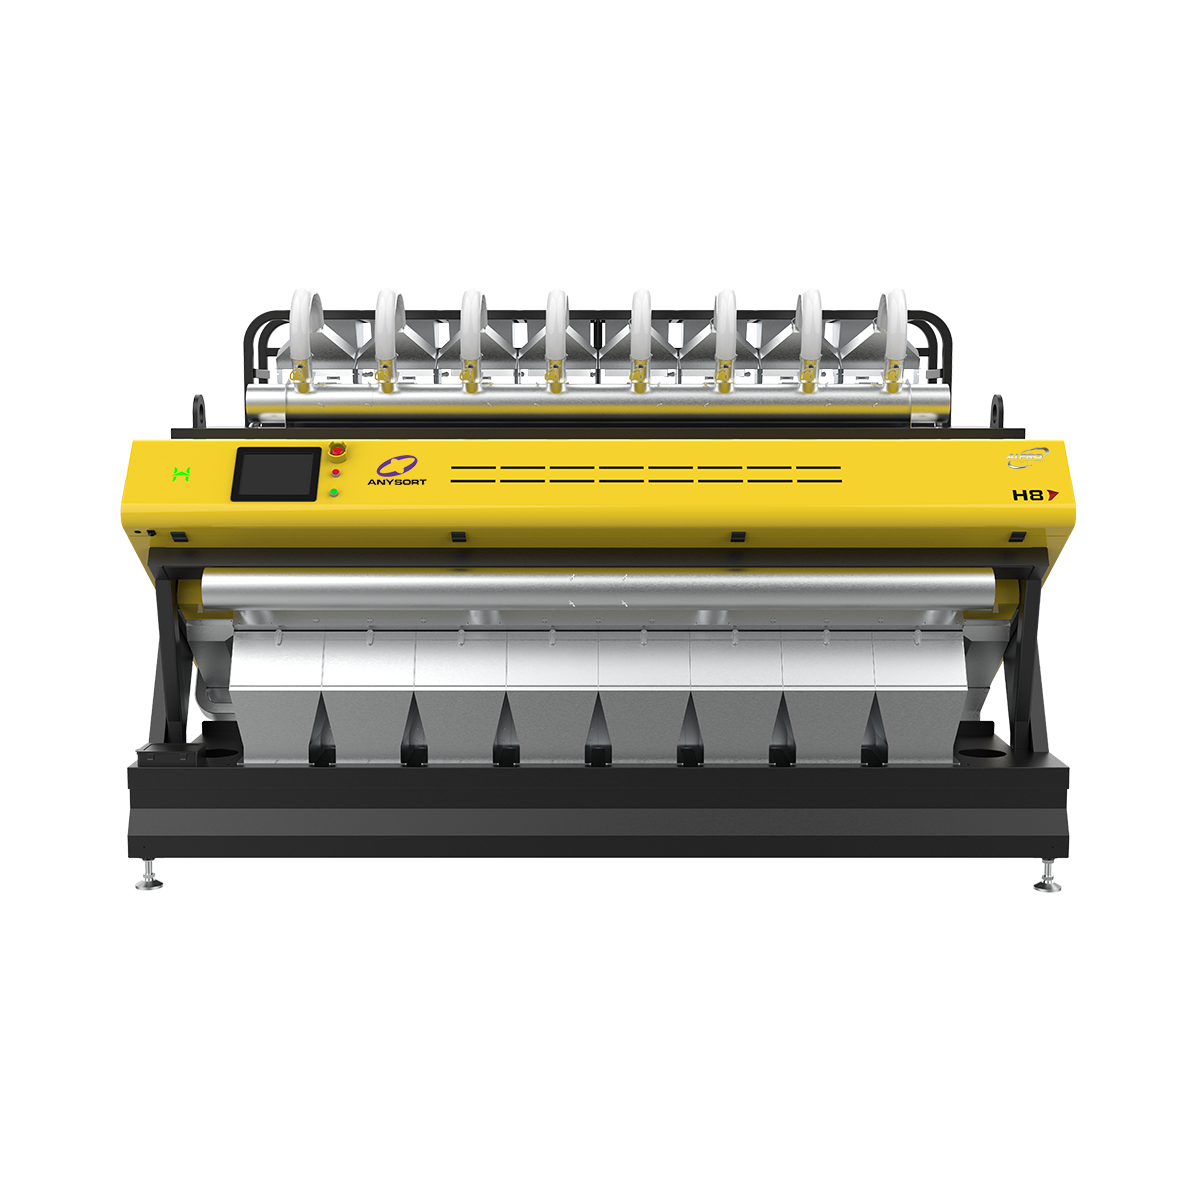
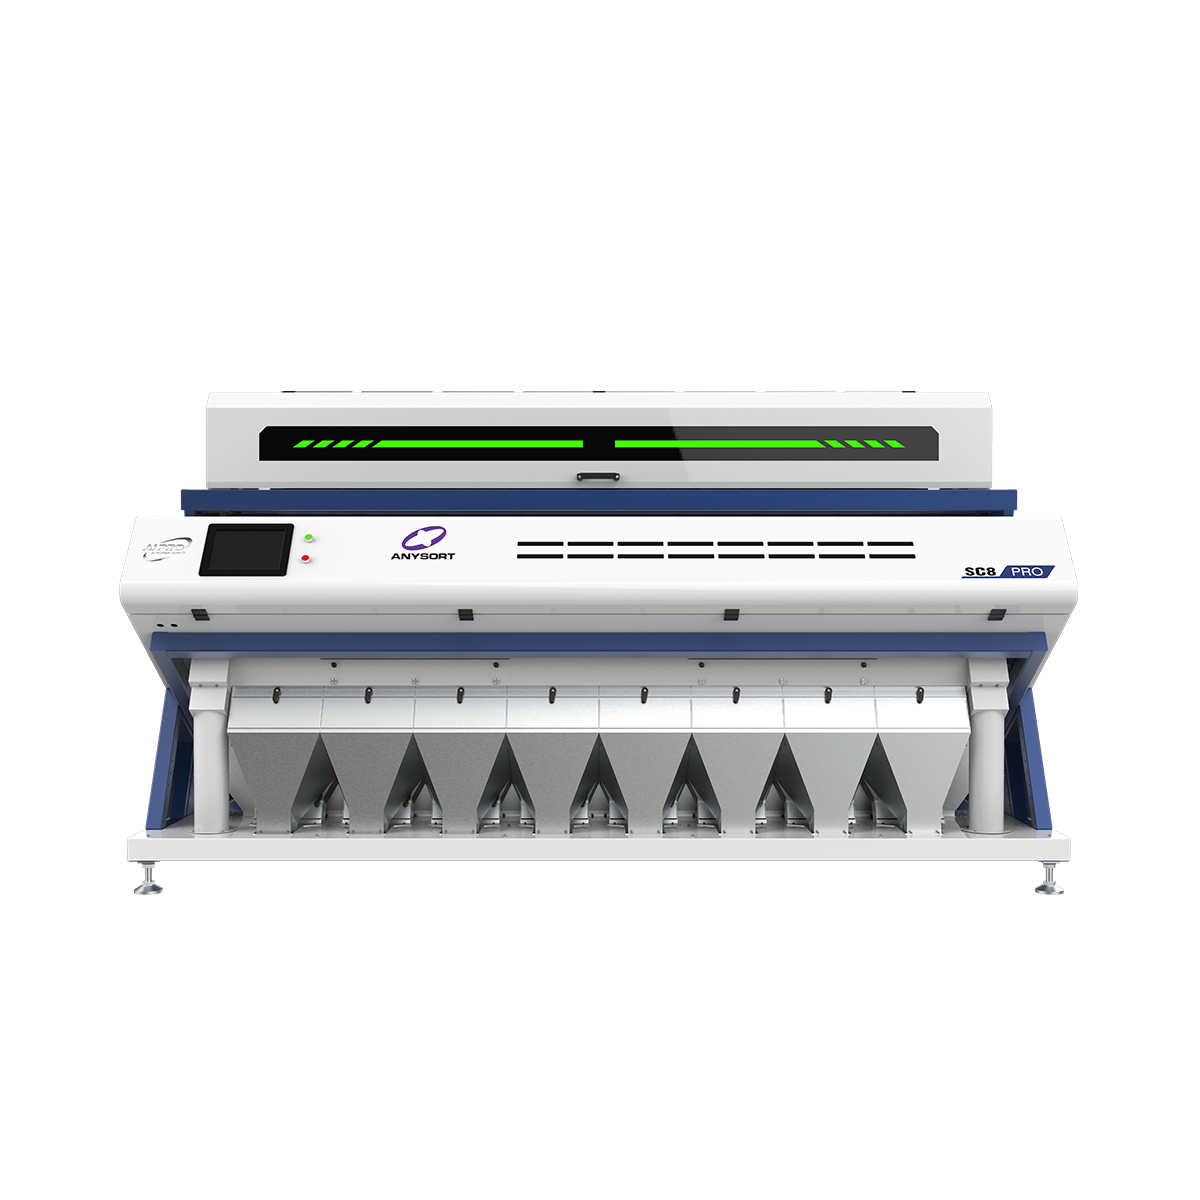
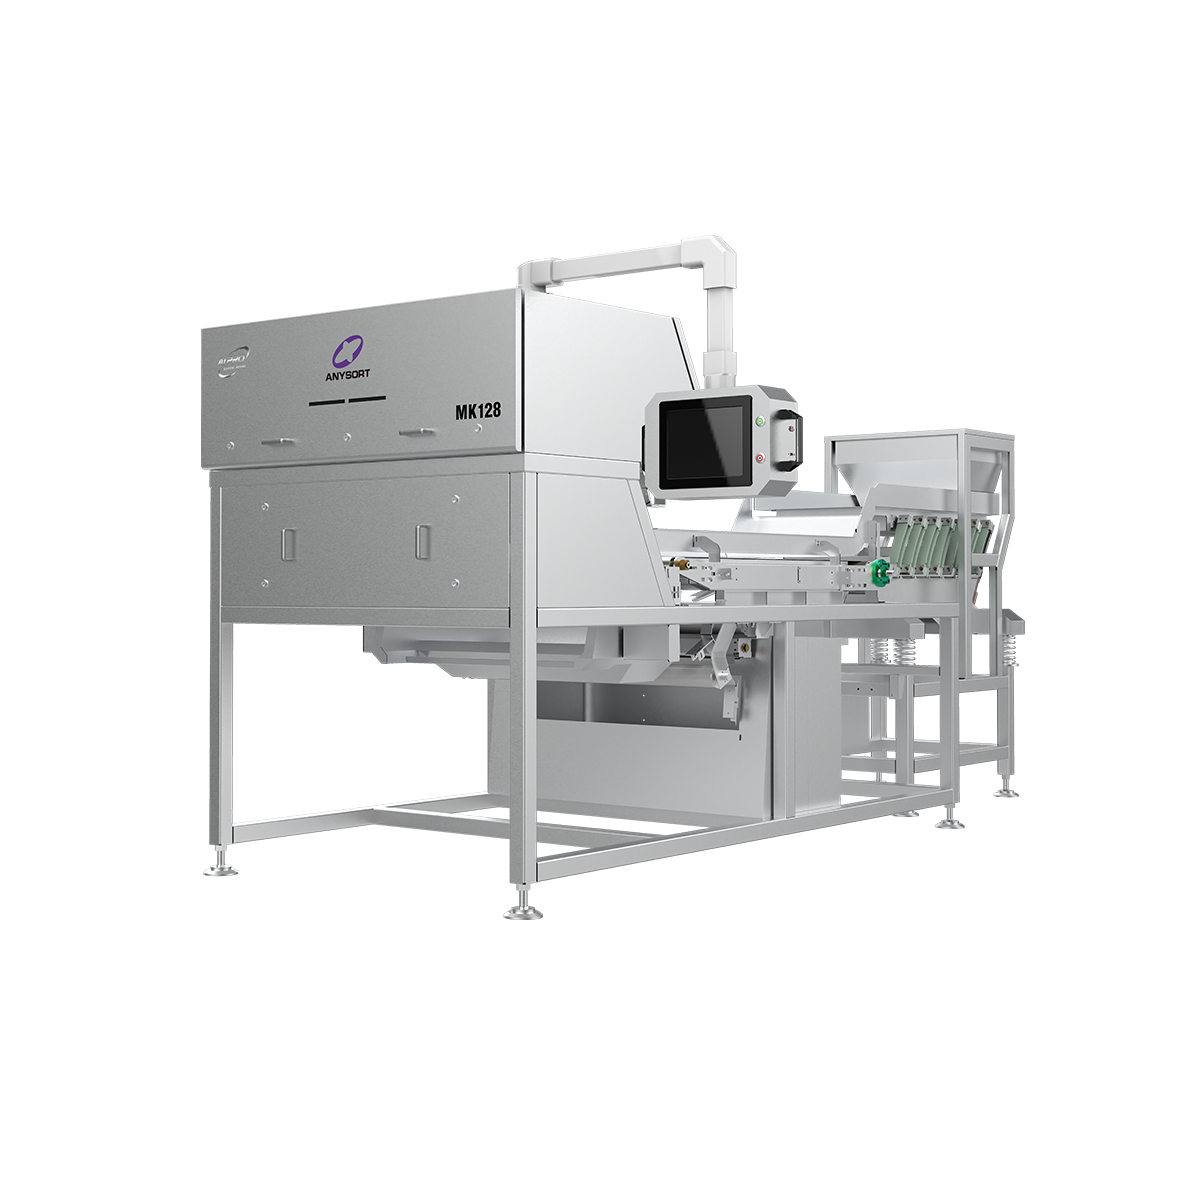
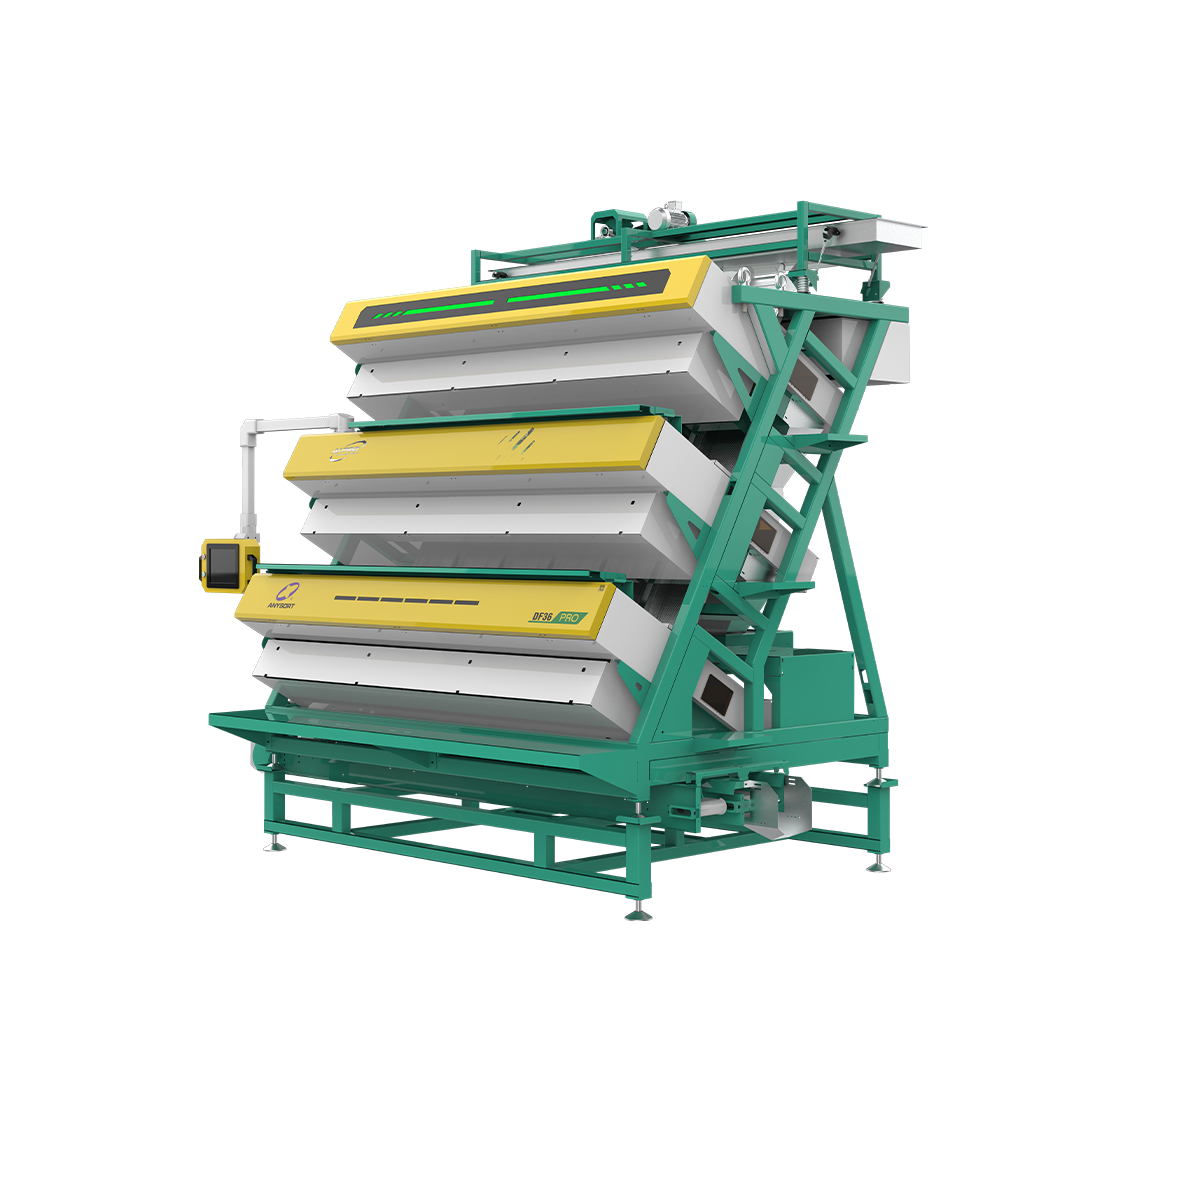
color sorter machine factory
A color sorter machine factory specializes in designing and manufacturing advanced sorting equipment that automatically separates materials based on color properties. These sophisticated systems represent a significant technological advancement in quality control and material processing across multiple industries. The color sorter machine factory produces machines equipped with high-resolution optical sensors and artificial intelligence technology to detect even the slightest color variations. These machines work by capturing detailed images of passing materials at remarkable speeds, then using machine learning algorithms to classify items with exceptional accuracy. The primary function of equipment from a color sorter machine factory is to eliminate defective, discolored, or contaminated materials from production streams, ensuring only premium-quality products reach consumers. Modern color sorter machine factory operations integrate LED lighting systems, high-speed cameras, and pneumatic ejection mechanisms to achieve sorting rates exceeding hundreds of pieces per minute. Industries including food processing, agricultural production, recycling facilities, and pharmaceutical manufacturing depend heavily on color sorter machine factory solutions. The technology eliminates manual inspection, reducing labor costs while dramatically improving consistency and reliability. A color sorter machine factory combines precision engineering with practical automation solutions that address real-world production challenges, making these systems indispensable for companies pursuing operational excellence and product quality standards.

 EN