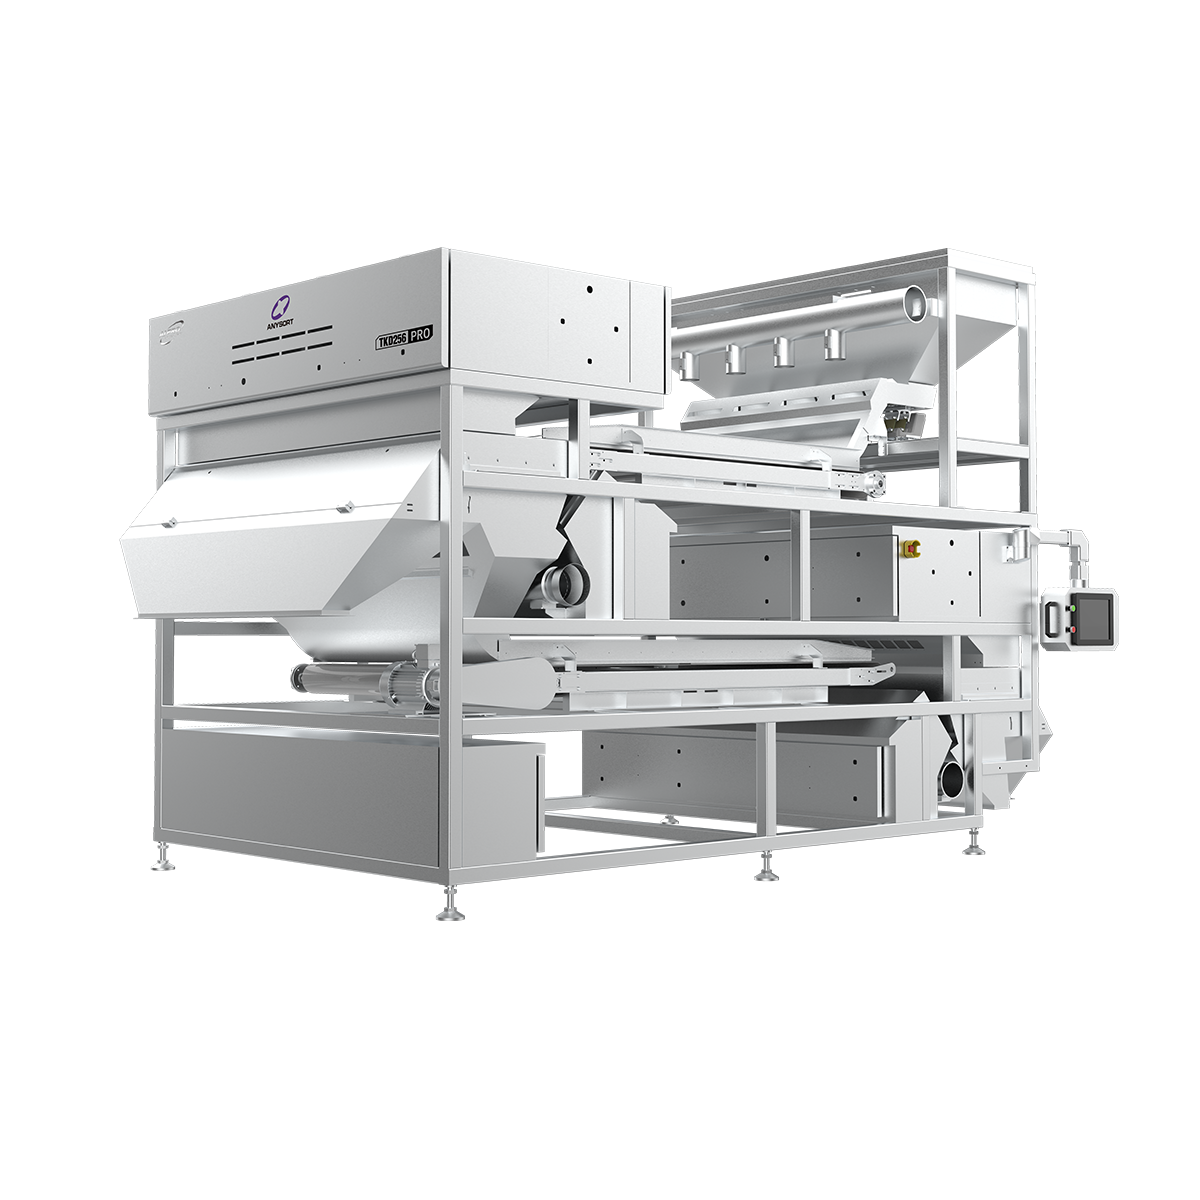
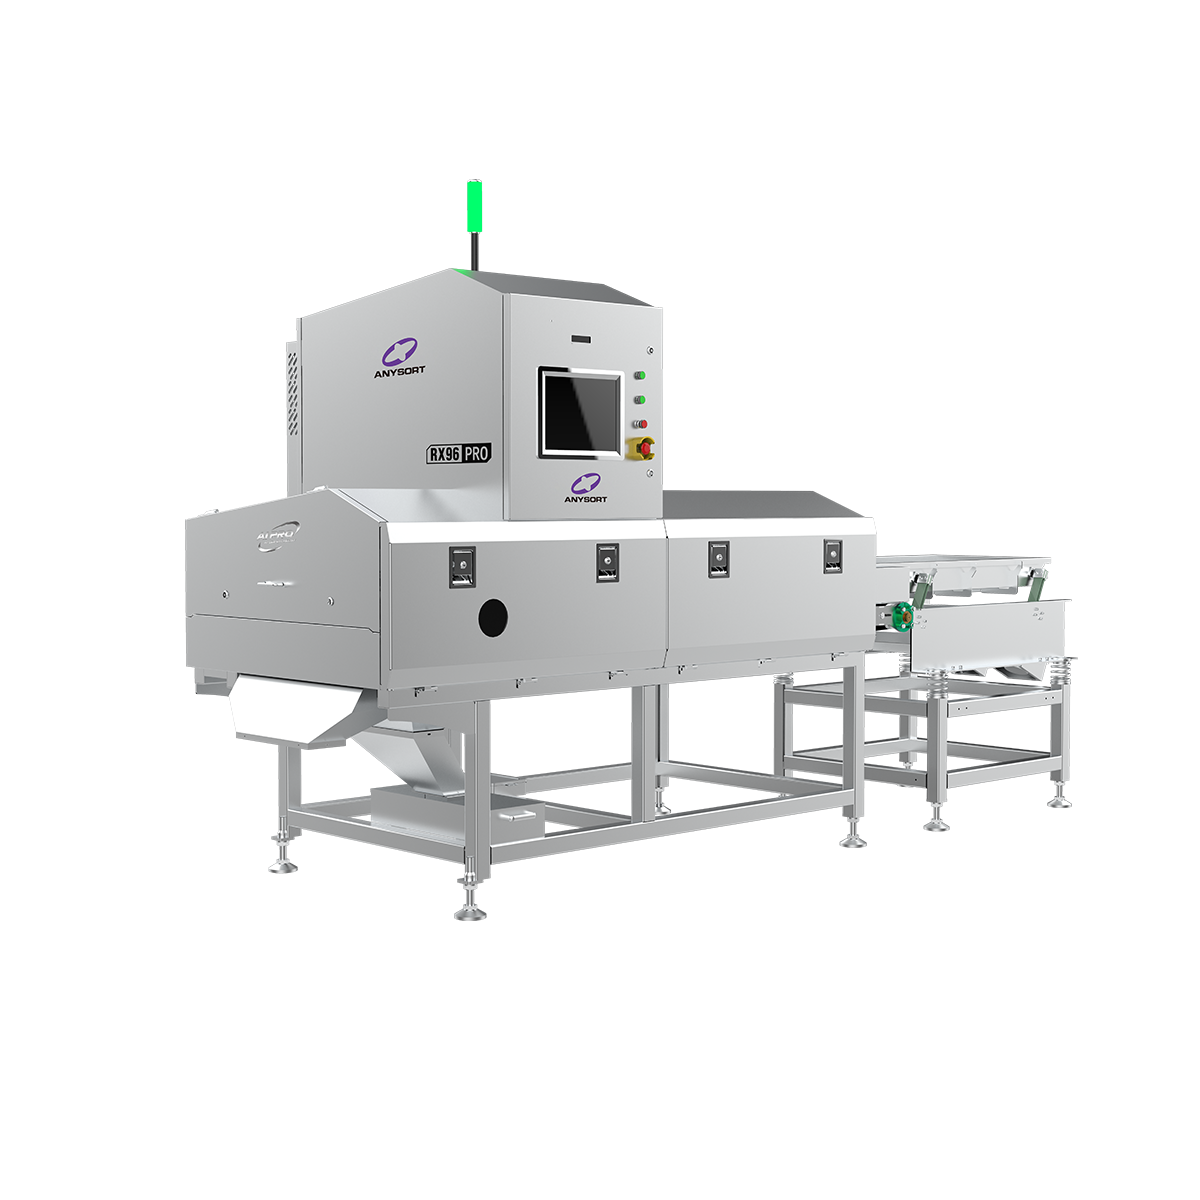
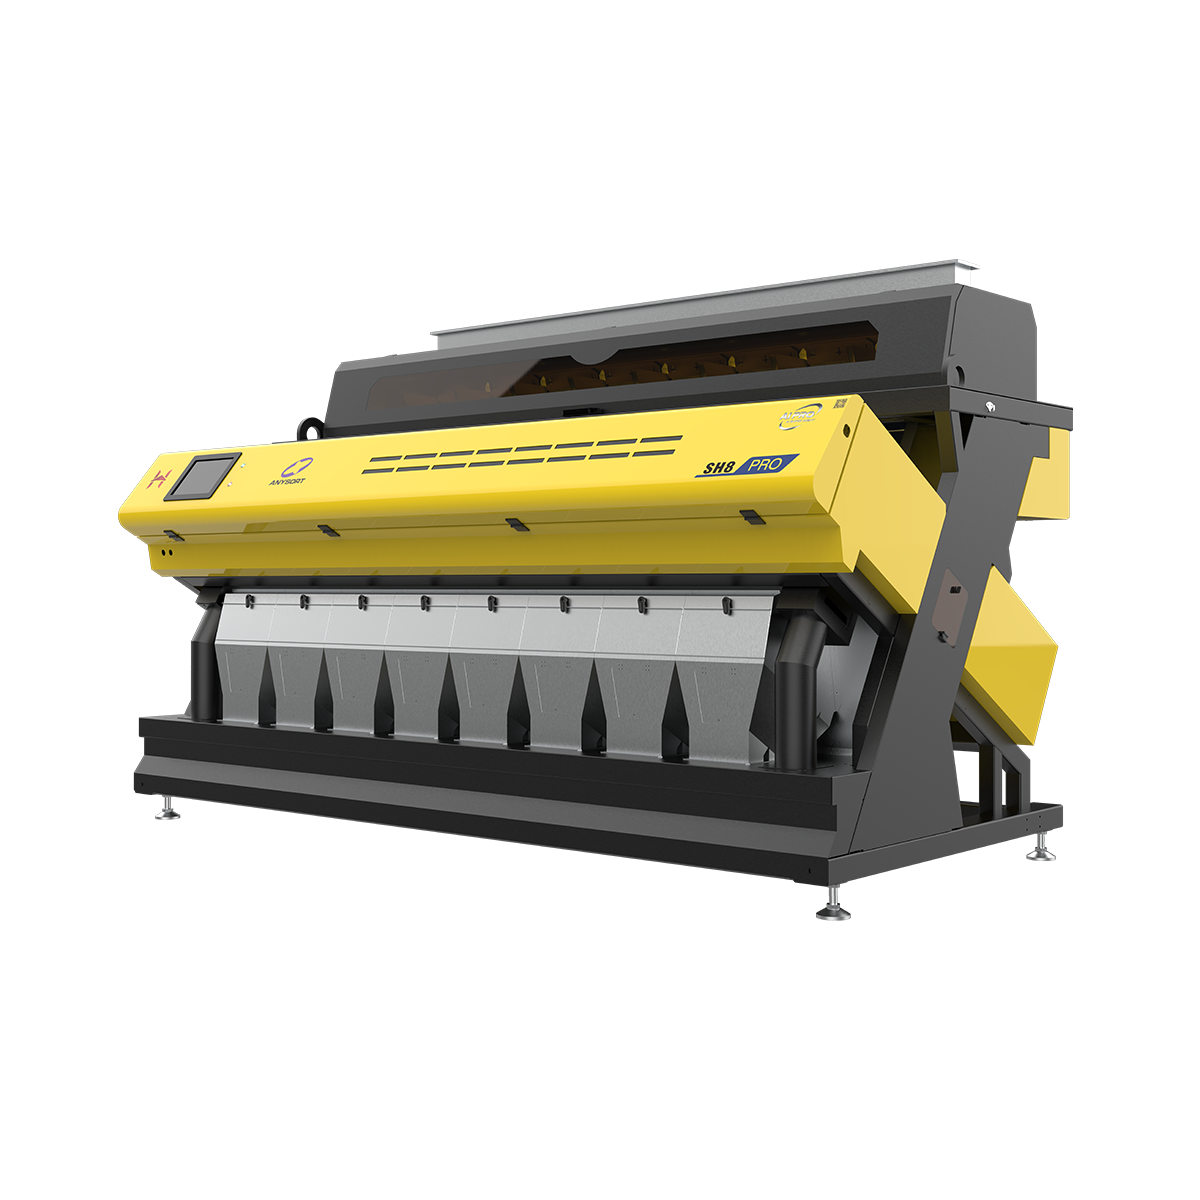
rice color sorter factory
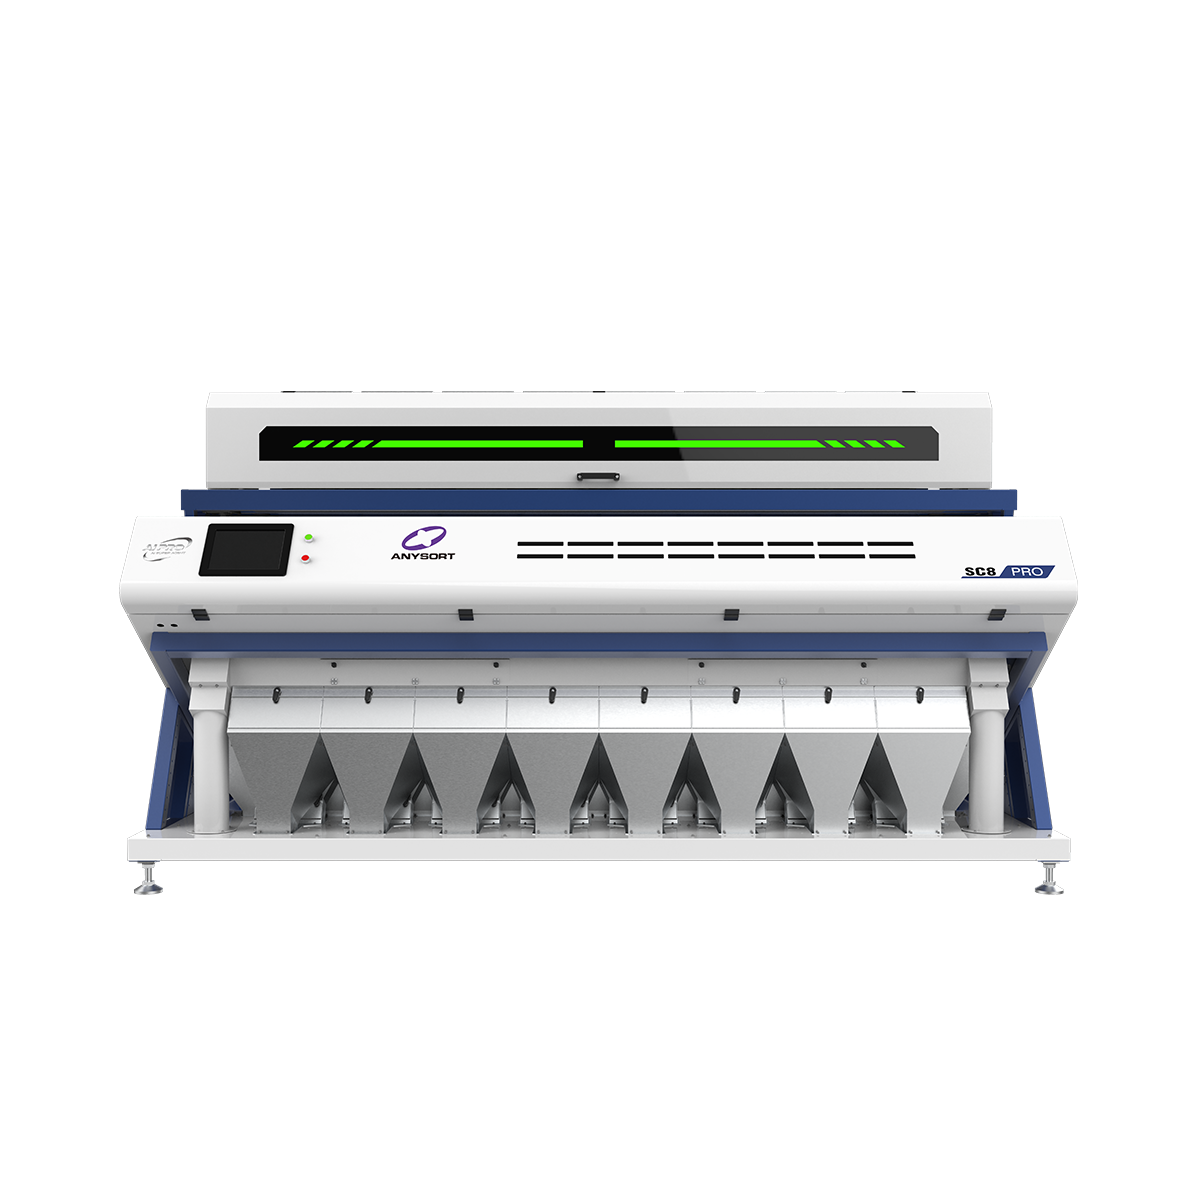
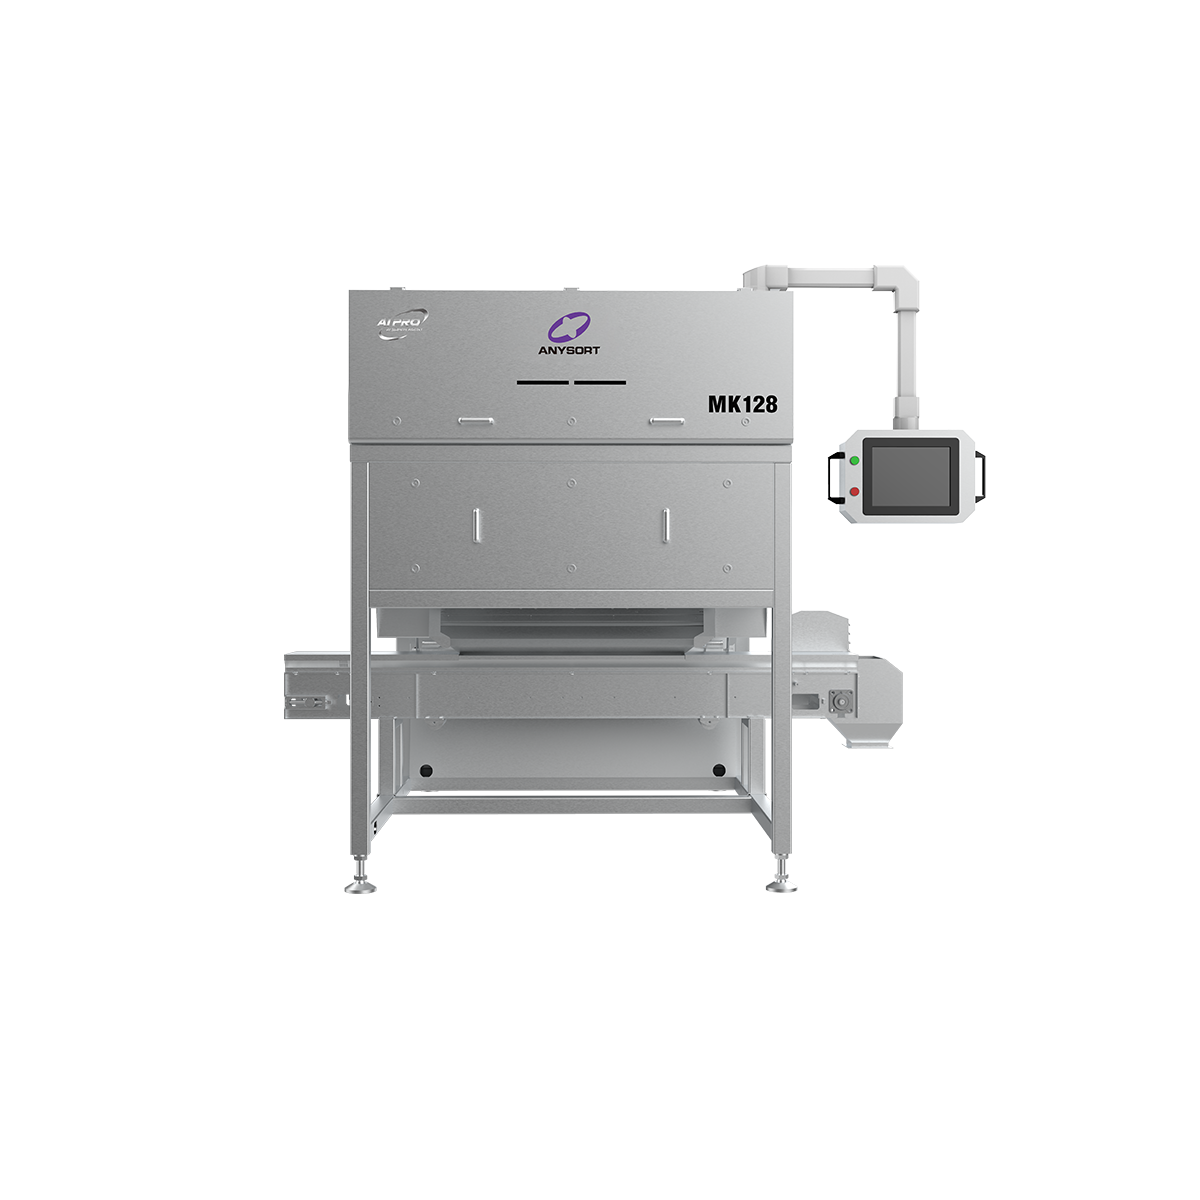
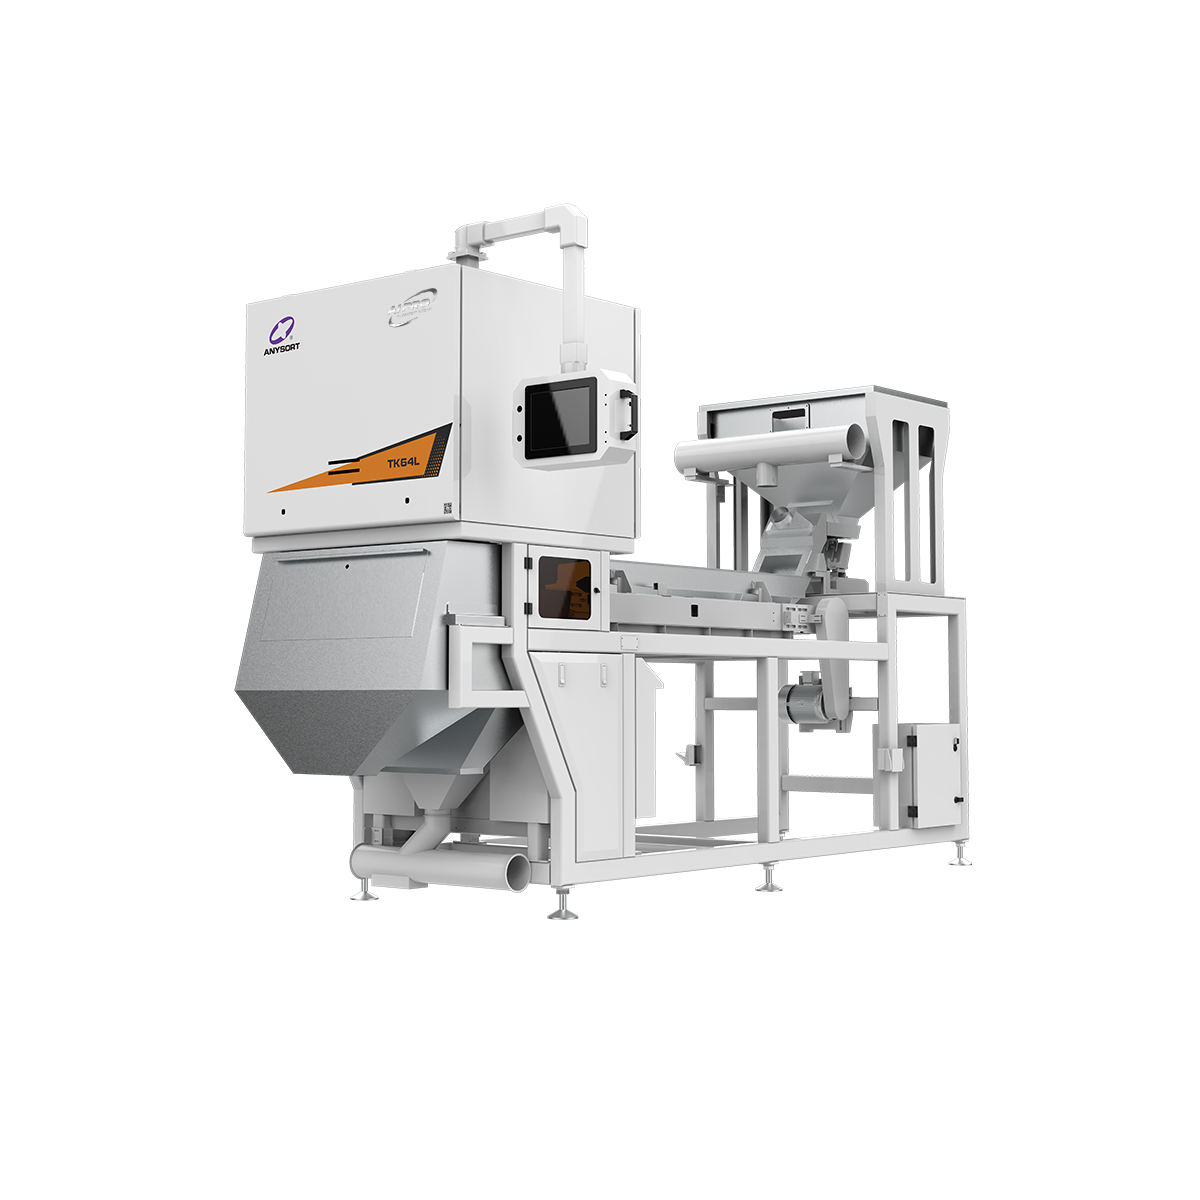
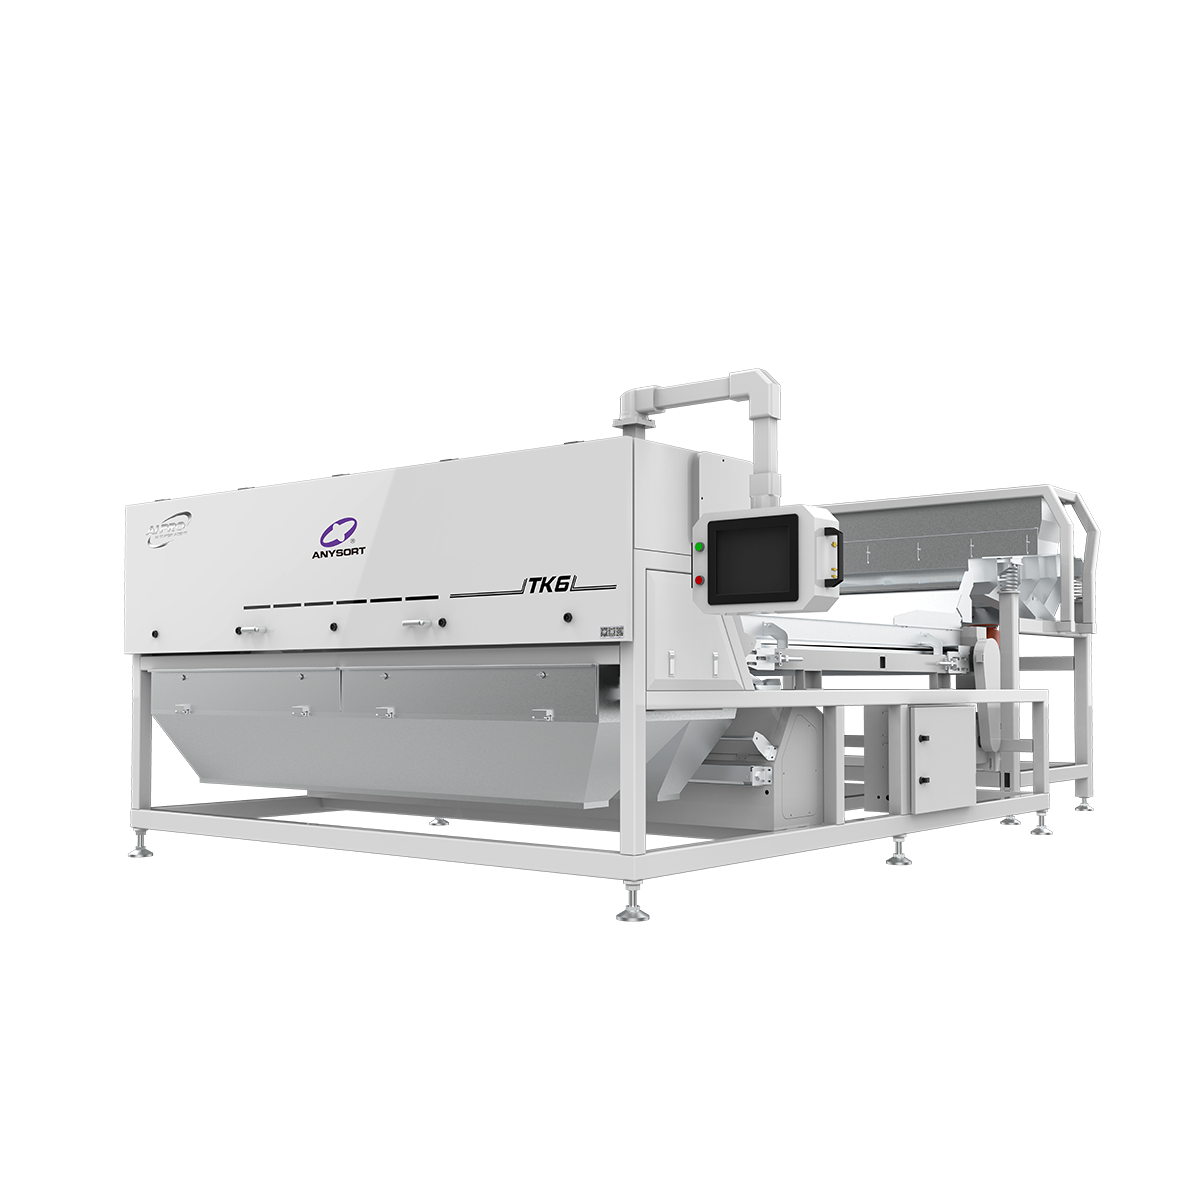
A rice color sorter factory represents a specialized manufacturing facility dedicated to producing advanced sorting equipment designed specifically for the rice processing industry. The rice color sorter factory utilizes cutting-edge optical scanning technology to detect and separate grains based on color variations, defects, and quality parameters. These facilities manufacture sophisticated machines that combine precision engineering with intelligent automation to deliver exceptional sorting accuracy.
The primary function of a rice color sorter factory involves designing and assembling high-capacity sorting systems that process large volumes of rice efficiently. The equipment produced by a rice color sorter factory employs charged-coupled device cameras and specialized algorithms to identify foreign materials, discolored grains, and quality inconsistencies in real time. This technological approach ensures that only premium-grade rice reaches consumers while removing inferior grains automatically.
Modern rice color sorter factory operations integrate multiple technological features including high-speed processing capabilities, user-friendly control interfaces, and robust mechanical components. The machines produced maintain consistent performance across varying production scales, from small processing facilities to large commercial operations. Applications extend throughout the rice industry, including white rice sorting, brown rice processing, jasmine rice refinement, and organic rice certification. The rice color sorter factory output serves exporters, millers, and distributors seeking to improve product quality and maximize market value. These sorting solutions have become essential infrastructure for rice producers committed to meeting international quality standards and customer expectations.

 EN