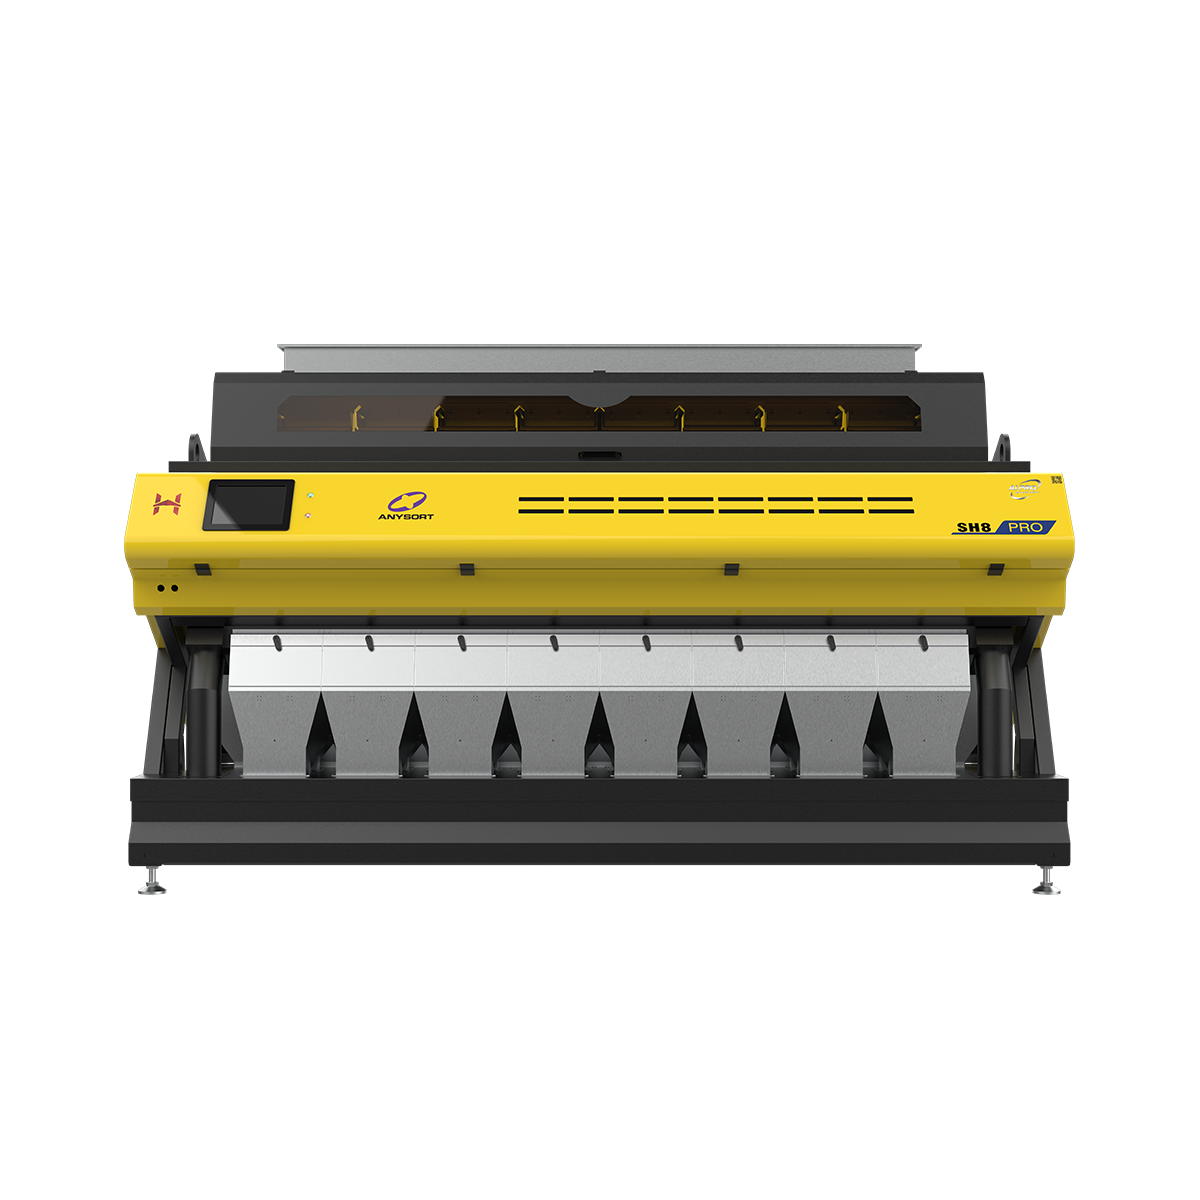
bean color sorter factories
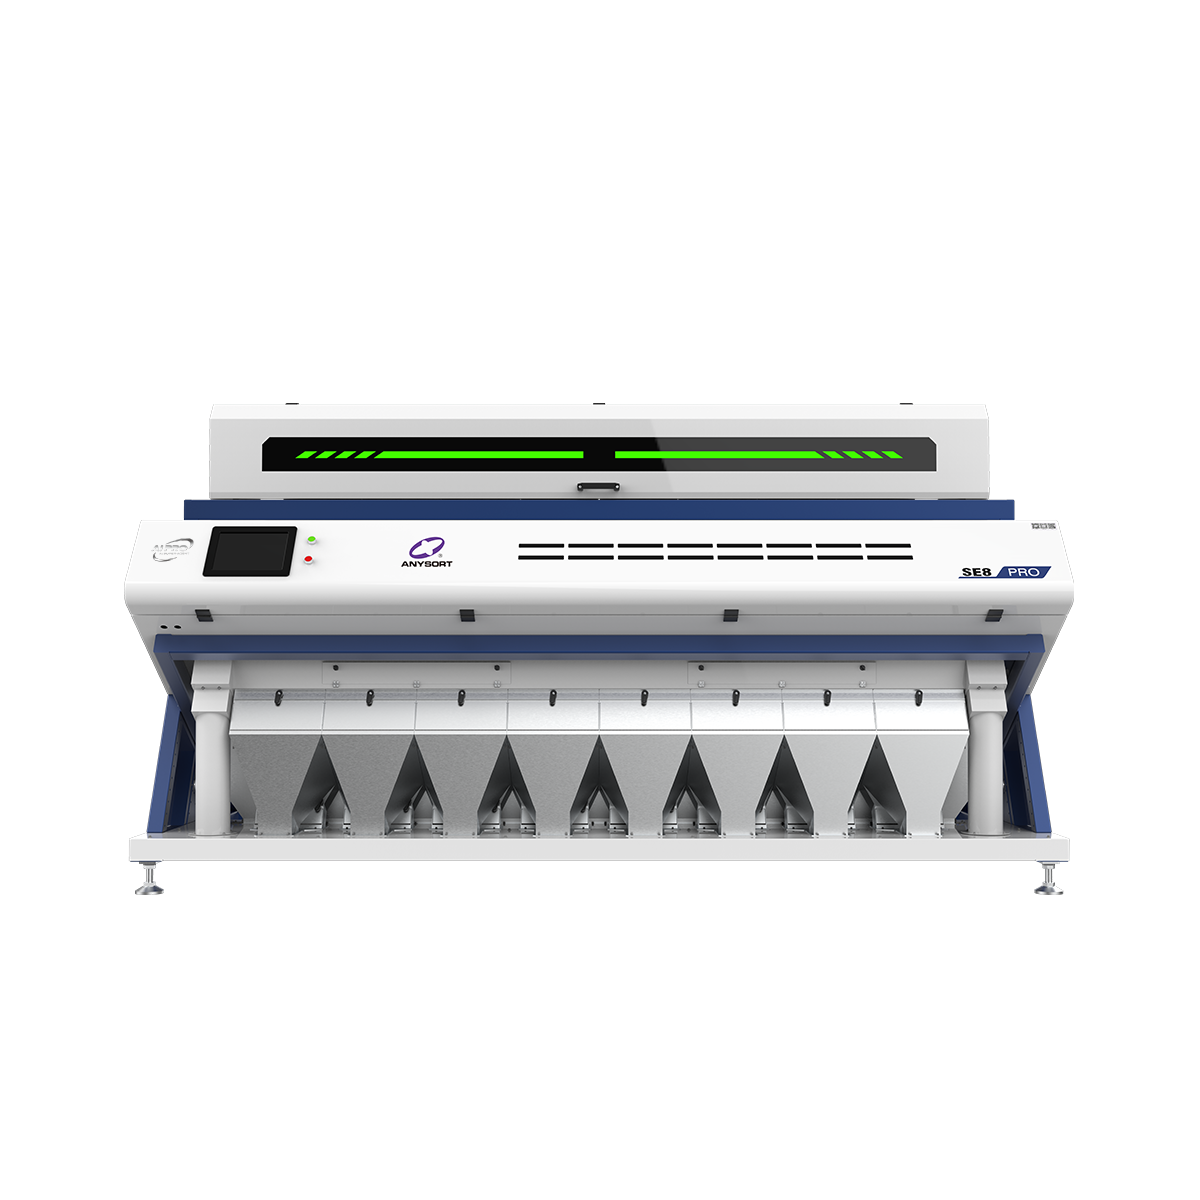
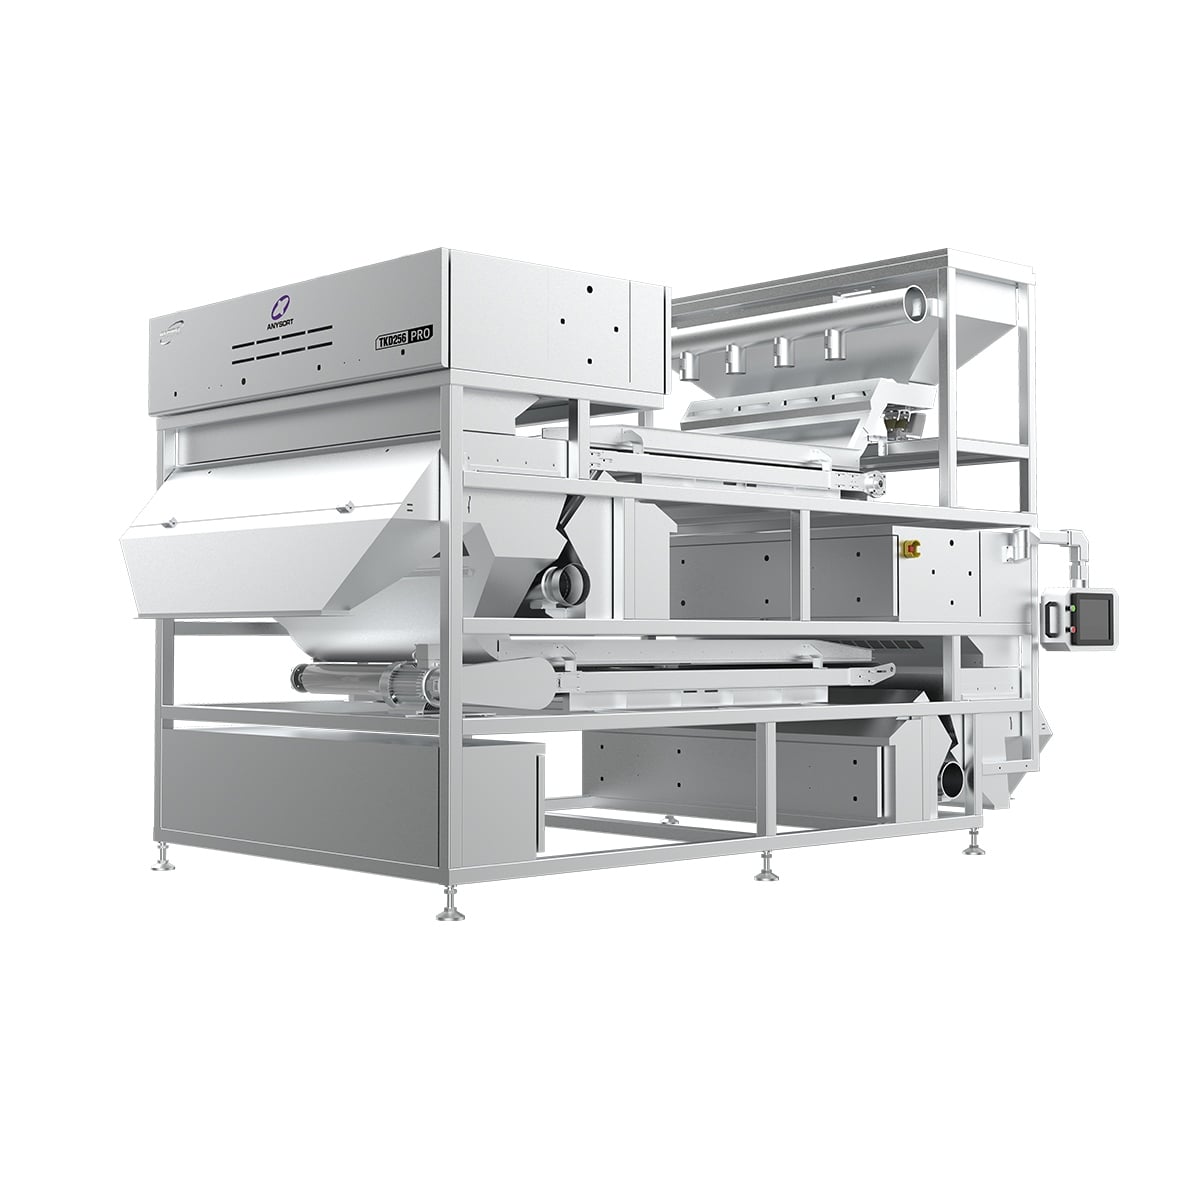
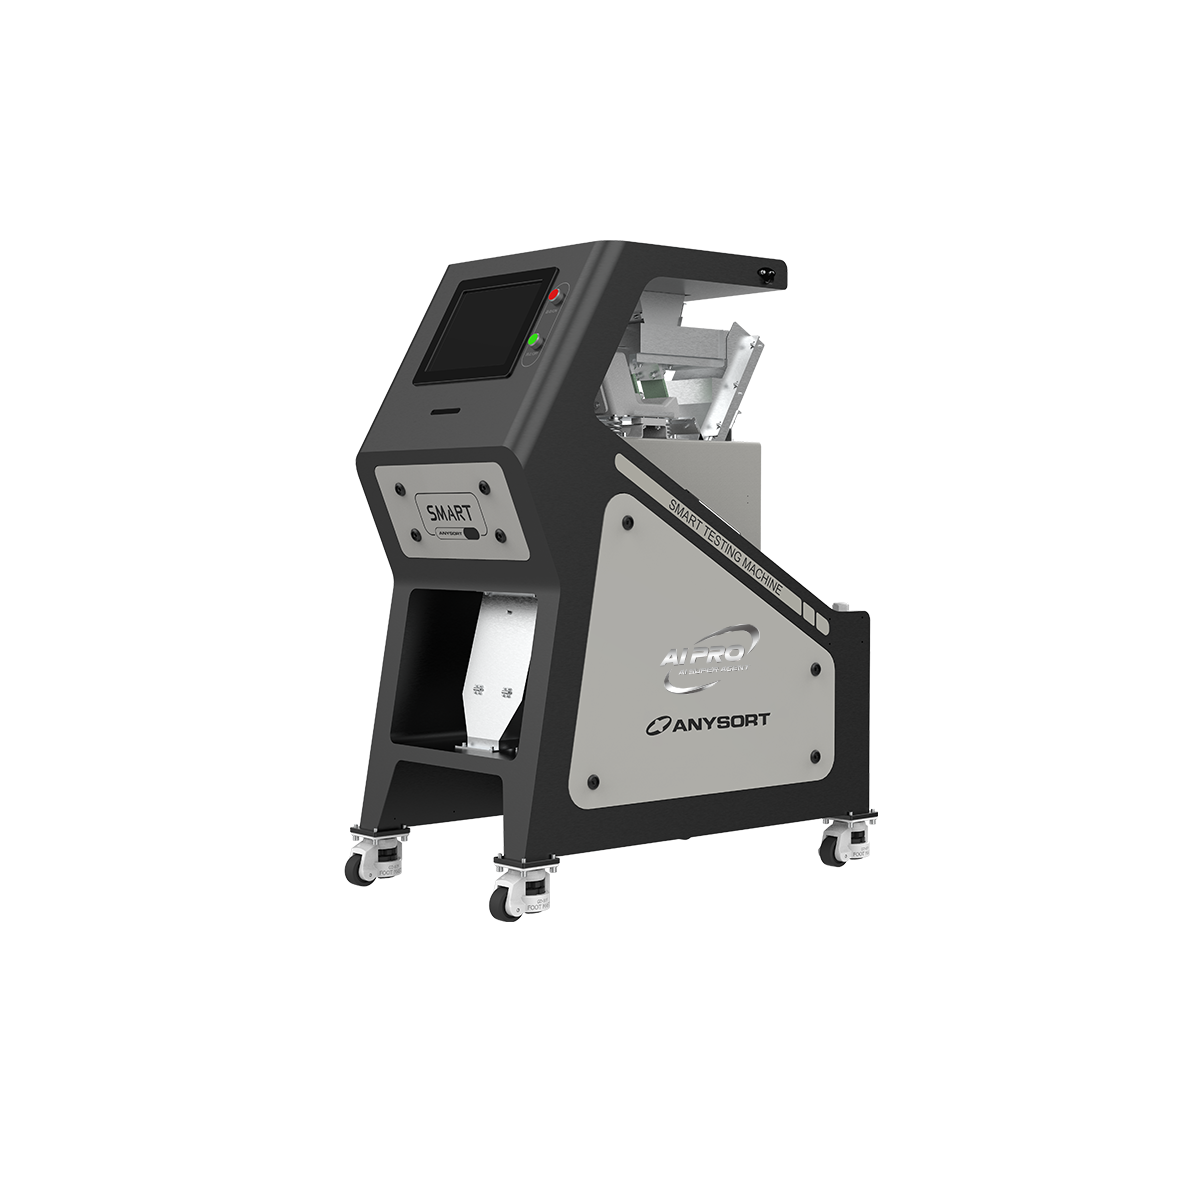
Bean color sorter factories represent advanced agricultural processing facilities specializing in automated grain sorting and quality assessment. These innovative bean color sorter factories utilize cutting-edge optical recognition technology to identify and separate beans based on color variations, size differences, and quality indicators with remarkable precision. The primary function of bean color sorter factories involves inspecting thousands of beans per minute, removing discolored, damaged, or defective units while maintaining the integrity of premium-grade products. Bean color sorter factories incorporate sophisticated camera systems and artificial intelligence algorithms that detect even subtle color gradations and physical imperfections invisible to human eyes. The technology integrated into bean color sorter factories ensures consistent product quality, reduces contamination risks, and maximizes yield efficiency. These facilities serve agricultural cooperatives, processing plants, and food manufacturers seeking reliable quality control solutions. The operational capacity of modern bean color sorter factories ranges from several tons to hundreds of tons daily, depending on the equipment specifications and configuration. Applications of bean color sorter factories extend across dried bean production, pulse processing, specialty crops, and large-scale agricultural operations. The implementation of bean color sorter factories significantly enhances sorting accuracy while simultaneously reducing labor costs and processing time. By automating the quality assessment process, bean color sorter factories enable food producers to maintain strict compliance with international food safety standards and consumer expectations for premium bean products.

 EN