sesame color sorter factory
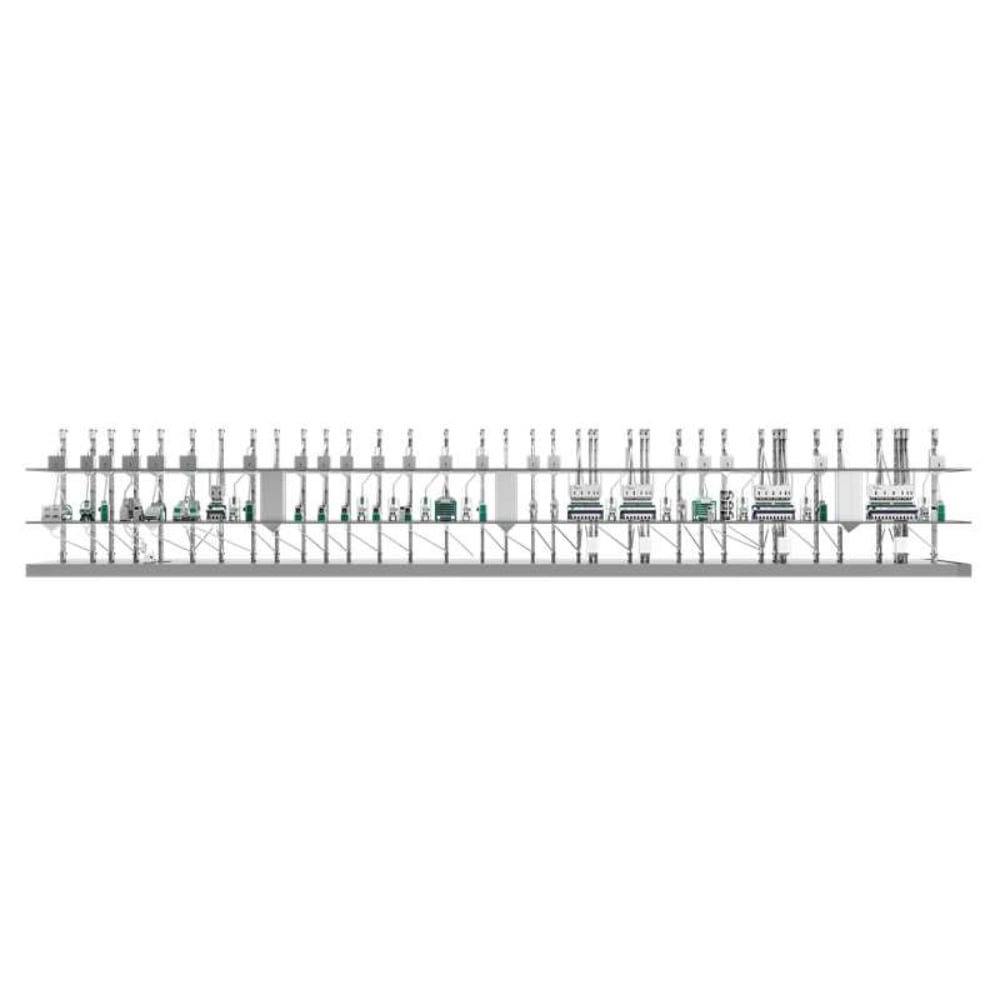
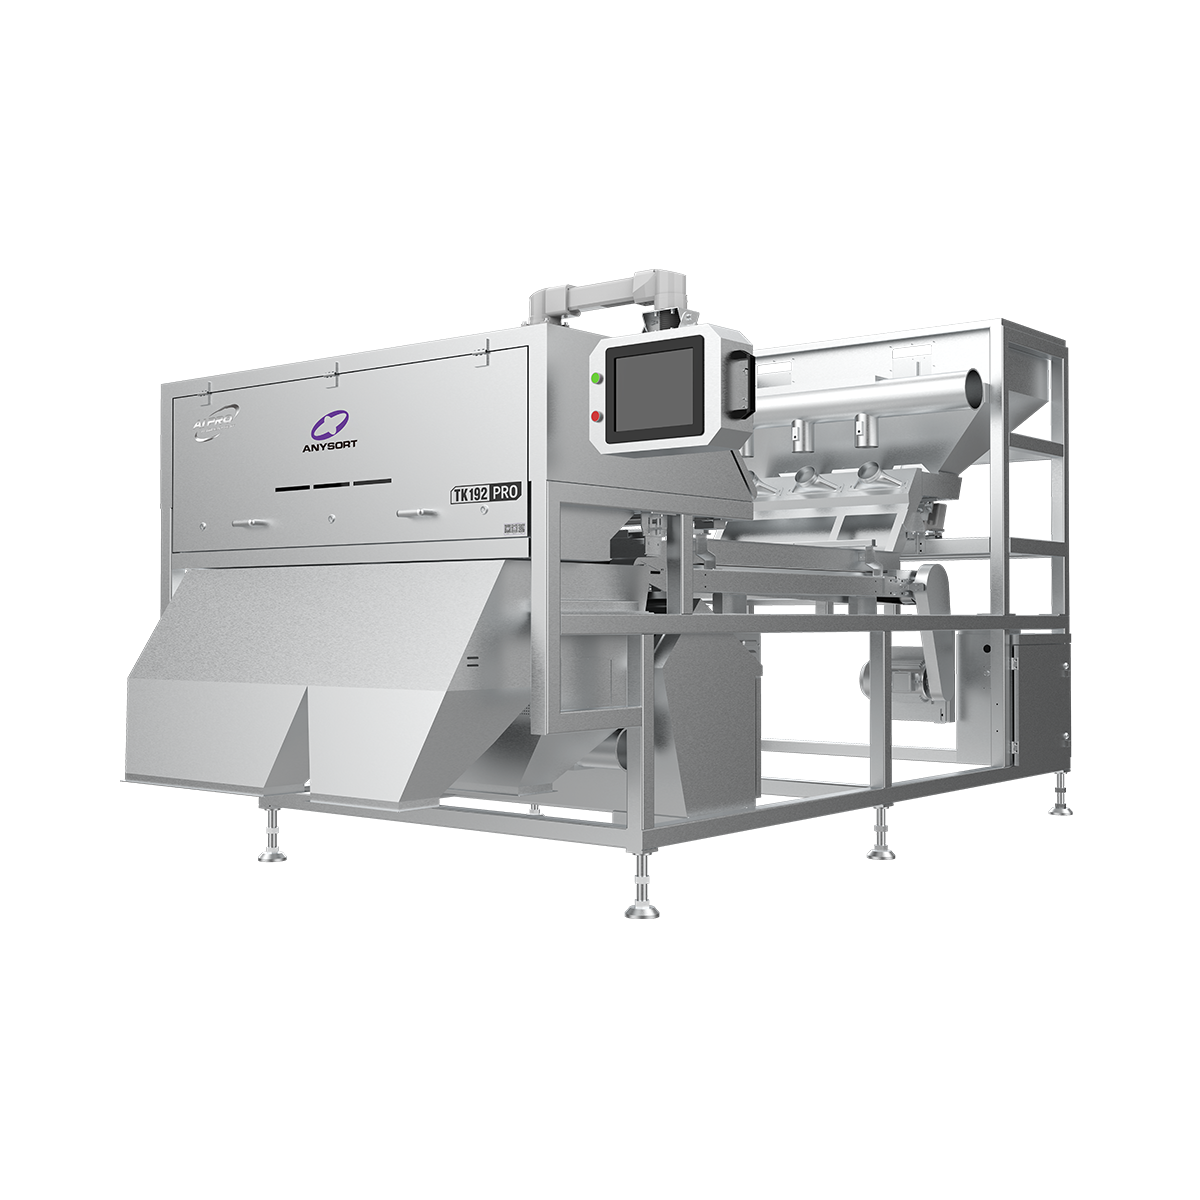
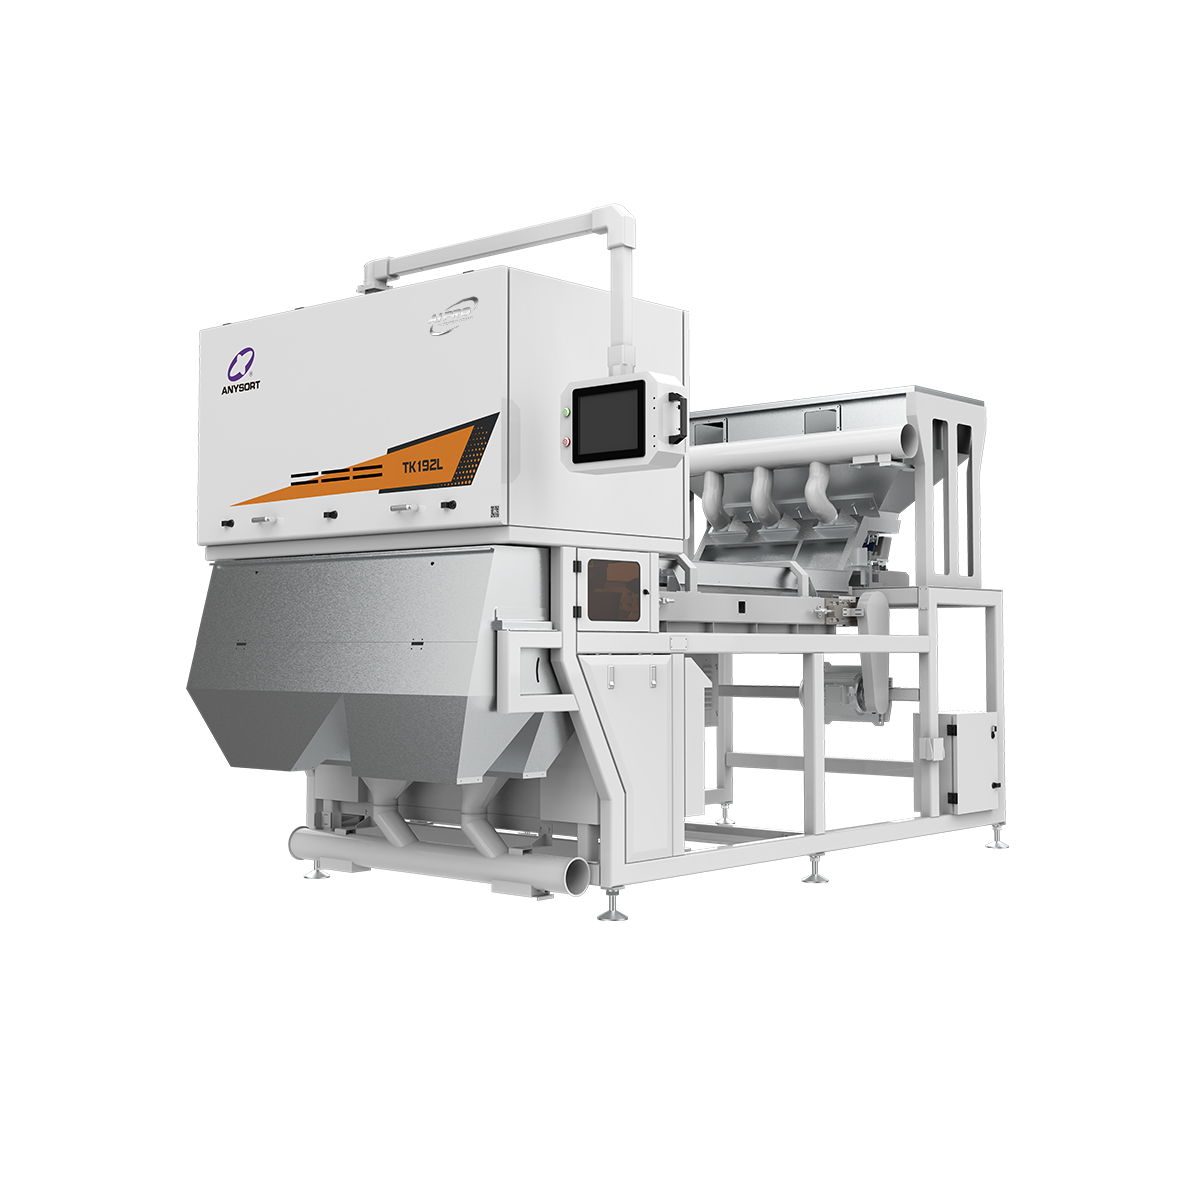
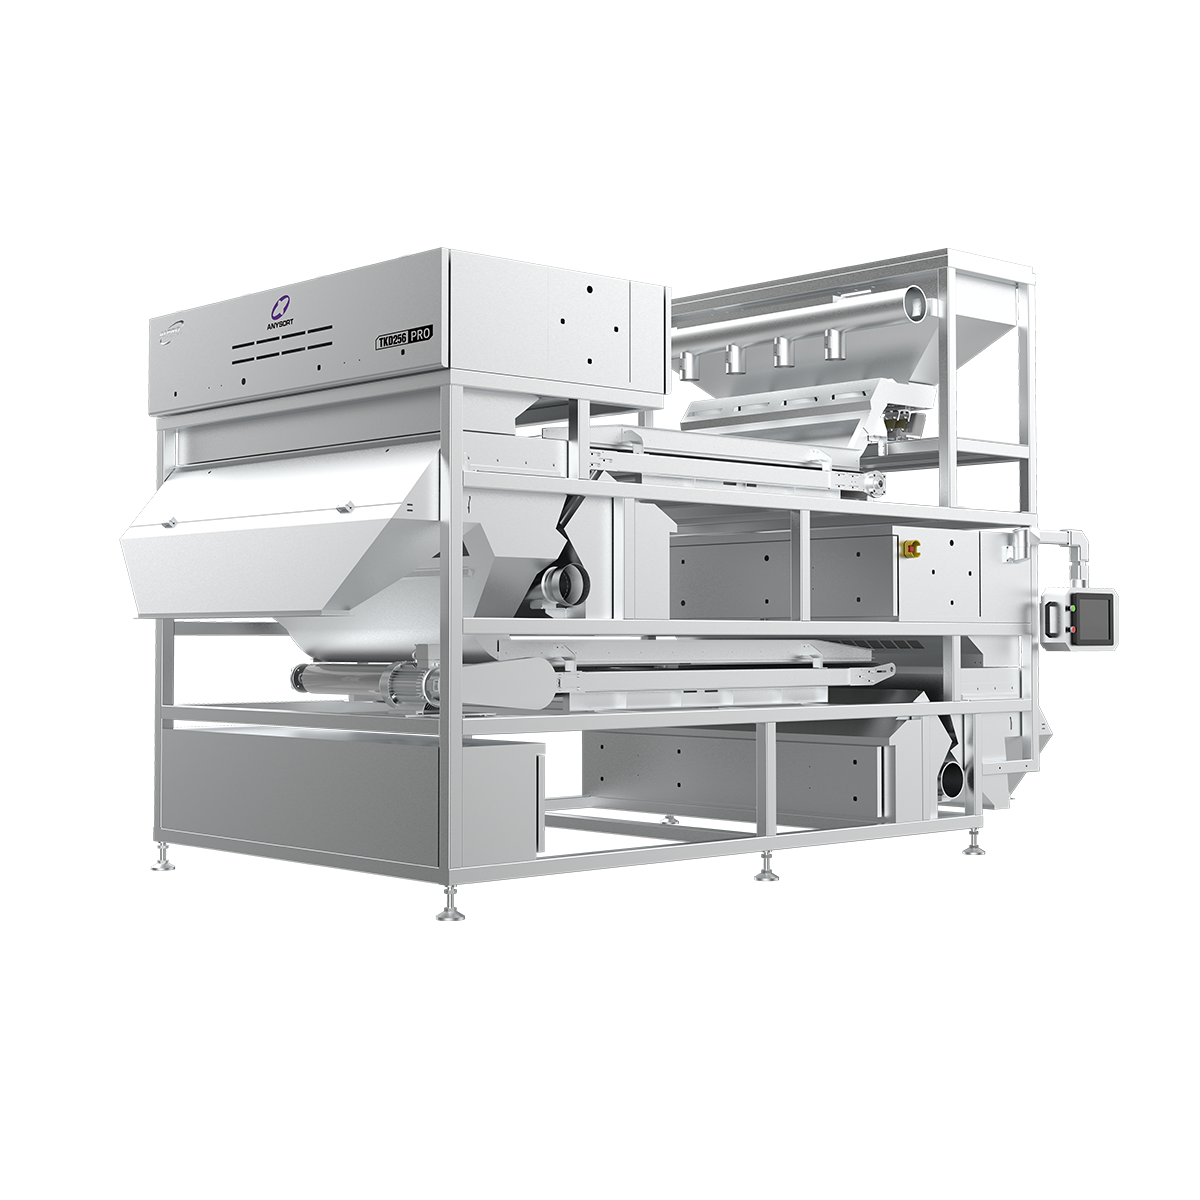
A sesame color sorter factory represents an advanced processing facility designed to handle large-scale sorting and quality control of sesame seeds. This specialized sesame color sorter factory utilizes cutting-edge optical technology to automatically separate sesame seeds based on color, size, and quality parameters. The primary function of a sesame color sorter factory is to enhance product consistency and eliminate defective seeds that could compromise final product quality.
The technological features integrated into a modern sesame color sorter factory include high-resolution cameras, artificial intelligence algorithms, and precision ejection systems. These components work together to identify impurities, discolored seeds, and foreign materials with remarkable accuracy. A sesame color sorter factory can process thousands of kilograms of sesame seeds daily while maintaining stringent quality standards.
Applications of sesame color sorter factory equipment extend across multiple industries including food processing, oil production, and agricultural export operations. The sesame color sorter factory technology ensures that only premium-grade seeds reach consumers, protecting brand reputation and market position. By implementing this technology, processors significantly reduce manual labor requirements and operational inconsistencies. The sesame color sorter factory represents a crucial investment for companies seeking competitive advantage in the global sesame market.

 EN