Color Sorter: Advanced Optical Sorting Equipment

All Categories

color sorter

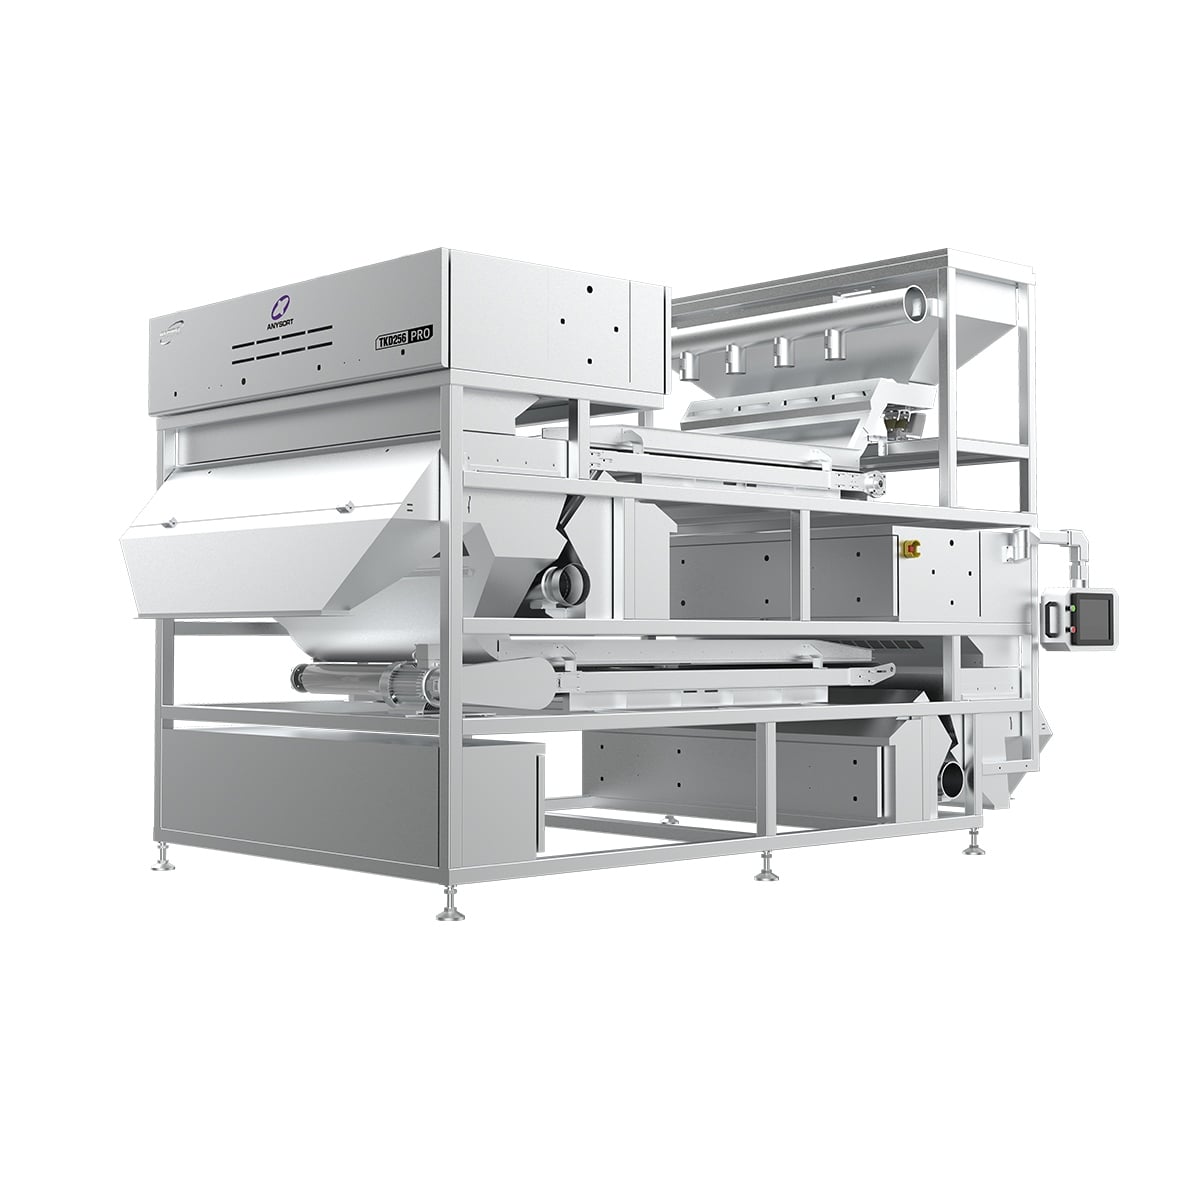
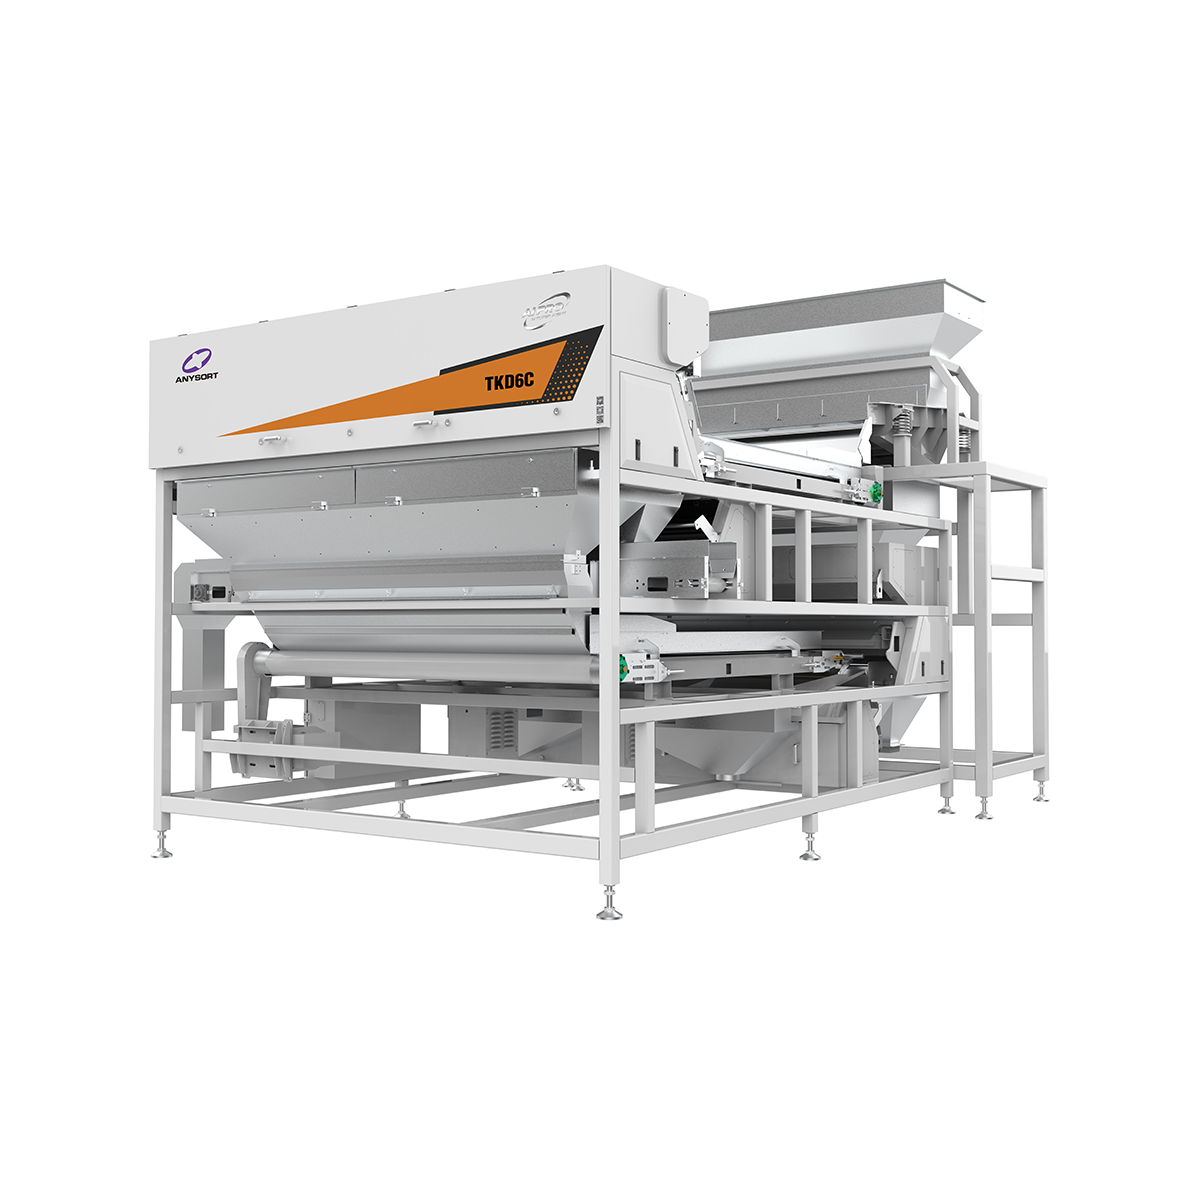
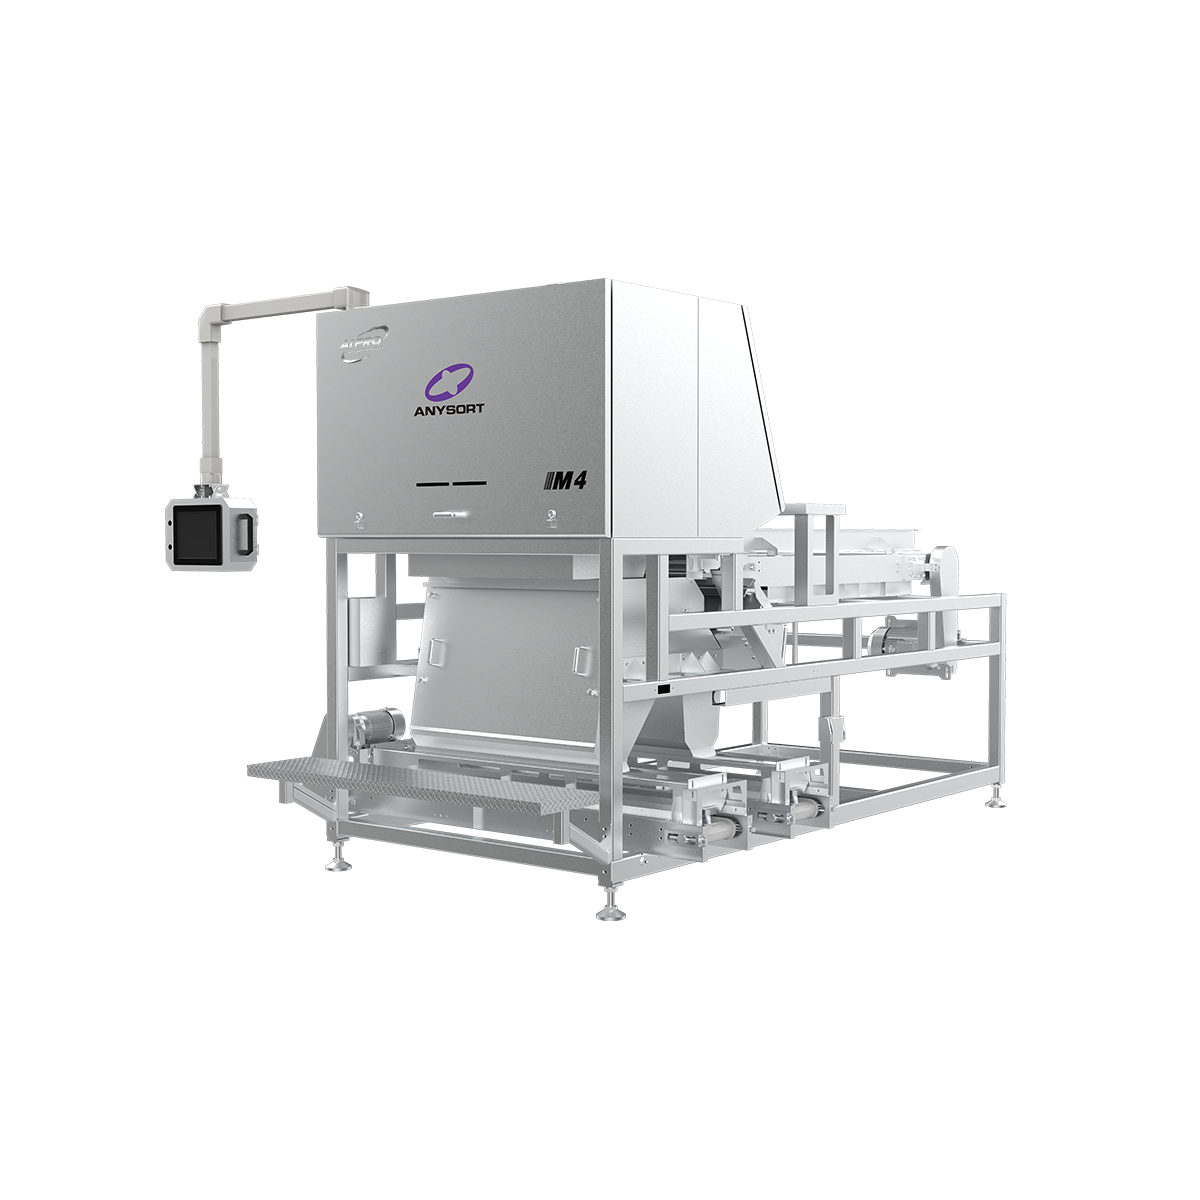
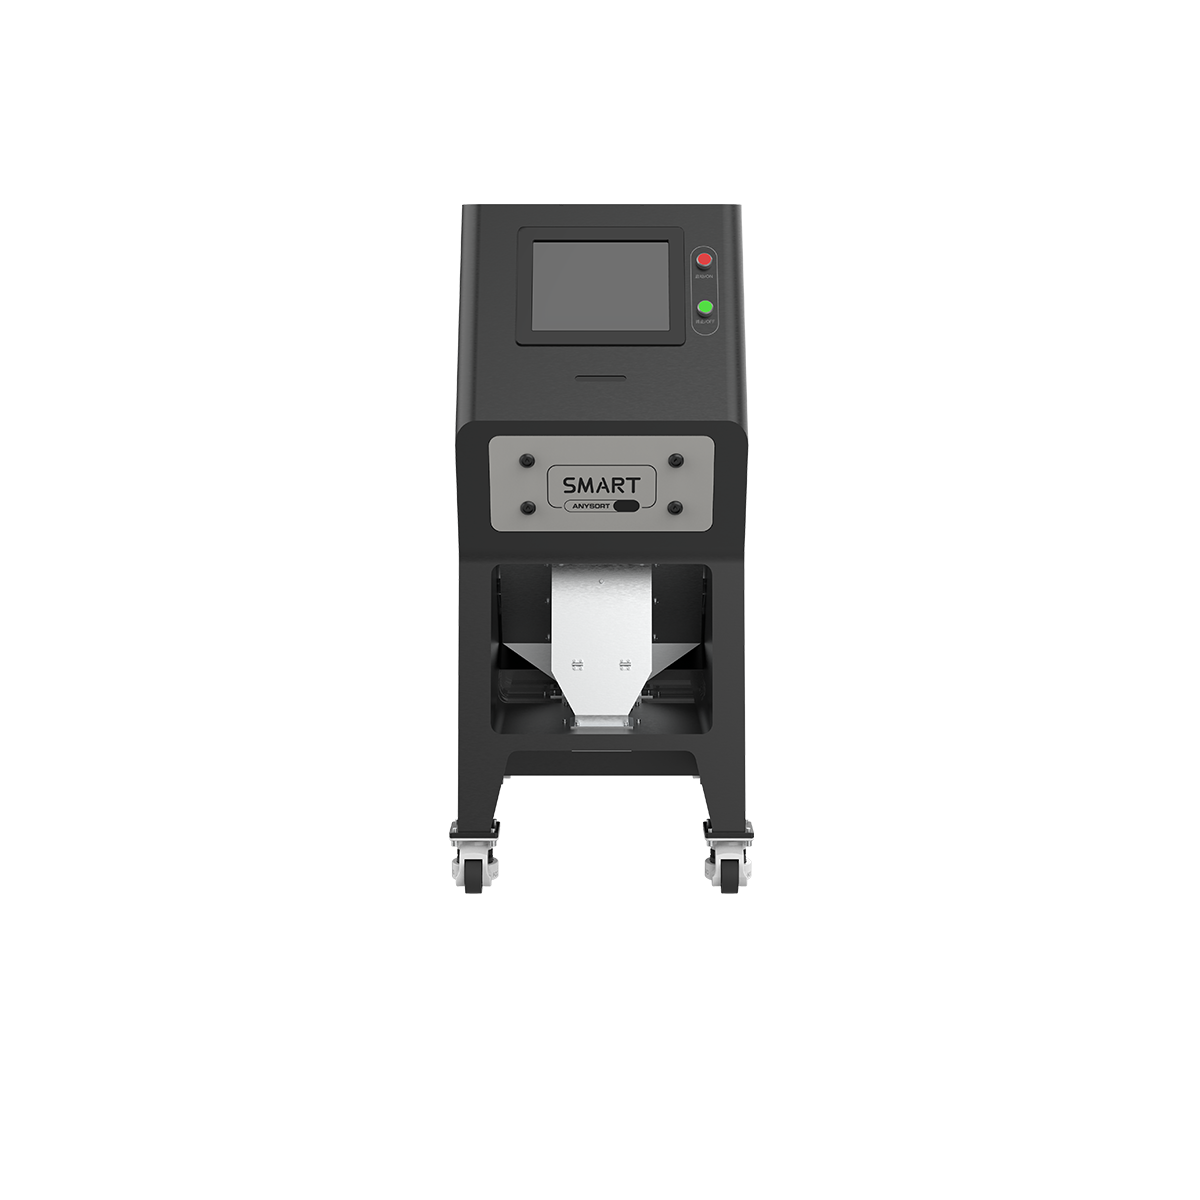
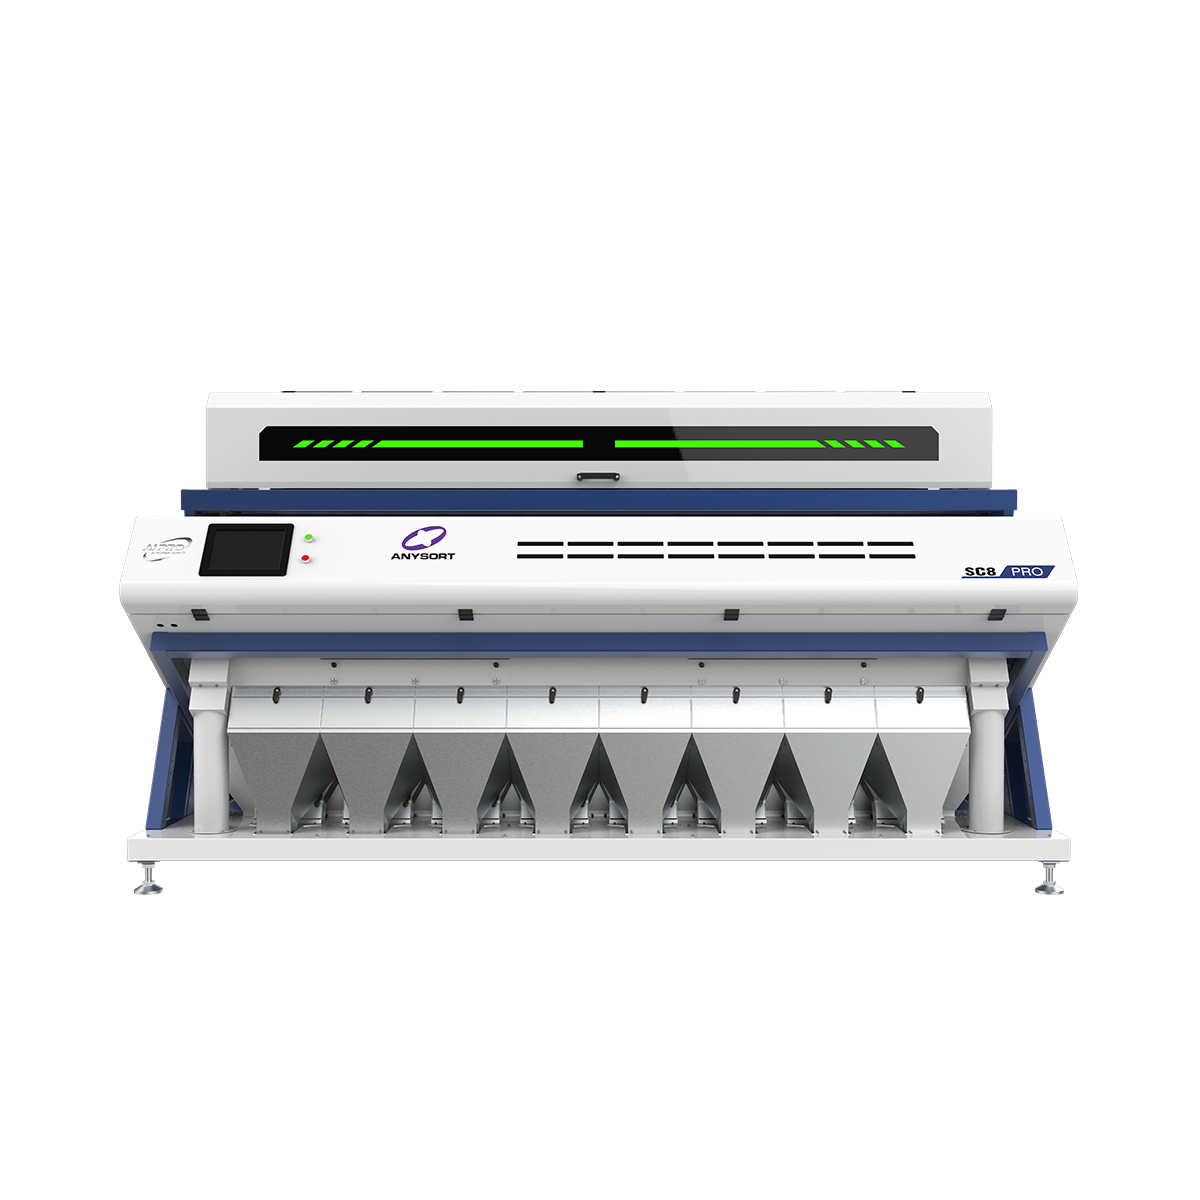
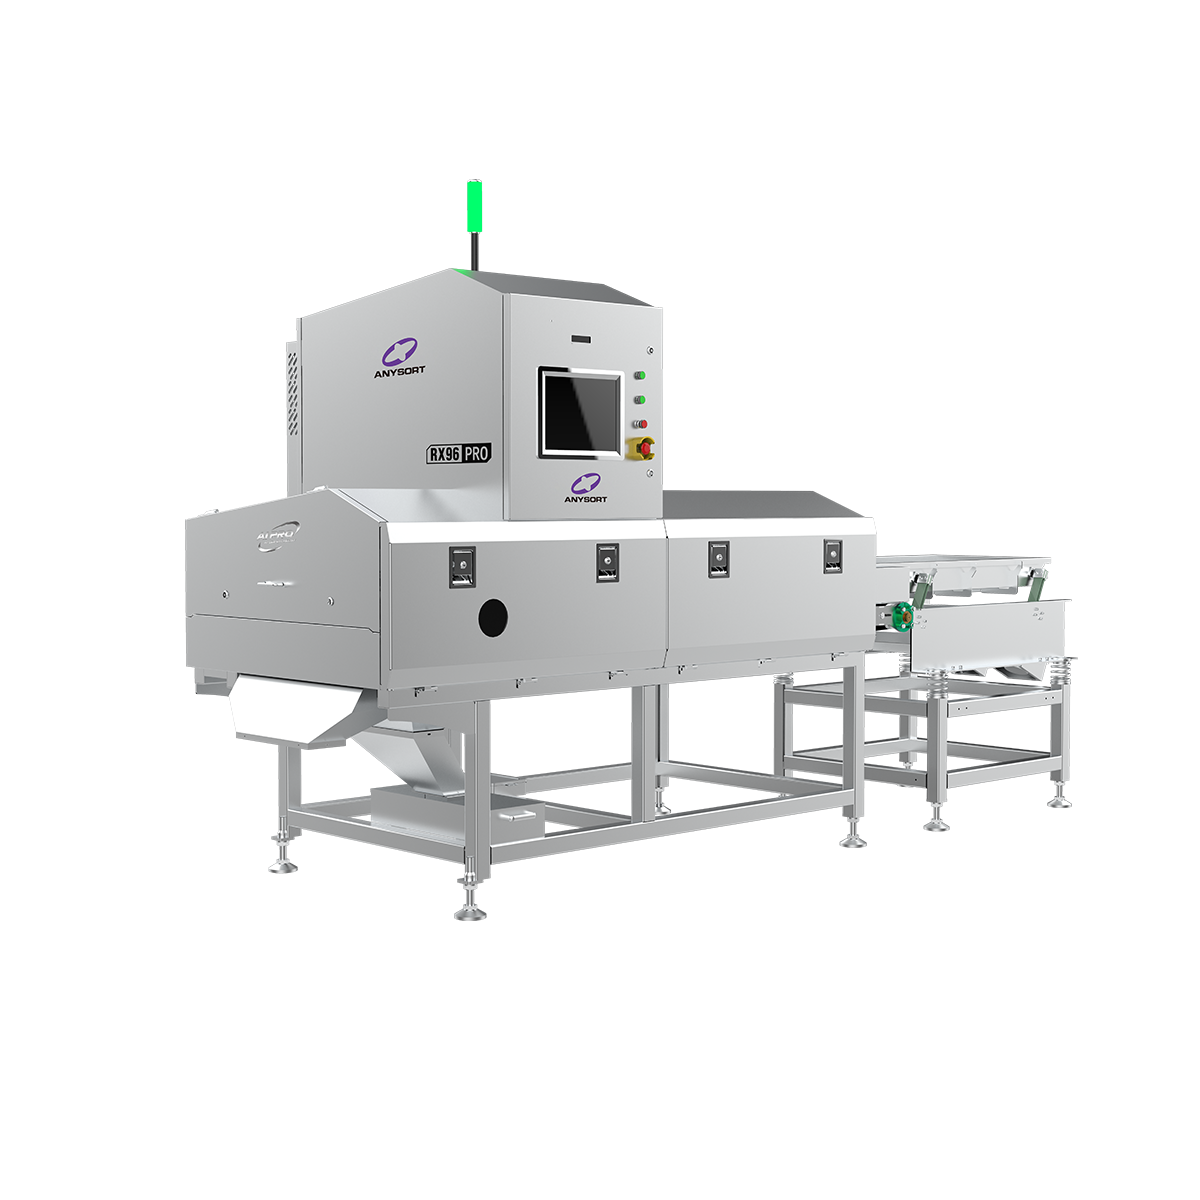
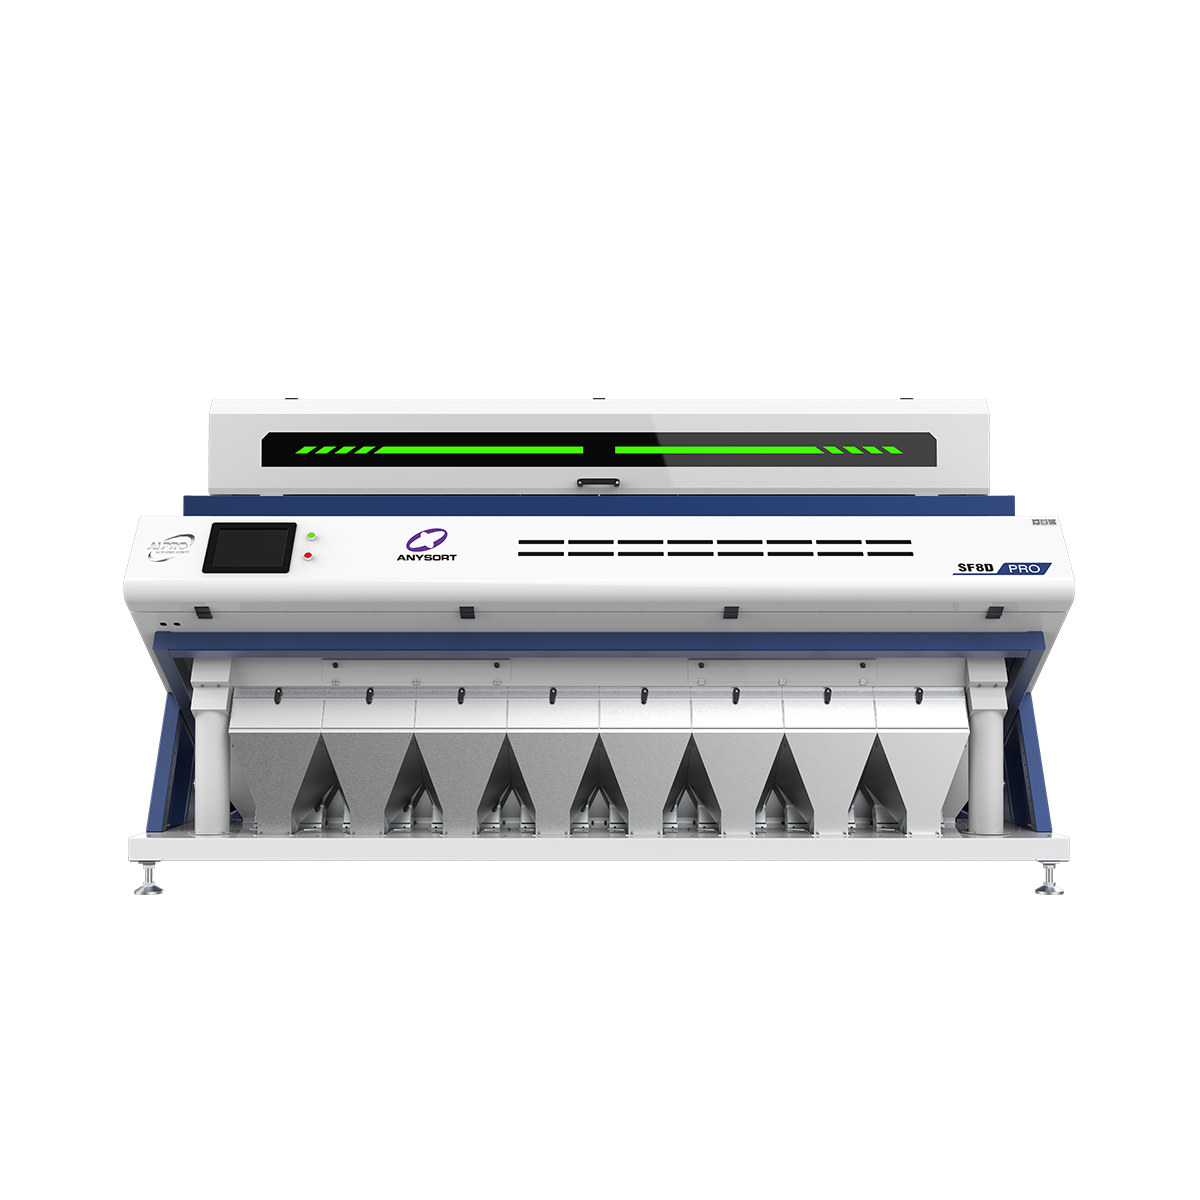
A color sorter is an advanced optical sorting machine designed to automatically separate and grade materials based on color differences and quality characteristics. This innovative equipment uses high-resolution cameras and sophisticated image processing technology to identify and remove defective items, foreign materials, and discolored particles from bulk materials with exceptional precision. The color sorter operates by capturing images of each particle as it passes through the sorting chamber, analyzing these images against predefined quality standards, and using pneumatic ejectors to divert unacceptable items into waste streams. Color sorter technology has revolutionized material processing across multiple industries by dramatically improving product quality while reducing manual labor costs. These machines can process hundreds of kilograms per hour, making them indispensable for high-volume operations. The color sorter employs advanced sensors that detect minute color variations invisible to the human eye, ensuring consistent quality control. Common applications include rice and grain processing, where the color sorter removes discolored kernels and foreign particles; plastic recycling, where it sorts different plastic types by color; and coffee bean processing, where it eliminates defective beans. Modern color sorter systems feature touchscreen interfaces, real-time monitoring capabilities, and data logging functions that allow operators to track sorting performance and adjust parameters instantly. The technology represents a significant investment in operational efficiency, delivering rapid return on investment through reduced waste, improved product consistency, and enhanced customer satisfaction. Whether processing agricultural commodities or recycled materials, the color sorter remains an essential component of modern production facilities.

Popular Products

The color sorter delivers transformative operational benefits that directly impact your bottom line and production efficiency. First, this equipment dramatically reduces manual sorting requirements, freeing your workforce to focus on higher-value tasks while minimizing labor-intensive processes. The color sorter improves product consistency by removing defective items with machine precision that far exceeds human capability, resulting in superior end products that command premium market prices. Your customers receive consistently high-quality materials, strengthening brand reputation and building long-term business relationships. The color sorter operates continuously without fatigue, maintaining peak performance throughout extended production runs, which enables higher throughput and greater production capacity than traditional sorting methods. This equipment significantly reduces waste by accurately identifying and separating marginal materials that human sorters might miss, maximizing yield from raw materials and improving profitability. The color sorter provides measurable cost savings through reduced product rejection rates, lower customer complaints, and decreased returns. Implementation of a color sorter creates substantial operational advantages: minimal maintenance requirements compared to mechanical alternatives, user-friendly controls requiring minimal training, and reliable performance across diverse material types. The color sorter delivers rapid return on investment through improved efficiency and reduced operational costs. For agricultural producers, food processors, recycling facilities, and manufacturing operations, the color sorter represents a game-changing technology that enhances competitiveness in increasingly quality-conscious markets. Organizations adopting color sorter technology report improved customer satisfaction scores and reduced production costs. This equipment transforms your sorting capability from a cost center into a quality investment that strengthens market position and drives sustainable profitability.

Latest News

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

color sorter

Precision Optical Detection System

Precision Optical Detection System

The color sorter incorporates state-of-the-art optical detection technology that identifies color variations and quality defects with extraordinary accuracy. High-resolution cameras capture detailed images of each material particle, while advanced algorithms analyze these images in milliseconds, comparing results against your customized quality parameters. This precision allows the color sorter to detect subtle color differences, contamination, and structural defects that remain invisible to human inspectors. The detection system operates at incredible speeds, processing materials continuously without reducing throughput. By implementing this advanced technology, the color sorter ensures your products consistently meet or exceed quality standards. The optical detection capabilities of the color sorter reduce product variability, enhance customer satisfaction, and protect brand reputation. Organizations using this technology report measurably improved product quality metrics and fewer customer complaints. The color sorter's detection precision directly translates to superior finished products and market differentiation.
High-Speed Sorting Capacity and Throughput

High-Speed Sorting Capacity and Throughput

A modern color sorter delivers exceptional sorting capacity, processing substantial volumes of material per hour while maintaining accurate quality control. This high-speed performance enables production facilities to increase throughput without requiring additional labor or significant facility expansion. The color sorter maintains consistent sorting accuracy even at maximum speed, ensuring that processing velocity never compromises quality standards. This performance characteristic makes the color sorter particularly valuable for high-volume operations processing hundreds of kilograms hourly. The equipment's sorting speed dramatically reduces production bottlenecks, allowing facilities to meet aggressive delivery deadlines and fulfill larger customer orders. By combining speed with precision, the color sorter maximizes operational efficiency and profitability. Industries relying on bulk material processing find that the color sorter's throughput capabilities transform production economics. The color sorter enables facilities to achieve previously impossible production targets while maintaining rigorous quality control. This combination of speed and accuracy represents a significant competitive advantage in time-sensitive markets.
Customizable Sorting Parameters and User Control

Customizable Sorting Parameters and User Control

The color sorter features intuitive customization capabilities that allow operators to adjust sorting criteria precisely matching your specific material requirements and quality standards. Touchscreen interfaces provide easy access to sorting parameters, enabling quick adjustments between different material types without requiring extensive recalibration. The color sorter stores multiple preset configurations, facilitating rapid transitions between products and minimizing production downtime. Advanced monitoring systems display real-time sorting data, performance metrics, and operational statistics that inform production decisions. This transparency helps identify efficiency improvements and troubleshoot sorting challenges immediately. The color sorter's flexible design accommodates varying material characteristics, sizes, and color ranges across diverse applications. Operators can quickly modify sensitivity levels, detection thresholds, and ejection parameters based on material batches or customer specifications. The color sorter's adaptability makes it suitable for facilities processing multiple product types. Remote monitoring capabilities on modern color sorter systems enable supervisors to track performance from central locations. This flexibility transforms the color sorter into a responsive tool that optimizes results across changing production scenarios.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy