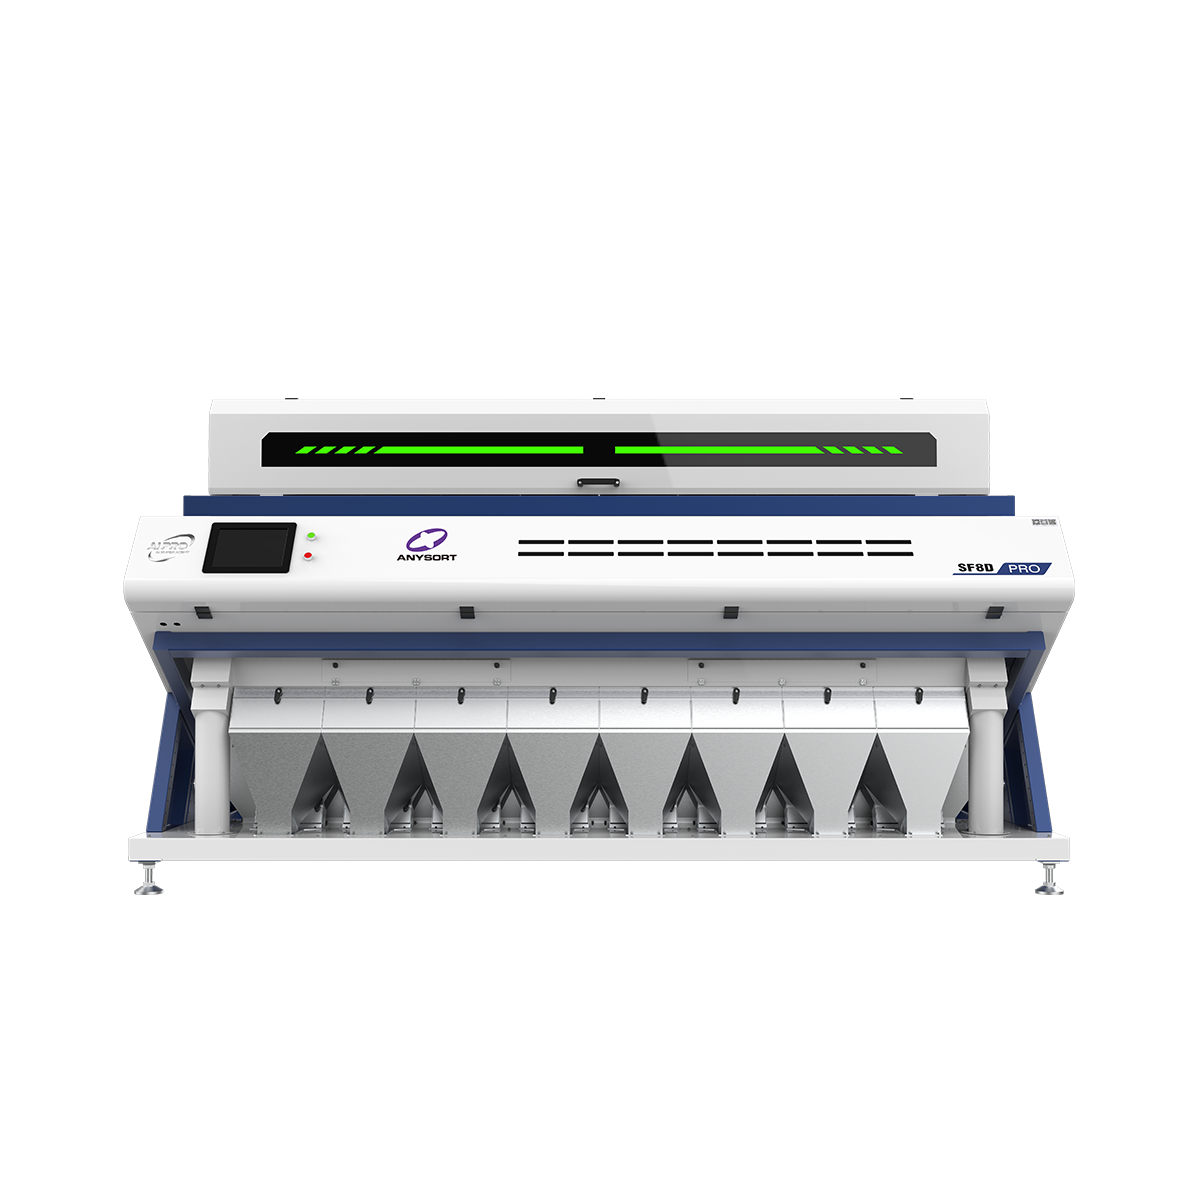
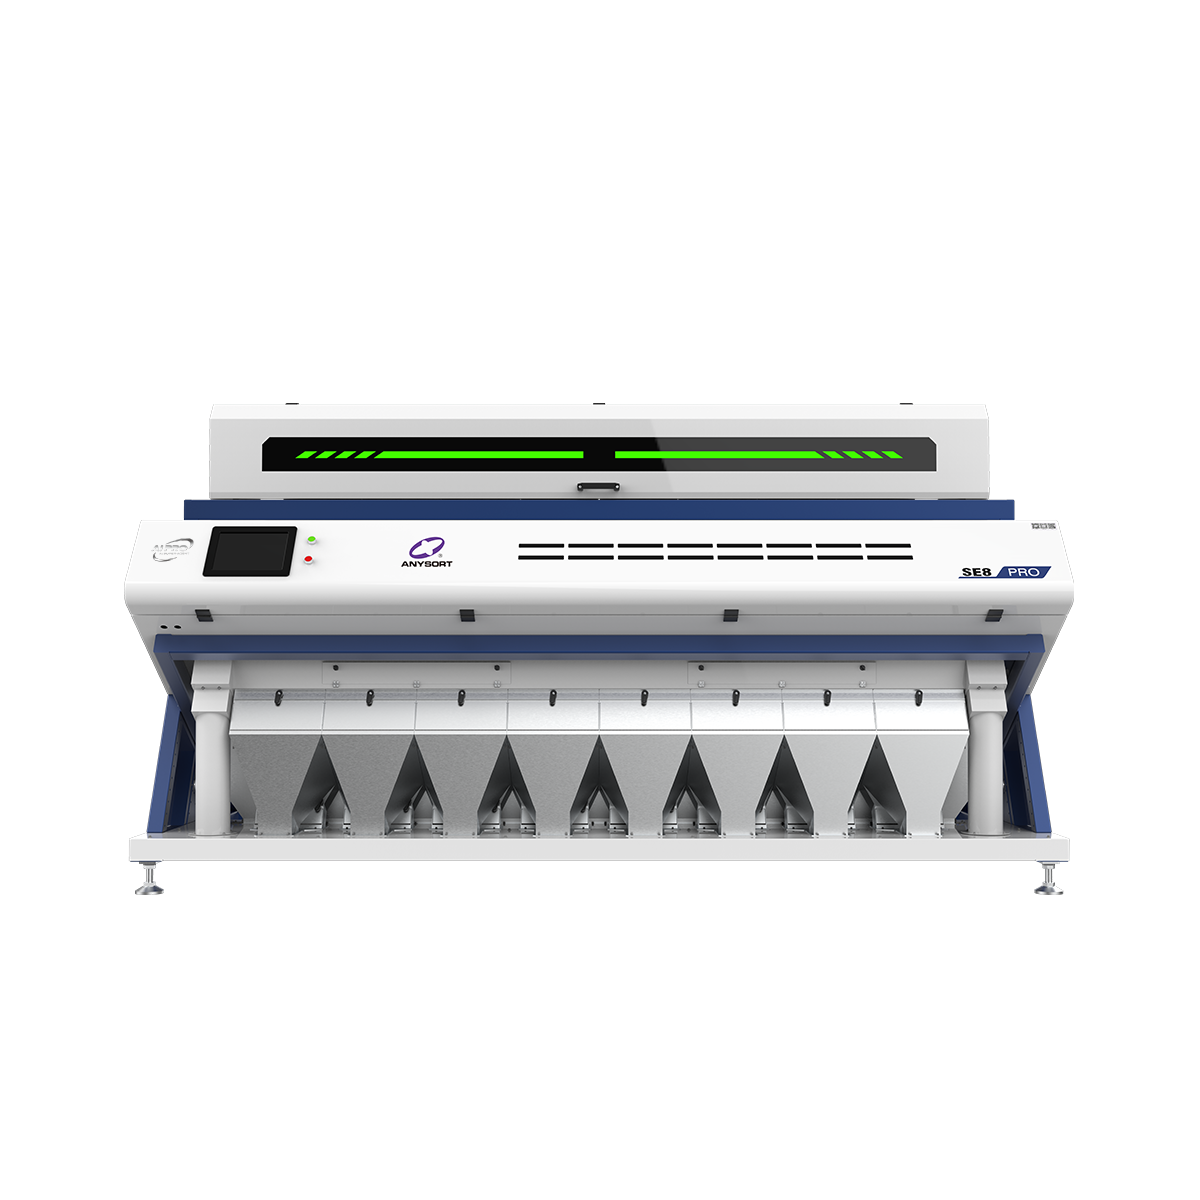
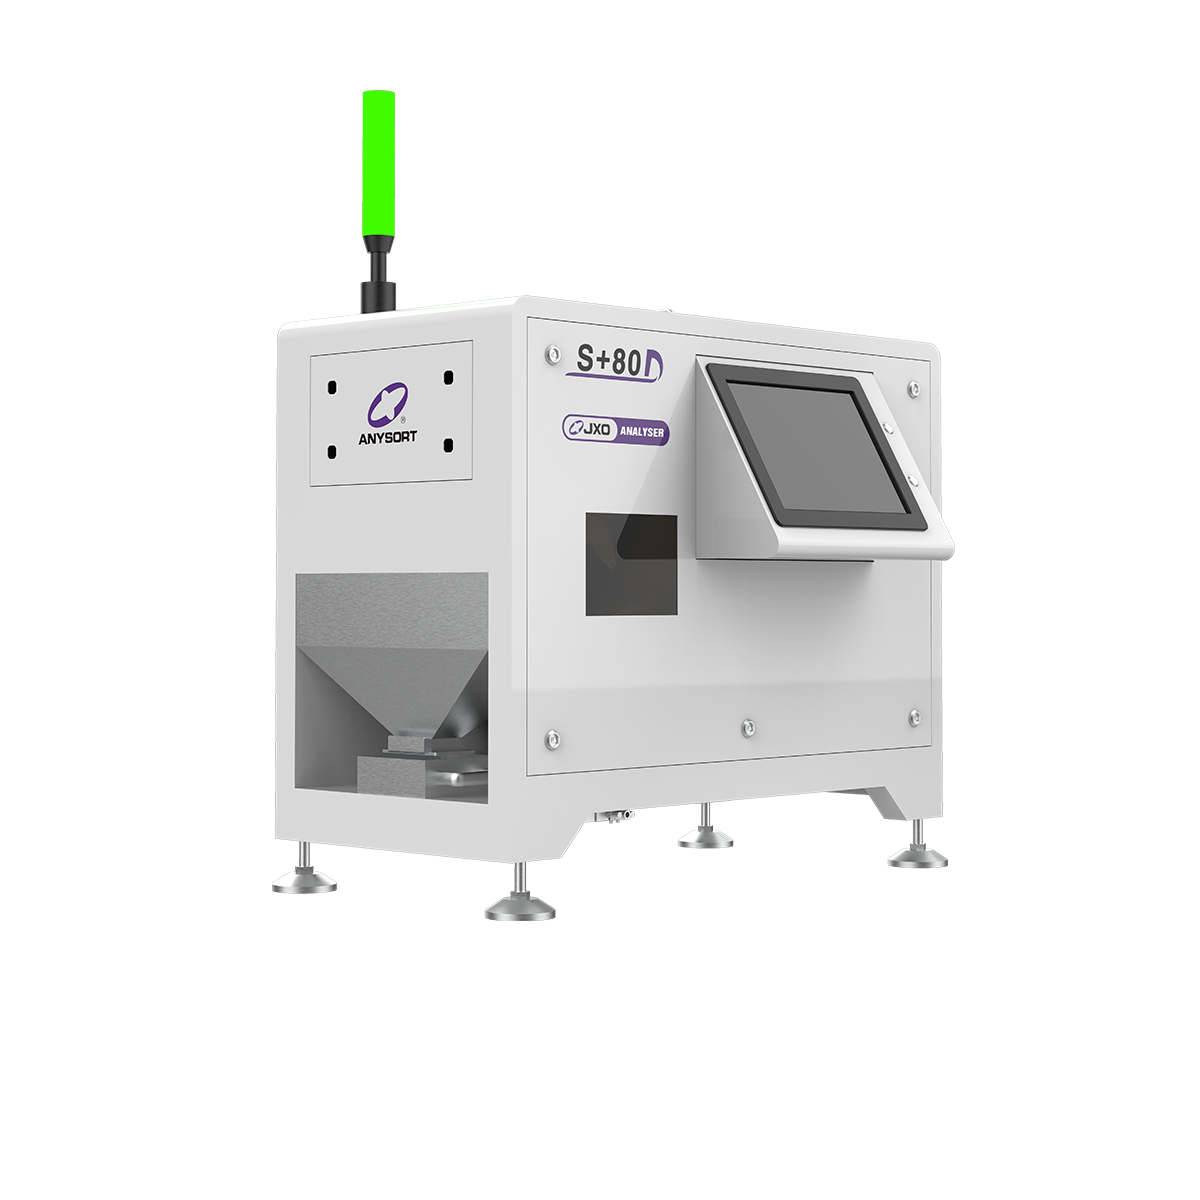
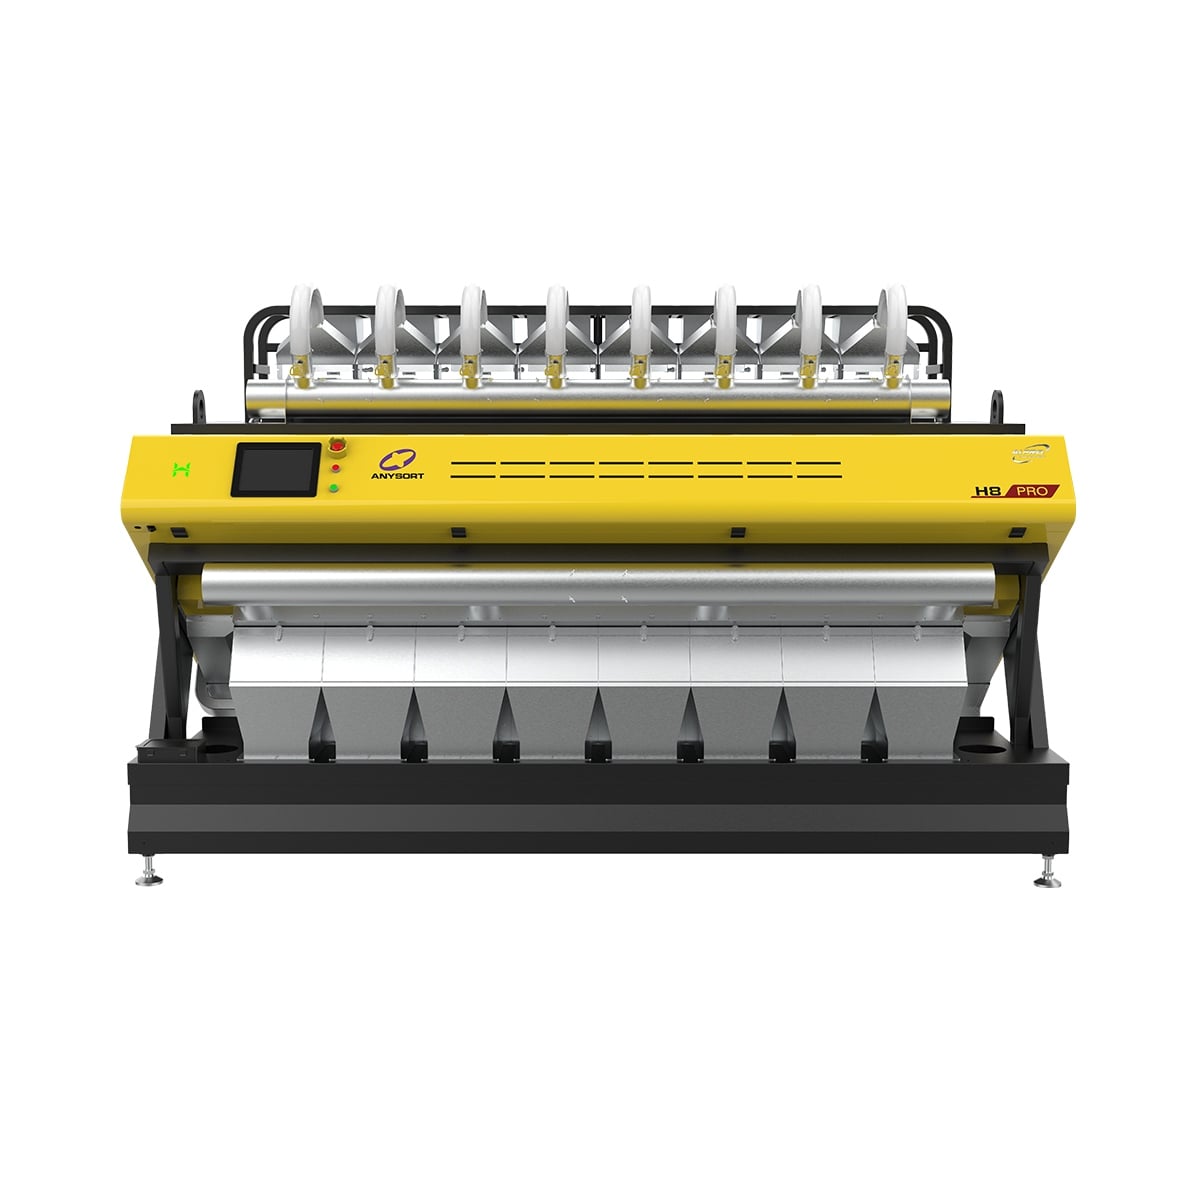
color sorting machine
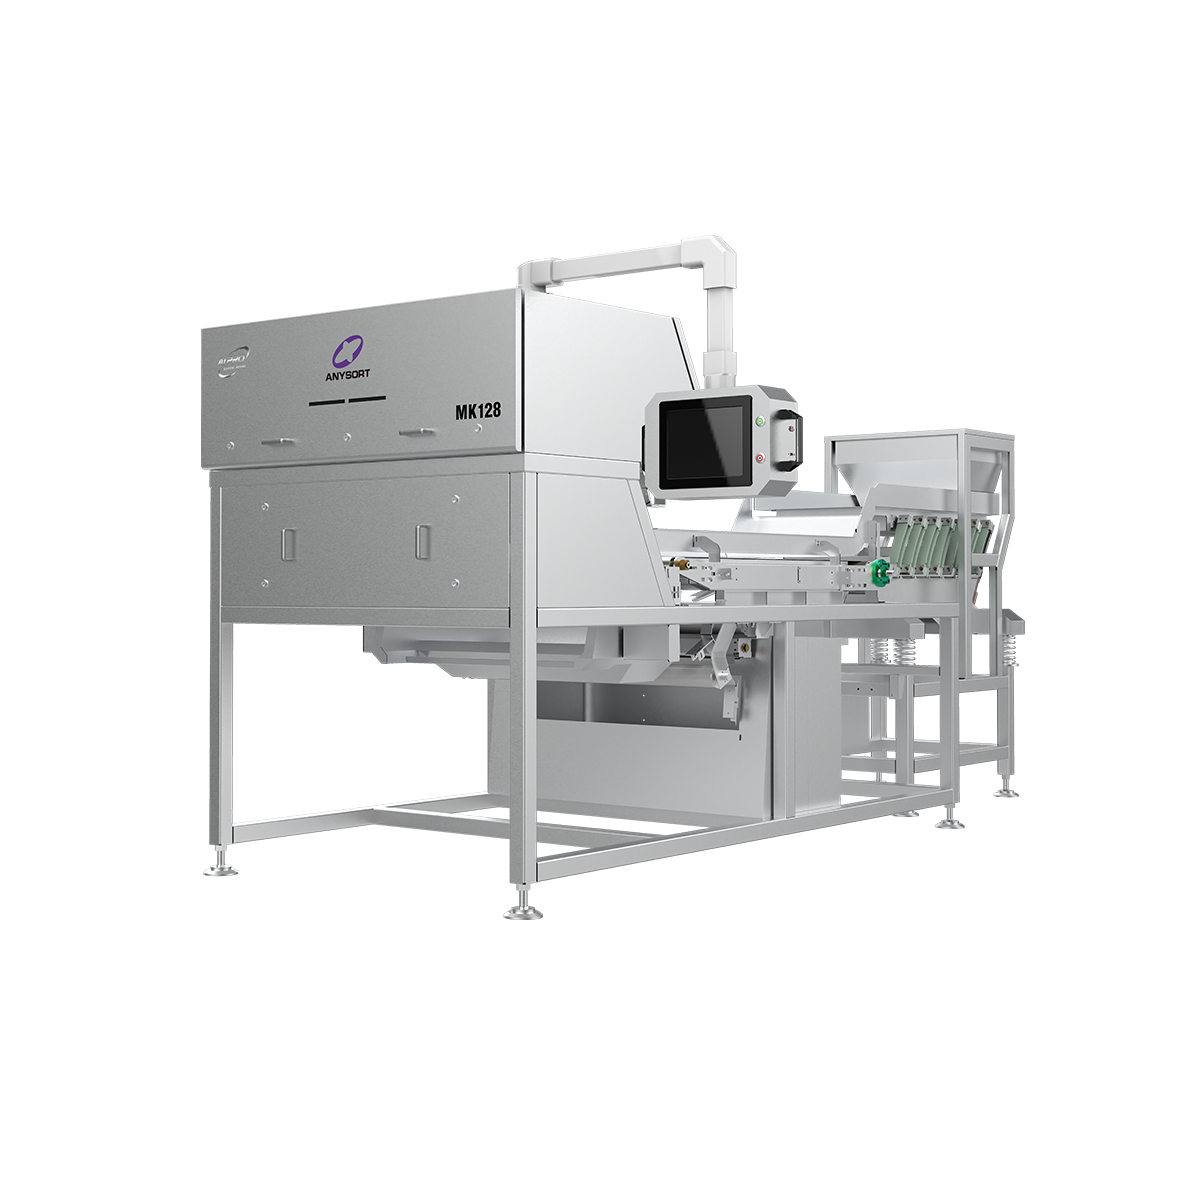
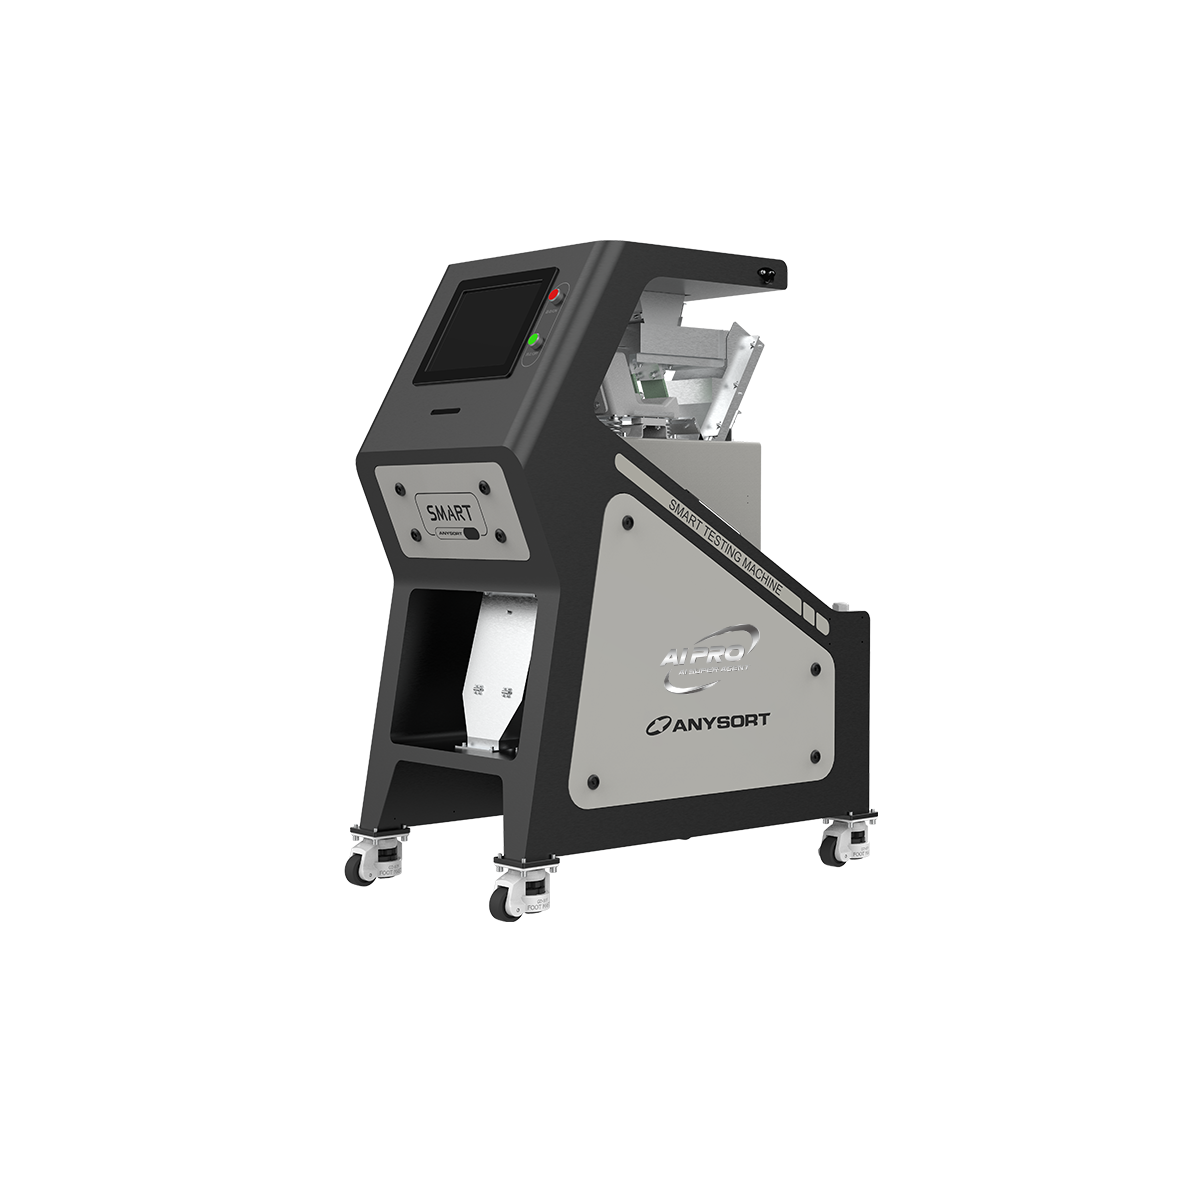
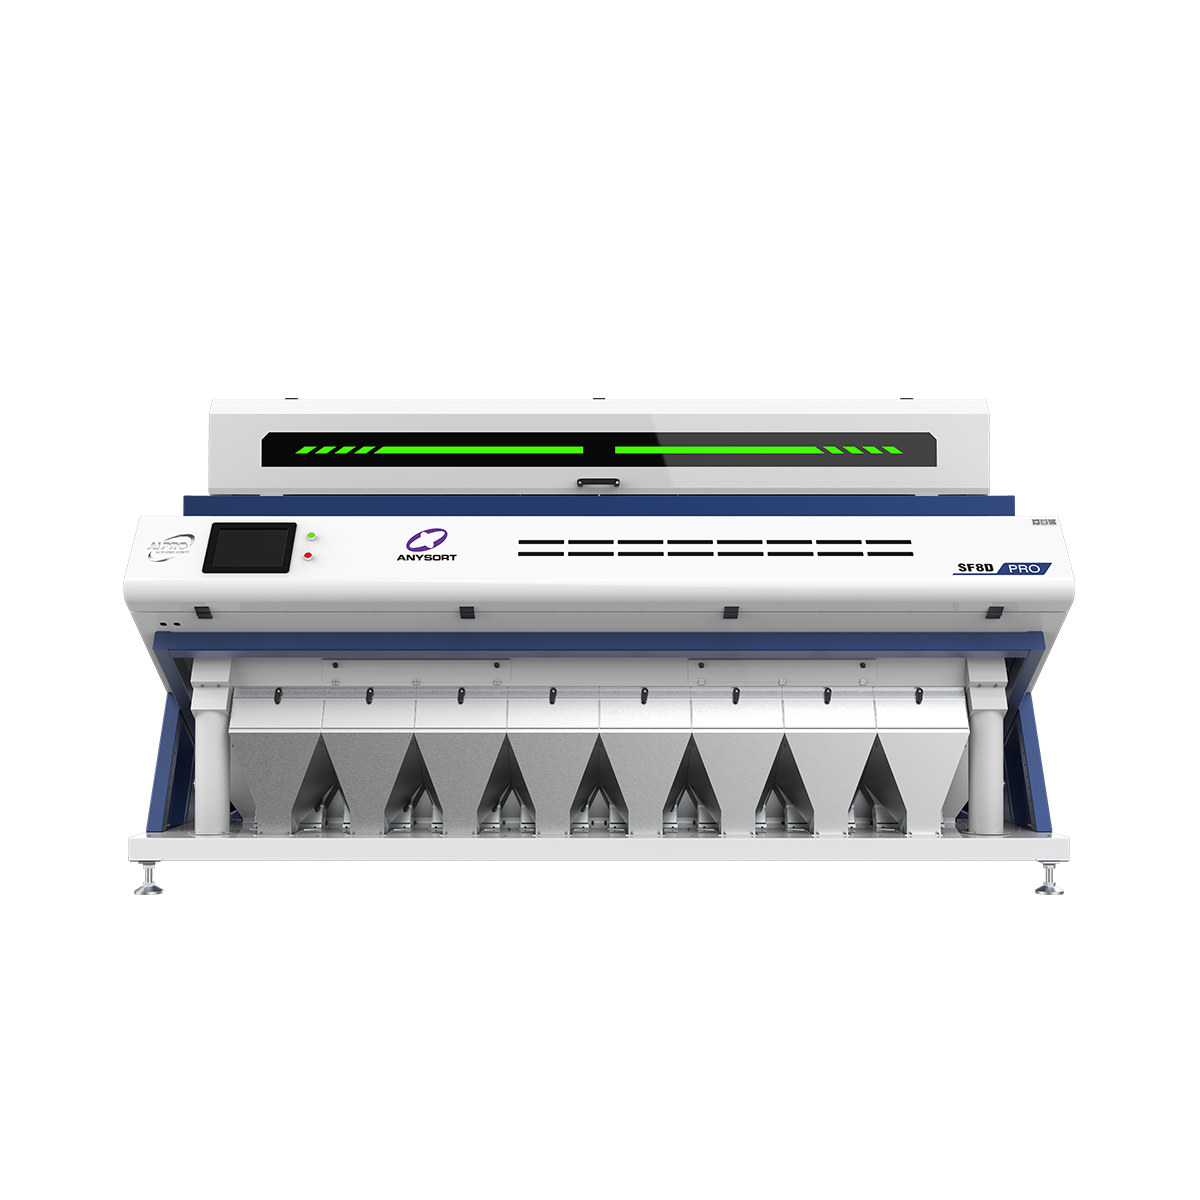
A color sorting machine is an advanced optical inspection system designed to automatically separate and categorize materials based on their color properties. This sophisticated equipment uses high-resolution cameras and artificial intelligence algorithms to identify color variations in products ranging from agricultural commodities to recycled materials. The color sorting machine operates by passing materials through a detection zone where sensors capture detailed color information, then pneumatic ejectors remove items that don't meet specified color standards.
The core technology behind a color sorting machine involves multiple sensor arrays working in conjunction with powerful processing units. These systems can analyze thousands of items per second, making real-time sorting decisions based on pre-programmed color parameters. Modern color sorting machines feature adjustable sensitivity settings, allowing operators to customize sorting precision for different applications and material types.
Key technological features include LED lighting systems that ensure consistent illumination, high-speed camera technology for accurate color detection, and sophisticated software interfaces for easy programming. The color sorting machine integrates seamlessly into existing production lines, offering both offline and online sorting capabilities. Applications span across diverse industries including food processing, agriculture, recycling, mining, and plastic manufacturing. Whether processing grains, rice, coffee beans, or plastic pellets, the color sorting machine delivers consistent, reliable results that improve product quality and reduce manual labor requirements significantly.

 EN