Rice Sorting Machine - Advanced Grain Quality Solutions

All Categories

rice sorting machine

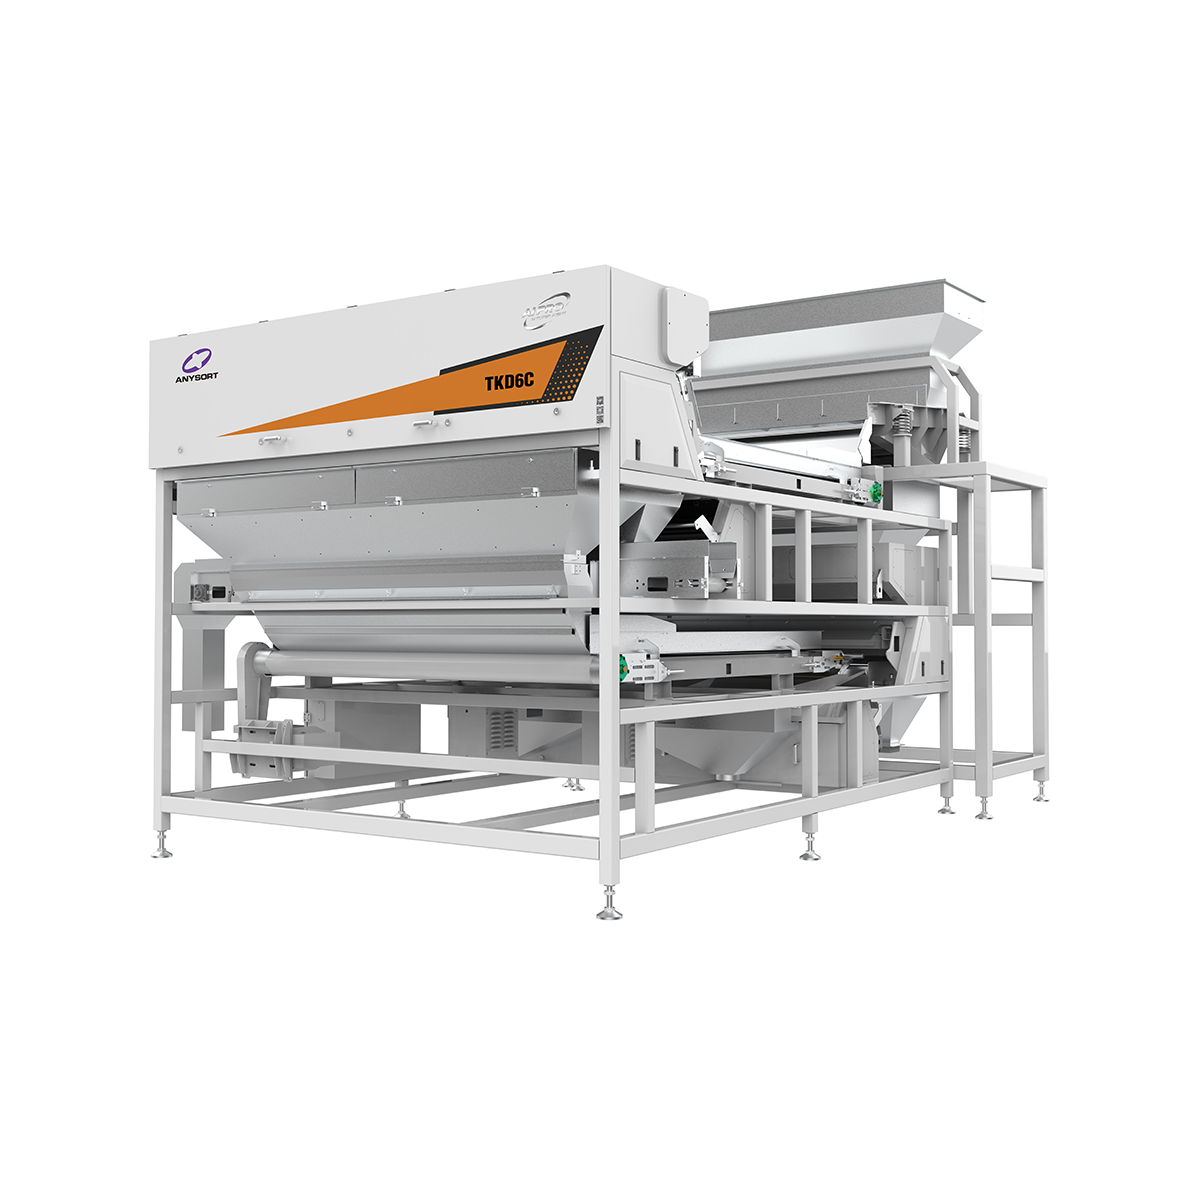
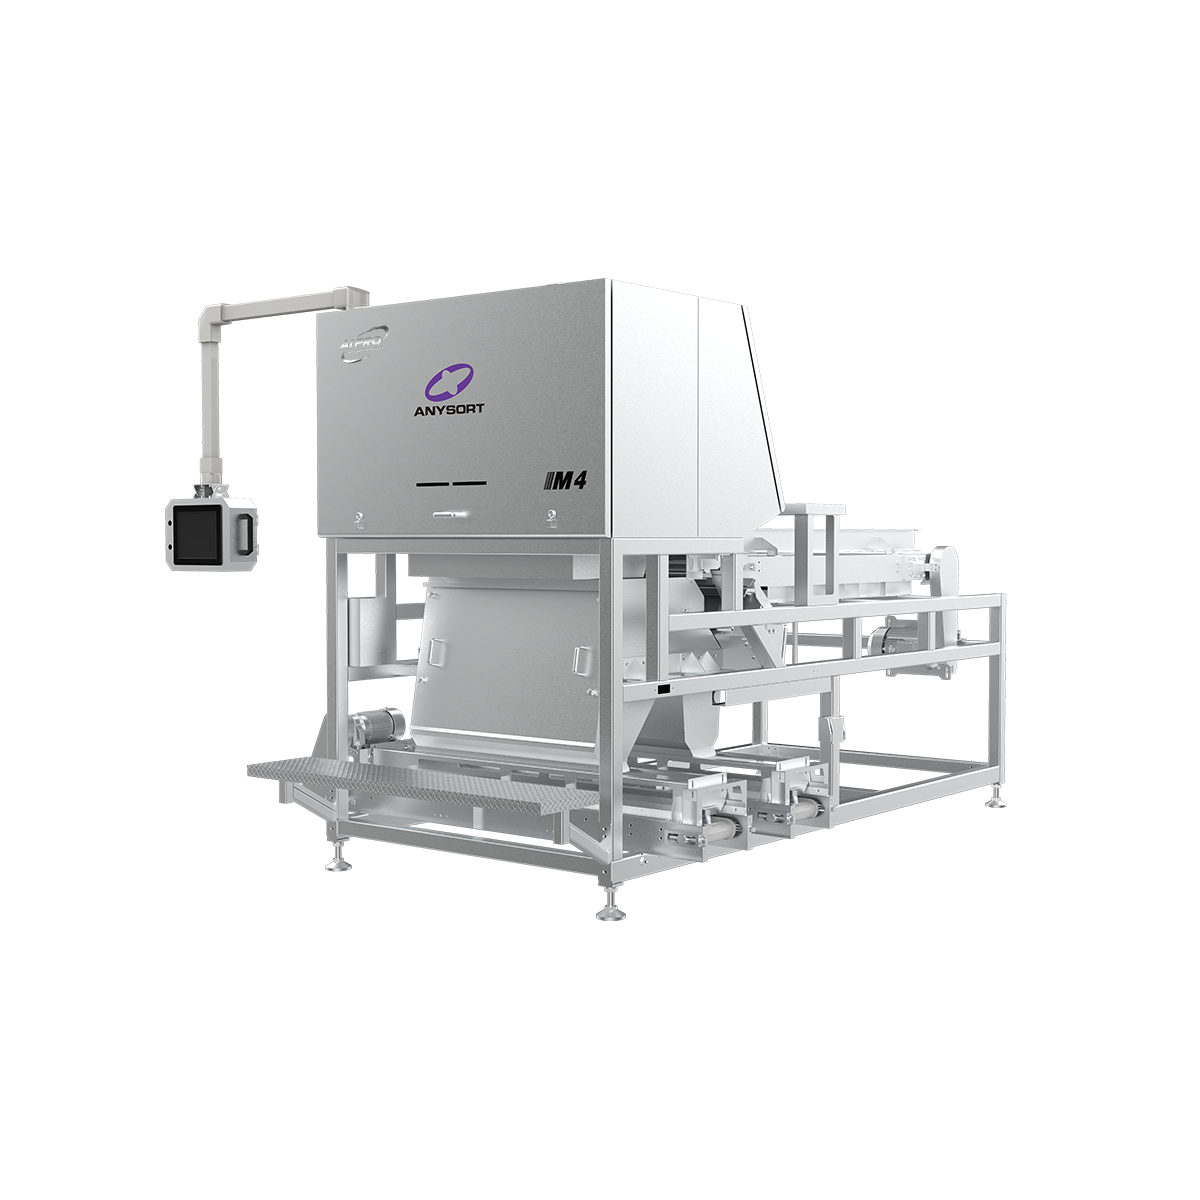
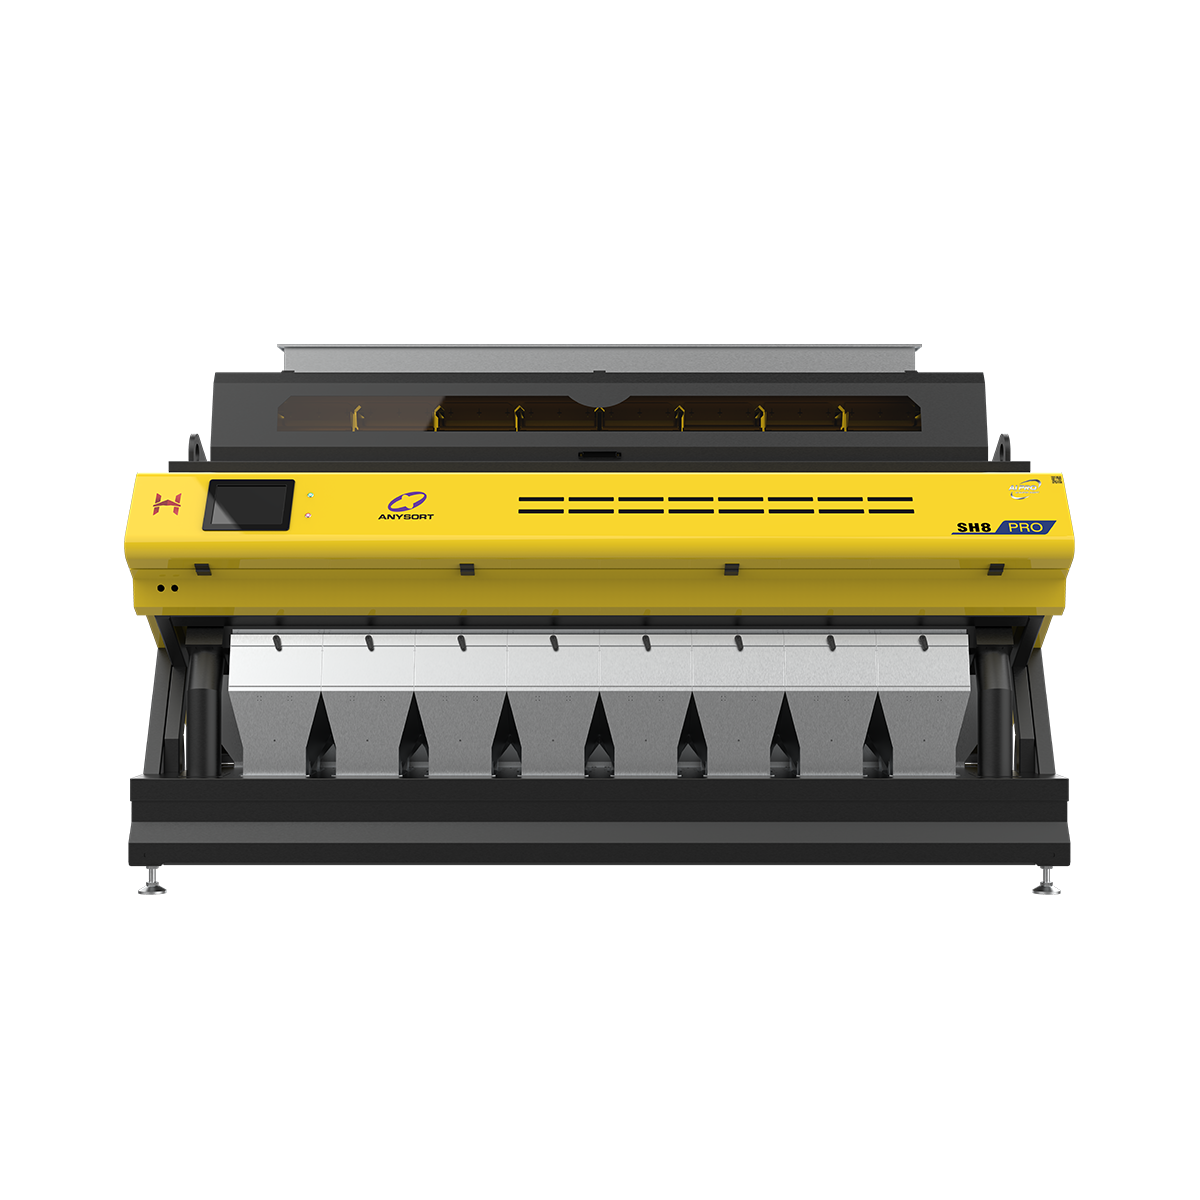
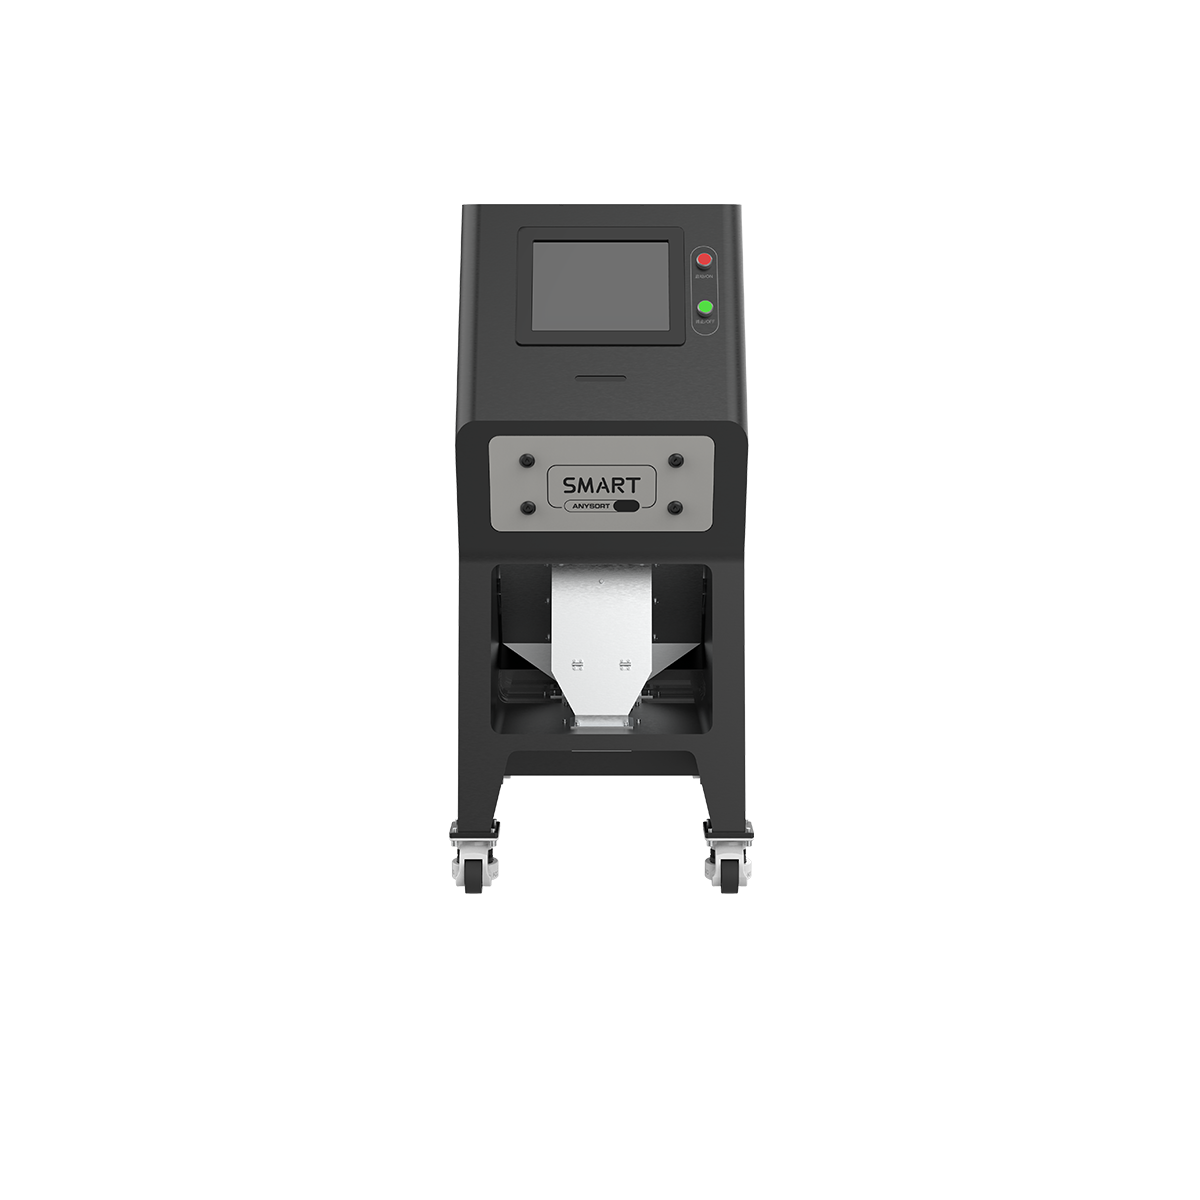
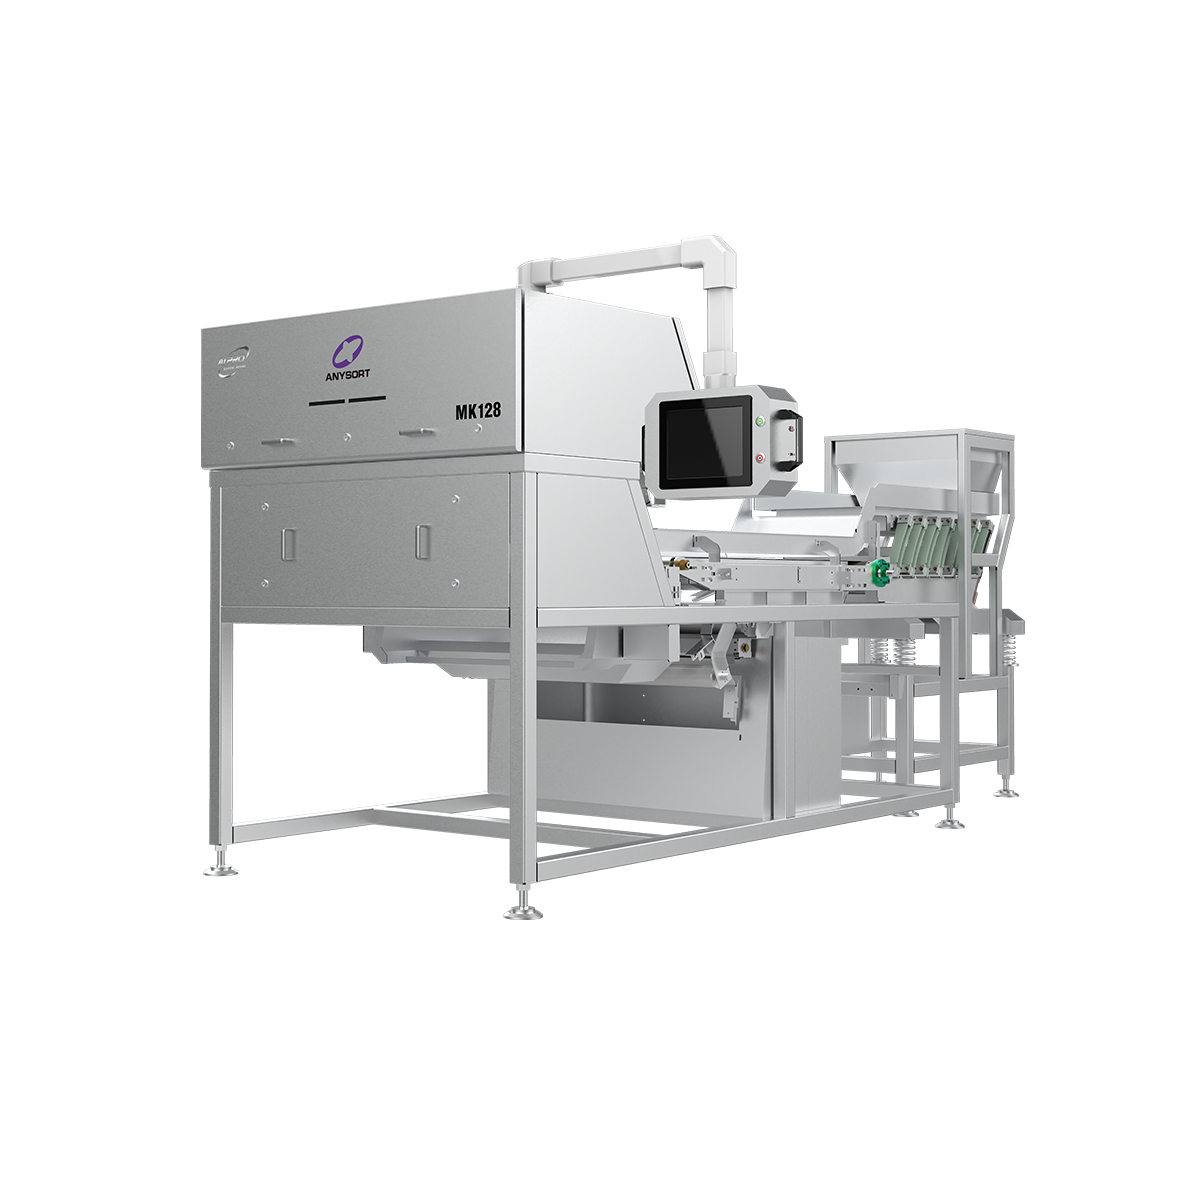
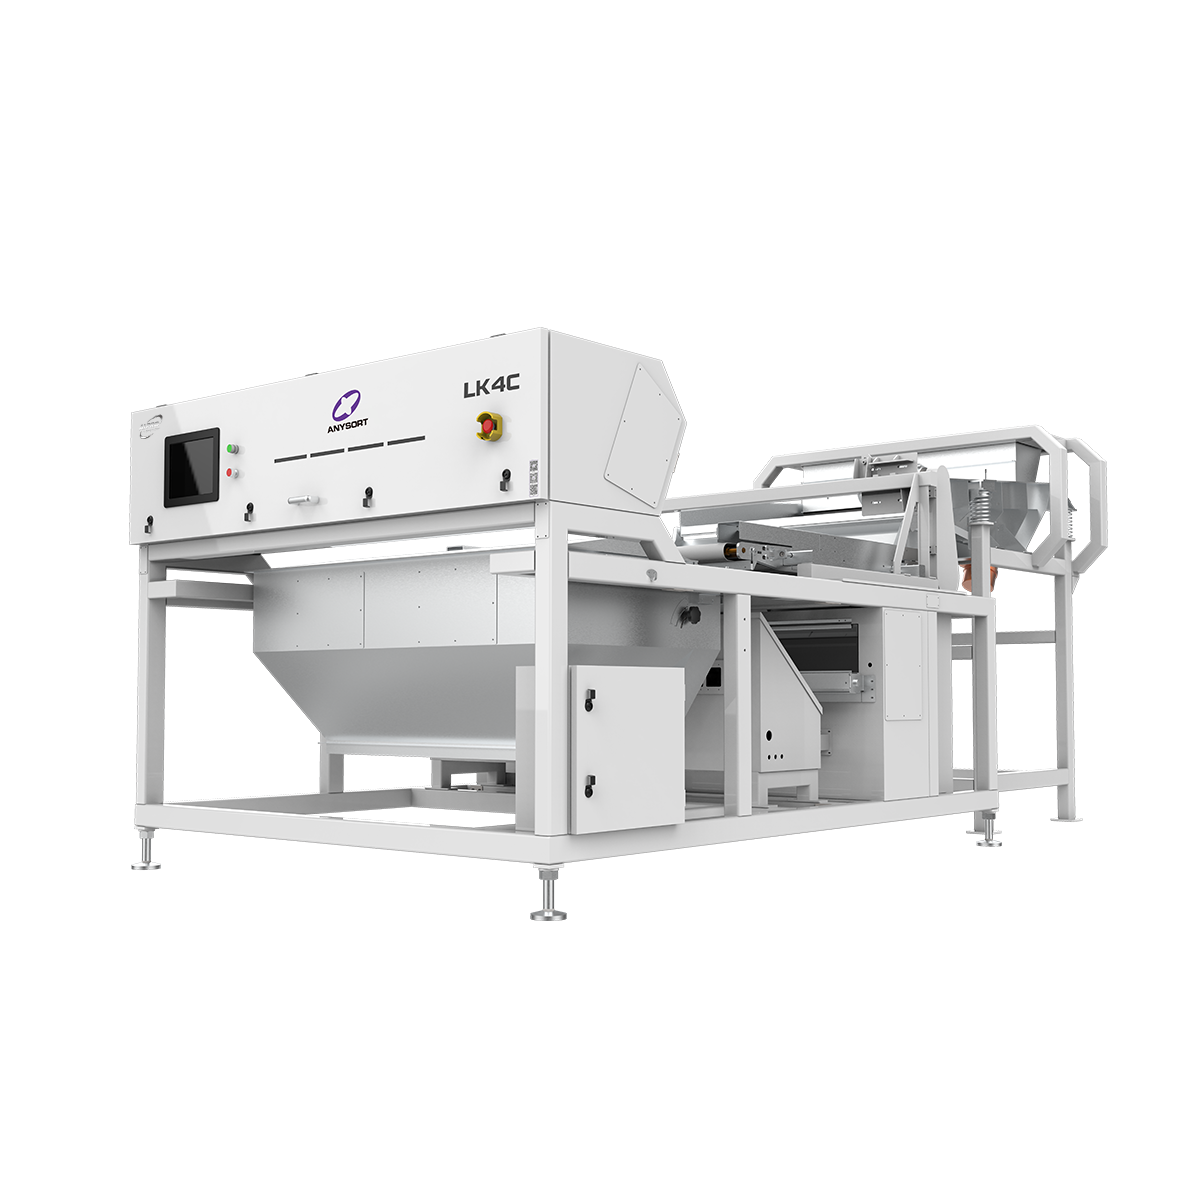
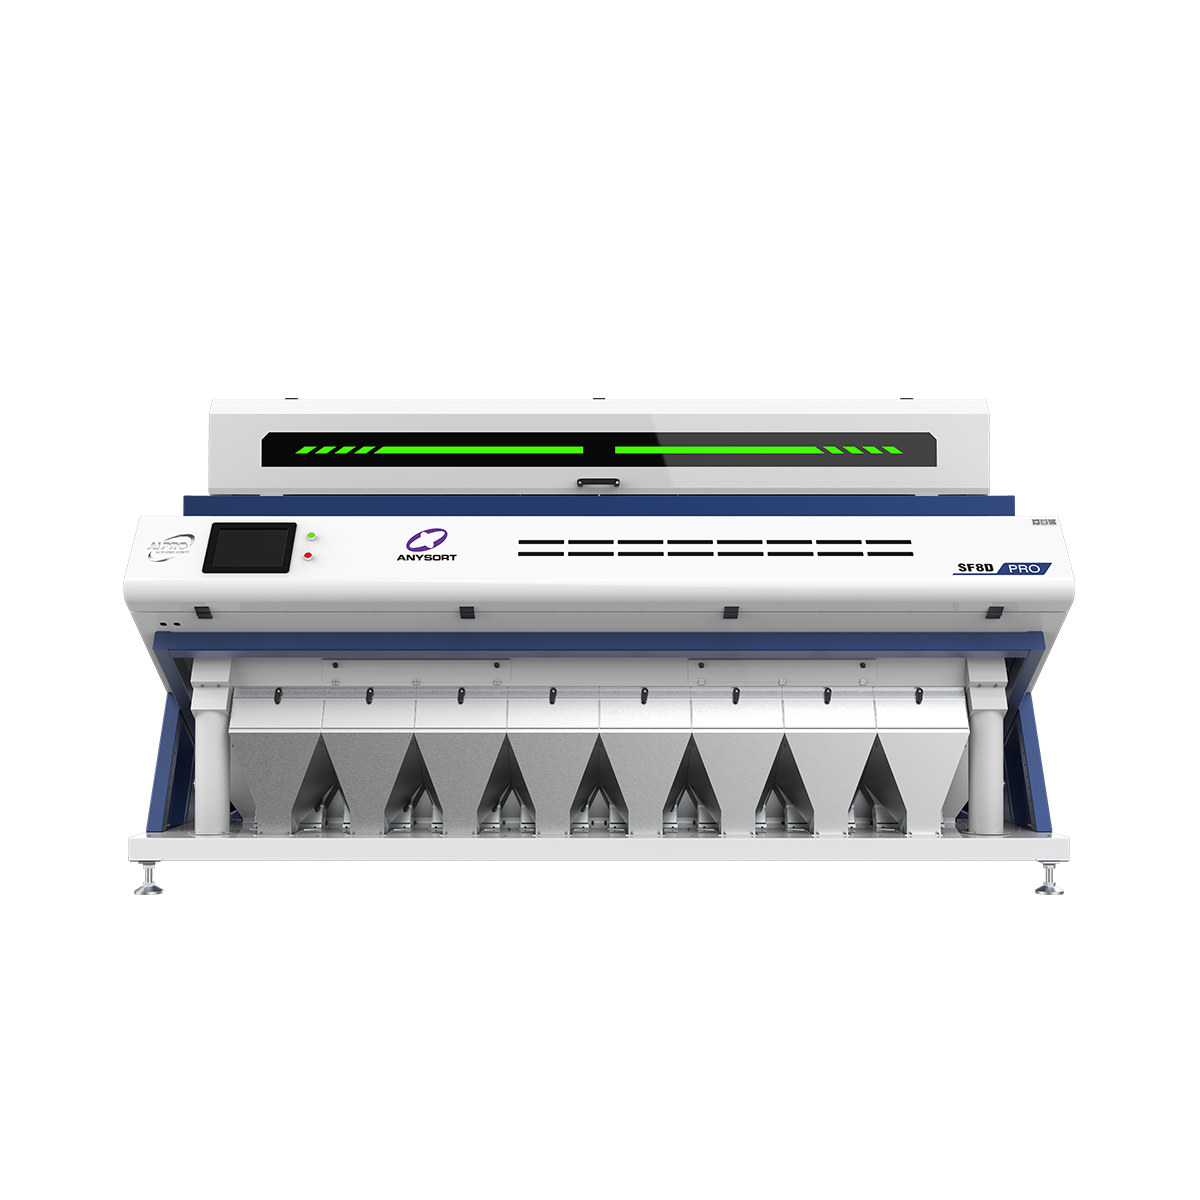
A rice sorting machine is an advanced technological solution designed to automatically separate and grade rice kernels based on quality, color, size, and defects. This machine uses sophisticated optical sensing technology combined with artificial intelligence to inspect thousands of rice grains per minute, ensuring consistent quality in rice processing operations. The rice sorting machine employs high-speed cameras and precision air-jet systems to remove discolored, broken, or foreign particles from rice batches with exceptional accuracy. Modern rice sorting machines feature multi-channel sorting capabilities, allowing simultaneous processing of different rice varieties without cross-contamination. The primary functions include detection of damaged kernels, removal of foreign materials, elimination of stones and debris, and separation of rice by size and color specifications. Advanced rice sorting machine models integrate machine learning algorithms that continuously improve detection accuracy over time. These systems operate with minimal human intervention, significantly reducing labor costs while maintaining superior quality standards. The rice sorting machine technology has become essential in commercial rice mills and processing facilities worldwide, helping producers meet strict international quality requirements and consumer expectations for premium rice products.

Popular Products

The rice sorting machine delivers substantial practical benefits that directly enhance your rice processing operations and profitability. First, this machine dramatically improves product quality by removing defective grains, foreign materials, and discolored kernels that would otherwise damage your brand reputation. Your customers receive consistently premium rice that meets their expectations, leading to increased loyalty and repeat purchases. The rice sorting machine operates at high throughput capacity, processing large quantities of rice daily while maintaining exceptional accuracy that manual sorting simply cannot achieve. This operational efficiency reduces processing time significantly, allowing you to handle more rice with fewer staff members, thereby lowering your labor expenses substantially. The investment in a rice sorting machine quickly pays for itself through reduced waste and improved yield rates, as more saleable rice reaches market rather than being discarded. Additionally, this equipment enables you to compete effectively in premium rice markets where quality standards are stringent and uncompromising. The rice sorting machine also provides consistent results across all batches, eliminating human error and variability that comes with manual sorting methods. For export markets especially, having certified quality through automated sorting gives you competitive advantages and opens doors to higher-value contracts. Furthermore, operating a rice sorting machine positions your business as a modern, technology-driven facility, enhancing your market reputation and customer confidence in your products and processes.

Latest News

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

rice sorting machine

Advanced Optical Detection Technology

Advanced Optical Detection Technology

The rice sorting machine utilizes cutting-edge optical sensor technology that captures detailed images of every single grain passing through the system. Using multiple wavelengths and high-resolution cameras, the rice sorting machine identifies even the smallest defects, discolorations, and irregularities that human eyes might miss. This sophisticated detection capability ensures that only premium-quality rice reaches your customers, protecting your brand reputation and maintaining consumer satisfaction. The machine's sensors work in conjunction with intelligent software algorithms that analyze grain characteristics in real-time, making split-second decisions about which kernels to retain and which to reject. By employing this advanced technology, your rice sorting machine achieves accuracy rates exceeding ninety-five percent, significantly outperforming traditional manual sorting methods.
High-Capacity Processing Performance

High-Capacity Processing Performance

A modern rice sorting machine handles enormous volumes of rice efficiently, processing between five to fifteen tons per hour depending on the specific model and grain size. This exceptional throughput capacity means your facility can process significantly more rice daily without requiring proportional increases in labor or facility expansion. The rice sorting machine maintains consistent performance throughout extended operational periods, delivering reliable results shift after shift without fatigue or concentration lapses. The machine's design optimizes material flow through multiple sorting channels simultaneously, maximizing efficiency while minimizing product damage. By investing in a rice sorting machine with high-capacity capabilities, you transform your processing operations into a lean, efficient system that maximizes profitability while meeting growing market demands for quality rice products.
Cost-Effective Quality Assurance Solution

Cost-Effective Quality Assurance Solution

Implementing a rice sorting machine substantially reduces your operational costs while dramatically improving output quality and market competitiveness. This equipment eliminates the need for large teams of manual sorters, directly reducing your payroll expenses and associated employment costs. The rice sorting machine minimizes product waste by accurately identifying and removing only genuinely defective grains, maximizing the percentage of your rice harvest that reaches profitable markets. Your facility experiences faster processing times and higher throughput, generating greater revenue per operational hour. The rice sorting machine delivers return on investment through improved yield rates and premium pricing opportunities for higher-quality products. Additionally, reduced labor requirements mean fewer training expenses and less management overhead related to personnel supervision and quality control monitoring.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy