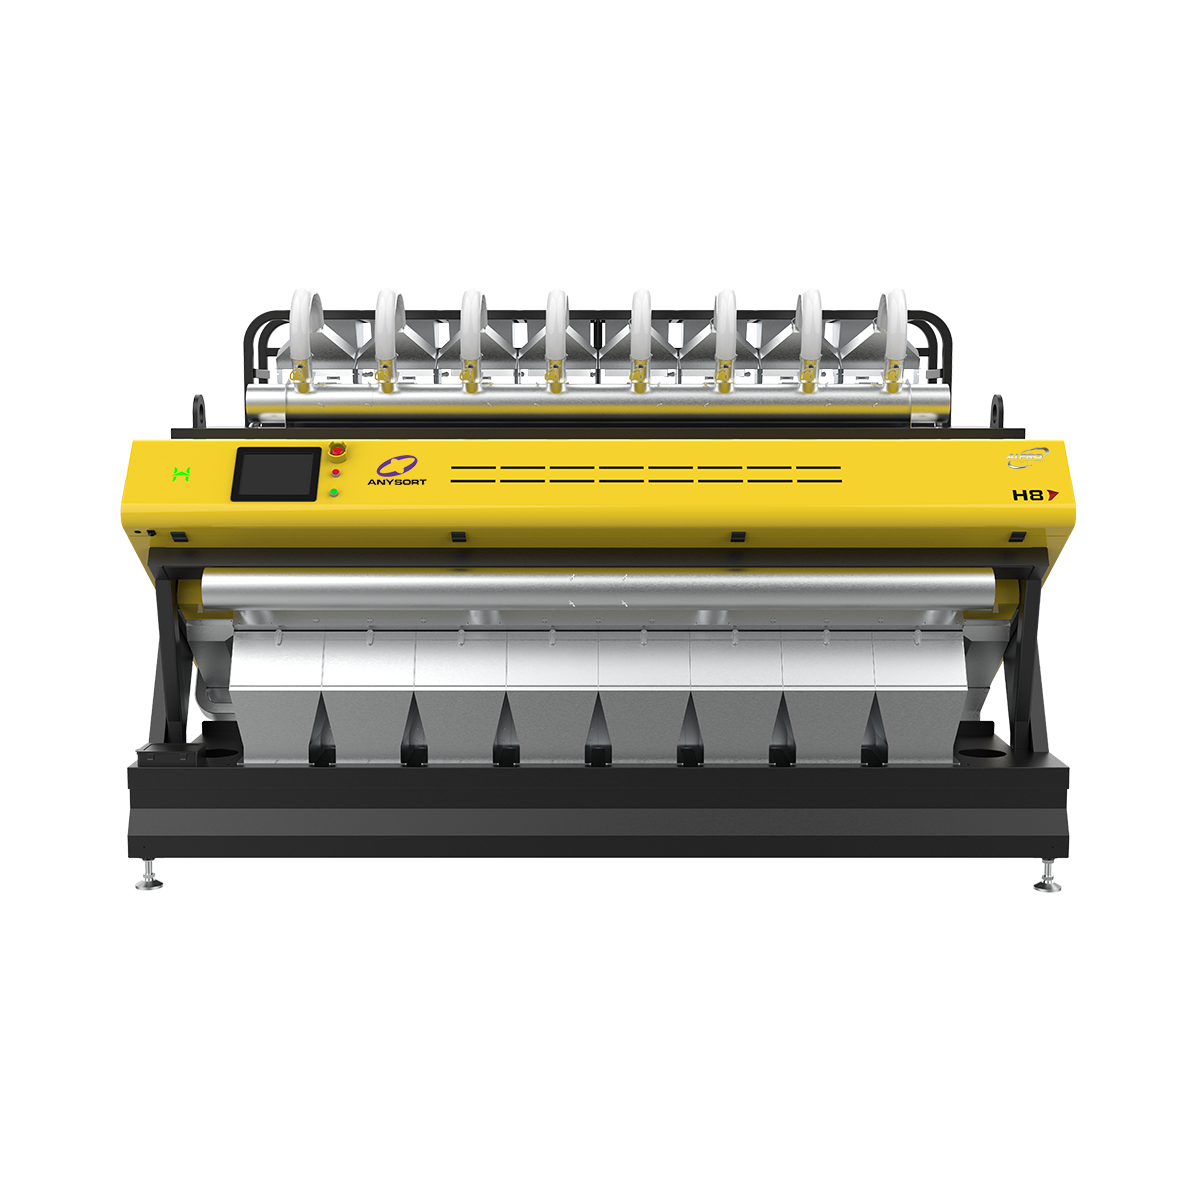
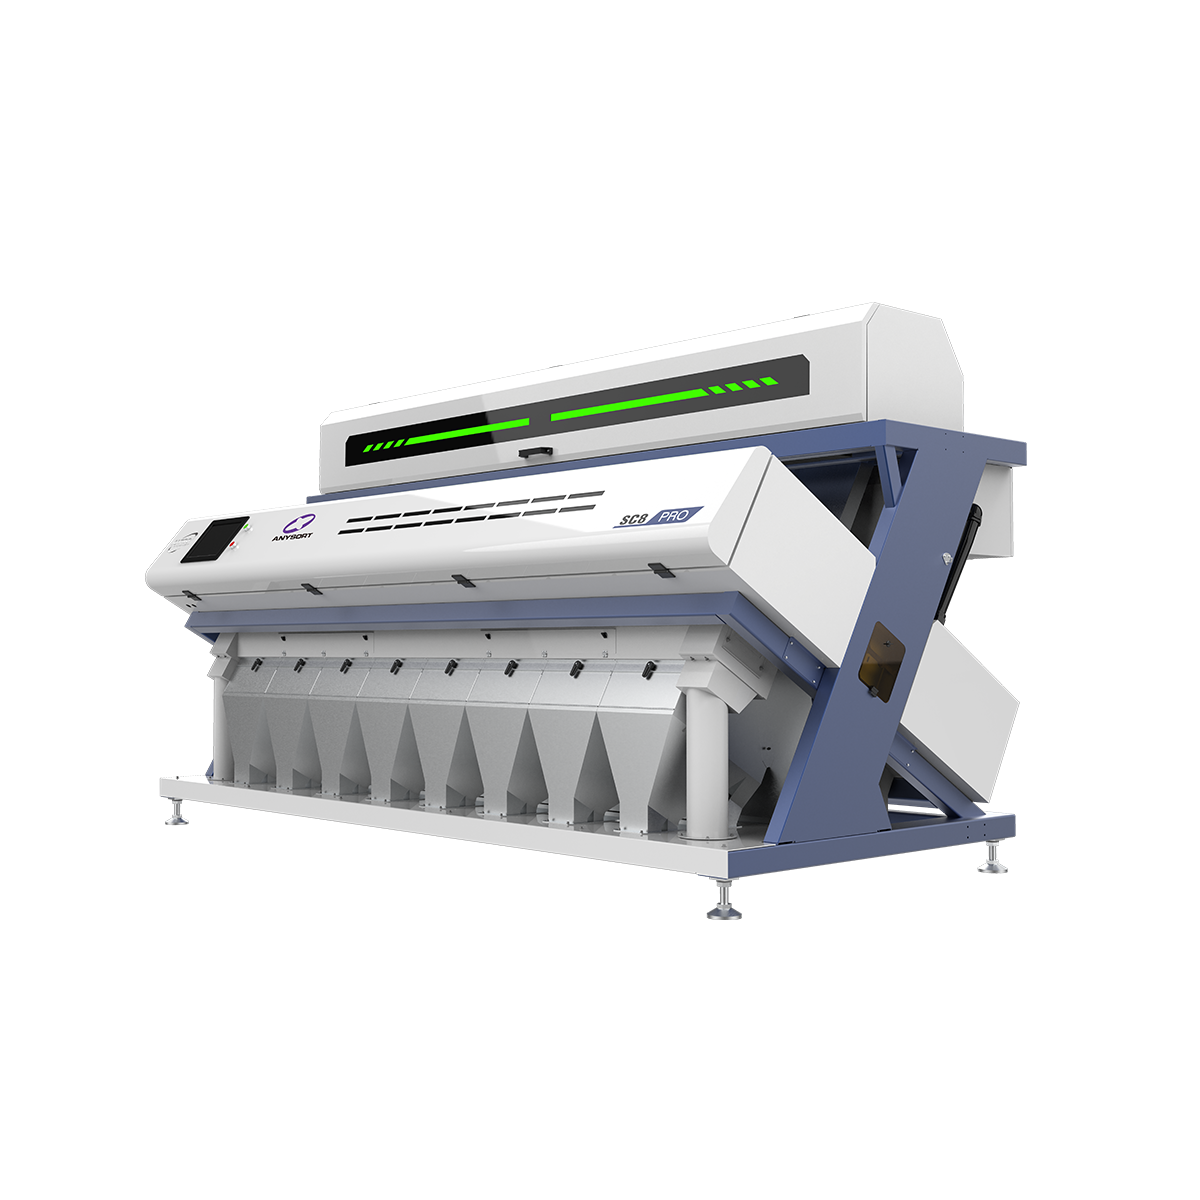
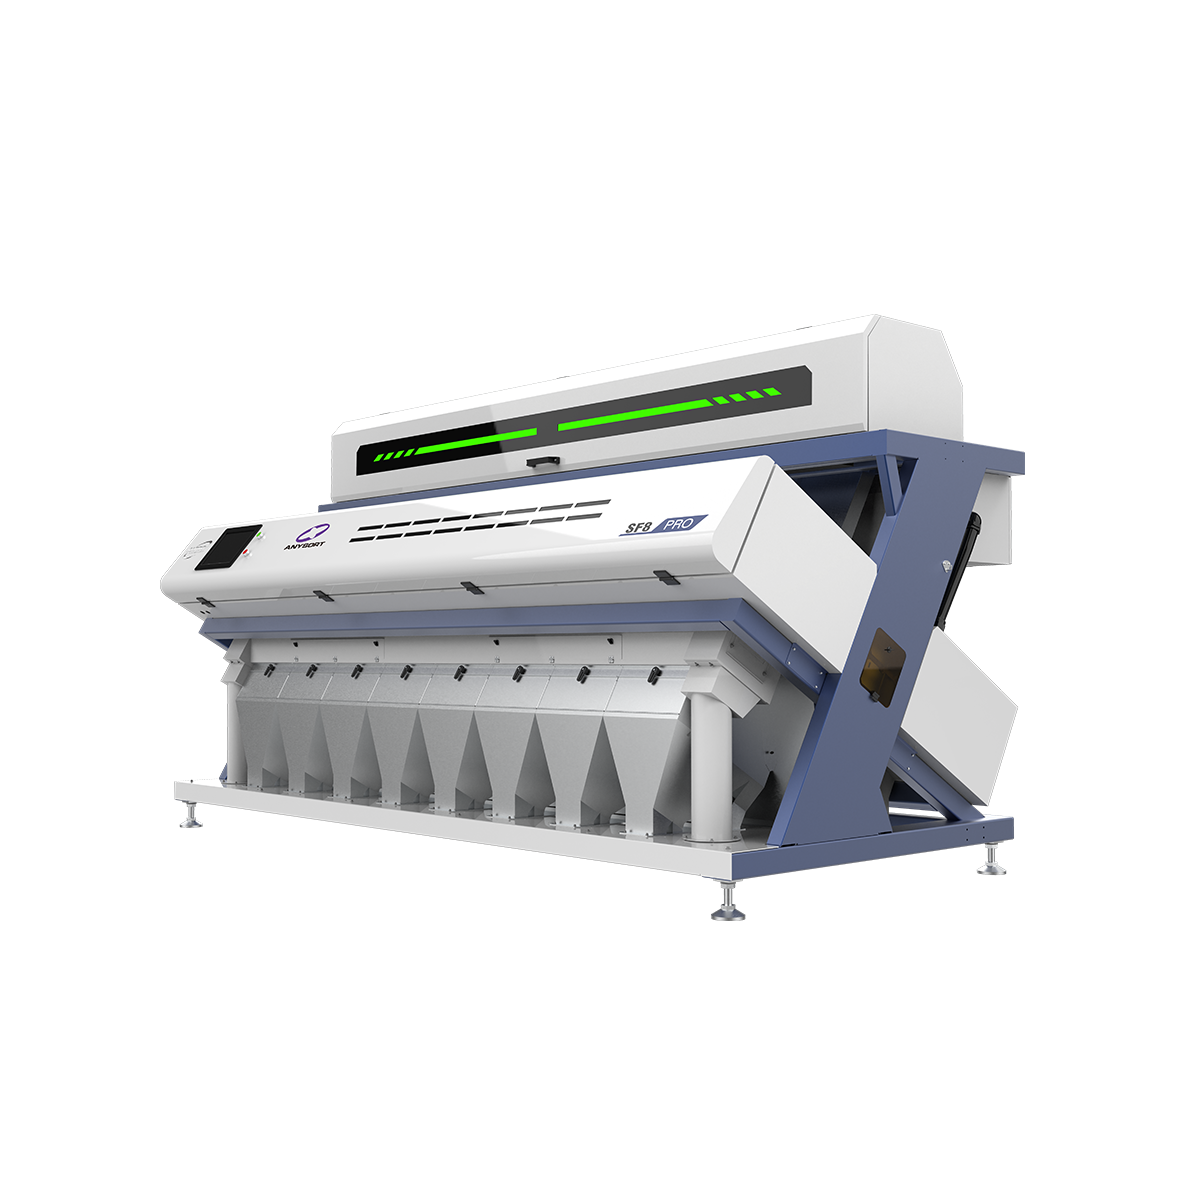
rice color sorting machine
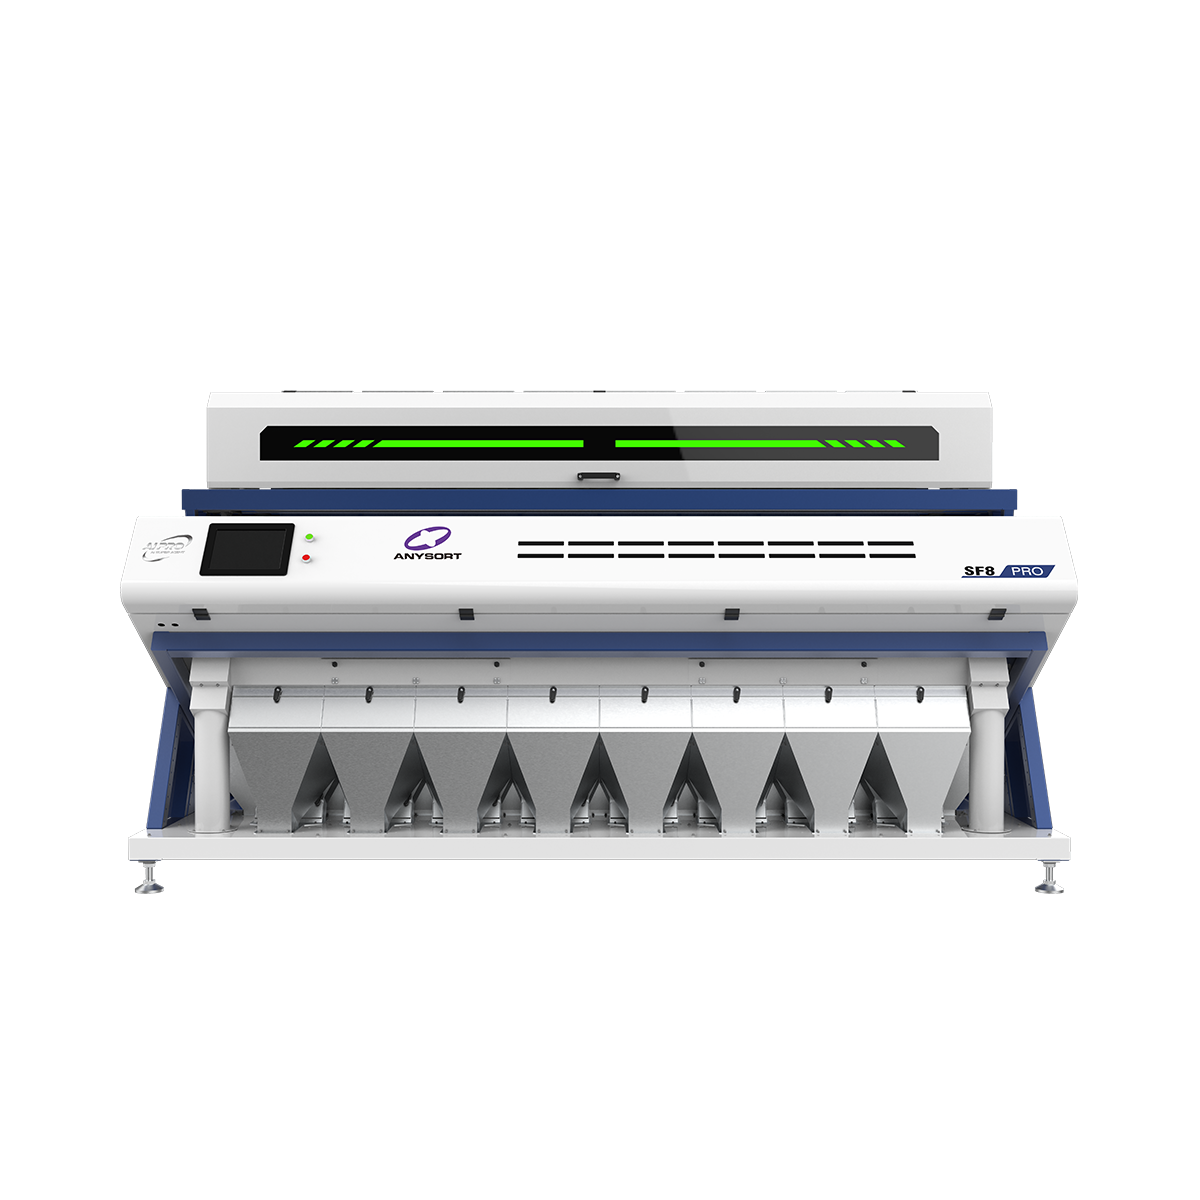
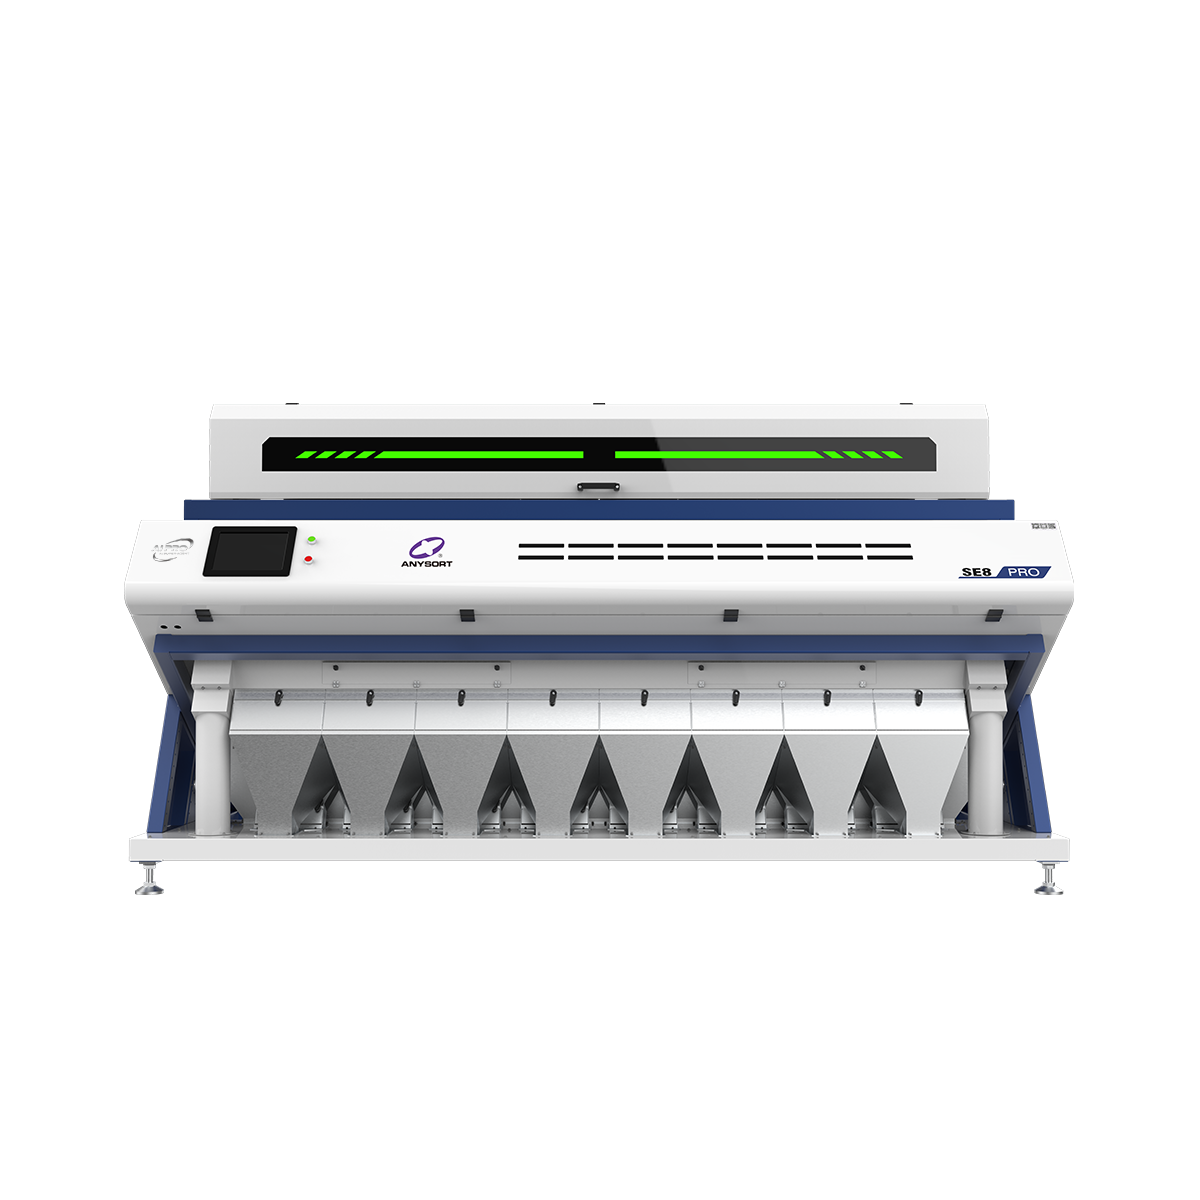
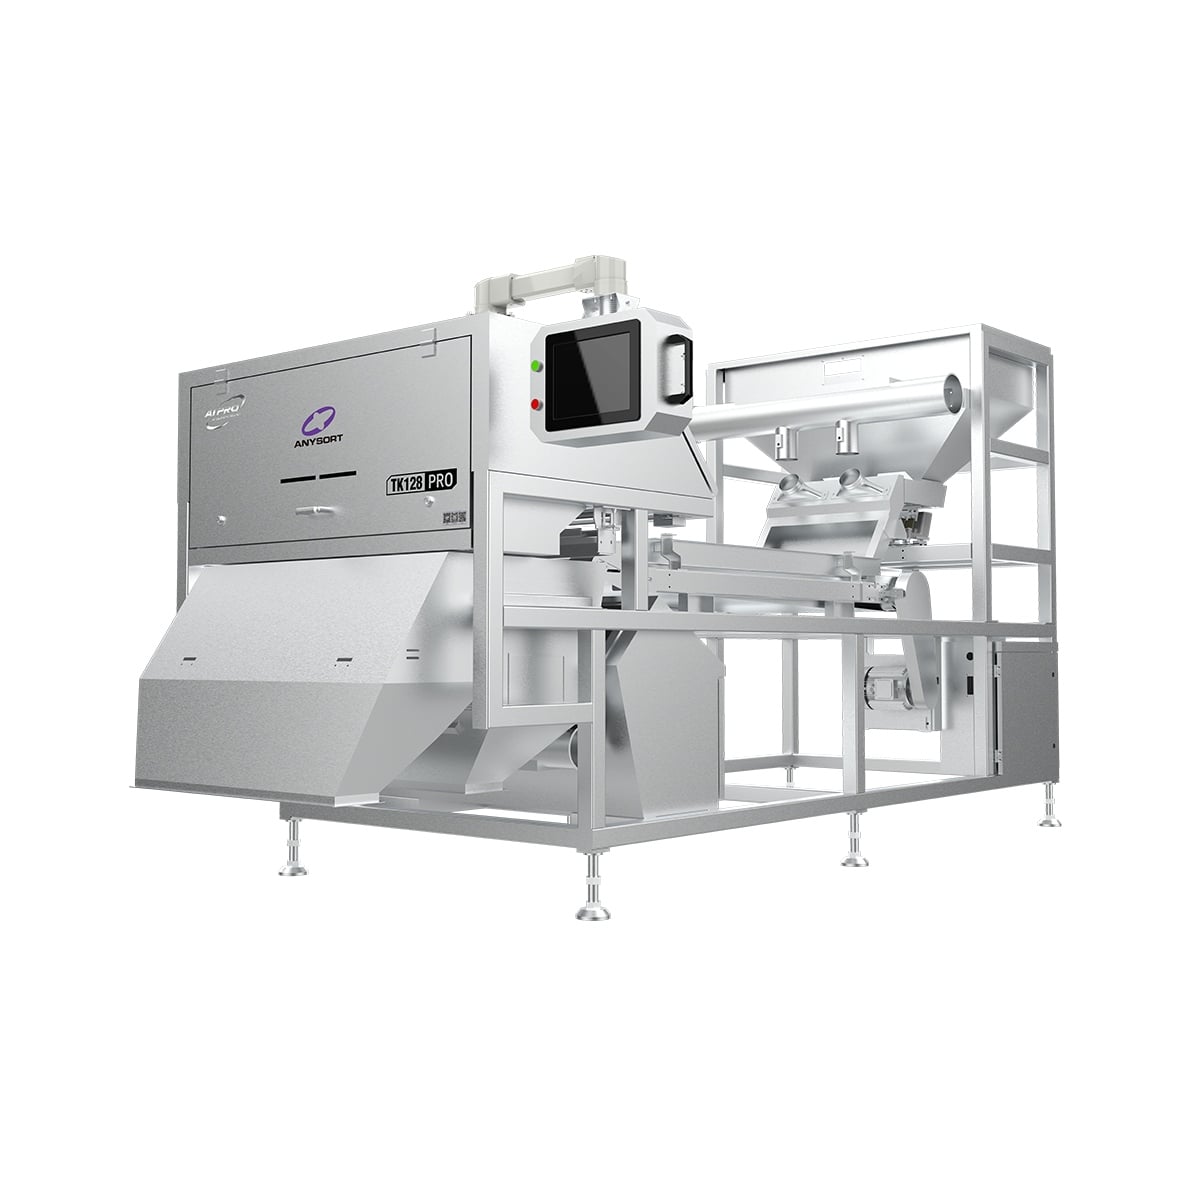
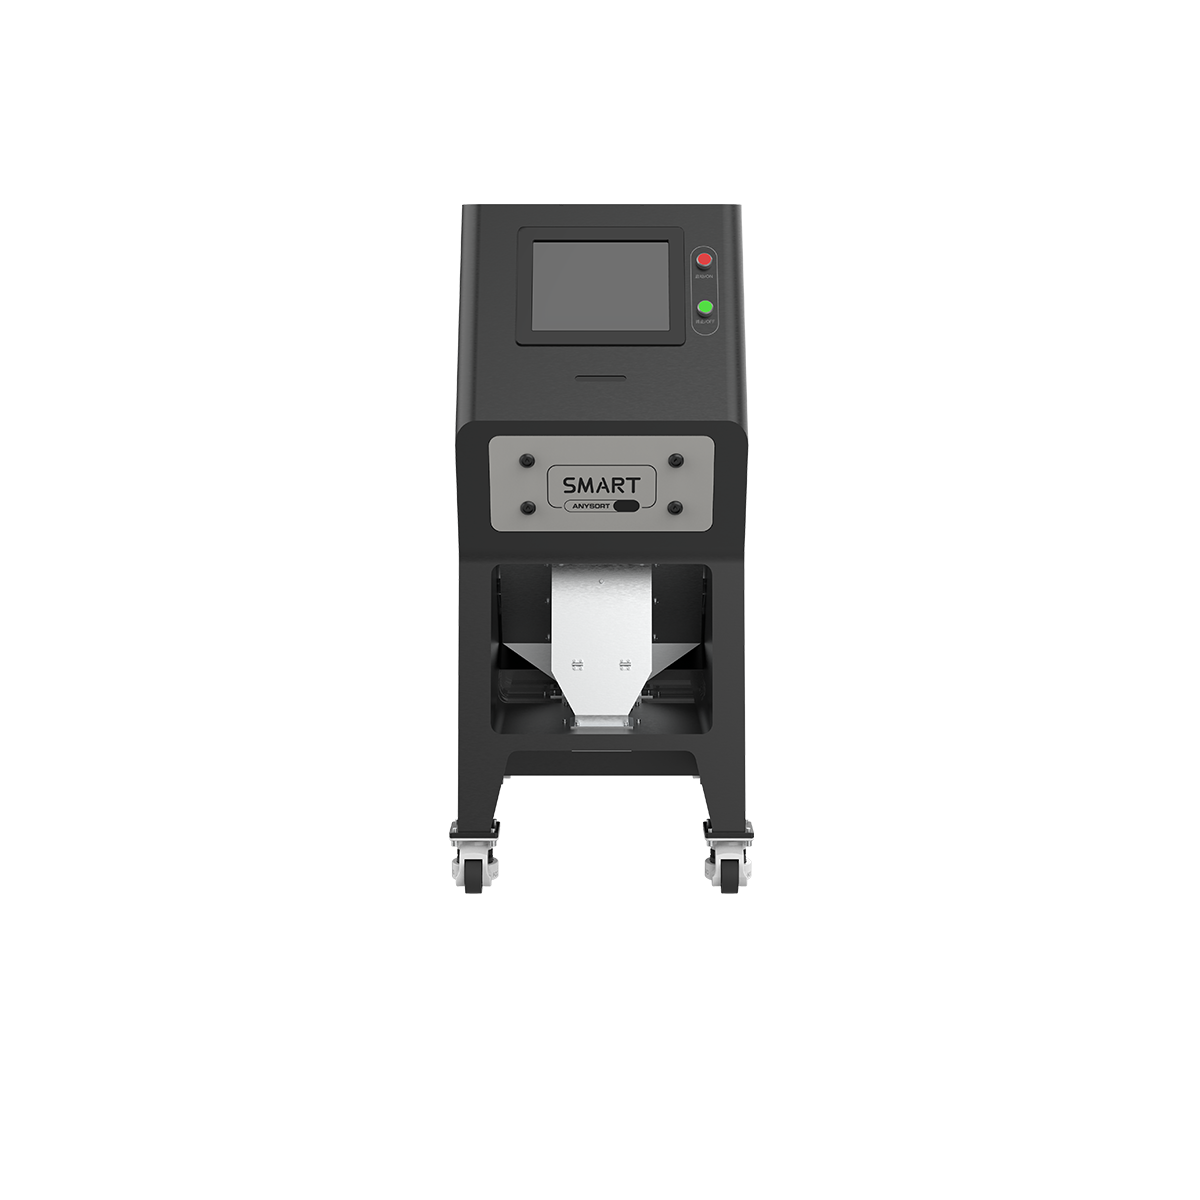
A rice color sorting machine is an advanced automated system designed to separate and grade rice grains based on their color and quality characteristics. This innovative rice color sorting machine utilizes cutting-edge optical sensing technology to identify and remove discolored, damaged, or foreign grains from the rice batch with remarkable precision. The rice color sorting machine operates by passing rice grains through high-speed cameras equipped with sophisticated image recognition algorithms that detect even minor color variations and impurities.
The primary function of a rice color sorting machine is to enhance the visual quality and commercial value of rice products. By eliminating yellow grains, black spots, and other defects, the rice color sorting machine ensures that only premium-grade rice reaches consumers. The technology behind this rice color sorting machine includes LED illumination systems, high-resolution imaging sensors, and artificial intelligence-powered analysis software that makes real-time sorting decisions.
Applications of the rice color sorting machine extend across various rice processing facilities, from small-scale operations to large industrial plants. The rice color sorting machine is particularly valuable in regions where rice production is significant, including Asia, where quality standards are increasingly stringent. Modern rice color sorting machine systems can process several tons of rice per hour while maintaining exceptional accuracy rates. These machines integrate seamlessly into existing production lines, enhancing overall efficiency and product consistency throughout the rice manufacturing process.

 EN