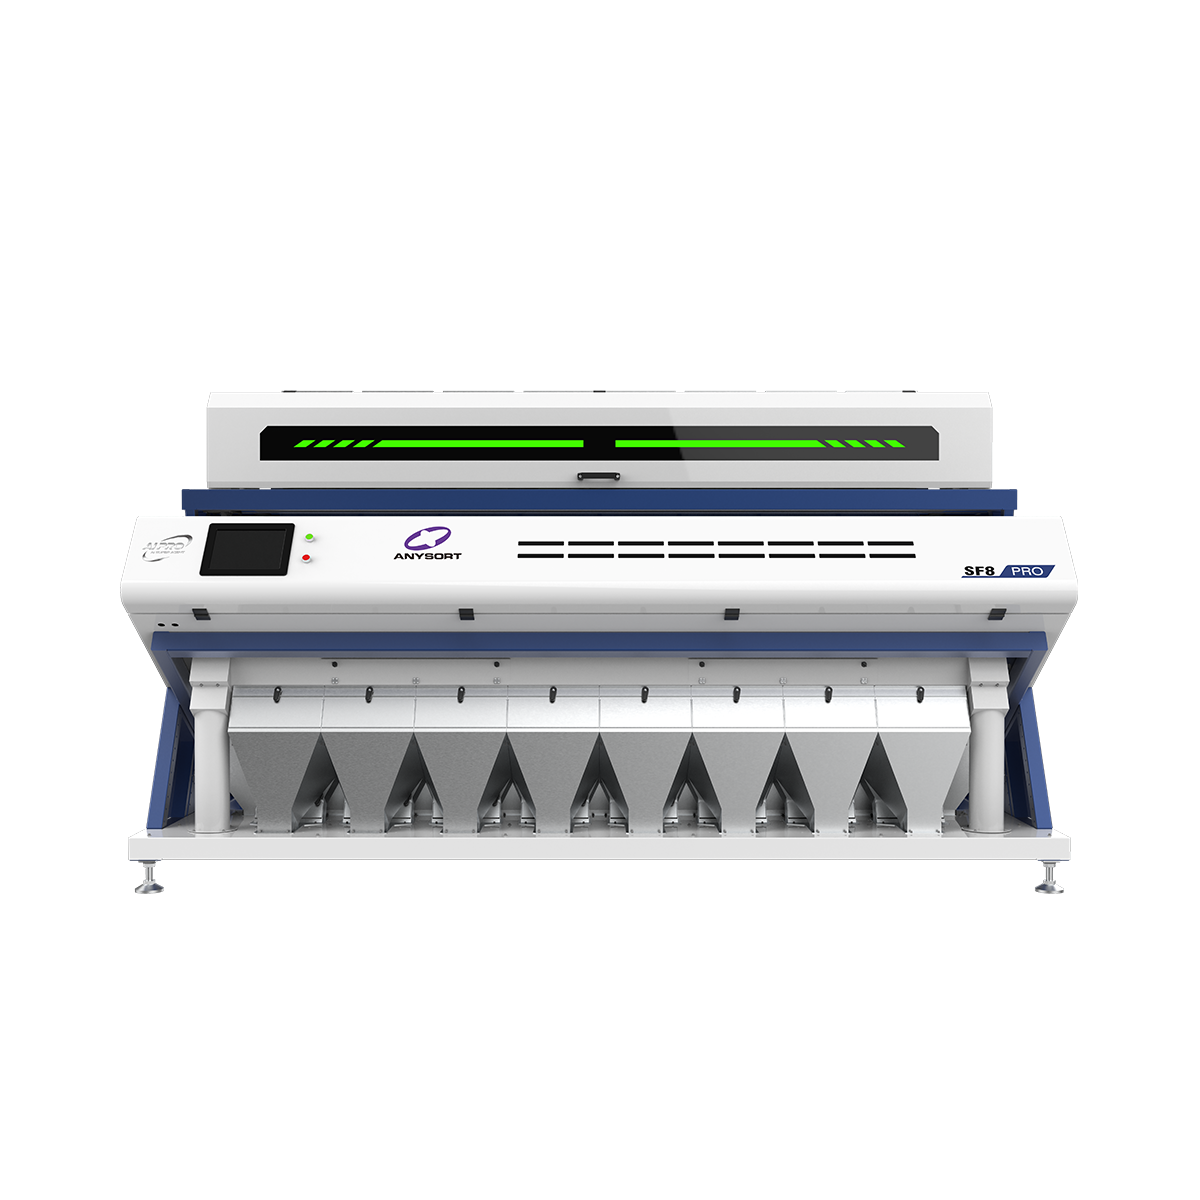
rice color sorter manufacturer
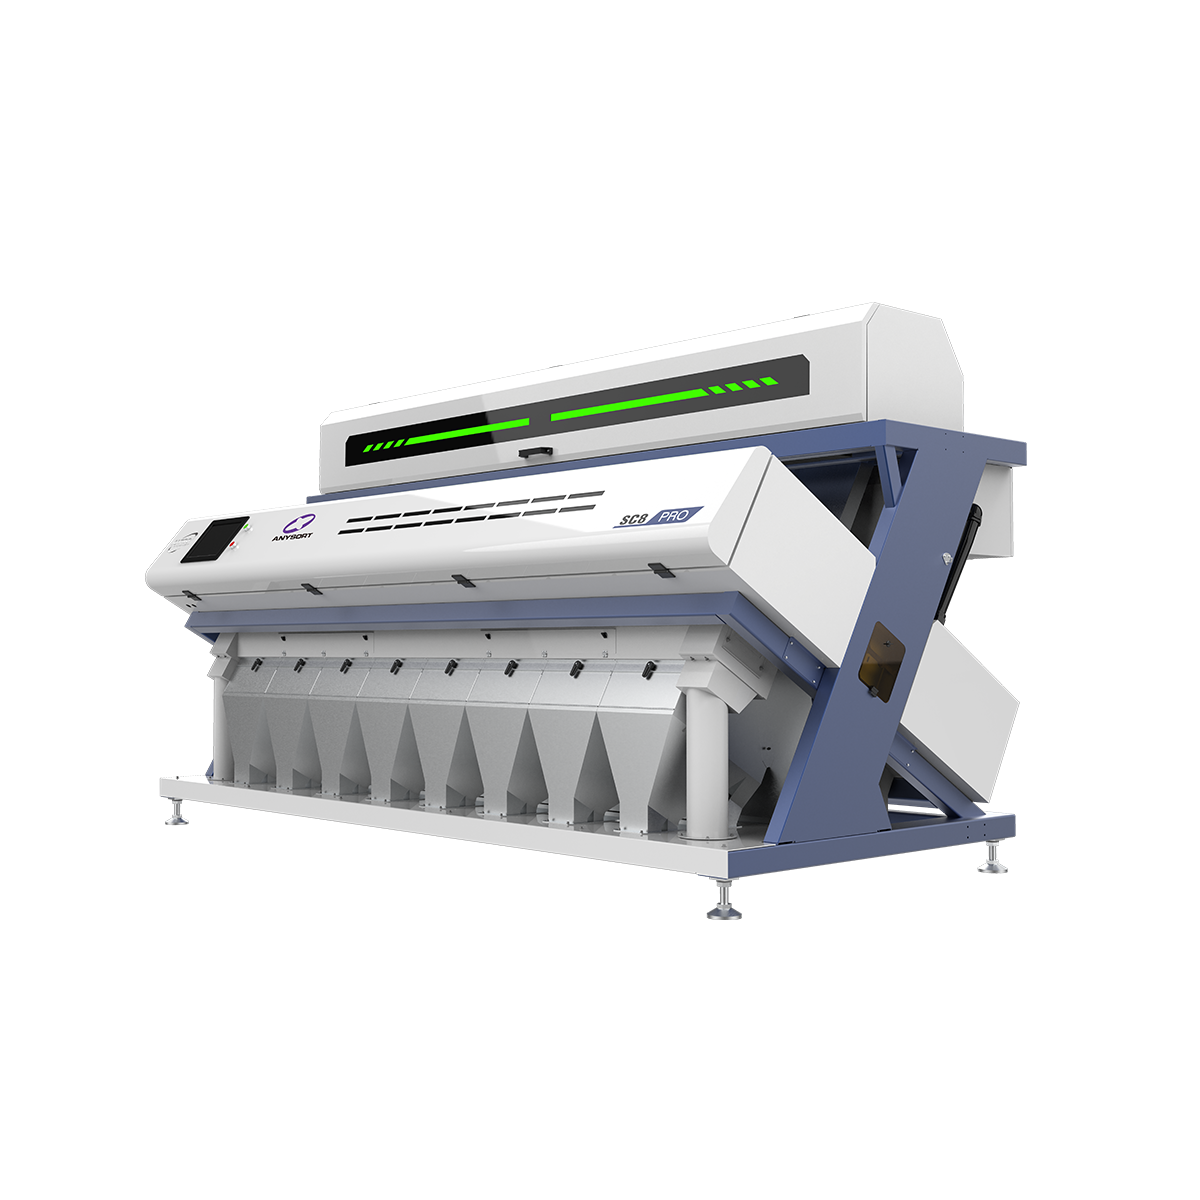
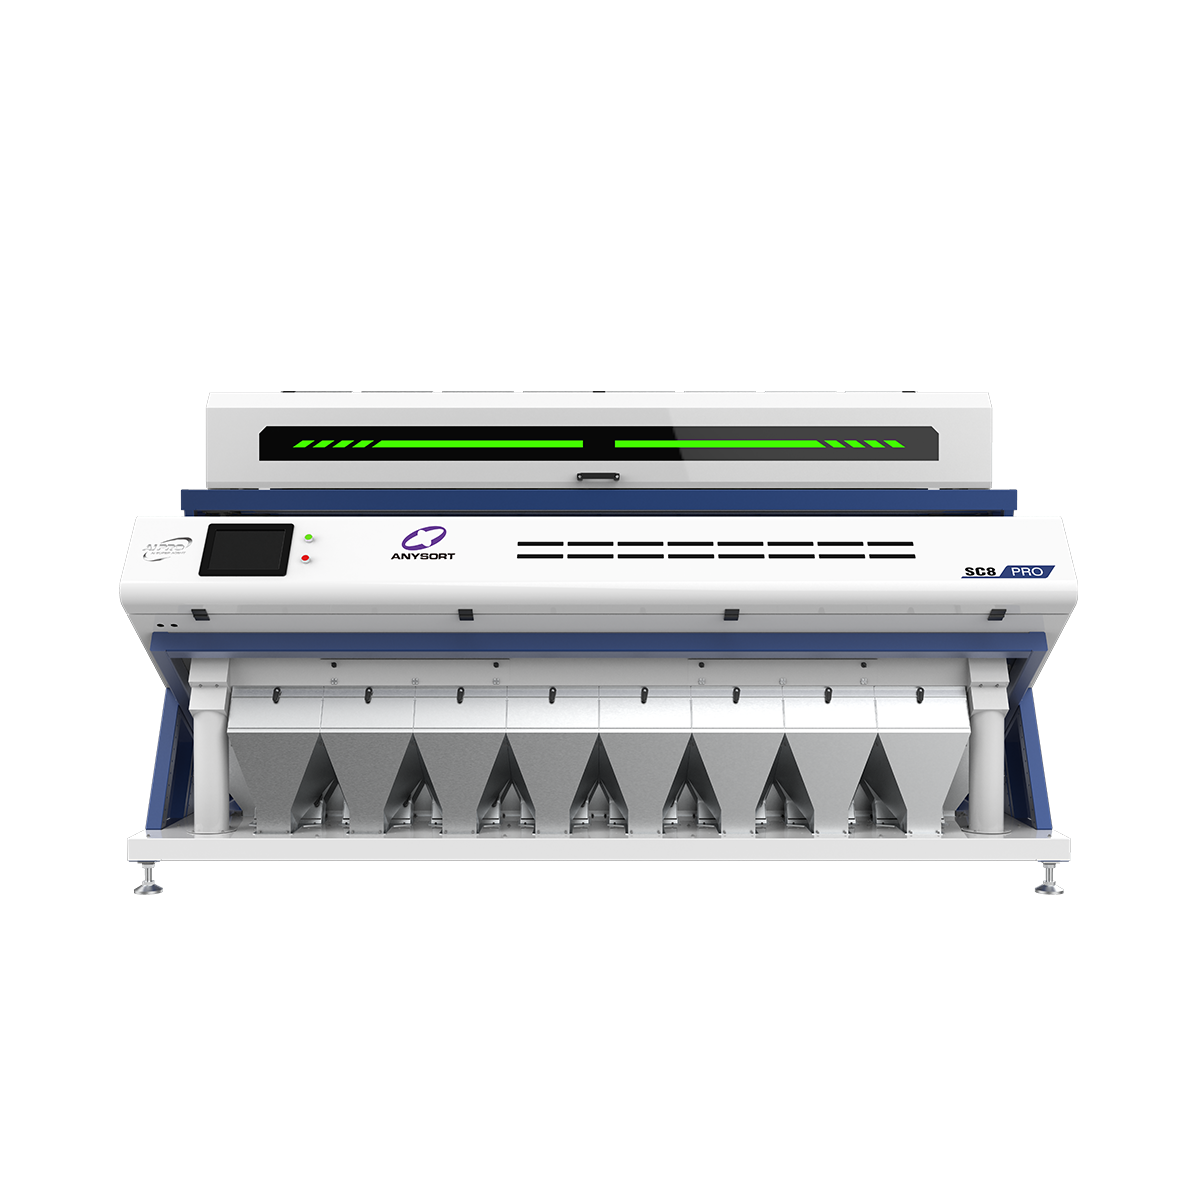
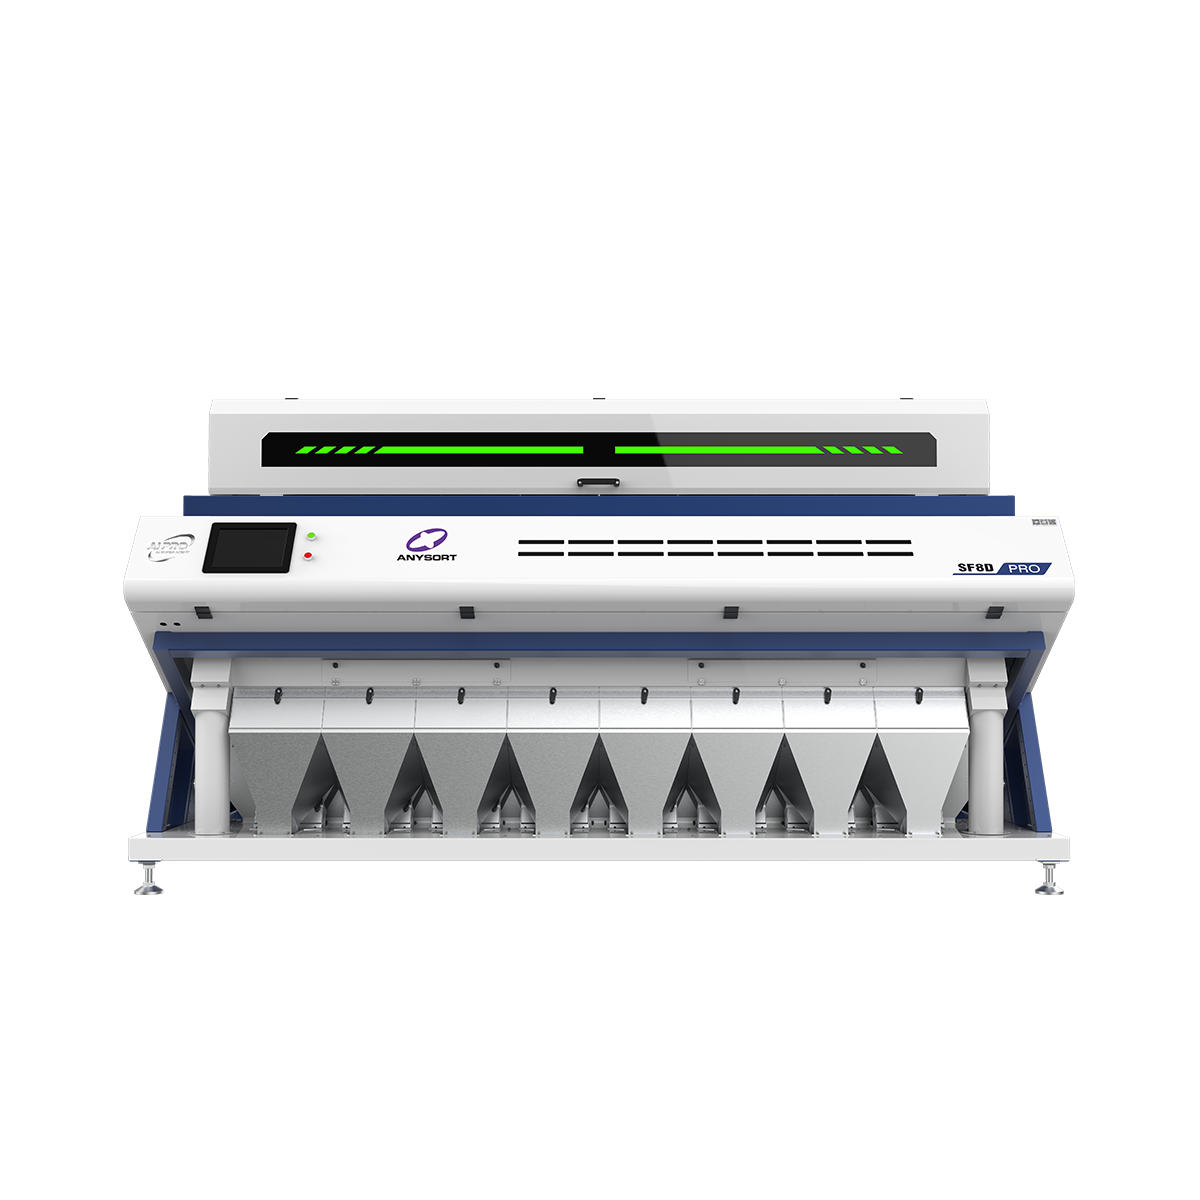
A rice color sorter manufacturer specializes in producing advanced optical sorting equipment designed to enhance grain quality and processing efficiency. These machines represent a crucial investment for rice mills, food processors, and agricultural operations worldwide. A professional rice color sorter manufacturer develops sorting systems that identify and remove discolored, damaged, and foreign materials from rice batches with exceptional precision.
The primary function of rice color sorter technology involves using high-resolution cameras and sophisticated artificial intelligence algorithms to analyze each grain individually. The rice color sorter manufacturer integrates multiple sensors that detect color variations, structural defects, and contamination instantly. This automated process ensures consistent quality output while dramatically reducing manual labor requirements.
Key technological features include advanced image processing systems, machine learning capabilities, and customizable sorting parameters. Modern rice color sorter manufacturer equipment operates at speeds exceeding 5 tons per hour, processing vast quantities without compromising accuracy. The systems feature intuitive interfaces, real-time monitoring dashboards, and comprehensive data logging for quality assurance.
Applications extend across diverse sectors including basmati rice processing, jasmine rice refinement, brown rice separation, and mixed grain sorting. A dedicated rice color sorter manufacturer provides solutions for small-scale operations and large industrial facilities alike. These versatile machines improve market competitiveness by delivering premium-grade products that command higher prices, making them essential tools in modern rice production and processing industries.

 EN