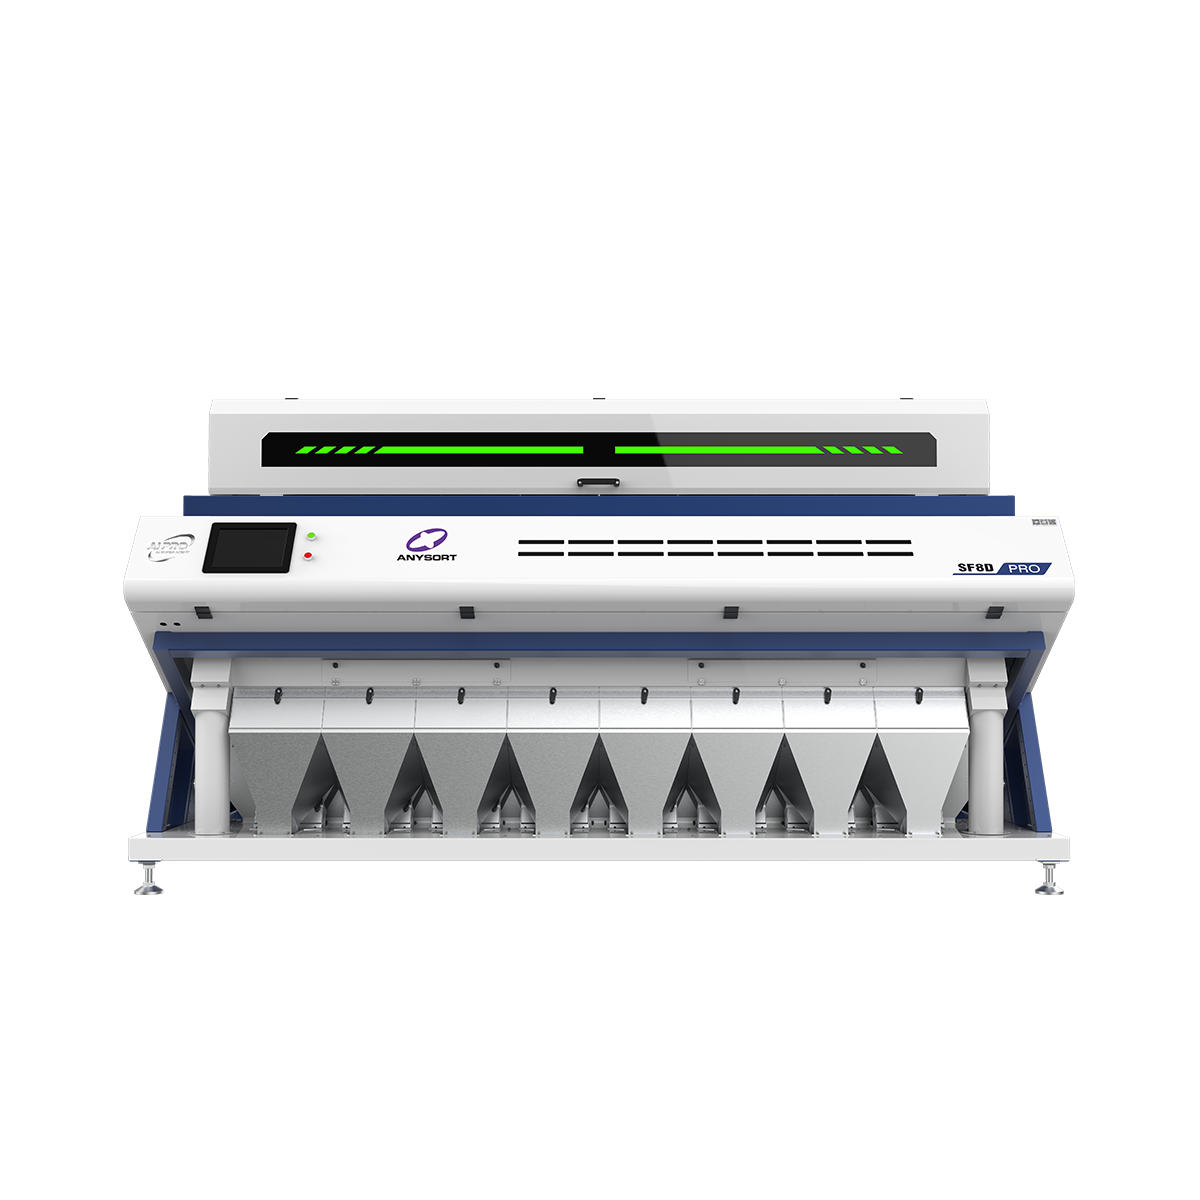
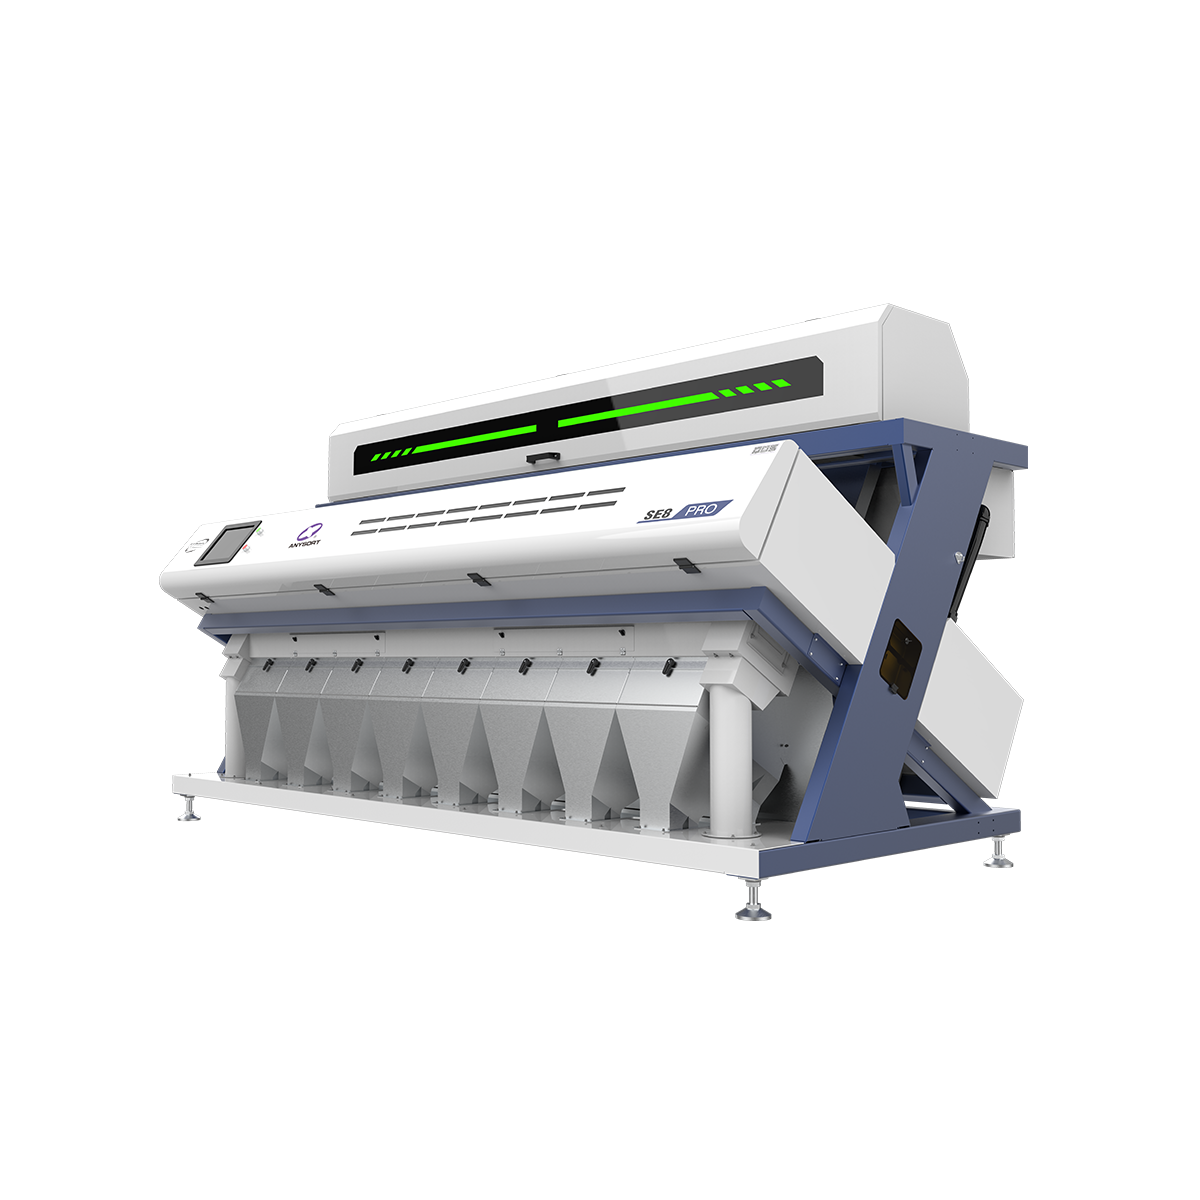
rice color sorter manufacturers
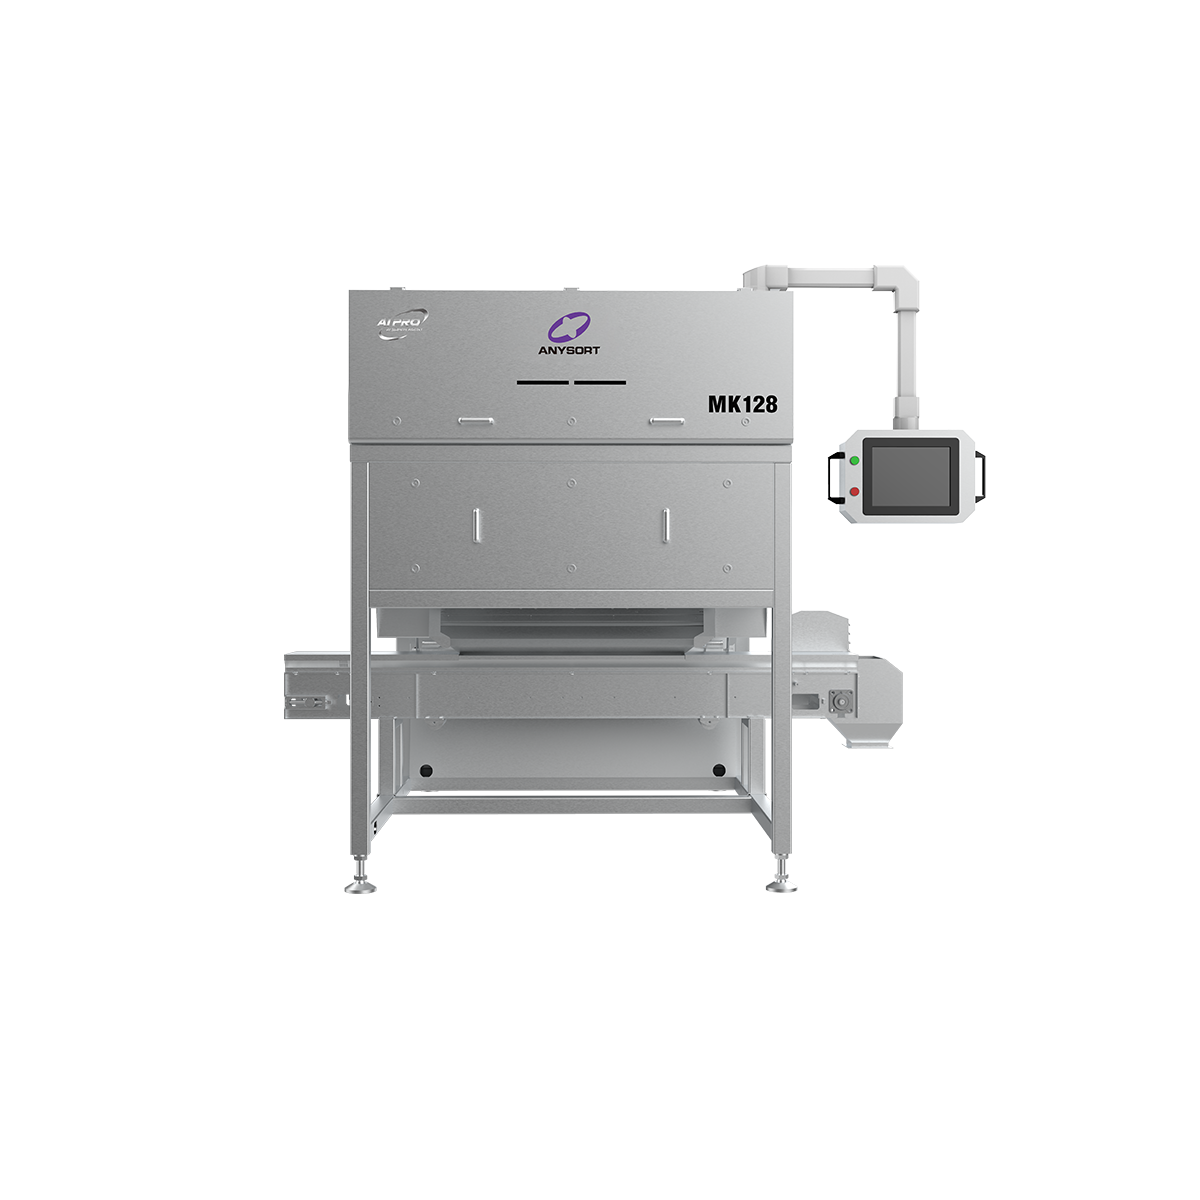
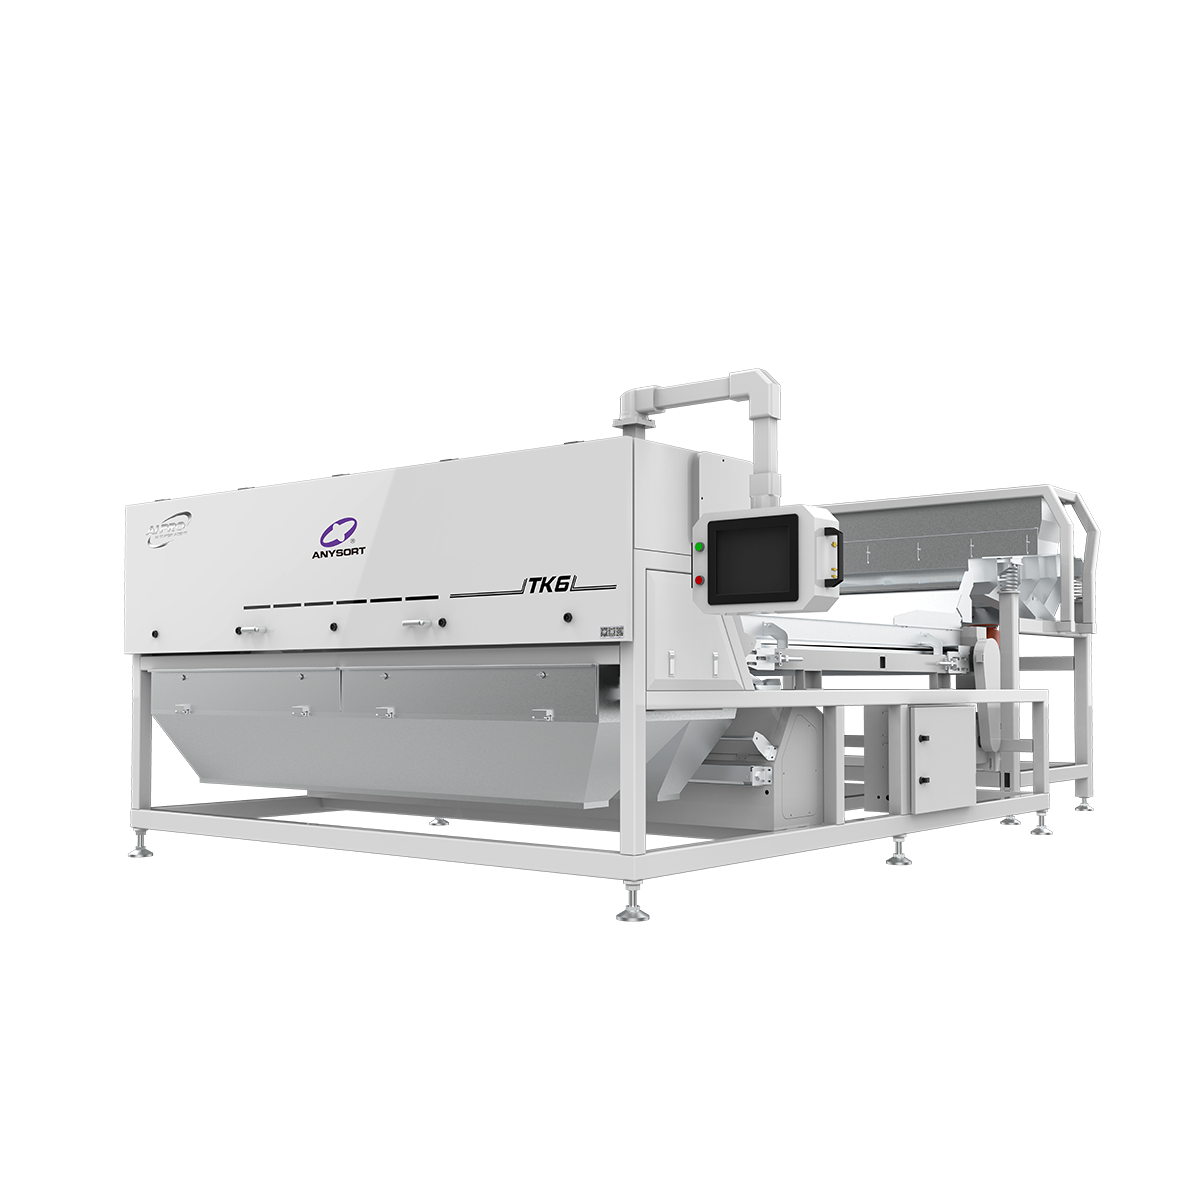
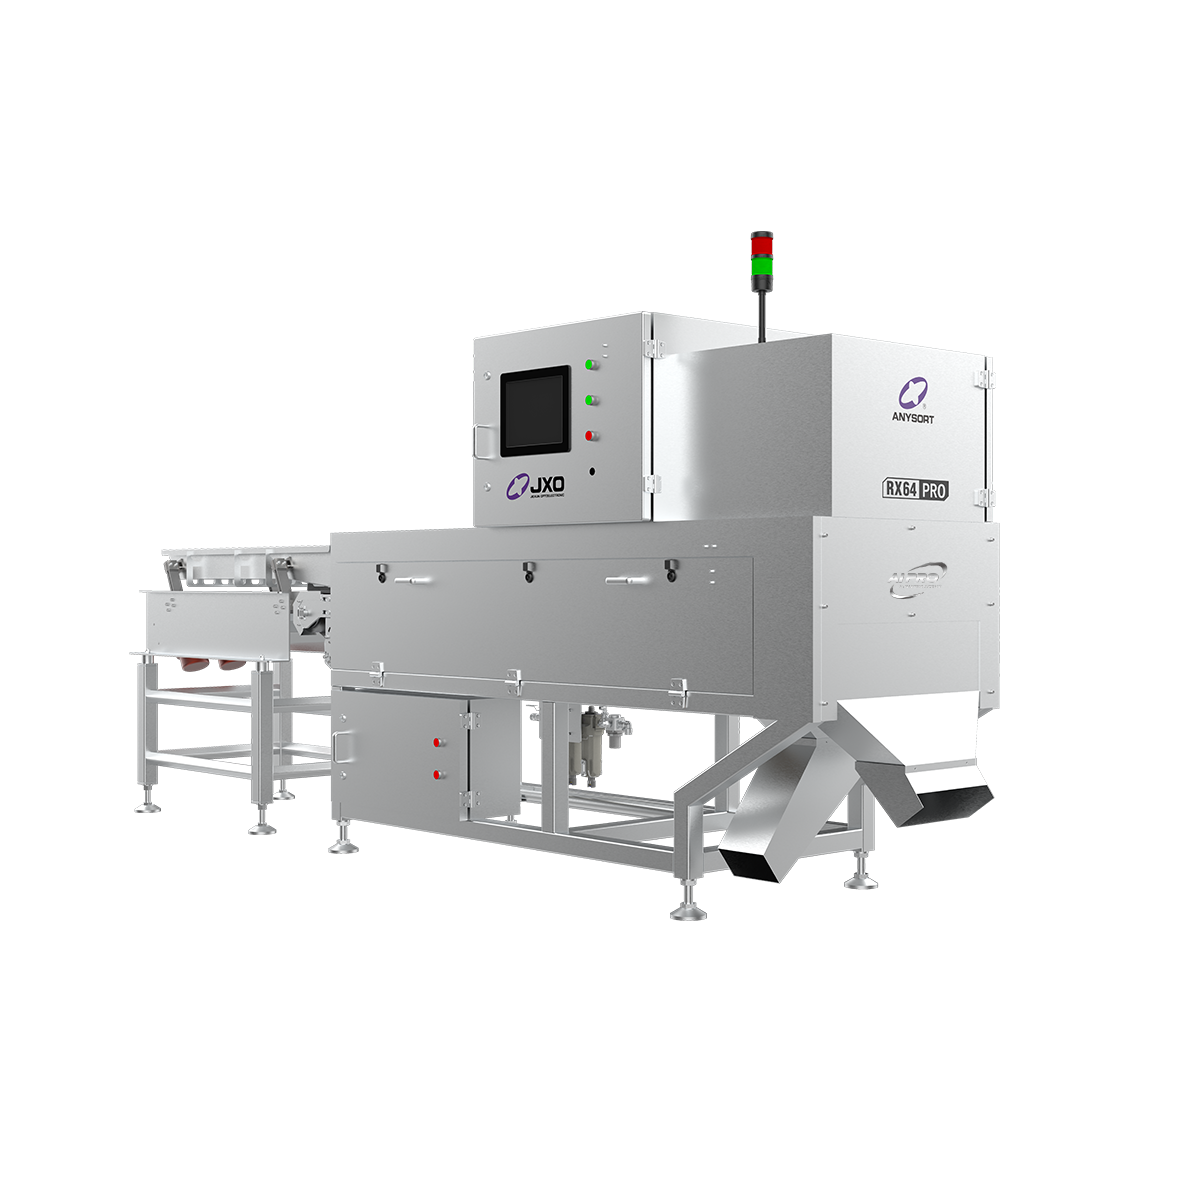
Rice color sorter manufacturers produce advanced optical sorting equipment designed to revolutionize grain processing industries worldwide. These sophisticated machines detect and separate grains based on color, appearance, and quality characteristics with exceptional precision. Rice color sorter manufacturers utilize cutting-edge technology to ensure only premium-quality rice reaches consumers while eliminating discolored, damaged, or foreign materials automatically.
The primary function of rice color sorter manufacturers' equipment involves scanning thousands of rice grains per second using high-resolution cameras and artificial intelligence algorithms. This technology allows rice color sorter manufacturers to achieve sorting accuracies exceeding 99.9 percent, significantly surpassing manual sorting methods. The systems process various rice varieties, including jasmine, basmati, arborio, and long-grain white rice, making them versatile solutions for diverse agricultural operations.
Technological features developed by rice color sorter manufacturers include real-time image processing, multi-spectral detection, and machine learning capabilities. These innovations enable equipment to identify subtle quality differences invisible to the human eye. Advanced rice color sorter manufacturers incorporate modular designs allowing customization for specific production requirements and processing volumes.
Applications for rice color sorter manufacturers' equipment extend throughout the global rice supply chain. Agricultural cooperatives, rice mills, export companies, and food processors all benefit from implementing these systems. By deploying rice color sorter manufacturers' solutions, businesses reduce waste, improve product consistency, meet strict international quality standards, and enhance profitability through increased yield of marketable rice.

 EN