Rice Color Sorter Machine Manufacturer

All Categories

rice color sorter machine manufacturer

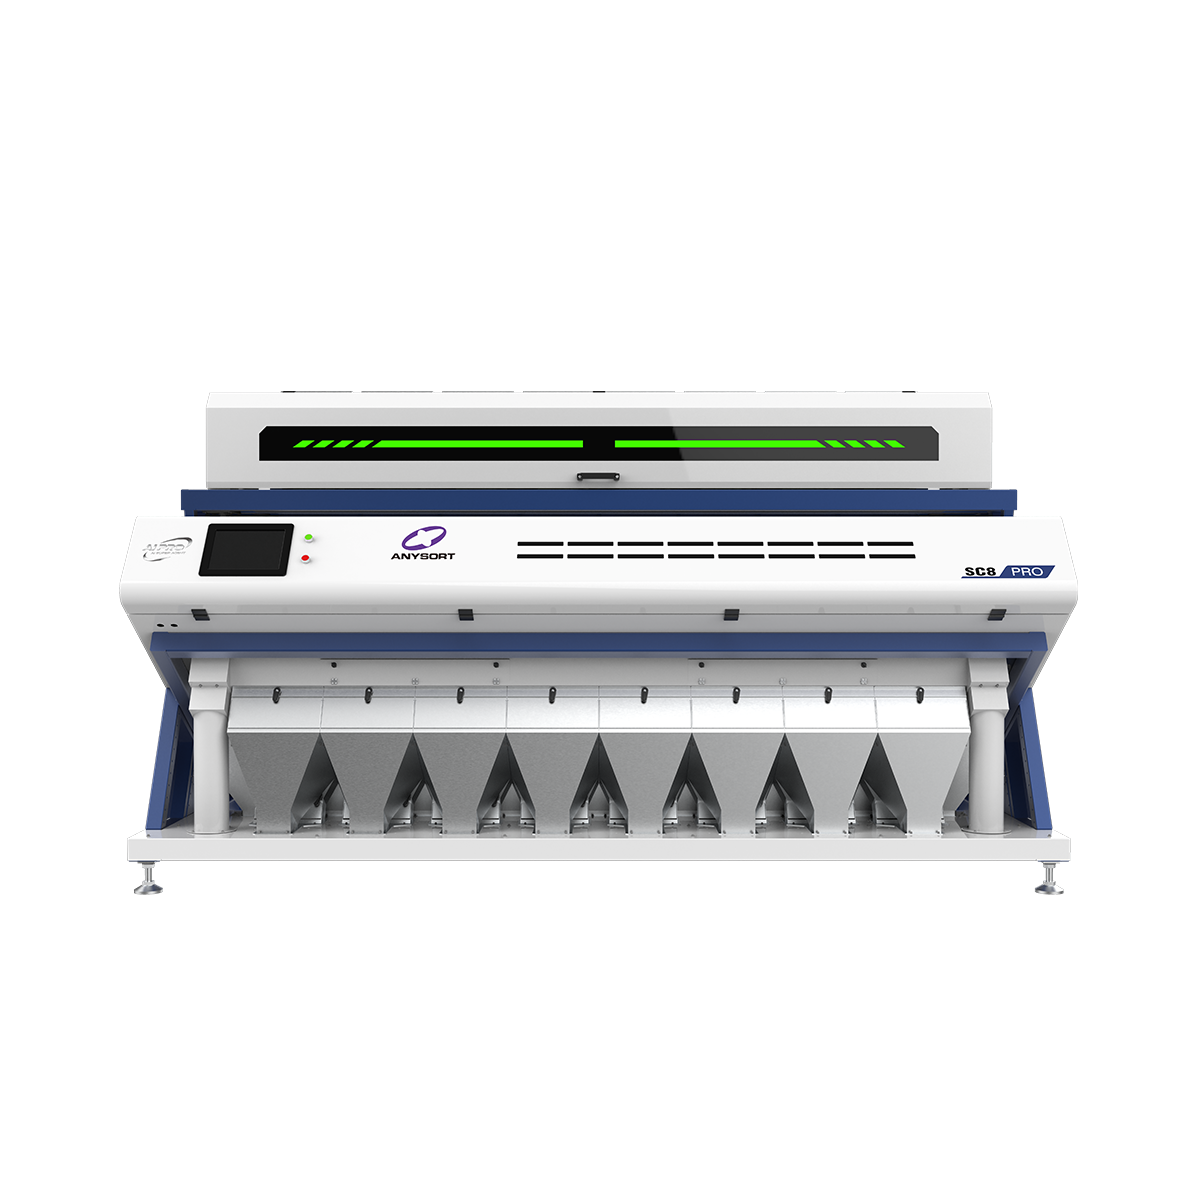
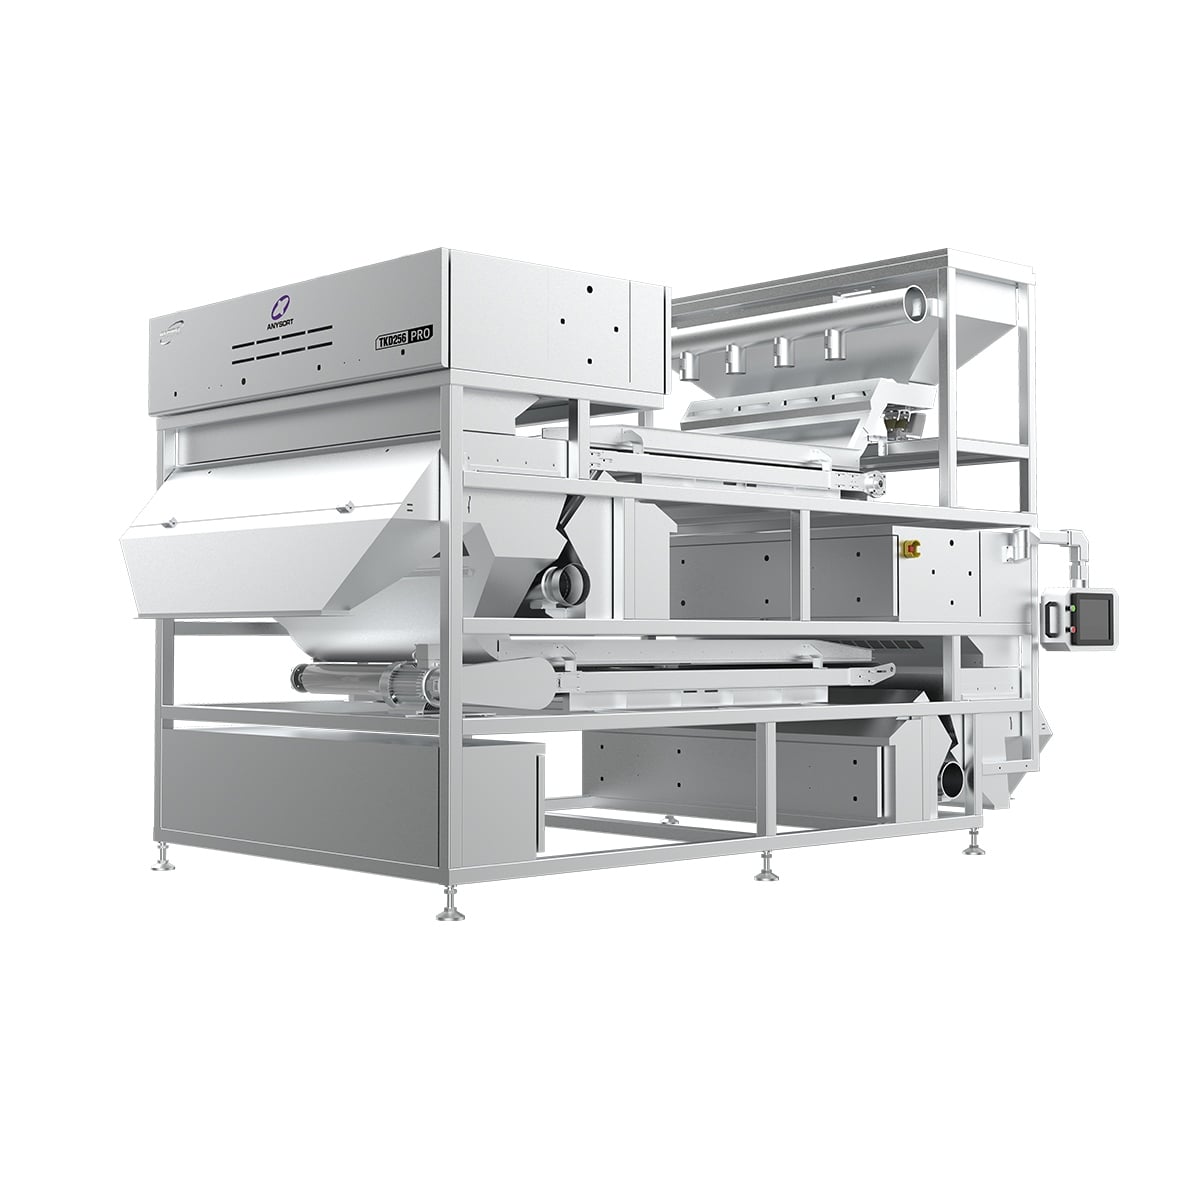
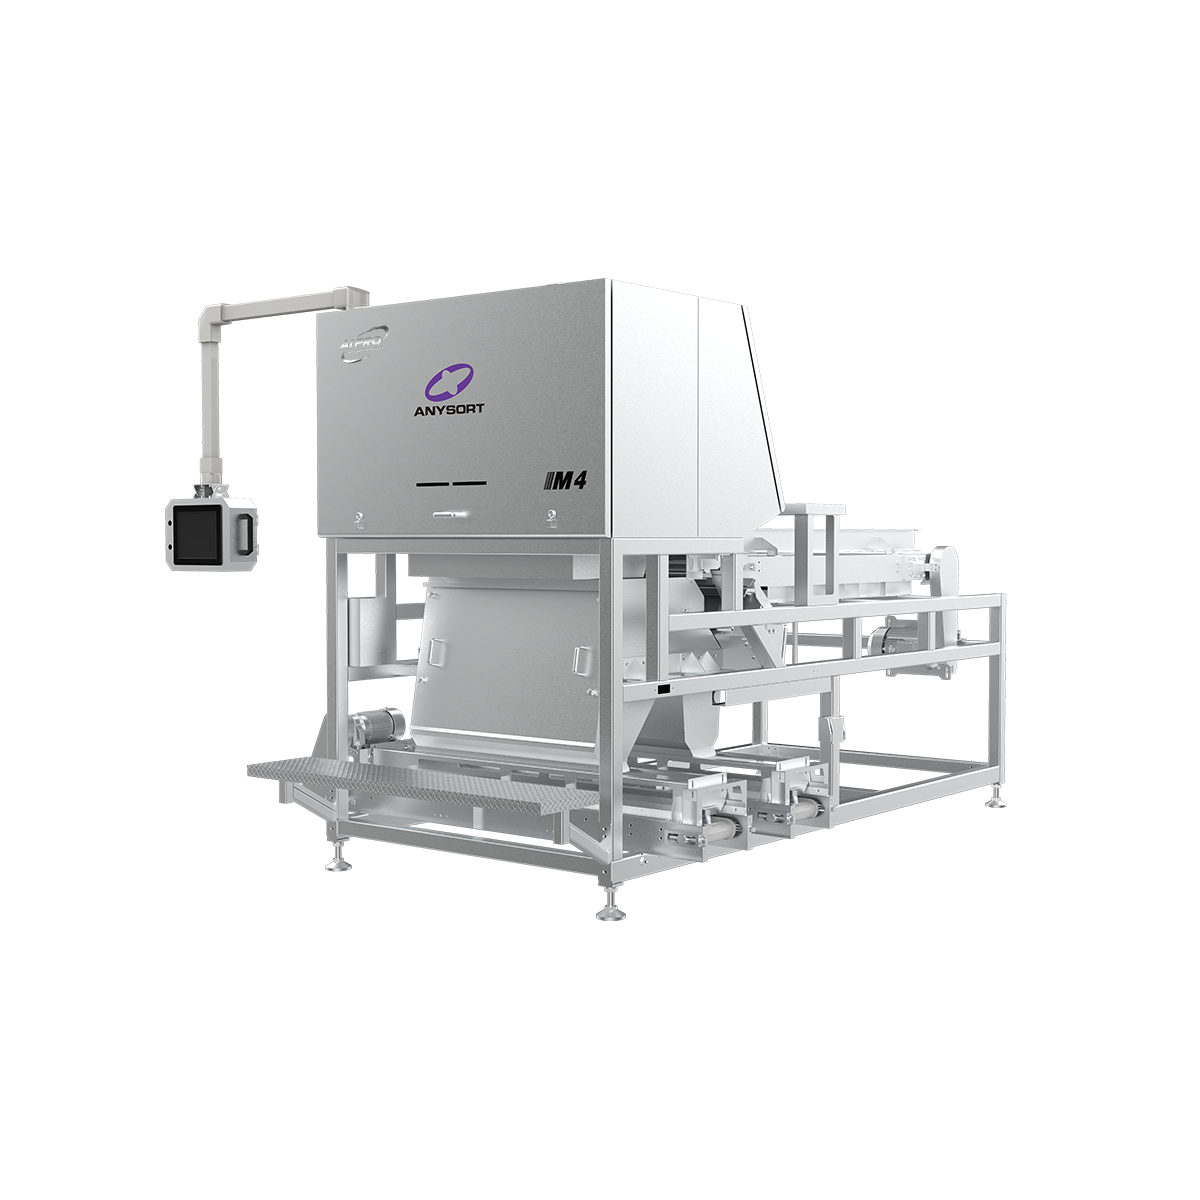
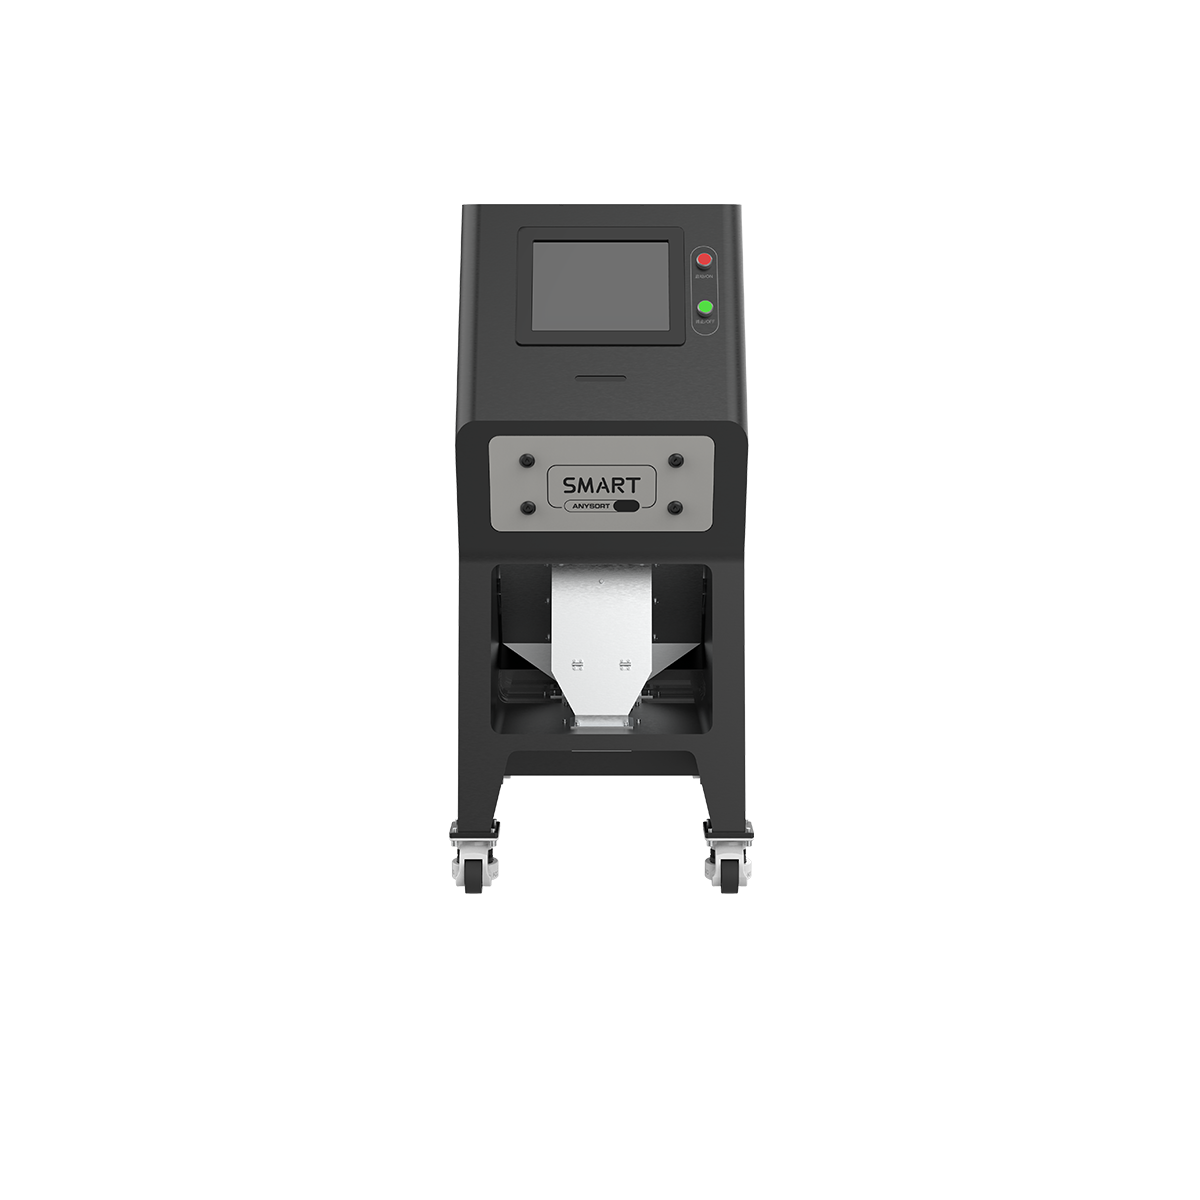
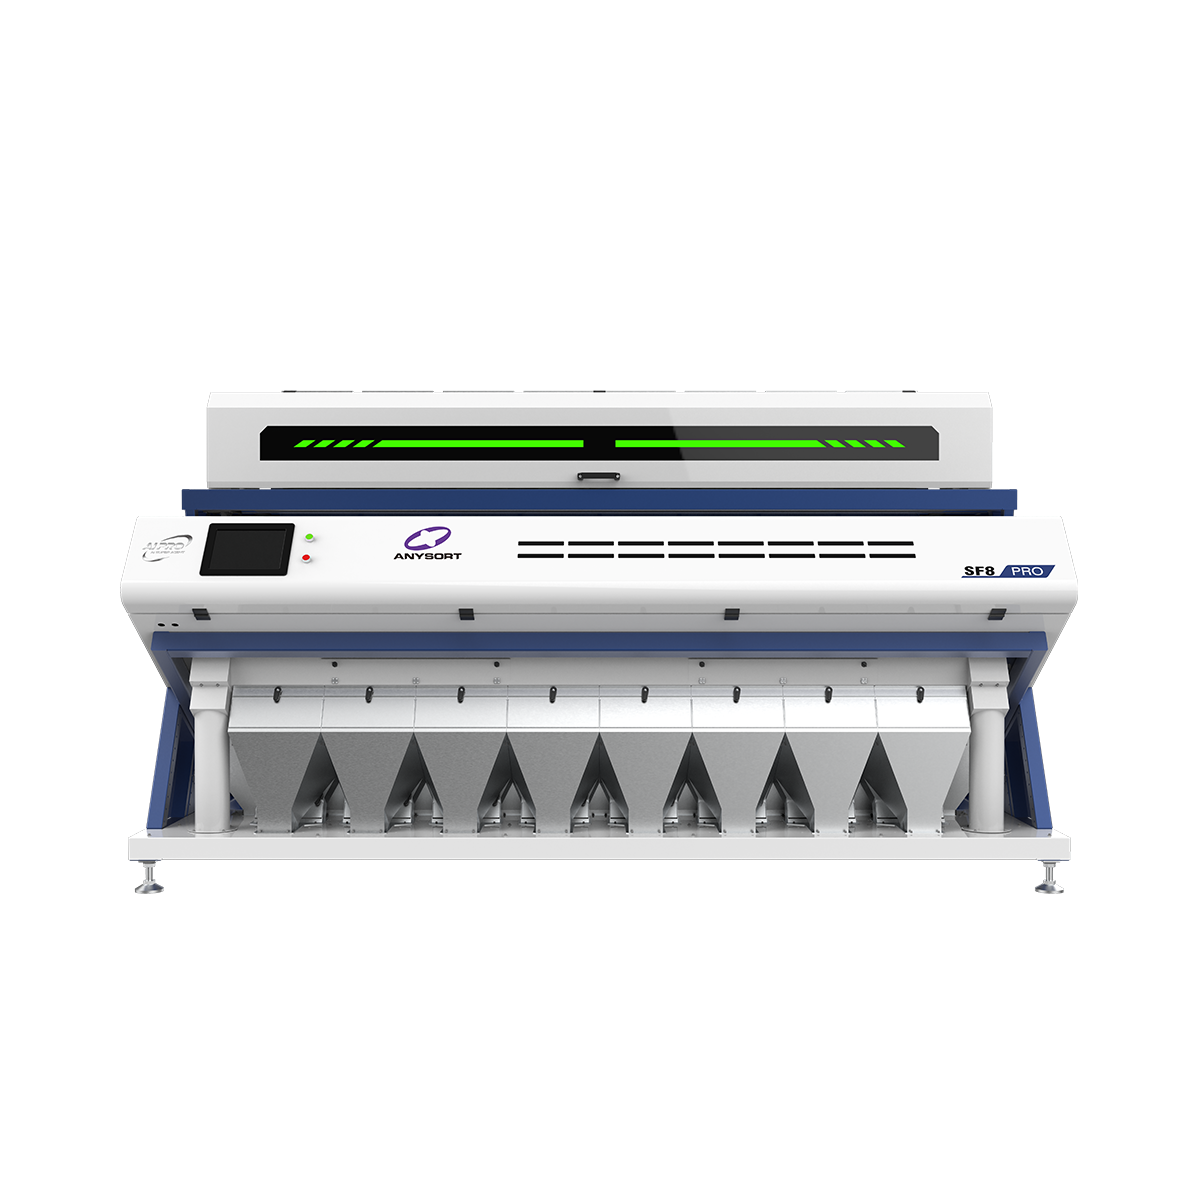
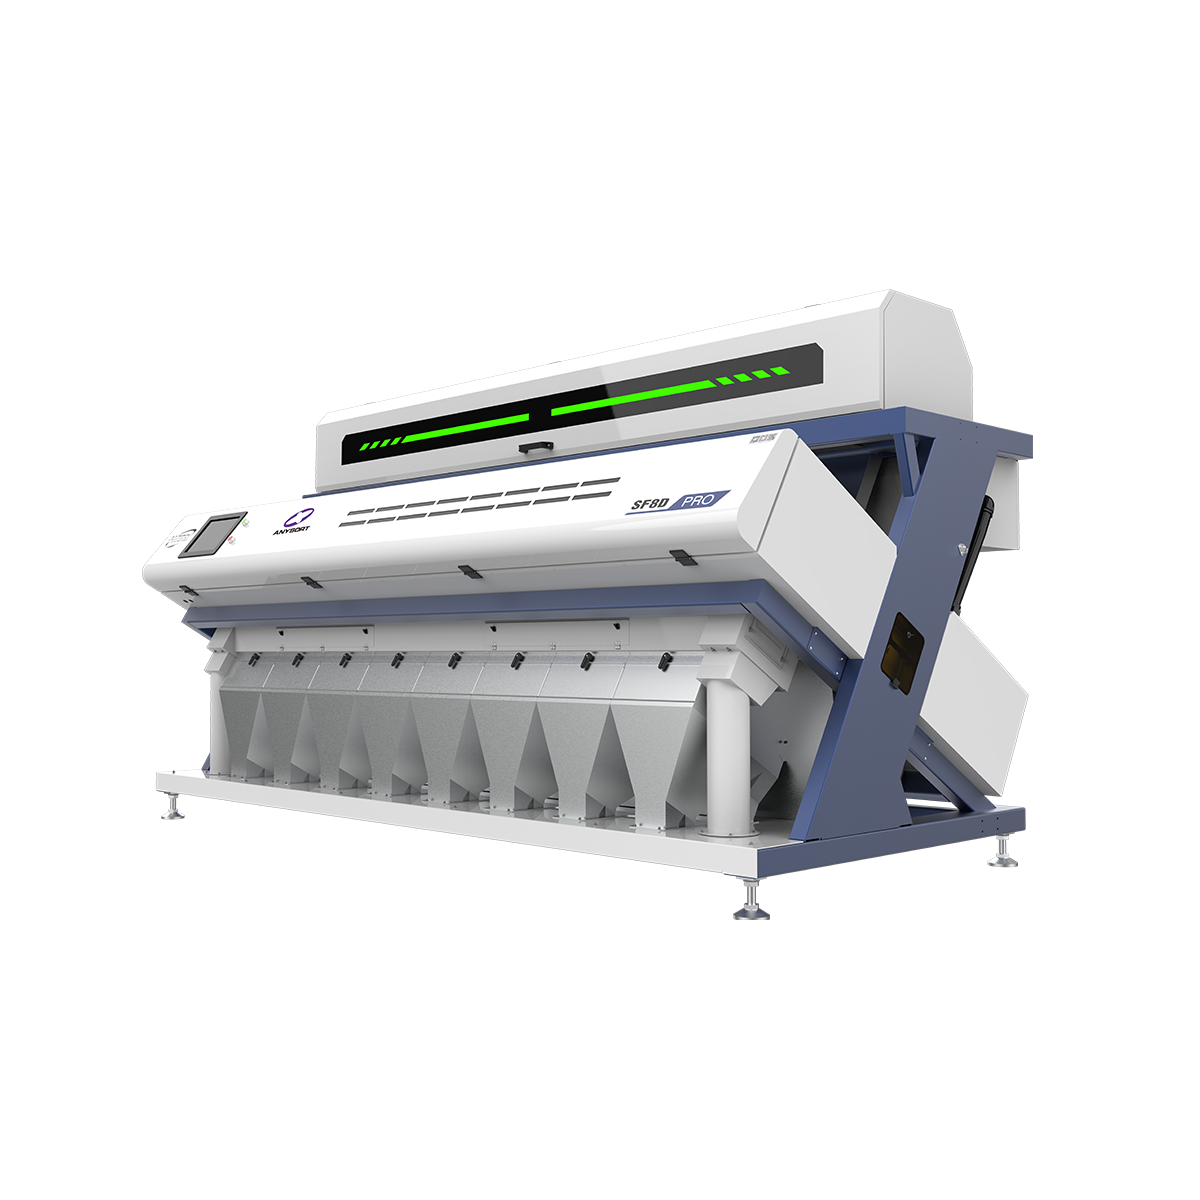
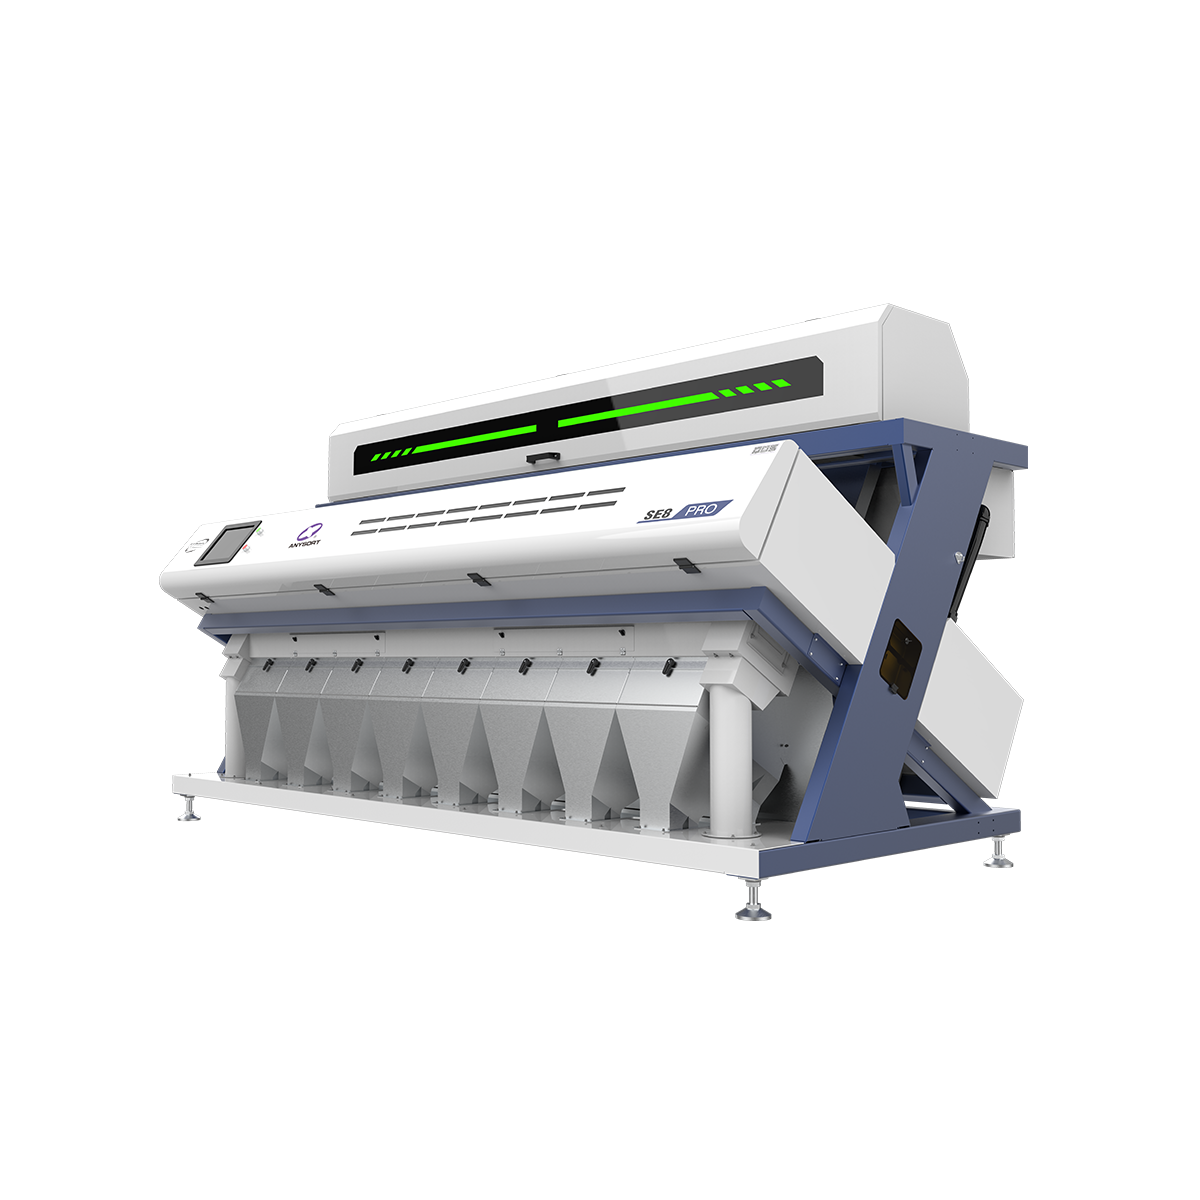
A rice color sorter machine manufacturer specializes in producing advanced optical sorting equipment designed to separate rice grains by color, size, and quality. These machines utilize cutting-edge technology to identify and remove discolored, damaged, or foreign particles from rice batches with exceptional precision. The rice color sorter machine manufacturer delivers solutions that enhance product quality while maintaining operational efficiency across rice processing facilities. The core function of equipment from a rice color sorter machine manufacturer involves using high-resolution cameras and artificial intelligence to scan thousands of grains per second. The system identifies variations in color, detecting yellow grains, broken pieces, stones, and other impurities that affect marketability. Once detected, pneumatic or mechanical ejectors remove these substandard grains instantly. Technological features include advanced image processing algorithms, multi-spectral detection capabilities, and intelligent sorting logic. A professional rice color sorter machine manufacturer integrates machine learning systems that continuously improve accuracy. The equipment handles various rice varieties, from long-grain to short-grain types, without requiring extensive recalibration. Applications span commercial rice mills, cooperative processing centers, export-oriented facilities, and specialty grain processors. Modern rice color sorter machine manufacturers create machines suitable for both small-scale operations and large industrial complexes. These systems support organic rice certification, premium grade production, and export-quality standards. The rice color sorter machine manufacturer provides comprehensive solutions that improve throughput while reducing labor costs and waste. Investment in this technology ensures competitive advantage in the global rice market while meeting international quality benchmarks consistently.

New Products

Choosing a reputable rice color sorter machine manufacturer offers substantial operational and financial benefits for grain processing businesses. These machines dramatically improve product quality by removing defects that human inspectors miss consistently. The result is higher market prices and stronger customer satisfaction for end products. Operational efficiency increases significantly when businesses partner with a competent rice color sorter machine manufacturer. Automated sorting reduces reliance on manual labor, lowering personnel costs while accelerating processing speed. Facilities process larger volumes daily without proportional increases in staffing expenses. The rice color sorter machine manufacturer delivers equipment that runs continuously with minimal downtime, maximizing production capacity year-round. Accuracy represents another critical advantage. A quality rice color sorter machine manufacturer creates systems achieving 99% detection rates for discolored and damaged grains. This precision prevents poor-quality rice from reaching consumers, protecting brand reputation and building customer loyalty. Buyers gain confidence knowing products meet consistent quality standards. Flexibility matters for diverse processing needs. Leading rice color sorter machine manufacturer models handle multiple rice varieties with simple parameter adjustments. Whether processing aromatic basmati, fragrant jasmine, or standard white rice, the equipment adapts efficiently. This versatility enables facilities to diversify their product lines profitably. Cost-effectiveness emerges through reduced waste and improved yields. The rice color sorter machine manufacturer designs systems that maximize usable output from raw rice batches. Lower reject rates translate directly to increased profitability. Additionally, certification compliance becomes easier, enabling access to premium market segments. Environmental benefits include reduced water usage and waste generation compared to traditional sorting methods. Sustainability-focused businesses appreciate these ecological advantages significantly.

Latest News

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

rice color sorter machine manufacturer

Advanced Optical Detection Technology

Advanced Optical Detection Technology

A leading rice color sorter machine manufacturer integrates sophisticated optical detection systems using multi-spectral imaging and artificial intelligence algorithms. These machines capture detailed grain information in milliseconds, analyzing color, shape, and size characteristics with extraordinary precision. The technology identifies defects invisible to human eyes, including internal damage and subtle discoloration. High-resolution cameras work alongside LED lighting systems that standardize detection conditions. Machine learning continuously refines sorting parameters based on processing results. The rice color sorter machine manufacturer ensures consistent detection accuracy across varying rice types and processing environments. This technological sophistication transforms raw rice into premium products meeting international quality standards. Facilities achieve competitive differentiation through superior product consistency and minimal waste production. The investment yields substantial returns through improved marketability and reduced rejection rates from buyers.
High-Speed Processing Capability

High-Speed Processing Capability

Modern equipment from a rice color sorter machine manufacturer processes rice at exceptional throughput rates, handling 5-10 tons per hour depending on specifications. This rapid processing capability enables facilities to maintain continuous production schedules without bottlenecks. The rice color sorter machine manufacturer designs machines that maintain accuracy even at maximum speeds, never compromising quality for quantity. Advanced pneumatic ejection systems remove detected defects instantaneously without slowing conveyor movement. Businesses maximize facility utilization, generating higher revenue from existing floor space. Processing speeds reduce storage requirements for raw materials, lowering operational overhead. The rice color sorter machine manufacturer equipment adapts to seasonal demand fluctuations seamlessly. Peak harvest periods become manageable through rapid grain sorting and processing. Competitive advantages emerge from faster order fulfillment and improved customer satisfaction. Facilities achieve profitability improvements by processing greater volumes with existing infrastructure.
Comprehensive Quality Assurance and Support

Comprehensive Quality Assurance and Support

Leading rice color sorter machine manufacturers provide extensive support systems ensuring long-term equipment performance and user satisfaction. Professional installation services customize equipment for specific facility layouts and processing requirements. Training programs enable staff to operate machines effectively and perform routine maintenance. The rice color sorter machine manufacturer offers responsive technical support addressing questions and troubleshooting issues promptly. Spare parts availability ensures minimal downtime when maintenance becomes necessary. Regular performance monitoring helps identify potential problems before failures occur. Extended warranty options protect investments against unexpected repair costs. This comprehensive support transforms equipment purchases into reliable, long-term business solutions. Facilities develop operational confidence knowing expert assistance remains readily available. The rice color sorter machine manufacturer commitment to customer success demonstrates industry professionalism and reliability standards.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy