rice color sorter company
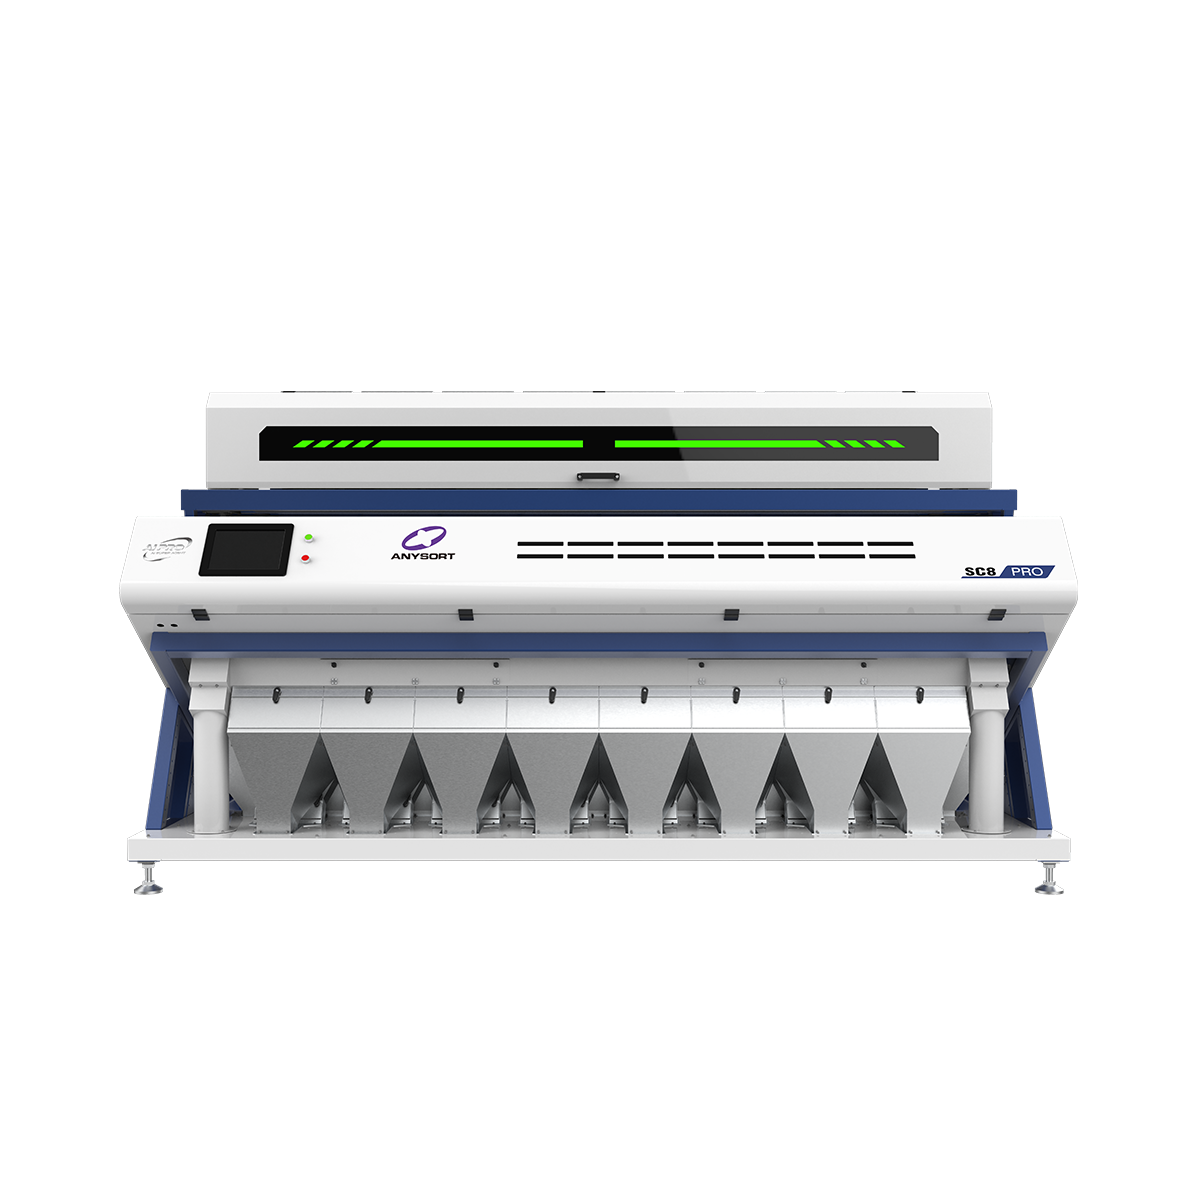
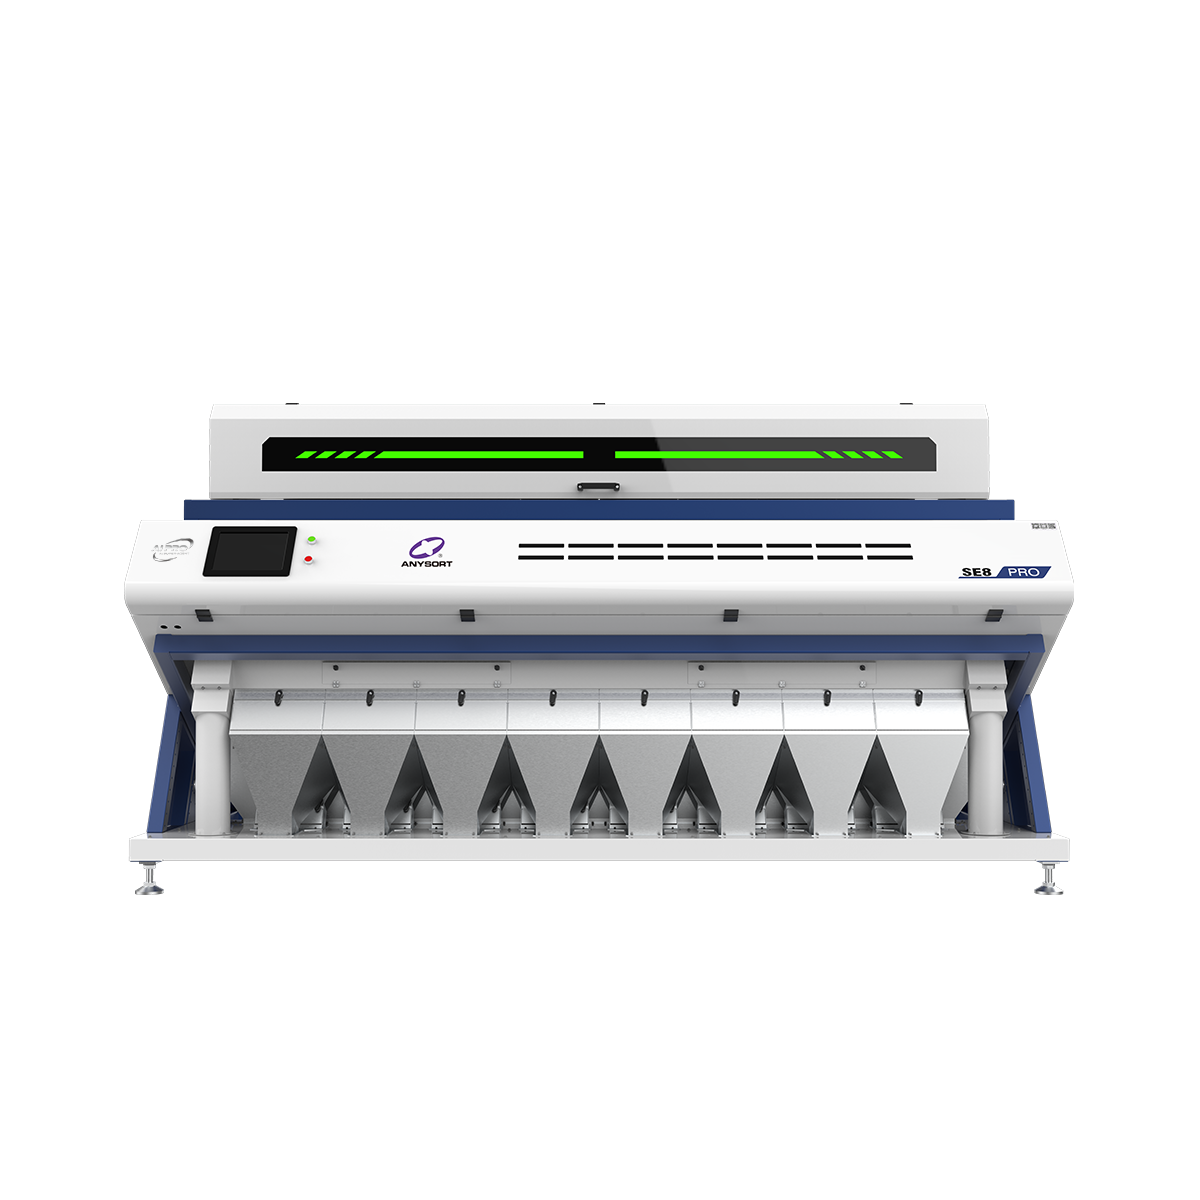
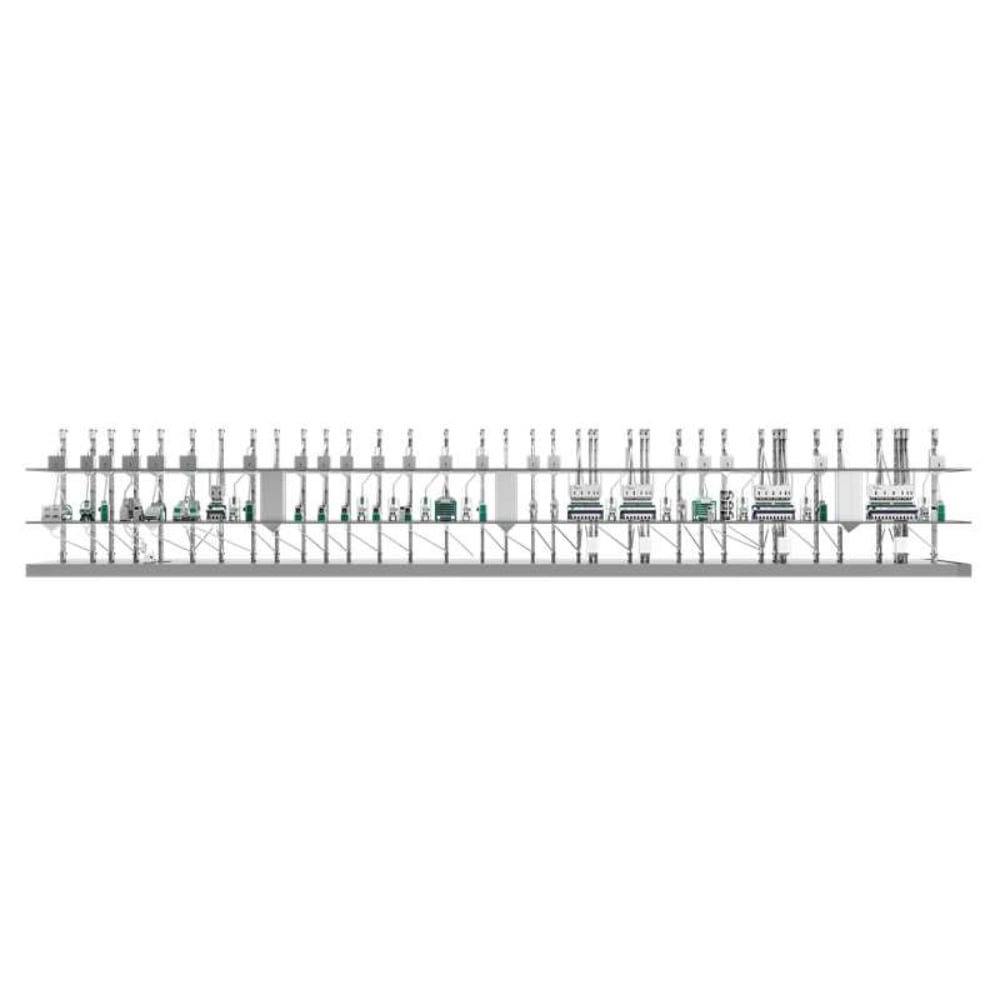
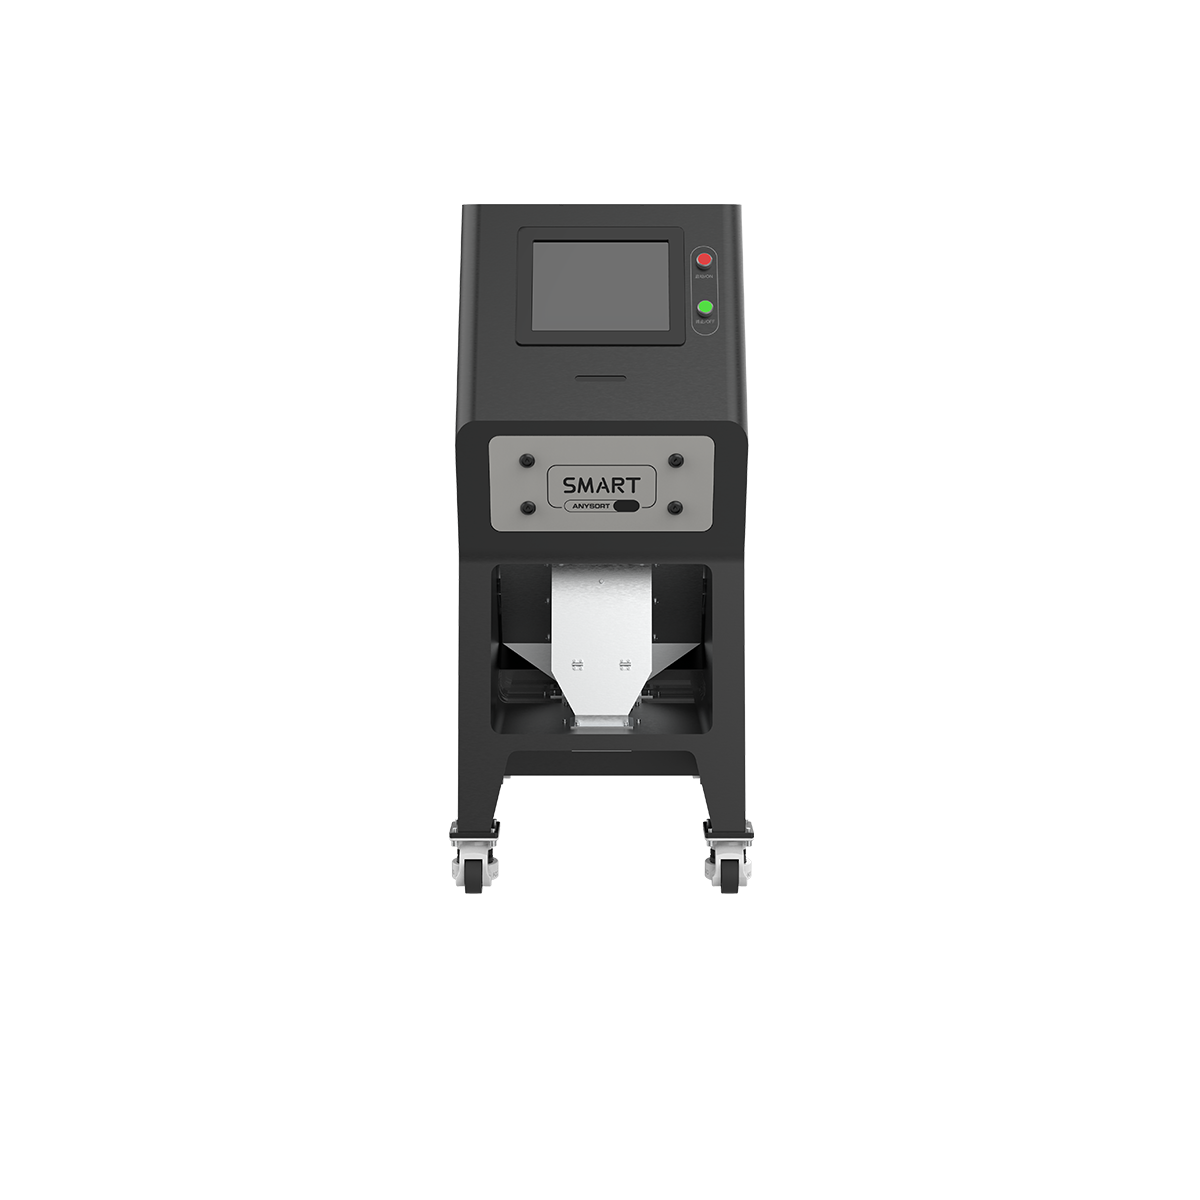
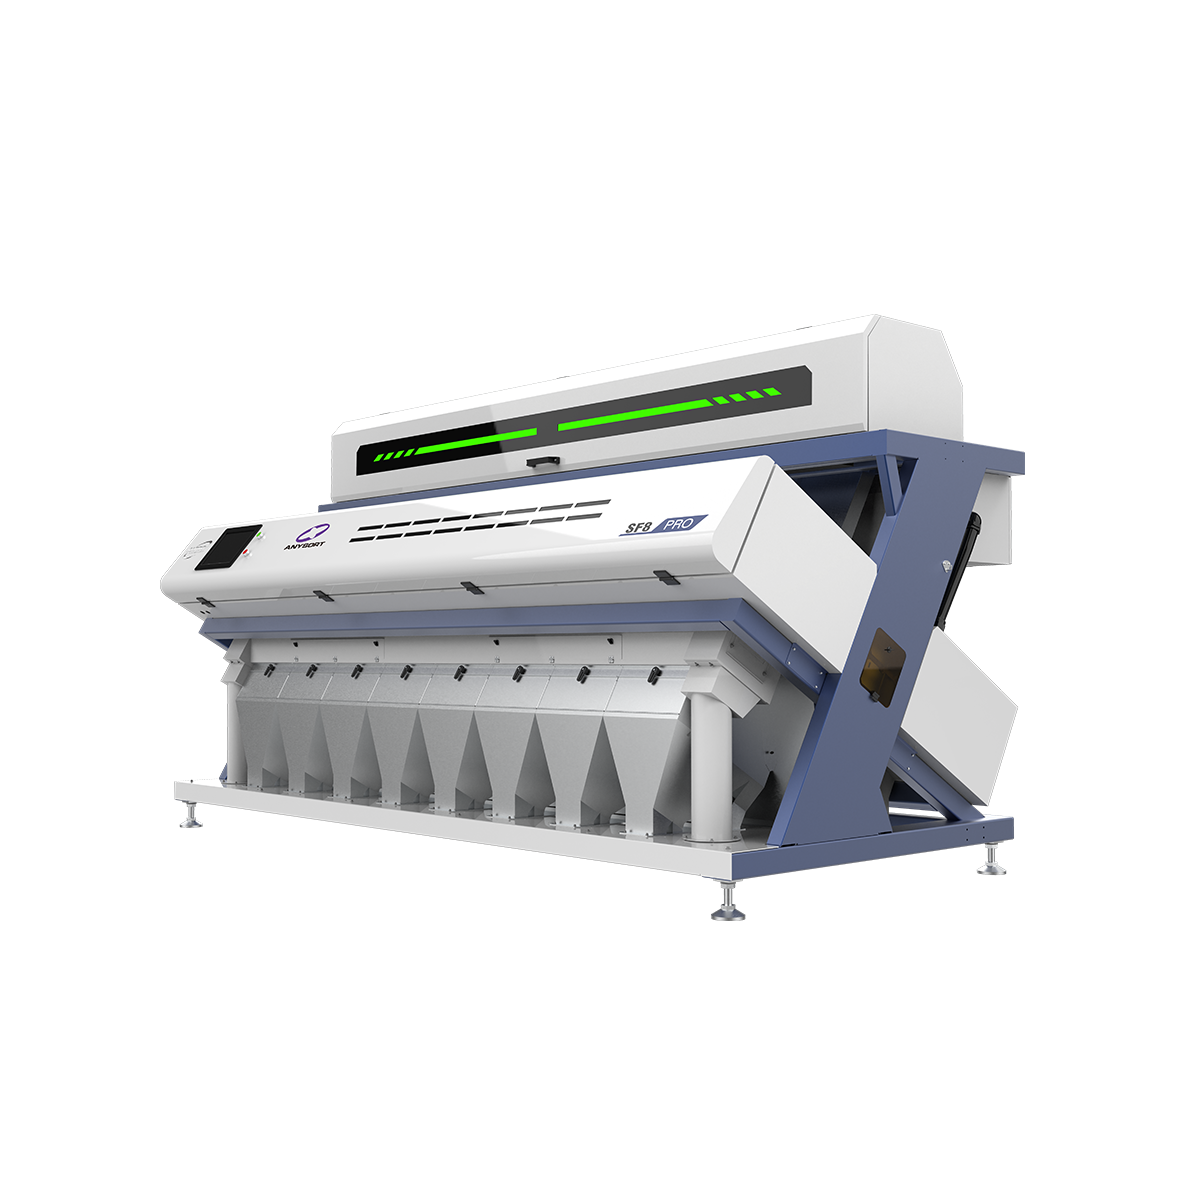
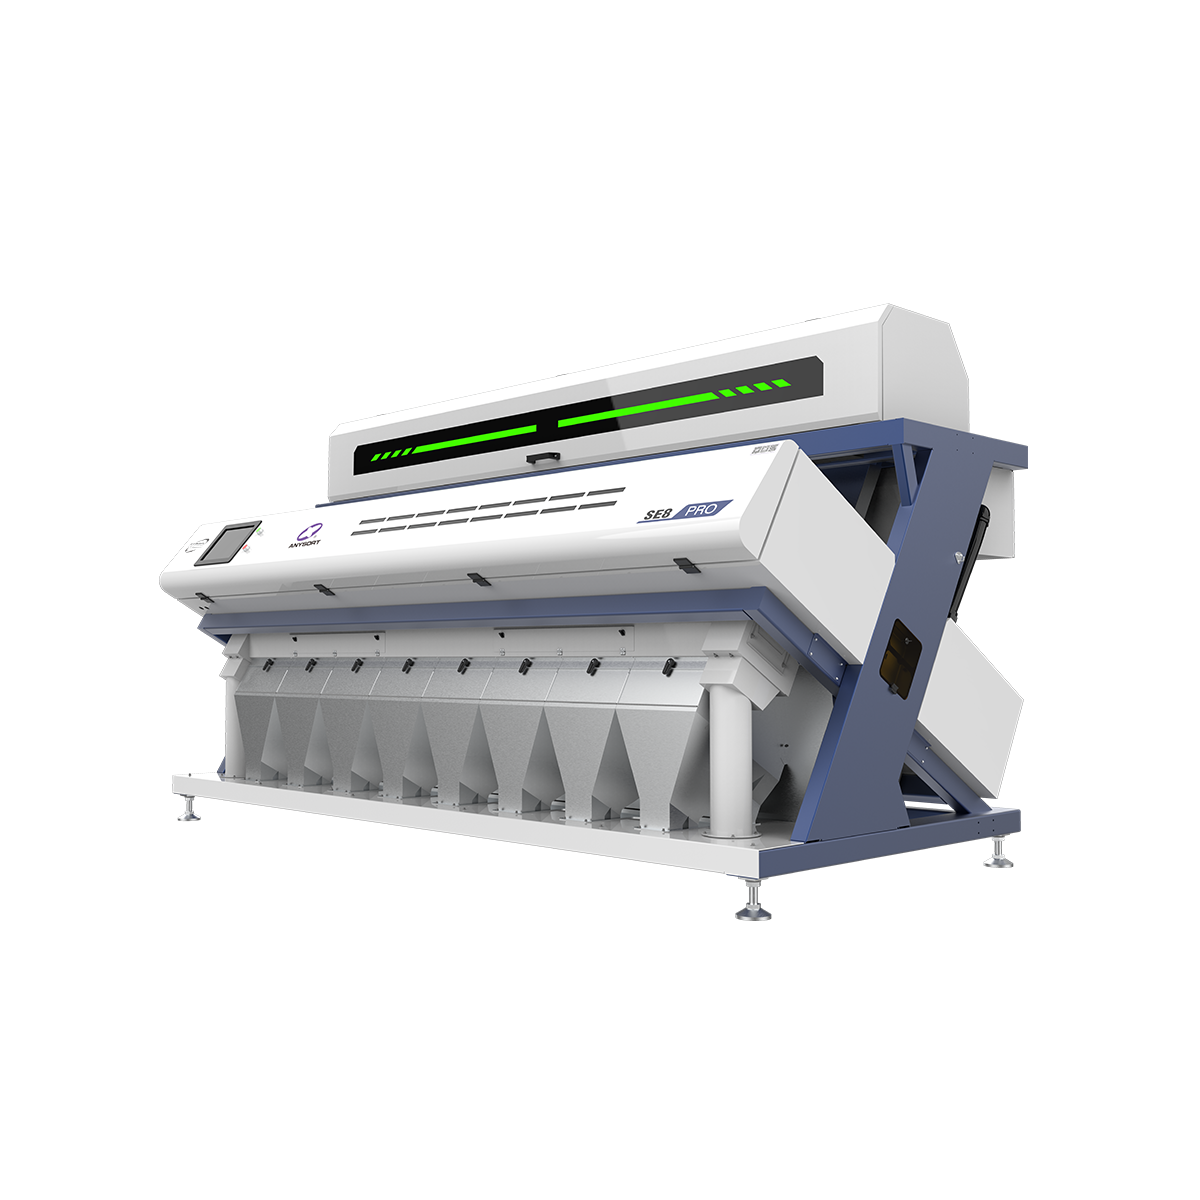
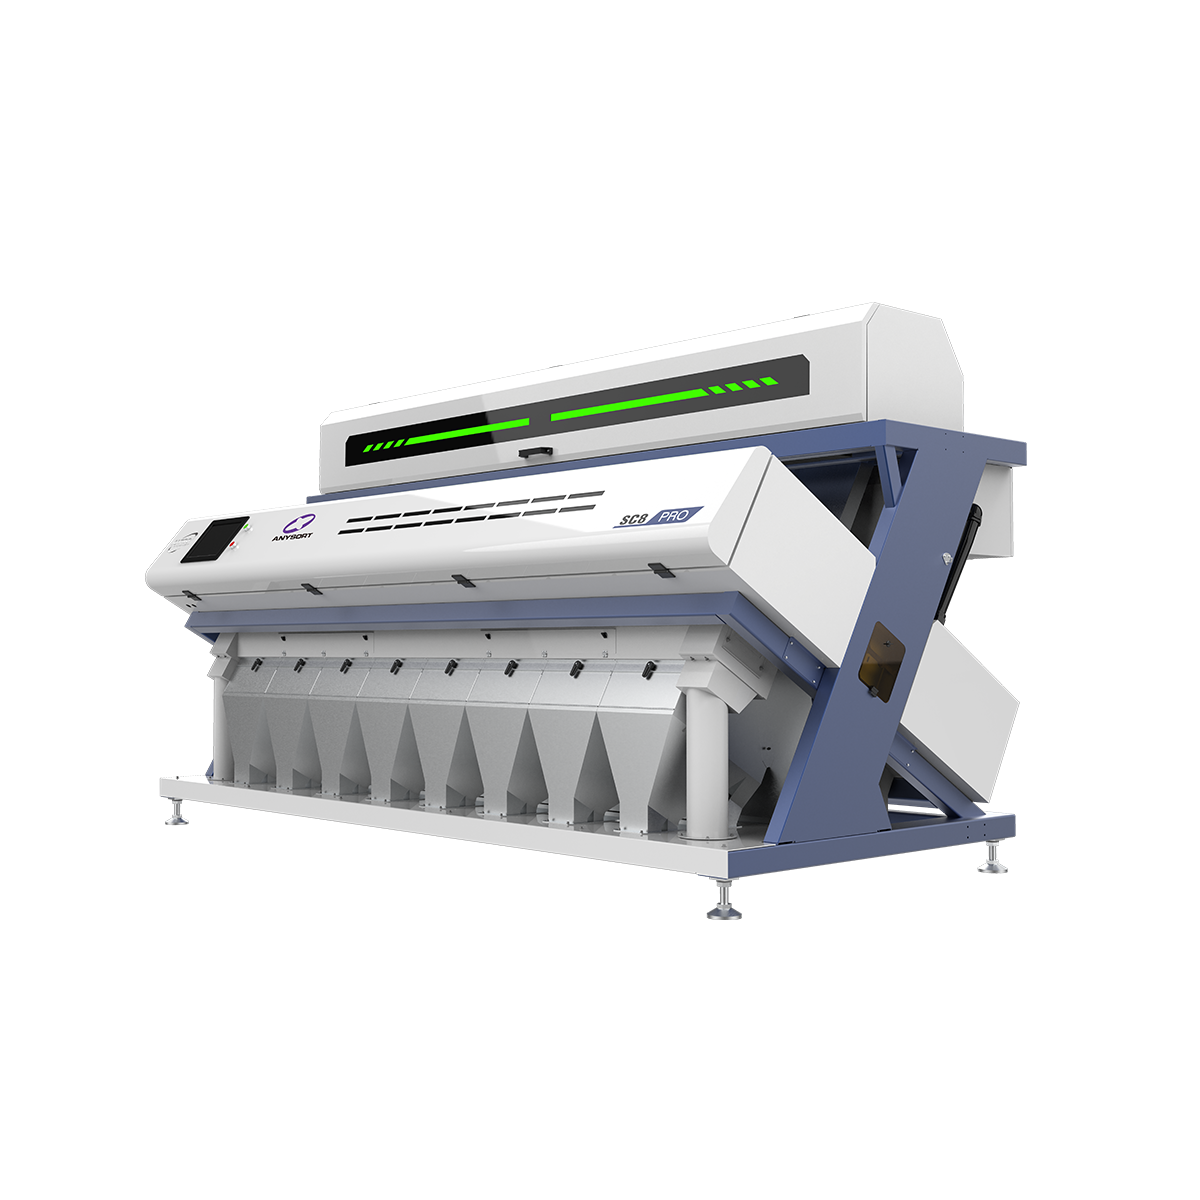
A rice color sorter company specializes in advanced optical sorting technology designed to automatically separate and grade rice by color, quality, and size. The rice color sorter company utilizes sophisticated imaging systems and artificial intelligence algorithms to inspect individual rice kernels at remarkable speeds, typically processing hundreds of kilograms per hour. These machines employ multi-spectral cameras that detect subtle color variations, defects, and foreign materials that would be impossible for human workers to identify consistently. The core function of a rice color sorter company is to enhance product quality while reducing labor costs and waste. Modern rice color sorter company systems integrate high-speed ejection mechanisms that remove discolored, broken, or contaminated grains with precision. The technological features include real-time processing capabilities, customizable sorting parameters, and data logging for quality control documentation. A rice color sorter company addresses critical challenges in rice processing by ensuring uniform grain appearance and maintaining international quality standards. Applications span commercial rice mills, agricultural cooperatives, export facilities, and specialty grain producers worldwide. The rice color sorter company technology eliminates manual sorting bottlenecks while improving consistency and traceability throughout the supply chain. Investment in equipment from a professional rice color sorter company delivers measurable improvements in final product appeal, market competitiveness, and customer satisfaction across diverse rice varieties and processing scales.

 EN