Quality Sorting Companies | Advanced Automated Solutions

All Categories

quality sorting companies

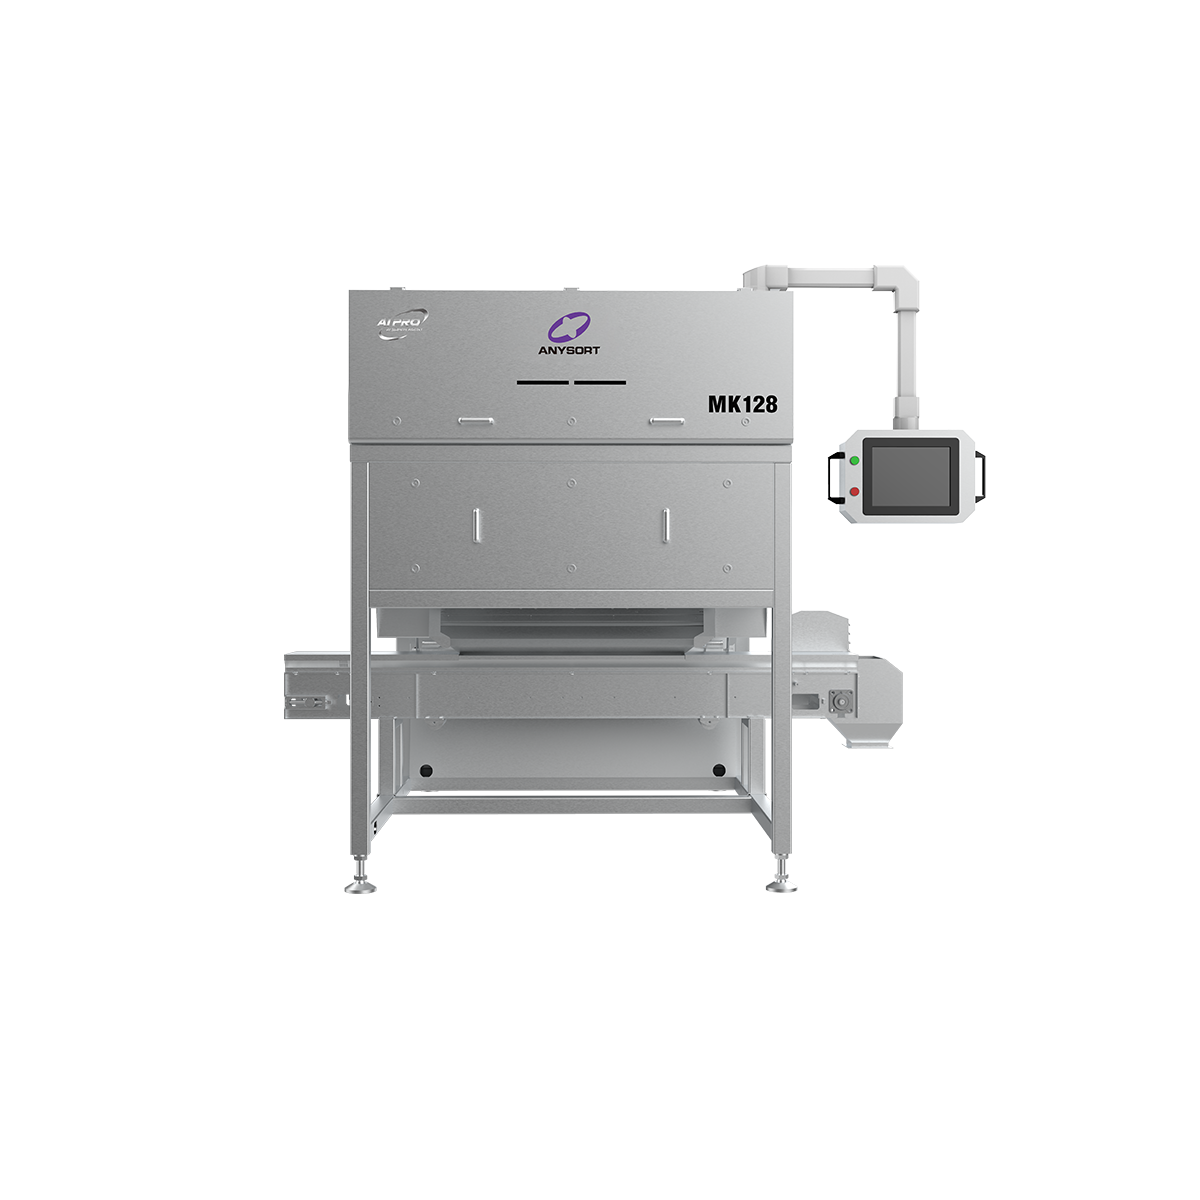
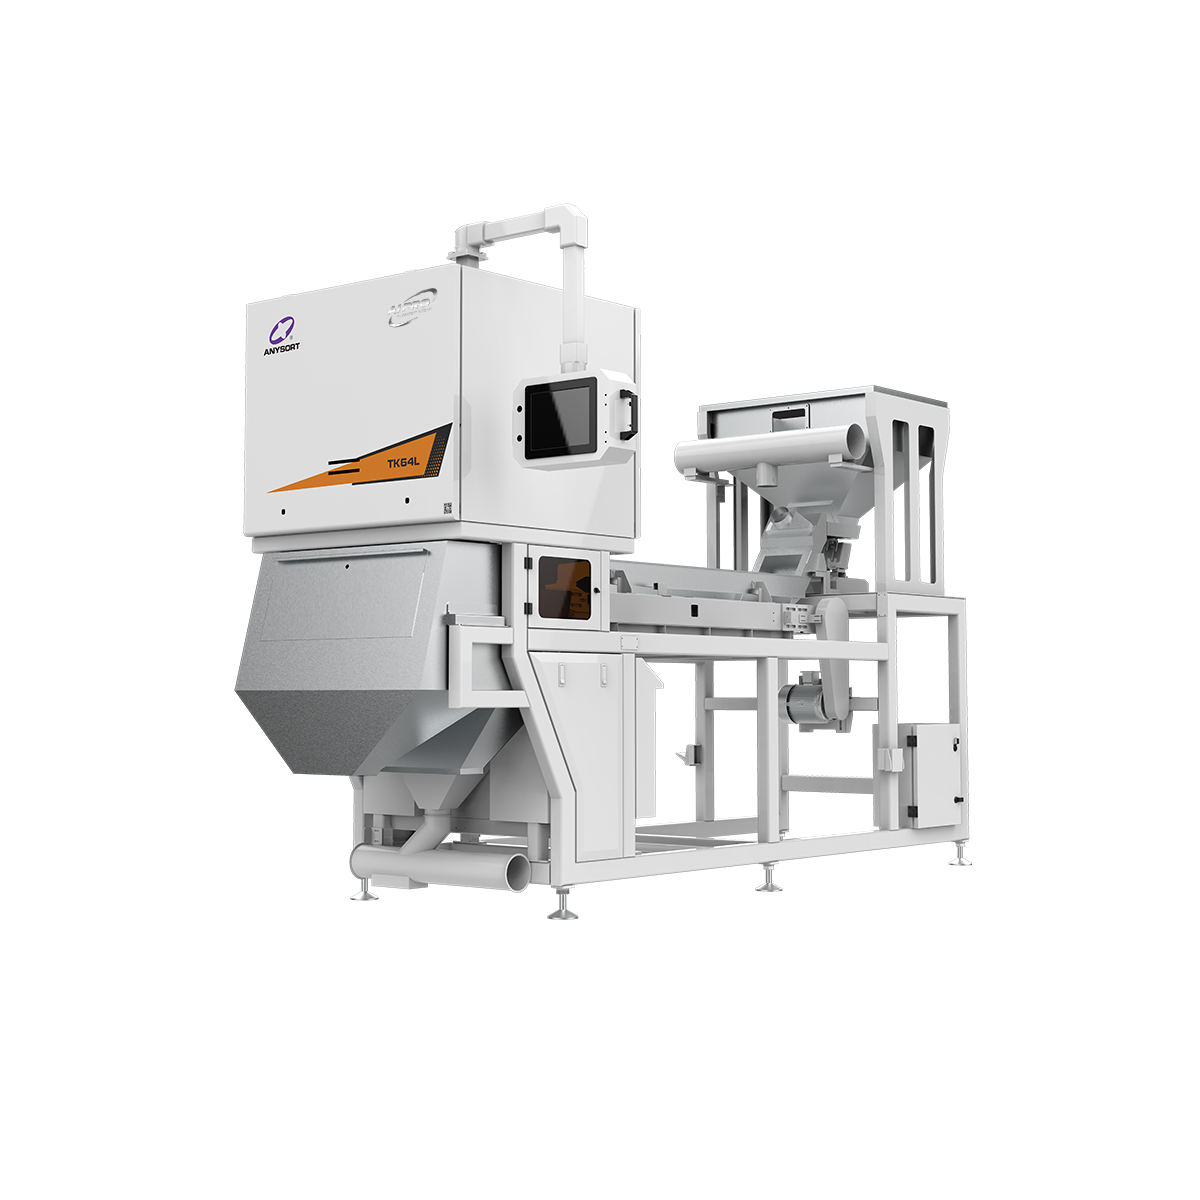
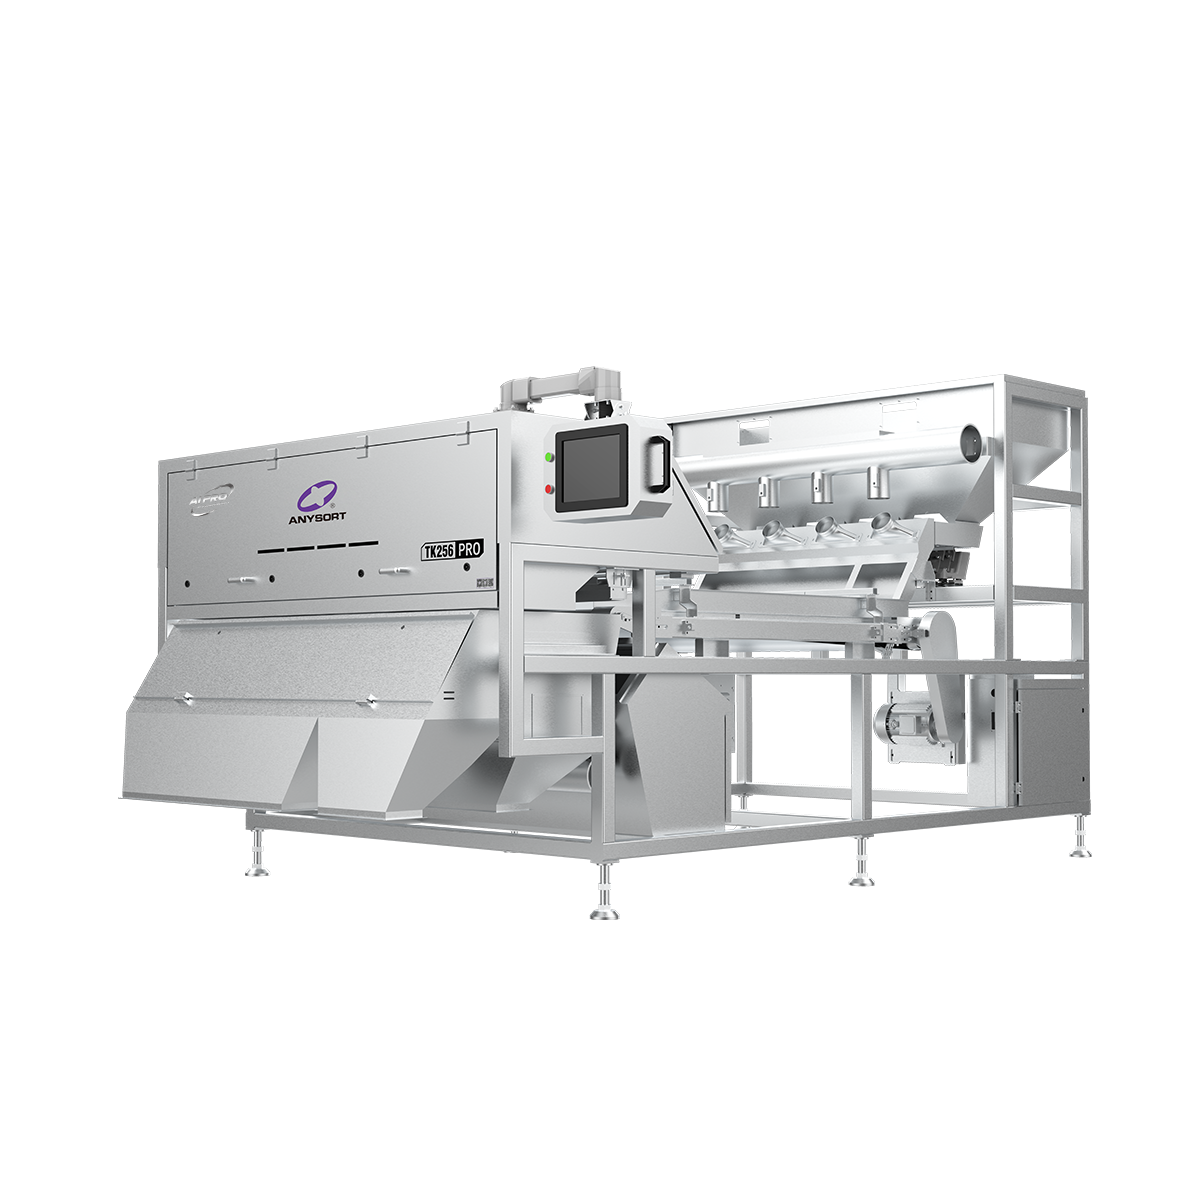
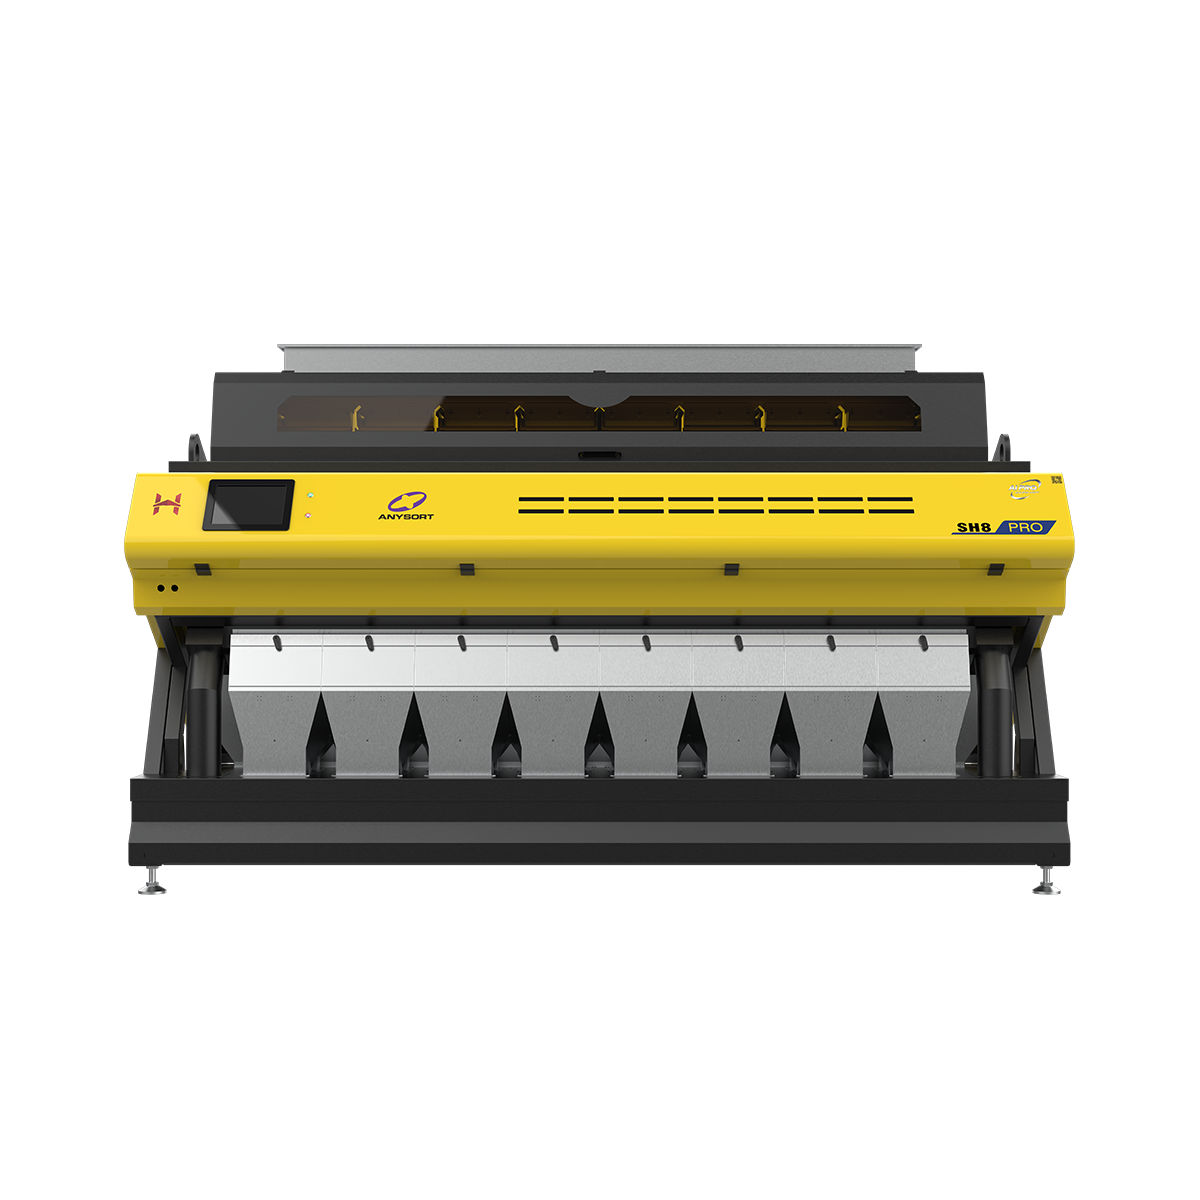
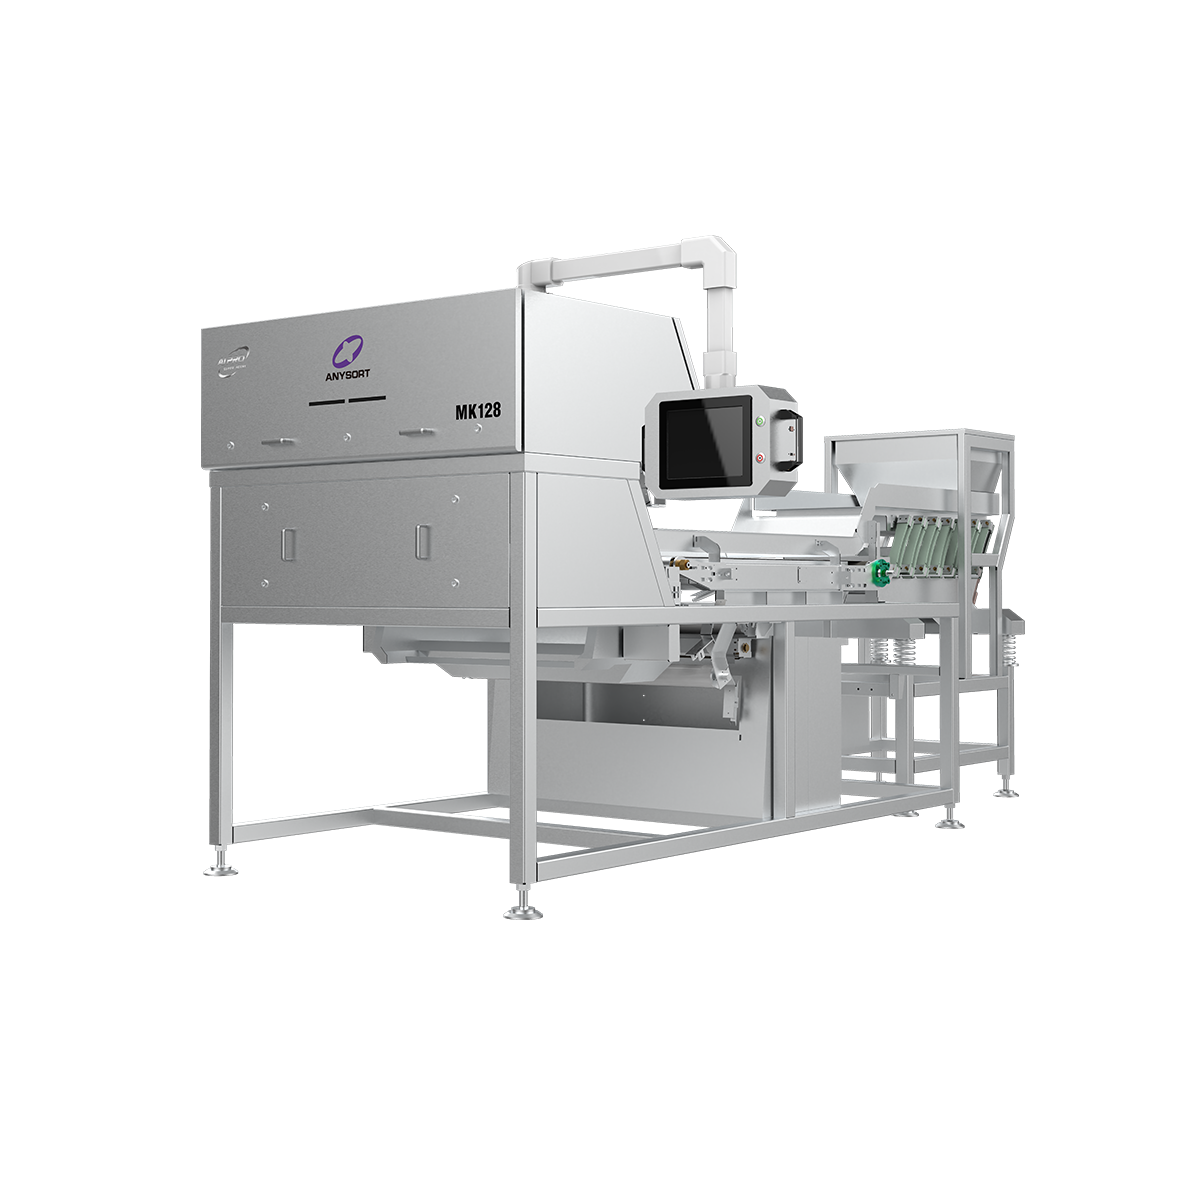
Quality sorting companies specialize in providing advanced automated systems designed to classify and separate materials based on specific quality criteria. These organizations deliver comprehensive solutions that enable businesses to enhance product consistency and eliminate defects efficiently. Quality sorting companies utilize cutting-edge technology to streamline production processes across various industries. The primary functions of quality sorting companies include material classification, defect detection, and product grading. These companies develop sophisticated sorting equipment that examines items using visual imaging, artificial intelligence, and sensor technology to ensure only premium products reach customers. Quality sorting companies serve sectors including food processing, recycling, agriculture, and manufacturing. Technological features delivered by quality sorting companies incorporate machine vision systems, spectral analysis, and real-time data processing. Modern quality sorting companies integrate artificial intelligence algorithms that continuously learn and improve detection accuracy. Advanced quality sorting companies employ multi-camera systems and high-speed processors to evaluate thousands of items per minute. Applications for quality sorting companies extend across diverse markets. In food production, quality sorting companies remove contaminated or substandard items. Manufacturing sectors utilize quality sorting companies to inspect components and ensure consistency. Recycling facilities partner with quality sorting companies to segregate materials efficiently. Agricultural operations depend on quality sorting companies for grain and produce grading. These versatile solutions help quality sorting companies maintain relevance across expanding industrial demands while delivering measurable improvements in product quality and operational efficiency.

New Products

Quality sorting companies deliver transformative benefits that directly impact your bottom line and operational performance. When you partner with quality sorting companies, you gain access to proven sorting technology that reduces manual inspection labor, saving significant personnel costs while improving accuracy rates substantially. Quality sorting companies eliminate human error from the sorting process, ensuring consistent product quality that strengthens customer satisfaction and brand reputation. Operationally, quality sorting companies enhance production throughput by processing materials at speeds that manual inspection cannot match. Your facility experiences minimal downtime since quality sorting companies offer reliable, continuous operation without fatigue-related performance degradation. Quality sorting companies provide detailed analytics and reporting systems that give you real-time visibility into your production quality metrics, enabling data-driven decision-making. The application suitability of quality sorting companies spans numerous industries and material types. Whether you handle agricultural products, manufactured components, or recycled materials, quality sorting companies adapt to your specific requirements through customizable parameters and adjustable sorting criteria. Quality sorting companies prove particularly valuable for businesses processing high volumes where manual quality control becomes impractical or cost-prohibitive. From a decision-useful perspective, quality sorting companies represent smart investments that deliver rapid return on investment through waste reduction and increased sellable product volume. Your business gains competitive advantage by consistently delivering superior quality products while reducing production costs. Quality sorting companies enable scalability, allowing your operation to grow production capacity without proportionally increasing quality control expenses. These solutions position your company as a quality leader while protecting profit margins through automated, reliable sorting performance that stakeholders recognize as essential to modern production success.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

quality sorting companies

Advanced Machine Vision Technology

Advanced Machine Vision Technology

Quality sorting companies employ sophisticated machine vision systems that capture and analyze product images with extraordinary precision. This technology enables quality sorting companies to detect microscopic defects, color variations, and structural anomalies that human inspectors would inevitably miss. The cameras used by quality sorting companies operate at incredible speeds, examining thousands of items every minute without sacrificing accuracy. Quality sorting companies integrate multi-spectral imaging capabilities that identify contaminants invisible to the naked eye. This advanced approach ensures quality sorting companies deliver unparalleled detection reliability across diverse product types. Businesses leveraging quality sorting companies benefit from consistent, objective quality assessments that eliminate subjective human judgment from sorting decisions. The investment in machine vision technology proves essential for companies competing in quality-sensitive markets where customer expectations demand absolute consistency and purity.
Artificial Intelligence and Machine Learning Integration

Artificial Intelligence and Machine Learning Integration

Modern quality sorting companies leverage artificial intelligence systems that continuously improve detection accuracy through machine learning algorithms. These intelligent systems enable quality sorting companies to adapt sorting parameters in real-time based on detected patterns and variations in product batches. Quality sorting companies implement AI-powered analytics that identify emerging quality issues before they become significant problems. The predictive capabilities of quality sorting companies allow facility managers to make proactive adjustments to production processes. Quality sorting companies train their algorithms on millions of images and data points, creating exceptionally sophisticated recognition systems. This technological advantage means quality sorting companies deliver superior performance compared to basic sorting equipment. Customers who choose quality sorting companies gain access to technology that becomes increasingly accurate and efficient over time, maximizing long-term value and competitive advantage while reducing dependency on manual intervention and human expertise.
Real-Time Data Analytics and Reporting

Real-Time Data Analytics and Reporting

Quality sorting companies provide comprehensive monitoring systems that generate actionable insights from continuous sorting operations. Advanced quality sorting companies capture detailed metrics about product composition, defect frequencies, and sorting accuracy trends. The data analytics platforms offered by quality sorting companies enable facility managers to identify quality improvement opportunities systematically. Quality sorting companies deliver customizable reports that highlight performance against established quality benchmarks and production targets. This transparency helps stakeholders understand sorting effectiveness and justify continued investment in automated systems. Quality sorting companies transform raw production data into strategic information that drives operational excellence. By implementing quality sorting companies, businesses gain competitive intelligence revealing patterns that guide product development and process optimization initiatives. The reporting capabilities ensure quality sorting companies provide clear documentation for regulatory compliance and quality assurance requirements, strengthening customer confidence and meeting industry standards consistently.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy