Wheat Color Sorter Machine: Quality Grain Sorting

All Categories

wheat color sorter machine

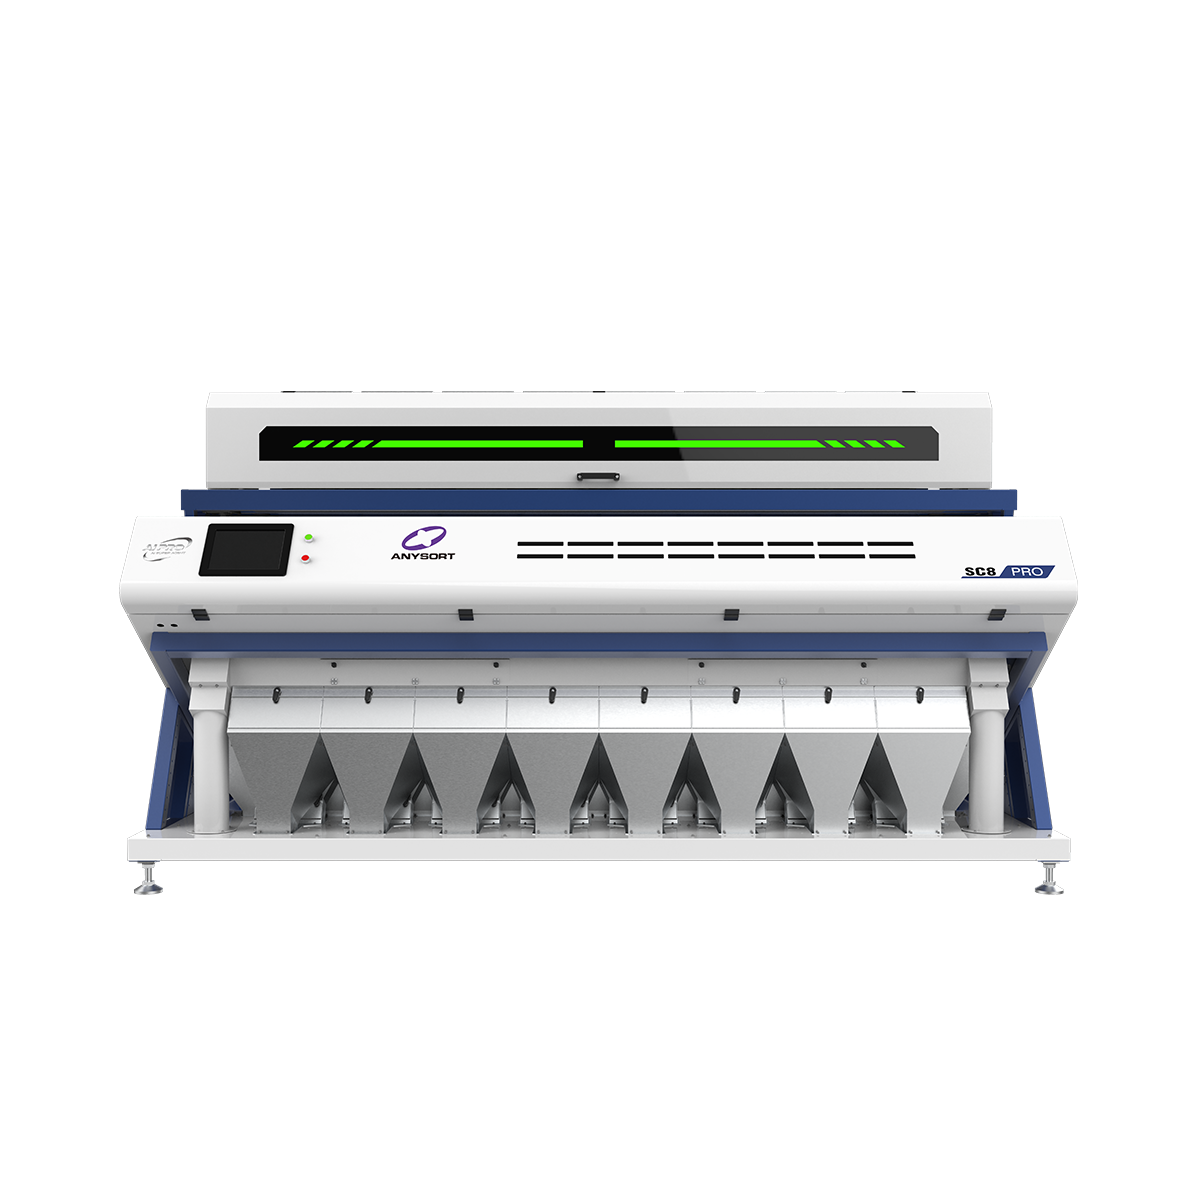
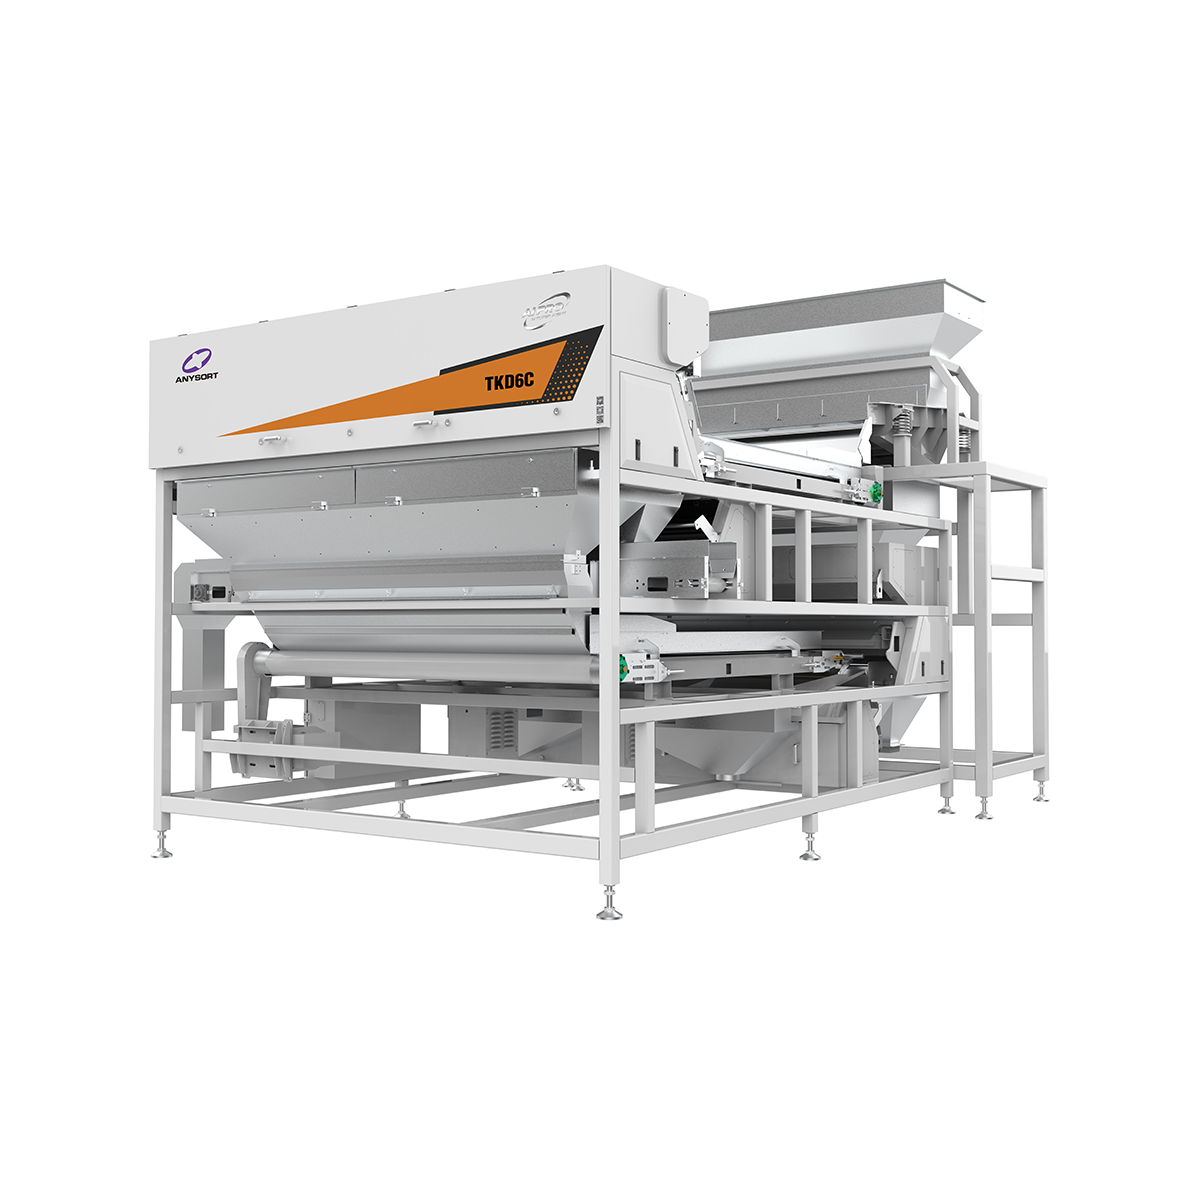
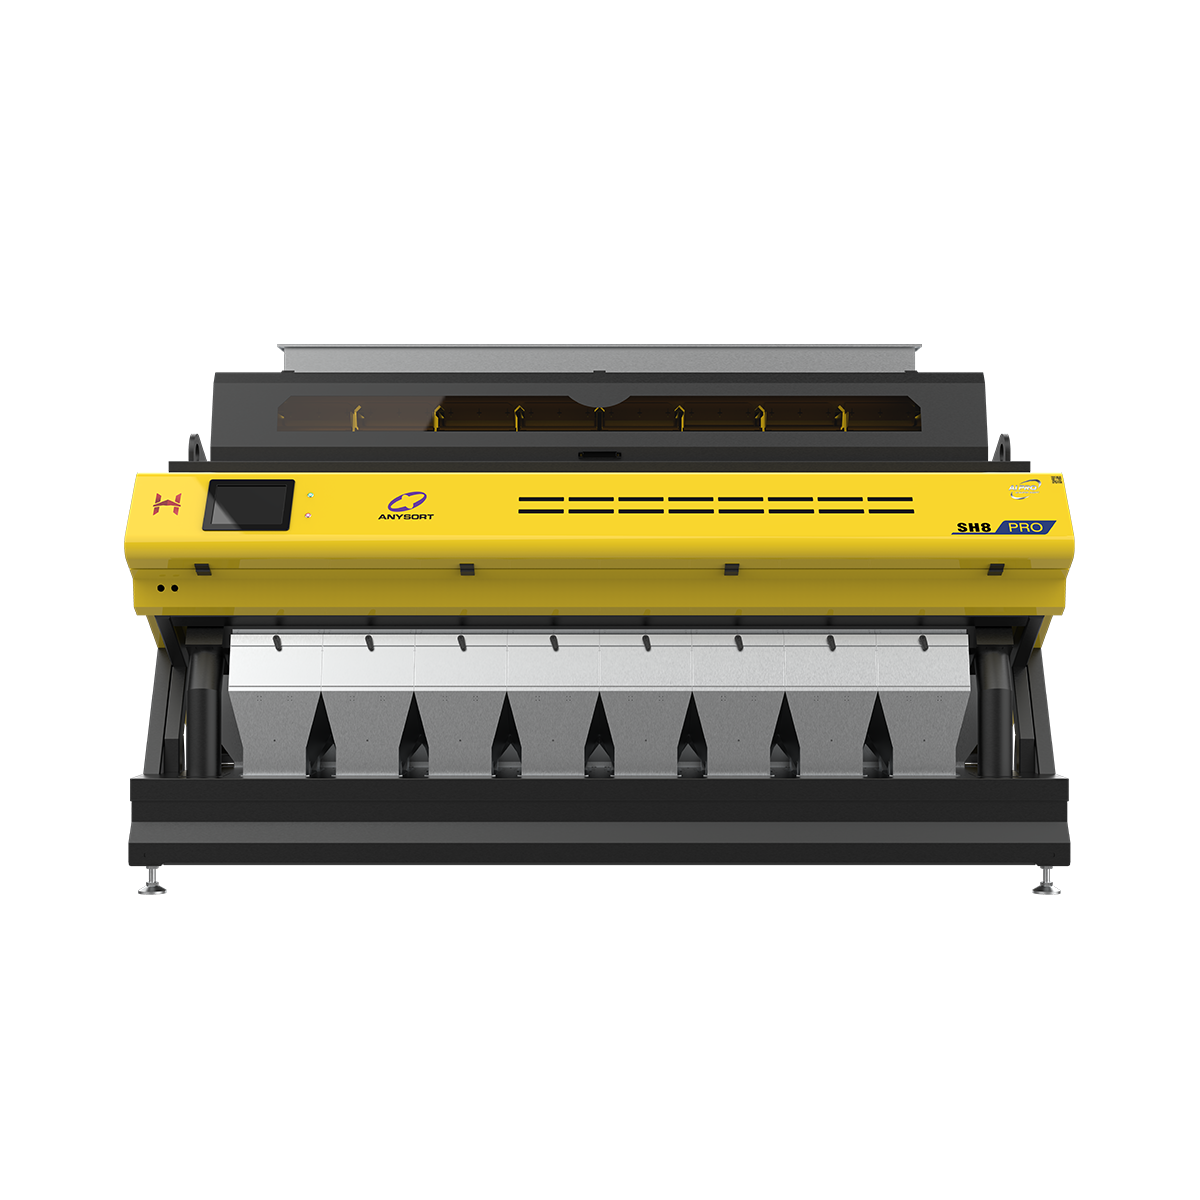
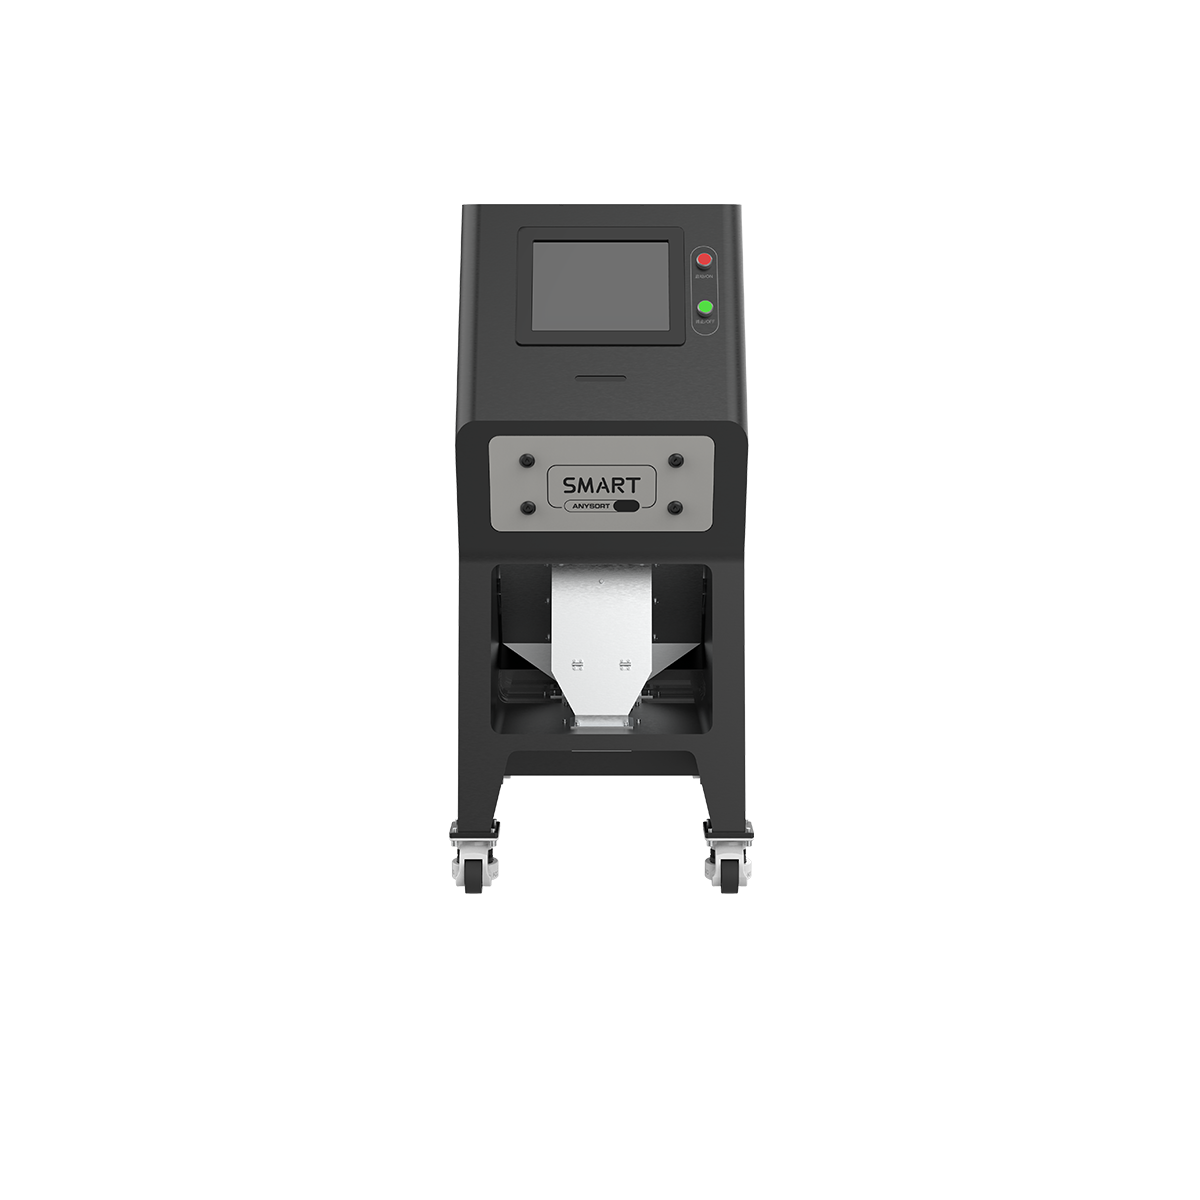
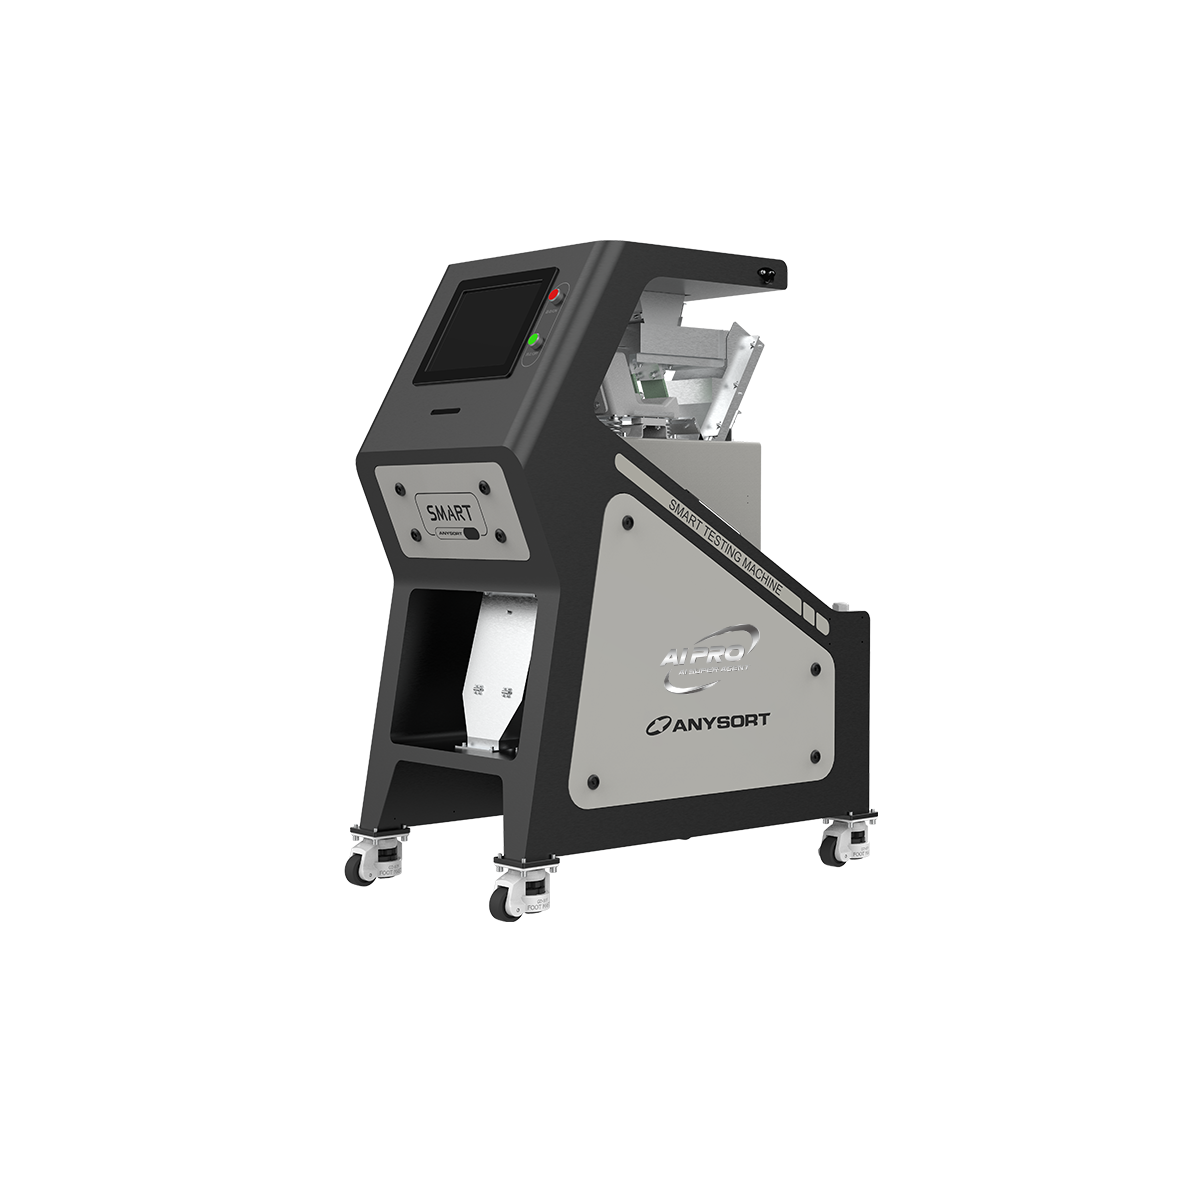
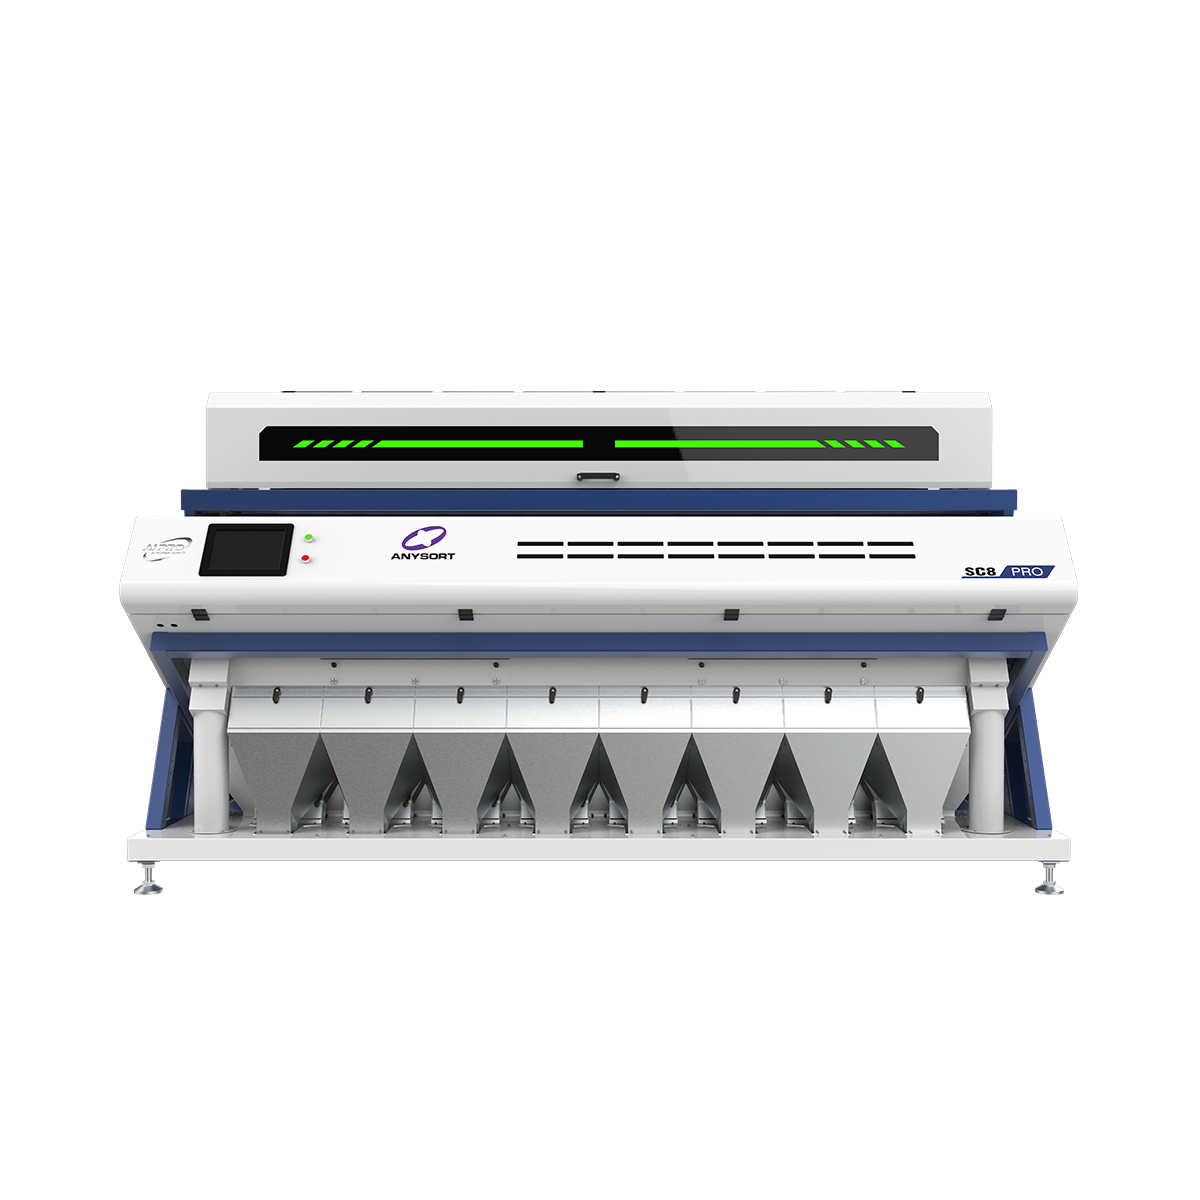
A wheat color sorter machine represents advanced technology designed to separate wheat grains based on color and quality characteristics. This wheat color sorter machine utilizes optical sensors and artificial intelligence to identify and remove discolored, damaged, or foreign particles from bulk wheat shipments with exceptional precision. The wheat color sorter machine operates through a sophisticated system where grains pass through a detection chamber, allowing high-speed cameras to capture detailed images of each grain. The machine then analyzes these images against programmed quality standards, automatically ejecting substandard grains while retaining premium quality wheat. Modern wheat color sorter machine models process thousands of grains per second, delivering consistent results that meet international quality requirements. The wheat color sorter machine incorporates multiple sorting channels, enabling simultaneous separation of different wheat varieties or quality grades. Its technological framework includes real-time monitoring systems, user-friendly interfaces, and adjustable parameters to accommodate various wheat types and customer specifications. The wheat color sorter machine finds extensive applications in flour mills, grain trading facilities, agricultural cooperatives, and food processing plants worldwide. By implementing a wheat color sorter machine into operations, facilities ensure that only premium-grade wheat reaches production lines, significantly reducing waste and enhancing final product quality. This equipment has become essential for businesses committed to maintaining strict quality control standards in the competitive grain market.

New Product Releases

The wheat color sorter machine delivers substantial operational benefits that directly impact profitability and efficiency. First, this wheat color sorter machine eliminates manual sorting labor, reducing personnel costs while maintaining consistent quality standards. The automation provided by a wheat color sorter machine ensures faster processing speeds, allowing facilities to handle larger grain volumes without expanding workforce requirements. Users benefit from the wheat color sorter machine's remarkable accuracy, as optical technology detects defects invisible to human inspectors, preventing contaminated grain from reaching consumers. The wheat color sorter machine's precision sorting improves end-product quality, enabling businesses to command premium prices for superior wheat grades. Environmental advantages emerge through reduced waste, as the wheat color sorter machine maximizes usable grain recovery rates compared to conventional sorting methods. The wheat color sorter machine requires minimal maintenance, featuring durable components designed for continuous operation in demanding industrial environments. Financial benefits include rapid return on investment through increased productivity and reduced material waste across production cycles. The wheat color sorter machine adapts seamlessly to different wheat varieties, from soft white wheat to hard red winter wheat, offering remarkable versatility. Facilities implementing a wheat color sorter machine experience enhanced traceability and documentation capabilities, supporting compliance with food safety regulations. The technology integrated into each wheat color sorter machine provides real-time data analytics, allowing operators to monitor performance metrics and optimize sorting parameters. Customers choosing a wheat color sorter machine gain competitive advantages through improved product consistency, stronger customer relationships, and sustainable business growth. The wheat color sorter machine represents a smart investment for any grain processing operation seeking modernization and operational excellence.

Practical Tips

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

wheat color sorter machine

Advanced Optical Detection Technology

Advanced Optical Detection Technology

The wheat color sorter machine employs cutting-edge optical sensor technology capable of analyzing thousands of grains every second with extraordinary precision. This wheat color sorter machine uses multi-spectral imaging systems that detect minute color variations, physical defects, and contaminants that traditional sorting methods miss entirely. The sophisticated sensors within the wheat color sorter machine continuously calibrate to environmental lighting conditions, ensuring consistent performance throughout operating days. High-resolution cameras integrated into the wheat color sorter machine capture detailed grain profiles, transmitting data to powerful processors that make instantaneous sorting decisions. The wheat color sorter machine's optical system distinguishes between quality grades with accuracy exceeding ninety-nine percent, significantly surpassing manual inspection capabilities. This technological advancement makes the wheat color sorter machine indispensable for maintaining food safety compliance and meeting international quality certifications required by major buyers.
High-Speed Processing Capacity

High-Speed Processing Capacity

Modern wheat color sorter machine models achieve processing speeds of up to ten tons per hour, dramatically exceeding traditional sorting methods. The wheat color sorter machine processes individual grains at millisecond intervals, enabling facilities to maximize throughput without sacrificing sorting accuracy or quality standards. This exceptional speed offered by the wheat color sorter machine allows grain facilities to process larger volumes with fewer machines, reducing facility footprint and operational complexity. The wheat color sorter machine maintains peak performance consistently throughout extended shifts, eliminating productivity losses associated with worker fatigue or human limitations. Advanced sorting channels integrated into each wheat color sorter machine distribute grains efficiently, preventing bottlenecks and ensuring smooth material flow. The wheat color sorter machine's processing capacity translates directly into financial benefits, enabling facilities to meet growing demand while maintaining competitive pricing structures. Businesses implementing this wheat color sorter machine experience substantially reduced processing timelines, allowing faster delivery to customers and improved cash flow management.
Intelligent Quality Grading System

Intelligent Quality Grading System

The wheat color sorter machine features intelligent algorithms that automatically categorize grains into multiple quality grades simultaneously. This wheat color sorter machine's software learns from operator input, continuously refining sorting accuracy and adapting to specific customer requirements. The wheat color sorter machine provides detailed sorting reports showing grade distribution, contamination levels, and quality metrics valuable for process optimization. Operators can program customized sorting parameters into the wheat color sorter machine, enabling flexible adjustment for different wheat varieties and market demands. The wheat color sorter machine generates comprehensive documentation supporting food traceability requirements and regulatory compliance across export markets. Real-time monitoring capabilities of the wheat color sorter machine alert operators to performance changes, enabling immediate corrective action. This intelligent system within the wheat color sorter machine maximizes value extraction from grain inventory while minimizing waste throughout production cycles.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy