Color Sorting Machines | Advanced Optical Sorting

All Categories

color sorting machines

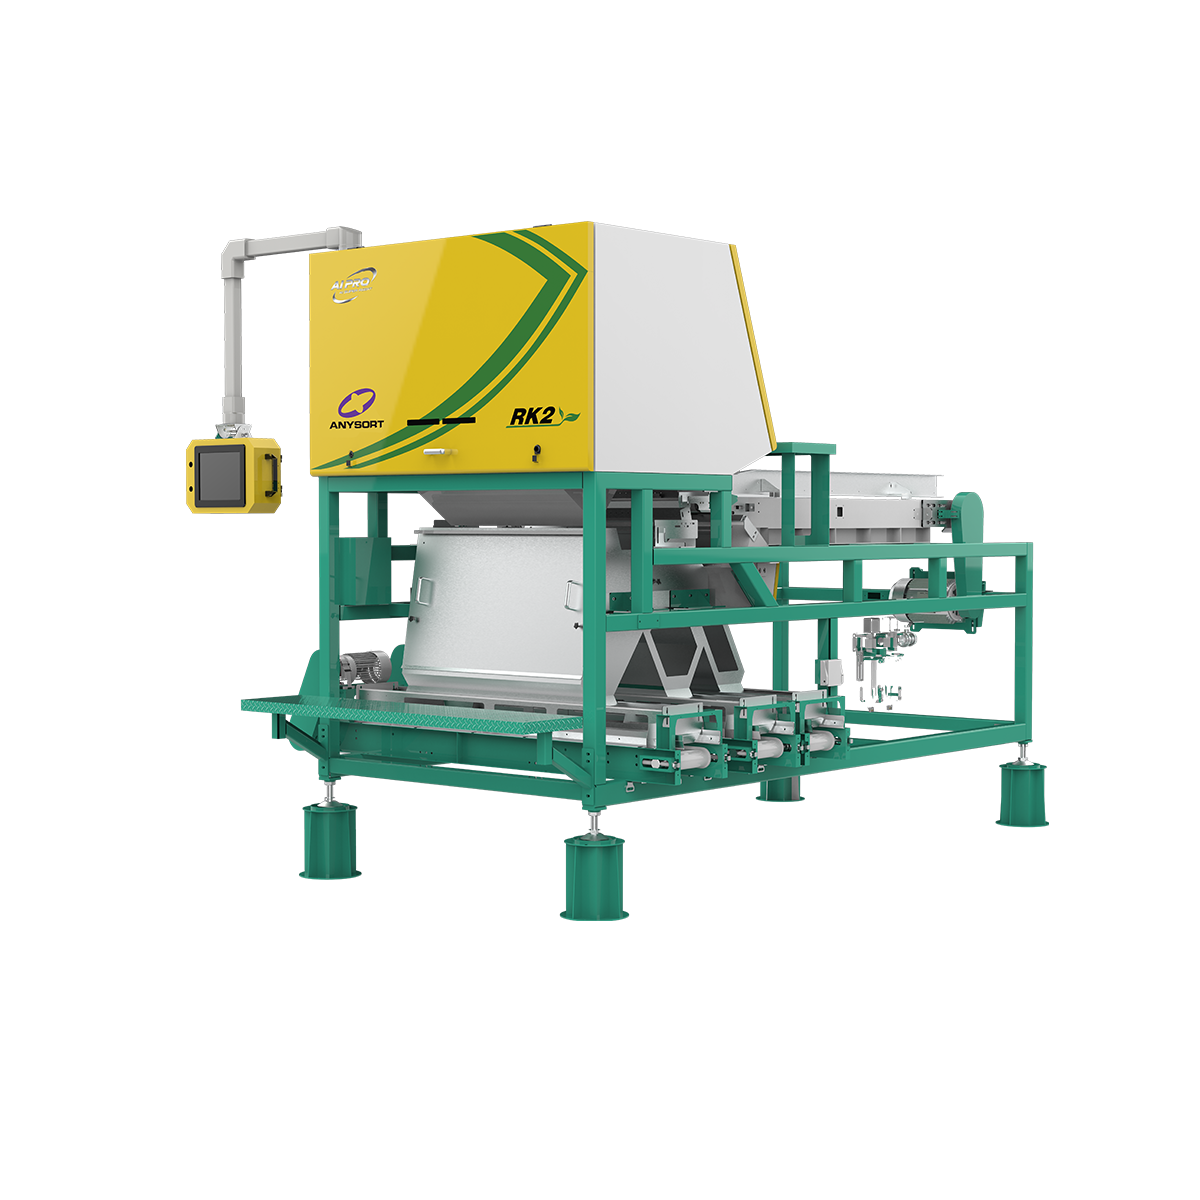
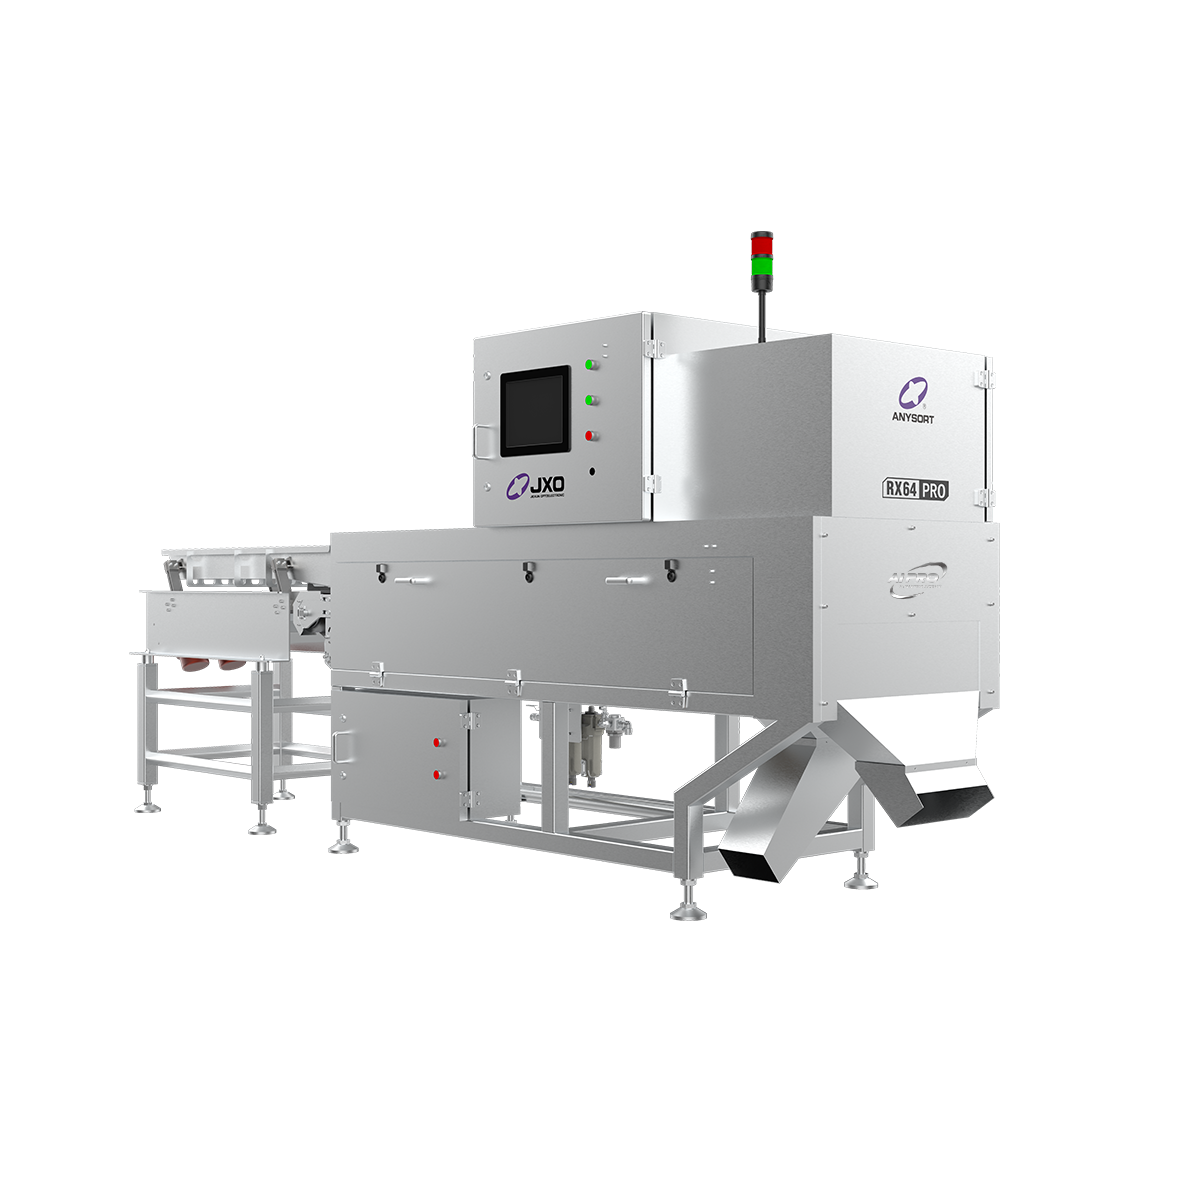
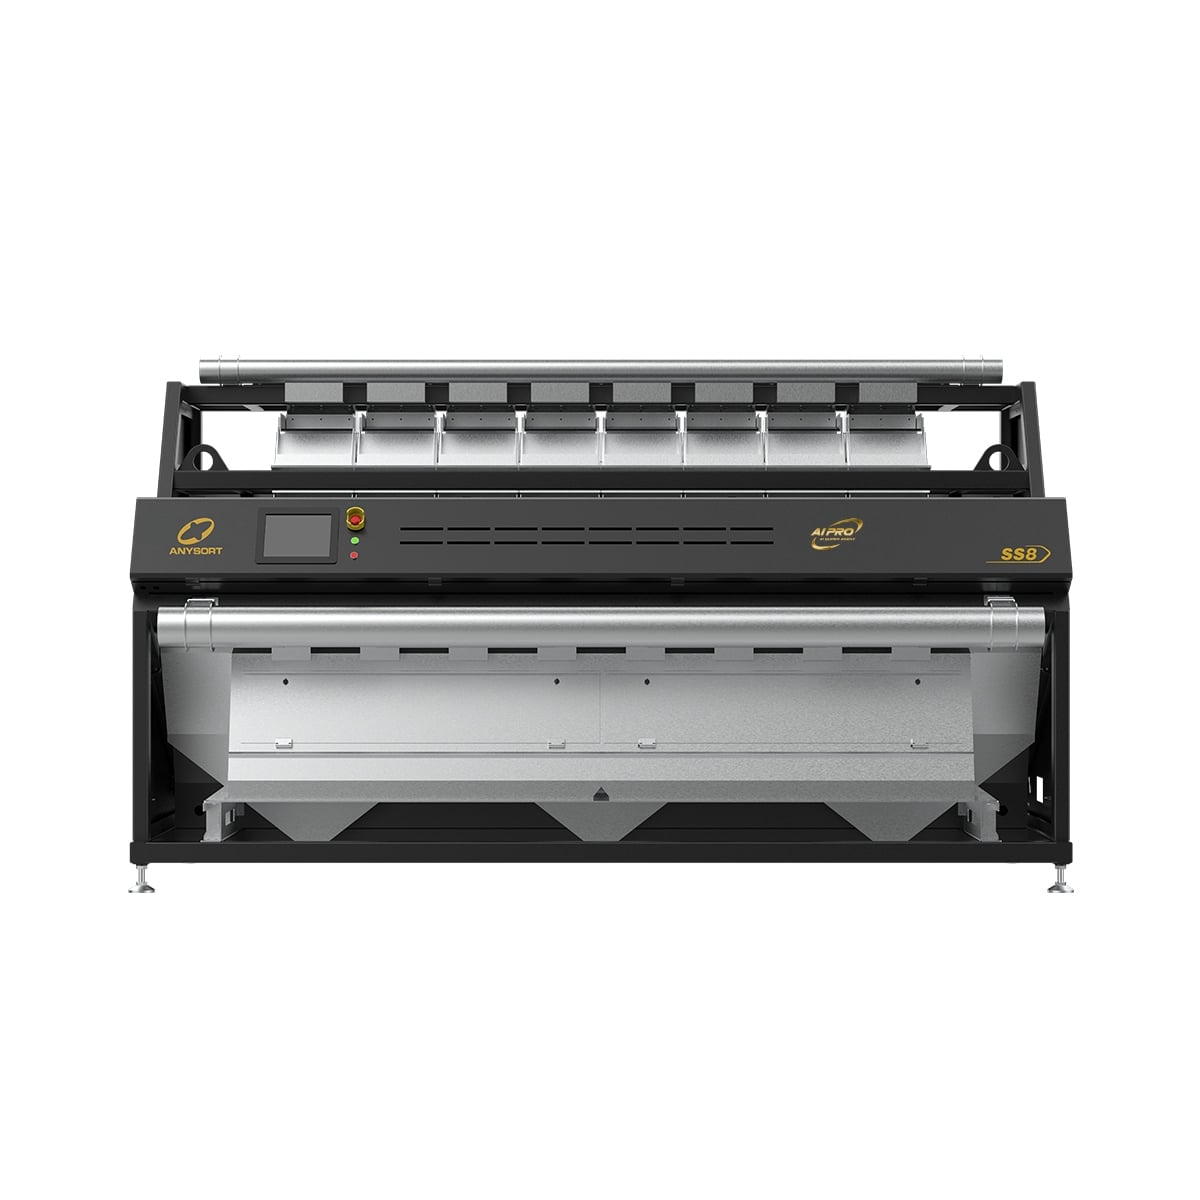
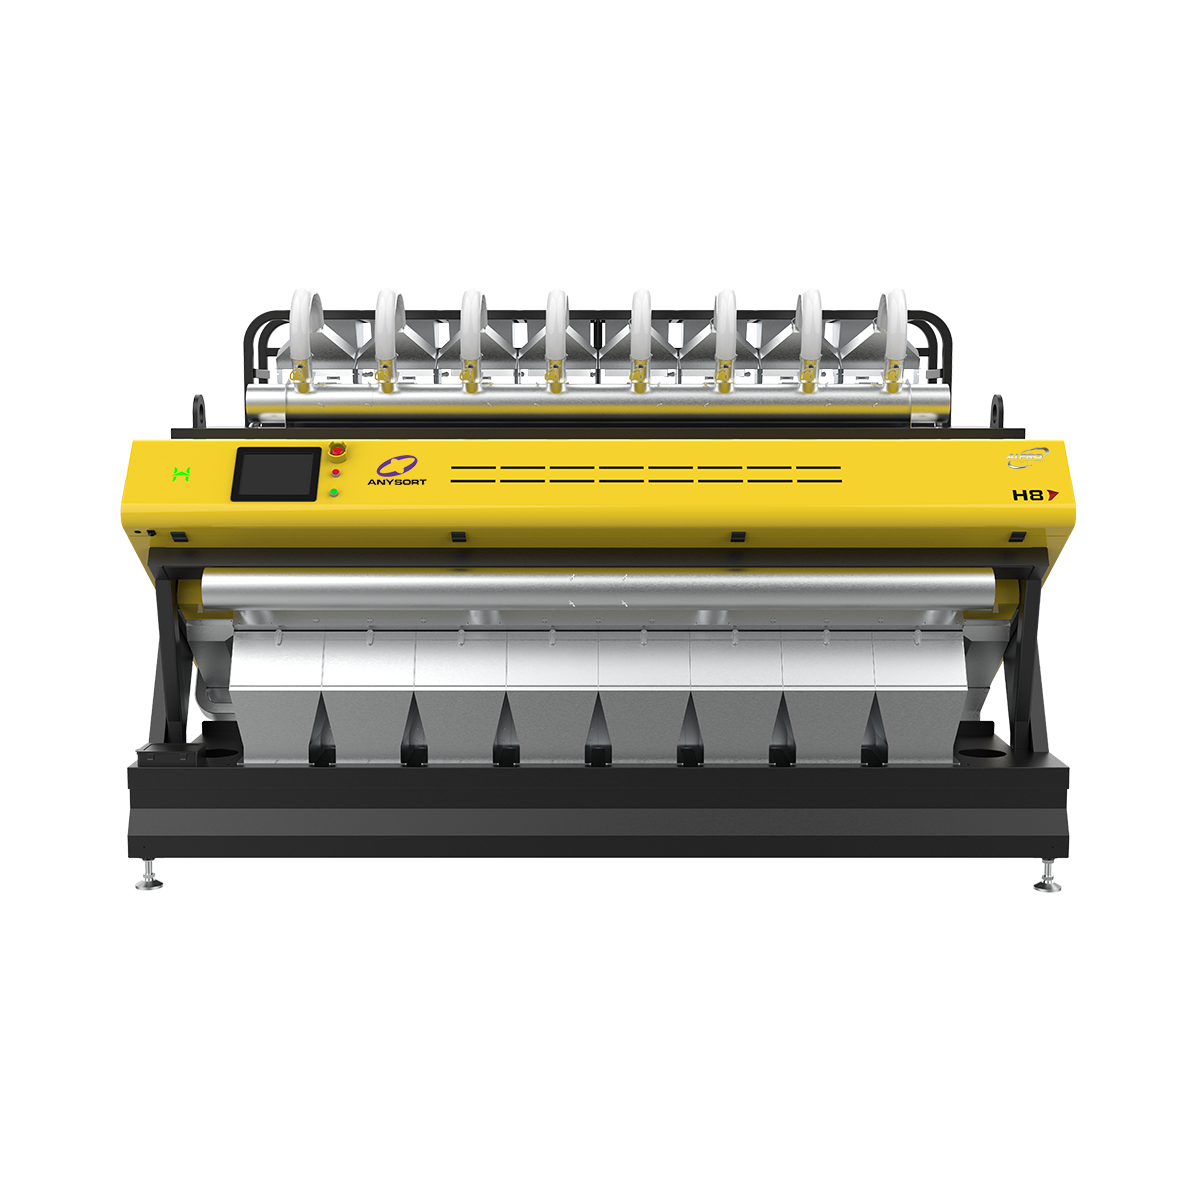
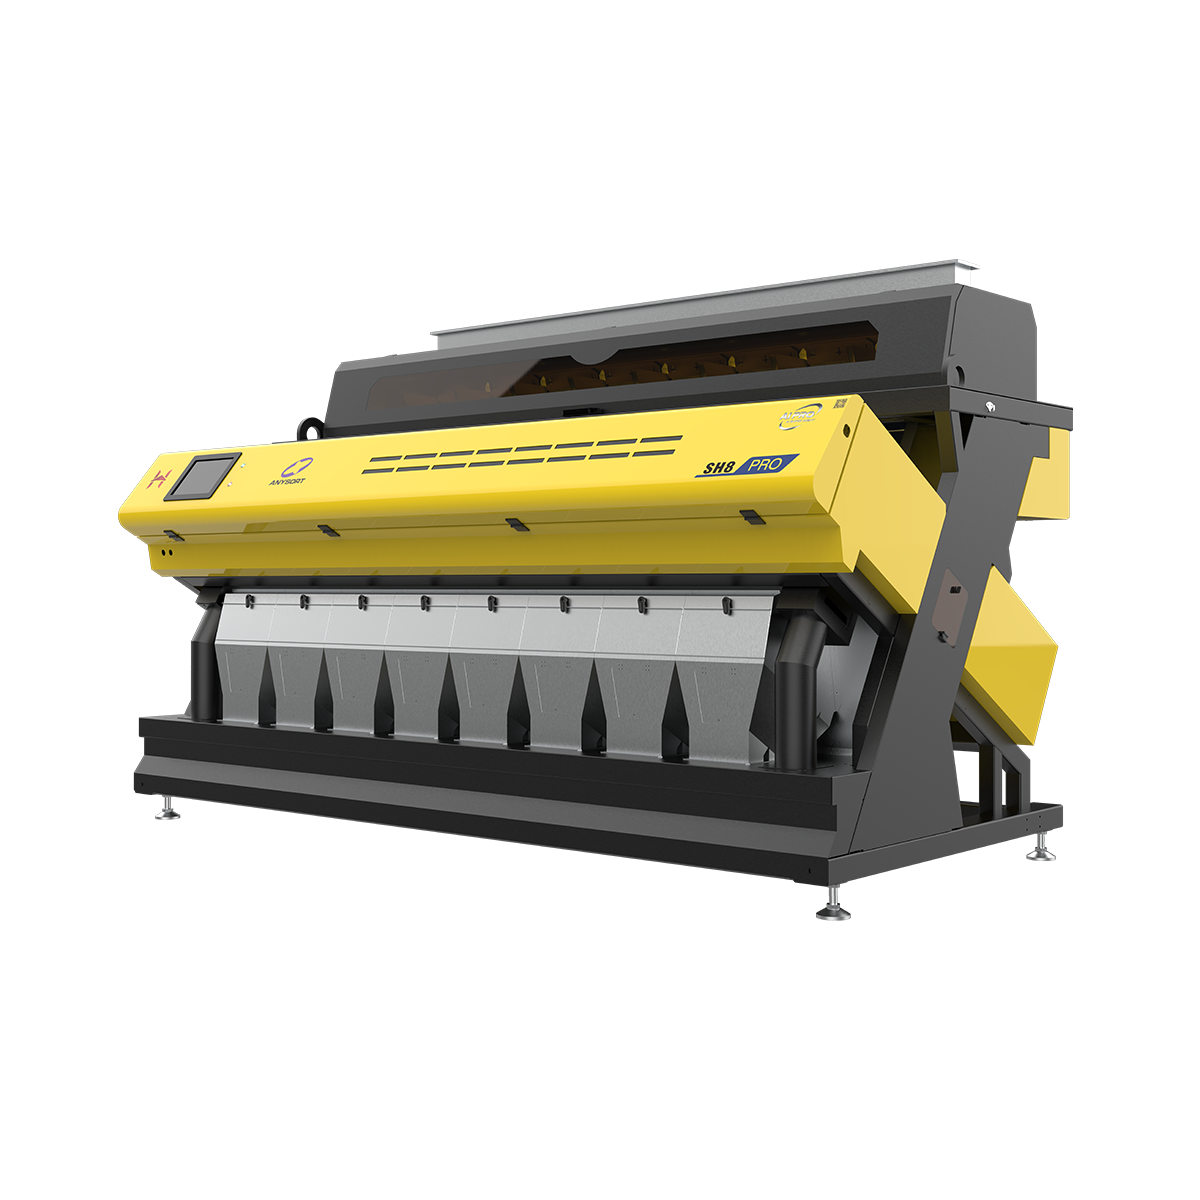
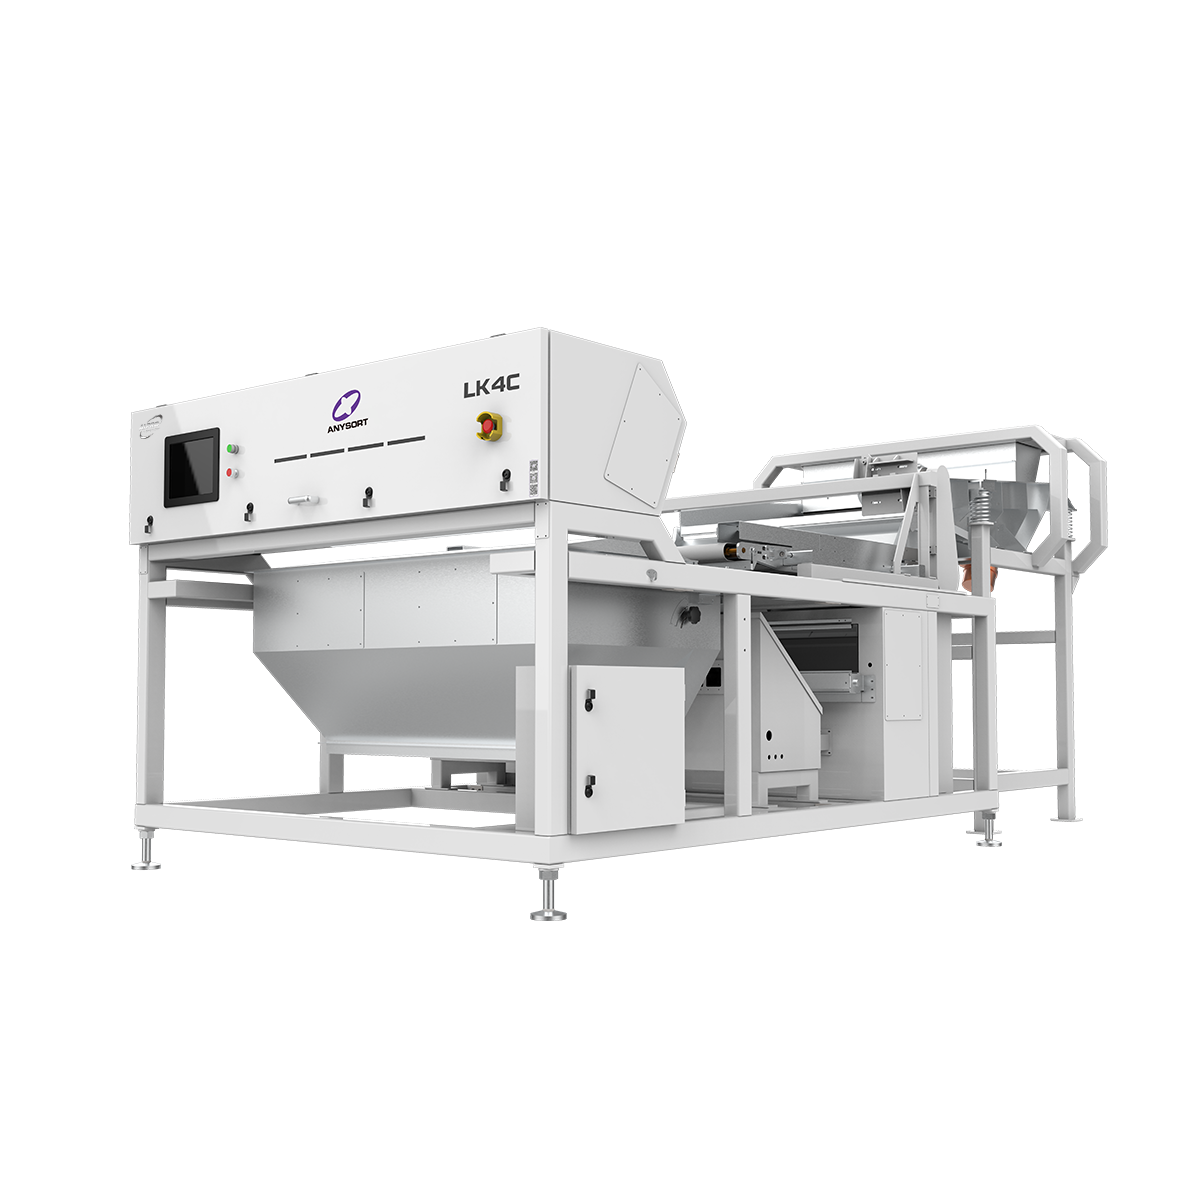
Color sorting machines represent advanced optical technology designed to automatically separate and grade materials based on color specifications. These sophisticated systems utilize high-resolution cameras and artificial intelligence to identify and categorize items with exceptional precision. Color sorting machines have become indispensable in numerous industries, from food processing to recycling and agriculture. The primary function of color sorting machines is to remove defective, discolored, or foreign materials from production streams. Using LED lighting and specialized sensors, these machines scan each item individually, comparing colors against predefined standards. Color sorting machines process materials at impressive speeds, often handling thousands of items per minute without compromising accuracy. Technologically, color sorting machines incorporate advanced features including multi-spectral imaging, machine learning algorithms, and pneumatic ejection systems. The systems employ sophisticated software that continuously adapts to variations in material properties and lighting conditions. Color sorting machines utilize real-time data processing to make instantaneous sorting decisions, ensuring consistent quality control throughout production cycles. Applications for color sorting machines span diverse sectors. In the food industry, they inspect grains, nuts, coffee beans, and dried fruits. Agricultural producers use color sorting machines for seed cleaning and crop sorting. Recycling facilities deploy these machines for plastic and material separation. Manufacturing environments benefit from color sorting machines for quality assurance and defect detection, making them essential investment for companies prioritizing product excellence and operational efficiency.

New Product Releases

Color sorting machines deliver exceptional practical benefits that directly impact operational performance and profitability. These systems significantly reduce manual labor requirements, as the machines automatically handle sorting tasks that previously demanded extensive workforce resources. By investing in color sorting machines, companies achieve substantial cost reductions while improving sorting accuracy far beyond human capabilities. Operational efficiency represents a major advantage of color sorting machines. These systems operate continuously without fatigue, maintaining consistent performance throughout extended production runs. Color sorting machines eliminate human error and bias, ensuring every item meets predetermined quality standards. The speed atency of color sorting machines means businesses process higher volumes in shorter timeframes, directly translating to increased productivity and revenue generation. Quality improvement stands out as another critical benefit. Color sorting machines identify and remove defective items that human inspectors might overlook, protecting brand reputation and customer satisfaction. These machines provide reliable contamination detection, preventing non-compliant products from reaching customers. Implementing color sorting machines demonstrates commitment to quality excellence that resonates with discerning consumers. Cost-effectiveness extends beyond labor savings. Color sorting machines reduce product waste by salvaging items with minor discoloration issues, maximizing material utilization. The machines minimize costly recalls and returns by ensuring only premium products ship to customers. Color sorting machines provide measurable return on investment through improved yields and reduced losses. Decision-useful context shows color sorting machines suit operations of varying scales. Small producers gain competitive advantages through automation, while large manufacturers enhance already-robust processes. Color sorting machines adapt to specific industry requirements, whether processing food products, recyclables, or manufactured components, making them versatile solutions for diverse business environments seeking operational excellence and consistent quality delivery.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

color sorting machines

Advanced Optical Technology for Unmatched Precision

Advanced Optical Technology for Unmatched Precision

Color sorting machines employ cutting-edge optical sensors and multi-spectral cameras that capture detailed images of every item passing through the system. This advanced imaging capability allows color sorting machines to detect subtle color variations that human eyes cannot perceive. The precision of color sorting machines ensures accurate identification of defects, foreign materials, and quality issues, regardless of production speed. Multi-spectral analysis enables color sorting machines to evaluate items across numerous wavelengths simultaneously, providing comprehensive assessment of material characteristics. This technological sophistication transforms color sorting machines into reliable quality guardians that maintain consistent standards throughout your production process. The accuracy achieved by color sorting machines minimizes false rejections while catching genuine defects, protecting product integrity and brand reputation. Industrial facilities implementing color sorting machines experience dramatic improvements in quality consistency, reduced customer complaints, and enhanced market competitiveness through superior product uniformity.
Intelligent Machine Learning Algorithms for Continuous Improvement

Intelligent Machine Learning Algorithms for Continuous Improvement

Modern color sorting machines feature sophisticated artificial intelligence that learns and adapts to changing production conditions automatically. These intelligent systems allow color sorting machines to recognize patterns and improve sorting accuracy over extended operational periods. Machine learning capabilities enable color sorting machines to handle material variations that static sorting parameters cannot address effectively. Color sorting machines continuously refine their decision-making processes, becoming increasingly efficient as they process more items. This adaptive intelligence ensures color sorting machines remain effective even when raw materials demonstrate natural variations in appearance or composition. The machine learning integration transforms color sorting machines into self-improving systems that require minimal manual adjustment or recalibration. Businesses gain the advantage of consistently accurate sorting that evolves alongside their production needs, making color sorting machines valuable long-term investments that deliver increasing returns as systems mature and optimize their performance algorithms.
High-Speed Processing with Reliable Performance

High-Speed Processing with Reliable Performance

Color sorting machines deliver impressive throughput capabilities, processing thousands of items every minute without sacrificing accuracy or requiring frequent maintenance interventions. The speed of color sorting machines dramatically accelerates production timelines, enabling businesses to meet demanding customer deadlines and increase revenue potential. Color sorting machines maintain consistent performance throughout extended operational periods, eliminating downtime associated with human fatigue or inefficiency. Pneumatic ejection systems integrated into color sorting machines ensure precisely-timed removal of rejected items at high velocities without damaging acceptable products. This combination of speed and reliability makes color sorting machines ideal for high-volume production environments where every minute impacts profitability. Color sorting machines reduce processing costs through exceptional efficiency, allowing lower per-unit processing expenses despite premium quality output. Industrial operations leverage the speed of color sorting machines to achieve competitive advantages in market response times while maintaining strict quality standards that distinguish premium products from inferior competitors.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy