Best Sorting Machines | Advanced Automation

All Categories

best sorting machines

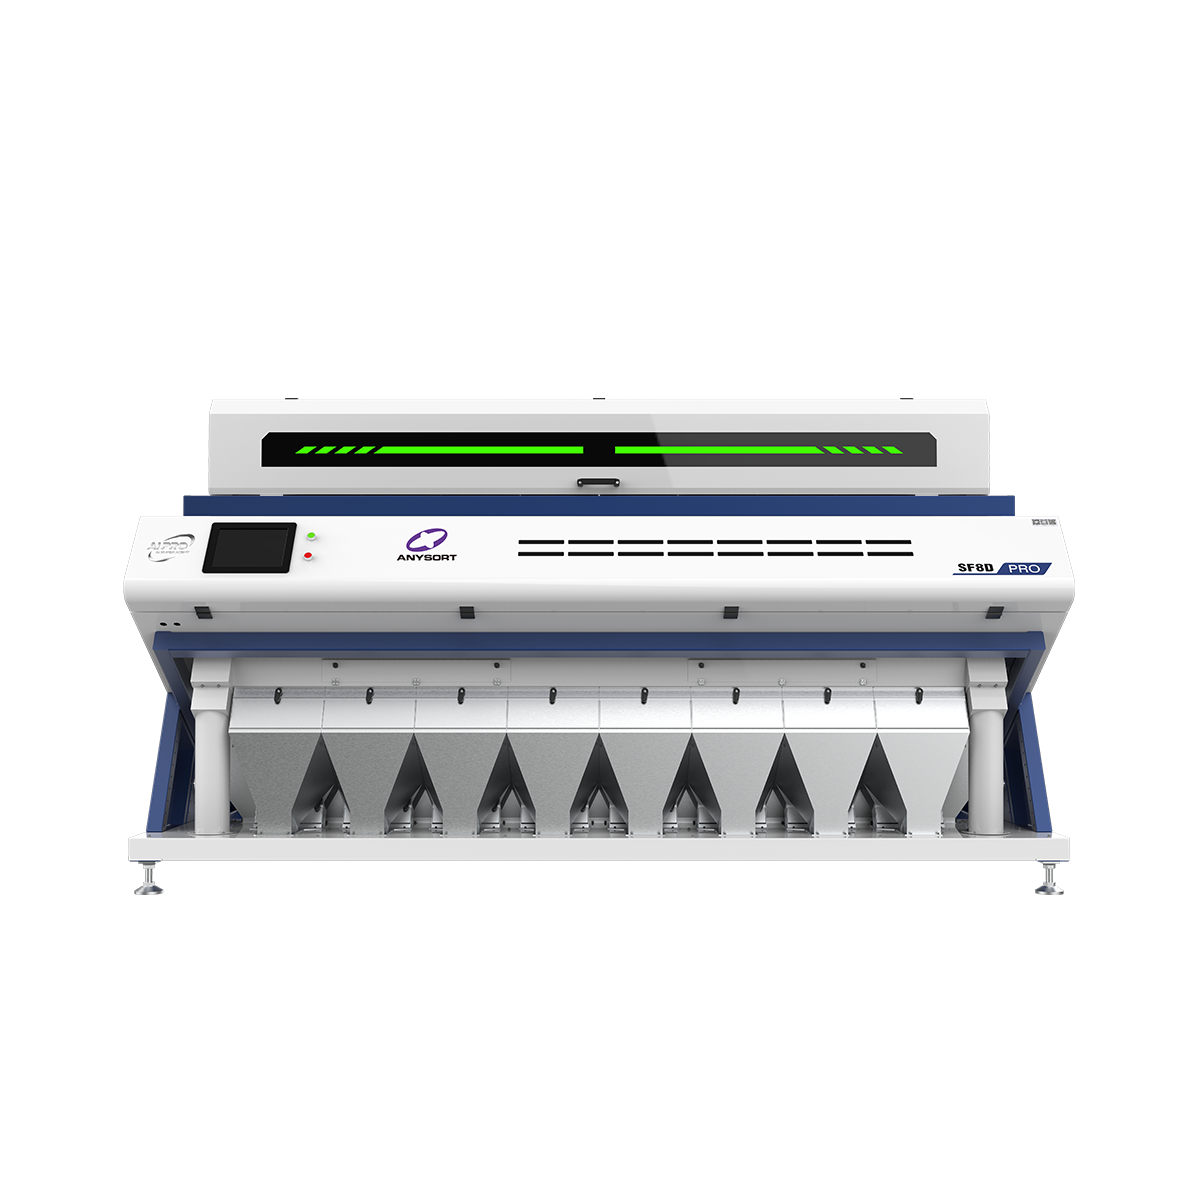
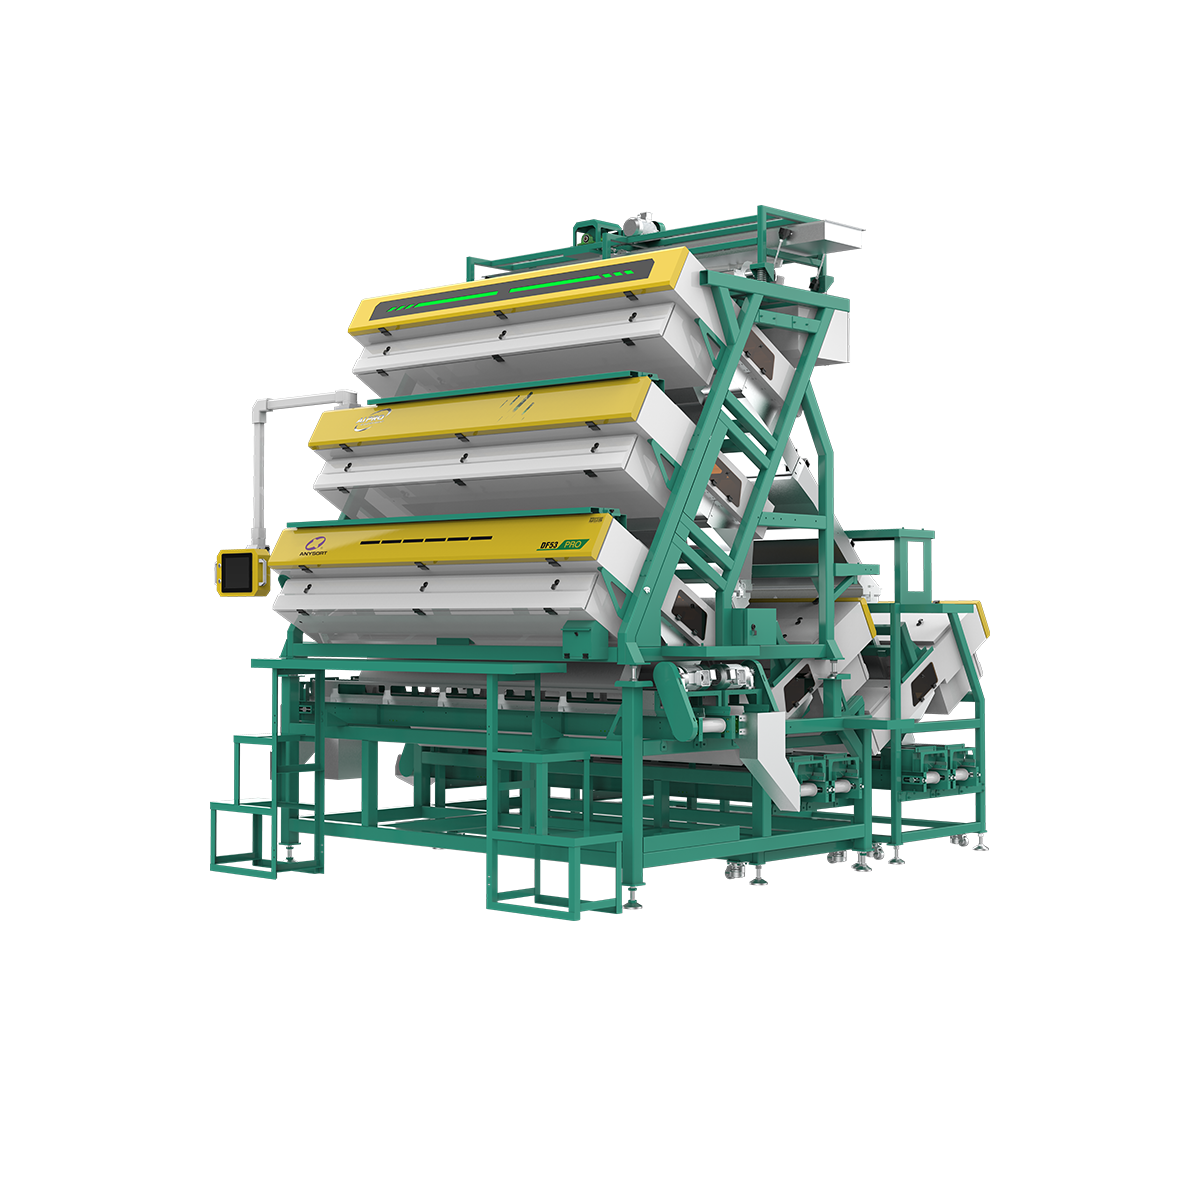
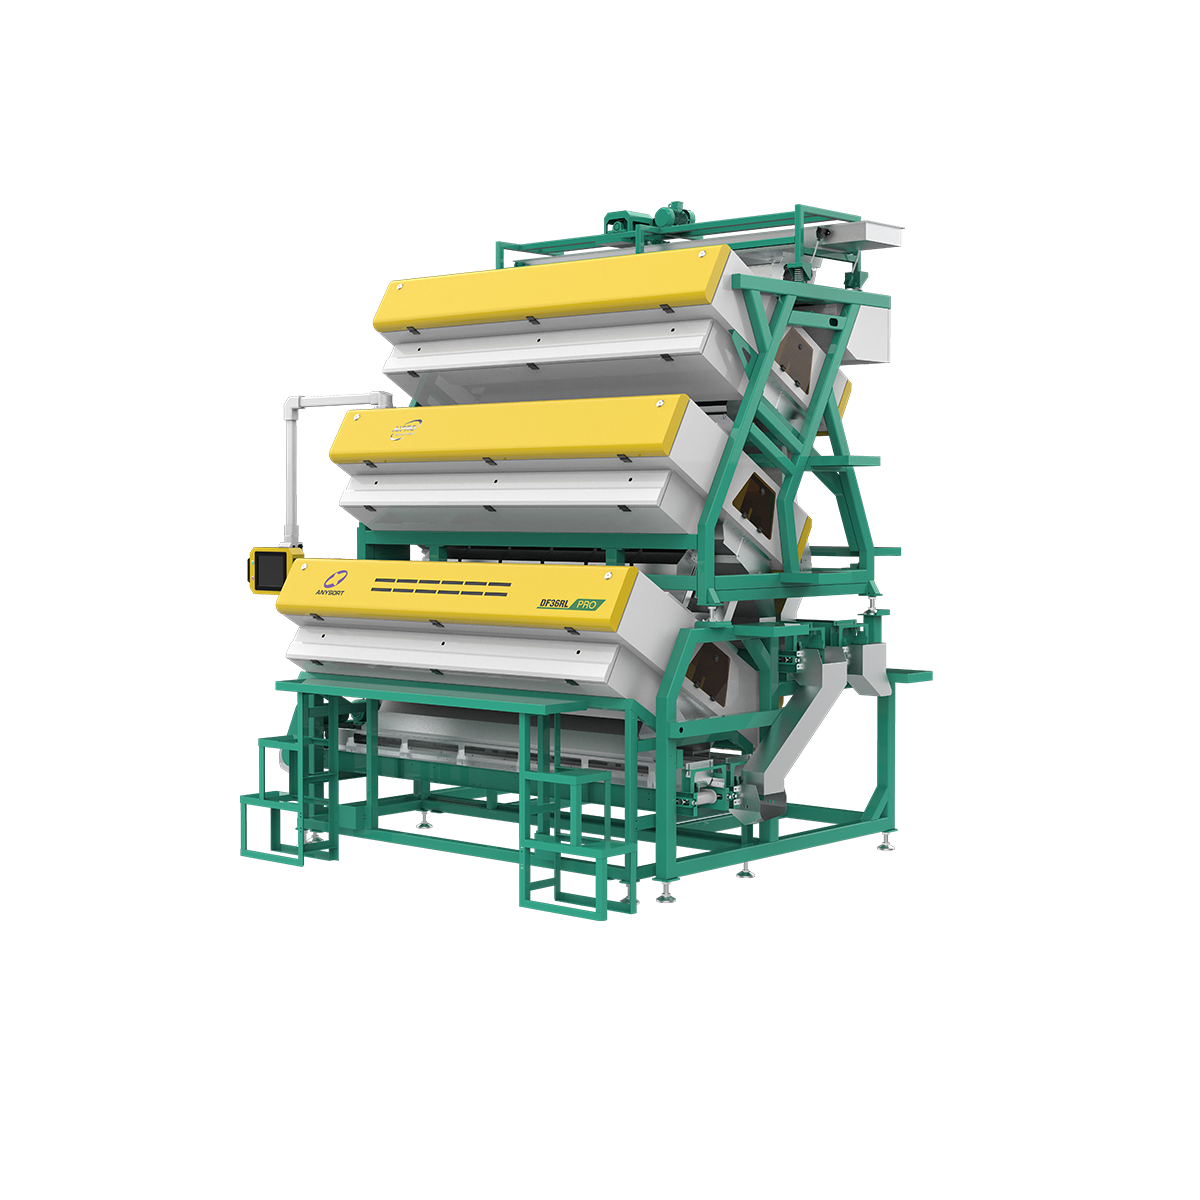
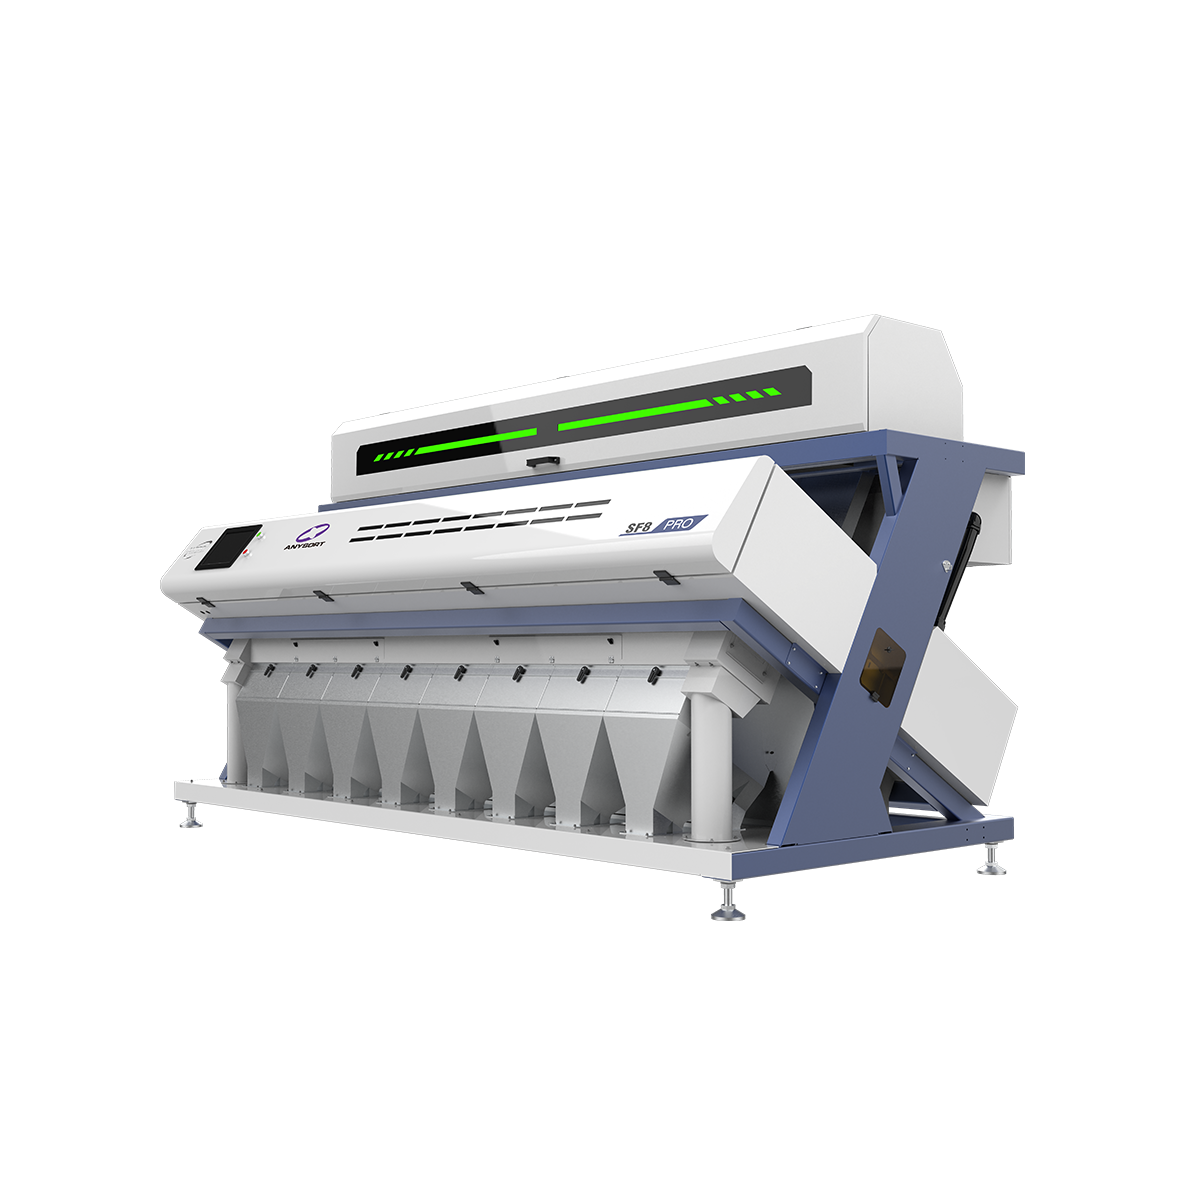
Best sorting machines represent cutting-edge technology designed to streamline material separation and organization across diverse industries. These best sorting machines utilize advanced optical sensors, artificial intelligence, and mechanical precision to categorize items by size, color, weight, and composition with remarkable accuracy. The primary function of best sorting machines involves automating the separation process, dramatically increasing throughput while maintaining consistent quality standards. Modern best sorting machines incorporate sophisticated technological features including high-speed cameras, laser detection systems, and machine learning algorithms that continuously improve sorting accuracy. These systems process thousands of items per minute, reducing manual labor requirements and human error significantly. Best sorting machines find applications in recycling facilities, food processing plants, agricultural operations, manufacturing environments, and postal services. The technological architecture of best sorting machines enables real-time decision-making through integrated computer vision systems. Operators can customize sorting parameters to meet specific requirements, making best sorting machines exceptionally versatile across different material types. Advanced best sorting machines feature modular designs, allowing businesses to scale operations as demand increases. Integration with existing production lines occurs seamlessly, minimizing disruption during implementation. These machines deliver exceptional performance metrics, processing diverse materials with precision that surpasses manual sorting capabilities by substantial margins.

New Products

Best sorting machines deliver substantial operational benefits that directly impact business profitability and efficiency. By automating the sorting process, best sorting machines eliminate repetitive manual work, allowing employees to focus on higher-value tasks requiring human judgment and expertise. This reallocation of workforce resources increases overall productivity while improving workplace safety by removing workers from potentially hazardous environments. The cost-effectiveness of best sorting machines becomes evident through reduced labor expenses and minimized material waste. These best sorting machines achieve sorting accuracy rates exceeding ninety-five percent consistently, ensuring that contaminated batches and misclassified materials are virtually eliminated. Businesses utilizing best sorting machines recover increased value from recycled materials and reduce costly processing errors. Operational benefits include continuous operation capabilities, with best sorting machines functioning reliably across extended shifts without fatigue-related performance degradation. Maintenance requirements remain minimal when proper protocols are followed, maximizing uptime and return on investment. Best sorting machines provide real-time analytics and reporting features, enabling managers to monitor performance metrics and identify optimization opportunities instantly. Application suitability spans multiple industries, making best sorting machines invaluable for recycling operations, food manufacturers, and logistics companies. The adaptability of best sorting machines to different material types and sorting criteria ensures long-term utility regardless of changing business requirements. Companies investing in best sorting machines experience rapid payback periods, typically recovering initial investment within eighteen to thirty-six months through efficiency gains and waste reduction.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

best sorting machines

Advanced Optical Recognition Technology

Advanced Optical Recognition Technology

The sophisticated optical recognition systems integrated into best sorting machines represent a significant technological breakthrough. These best sorting machines employ multiple camera angles and spectroscopic analysis to identify materials with extraordinary precision. The optical recognition technology within best sorting machines operates at speeds exceeding ten thousand items per hour, processing materials faster than any human operator could achieve. This advanced system distinguishes subtle variations in material properties, ensuring accurate classification even when items appear similar to the naked eye. Best sorting machines featuring this technology reduce contamination rates dramatically, protecting downstream processes from incompatible materials. The continuous learning algorithms embedded in best sorting machines improve accuracy over time as the system encounters diverse material variations. For recycling facilities and manufacturing operations, this technological advantage translates directly into higher-quality end products and reduced processing costs.
Intelligent Automation and AI Integration

Intelligent Automation and AI Integration

Best sorting machines powered by artificial intelligence represent the next generation of industrial automation. These best sorting machines continuously learn from sorting decisions, adapting their algorithms to recognize new material types and characteristics automatically. The AI integration in best sorting machines enables predictive maintenance alerts, notifying operators before component failures occur. Best sorting machines can simultaneously manage multiple sorting criteria, making complex decisions in milliseconds that would require extensive manual evaluation. The machine learning capabilities of best sorting machines improve consistency and reliability while reducing the need for frequent recalibration. Companies deploying best sorting machines benefit from systems that become increasingly intelligent with each operational hour. This artificial intelligence advancement makes best sorting machines future-proof investments that adapt to evolving industrial requirements without requiring complete system replacement.
Customizable Sorting Parameters and Scalability

Customizable Sorting Parameters and Scalability

Best sorting machines offer unprecedented flexibility through customizable sorting parameters that adapt to specific business requirements. These best sorting machines allow operators to adjust sensitivity levels, sorting criteria, and output destinations through intuitive control interfaces. The modular architecture of best sorting machines enables seamless capacity expansion, allowing businesses to add additional sorting lanes as production demands increase. Best sorting machines integrate effortlessly with existing conveyor systems and production equipment, minimizing installation complexity. Configuration adjustments for best sorting machines require minimal downtime, enabling rapid transitions between different material types and sorting specifications. The scalability features of best sorting machines ensure that initial investments remain relevant as businesses grow. Companies utilizing best sorting machines enjoy exceptional flexibility that accommodates seasonal demand fluctuations and product diversification strategies without requiring supplementary capital equipment purchases.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy