Cashew Color Sorter Machine | Advanced Quality Control

All Categories

cashew color sorter machine

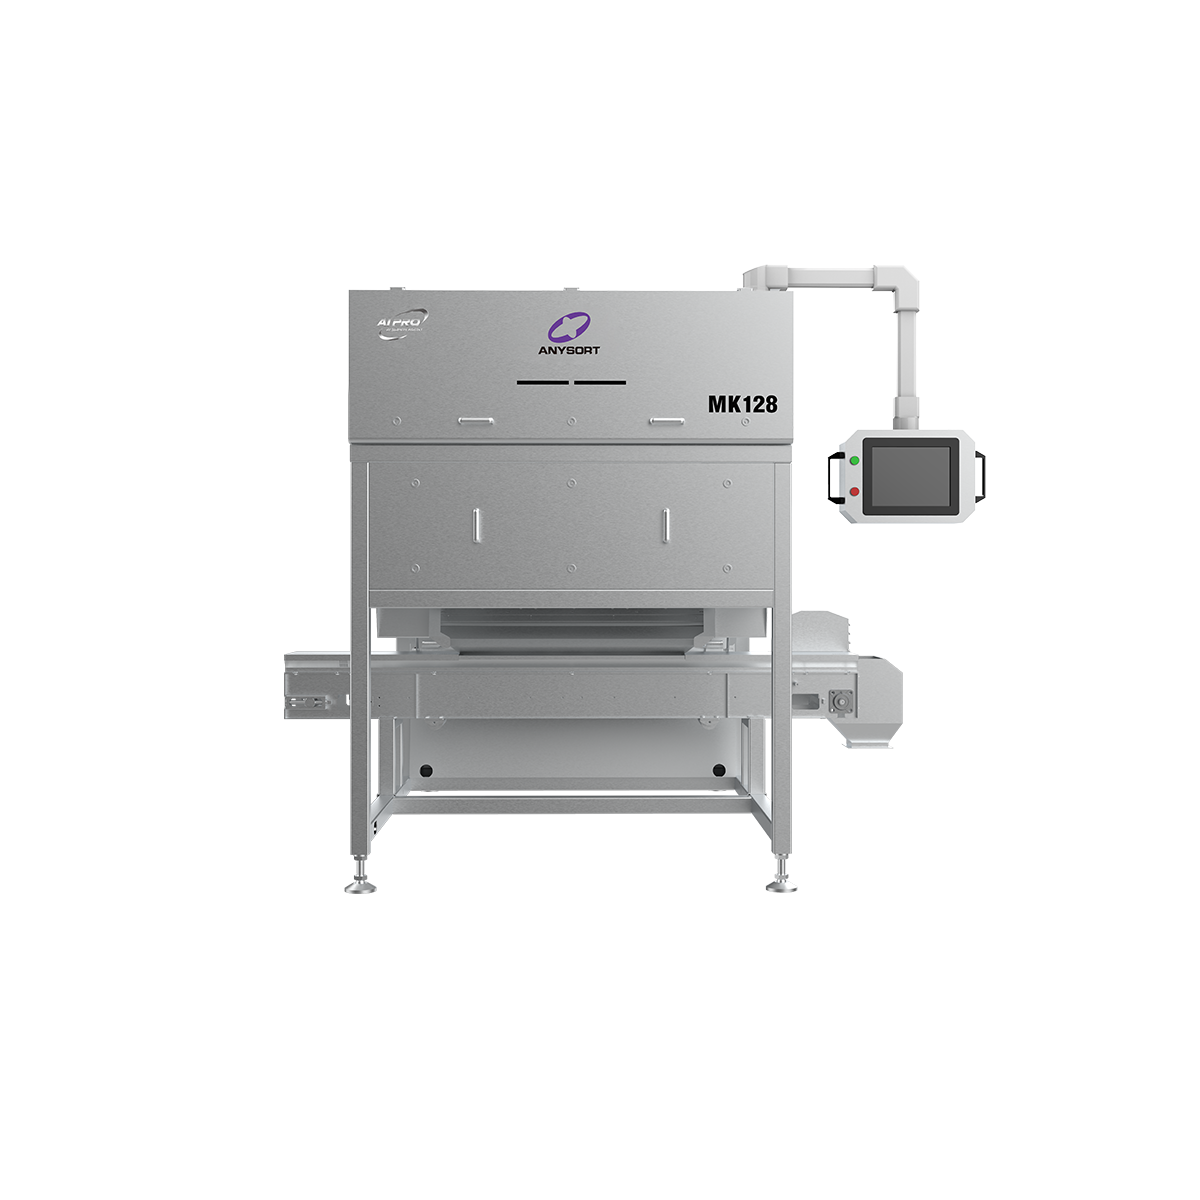
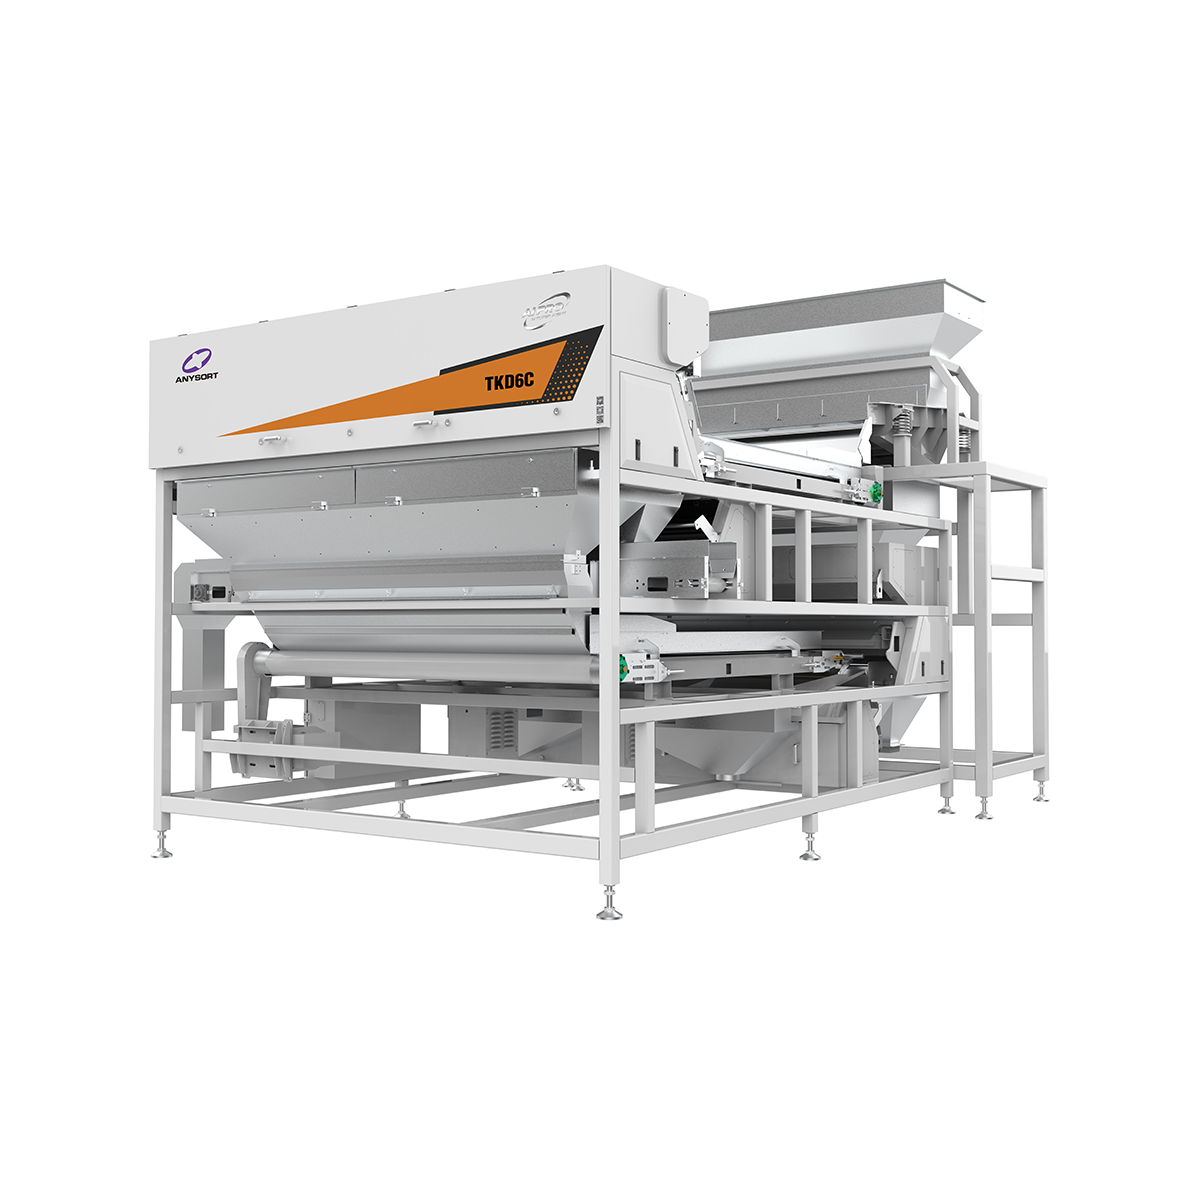
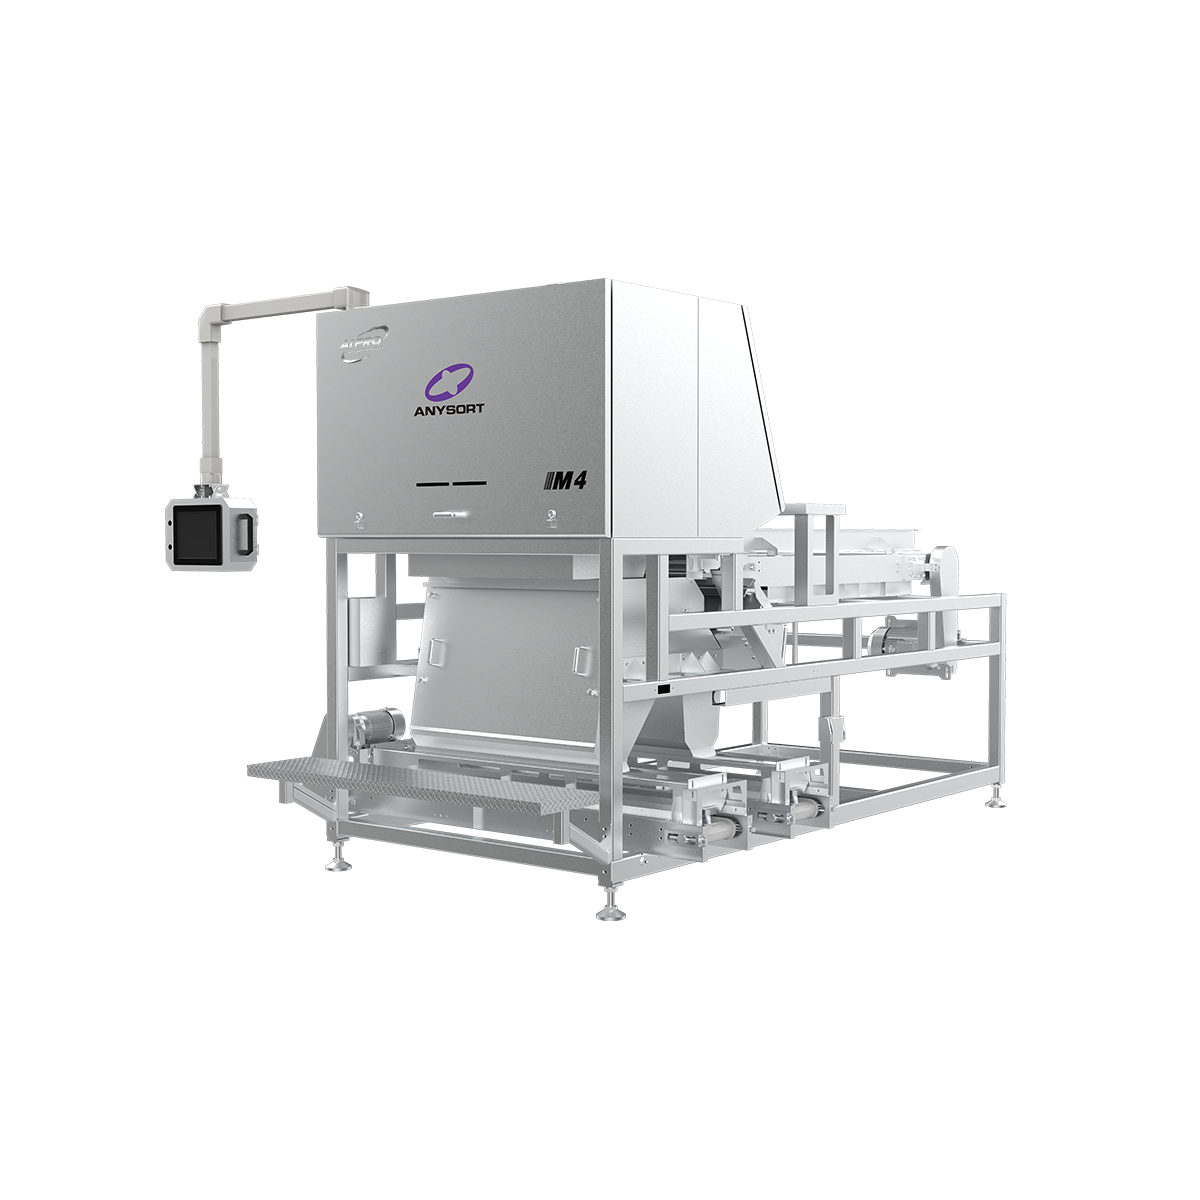
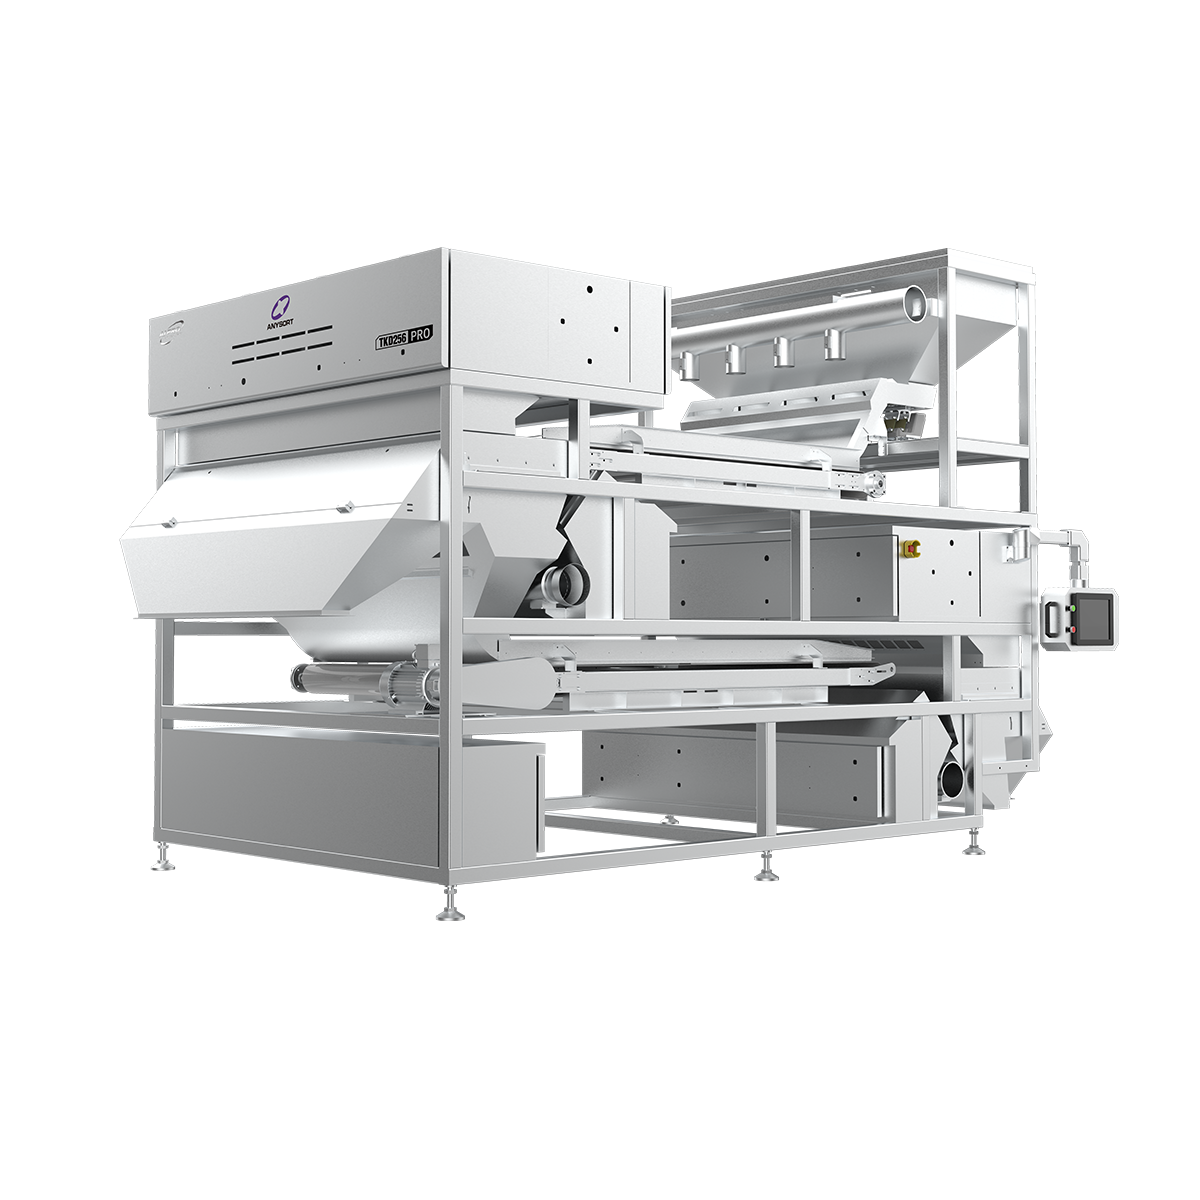
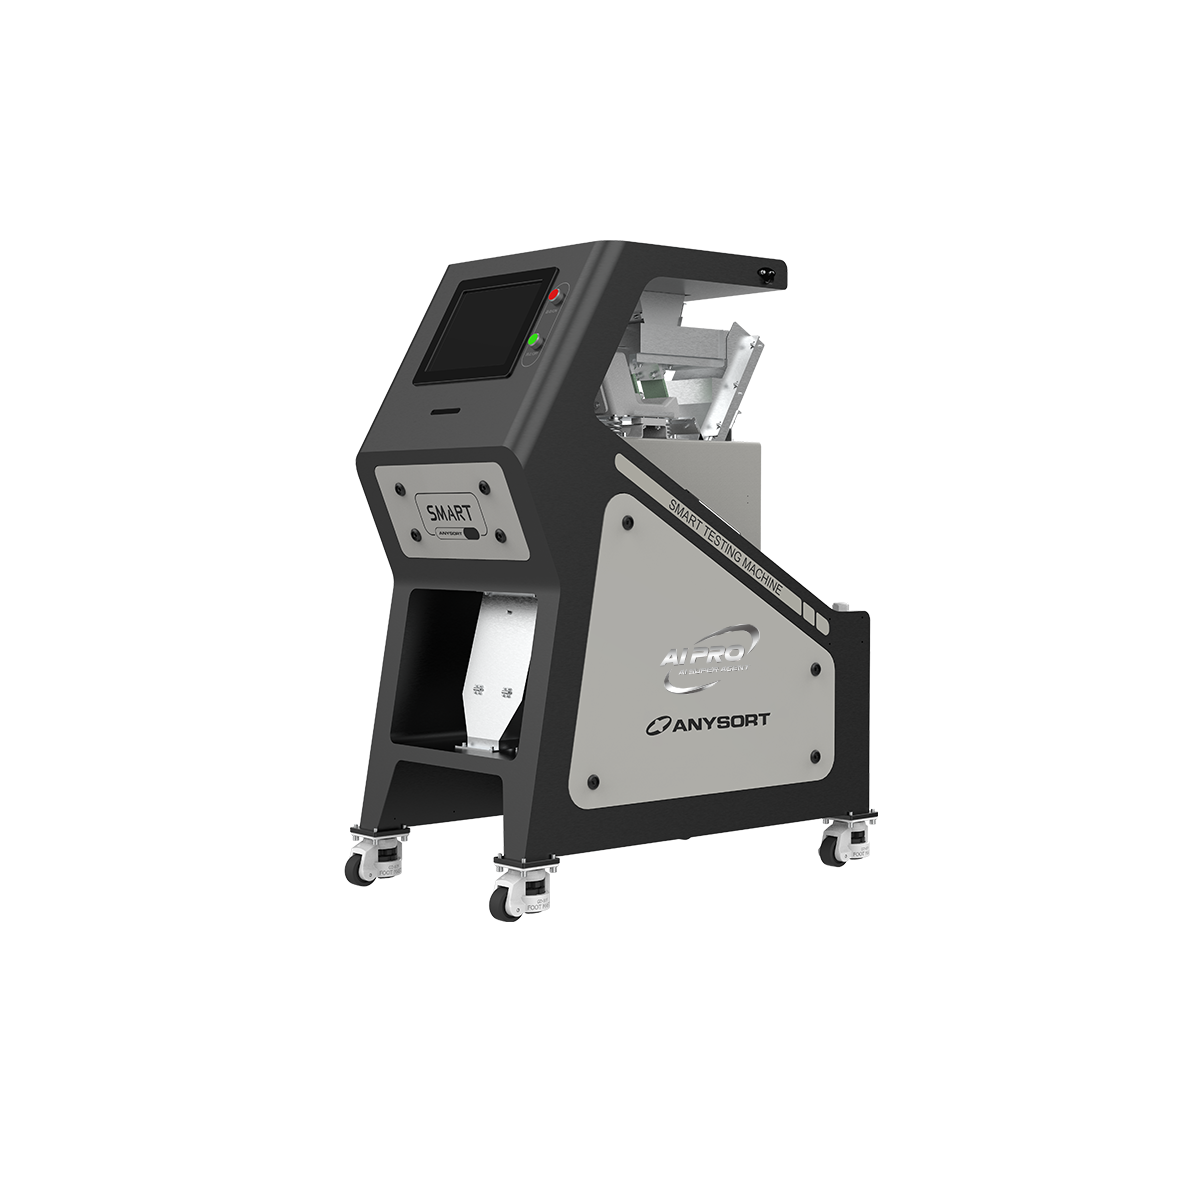
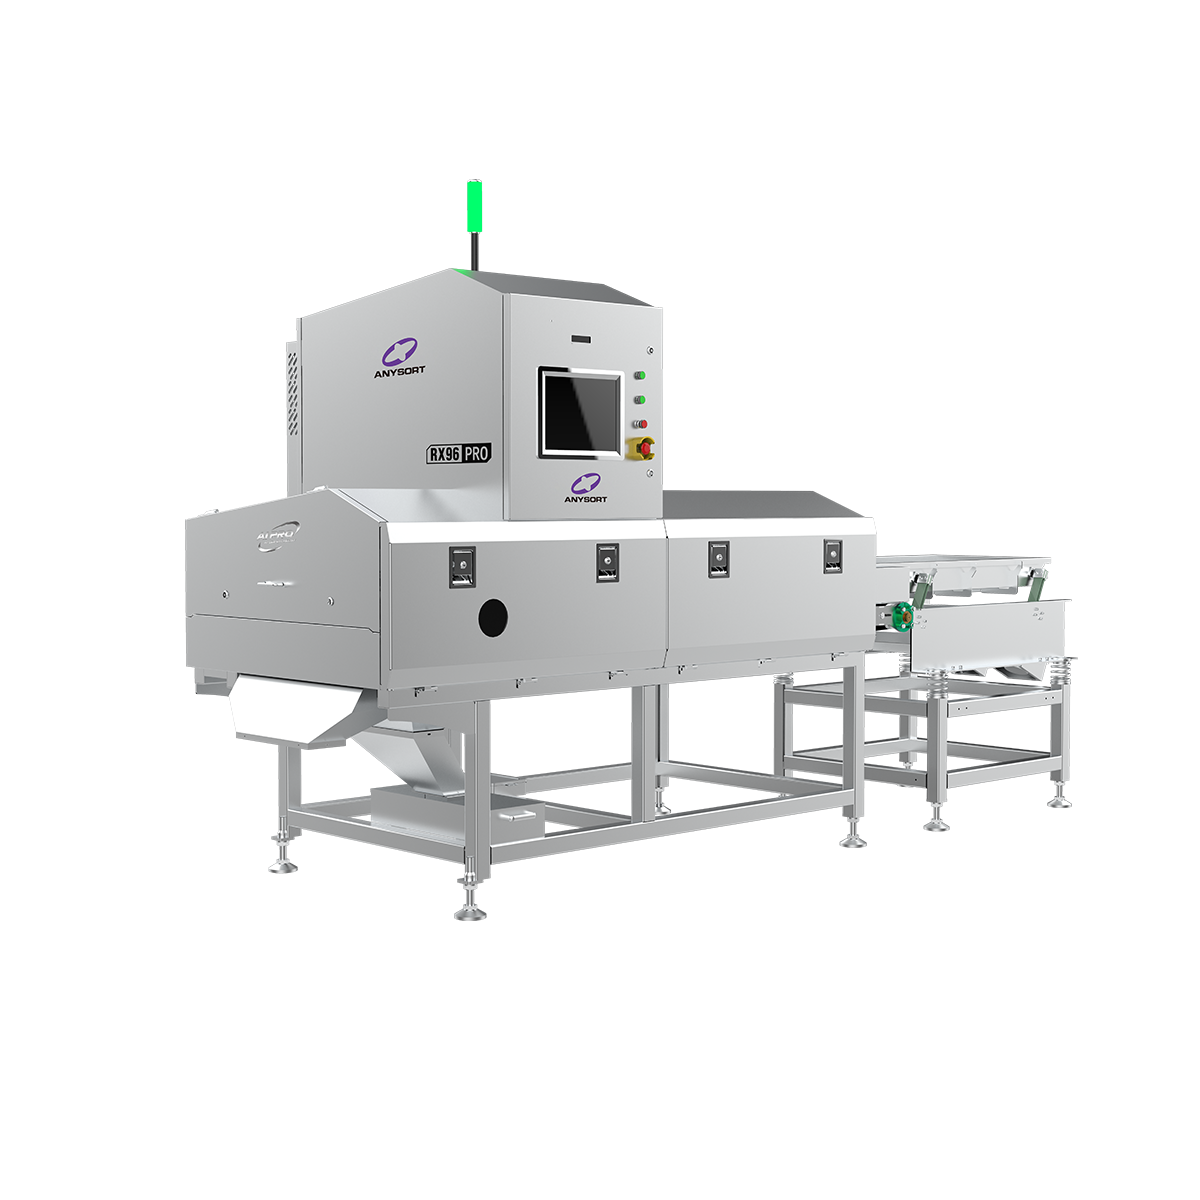
A cashew color sorter machine represents advanced technology designed to automatically classify cashews based on color, size, and quality specifications. This innovative equipment serves as an essential tool in cashew processing facilities, significantly streamlining production workflows. The cashew color sorter machine utilizes optical sensing technology combined with artificial intelligence algorithms to detect subtle color variations that human eyes might miss. Modern cashew color sorter machines feature high-speed cameras and LED lighting systems that capture detailed images of each cashew nut as it passes through the sorting mechanism. The sorting process identifies defects, discoloration, and quality inconsistencies with remarkable precision. A cashew color sorter machine can process thousands of nuts per hour, dramatically increasing operational efficiency compared to manual sorting methods. The machine automatically ejects substandard cashews while directing premium-quality nuts to designated collection areas. This automated cashew color sorter machine reduces labor costs and eliminates human error from the sorting process. Processors can establish customizable sorting parameters to meet specific market demands and quality standards. The technology integrates seamlessly into existing production lines, requiring minimal modifications to current infrastructure. Advanced cashew color sorter machines feature user-friendly interfaces, enabling operators to monitor performance in real-time and adjust settings as needed. These machines contribute substantially to product consistency, helping processors maintain competitive advantages in global markets where quality expectations continue rising.

New Products

The cashew color sorter machine delivers transformative operational benefits that directly impact your bottom line. By automating the sorting process, this equipment eliminates tedious manual labor while achieving superior accuracy in quality detection. Your facility experiences dramatic productivity increases, with each cashew color sorter machine processing significantly higher volumes than traditional hand-sorting methods. Cost savings accumulate quickly as labor expenses decrease and waste reduction improves substantially. The cashew color sorter machine ensures consistent output quality, enabling you to meet strict customer specifications and industry standards reliably. Processors gain competitive advantages by delivering uniform-quality cashews that command premium market prices. The machine reduces physical strain on workers by eliminating repetitive sorting tasks, creating safer working environments. Your facility can implement flexible sorting criteria tailored to different customer requirements without expensive equipment modifications. A cashew color sorter machine requires minimal maintenance while providing years of dependable operation, delivering exceptional return on investment. Real-time monitoring capabilities allow operators to track performance metrics and identify potential issues before they impact production. The technology handles diverse cashew varieties and sizes effectively, maximizing operational flexibility. By consistently removing defective nuts, your cashew color sorter machine protects brand reputation and customer satisfaction. Environmental benefits emerge as resource utilization improves and waste decreases substantially. Integration with existing production infrastructure proves straightforward, minimizing implementation disruption. Modern cashew color sorter machines adapt to evolving market demands, supporting business growth without requiring complete equipment replacement. The equipment provides transparent sorting documentation, enabling you to verify compliance with quality assurance protocols and regulatory requirements effortlessly.

Tips And Tricks

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew color sorter machine

Advanced Optical Recognition Technology

Advanced Optical Recognition Technology

The cashew color sorter machine employs sophisticated optical sensors and high-definition imaging systems that detect minute color variations invisible to human inspectors. This technology utilizes multiple LED light wavelengths to illuminate cashews from different angles, capturing comprehensive data about surface characteristics. Artificial intelligence algorithms analyze these detailed images instantly, identifying defects, discoloration, mold spots, and quality inconsistencies with remarkable precision. The cashew color sorter machine processes each nut in milliseconds, achieving sorting accuracy exceeding 99 percent. This advanced recognition capability ensures that only premium-quality cashews reach your customers, protecting your brand reputation while maintaining customer loyalty. The machine continuously learns and adapts to variations in nut appearance, improving performance over time. Your facility benefits from consistent quality standards that manual sorting cannot achieve.
Exceptional Processing Speed and Capacity

Exceptional Processing Speed and Capacity

Modern cashew color sorter machines process thousands of nuts per hour, dramatically exceeding manual sorting capabilities. The high-speed conveyor systems work seamlessly with optical detection mechanisms, creating efficient production flows that maximize facility throughput. Your cashew color sorter machine adapts to different processing speeds based on specific requirements, accommodating varying production demands throughout operational schedules. The equipment handles diverse cashew sizes and varieties without requiring time-consuming adjustments or calibrations. This exceptional capacity directly translates to increased profitability, as your facility produces more sellable product within standard operating hours. A cashew color sorter machine eliminates production bottlenecks that traditionally occurred during quality control stages. Processors gain flexibility to meet urgent customer orders while maintaining consistent quality standards. The machine's reliability ensures minimal downtime, keeping your production line moving continuously.
Cost-Effective Long-Term Investment

Cost-Effective Long-Term Investment

Installing a cashew color sorter machine represents a strategic investment that delivers substantial returns through multiple financial benefits. Labor cost reductions become immediately apparent as the equipment performs work previously requiring numerous employees. The cashew color sorter machine significantly decreases product waste by accurately identifying and removing defective nuts before they reach market. Your facility reduces material losses, directly improving profit margins and overall operational efficiency. Energy consumption remains remarkably low compared to alternative automated systems, minimizing utility costs. Maintenance requirements are straightforward and inexpensive, with components designed for extended lifespan and durability. A cashew color sorter machine requires minimal calibration adjustments, reducing technical support expenses significantly. The equipment's reliability creates predictable operational costs, simplifying budget planning and financial projections. Rapid payback periods make this investment accessible to facilities of various sizes and economic circumstances.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy