Cashew Nut Sorting Machine | Precision Grading

All Categories

cashew nut sorting machine

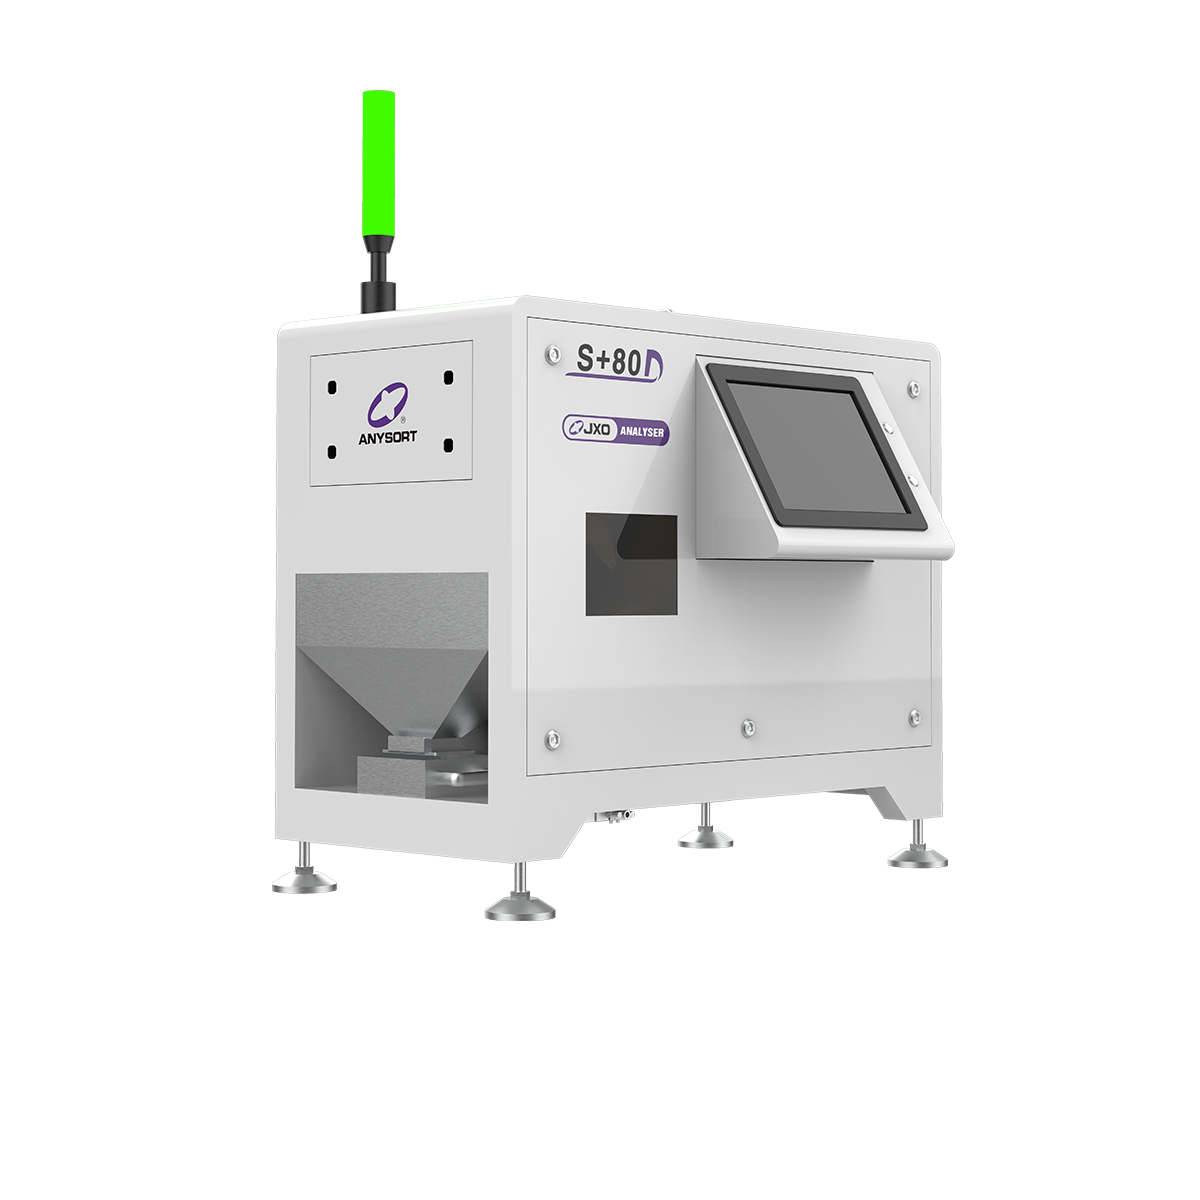
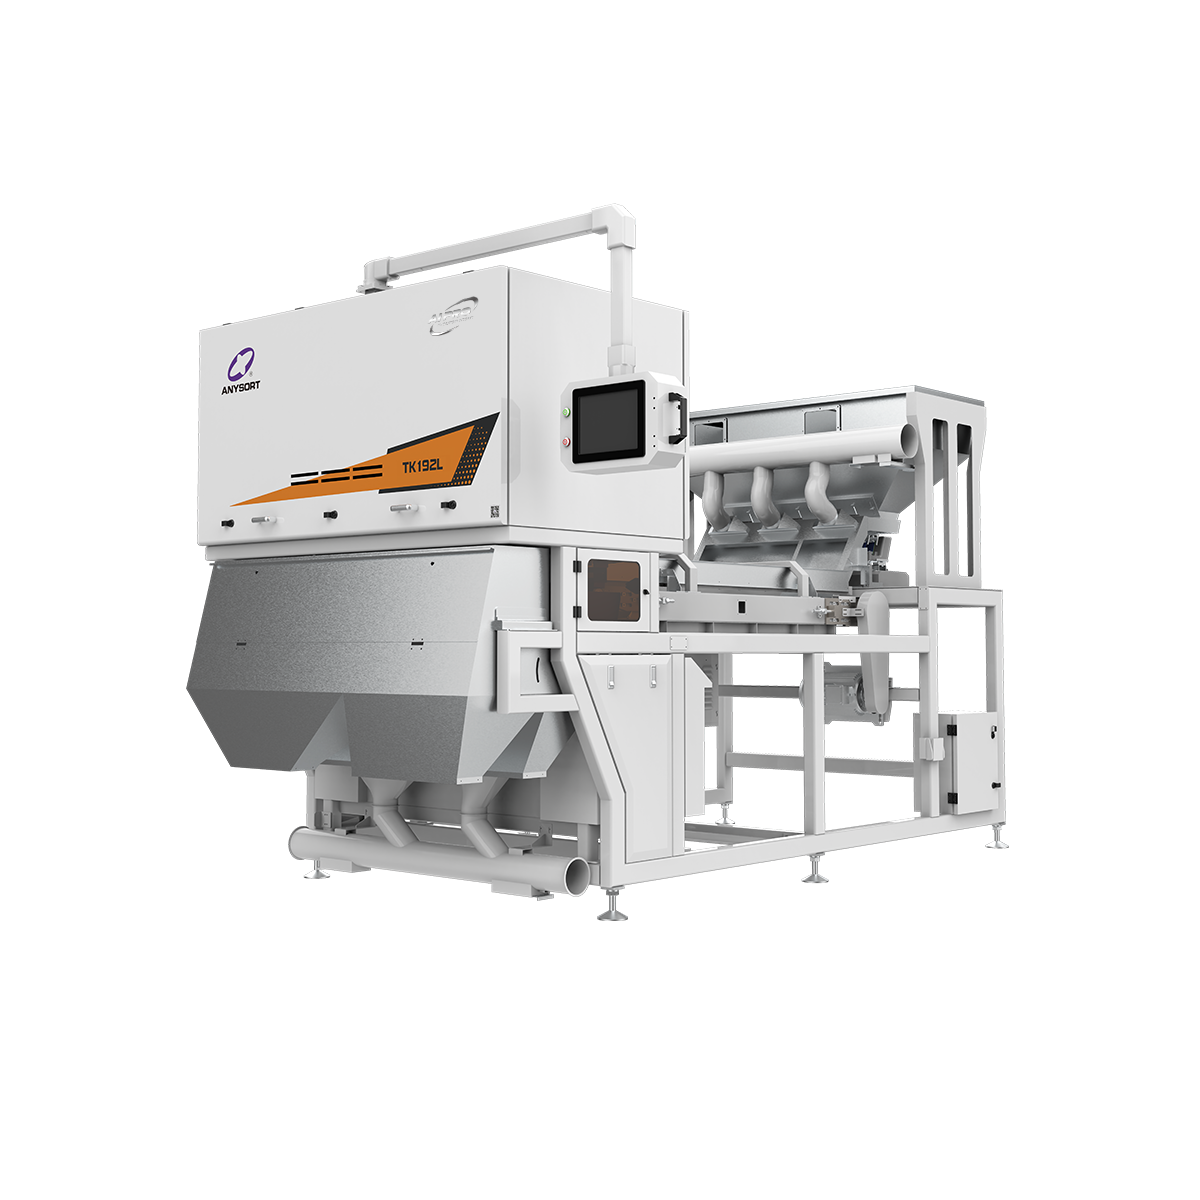
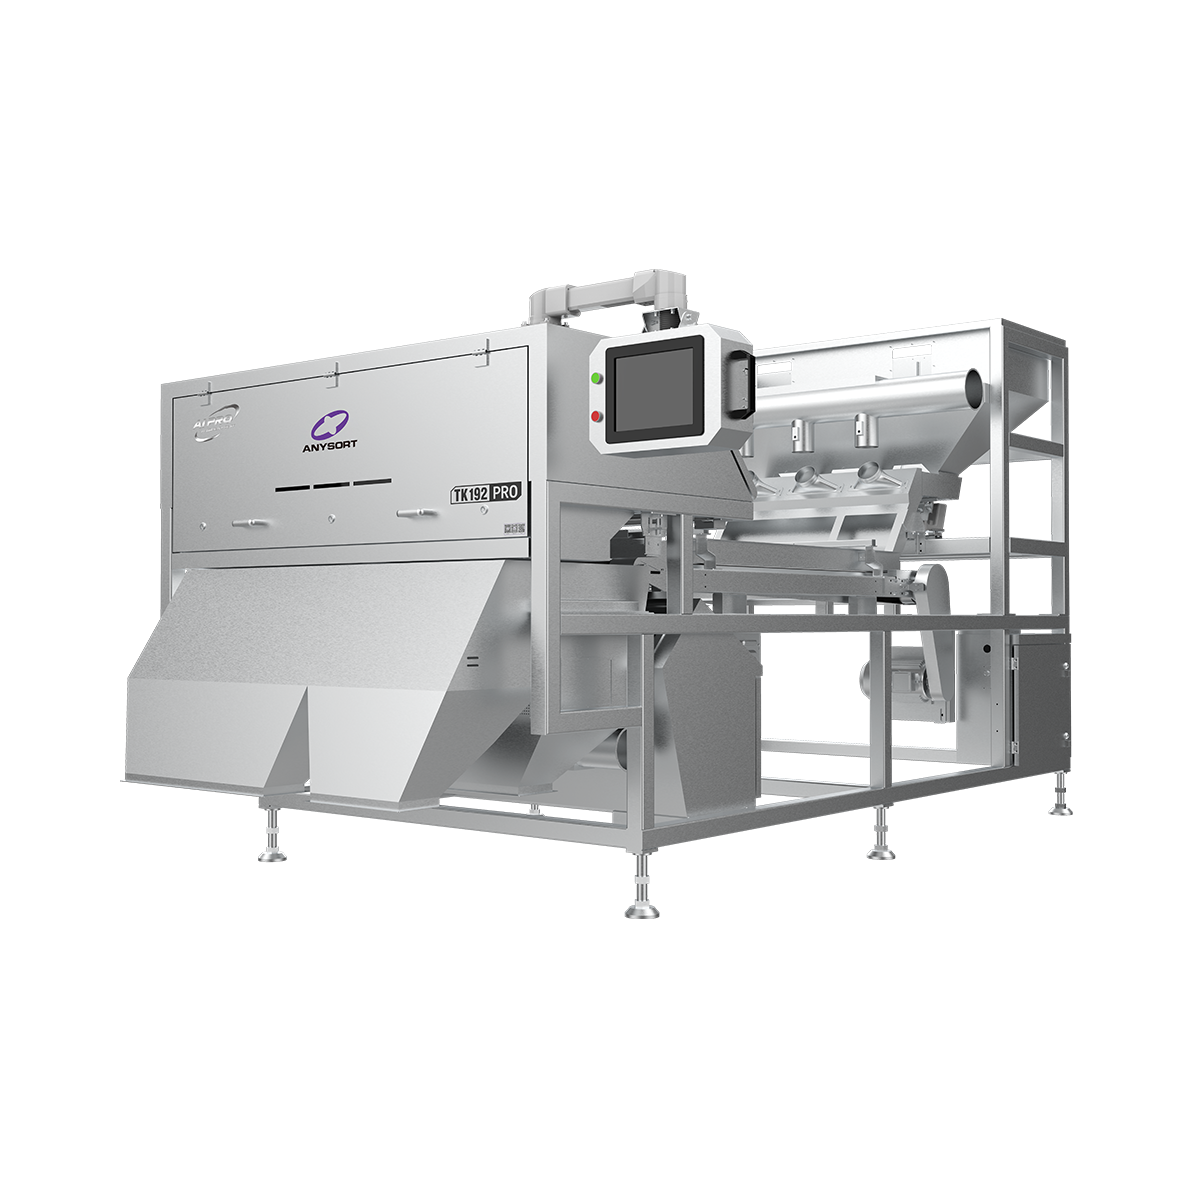
A cashew nut sorting machine is an advanced piece of processing equipment designed to automatically separate and grade cashew nuts based on size, weight, and quality. This innovative cashew nut sorting machine utilizes cutting-edge technology to streamline production workflows in food processing facilities worldwide. The primary function of a cashew nut sorting machine is to categorize nuts into uniform grades, ensuring consistent product quality for commercial distribution. Modern cashew nut sorting machines incorporate optical sensors, mechanical sieves, and pneumatic systems that work seamlessly together. These technological features enable rapid processing of large volumes while maintaining precision and accuracy. The cashew nut sorting machine operates with minimal human intervention, significantly reducing labor costs and production time. Sophisticated algorithms within the system detect defects, discoloration, and irregular shapes, automatically removing substandard nuts from the production line. The machine handles both whole and broken cashew kernels with equal efficiency. Applications of the cashew nut sorting machine span across nut processing plants, food manufacturing facilities, and export operations. Agricultural businesses benefit tremendously from implementing this technology, as it improves yield quality and market competitiveness. The cashew nut sorting machine has become indispensable in meeting international food safety standards and consumer expectations for premium-grade nuts. Whether processing small batches or industrial-scale quantities, this equipment delivers consistent results and enhanced productivity throughout operations.

Popular Products

Choosing a cashew nut sorting machine delivers substantial operational and financial benefits to food processing businesses. The most compelling advantage lies in dramatically increased efficiency and throughput capacity compared to manual sorting methods. By automating the sorting process, your facility processes significantly more nuts daily while maintaining superior quality standards. Cost reduction represents another major advantage of investing in a cashew nut sorting machine. Labor expenses decrease substantially since the machine performs work that previously required multiple workers, allowing reallocation of your workforce to other valuable tasks. Quality consistency improves remarkably when using a cashew nut sorting machine, as automated systems eliminate human error and subjectivity in grading decisions. Every batch maintains identical standards, enhancing customer satisfaction and brand reputation. The cashew nut sorting machine reduces product waste by accurately identifying and separating damaged or inferior nuts, maximizing your profit margins. Food safety compliance becomes straightforward with this technology, as the machine ensures all processed nuts meet regulatory requirements and industry standards. Operational reliability is exceptional since modern machines feature durable construction and require minimal maintenance interventions. The cashew nut sorting machine adapts flexibly to various nut sizes and processing requirements without extensive recalibration. Businesses gain competitive advantages in global markets by producing consistently graded, premium-quality cashews. Return on investment typically materializes within months through increased productivity and reduced operational costs. The cashew nut sorting machine essentially transforms your processing capacity while simultaneously improving product quality, making it an essential acquisition for serious industry participants seeking sustainable growth.

Latest News

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew nut sorting machine

Advanced Optical Technology for Precision Grading

Advanced Optical Technology for Precision Grading

The cashew nut sorting machine incorporates state-of-the-art optical sensing technology that identifies and categorizes nuts with extraordinary precision. High-resolution cameras and sophisticated image processing algorithms scan each individual nut, detecting minute variations in size, color, shape, and surface quality that human inspectors might overlook. This optical system ensures every cashew nut sorting machine delivers consistent grading results, eliminating subjective judgment from quality control processes. The technology processes nuts at remarkable speeds, examining hundreds of units per minute without sacrificing accuracy. Real-time data collection from the optical sensors enables continuous process monitoring and quality assurance. The advanced optical components within the cashew nut sorting machine maintain calibration automatically, adjusting for minor variations throughout production runs. Businesses benefit from detailed analytics that track quality metrics, identify trends, and support data-driven decision-making. This technological sophistication makes the cashew nut sorting machine superior to traditional mechanical methods for achieving premium-grade outputs.
Significant Cost Reduction and Labor Savings

Significant Cost Reduction and Labor Savings

Operating a cashew nut sorting machine substantially reduces operational expenses while maximizing profitability across your entire processing operation. The automated system replaces multiple manual laborers, generating immediate savings in wages, benefits, and training costs associated with employment. Energy consumption remains remarkably efficient compared to alternative sorting methods, contributing additional savings to your bottom line. The cashew nut sorting machine operates continuously without fatigue, maintaining consistent productivity throughout extended shifts without performance degradation. Reduced product waste directly increases revenue per processed batch, as fewer defective nuts exit your facility. The machine's durability means minimal maintenance requirements, lowering ongoing operational expenses significantly. Training new operators requires minimal time investment since the cashew nut sorting machine features intuitive controls and straightforward operation protocols. Investment in this technology quickly demonstrates positive financial returns through quantifiable productivity improvements and reduced labor allocations. Businesses consistently report recouping equipment investments within eighteen months through operational efficiencies and quality improvements generated by their cashew nut sorting machine.
Enhanced Quality Control and Market Competitiveness

Enhanced Quality Control and Market Competitiveness

The cashew nut sorting machine elevates your facility's quality standards to levels that manually-sorted products cannot consistently achieve. Precise grading ensures every cashew nut sorting machine output meets international quality benchmarks and consumer expectations for premium products. Customers receive uniformly sized, perfectly calibrated nuts that command higher market prices and strengthen brand loyalty. The technology eliminates contamination risks by identifying and removing damaged nuts before packaging. Regulatory compliance becomes automatic with a cashew nut sorting machine managing quality control, protecting your business from costly violations and recalls. Consistent quality enables expansion into premium market segments and luxury product categories. Export opportunities increase substantially when products meet global quality standards reliably. The cashew nut sorting machine creates competitive differentiation in crowded markets by producing superior products that justify premium pricing strategies. Businesses establish themselves as quality leaders when implementing this advanced technology, attracting discerning customers willing to pay more for excellence and consistency.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy