cashew color sorter machine
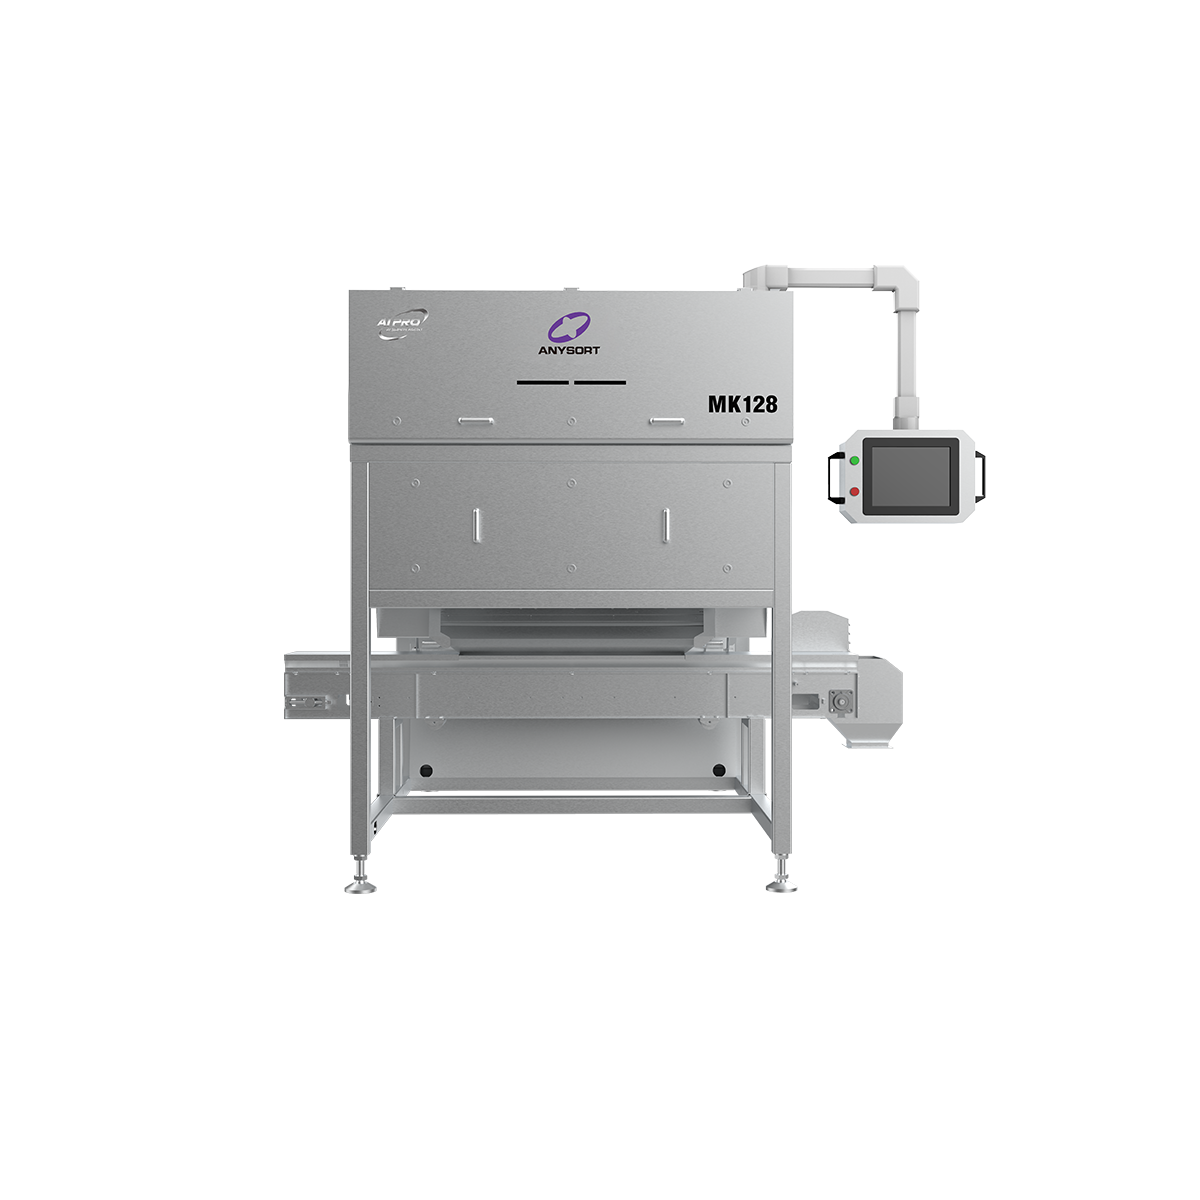
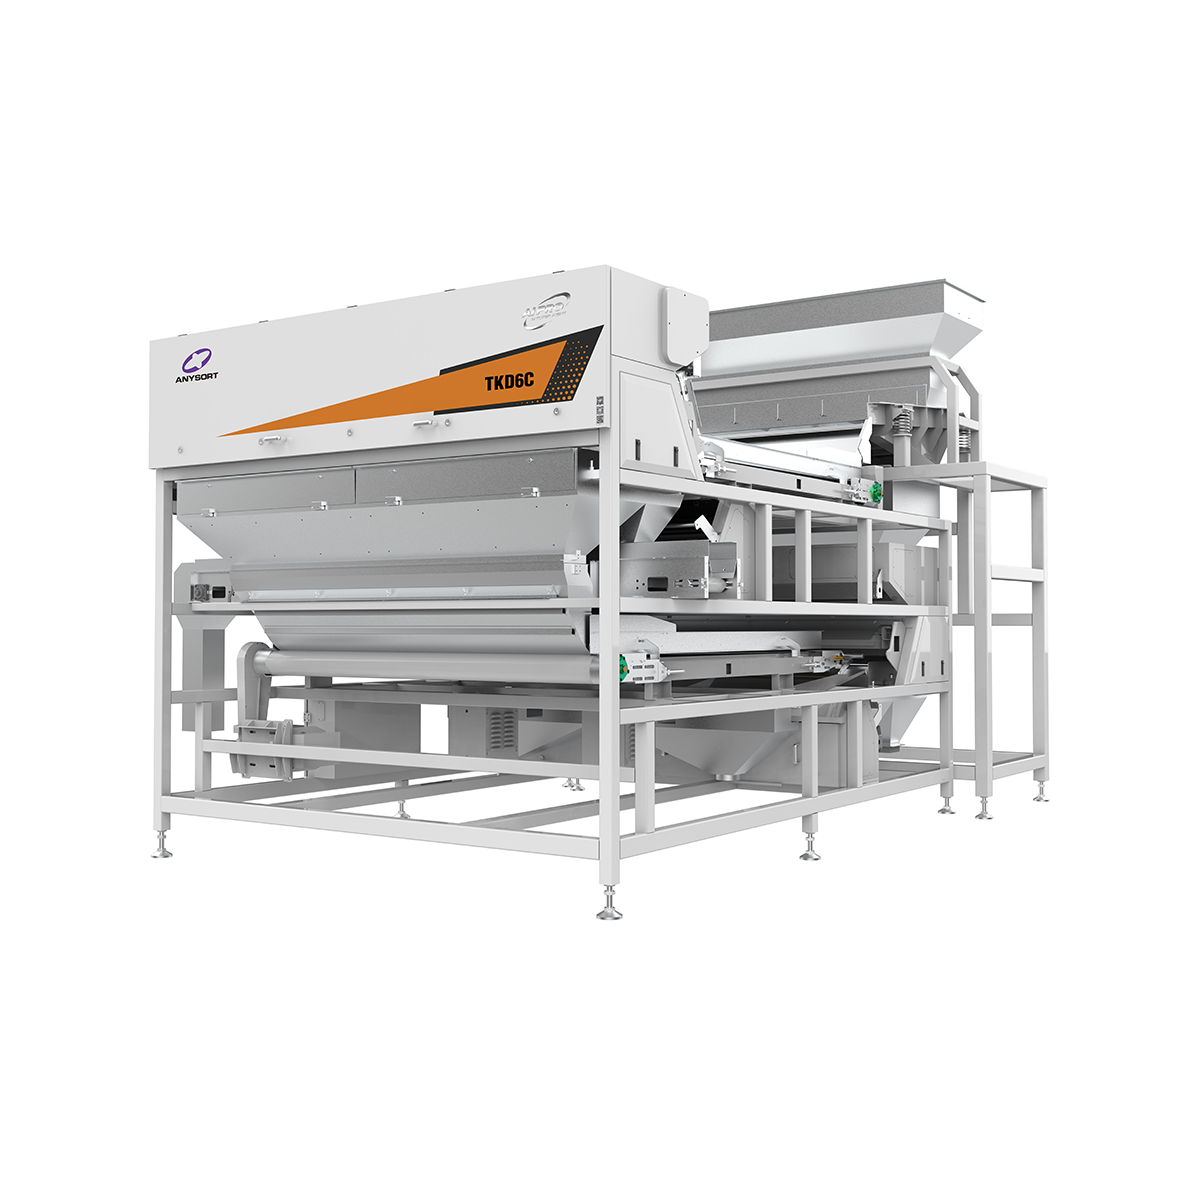
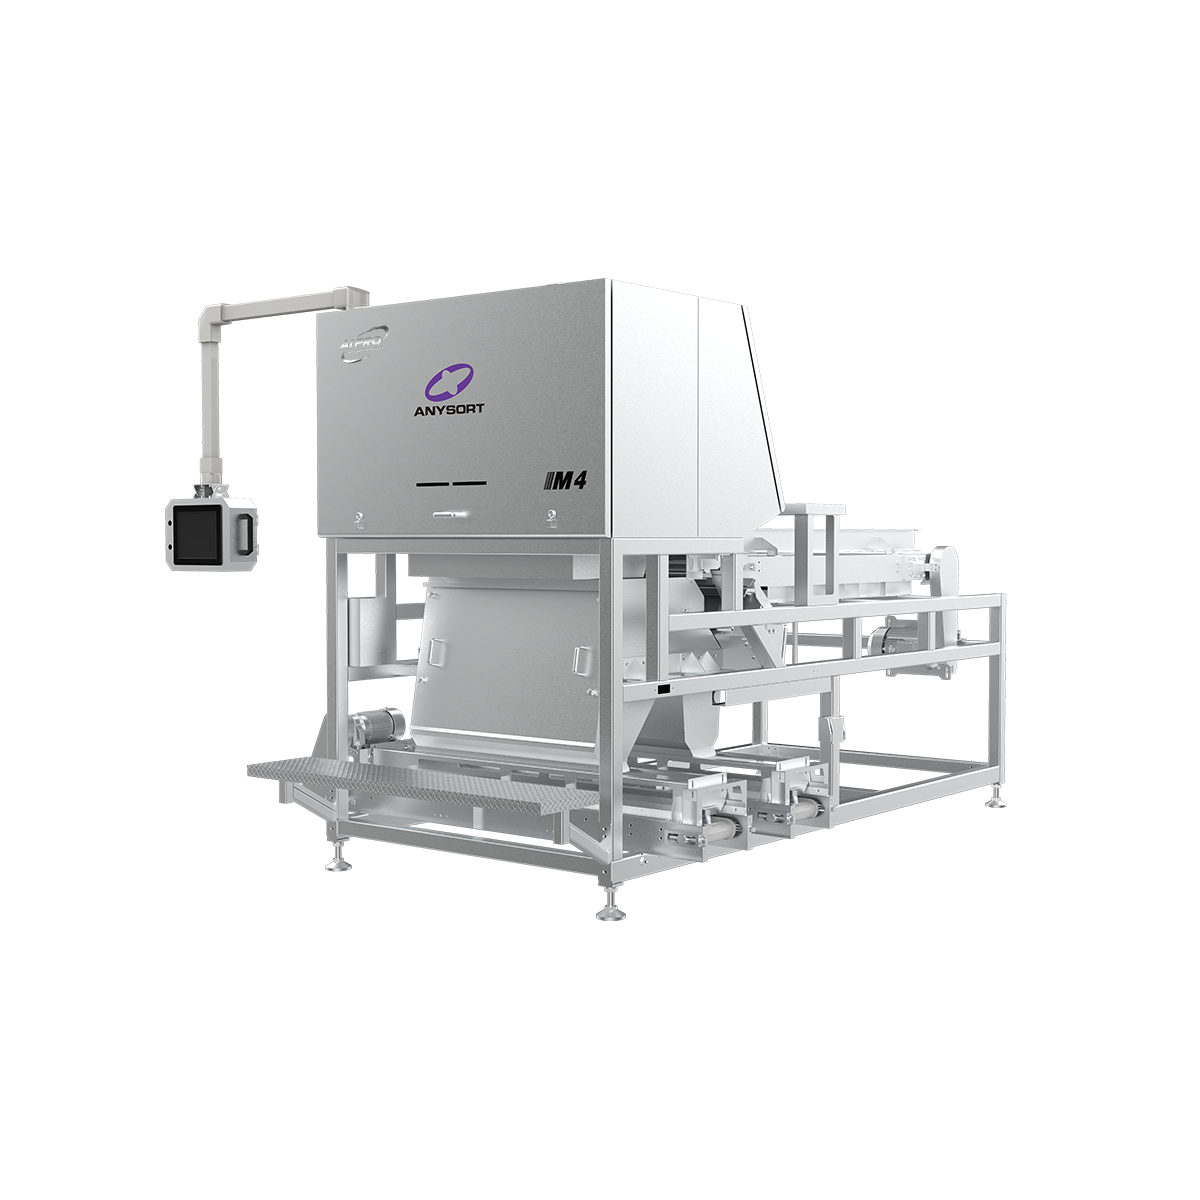
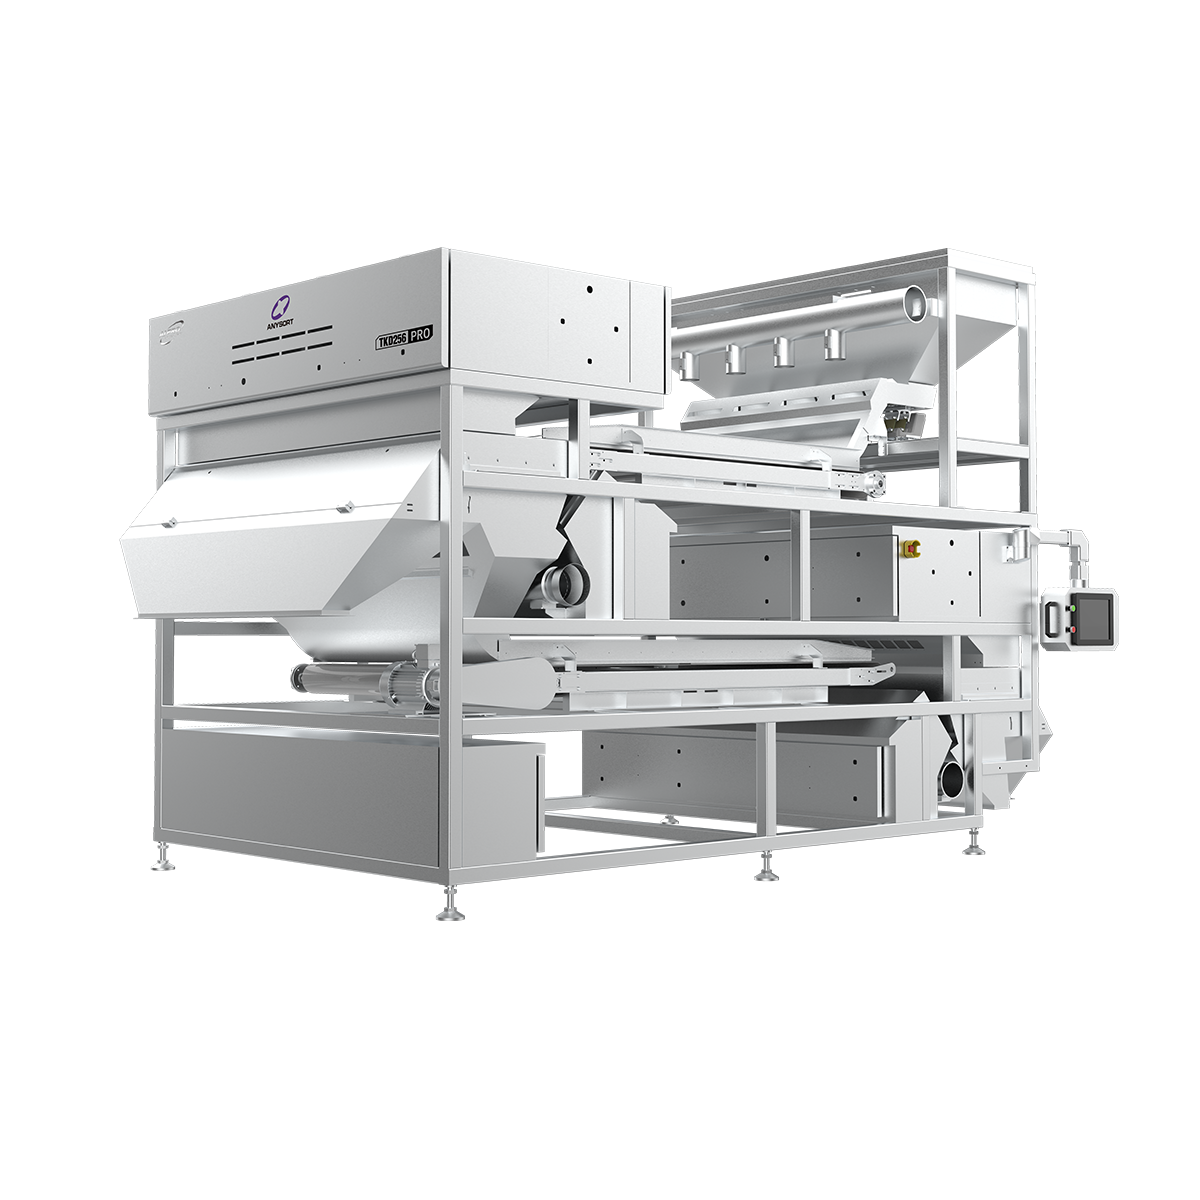
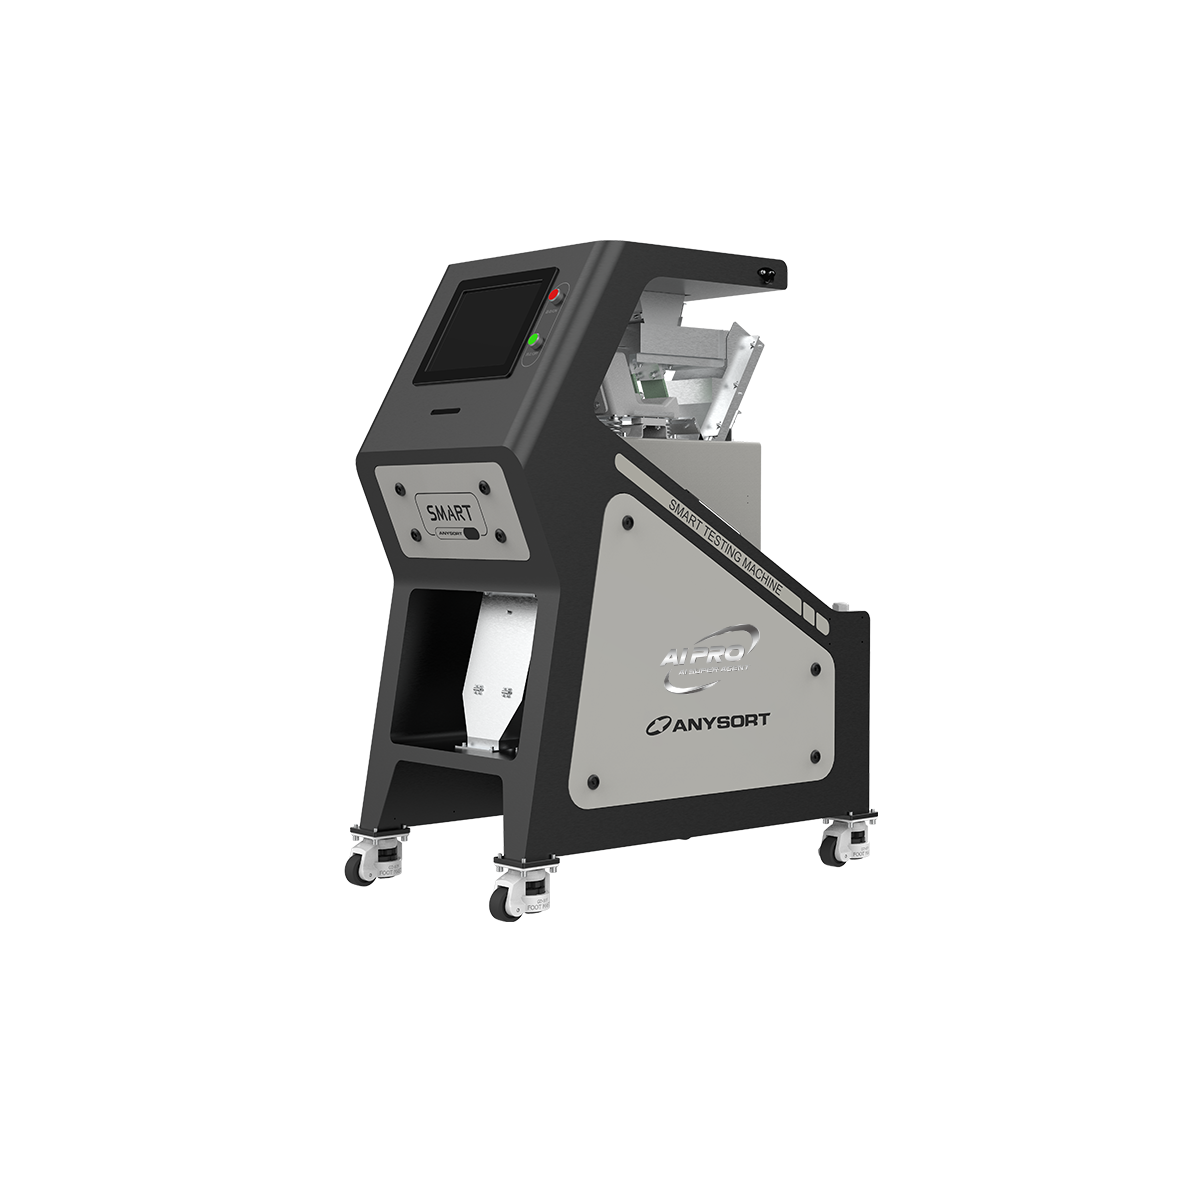
A cashew color sorter machine represents advanced technology designed to automatically classify cashews based on color, size, and quality specifications. This innovative equipment serves as an essential tool in cashew processing facilities, significantly streamlining production workflows. The cashew color sorter machine utilizes optical sensing technology combined with artificial intelligence algorithms to detect subtle color variations that human eyes might miss. Modern cashew color sorter machines feature high-speed cameras and LED lighting systems that capture detailed images of each cashew nut as it passes through the sorting mechanism. The sorting process identifies defects, discoloration, and quality inconsistencies with remarkable precision. A cashew color sorter machine can process thousands of nuts per hour, dramatically increasing operational efficiency compared to manual sorting methods. The machine automatically ejects substandard cashews while directing premium-quality nuts to designated collection areas. This automated cashew color sorter machine reduces labor costs and eliminates human error from the sorting process. Processors can establish customizable sorting parameters to meet specific market demands and quality standards. The technology integrates seamlessly into existing production lines, requiring minimal modifications to current infrastructure. Advanced cashew color sorter machines feature user-friendly interfaces, enabling operators to monitor performance in real-time and adjust settings as needed. These machines contribute substantially to product consistency, helping processors maintain competitive advantages in global markets where quality expectations continue rising.

 EN