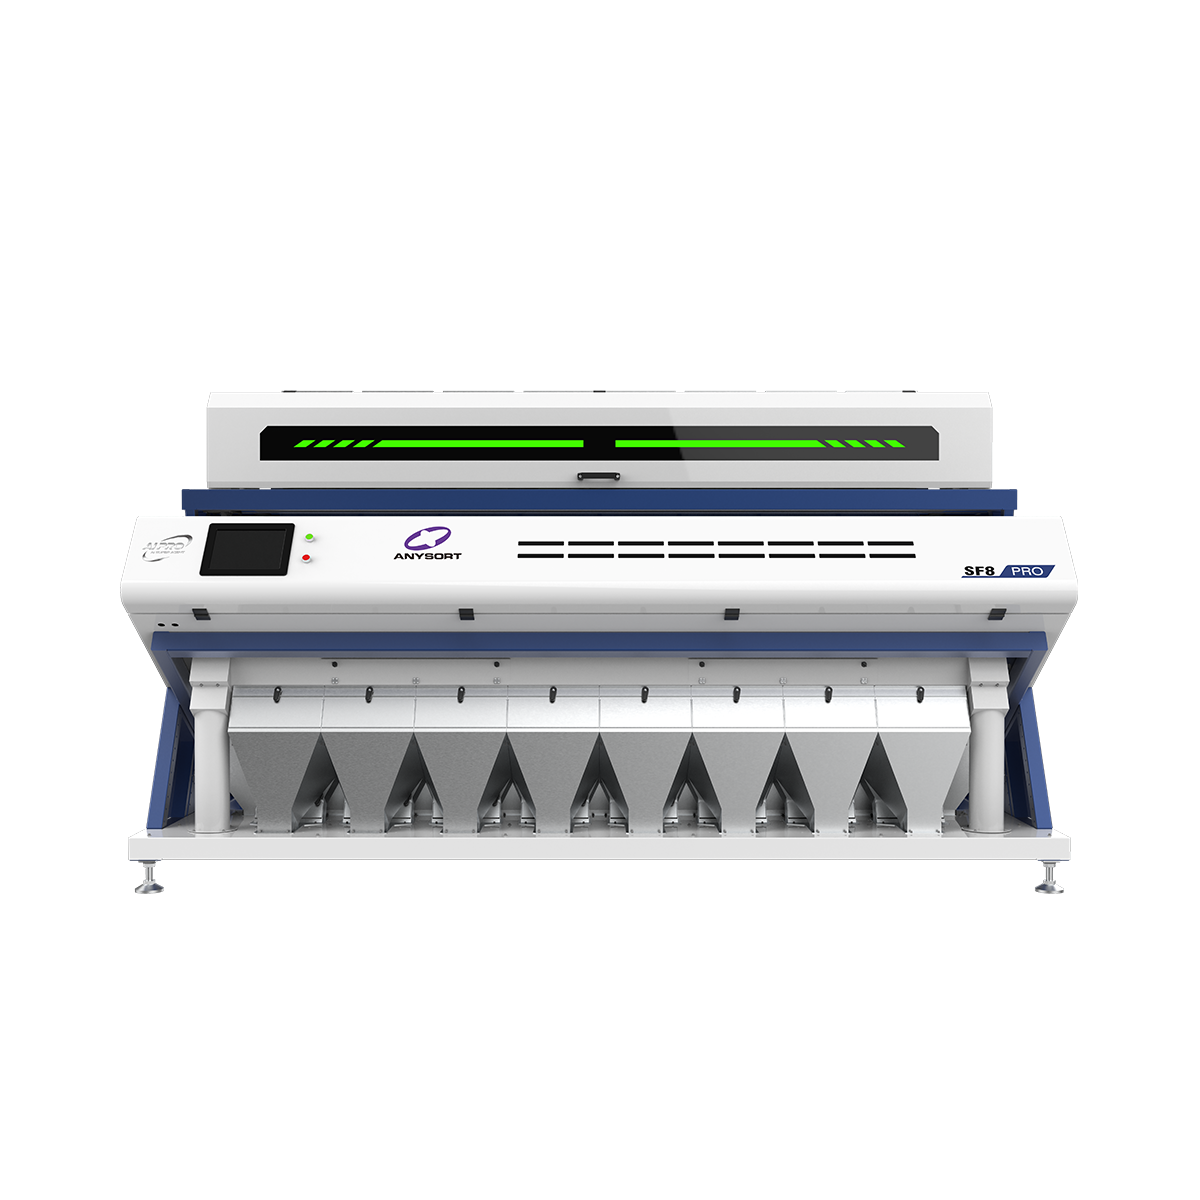
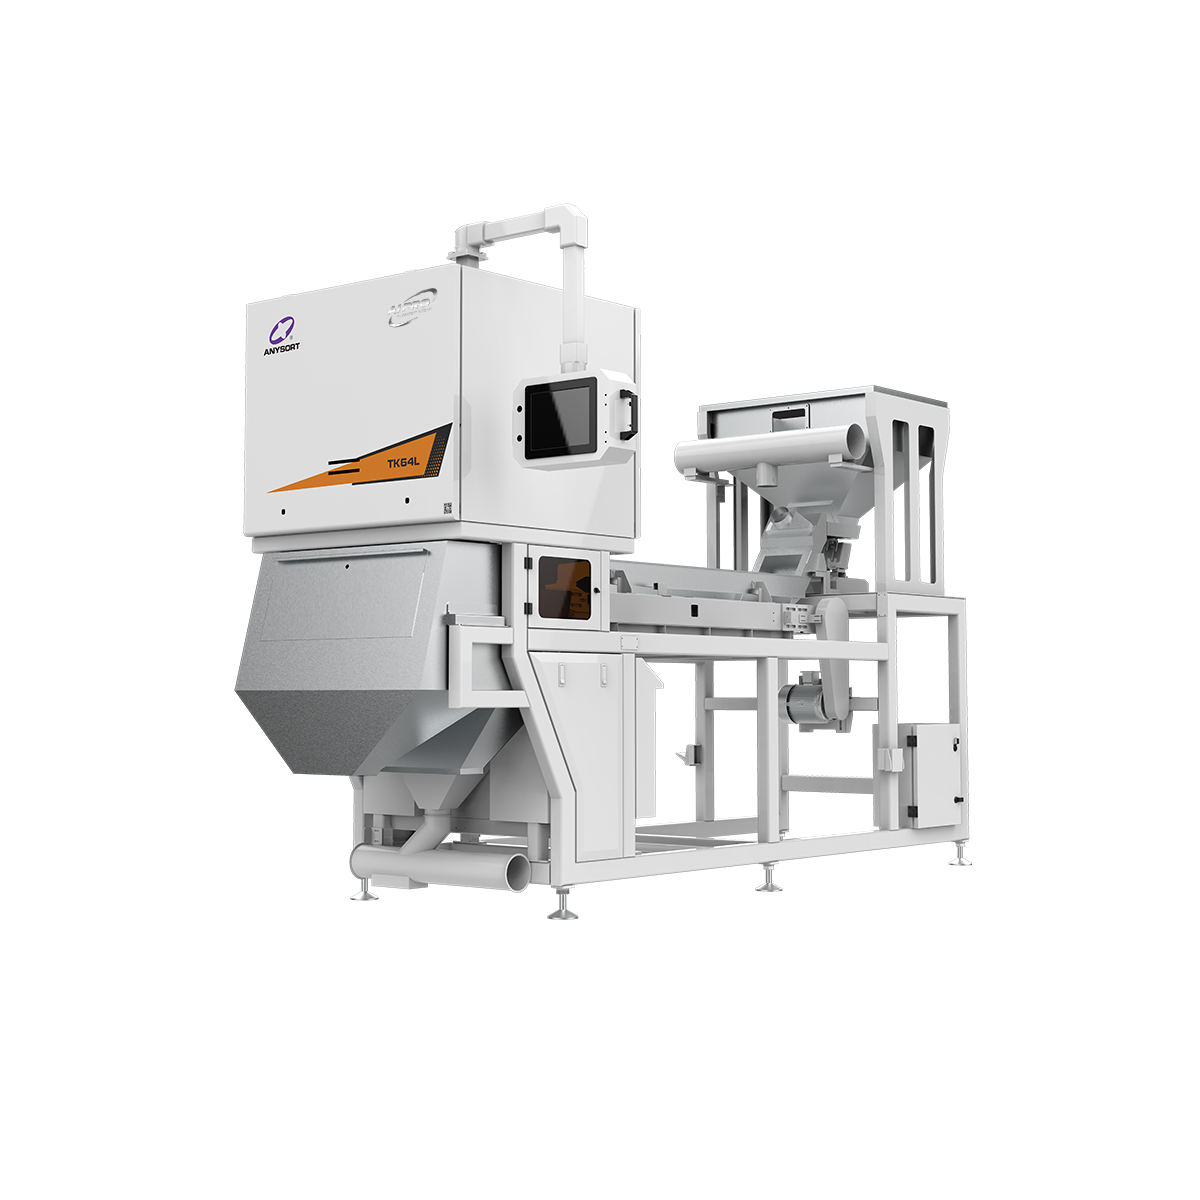
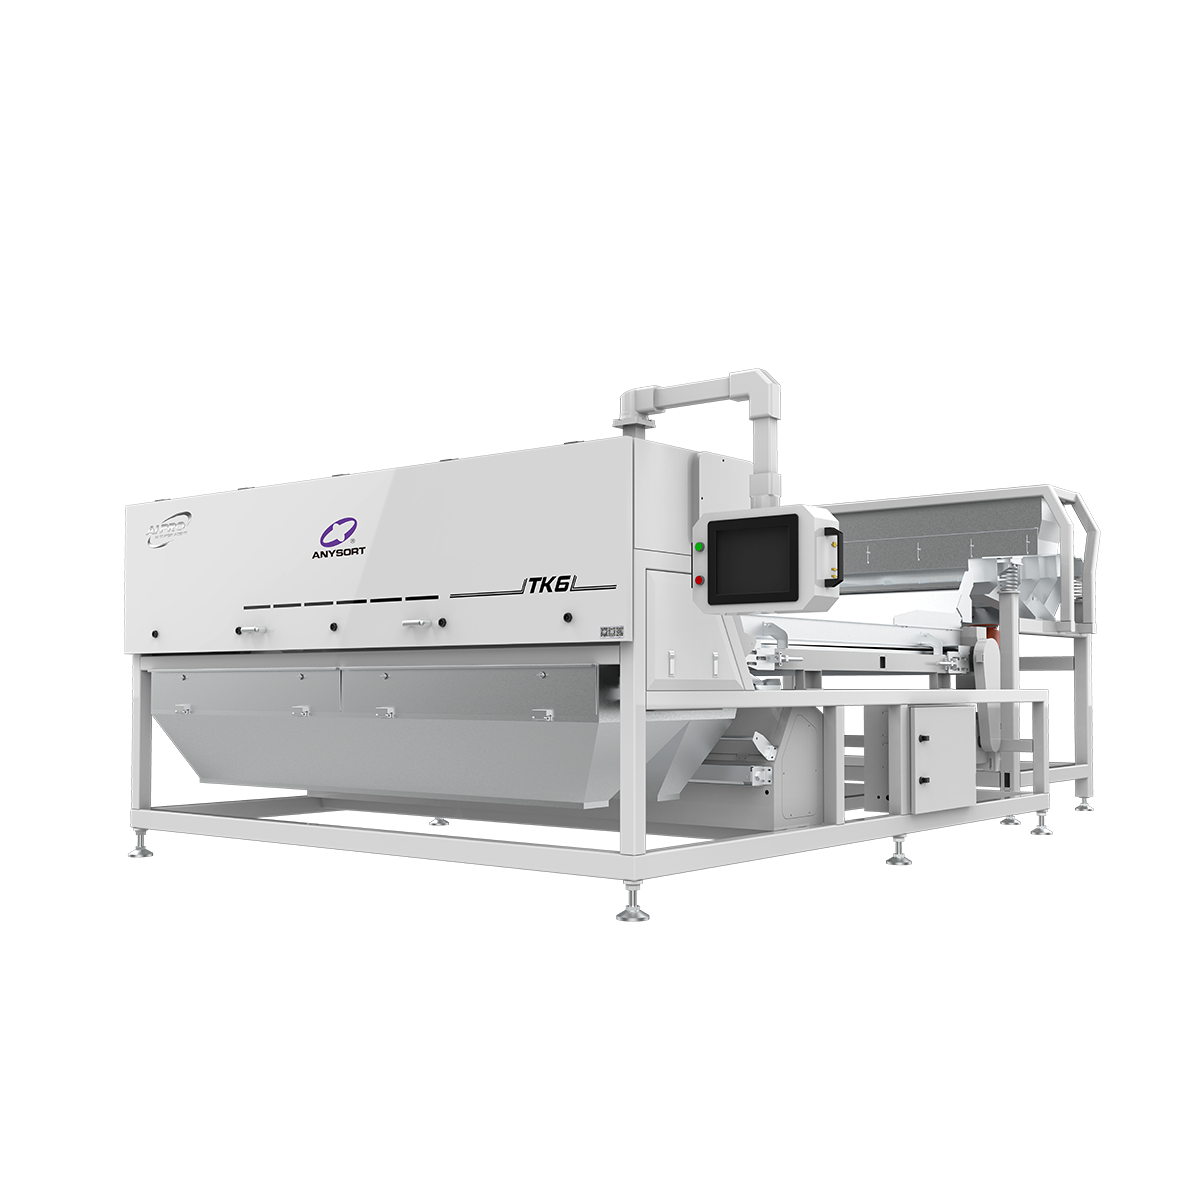
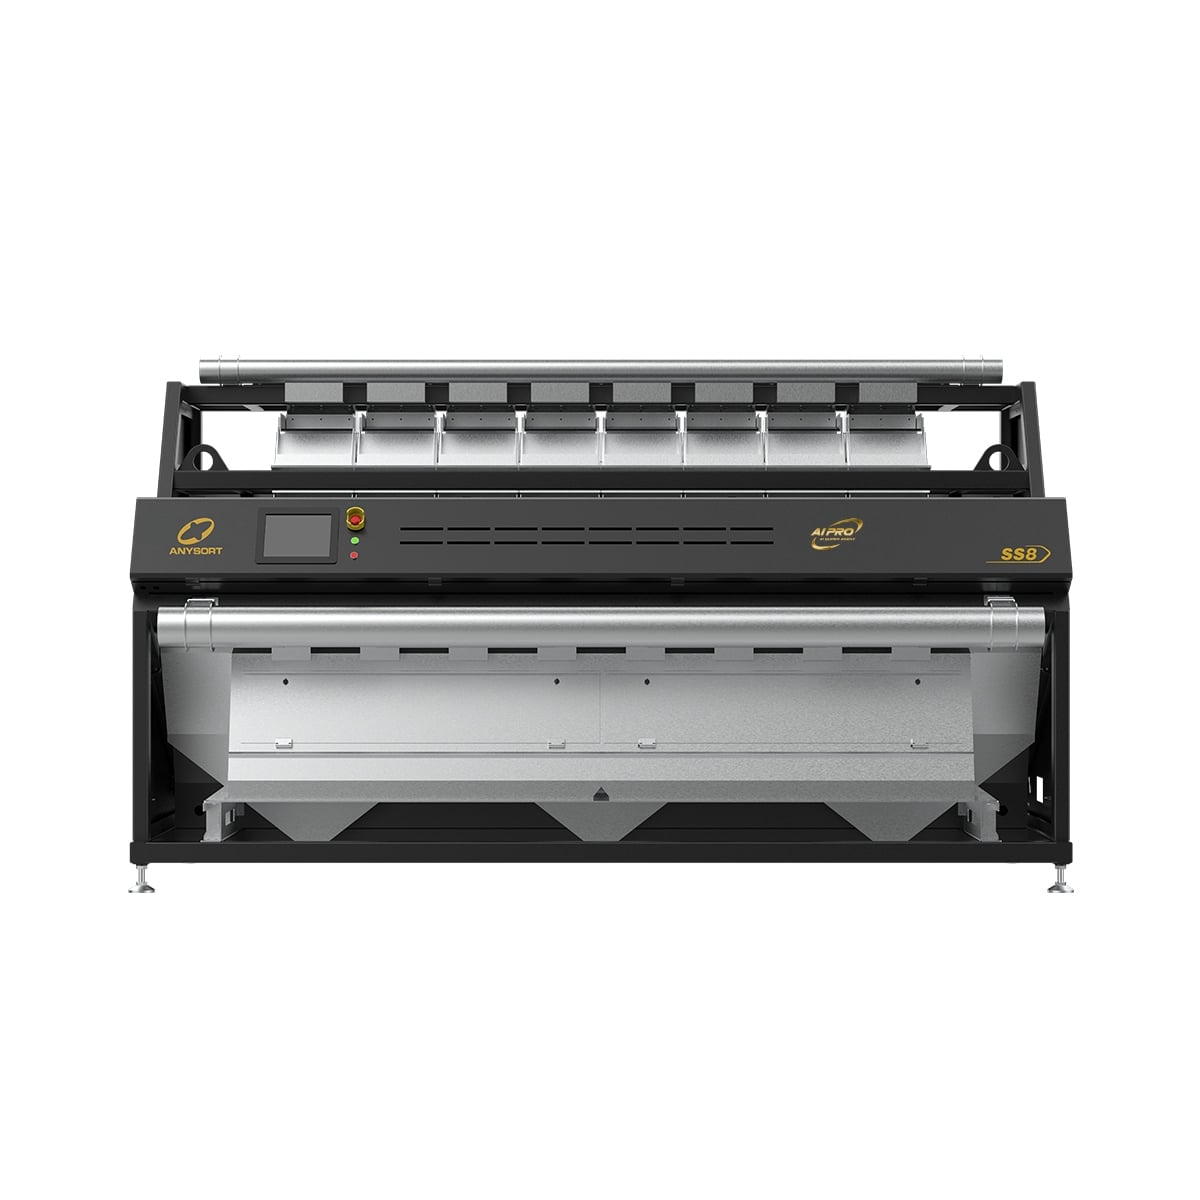
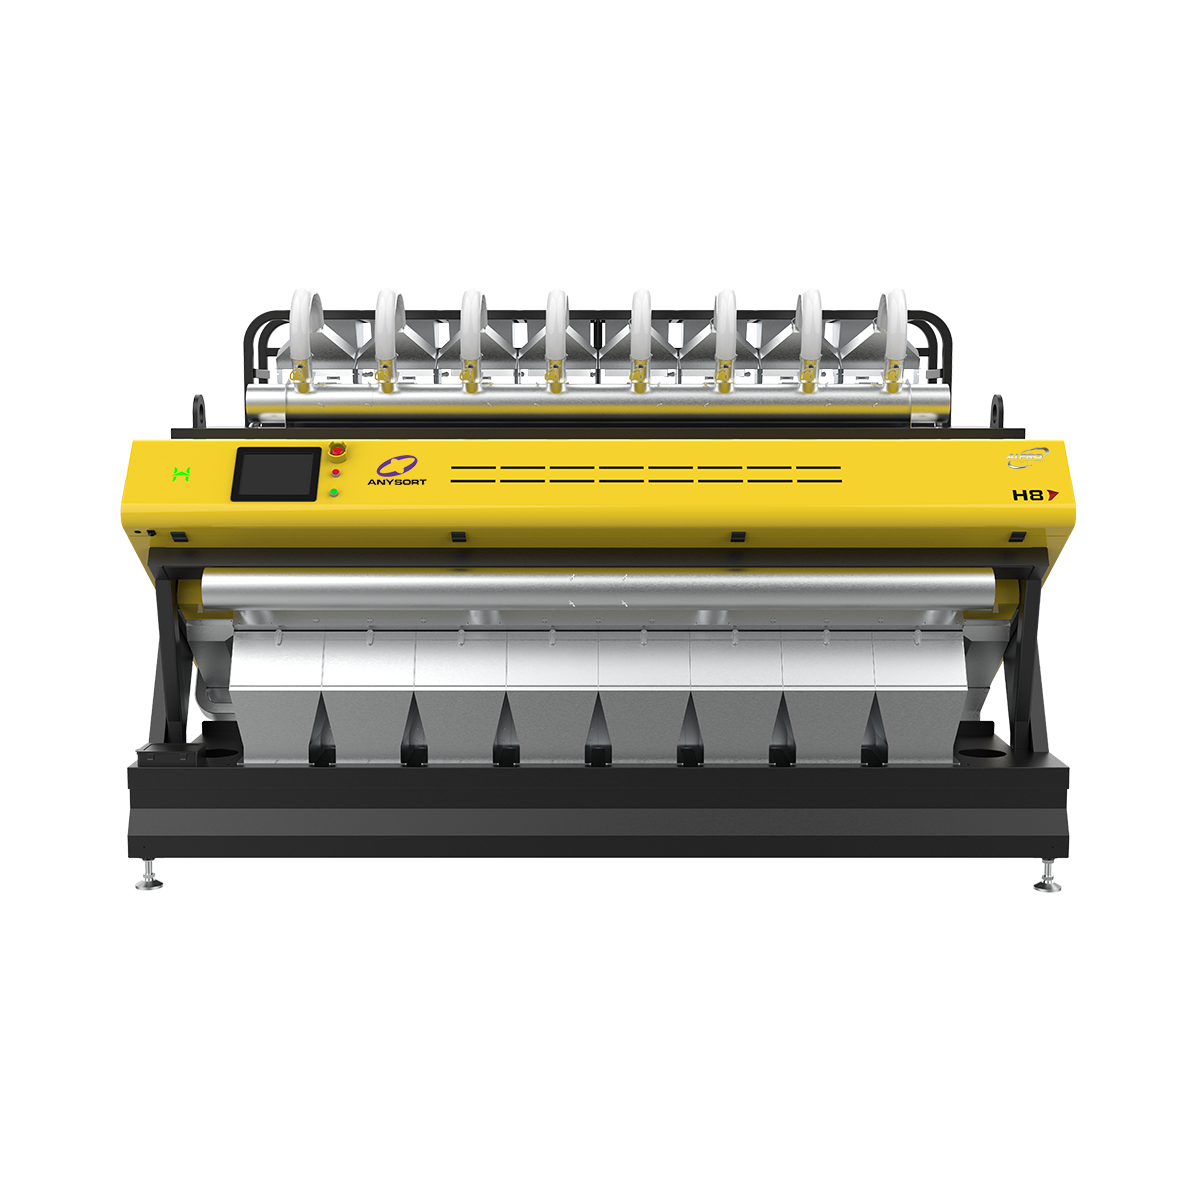
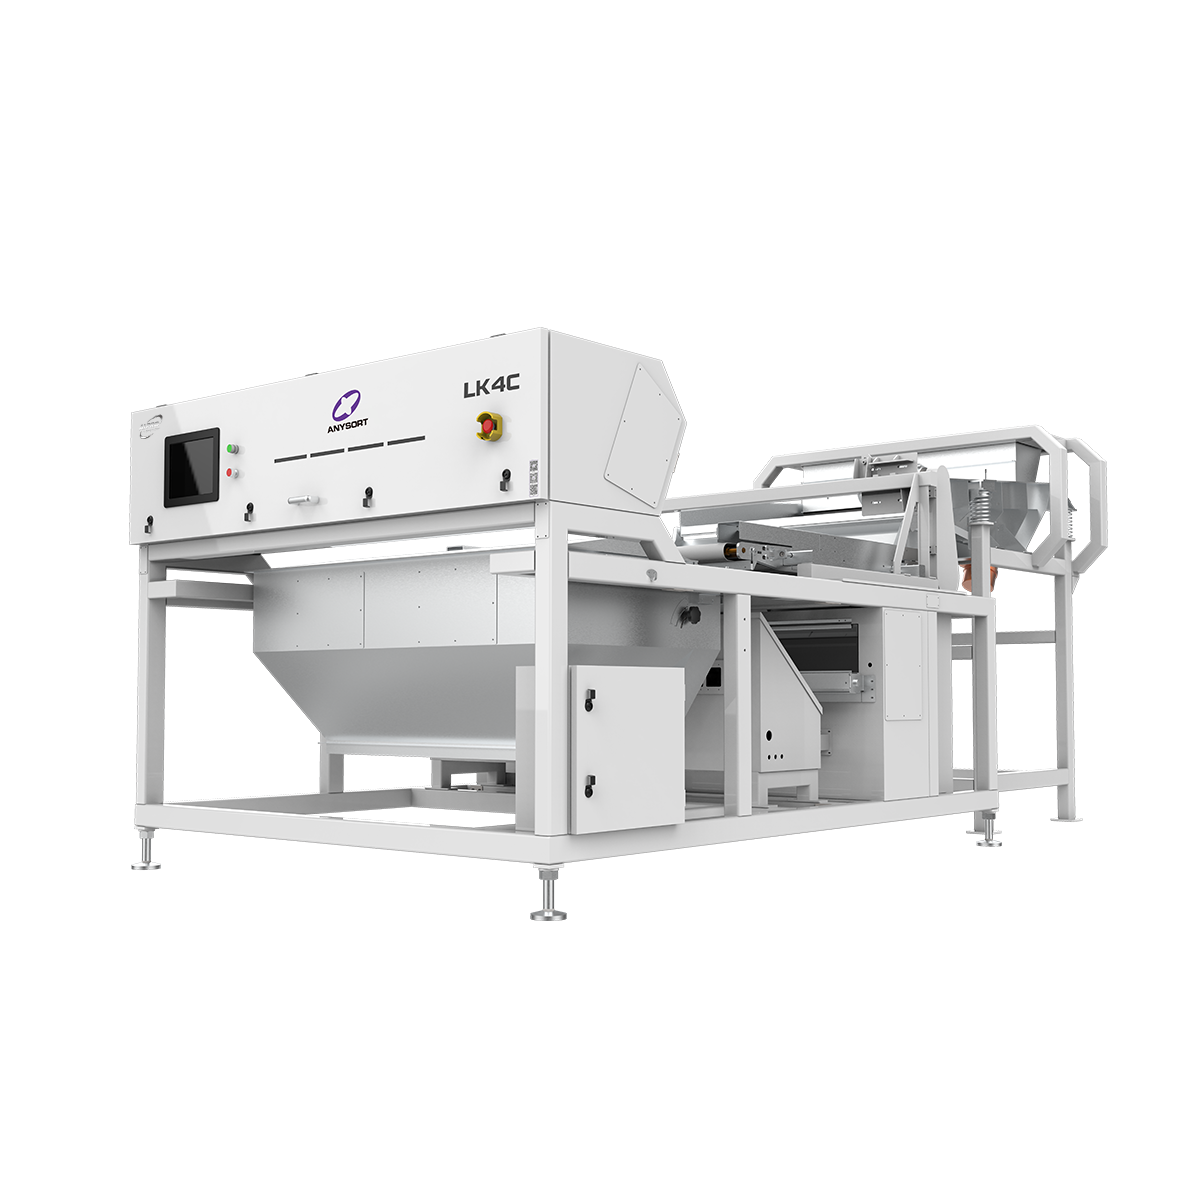
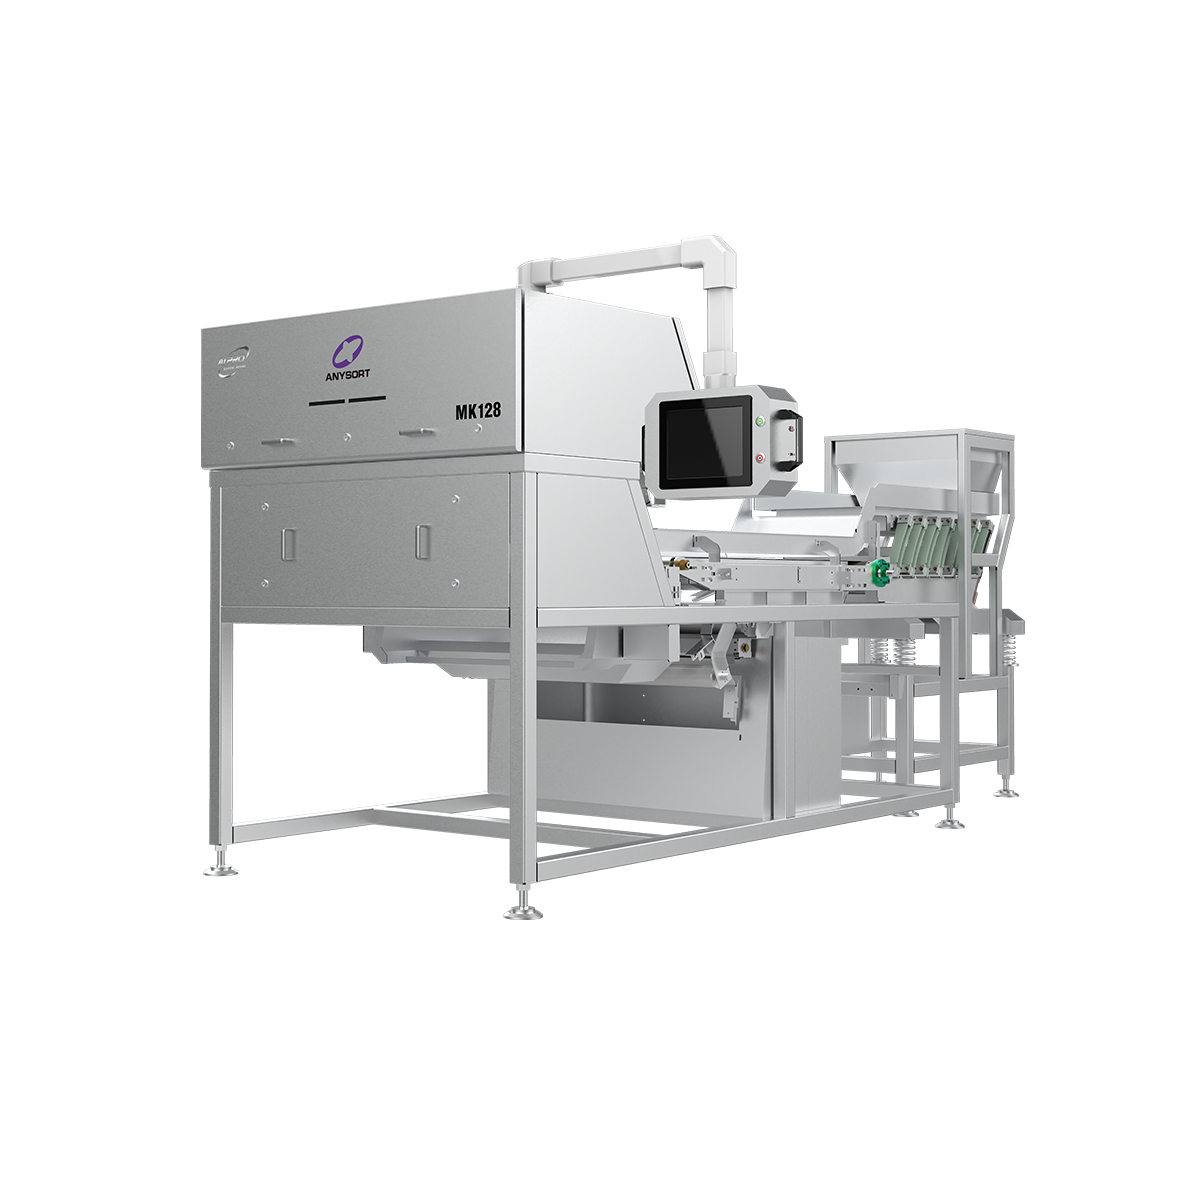
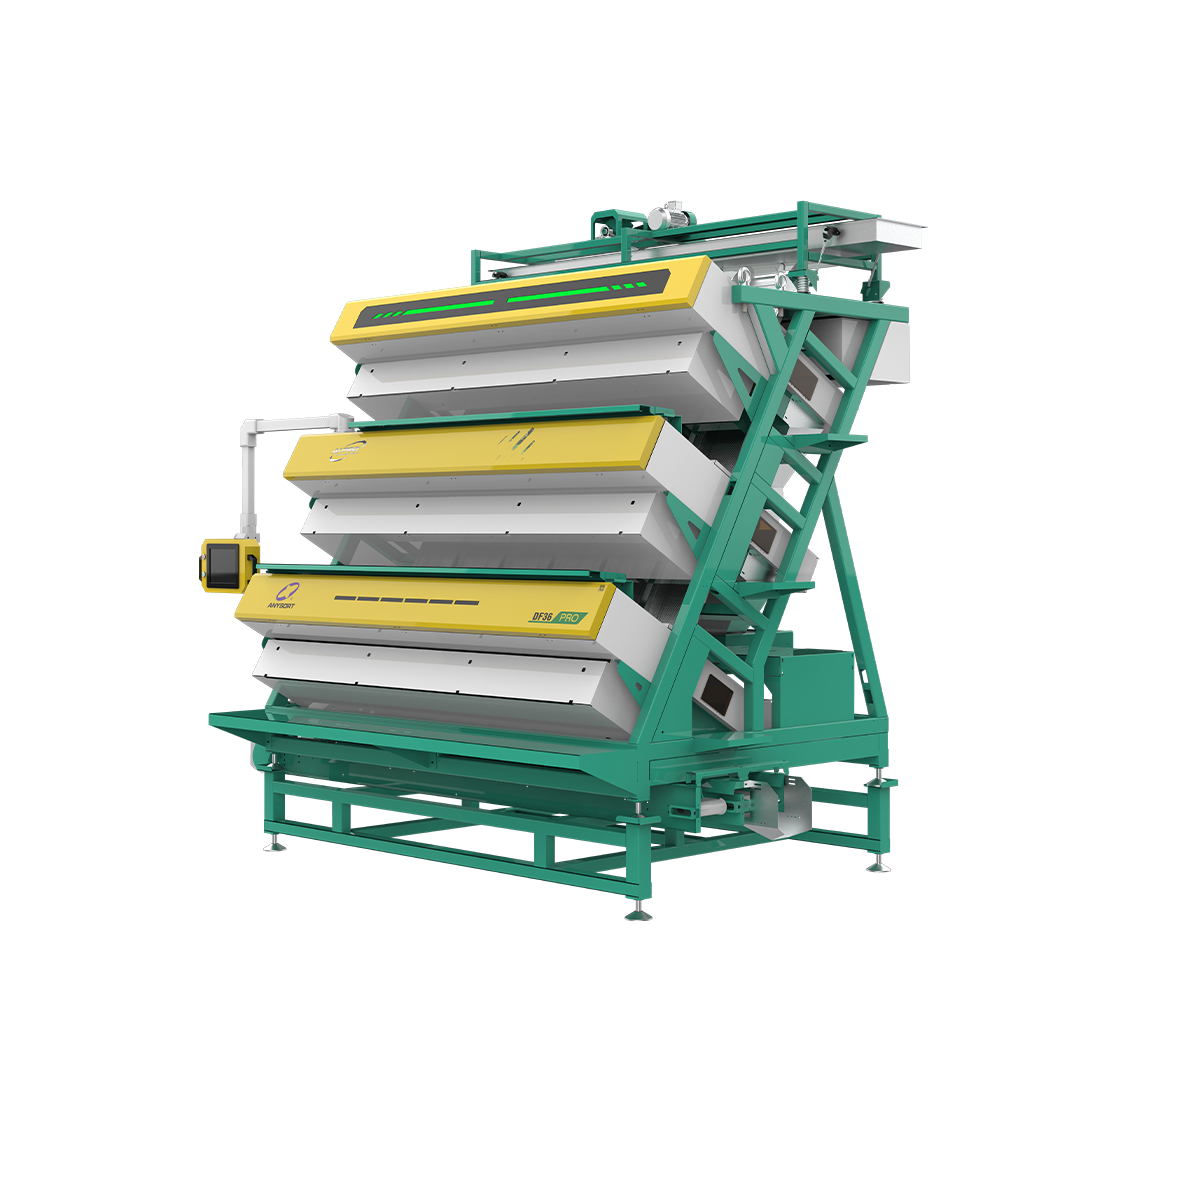
Rice Color Sorter Machine

All Categories

rice color sorter machine

A rice color sorter machine represents advanced technology designed to automatically separate rice grains by color and quality. This innovative rice color sorter machine uses optical scanning and artificial intelligence to detect defects, discolored grains, and foreign materials with remarkable precision. The rice color sorter machine operates by passing rice through a high-speed camera system that captures images of each grain, analyzing them against pre-set quality standards. Modern rice color sorter machine systems can process up to 6 tons per hour while maintaining exceptional accuracy rates exceeding 99 percent. The technology behind the rice color sorter machine includes LED lighting, high-resolution cameras, and sophisticated sorting algorithms that work together seamlessly. These machines feature multiple discharge channels, allowing sorted rice to be separated into different quality grades simultaneously. The rice color sorter machine is equipped with user-friendly interfaces that enable operators to adjust sorting parameters easily. Applications span across rice mills, food processing facilities, and agricultural cooperatives worldwide. The rice color sorter machine delivers consistent results regardless of rice variety, whether processing white rice, brown rice, or specialty varieties. Investment in a rice color sorter machine significantly reduces manual labor costs while improving product quality and market competitiveness. The machine's durability and low maintenance requirements make it a cost-effective solution for rice processing operations of all sizes seeking efficiency and quality assurance.

Popular Products

Rice color sorter machines deliver exceptional value to buyers through superior operational efficiency and quality enhancement. The primary advantage of a rice color sorter machine is its ability to remove defective grains automatically, ensuring only premium quality rice reaches customers. This eliminates costly manual sorting processes and reduces labor expenses substantially. Businesses using a rice color sorter machine experience increased production throughput while maintaining consistent quality standards that enhance brand reputation. The rice color sorter machine minimizes product waste by precisely separating damaged grains, broken pieces, and discolored kernels that would otherwise reduce marketability. Operational benefits include 24/7 automated processing capability, which maximizes productivity compared to traditional hand-sorting methods. A rice color sorter machine adapts to various rice types and processing requirements without extensive reconfiguration, providing flexibility for diverse operations. The technology ensures food safety compliance by removing foreign objects and contaminated grains that pose health risks. Investment in a rice color sorter machine yields rapid returns through premium pricing opportunities and reduced losses from rejected batches. The machine's precision sorting capabilities enable processors to create multiple quality grades simultaneously, opening new market segments and revenue streams. Companies deploying a rice color sorter machine report improved employee satisfaction by eliminating monotonous manual work. The equipment's intelligent sorting system learns and adapts over time, improving accuracy continuously. Additionally, the rice color sorter machine provides detailed reporting on sorting outcomes, helping operators make data-driven decisions for process optimization and quality management improvements.

Practical Tips

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

rice color sorter machine

Advanced Optical Technology for Precision Sorting

Advanced Optical Technology for Precision Sorting

The rice color sorter machine utilizes cutting-edge optical scanning technology with high-resolution cameras and specialized lighting systems to examine every single grain. This sophisticated rice color sorter machine can distinguish between acceptable rice and defective grains with extraordinary accuracy, detecting even subtle color variations and surface imperfections invisible to human eyes. The advanced sensors in a rice color sorter machine capture multiple images per grain from different angles, ensuring comprehensive quality assessment. The system processes this visual data through artificial intelligence algorithms that compare each grain against established quality parameters in milliseconds. This precision capability makes the rice color sorter machine invaluable for premium rice producers who demand consistent excellence. The optical technology eliminates human error and fatigue associated with manual inspection, delivering uniform results every processing cycle. Users can customize sorting sensitivity settings within the rice color sorter machine interface, adapting to specific rice variety requirements and market demands. The enhanced accuracy of a rice color sorter machine translates directly into higher customer satisfaction and reduced product returns. Investment protection is ensured through this technology's reliability and consistent performance under continuous operational demands.
High-Capacity Processing for Large-Scale Operations

High-Capacity Processing for Large-Scale Operations

A rice color sorter machine handles impressive processing volumes reaching up to 6 tons per hour, making it ideal for commercial rice mills and large agricultural operations. This exceptional capacity of the rice color sorter machine means businesses can process substantial daily quantities without bottlenecks or production delays. The rice color sorter machine's high-speed performance maintains sorting accuracy despite rapid throughput, which distinguishes it from slower alternative technologies. Multiple discharge channels within the rice color sorter machine enable simultaneous distribution of sorted rice into different quality categories, maximizing efficiency. Operators benefit from the rice color sorter machine's ability to run continuously for extended periods, supporting 24/7 production schedules that maximize facility utilization. The system's robust construction ensures the rice color sorter machine maintains reliability even under demanding operational conditions requiring consistent high-volume processing. This capacity advantage of the rice color sorter machine directly reduces processing time per batch, accelerating inventory turnover and cash flow. Large-scale processors find the rice color sorter machine essential for meeting contracted supply volumes while maintaining quality commitments. The machine's performance scalability means your rice color sorter machine investment grows with your business expansion needs.
Cost Reduction and Return on Investment Benefits

Cost Reduction and Return on Investment Benefits

Implementing a rice color sorter machine delivers substantial financial benefits through labor cost elimination and productivity gains that quickly justify the investment. The rice color sorter machine replaces multiple manual sorters, reducing payroll expenses while improving output consistency significantly. Processing efficiency improvements within the rice color sorter machine lower per-unit production costs, enhancing profit margins substantially. Minimal waste from the rice color sorter machine's precise sorting means every gram of purchasable rice reaches market, maximizing revenue per ton processed. The rice color sorter machine reduces product returns and customer complaints through superior quality assurance, protecting brand reputation and repeat business. Maintenance costs remain low for the rice color sorter machine, with durable components designed for extended operational lifespan and minimal downtime. Energy efficiency features of the rice color sorter machine keep utility expenses reasonable despite high-speed operation. Companies achieve break-even points on rice color sorter machine investments within months rather than years, owing to immediate labor and waste reduction benefits. Premium pricing opportunities emerge when processors using a rice color sorter machine deliver consistently superior quality products commanding higher market values. The transparent cost-benefit analysis of a rice color sorter machine makes financial planning straightforward for business decision-makers and investors.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy