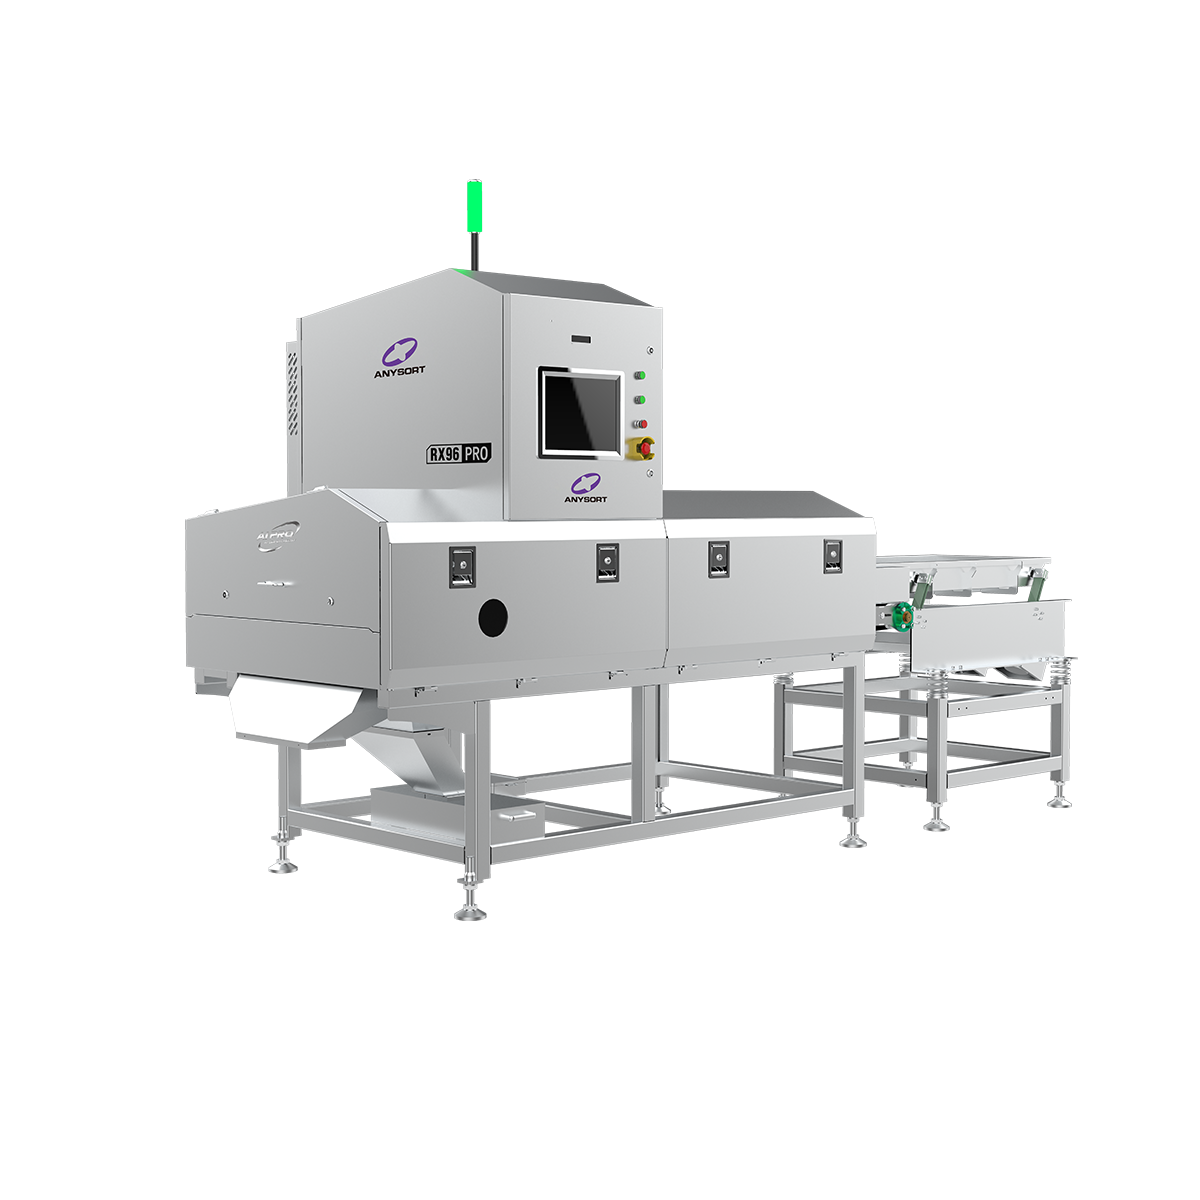
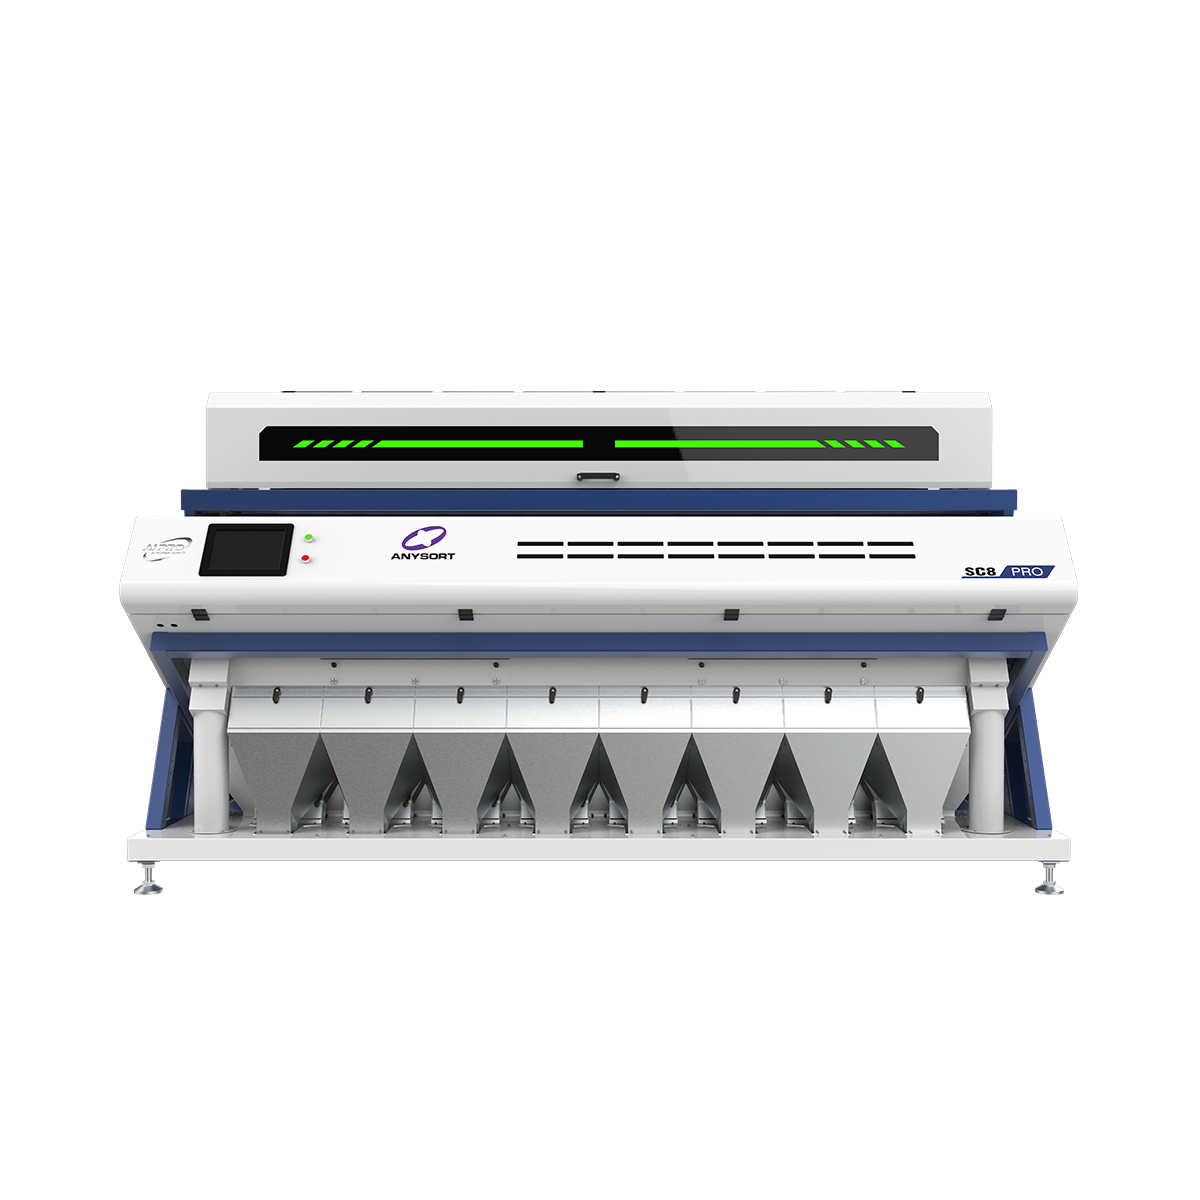
color sorter machine market
The color sorter machine market represents a significant segment within the industrial automation and food processing equipment industry. These sophisticated machines utilize advanced optical sensing technology to automatically classify and separate materials based on color characteristics. The color sorter machine market has experienced substantial growth due to increasing demand for quality control and product consistency across various sectors.
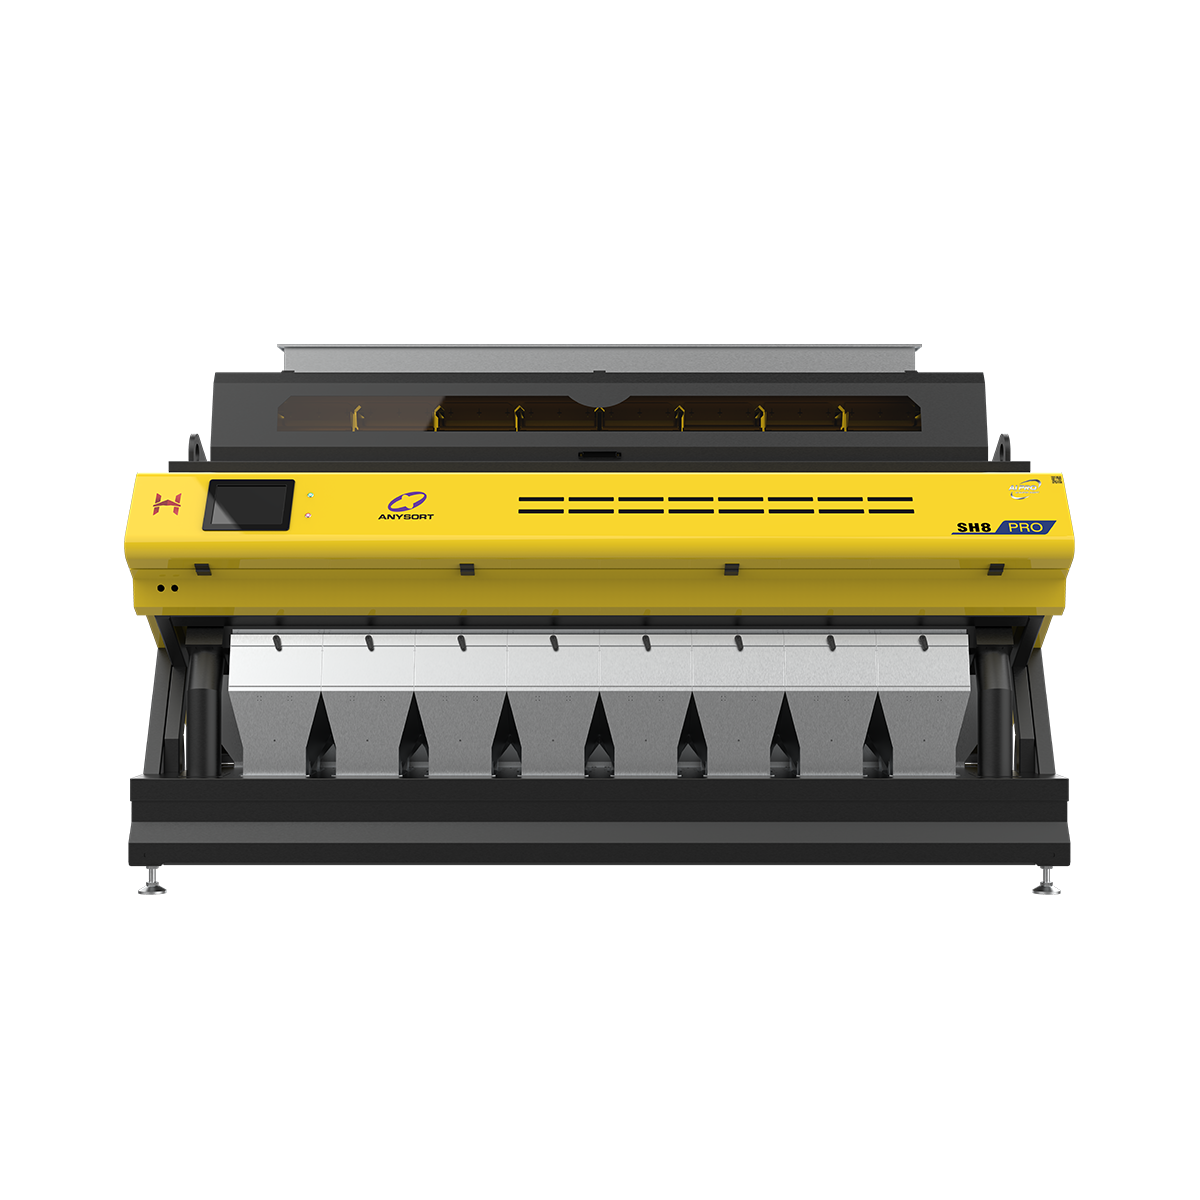
Color sorter machines function by capturing high-resolution images of products passing through their sorting channels. Advanced cameras and sensors detect subtle color variations, defects, and foreign materials that human operators might miss. The color sorter machine market benefits from machine learning algorithms that continuously improve sorting accuracy. These systems process thousands of items per minute, significantly exceeding manual sorting capabilities.
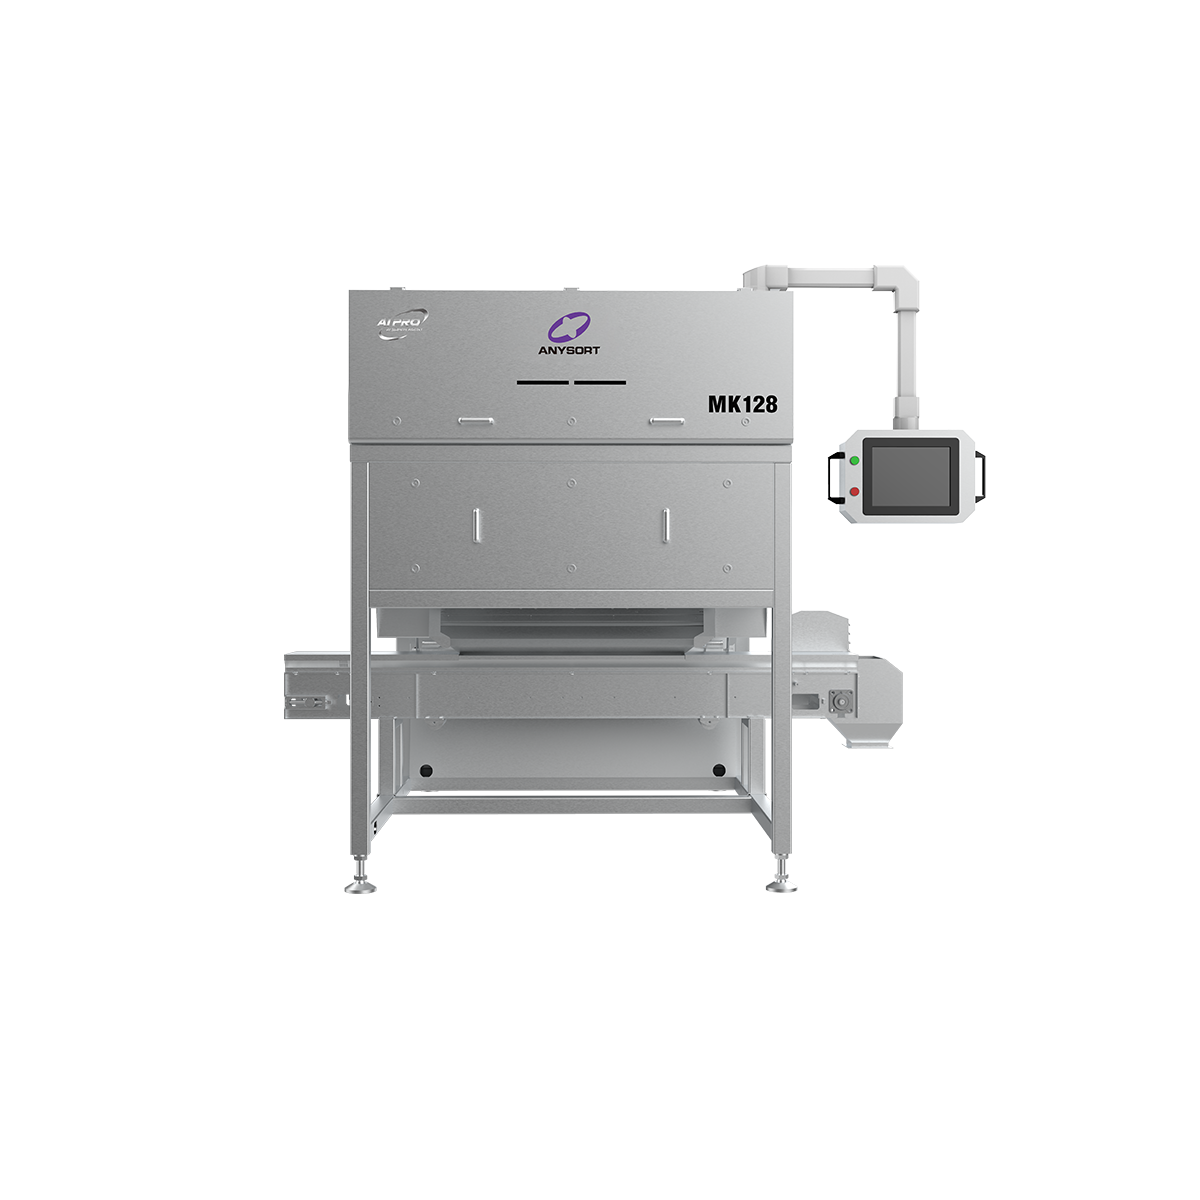
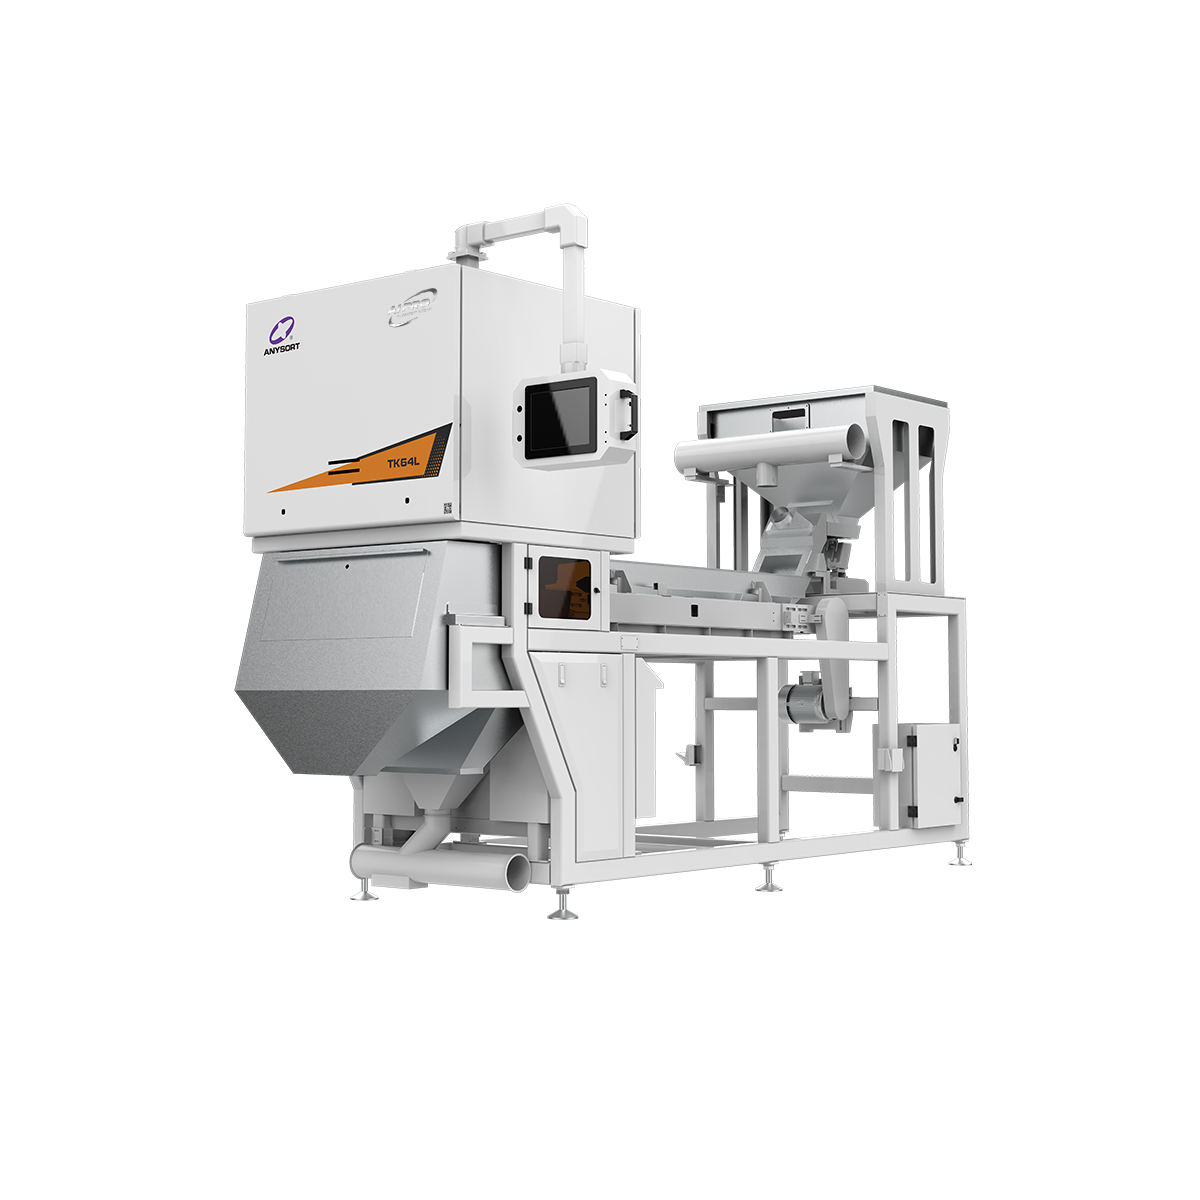
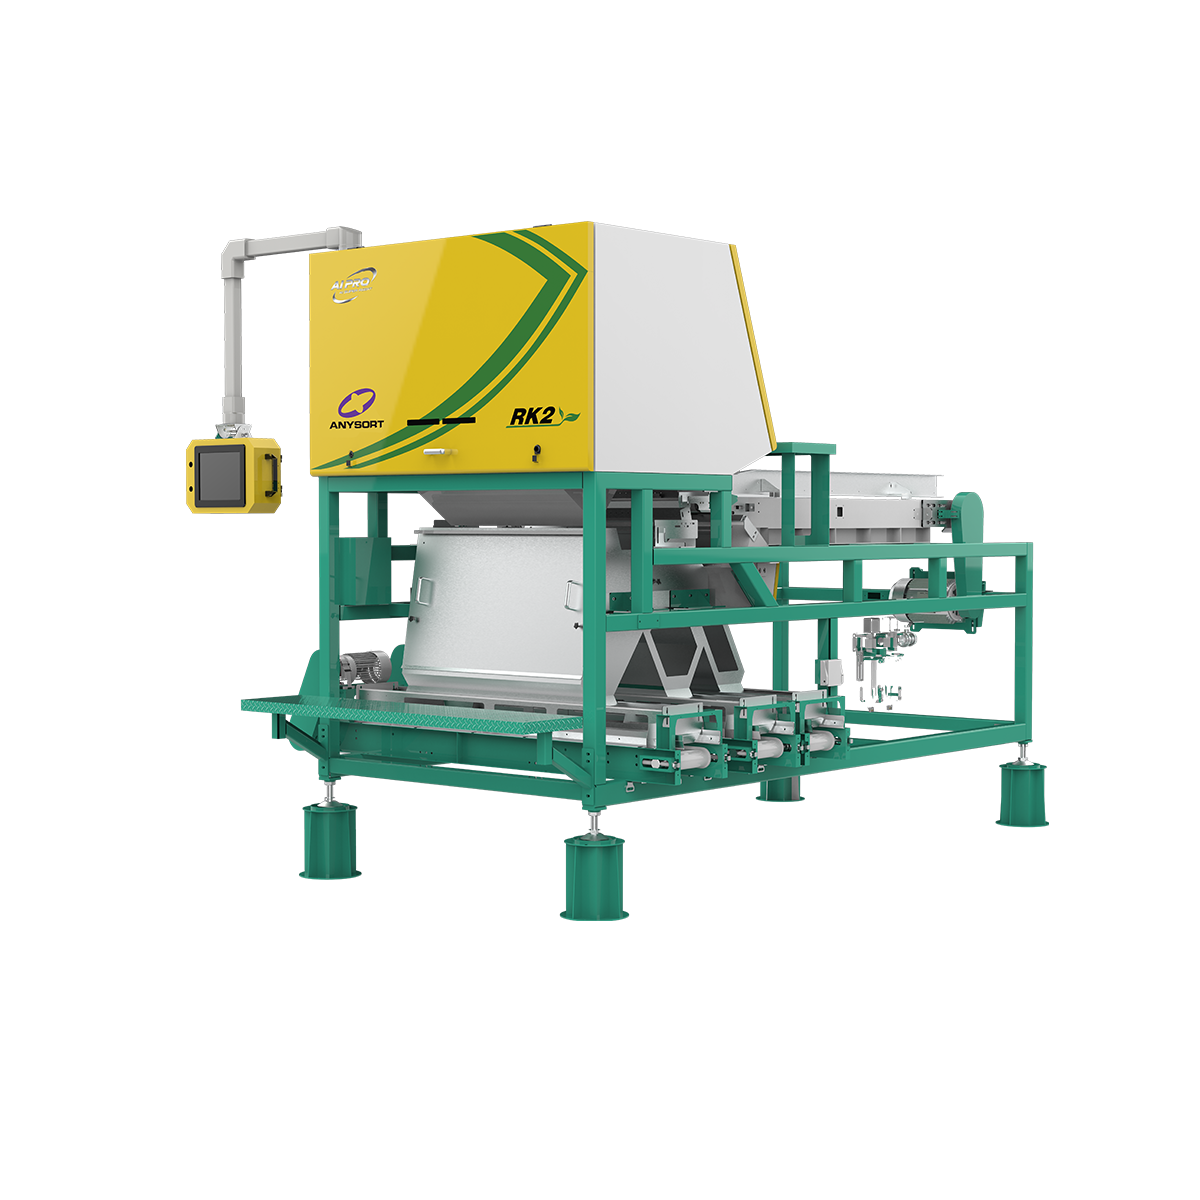
Key technological features include RGB and multispectral imaging, real-time data processing, and pneumatic ejection systems. Modern color sorter machine market participants offer machines with adjustable sensitivity levels, allowing operators to customize sorting parameters for specific applications. Integration with conveyor systems enables seamless workflow automation.
Applications span agriculture, food processing, recycling, and mining industries. In agriculture, the color sorter machine market serves grain sorting, rice processing, and dried fruit quality control. Food manufacturers rely on these machines to remove discolored items, contaminated products, and foreign objects. The color sorter machine market continues expanding as industries prioritize quality assurance and operational efficiency.

 EN