Bottle Recycling Machine | Automated Sorting Solutions

All Categories

bottle recycling machine

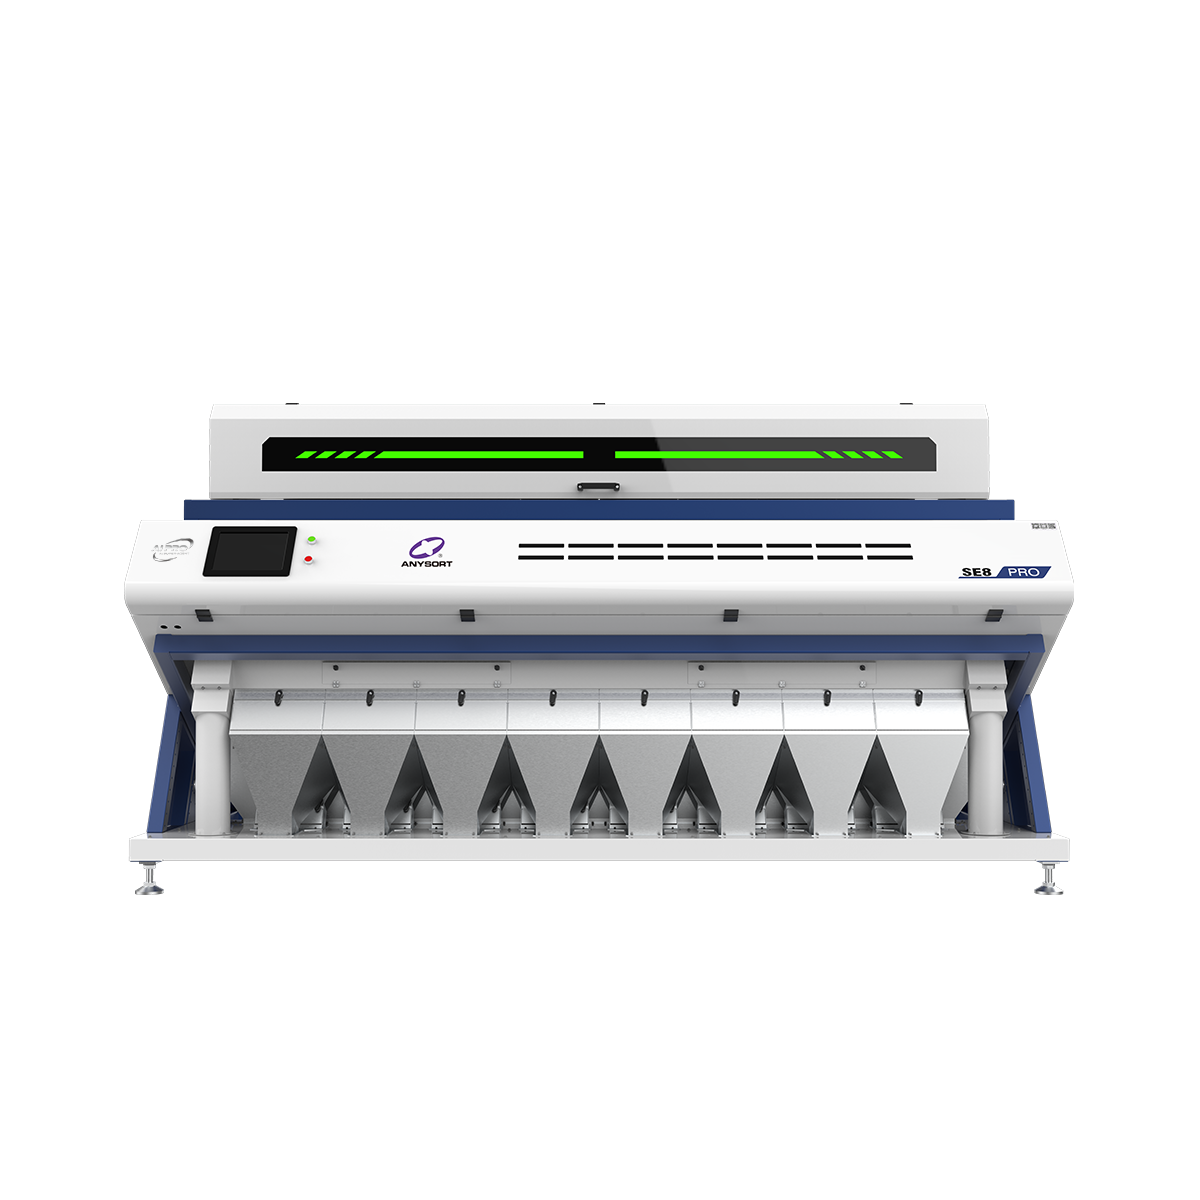
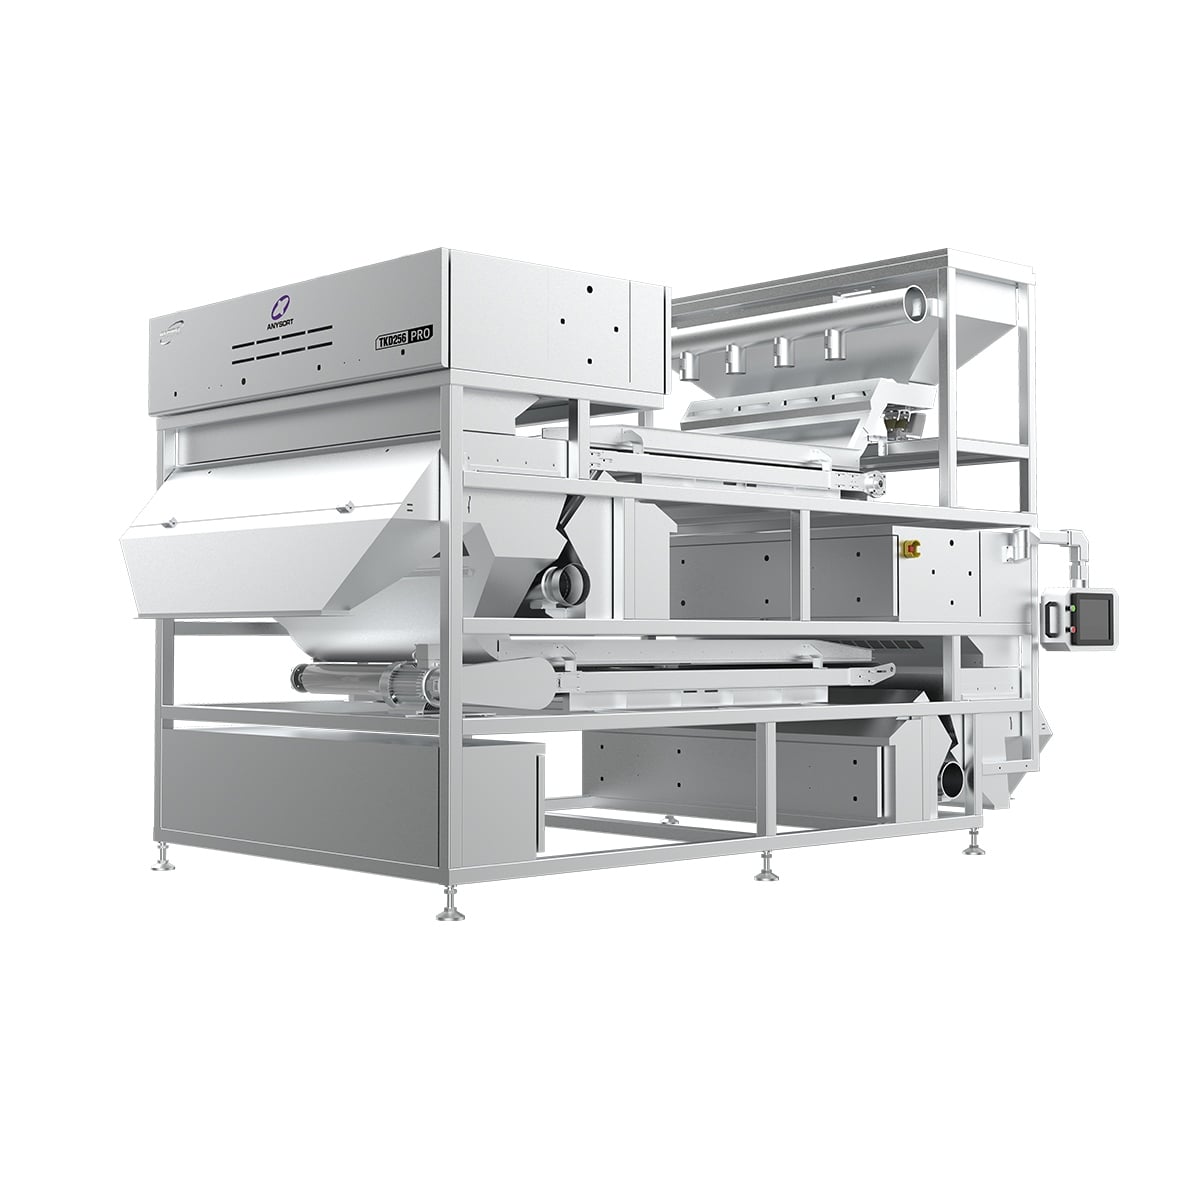
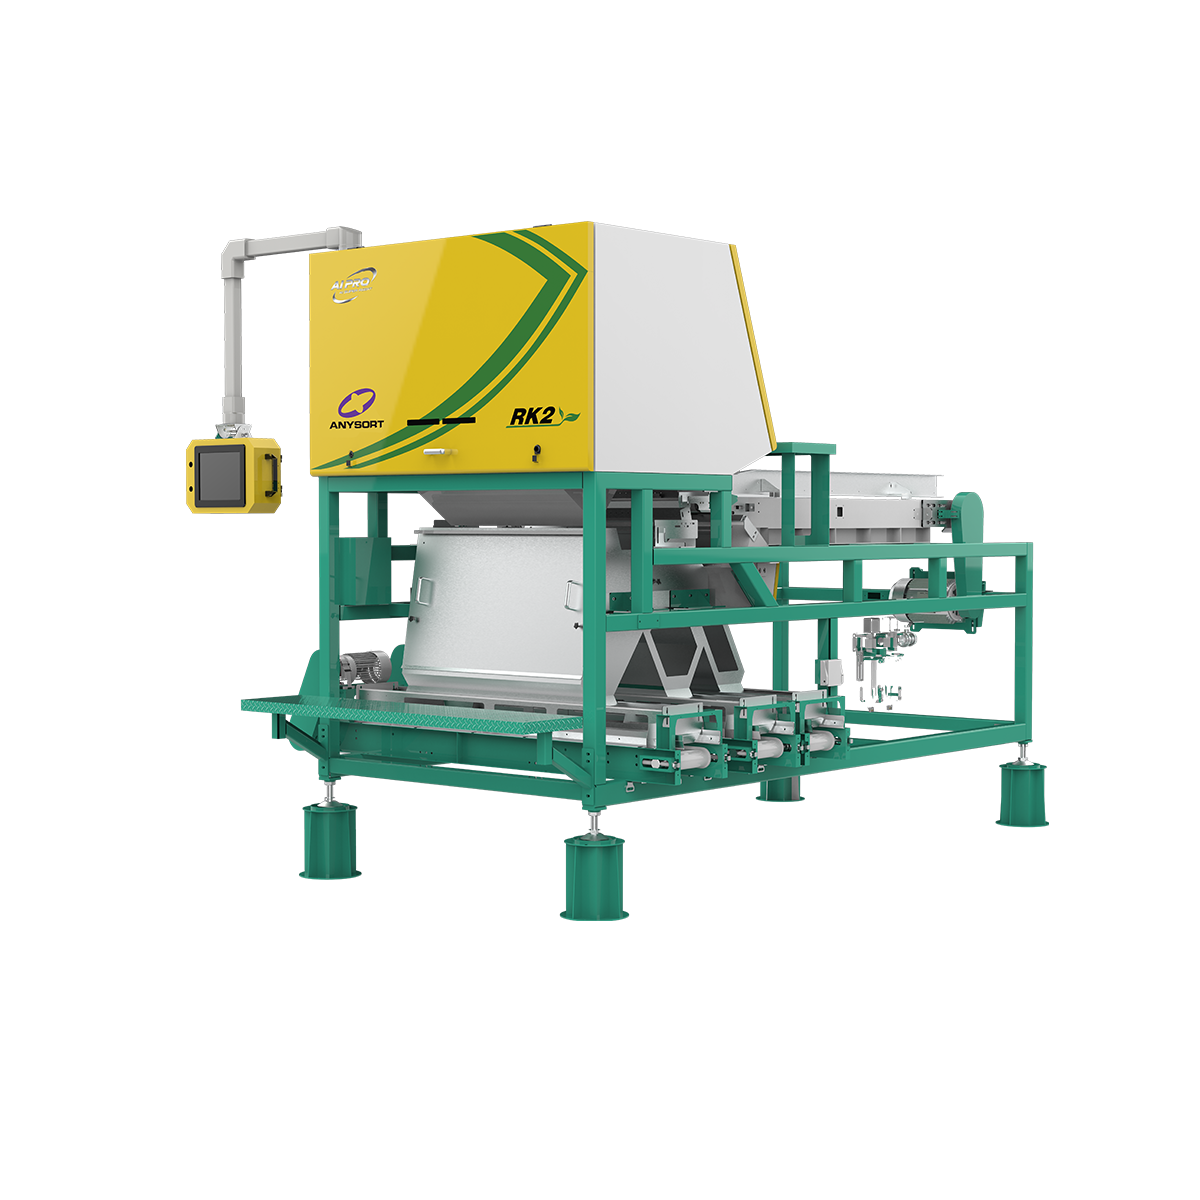
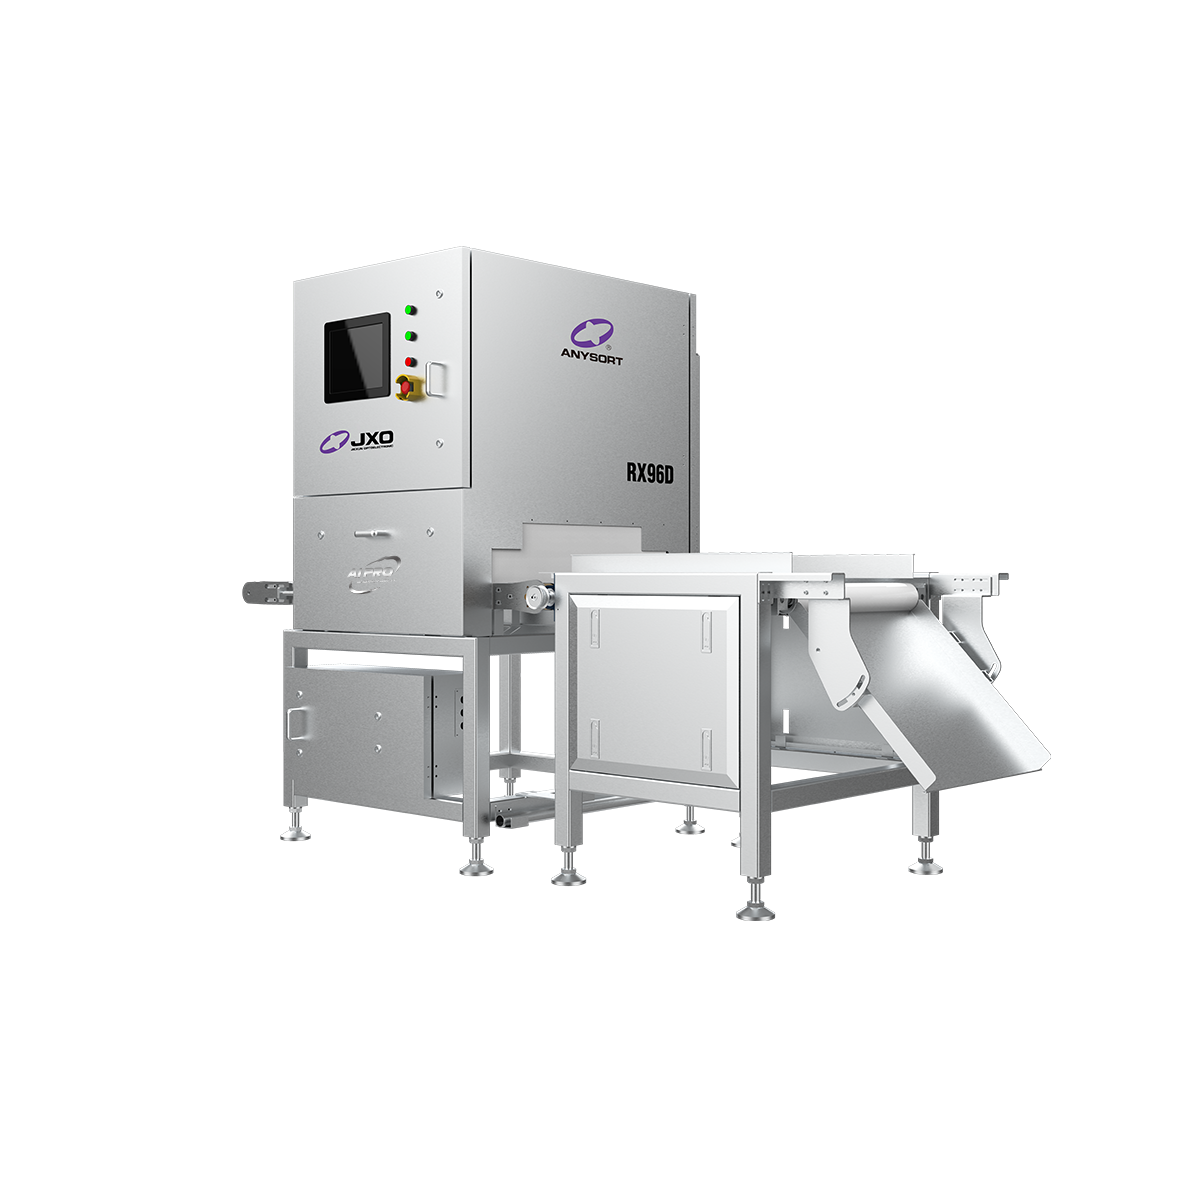
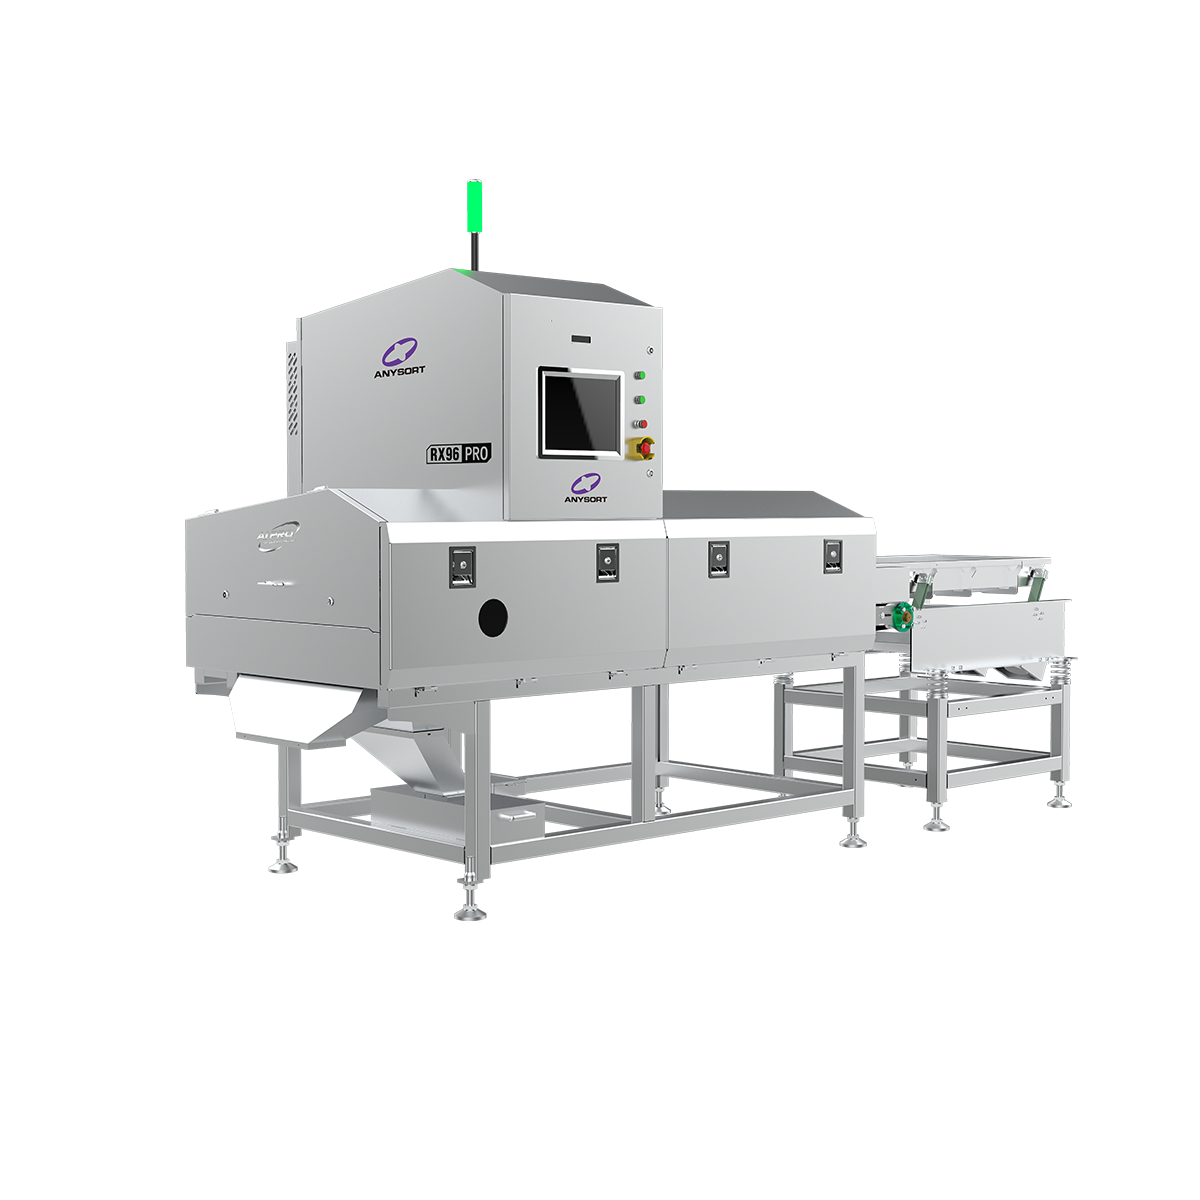
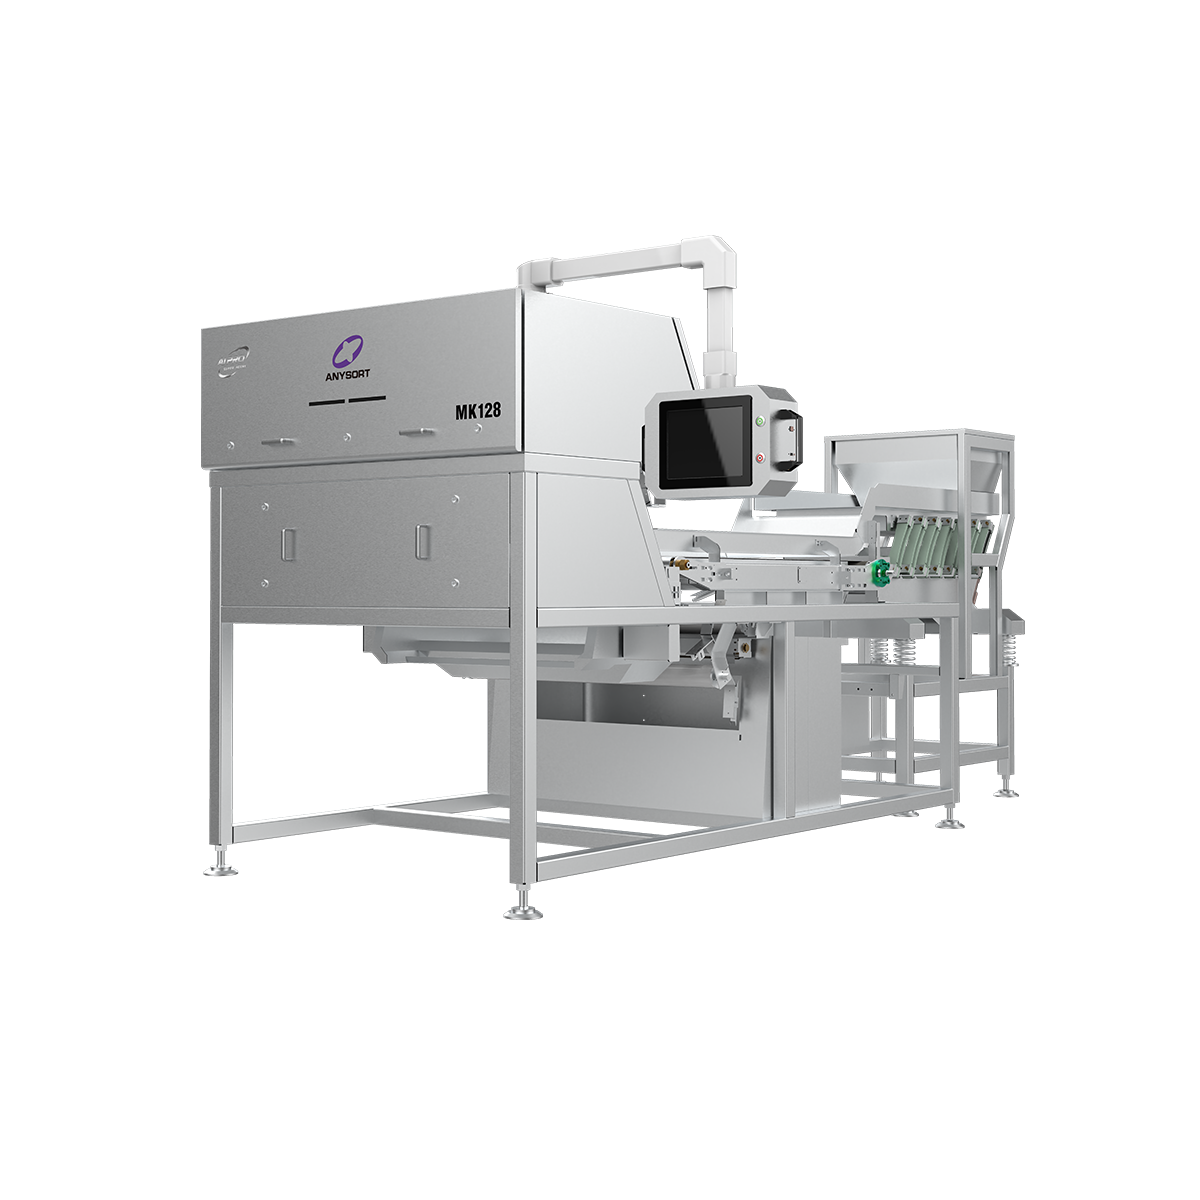
A bottle recycling machine is an innovative automated system designed to collect, sort, and process used bottles efficiently. This machine represents a significant advancement in waste management technology, enabling businesses and municipalities to handle bottle waste at scale while promoting environmental sustainability. The bottle recycling machine operates by accepting various bottle types, including plastic, glass, and aluminum containers. Through sophisticated sensor technology and mechanical sorting mechanisms, the machine automatically categorizes bottles by material composition and color. This automated sorting capability ensures higher purity levels in recycled materials, making them more valuable for manufacturers. Key technological features of a bottle recycling machine include optical scanning systems, pneumatic compression units, and integrated data tracking. The optical sensors identify bottle materials and colors with remarkable accuracy, while compression components reduce volume, maximizing storage capacity. Many modern bottle recycling machine models include IoT connectivity, allowing real-time monitoring of collection statistics and operational performance. Applications for bottle recycling machine systems span multiple sectors. Retail establishments, restaurants, and beverage distribution centers benefit from compact models designed for high-volume collection. Municipalities deploy larger bottle recycling machine installations at recycling facilities to process community waste. Educational institutions and corporate offices utilize bottle recycling machine technology to meet sustainability goals and reduce landfill contributions. The bottle recycling machine streamlines the entire recycling workflow, from initial collection through material separation. By automating labor-intensive sorting processes, this equipment reduces operational costs while improving material quality. Whether implemented in commercial settings or municipal recycling centers, the bottle recycling machine delivers measurable environmental impact and economic returns.

New Product Releases

The bottle recycling machine delivers substantial practical benefits that transform how organizations approach waste management. This equipment operates continuously without requiring constant human supervision, reducing labor costs significantly while maintaining consistent processing quality. Businesses experience immediate operational efficiency gains when implementing a bottle recycling machine system. Cost savings represent one of the most compelling advantages of bottle recycling machine technology. Automated sorting reduces contamination in recycled materials, enabling better market prices for processed content. Companies eliminate expensive manual labor traditionally associated with bottle sorting, directly improving profit margins. The bottle recycling machine recycles bottles faster than manual methods, accelerating cash flow from material sales. Environmental benefits make the bottle recycling machine an essential tool for corporate responsibility initiatives. This equipment diverts substantial quantities of bottles from landfills, reducing environmental impact. Organizations demonstrate genuine sustainability commitment by deploying bottle recycling machine solutions, enhancing brand reputation with environmentally conscious consumers. The bottle recycling machine enables measurable reporting on waste diversion metrics. Operational suitability varies across different business types. Beverage retailers find bottle recycling machine units ideal for high-volume collection environments. Hospitality venues benefit from compact models fitting limited spaces while processing substantial quantities. Municipal facilities utilize industrial-scale bottle recycling machine systems for comprehensive community waste processing. Educational campuses successfully deploy bottle recycling machine technology to align with institutional sustainability pledges. Decision-useful context clarifies why bottle recycling machine investment makes business sense. Equipment ROI typically materializes within months through reduced labor expenses and material revenue. Organizations scaling sustainability efforts discover that bottle recycling machine automation provides competitive advantages. The technology demonstrates commitment to environmental standards increasingly required by regulations and consumer expectations. Implementing a bottle recycling machine positions businesses as industry leaders in waste management innovation.

Latest News

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

bottle recycling machine

Advanced Automated Sorting Technology

Advanced Automated Sorting Technology

The bottle recycling machine incorporates cutting-edge optical recognition systems that identify and sort bottles by material type and color with exceptional precision. This automated sorting capability eliminates the need for manual labor, dramatically reducing operational costs while ensuring superior material purity. The bottle recycling machine uses infrared sensors and machine learning algorithms to distinguish between plastic varieties, glass colors, and aluminum compositions instantly. This technological advantage means businesses maximize revenue from recycled materials by delivering consistently pure sorted batches to processors. The bottle recycling machine automatically rejects contaminated items, protecting downstream manufacturing operations. Organizations benefit from reduced processing time and improved product quality metrics. The precision sorting offered by a bottle recycling machine significantly outperforms manual methods, making it essential for high-volume recycling operations seeking competitive advantages in material markets.
Space-Efficient Design with Maximum Capacity

Space-Efficient Design with Maximum Capacity

Modern bottle recycling machine models feature intelligent compact designs that maximize collection capacity while minimizing footprint requirements. These machines incorporate powerful compression technology that reduces bottle volume dramatically, allowing single units to process material equivalent to much larger conventional containers. The bottle recycling machine's vertical orientation and modular construction suit diverse location constraints from retail floors to municipal facilities. The bottle recycling machine provides exceptional throughput despite compact dimensions, processing hundreds of bottles hourly while maintaining minimal spatial impact. Businesses appreciate how bottle recycling machine solutions fit seamlessly into existing environments without requiring facility modifications. The compression feature enables organizations to collect more material between emptying cycles, reducing labor-intensive maintenance tasks. Space-efficient bottle recycling machine deployment particularly benefits urban locations, retail establishments, and campuses where real estate constraints limit traditional recycling infrastructure expansion.
Real-Time Data Tracking and Sustainability Reporting

Real-Time Data Tracking and Sustainability Reporting

Contemporary bottle recycling machine systems integrate IoT connectivity enabling real-time monitoring of collection metrics and operational performance. Organizations access comprehensive dashboards displaying processed bottle quantities, material composition breakdowns, and system efficiency ratings. The bottle recycling machine provides actionable data supporting sustainability initiatives and corporate reporting obligations. Cloud-based platforms associated with bottle recycling machine networks facilitate remote monitoring and predictive maintenance alerts. This data transparency helps businesses validate environmental impact claims with concrete documentation. The bottle recycling machine generates detailed reports supporting regulatory compliance and stakeholder communications. Companies demonstrate measurable progress toward sustainability targets through bottle recycling machine performance analytics. Organizations utilize this intelligence for optimizing collection schedules and predicting revenue from processed materials. Real-time tracking transforms bottle recycling machine deployment into comprehensive waste management systems beyond simple collection, enabling data-driven decision-making that enhances profitability while demonstrating environmental responsibility.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy