best rice color sorter
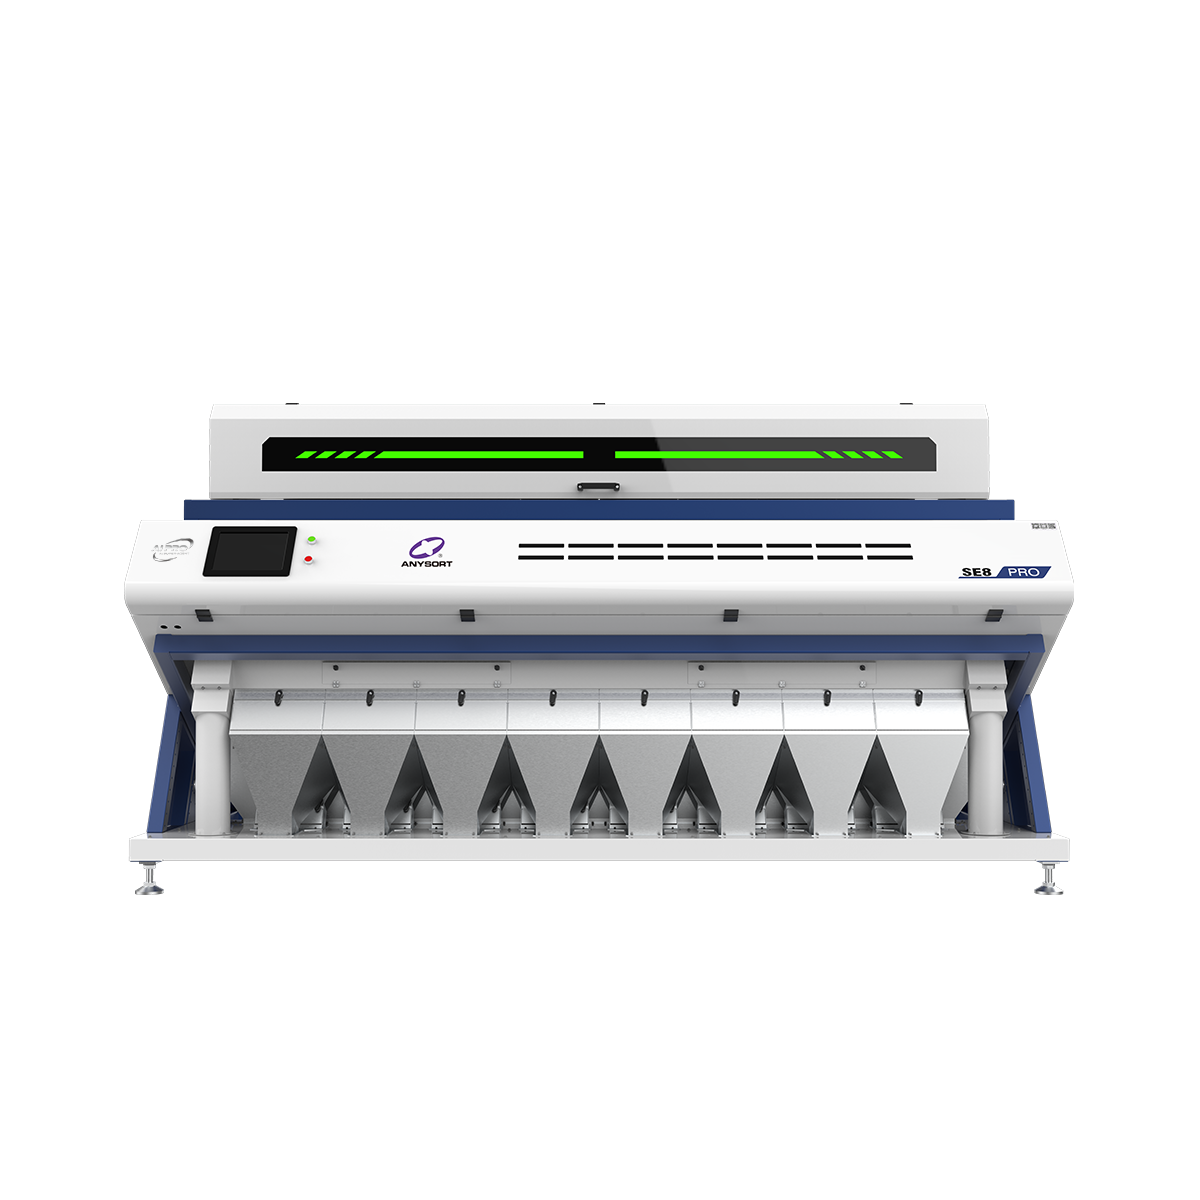
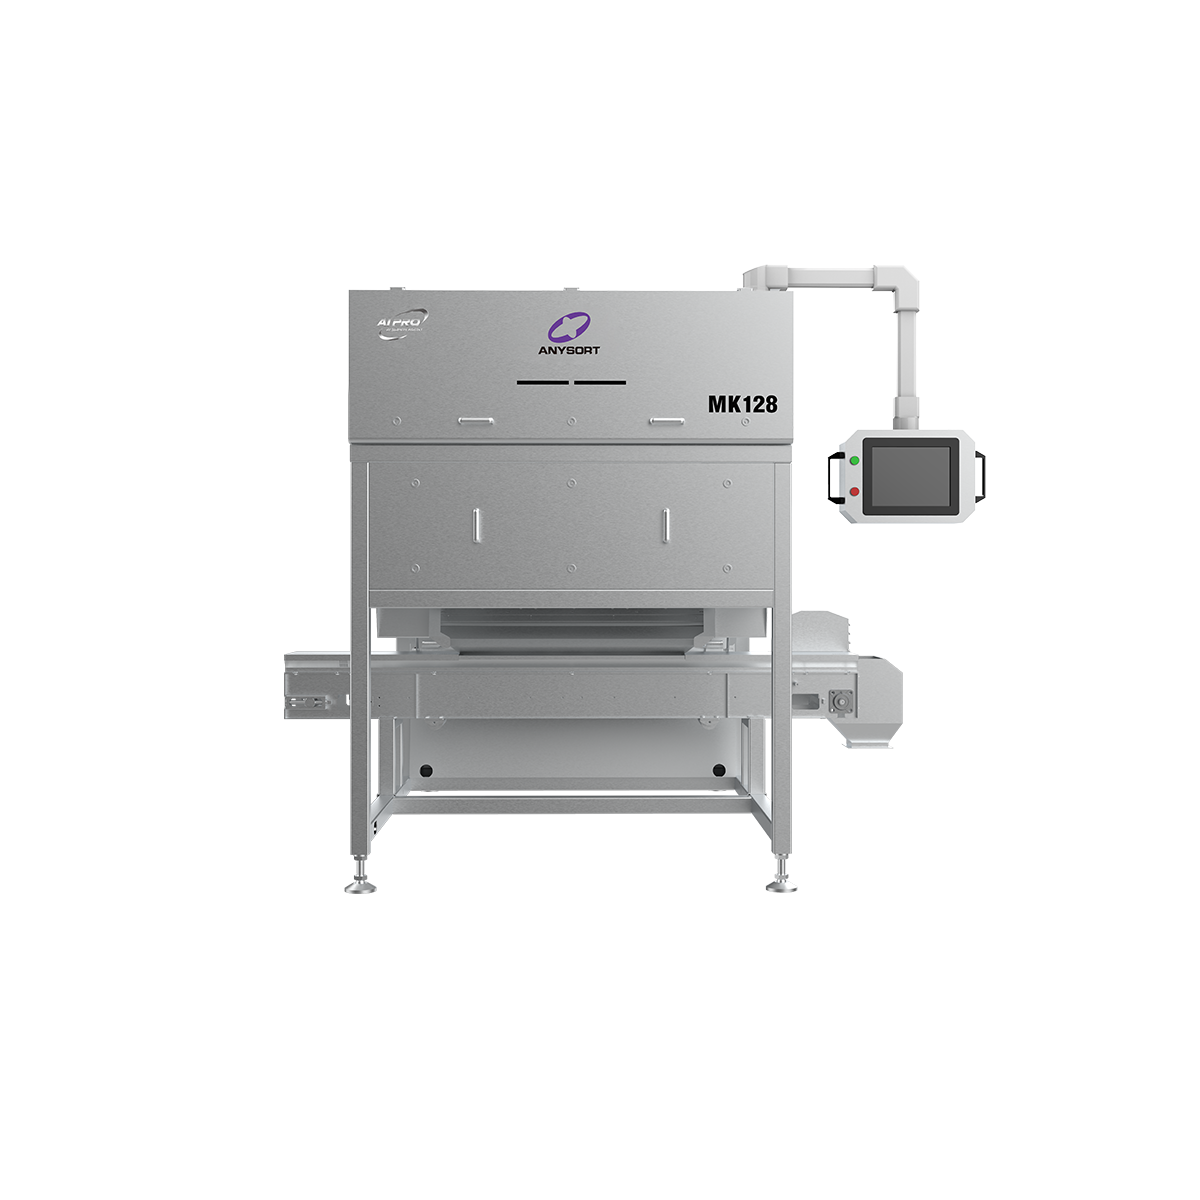
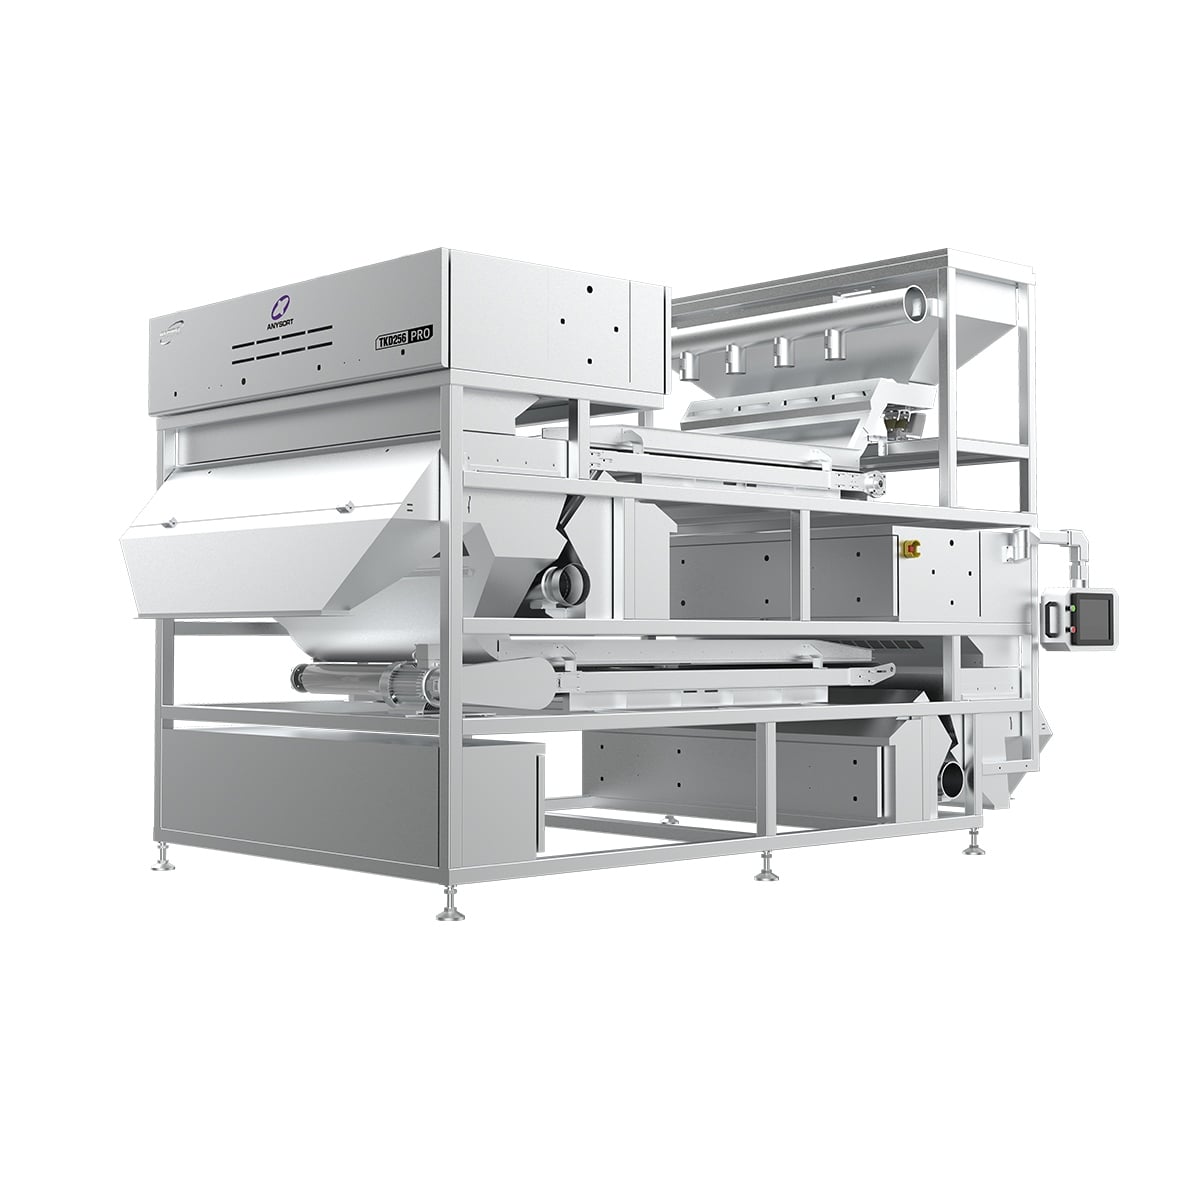
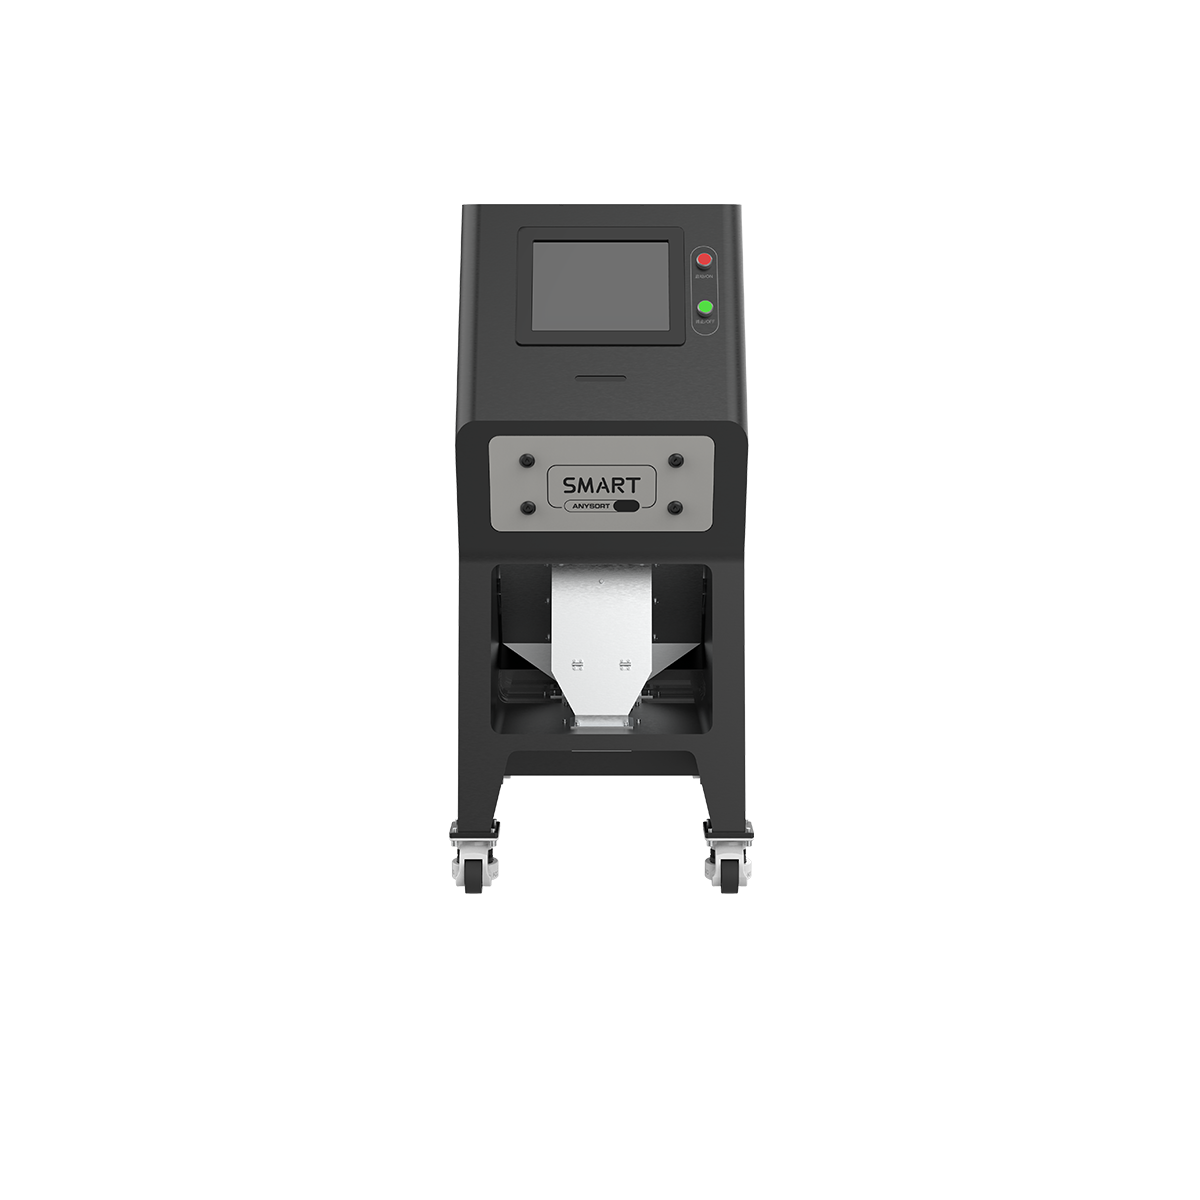
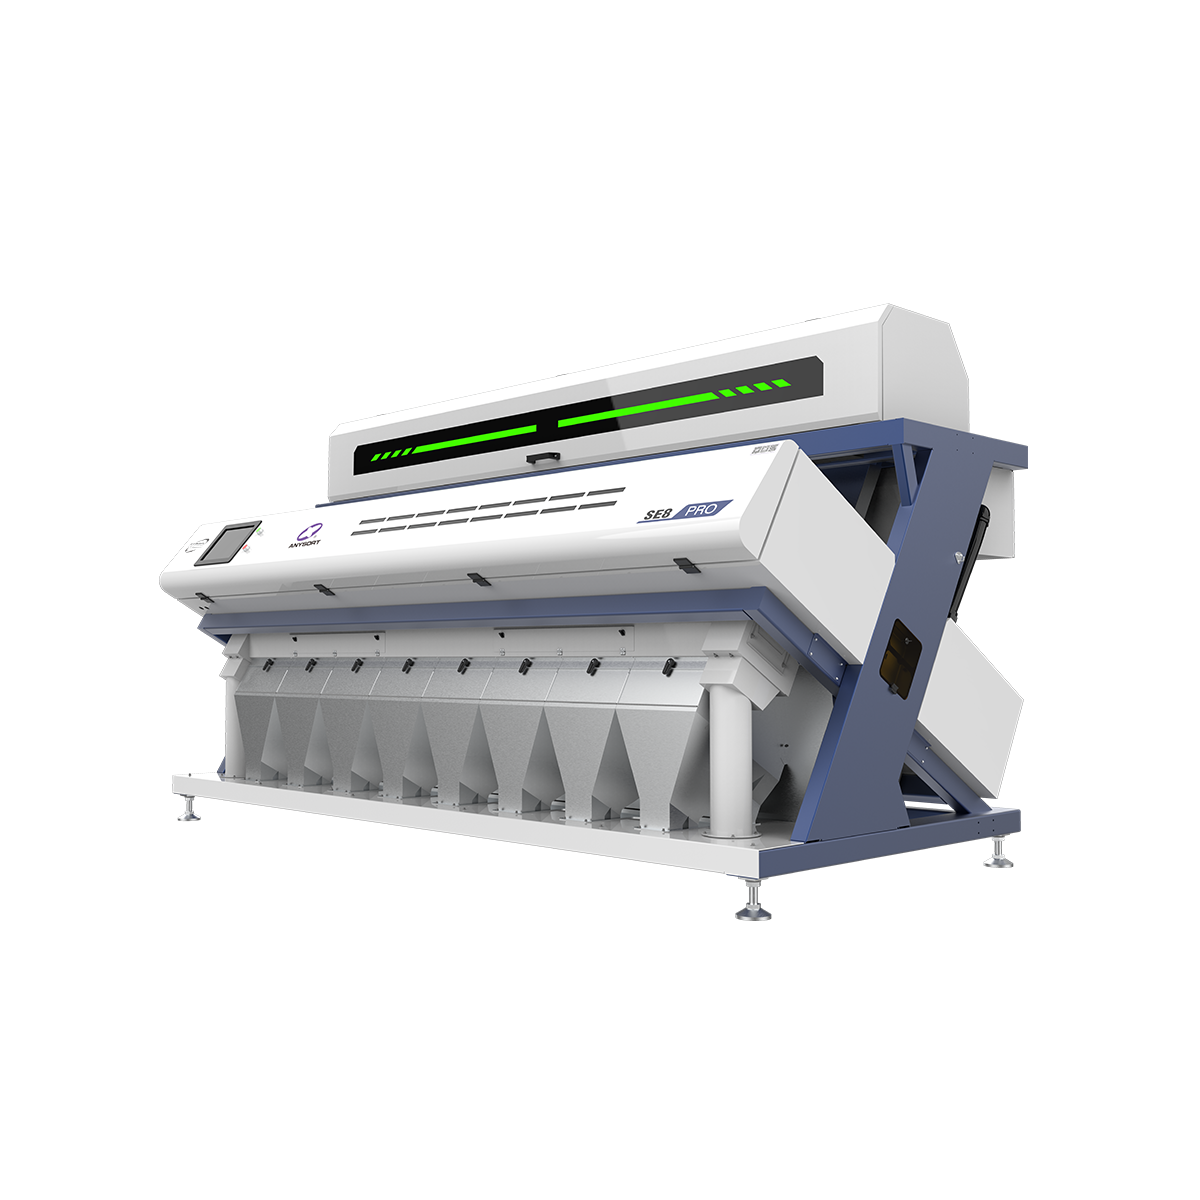
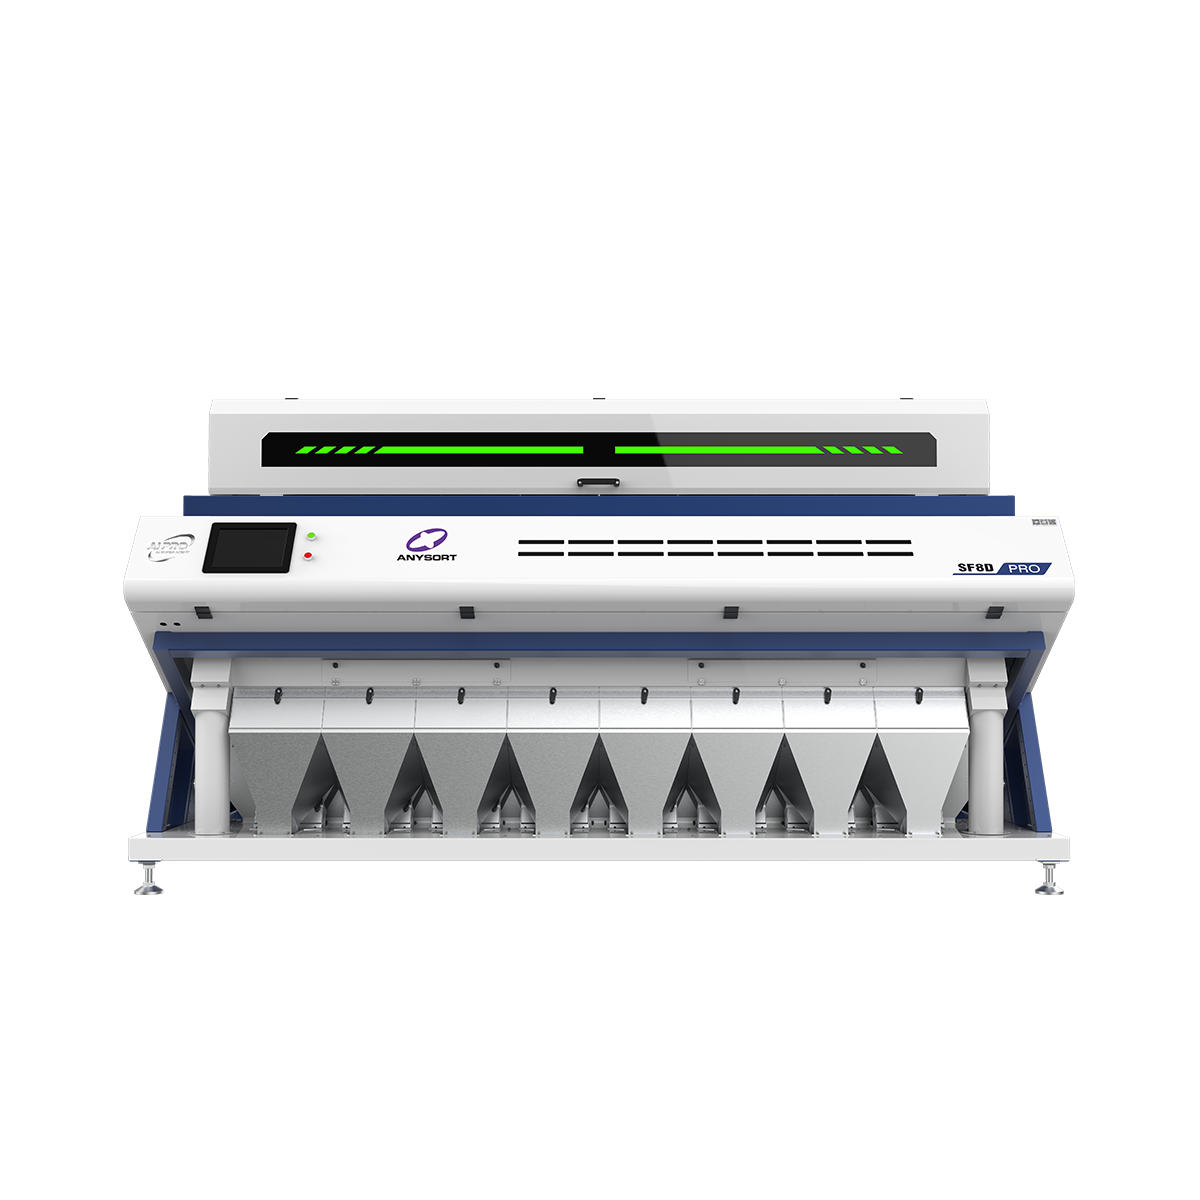
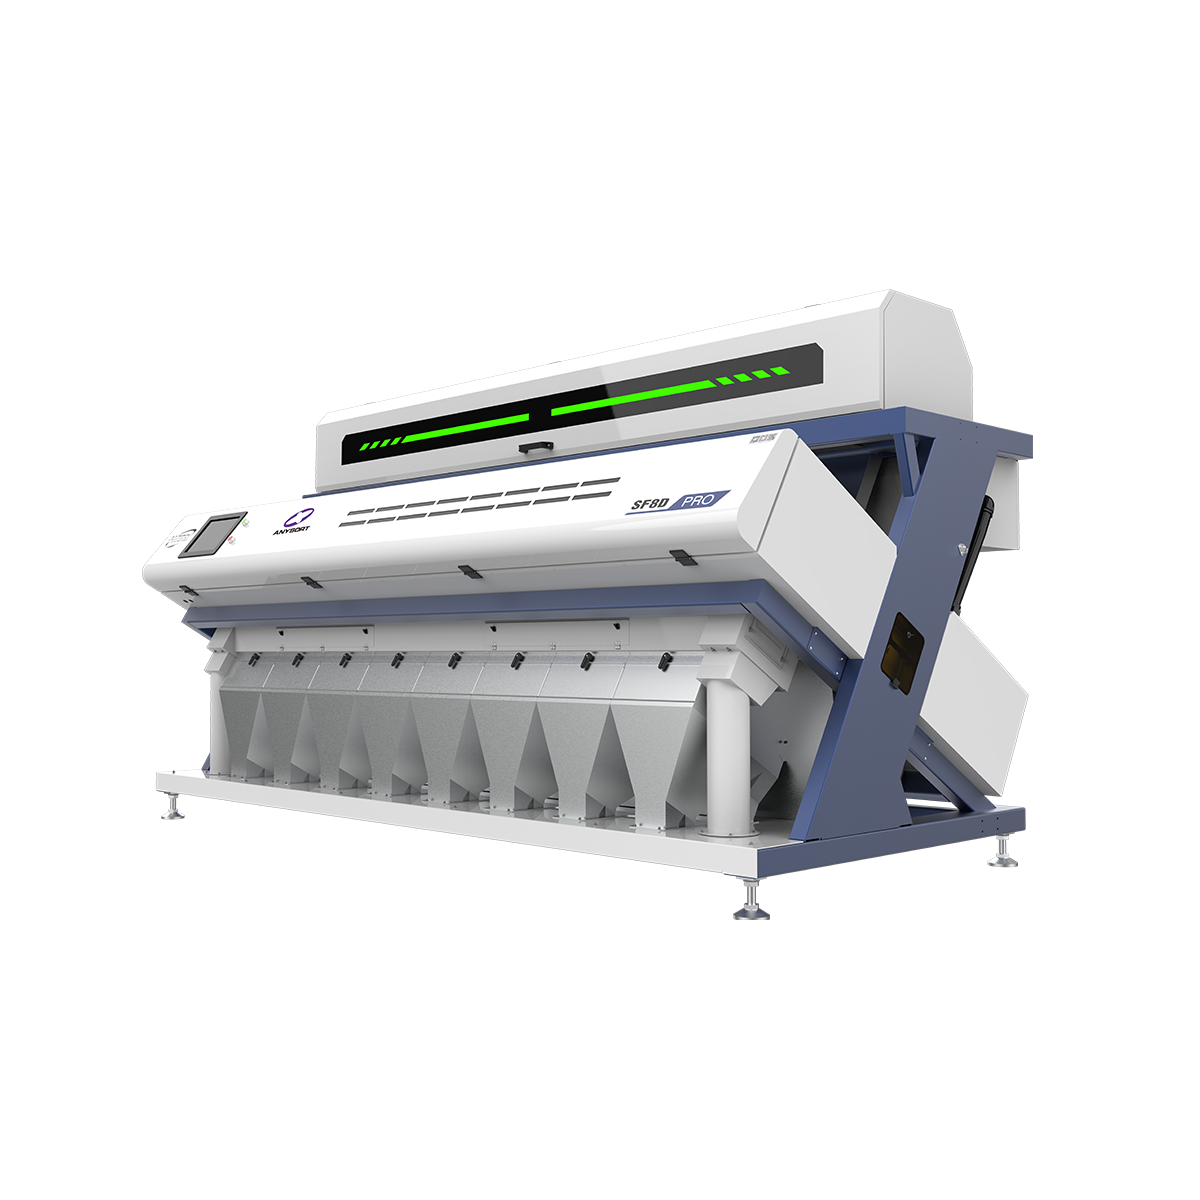
The best rice color sorter represents cutting-edge technology designed to revolutionize grain processing operations worldwide. This advanced best rice color sorter machine utilizes sophisticated optical scanning systems combined with artificial intelligence to identify and separate rice grains based on color, quality, and physical characteristics with exceptional precision. The best rice color sorter operates by capturing high-resolution images of individual rice kernels as they pass through the sorting chamber, then making instantaneous decisions to eject defective or discolored grains using compressed air jets. Modern best rice color sorter equipment incorporates multiple sensor technologies including RGB cameras and infrared detection to ensure comprehensive quality assessment. The primary functions include removing discolored rice, broken kernels, foreign materials, and damaged grains that compromise final product quality. A professional best rice color sorter can process up to fifteen tons of rice per hour while maintaining accuracy rates exceeding ninety-nine percent. These machines feature user-friendly interfaces with touchscreen controls, allowing operators to adjust sorting parameters quickly. The best rice color sorter technology finds widespread application in rice mills, food processing facilities, and export operations where quality standards demand perfection. Industries utilizing best rice color sorter systems benefit from reduced manual labor, improved product consistency, and enhanced market competitiveness. The machine's robust construction ensures reliability across continuous-duty operations, making it an essential investment for businesses prioritizing quality assurance and operational efficiency in rice processing.

 EN