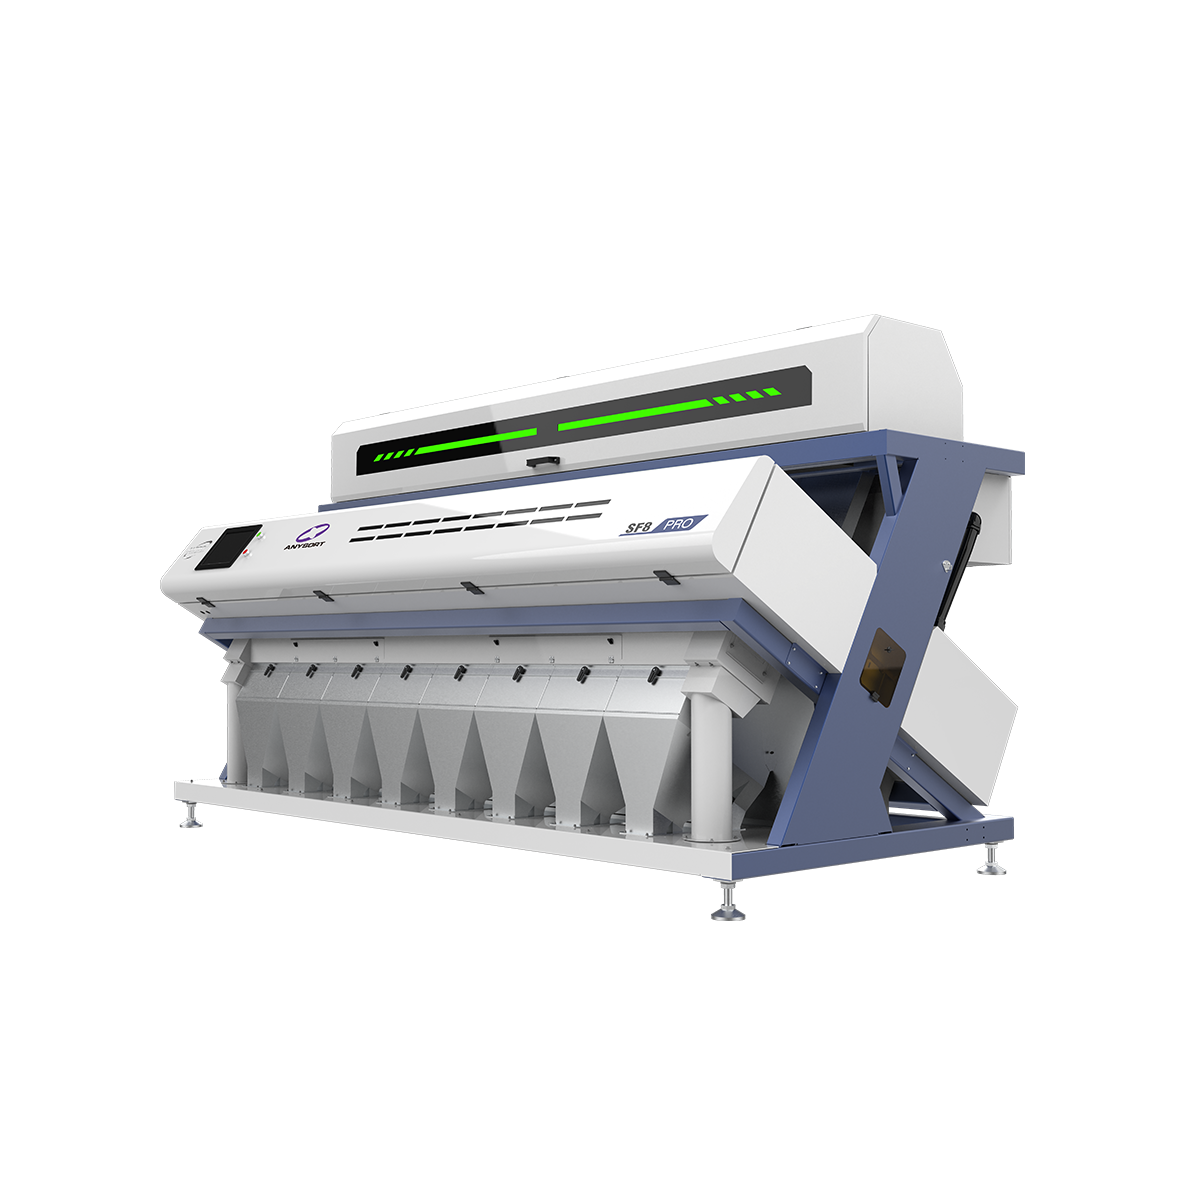
industrial sorting machine
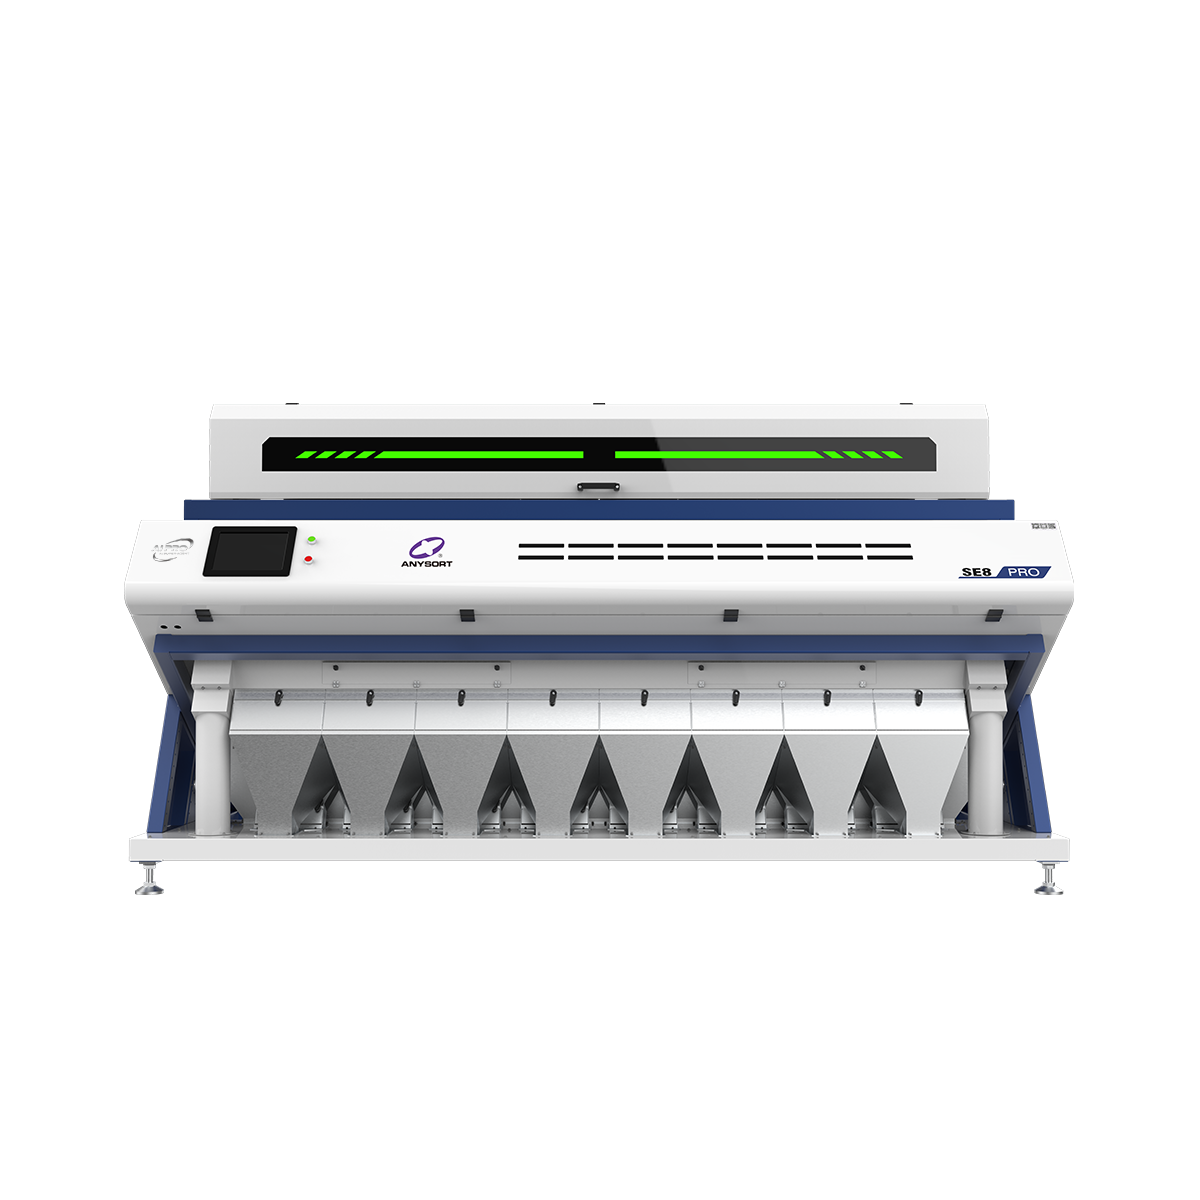
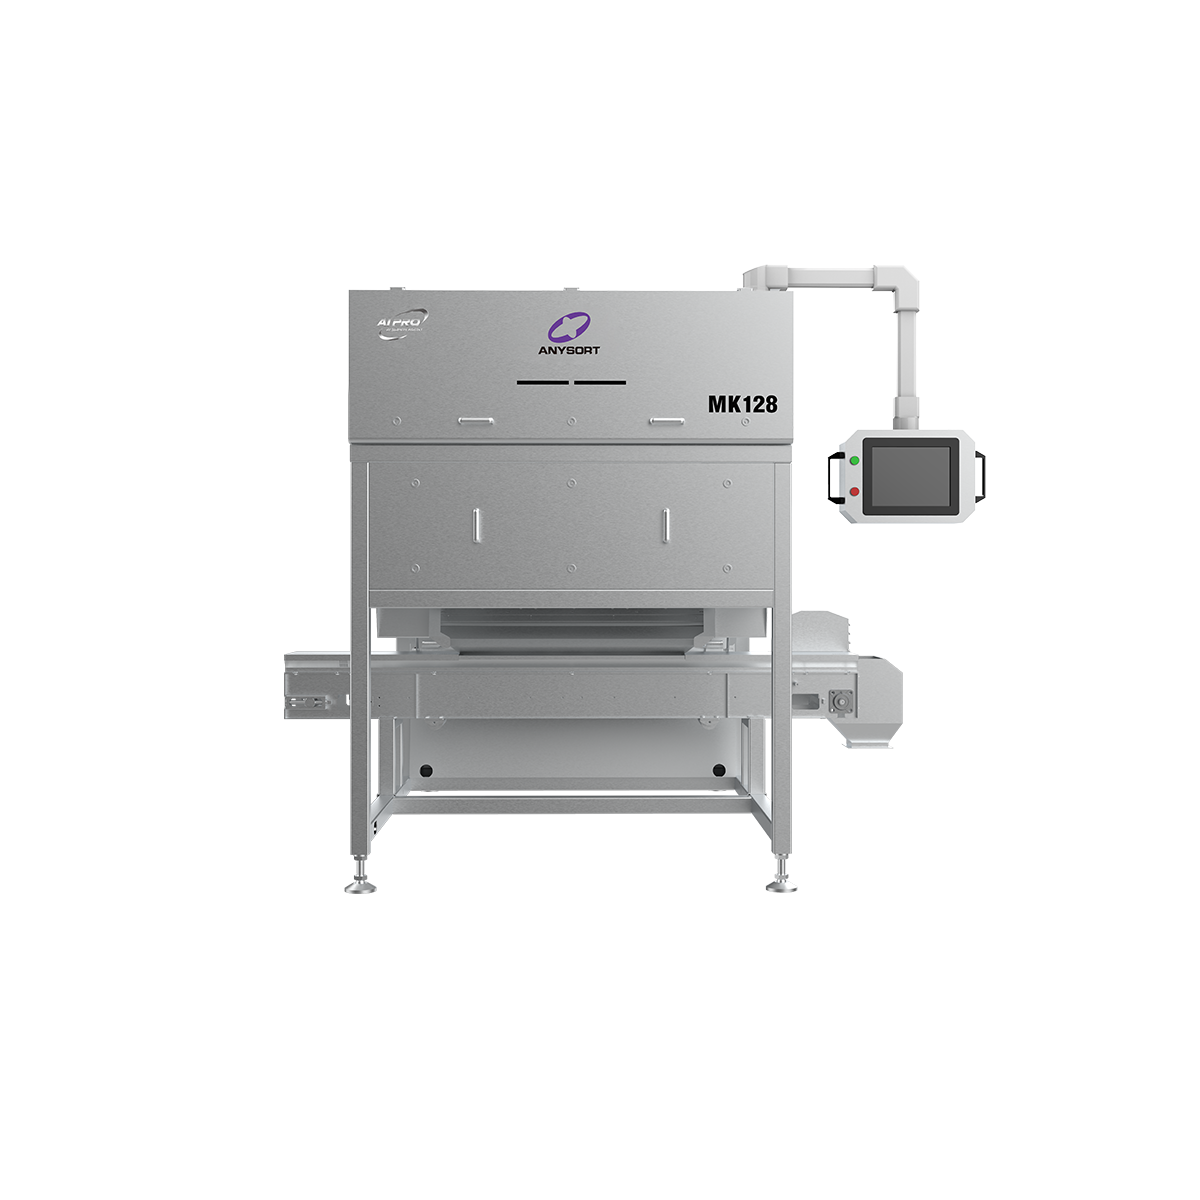
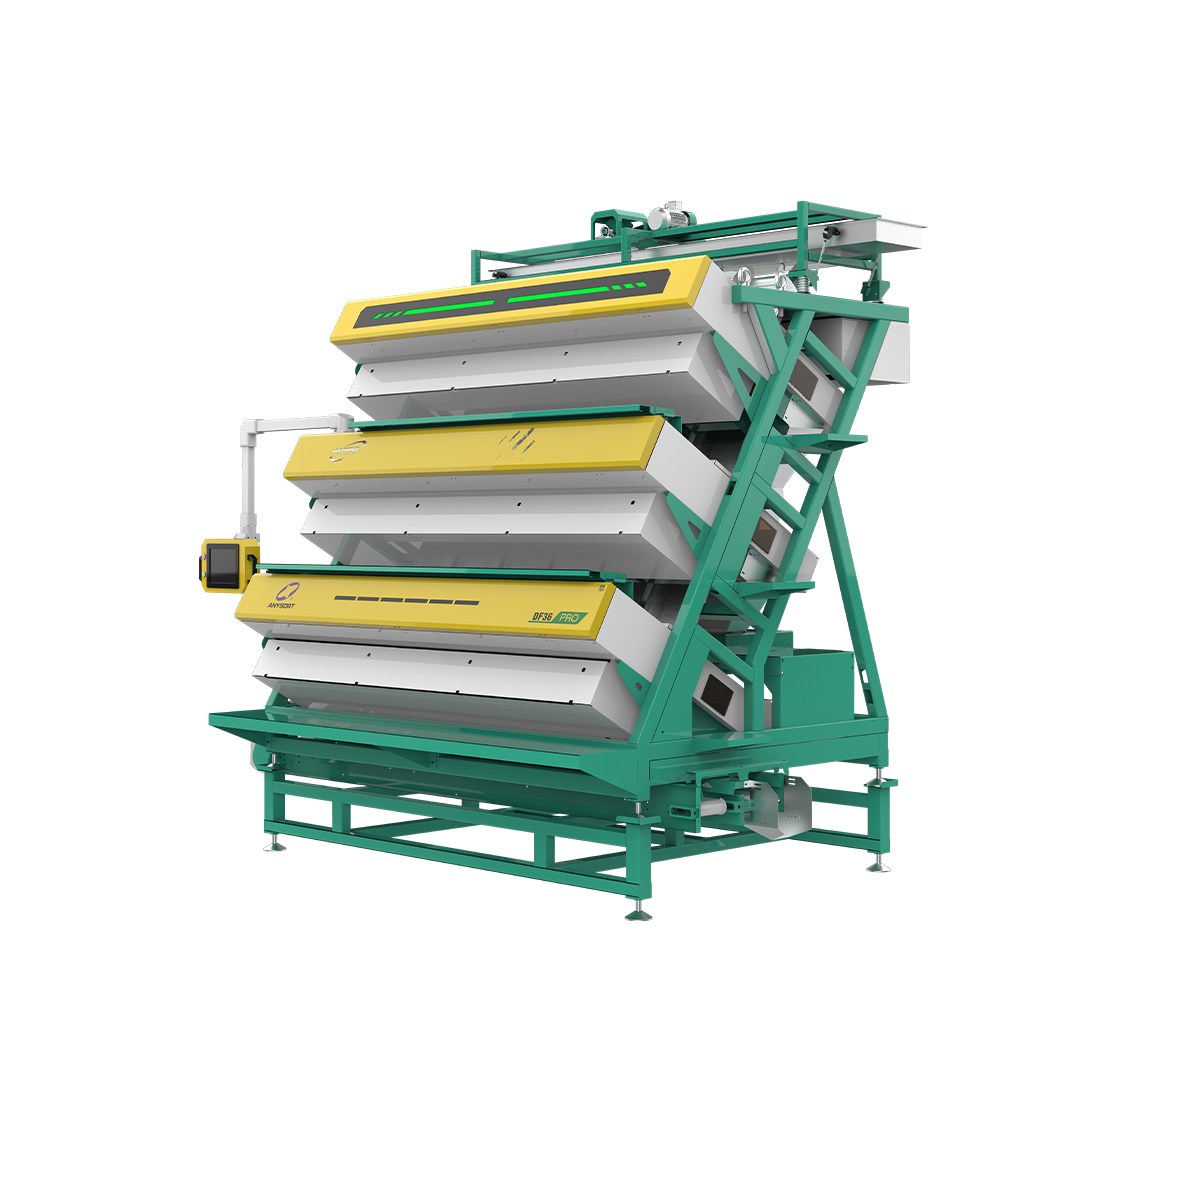
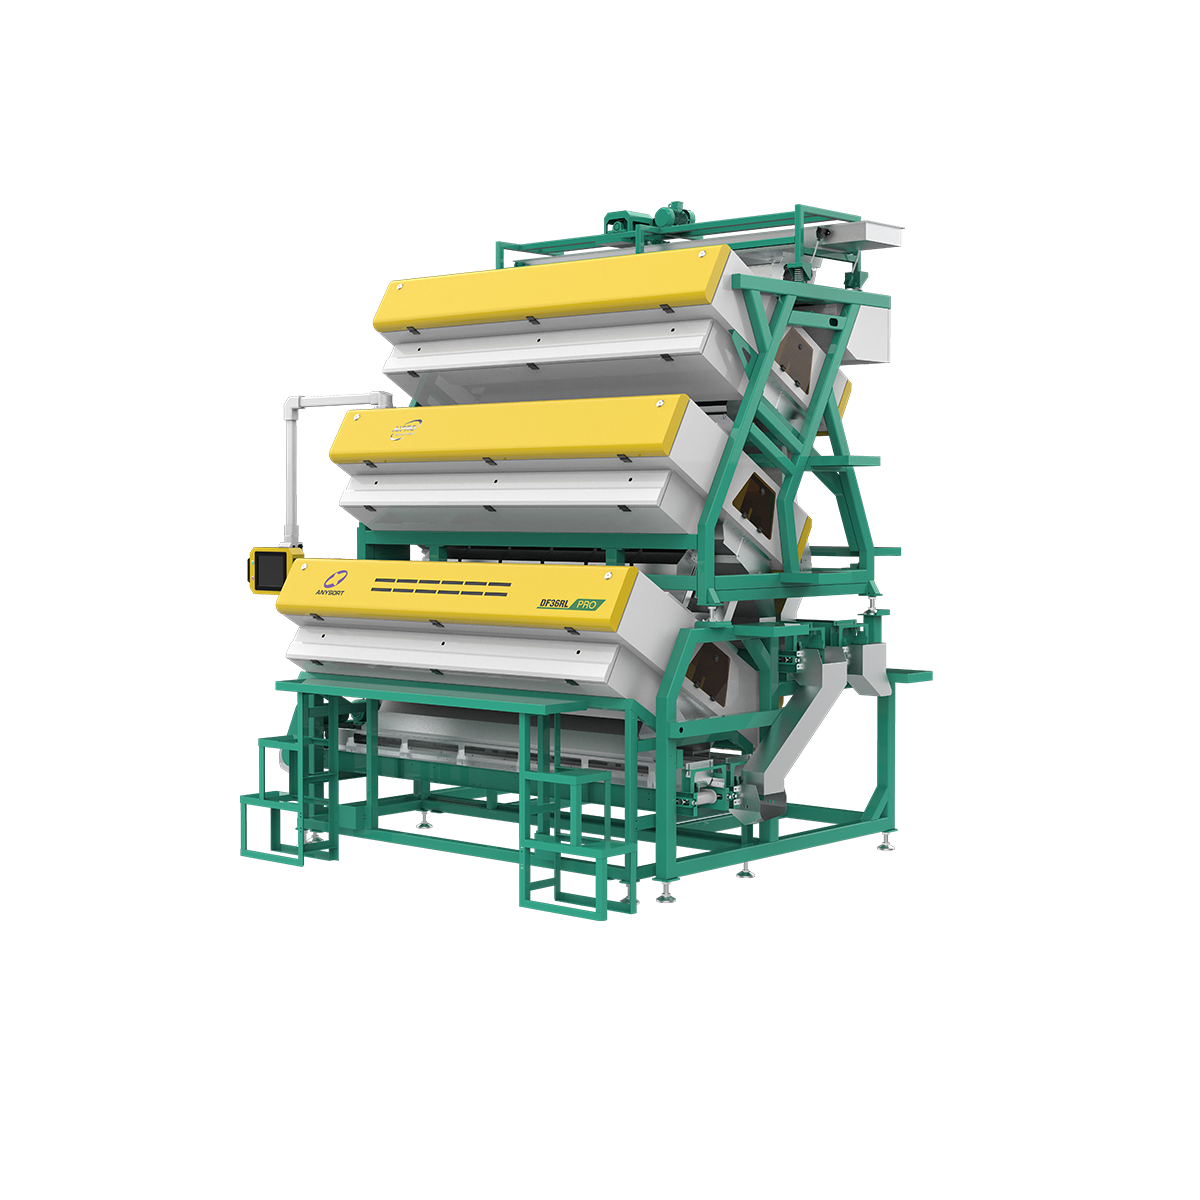
An industrial sorting machine is a sophisticated automated system designed to classify, separate, and organize materials based on specific criteria such as size, weight, color, density, or composition. These machines represent a critical advancement in modern manufacturing and processing operations across multiple industries. The industrial sorting machine utilizes cutting-edge sensor technology, including optical cameras, infrared detectors, and weight sensors, to identify and categorize items with exceptional precision and speed. Modern industrial sorting machines can process thousands of items per hour, dramatically improving operational efficiency compared to manual sorting methods. The technology behind an industrial sorting machine incorporates artificial intelligence and machine learning algorithms that enable continuous improvement and adaptation to various material types. These machines feature robust construction materials designed to withstand harsh industrial environments while maintaining consistent performance. An industrial sorting machine typically includes multiple discharge chutes or collection bins that direct sorted materials to designated locations. The system operates through a conveyor belt mechanism that moves materials past detection sensors, which analyze each item in milliseconds. Applications for the industrial sorting machine span across recycling facilities, food processing plants, mining operations, pharmaceutical manufacturing, and agricultural processing. The versatility of an industrial sorting machine makes it an indispensable tool for businesses seeking to maximize productivity and minimize waste. Installation of an industrial sorting machine requires minimal operational training, as most systems feature intuitive control interfaces and automated operation modes. The investment in an industrial sorting machine typically yields rapid return on investment through reduced labor costs and increased throughput.

 EN