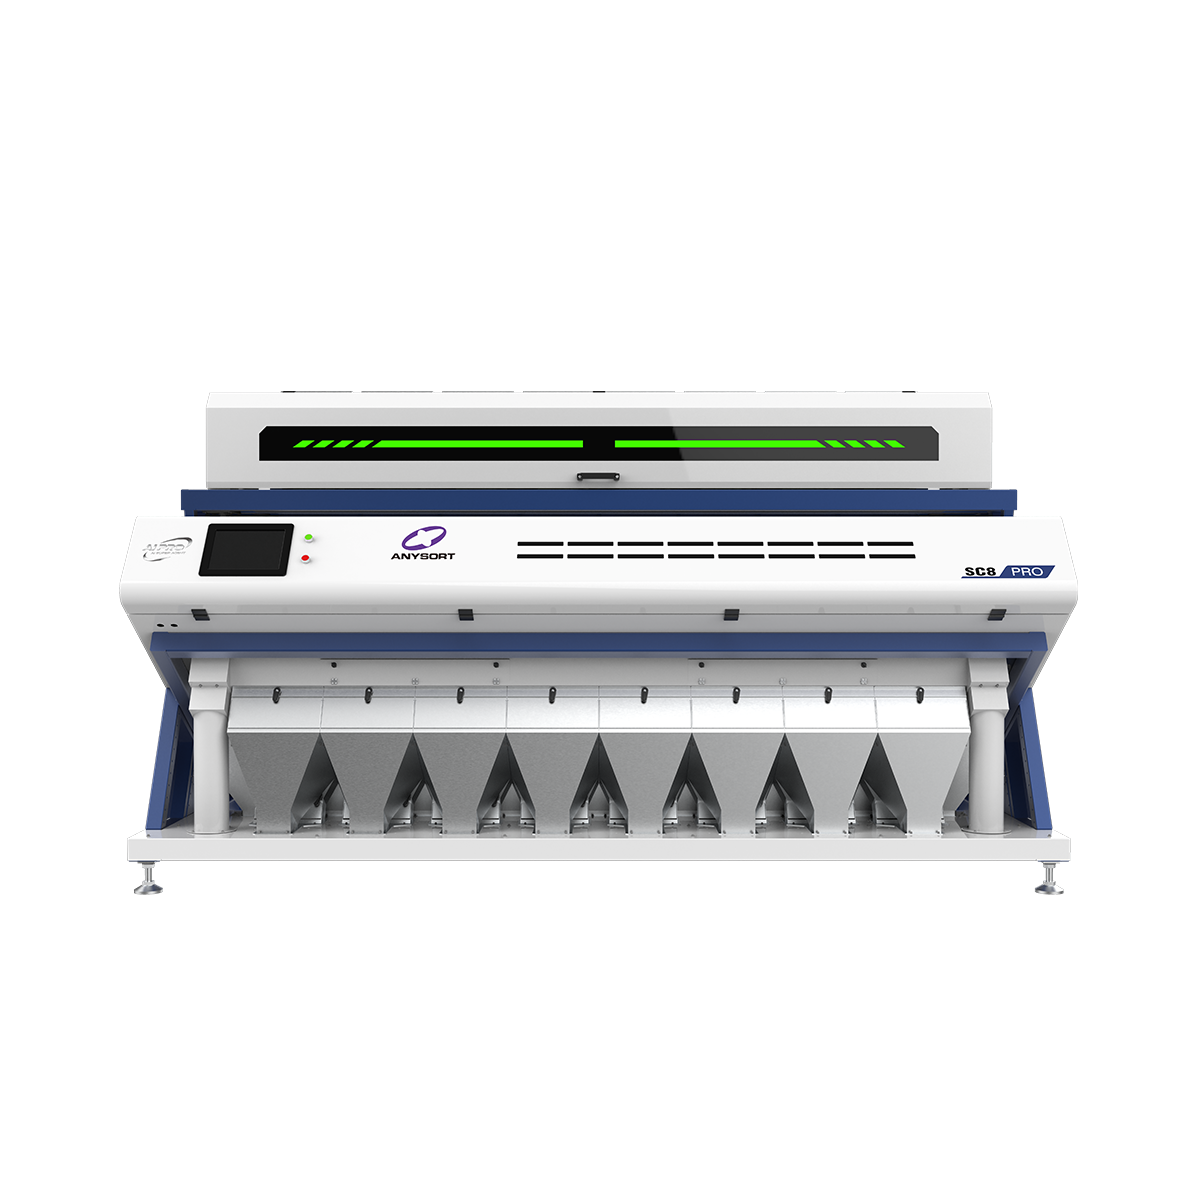
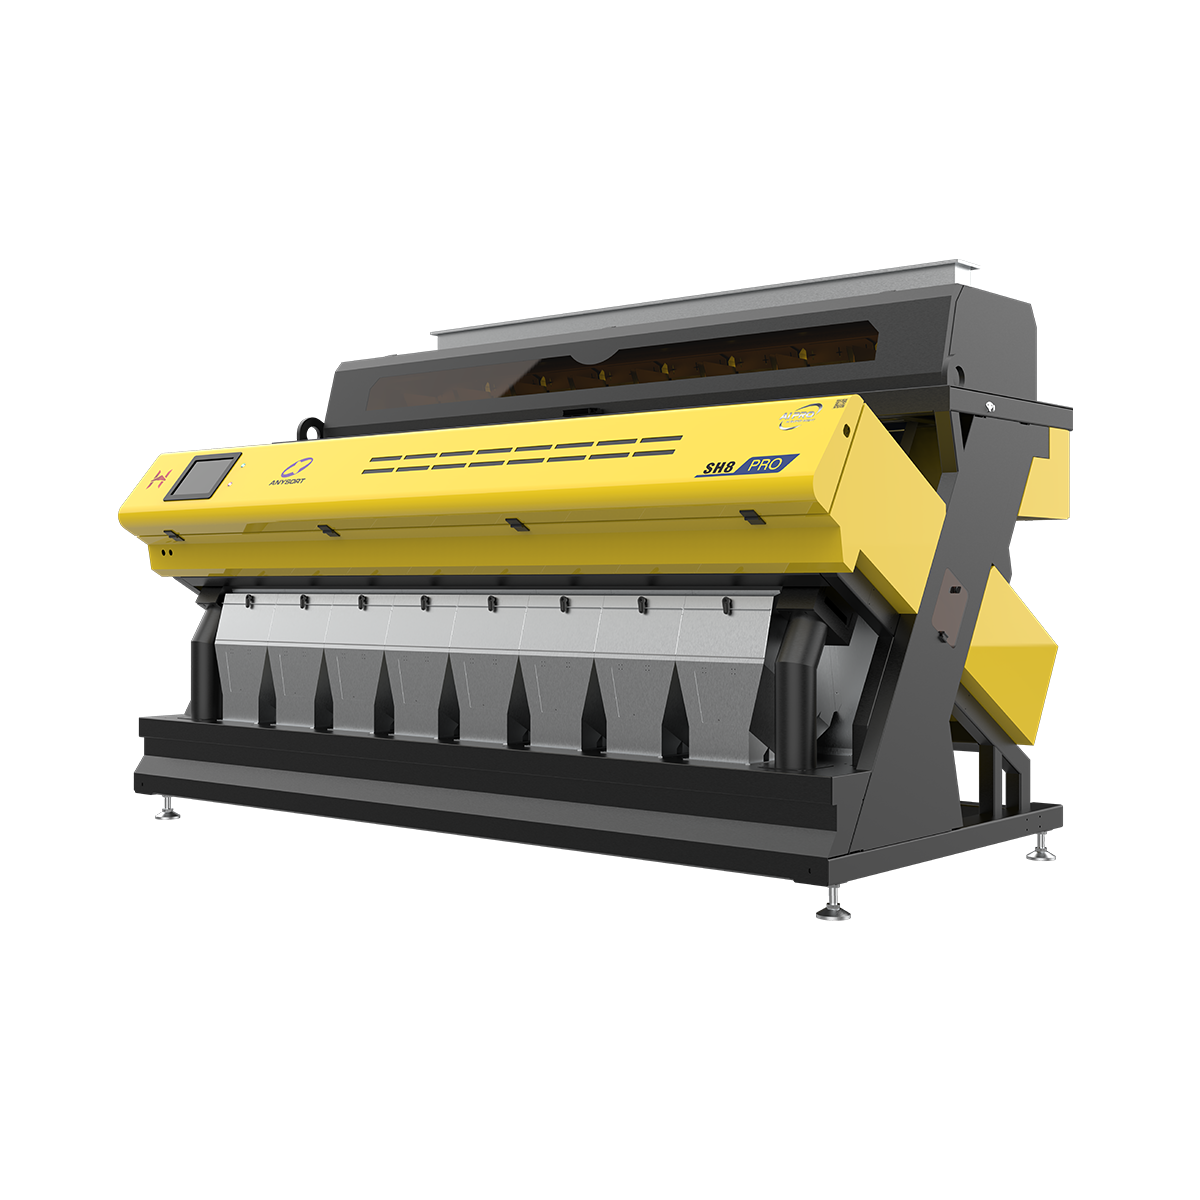
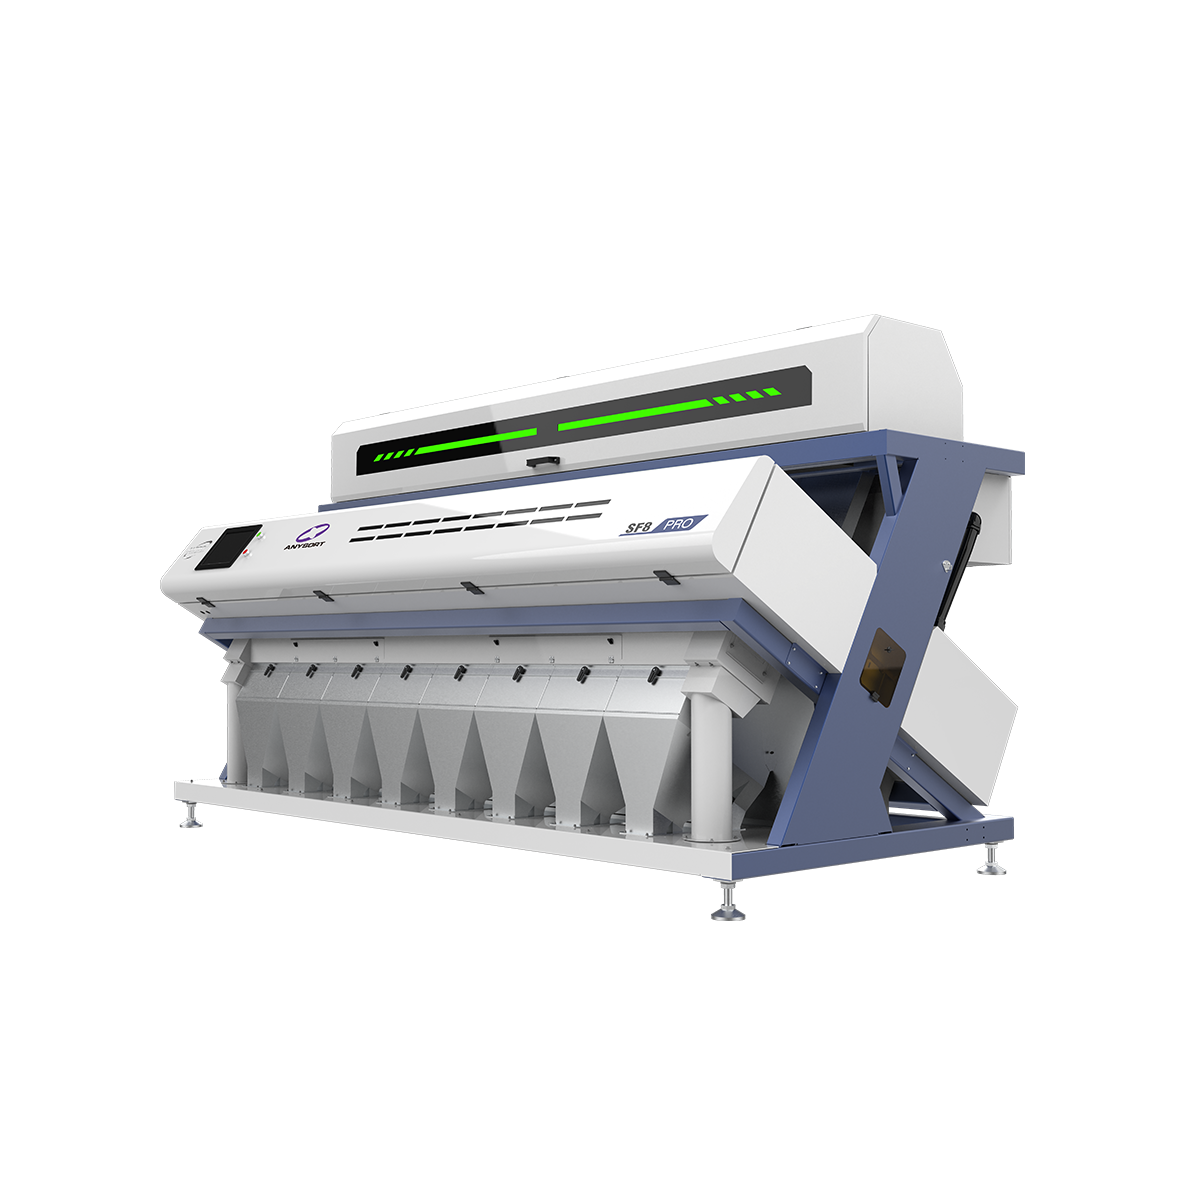
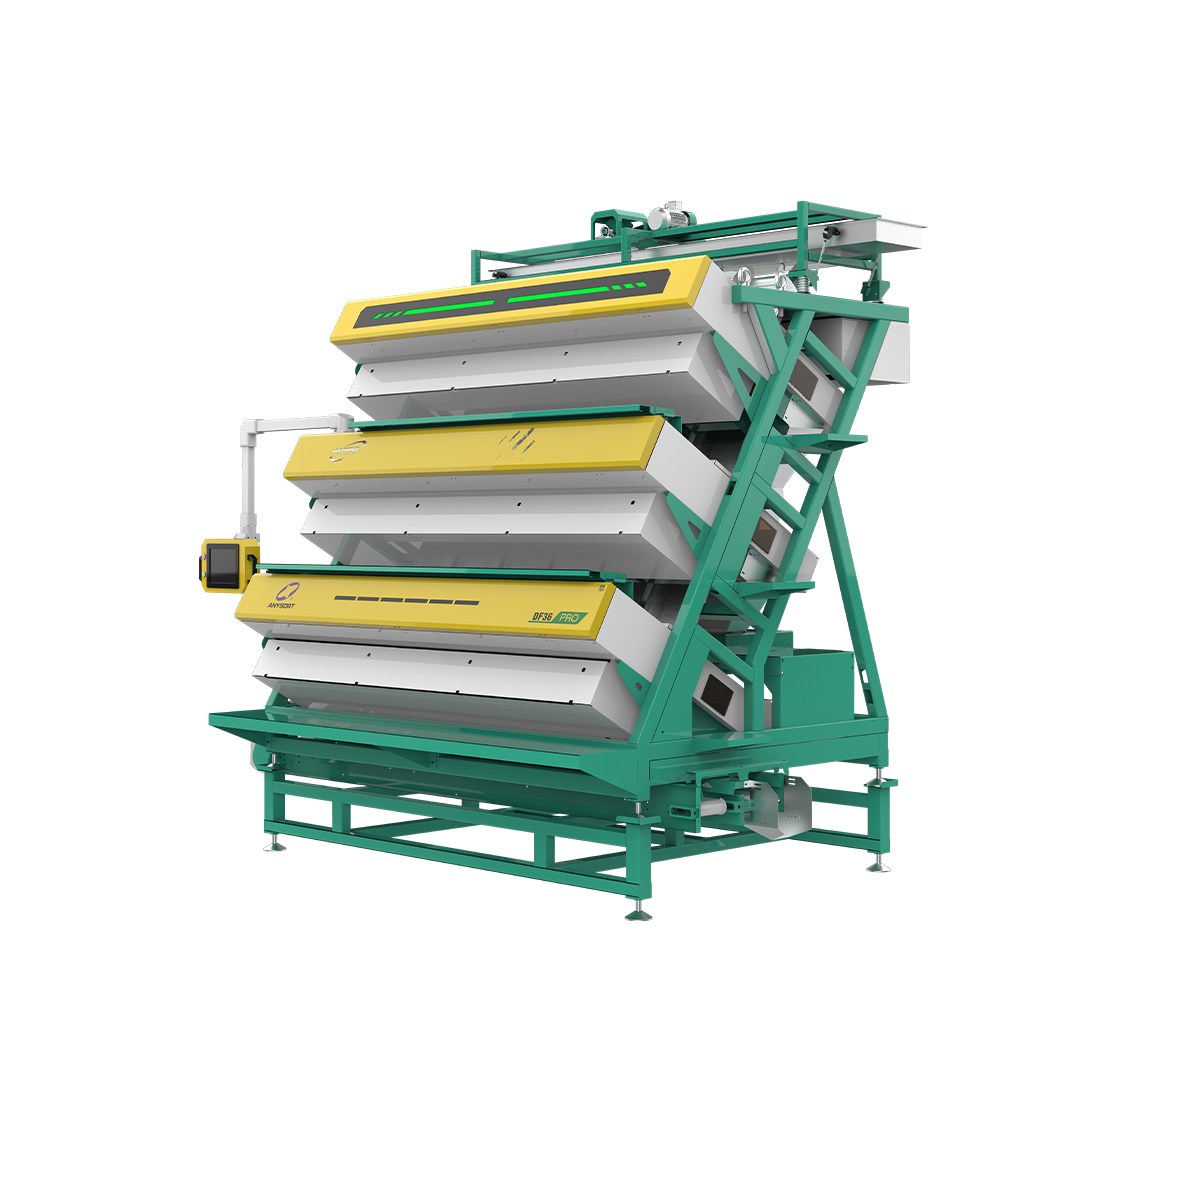
colour separator machine
A colour separator machine is a sophisticated industrial device designed to automatically sort, separate, and classify materials based on their color characteristics. This advanced technology uses optical sensors and intelligent algorithms to identify and categorize items with precision, making it an essential tool across numerous industries. The colour separator machine operates by scanning each item as it passes through the detection zone, analyzing its color properties, and directing it to the appropriate output channel using pneumatic or mechanical systems.
The technological features of a colour separator machine include high-resolution cameras, LED lighting systems, and real-time image processing capabilities. These components work together to ensure accurate color detection even under varying lighting conditions. Modern colour separator machines incorporate artificial intelligence and machine learning to continuously improve sorting accuracy and adapt to different material types.
Applications for the colour separator machine span multiple sectors, including food processing, recycling, agriculture, pharmaceuticals, and manufacturing. In the food industry, these machines separate grains, nuts, and beans by removing discolored or defective items. The colour separator machine proves invaluable in recycling operations, where it efficiently sorts plastic, glass, and other materials by color. Agricultural operations utilize colour separator machines to enhance crop quality by removing damaged or unsuitable produce. The versatility and reliability of colour separator machines make them indispensable for businesses seeking to improve product quality, increase throughput, and maintain competitive advantages in their respective markets.

 EN