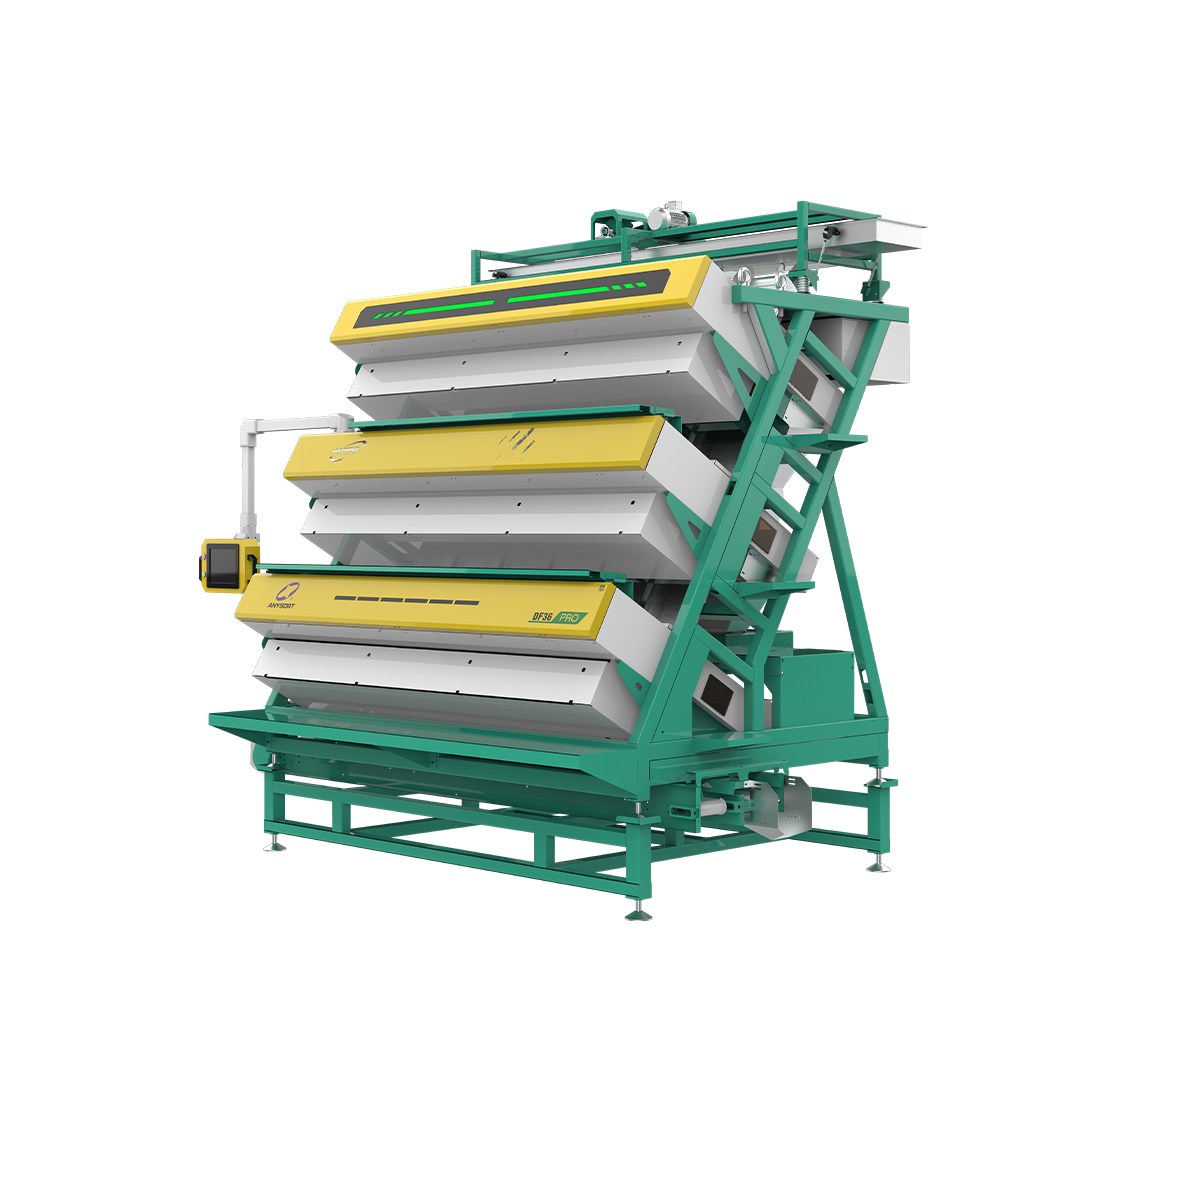
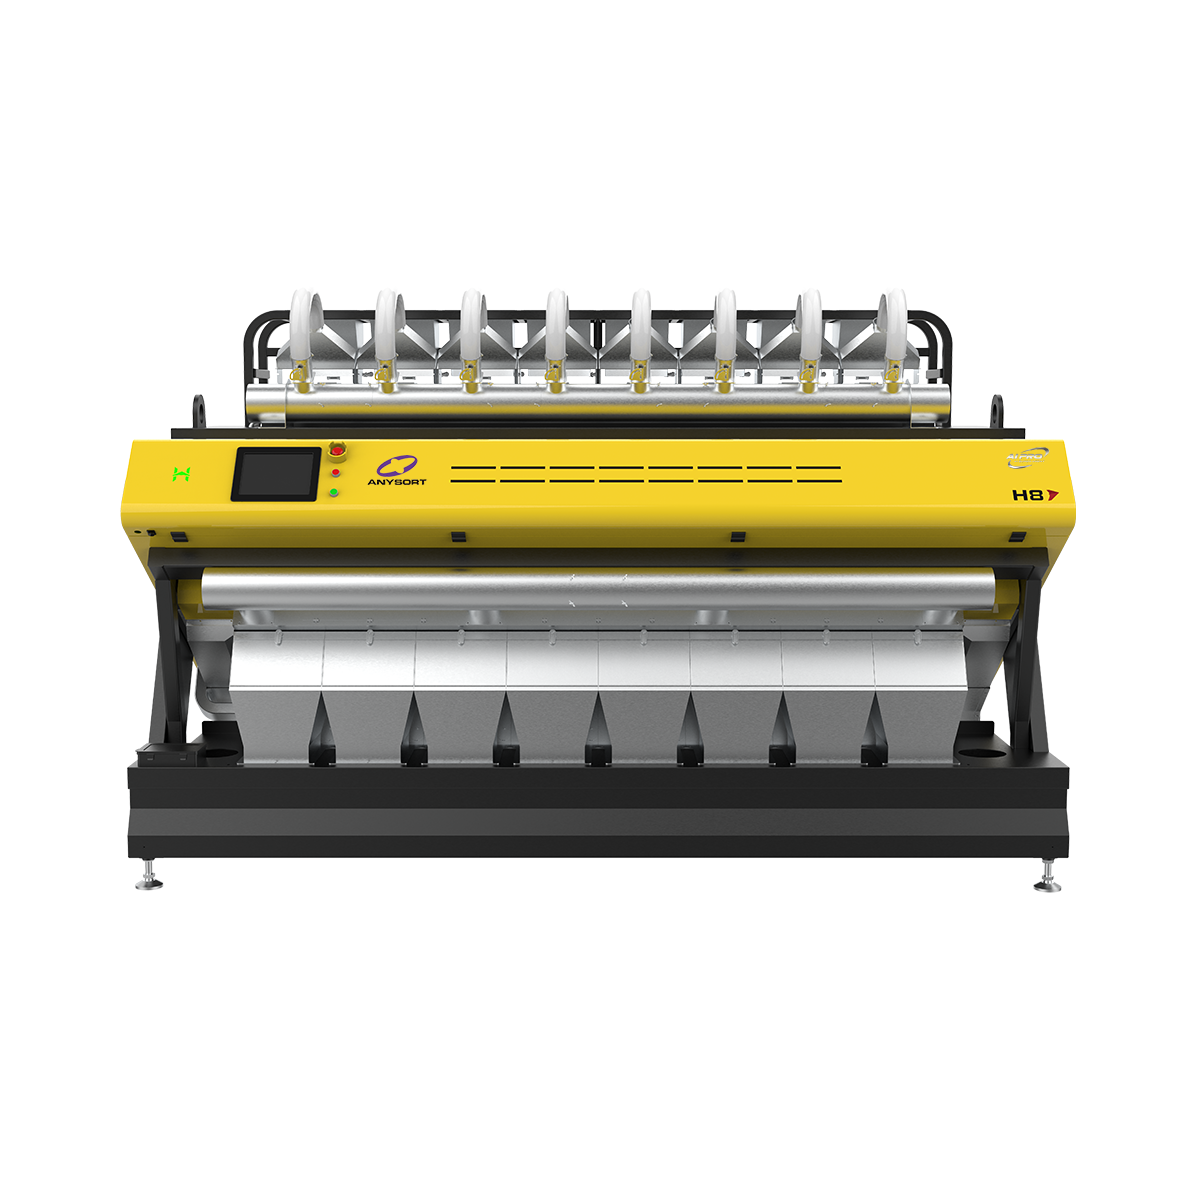
cashew sorting machine
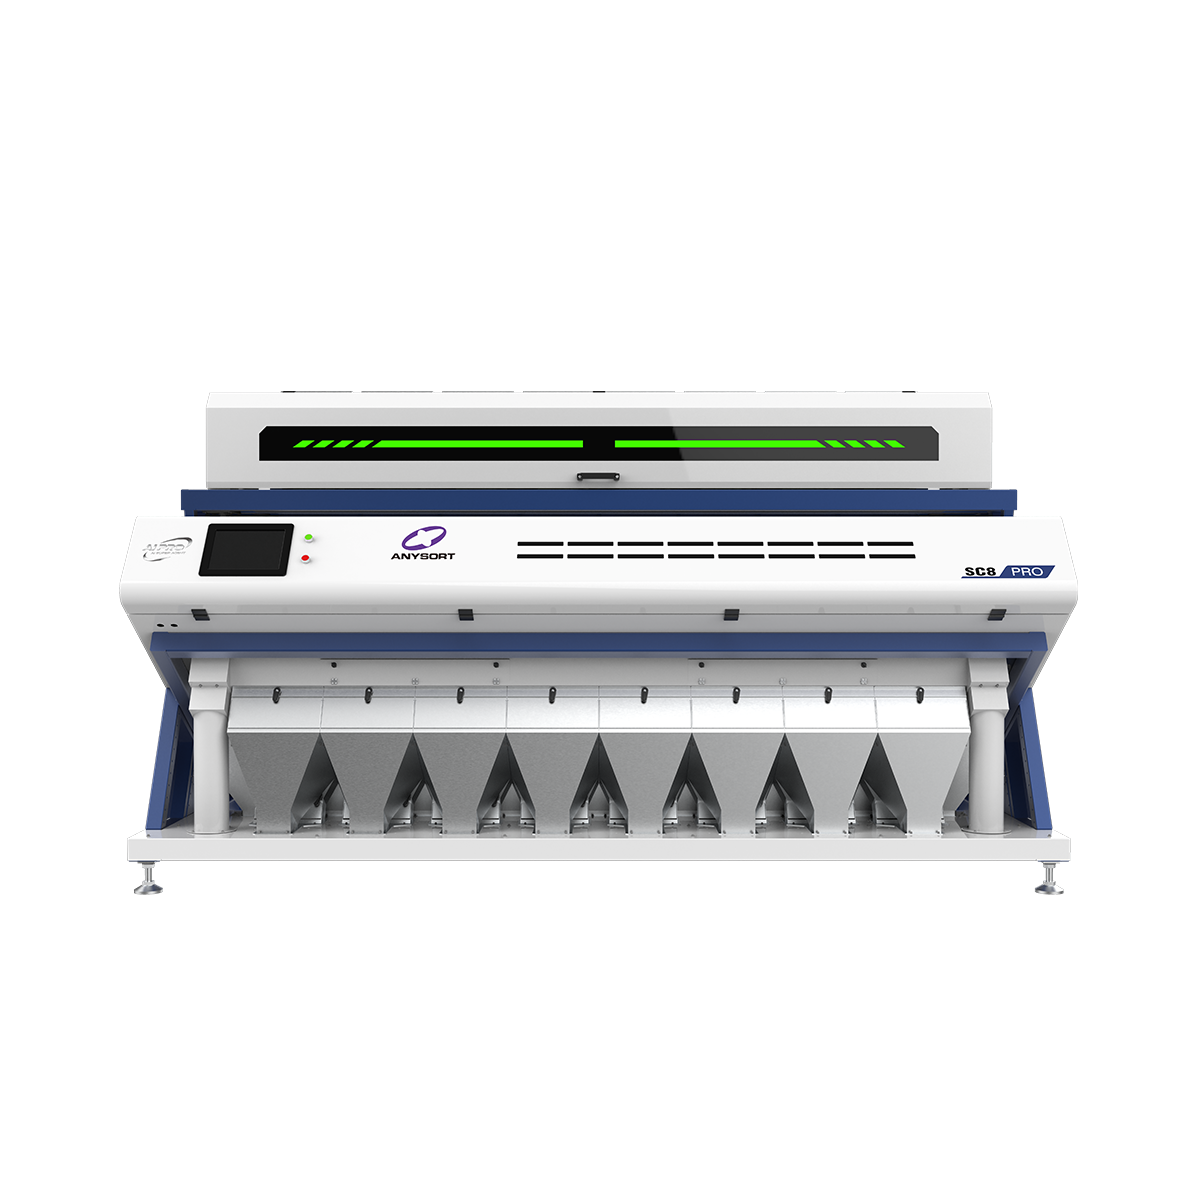
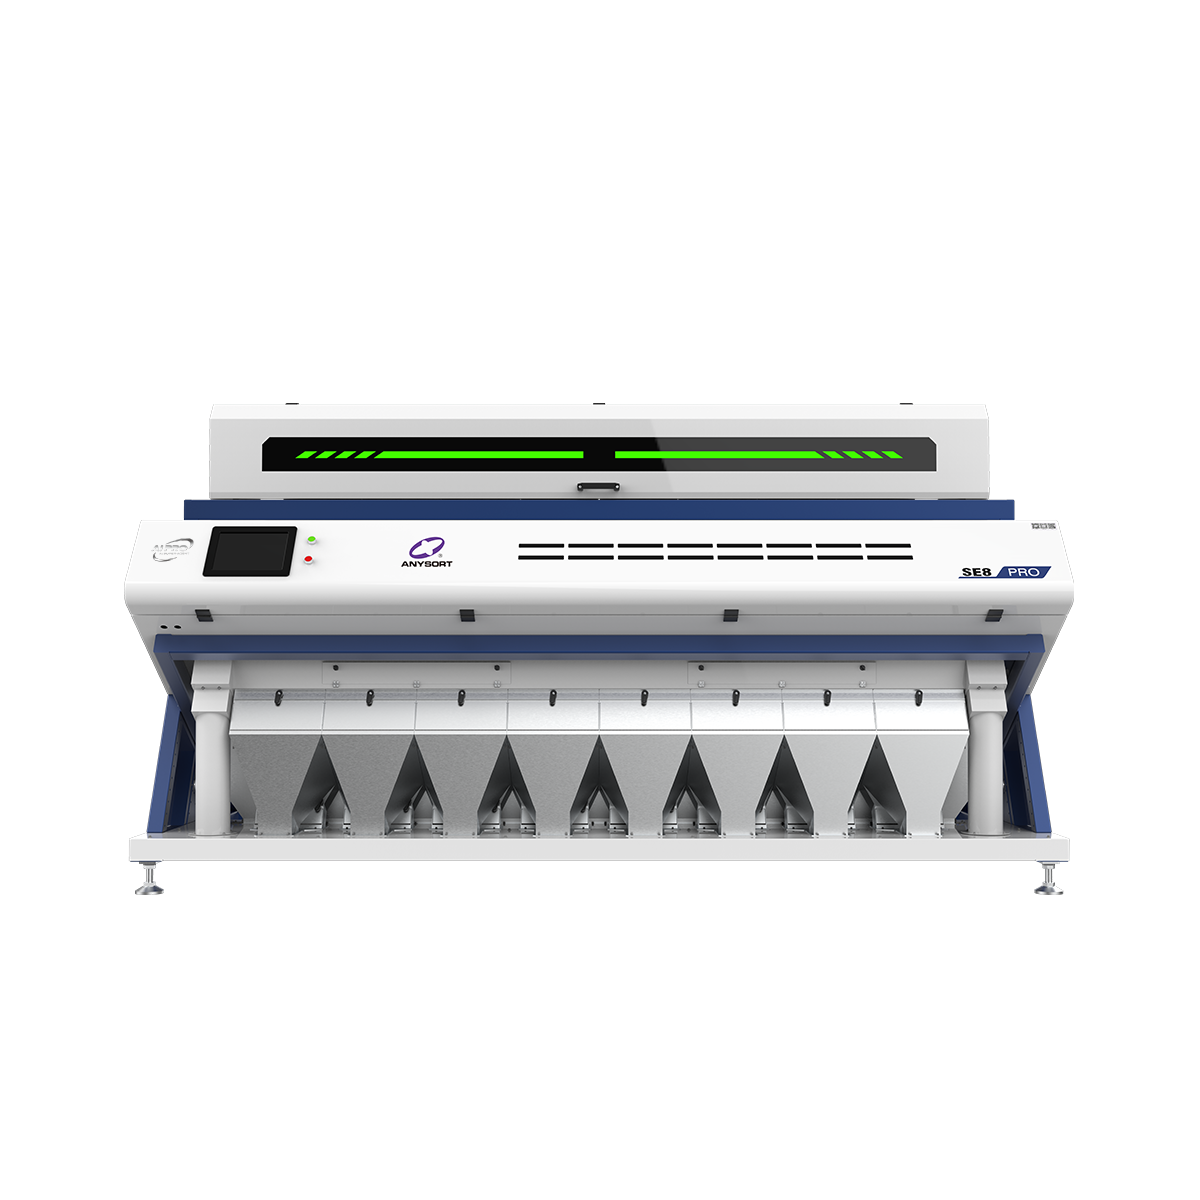
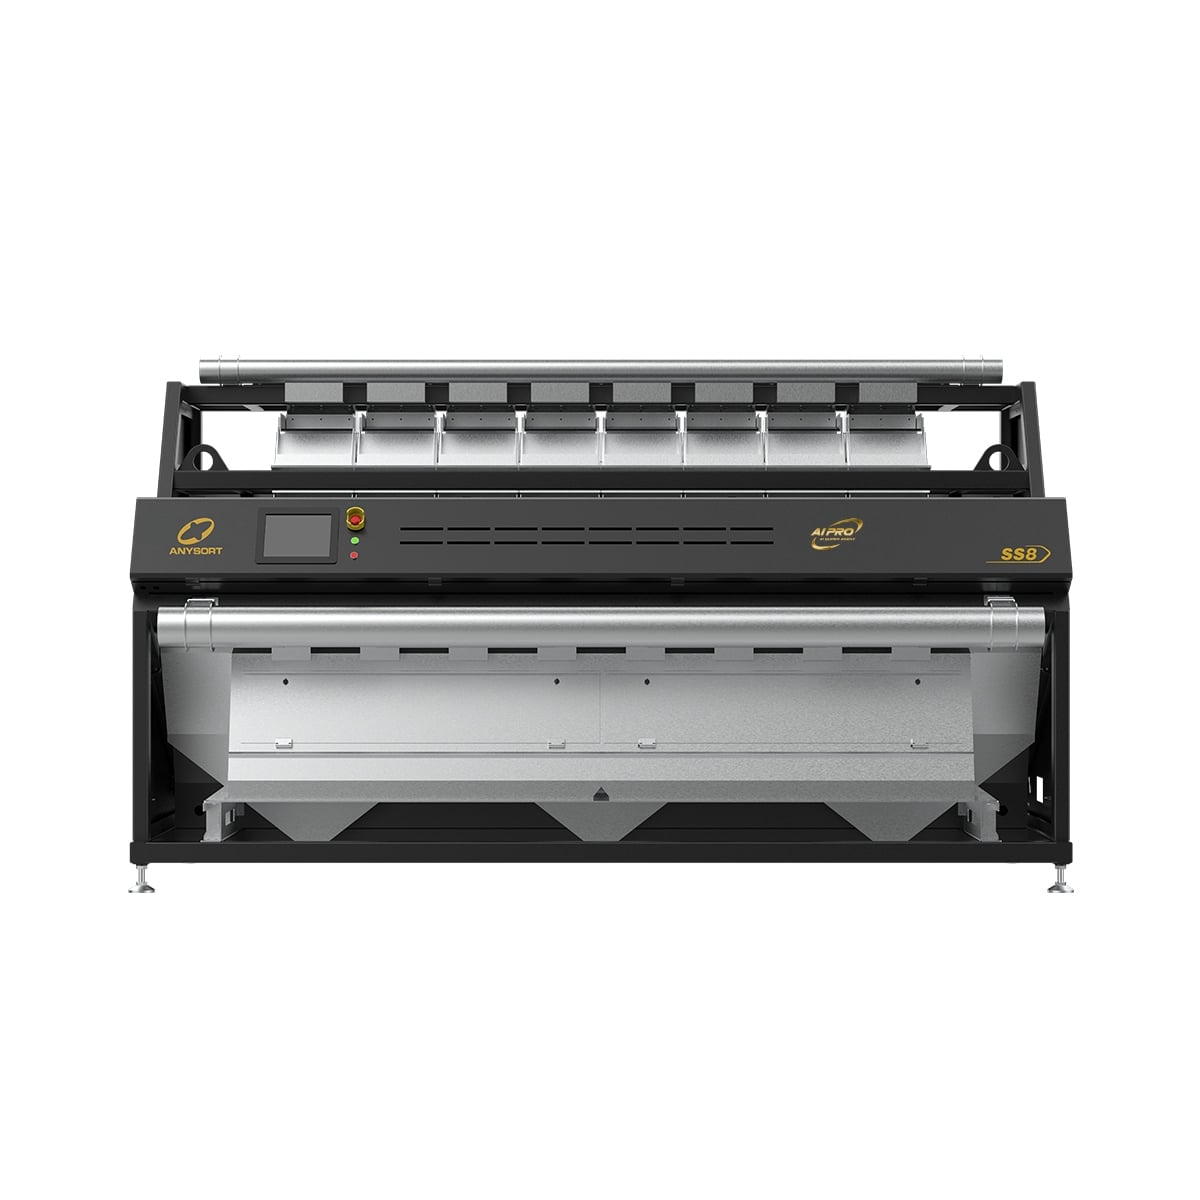
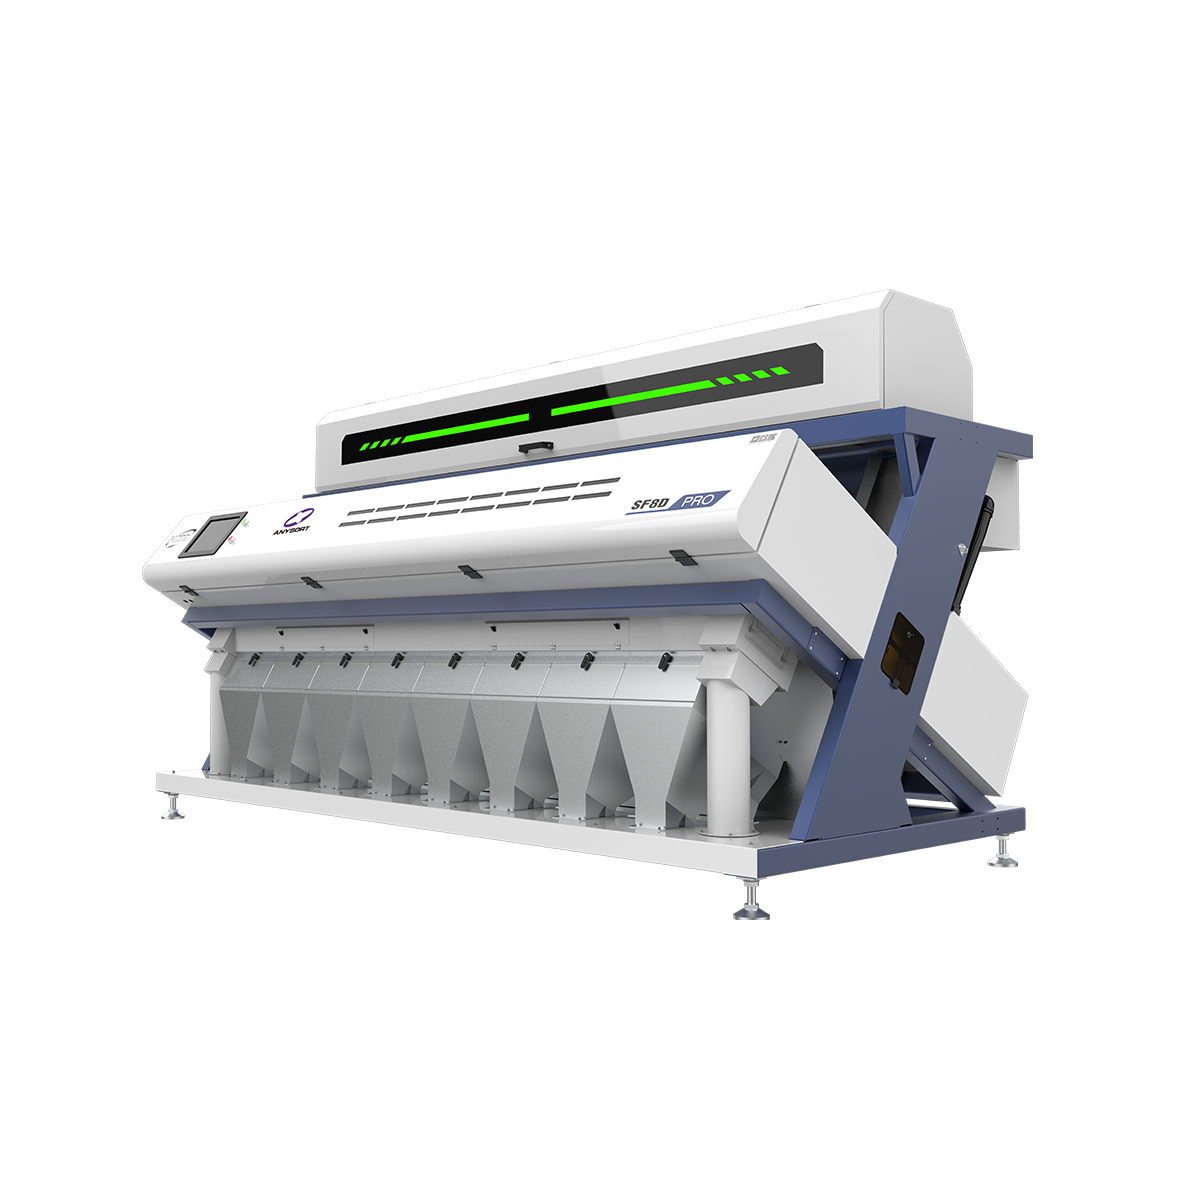
A cashew sorting machine is an advanced piece of equipment designed to automatically organize cashews by size, quality, and weight with precision and efficiency. This innovative cashew sorting machine utilizes cutting-edge sensor technology and sophisticated algorithms to evaluate each cashew individually, ensuring consistent sorting results. The primary function of a cashew sorting machine is to separate raw and roasted cashews into distinct grades, removing defective nuts and foreign materials in the process.
Modern cashew sorting machines incorporate optical sensors, weight detection systems, and artificial intelligence to achieve exceptional accuracy rates exceeding 99 percent. These machines can process hundreds of kilograms of cashews per hour, dramatically increasing productivity compared to manual sorting methods. The cashew sorting machine operates through a combination of conveyor belts, rotating discs, and ejection mechanisms that work seamlessly together.
Applications for a cashew sorting machine extend across multiple sectors, including food processing facilities, agricultural operations, and export companies. Whether handling large-scale commercial operations or specialized sorting requirements, the cashew sorting machine adapts to various production demands. The technology behind modern cashew sorting machines continues to evolve, incorporating machine learning capabilities that improve accuracy over time. These systems integrate easily into existing production lines, offering manufacturers a reliable solution for quality control and standardization in cashew processing operations.

 EN