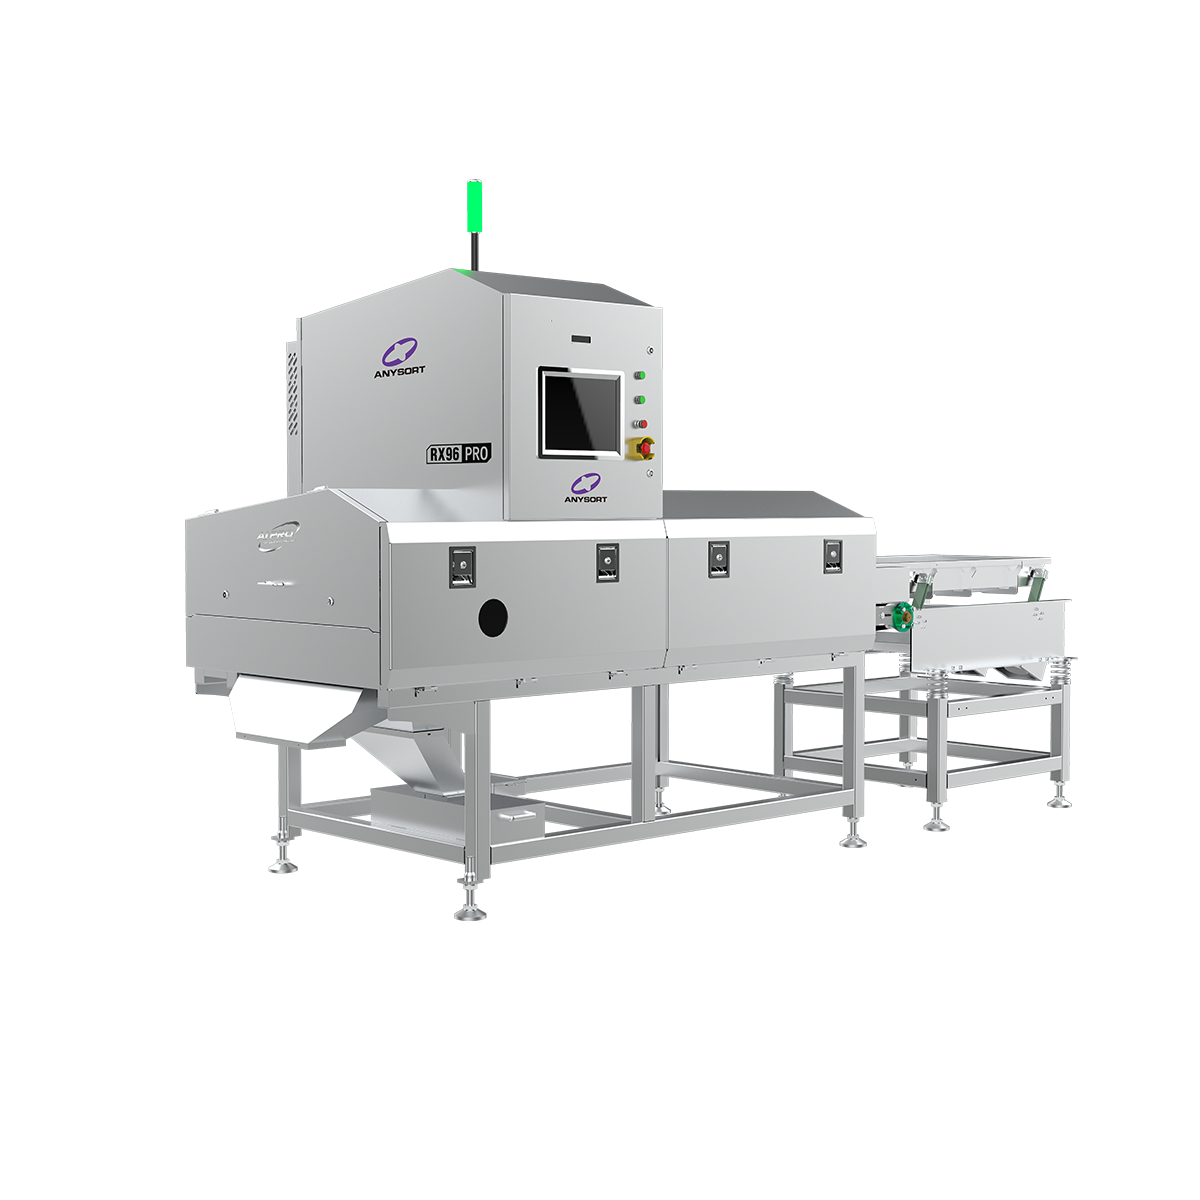
PET Bottle Recycling Machine | Plastic Waste Solutions

All Categories

pet bottle recycling machine

A pet bottle recycling machine is an innovative industrial solution designed to transform plastic waste into valuable reusable materials. This advanced equipment processes used plastic bottles through a systematic approach that includes collection, sorting, cleaning, and material conversion. The pet bottle recycling machine operates by first receiving sorted plastic containers, which are then cleaned to remove labels and contaminants. The cleaned bottles pass through a shredding mechanism that cuts them into small flakes, preparing them for further processing. The technological features of a pet bottle recycling machine include automated sorting systems that use optical sensors to distinguish between different plastic types and colors. The machine incorporates high-speed shredders capable of processing hundreds of kilograms per hour, ensuring efficient production output. Advanced washing units remove adhesives and residual content, while drying systems prepare the material for granulation. The pet bottle recycling machine typically includes pelletizing equipment that transforms flakes into uniform pellets suitable for manufacturing new products. Applications for a pet bottle recycling machine span multiple industries, including plastic manufacturing, textile production, and packaging companies. Recycled PET material from these machines becomes raw material for producing new bottles, fiber fabrics, automotive components, and consumer goods. Environmental facilities and waste management centers utilize pet bottle recycling machines to process post-consumer waste responsibly. The machine supports circular economy initiatives by reducing landfill waste and decreasing demand for virgin plastic production, making it essential infrastructure for sustainable manufacturing operations worldwide.

New Products

The pet bottle recycling machine delivers substantial operational and economic benefits for businesses committed to sustainability. First, the machine dramatically reduces processing costs by automating labor-intensive recycling tasks that traditionally required significant human intervention. Operators can process larger quantities of plastic waste with minimal staffing, directly improving profit margins and operational efficiency. Second, a pet bottle recycling machine enables companies to generate revenue streams from waste materials. Recycled PET pellets command market value, transforming what was previously considered waste into sellable products. This revenue potential makes waste management financially attractive rather than purely cost-driven. Third, businesses using pet bottle recycling machines demonstrate environmental responsibility, enhancing their corporate image and attracting environmentally conscious consumers and partners. Fourth, the technology provides consistent material quality through standardized processing parameters. The pet bottle recycling machine ensures uniform pellet sizes and properties, meeting specifications required by downstream manufacturers. This reliability reduces production complications for companies purchasing recycled materials. Fifth, implementing a pet bottle recycling machine reduces dependency on virgin plastic sourcing, providing supply chain resilience and price stability. As virgin plastic costs fluctuate based on crude oil prices, recycled alternatives offer predictable pricing. Sixth, the machine supports regulatory compliance with environmental legislation increasingly mandating plastic waste reduction and recycling targets. Facilities with pet bottle recycling machines easily meet compliance requirements while avoiding potential fines. Seventh, the operation generates positive community relations by visibly addressing plastic waste challenges. Companies demonstrating commitment to recycling attract partnerships with eco-conscious organizations and government agencies offering incentives for waste reduction initiatives.

Latest News

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

pet bottle recycling machine

Advanced Automated Sorting and Processing Capability

Advanced Automated Sorting and Processing Capability

The pet bottle recycling machine features state-of-the-art automated sorting technology that efficiently separates different plastic types and colors without manual intervention. Optical sensor systems analyze each bottle in real-time, directing materials to appropriate processing lanes based on composition and characteristics. This intelligent categorization ensures high-purity material output essential for premium recycled products. The pet bottle recycling machine can simultaneously process multiple plastic grades, maximizing throughput while maintaining quality standards. Automated processing eliminates human sorting errors that compromise final product quality, ensuring consistency that manufacturers demand. The machine's continuous operation capability means facilities achieve remarkable productivity rates, processing tons of material daily. This sophisticated automation transforms recycling from a labor-intensive operation into an efficient, scalable solution perfect for large-scale waste management facilities.
High-Capacity Material Conversion with Quality Assurance

High-Capacity Material Conversion with Quality Assurance

A modern pet bottle recycling machine converts processed plastic into uniform pellets through integrated granulation systems that guarantee consistent product specifications. The machine combines washing, drying, and pelletizing functions within a single integrated unit, streamlining the entire conversion process. High-capacity shredders handle substantial material volumes, cutting cleaned flakes into ideal particle sizes for granulation. The pet bottle recycling machine maintains precise temperature and moisture controls throughout processing, producing pellets with reliable melting points and flow characteristics. Quality assurance mechanisms include automated testing that verifies pellet properties before discharge, rejecting substandard material. This commitment to quality ensures downstream manufacturers receive dependable raw materials suitable for demanding applications. The machine's capacity to deliver superior recycled PET pellets makes it invaluable for industries requiring stringent material specifications.
Sustainable Environmental Impact and Economic Return

Sustainable Environmental Impact and Economic Return

Implementing a pet bottle recycling machine directly addresses critical environmental challenges while generating measurable economic returns. Each unit processes hundreds of tons of plastic waste annually, preventing equivalent amounts from reaching landfills or oceans. The pet bottle recycling machine enables circular economy principles by converting post-consumer waste into valuable manufacturing inputs, reducing virgin plastic demand significantly. Environmental benefits include decreased energy consumption compared to virgin plastic production, reduced carbon emissions, and preserved natural resources. Economically, facilities operating a pet bottle recycling machine benefit from tipping fees on incoming waste materials and revenue generated from selling recycled pellets. Companies achieve sustainability targets while improving financial performance simultaneously. This dual benefit makes environmental responsibility economically rational rather than purely altruistic, encouraging widespread adoption of pet bottle recycling machines across industries worldwide.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy