Pet Bottle Recycling Equipment Solutions

All Categories

pet bottle recycling equipment

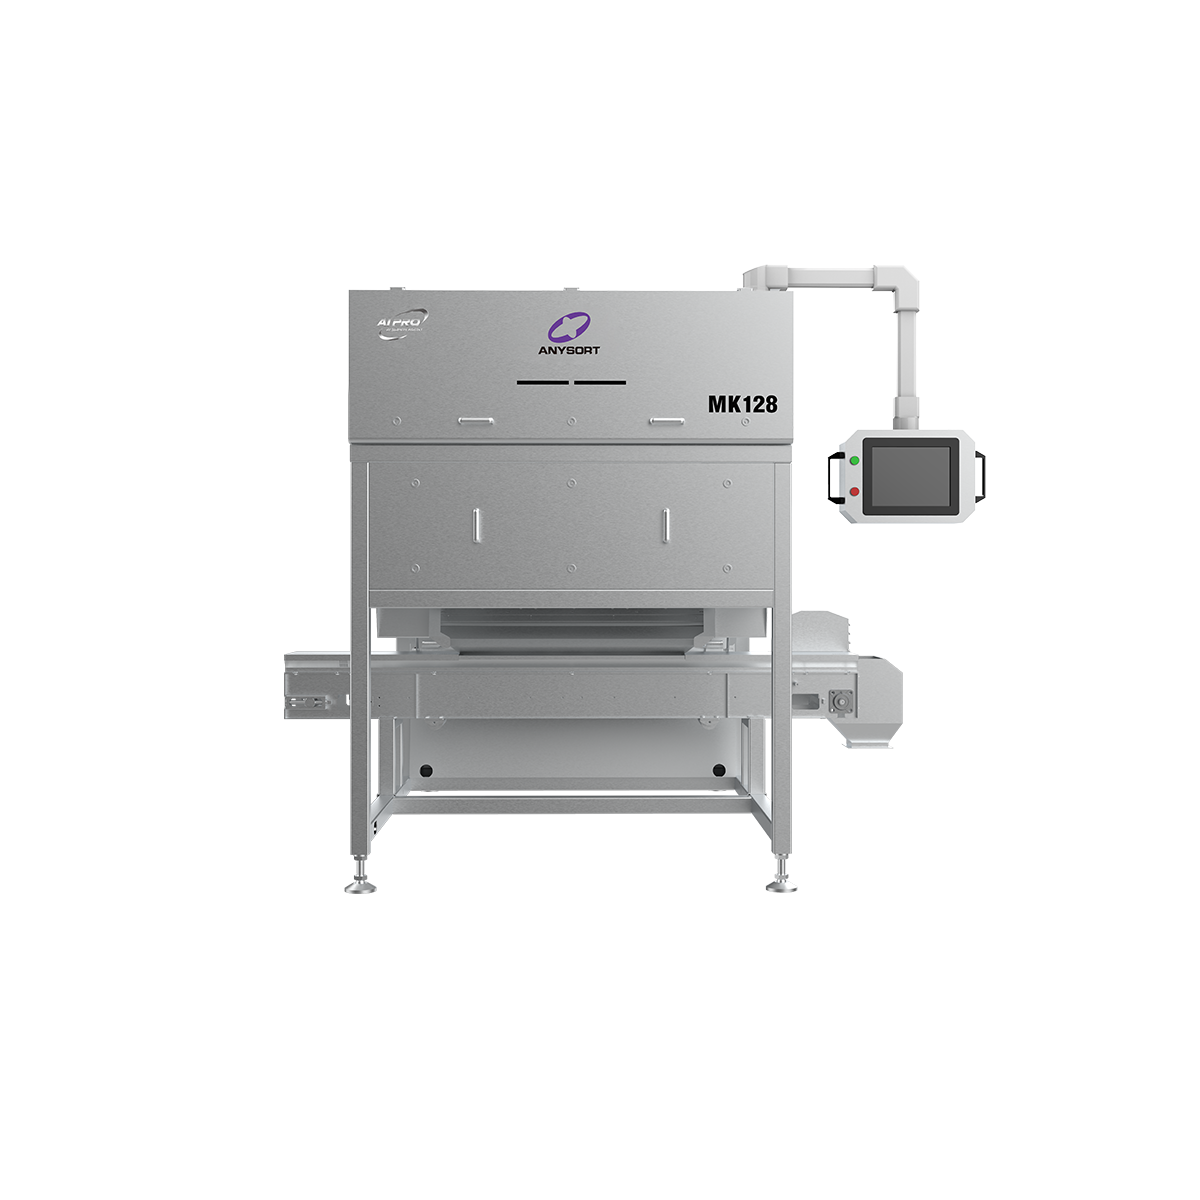
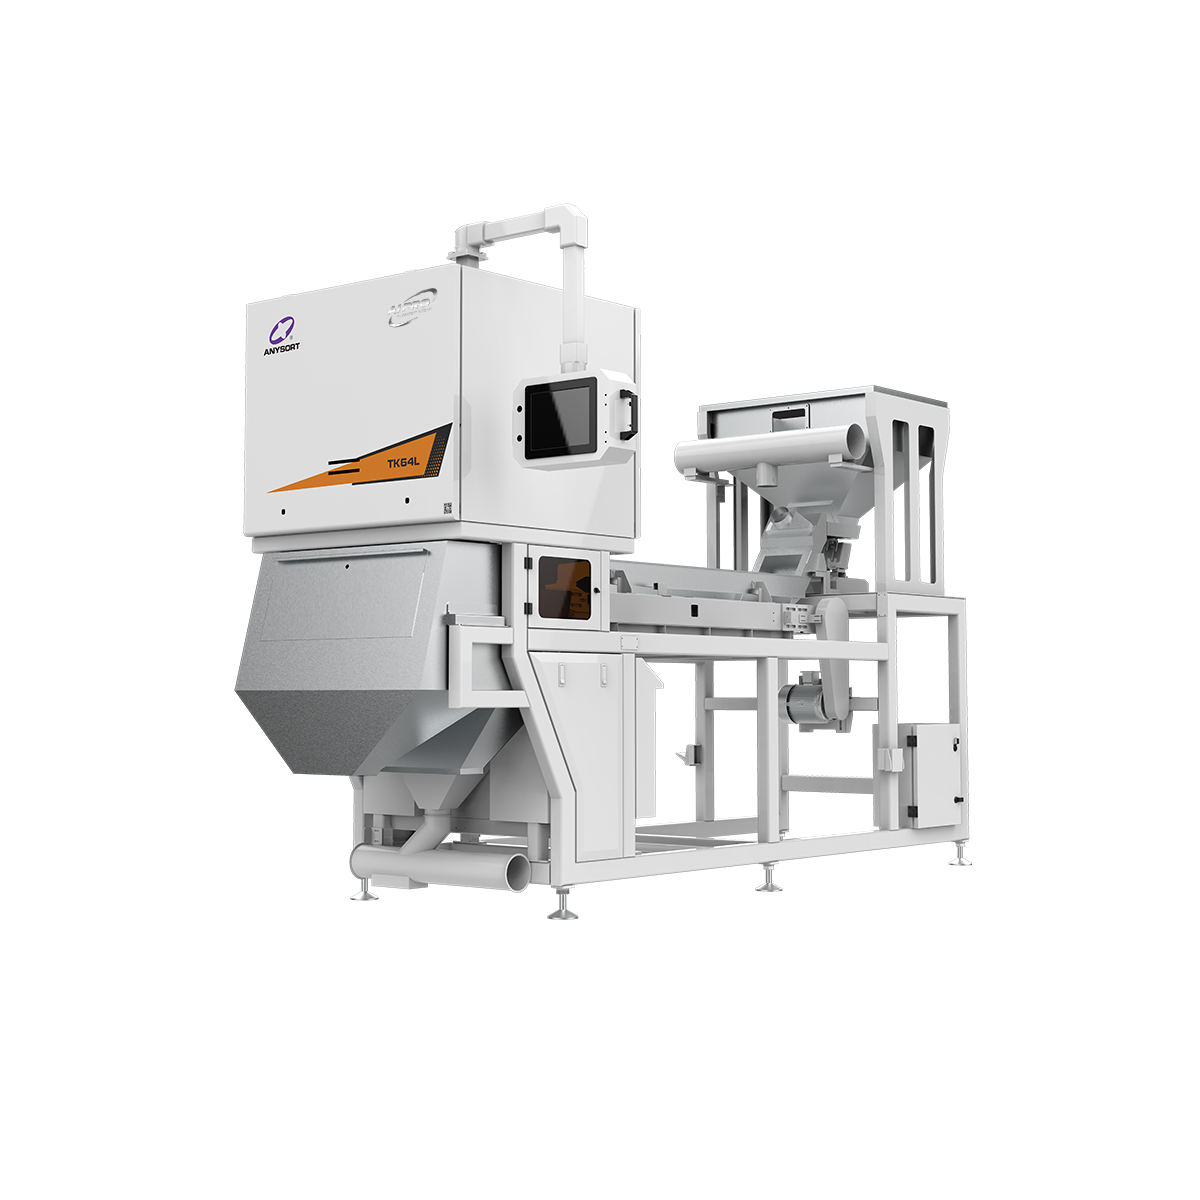
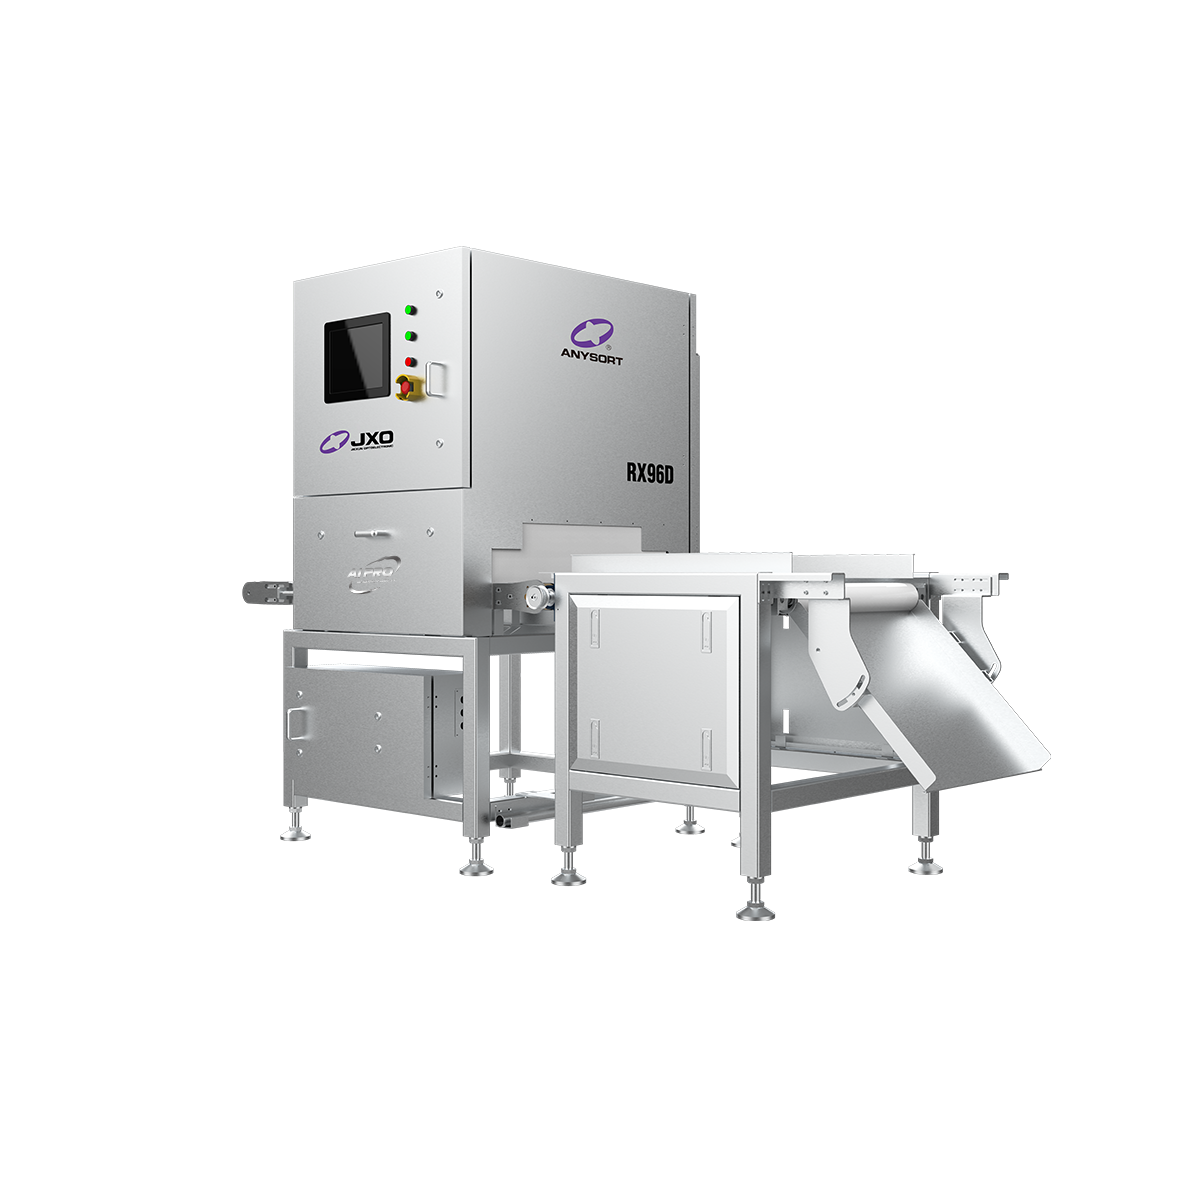
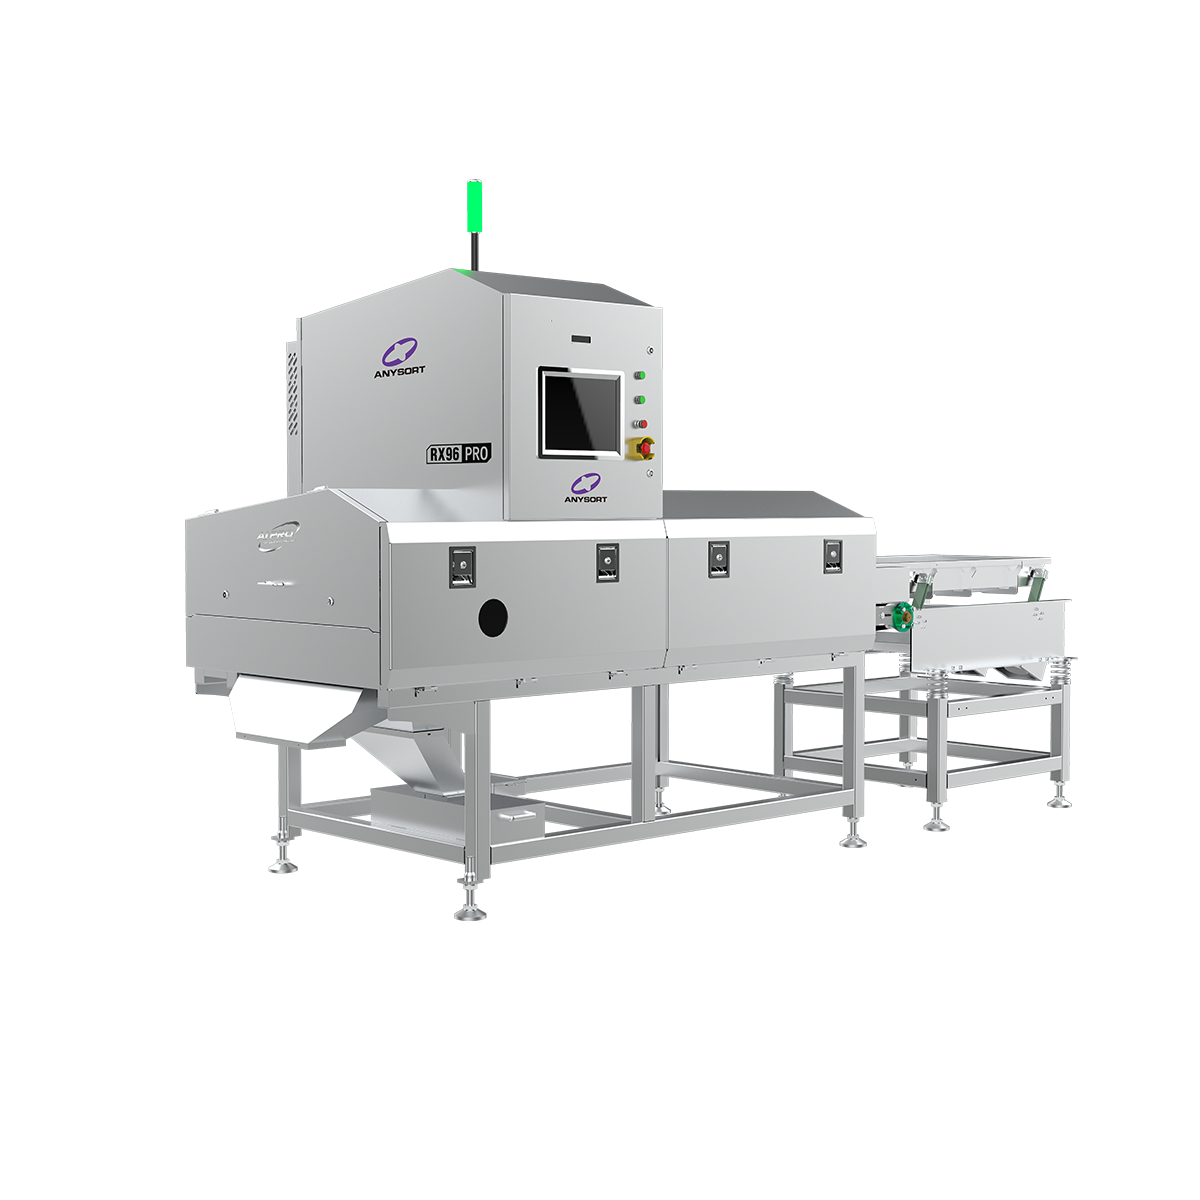
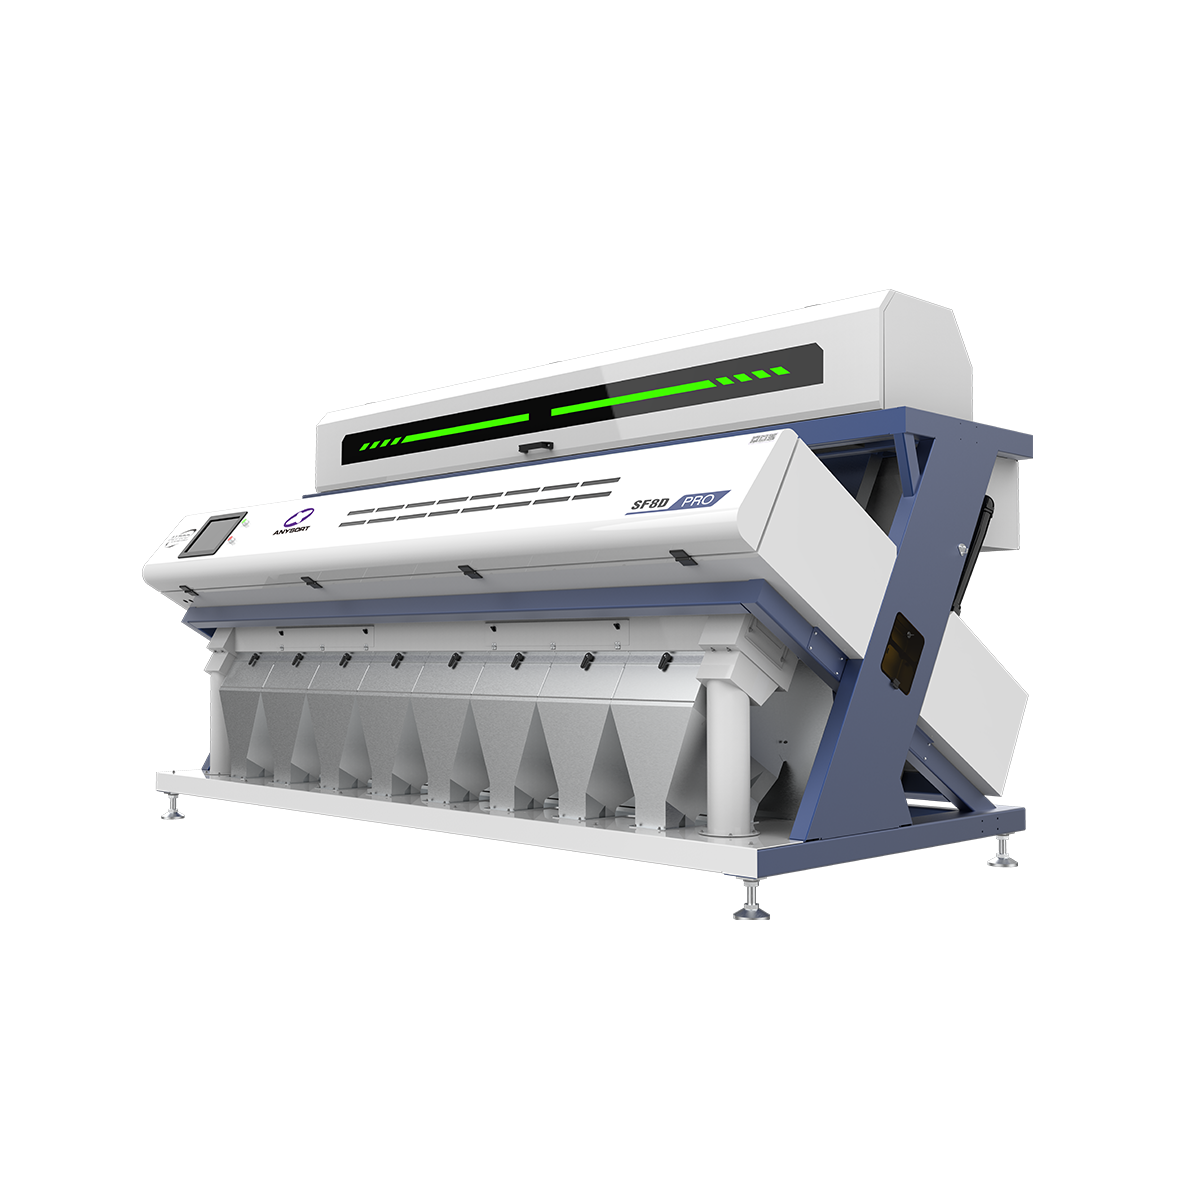
Pet bottle recycling equipment represents a modern solution for processing and managing plastic waste effectively. This specialized machinery handles the collection, sorting, and transformation of used PET bottles into reusable materials. Pet bottle recycling equipment operates through multiple stages, including initial collection, cleaning, shredding, and compacting processes that reduce waste volume significantly. The primary function of pet bottle recycling equipment involves converting discarded plastic bottles into valuable raw materials for manufacturing new products. Advanced pet bottle recycling equipment features automated sorting systems that separate different plastic grades, ensuring material purity and quality. Technological innovations include optical scanning sensors, magnetic separation mechanisms, and hydraulic compression systems that enhance processing efficiency. Modern pet bottle recycling equipment incorporates IoT connectivity and data monitoring capabilities for real-time operational insights. The equipment uses energy-efficient motors and optimized workflows to minimize environmental impact while maximizing output. Pet bottle recycling equipment applications span municipal waste management facilities, commercial recycling centers, and industrial manufacturing plants. These systems handle various bottle types and sizes, processing them into clean flakes, pellets, or compressed blocks. The technological features ensure minimal material loss and contamination during processing. Pet bottle recycling equipment represents a critical investment for organizations committed to circular economy principles and sustainable waste management practices.

New Product Releases

Pet bottle recycling equipment delivers substantial operational and financial benefits for businesses committed to sustainability. The equipment reduces waste disposal costs by transforming discarded bottles into valuable secondary materials, creating revenue opportunities through resale of processed plastics. Pet bottle recycling equipment streamlines waste management operations, eliminating manual sorting inefficiencies and reducing labor requirements significantly. Operational advantages include continuous processing capabilities, with modern pet bottle recycling equipment functioning reliably throughout extended work cycles. The automated systems minimize human error and safety risks associated with manual waste handling. Pet bottle recycling equipment enables businesses to meet environmental regulations and corporate sustainability targets effectively. Practical benefits for facility managers include reduced storage space requirements, as pet bottle recycling equipment compresses materials to approximately one-tenth their original volume. This compression capability optimizes transportation and storage logistics substantially. The equipment's user-friendly interface allows staff to monitor operations easily without extensive technical training. Pet bottle recycling equipment applications suit diverse facility sizes, from small community centers to large industrial complexes. Businesses utilizing pet bottle recycling equipment report improved brand reputation and customer loyalty through demonstrated environmental commitment. The equipment generates consistent material output, enabling predictable revenue streams from recycled plastic sales. Financial advantages extend to tax incentives and grants available for sustainable waste management implementations. Pet bottle recycling equipment investment payback periods typically range from two to four years, depending on processing volume and local market conditions. Organizations benefit from operational flexibility, as modern equipment adapts to varying input materials and production demands efficiently.

Tips And Tricks

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

pet bottle recycling equipment

Advanced Automated Sorting Technology

Advanced Automated Sorting Technology

Modern pet bottle recycling equipment incorporates sophisticated optical scanning and artificial intelligence systems that automatically identify and separate different plastic types and colors. This advanced sorting capability ensures material purity, significantly improving the quality of recycled output. Pet bottle recycling equipment equipped with this technology reduces contamination rates to below two percent, meeting stringent industry standards. The automated sorting process occurs at remarkable speeds, processing thousands of bottles hourly without human intervention. This technological innovation eliminates manual sorting inefficiencies and associated labor costs substantially. Pet bottle recycling equipment with advanced sorting provides consistent, high-quality material streams that command premium prices in secondary plastic markets. The precision sorting capabilities enable businesses to maximize revenue from recovered materials, as cleaner plastic streams qualify for higher-value applications. This feature makes pet bottle recycling equipment particularly valuable for commercial operations prioritizing profitability alongside environmental responsibility. Enhanced sorting accuracy directly translates to improved competitive advantage in recycled material markets.
Compact Design with High Processing Capacity

Compact Design with High Processing Capacity

Pet bottle recycling equipment combines space-efficient design with impressive processing volumes, making it ideal for facilities with limited space constraints. Modern equipment achieves compression ratios enabling processing of hundreds of kilograms of bottles into manageable, transportable packages daily. This exceptional capacity-to-footprint ratio represents significant operational advantage for urban recycling centers and commercial waste facilities. The compact architecture of pet bottle recycling equipment allows installation in modest facility spaces while maintaining substantial output capabilities. Hydraulic compression systems reduce processed materials to densities up to four hundred kilograms per cubic meter, optimizing storage and transportation efficiency. Pet bottle recycling equipment's intelligent design eliminates the need for large dedicated warehouse areas typically required by conventional recycling operations. Businesses implementing pet bottle recycling equipment experience remarkable improvements in facility logistics and supply chain management. The equipment's efficiency means fewer delivery trips and reduced transportation costs for processed materials. Compact pet bottle recycling equipment configurations adapt seamlessly to existing facility layouts, minimizing installation complexity and operational disruption.
Energy-Efficient Operation with Real-Time Monitoring

Energy-Efficient Operation with Real-Time Monitoring

Contemporary pet bottle recycling equipment features energy-conscious motor systems and intelligent power management that reduce operational electricity consumption by up to forty percent compared to older equipment models. Pet bottle recycling equipment incorporates IoT sensors providing continuous performance monitoring, predictive maintenance alerts, and production analytics through cloud-based platforms. This technological integration enables facility managers to optimize operations and identify efficiency improvements proactively. Real-time monitoring capabilities in pet bottle recycling equipment track processing metrics, material volumes, and equipment health indicators continuously. Operators receive instant notifications regarding maintenance requirements, preventing costly breakdowns and production delays. Pet bottle recycling equipment's data insights support informed decision-making regarding operational adjustments and resource allocation. Energy-efficient operation directly translates to reduced operational costs and improved environmental sustainability metrics for organizations. Pet bottle recycling equipment's smart systems automatically adjust processing speeds based on material type and volume, maximizing efficiency while minimizing energy waste. This responsive technology ensures facilities operate at optimal energy levels throughout daily operations, supporting both financial performance and environmental objectives simultaneously.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy