Sorter Rice Machine | Advanced Grain Sorting

All Categories

sorter rice

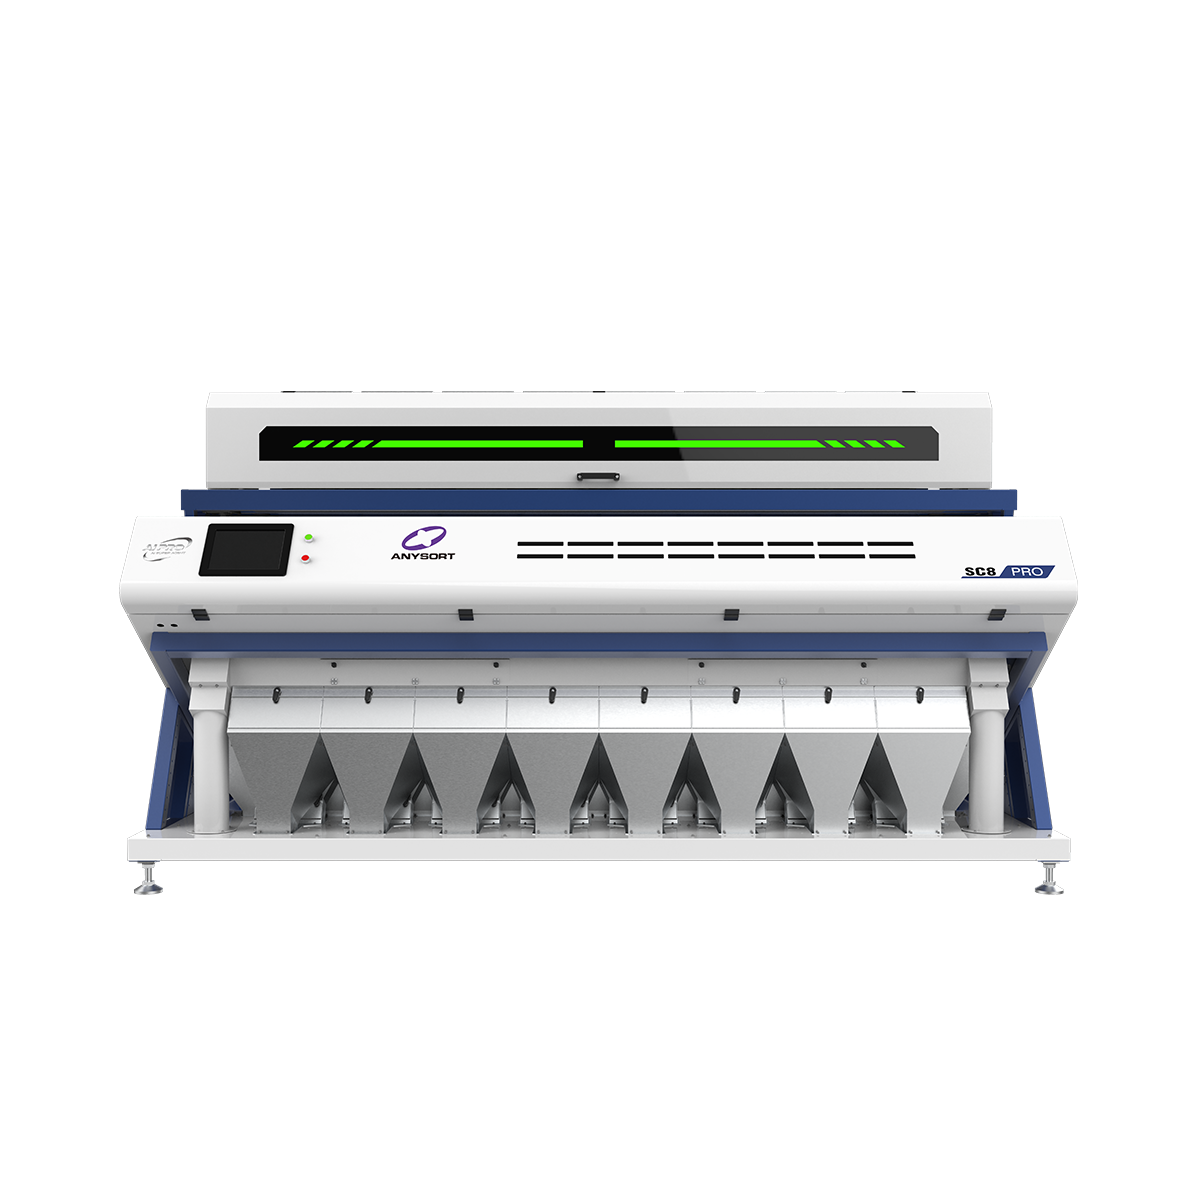
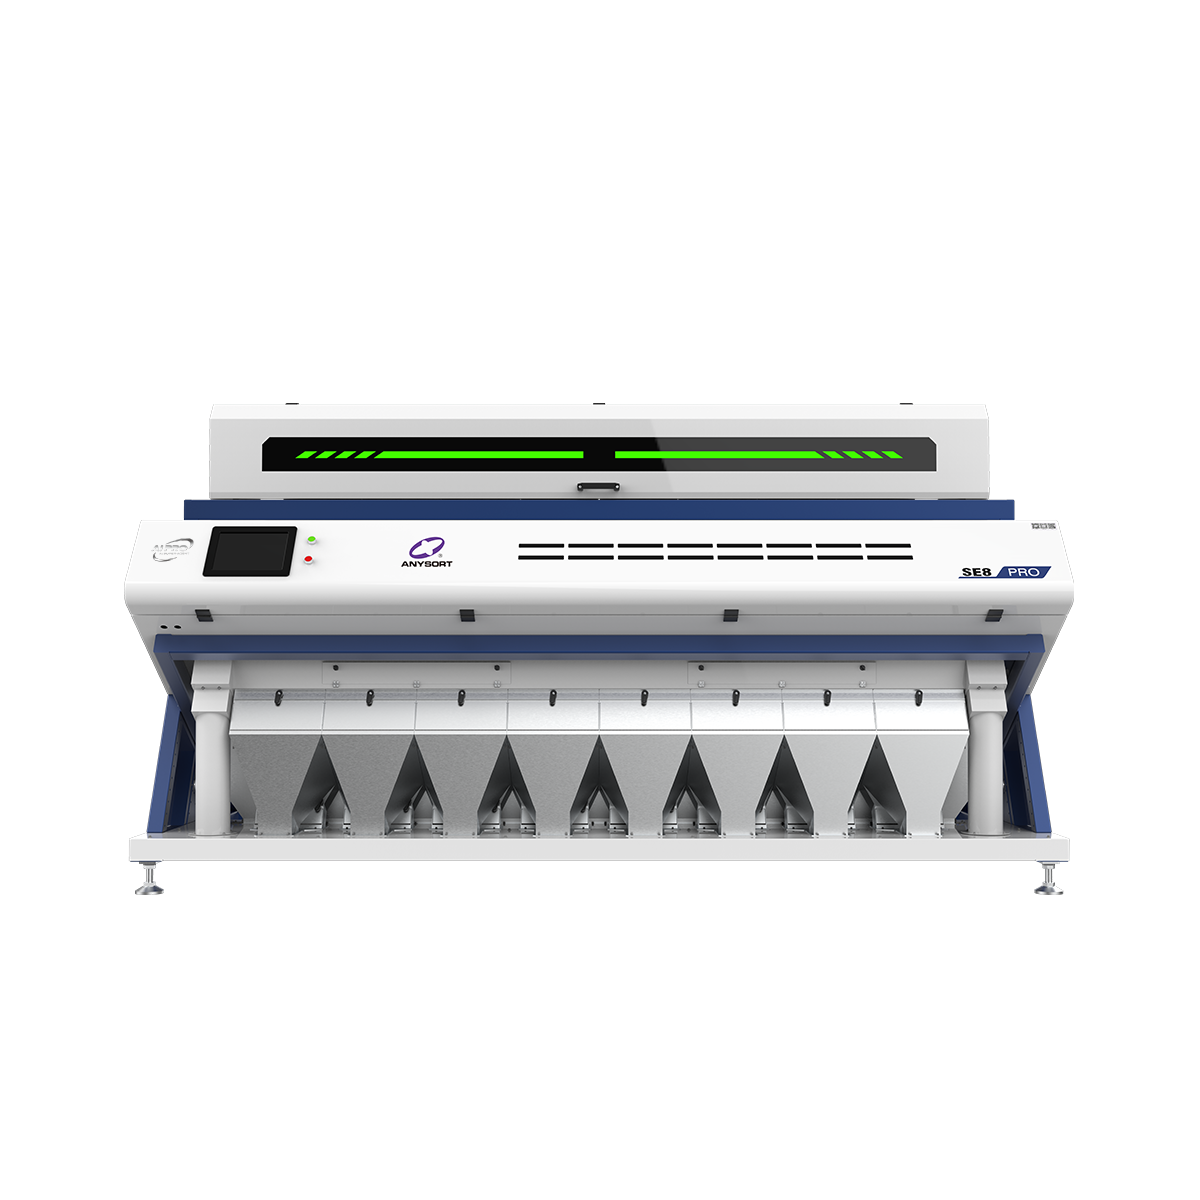
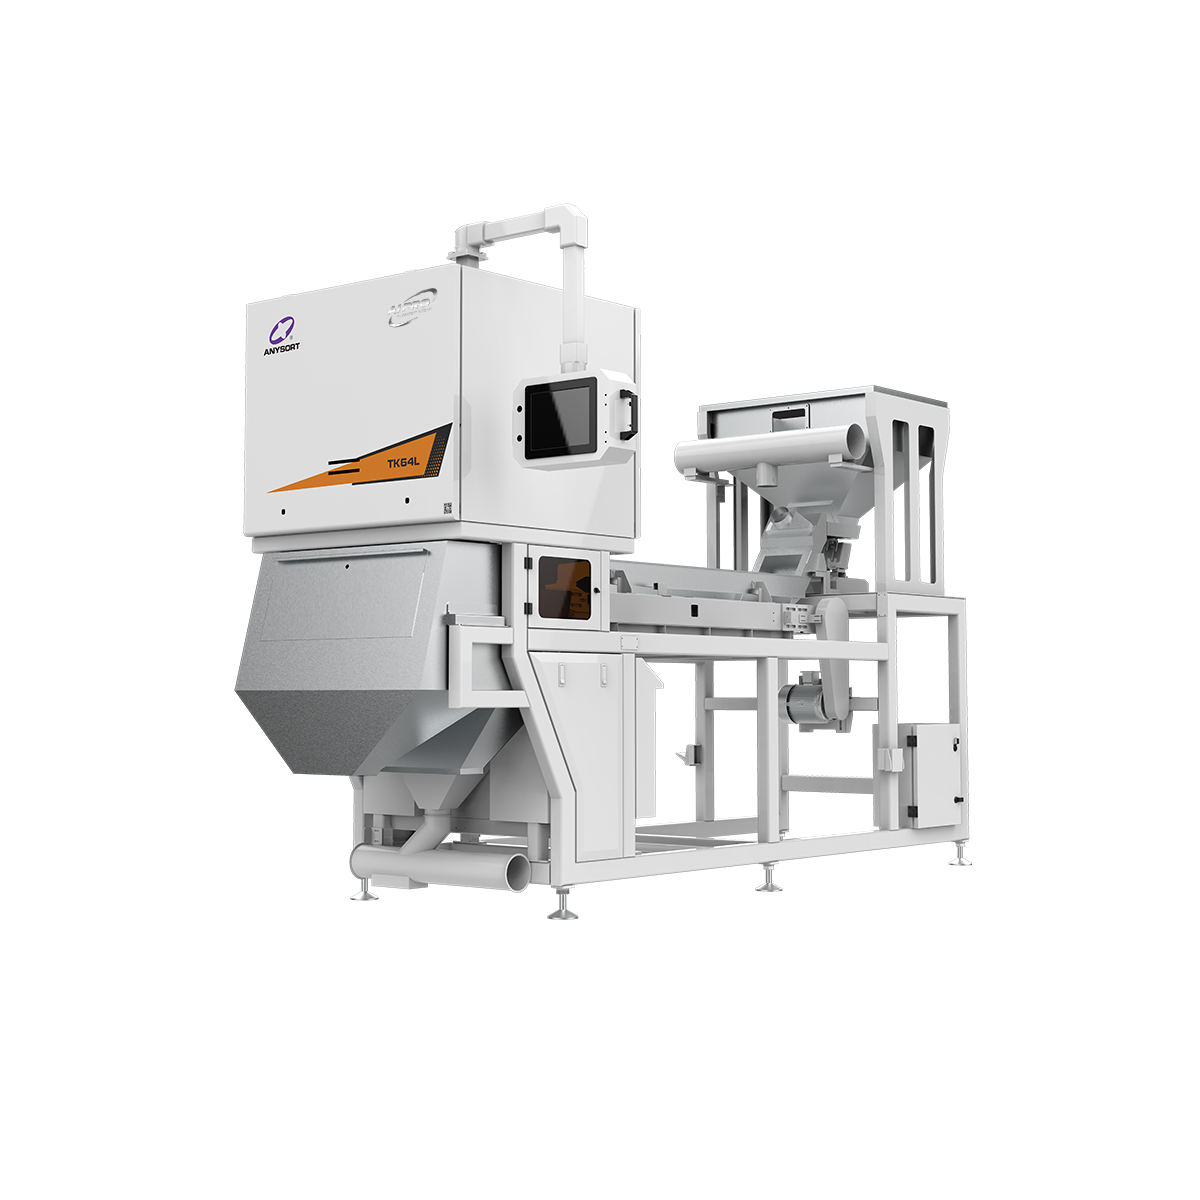
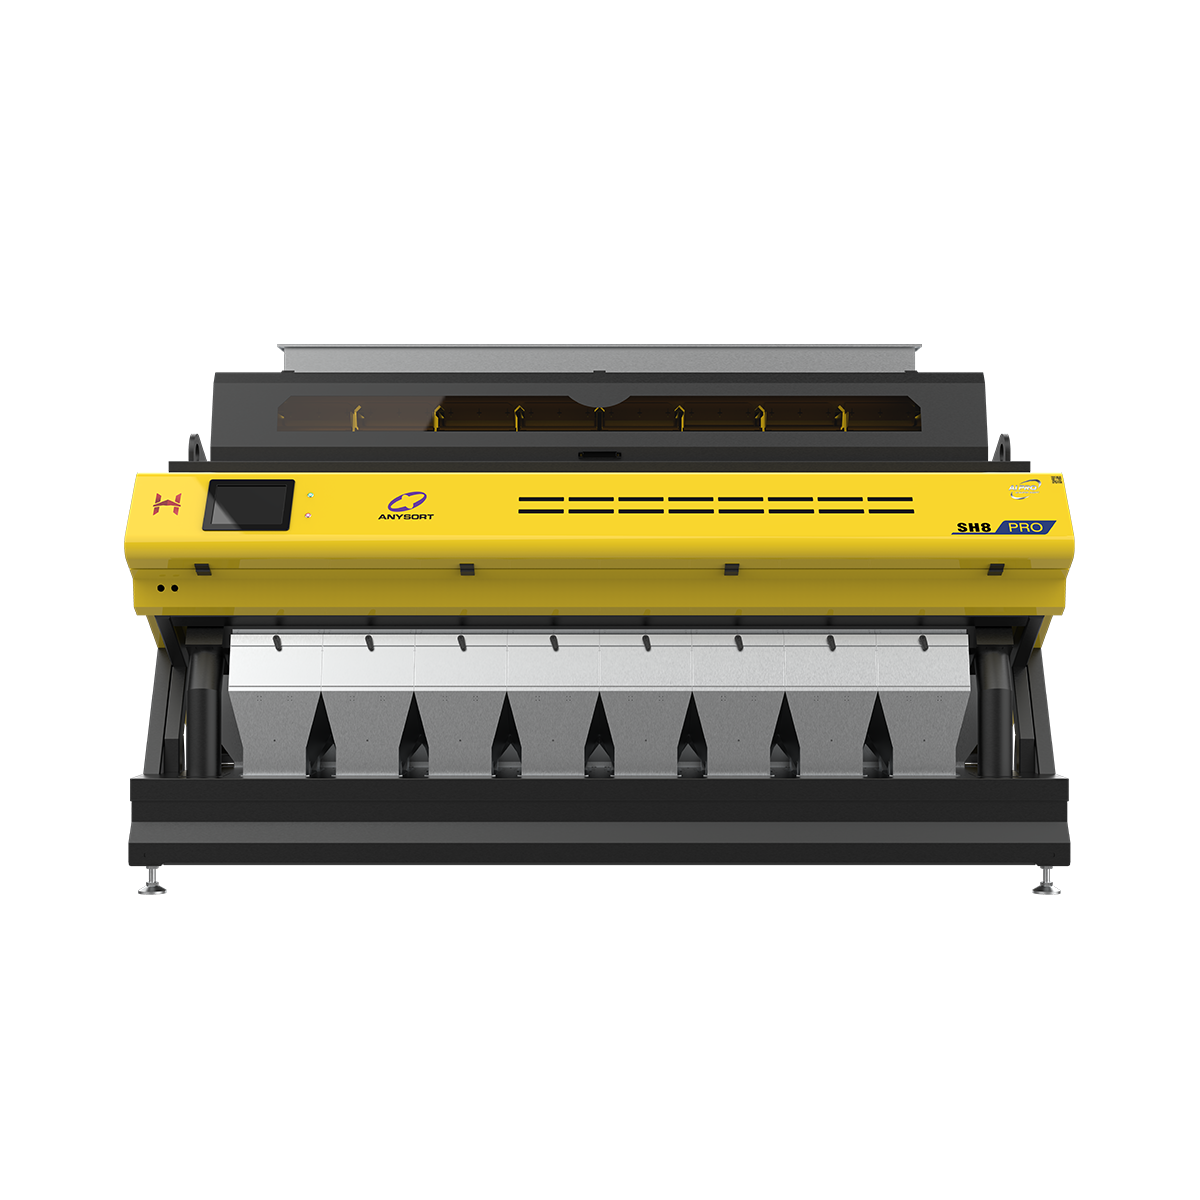
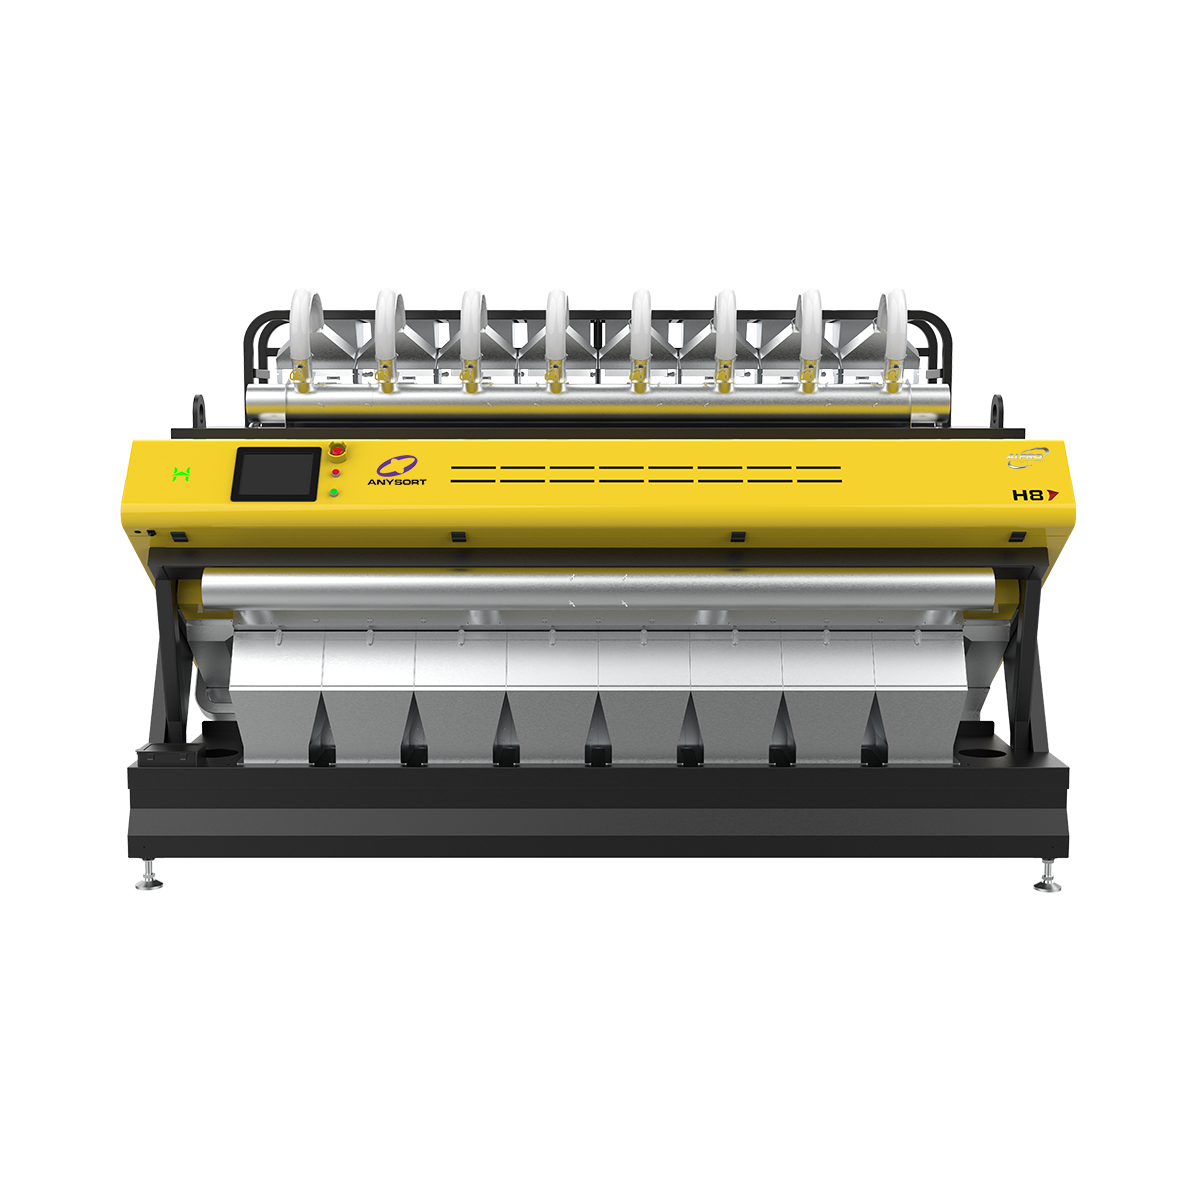
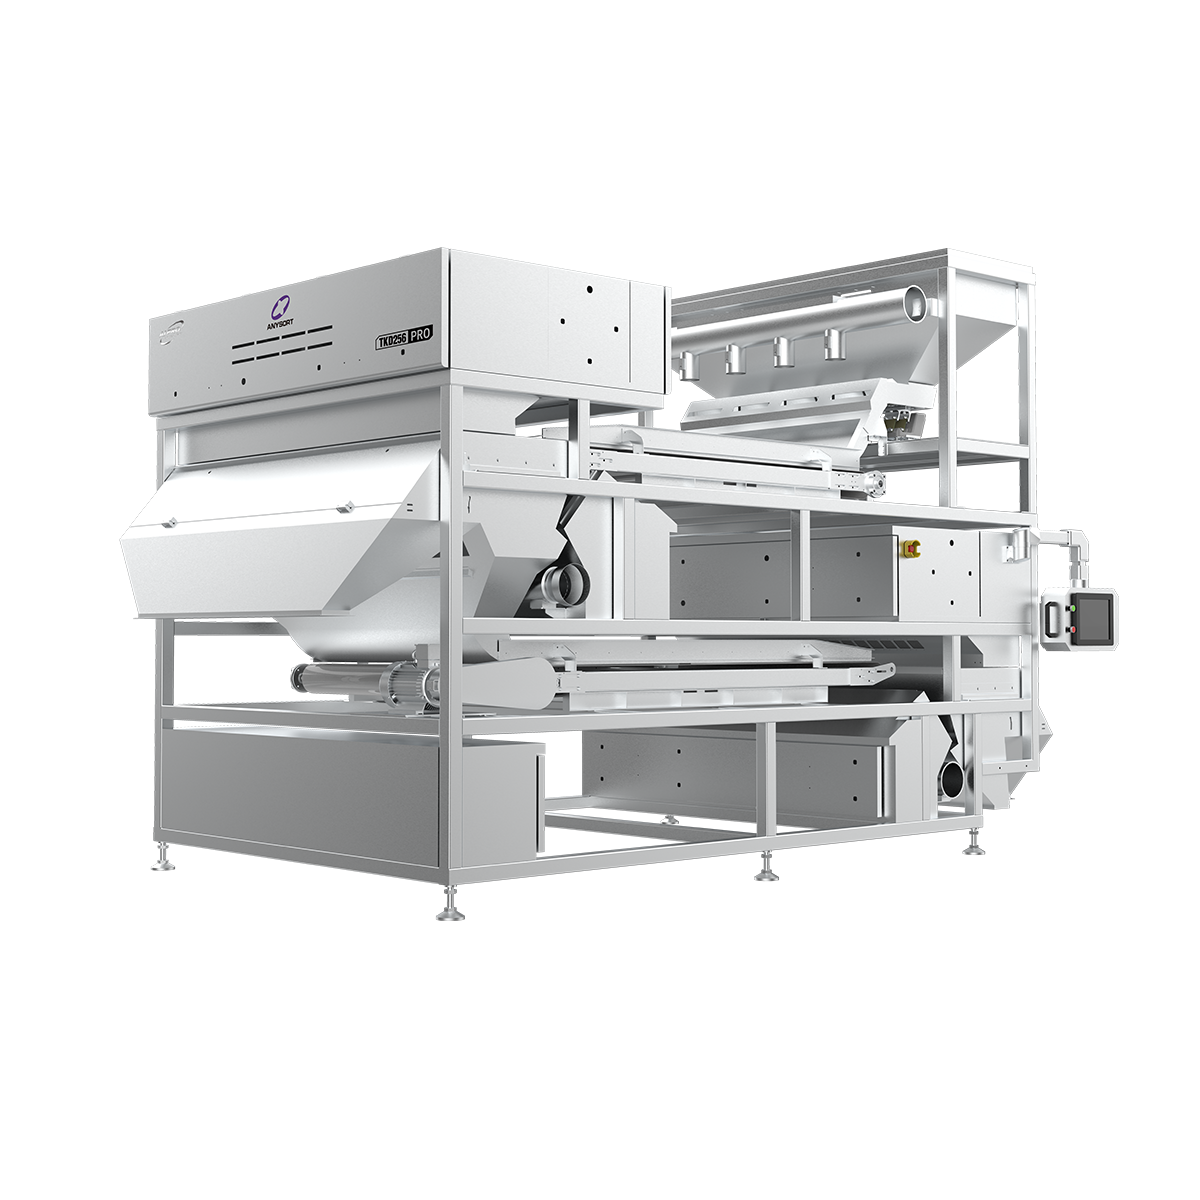
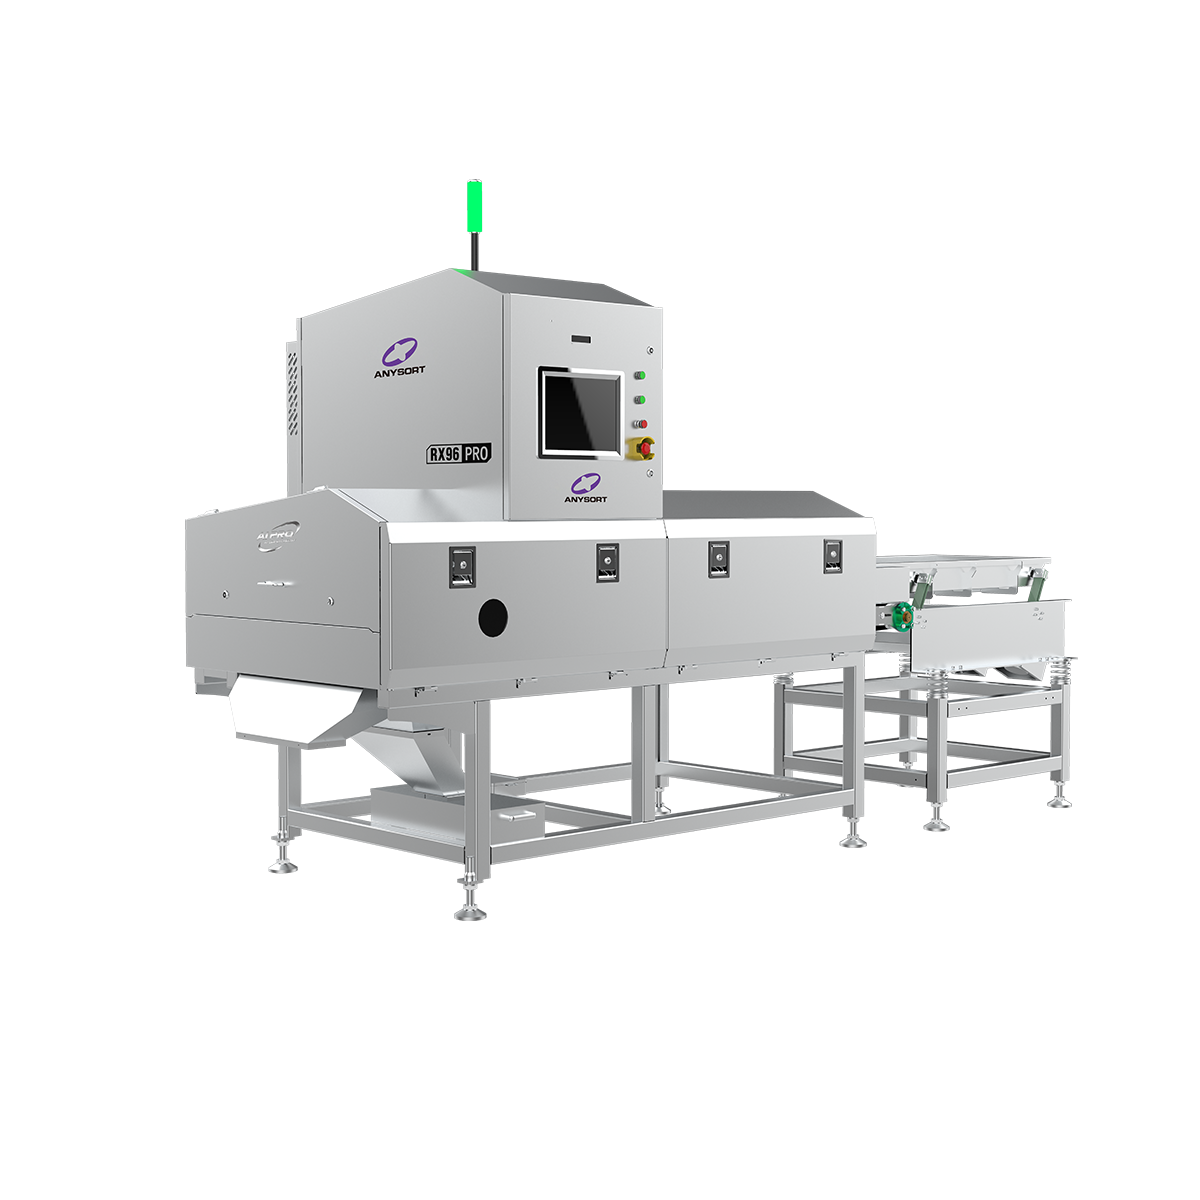
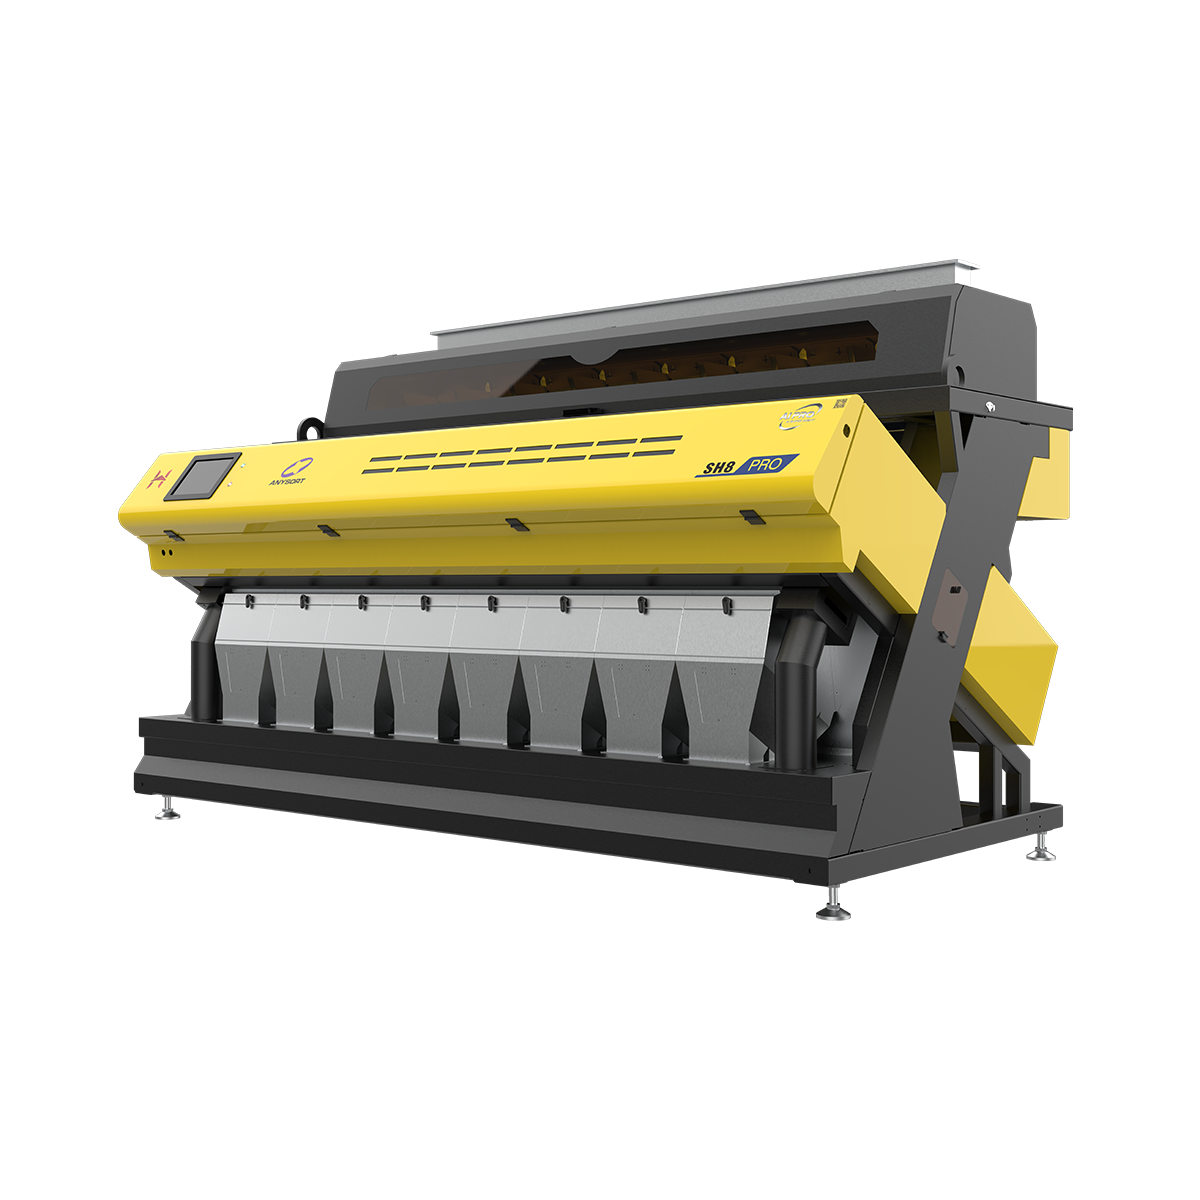
A sorter rice machine represents a revolutionary advancement in grain processing technology, designed to automatically classify and separate rice grains based on quality, size, and color characteristics. The sorter rice system utilizes advanced optical scanning and artificial intelligence to identify defects, discolored grains, and foreign materials with exceptional precision. This sophisticated sorter rice equipment processes large volumes of rice efficiently, ensuring only premium-quality grains reach consumers while removing broken kernels, chalky rice, and contaminated particles seamlessly. The primary function of a sorter rice machine is to enhance product quality and maximize yield by eliminating inferior grains that would otherwise compromise the final product. Modern sorter rice technology incorporates high-speed cameras, spectral analysis, and machine learning algorithms that work together to achieve sorting accuracy exceeding 99 percent. These systems are engineered to handle various rice varieties, from long-grain white rice to specialty aromatic and brown rice options. The sorter rice machines operate continuously throughout production cycles, maintaining consistent quality standards while significantly reducing labor-intensive manual sorting processes. By implementing sorter rice technology in processing facilities, producers can meet stringent international quality requirements, enhance brand reputation, and improve profitability through waste reduction and efficiency gains.

New Products

The sorter rice machine delivers substantial operational and financial benefits that transform rice processing businesses. First, implementing a sorter rice system dramatically improves product quality, ensuring only visually perfect and healthy grains are packaged and sold to consumers. This quality assurance directly increases customer satisfaction and brand loyalty while commanding premium market prices. Second, the sorter rice equipment operates with exceptional speed and efficiency, processing hundreds of kilograms per hour while maintaining accuracy that surpasses manual sorting capabilities. This increased throughput allows processing facilities to handle larger volumes without proportional increases in labor costs, making sorter rice technology economically superior to traditional methods. Third, sorter rice machines reduce operational expenses by minimizing human error and eliminating the need for extensive manual labor, which represents one of the largest cost components in conventional rice processing. The sorter rice system generates consistent, reliable results regardless of operator experience level, ensuring uniform quality across all production batches. Additionally, sorter rice technology enhances workplace safety by reducing repetitive strain injuries associated with manual sorting tasks. The equipment also minimizes product waste by recovering rice grains that might otherwise be discarded, directly improving profit margins. Finally, investing in sorter rice machinery demonstrates commitment to modern processing standards, helping businesses comply with international food safety regulations and quality certifications required for export markets and premium retail distribution channels.

Practical Tips

How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

sorter rice

Precision Optical Sorting Technology

Precision Optical Sorting Technology

The sorter rice machine features cutting-edge optical detection systems that employ multiple high-resolution cameras and spectral sensors to evaluate each grain individually. This advanced technology enables the sorter rice equipment to identify subtle imperfections, color variations, and structural abnormalities that human eyes cannot consistently detect. The system analyzes rice grains at extraordinary speeds, classifying thousands of kernels per second with precision accuracy. The sorter rice technology uses sophisticated algorithms to differentiate between acceptable quality grains and those requiring removal, whether due to discoloration, damage, or contamination. This optical excellence ensures that the sorter rice machine maintains the highest quality standards, preserving the nutritional value and aesthetic appeal of the final product while removing any grain that could compromise customer satisfaction or regulatory compliance.
High-Capacity Processing Performance

High-Capacity Processing Performance

The sorter rice system is engineered to deliver exceptional processing capacity without compromising accuracy or reliability. Modern sorter rice machines can process between 500 to 2,000 kilograms per hour depending on the specific model and rice variety being sorted. This impressive throughput means the sorter rice equipment can easily accommodate the demands of large-scale commercial operations, processing entire daily production volumes efficiently. The sorter rice technology incorporates robust mechanical design and industrial-grade components that withstand continuous operation under demanding conditions. Facilities utilizing sorter rice machinery experience significant productivity improvements, completing sorting tasks in a fraction of the time required by manual methods. The sorter rice machine maintains consistent performance throughout extended operational periods, requiring minimal downtime for maintenance while delivering reliable, repeatable results that exceed traditional processing capabilities and support business growth.
Intelligent Quality Control System

Intelligent Quality Control System

The sorter rice equipment incorporates artificial intelligence and machine learning capabilities that continuously improve sorting accuracy and adapt to different rice varieties. The sorter rice system learns from each sorting cycle, refining its detection algorithms to identify emerging quality issues and optimize classification parameters automatically. This intelligent approach means the sorter rice machine becomes more effective over time, delivering increasingly superior results as it processes more product. The sorter rice technology provides real-time quality monitoring, detailed sorting reports, and predictive maintenance alerts that help operators maintain peak performance. The system allows easy customization of sorting parameters to accommodate different rice grades, processing requirements, and quality standards specific to various market segments. By implementing sorter rice intelligence systems, facilities gain unprecedented visibility into product quality metrics and production efficiency data that support continuous improvement initiatives and data-driven decision-making processes.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy