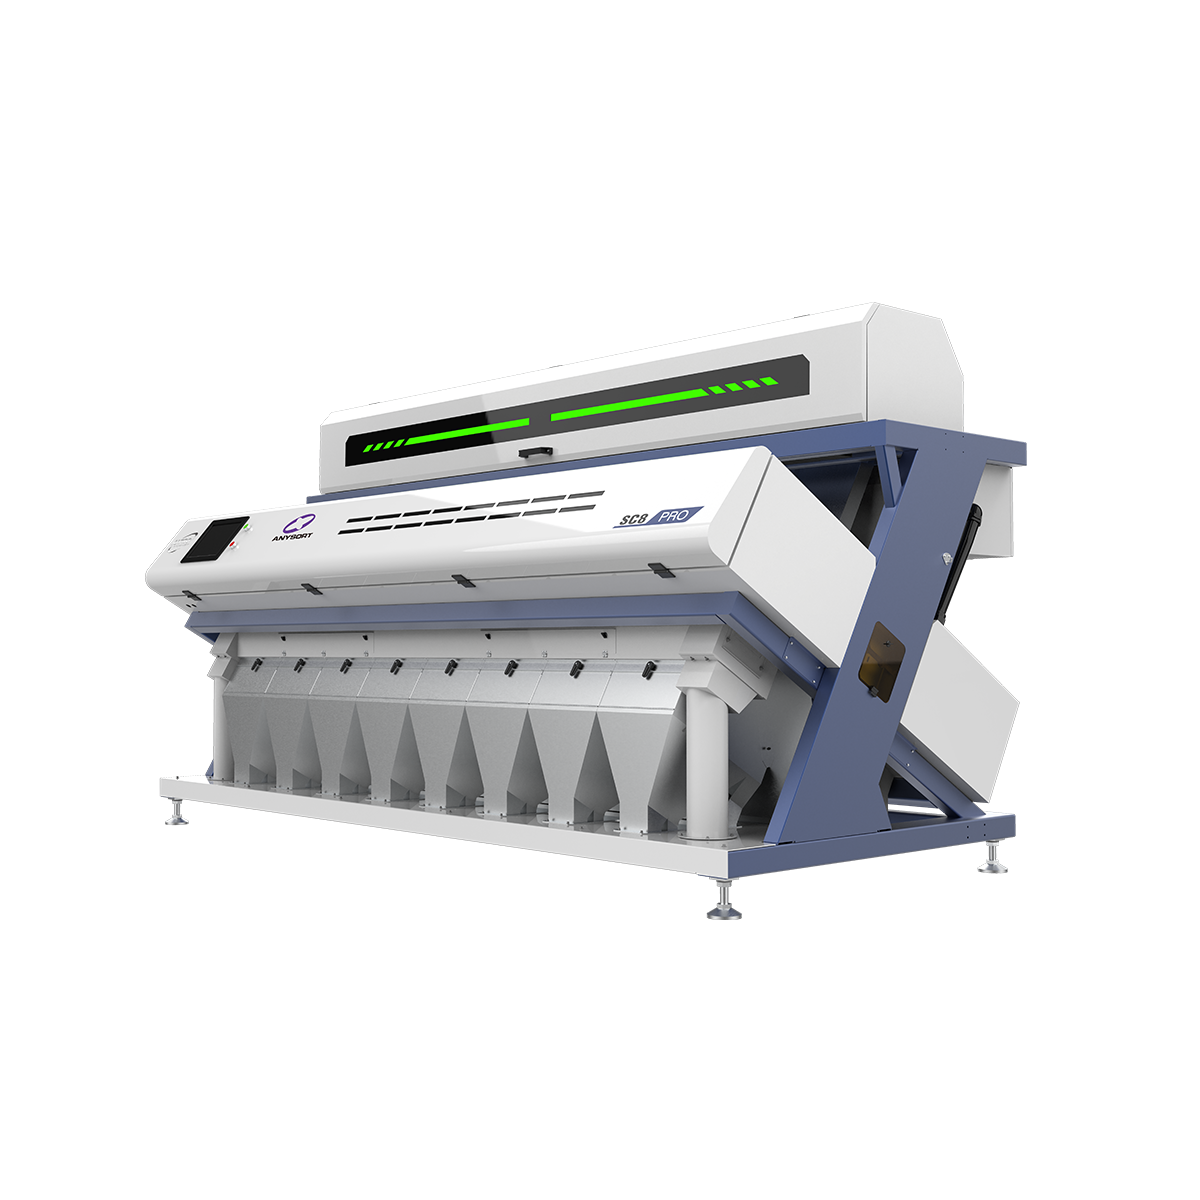
Waste Bottle Recycling Machine

All Categories

waste bottle recycling machine

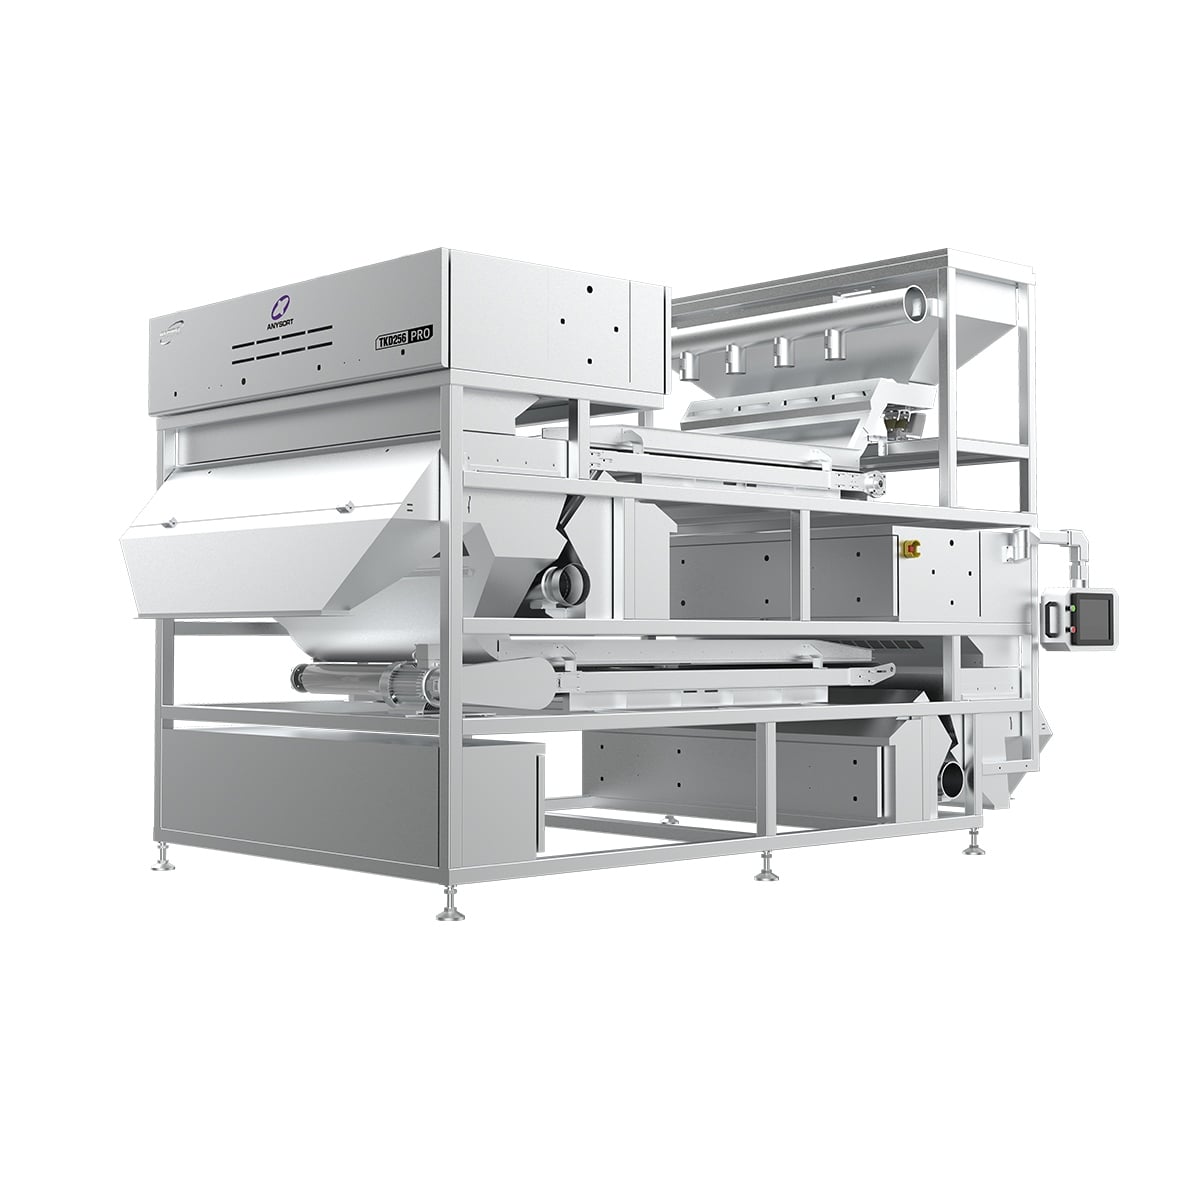
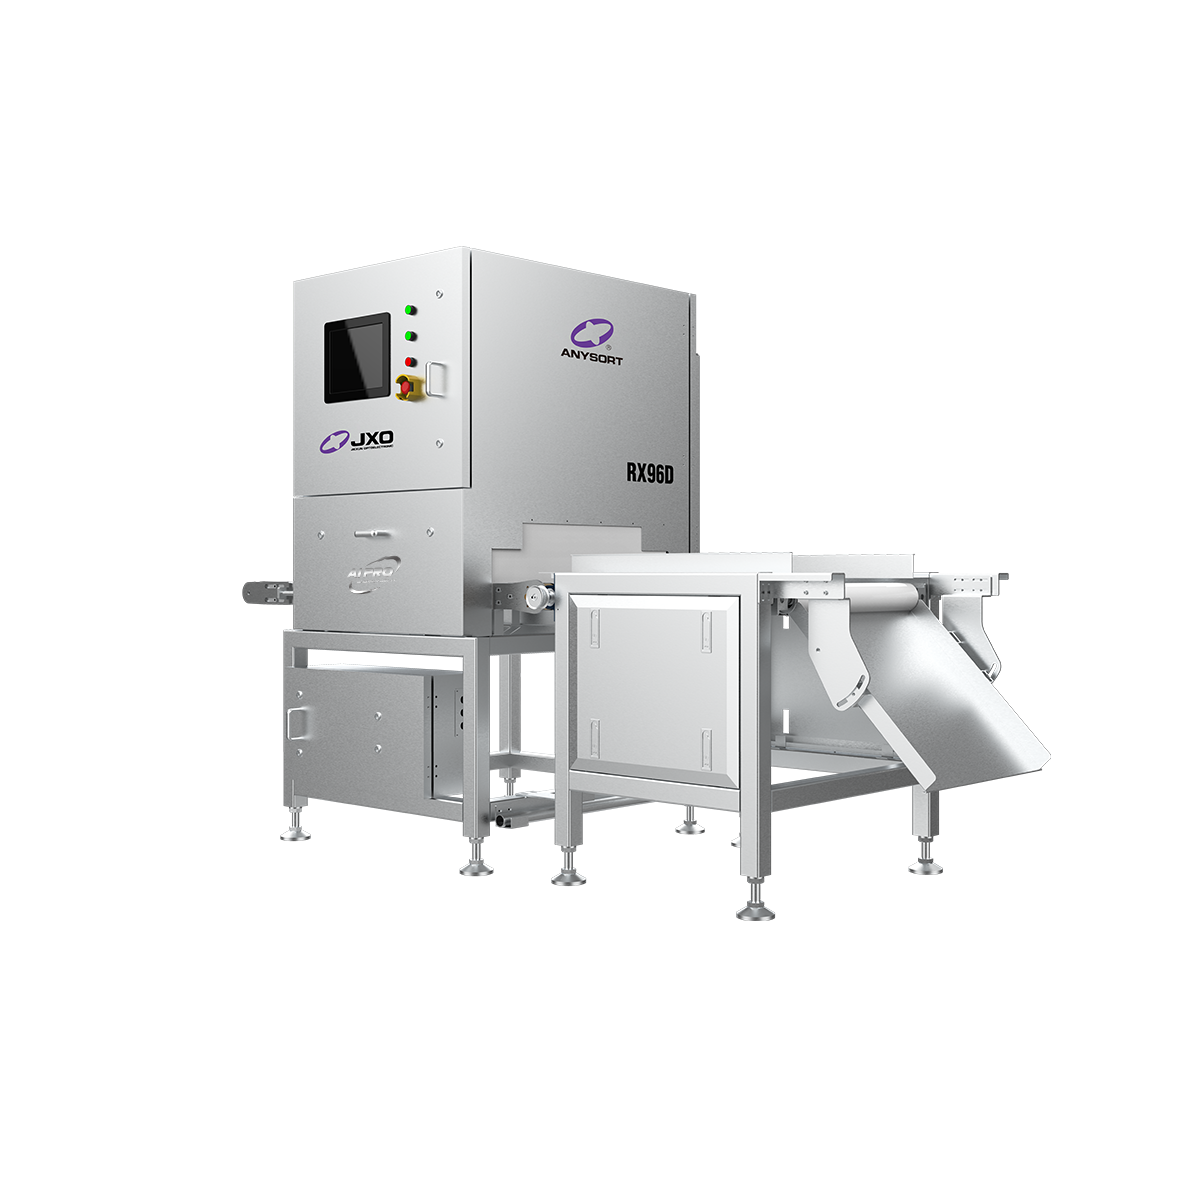
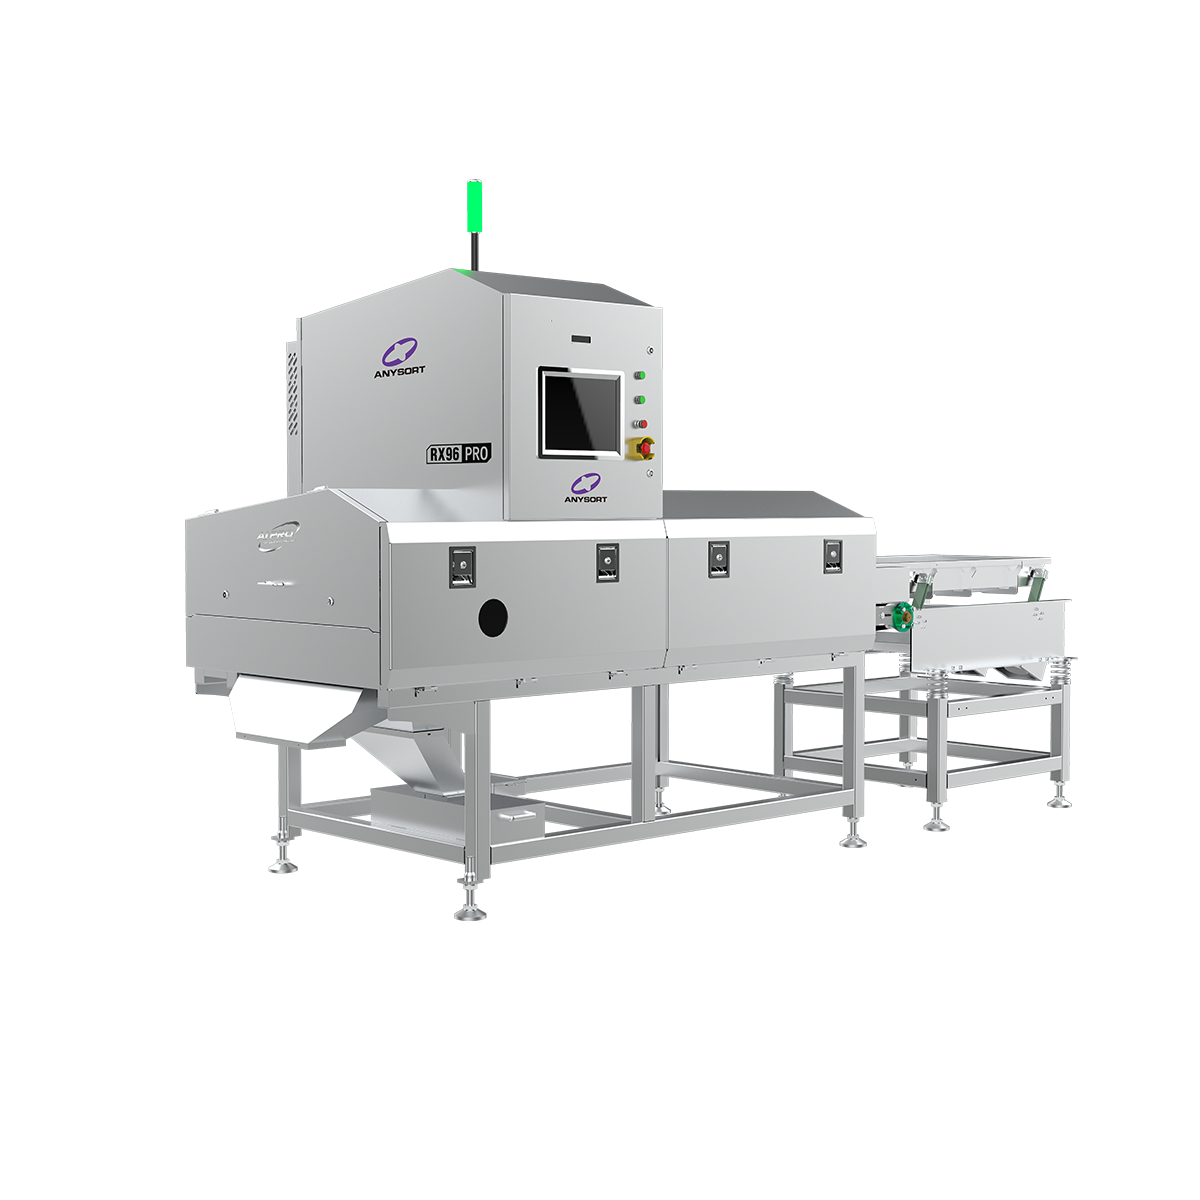
A waste bottle recycling machine is an innovative industrial solution designed to process and transform discarded plastic and glass bottles into reusable materials. This advanced waste bottle recycling machine automates the entire recycling process, from collection and sorting to compression and material separation. The technology uses sophisticated mechanical systems to crush, clean, and compact bottles, significantly reducing their volume for easier transportation and storage. The waste bottle recycling machine incorporates optical sorting technology that identifies different plastic types and colors, ensuring proper material classification. Modern waste bottle recycling machines feature automated feeding systems that continuously process incoming bottles without manual intervention. These machines are equipped with powerful hydraulic or pneumatic compression systems that reduce bottle volume by up to 90 percent. The waste bottle recycling machine also includes washing and drying components that remove contaminants before material processing. Advanced sensors monitor operational parameters, ensuring consistent quality output. The technology supports environmental sustainability by diverting significant quantities of waste from landfills. Processing capacity ranges from 500 to 5,000 kilograms per hour, depending on machine specifications. The waste bottle recycling machine represents a crucial step in circular economy initiatives, transforming waste materials into valuable secondary resources. Integration with existing recycling facilities makes this equipment an essential component of modern waste management infrastructure.

New Product Releases

The waste bottle recycling machine delivers substantial operational and financial benefits to recycling facilities and waste management companies. First, operational efficiency improves dramatically as automated processes reduce manual labor requirements by 75 percent. The waste bottle recycling machine maximizes material recovery rates, converting more waste into usable resources compared to traditional methods. Processing costs decrease significantly because the machinery handles volume reduction automatically, lowering transportation and storage expenses. Facilities operating a waste bottle recycling machine experience improved safety conditions, eliminating worker exposure to hazardous materials and sharp objects. Revenue generation increases through higher-quality sorted materials that command better market prices. The waste bottle recycling machine requires minimal floor space despite its substantial processing capacity, making it suitable for facilities with space constraints. Environmental benefits are substantial, as each machine diverts thousands of tons of waste annually from landfills. Maintenance is straightforward with accessible components and user-friendly interfaces requiring minimal technical training. The waste bottle recycling machine operates continuously with minimal downtime, providing reliable production schedules. Energy efficiency improvements reduce operational costs while supporting sustainability goals. Integration capabilities allow seamless connection with existing conveyor systems and sorting equipment. Investment returns occur quickly due to reduced labor costs and increased material throughput. The waste bottle recycling machine supports compliance with environmental regulations and corporate sustainability commitments. Scalability options enable facilities to expand capacity as demand grows. Advanced monitoring systems provide real-time data for optimization and predictive maintenance planning.

Practical Tips

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

waste bottle recycling machine

Advanced Automated Sorting Technology

Advanced Automated Sorting Technology

The waste bottle recycling machine incorporates cutting-edge optical recognition systems that automatically identify and separate different bottle materials with exceptional accuracy. This technology distinguishes between PET, HDPE, PVC, and other plastic types instantaneously, eliminating sorting errors and contamination issues. The waste bottle recycling machine uses infrared sensors and artificial intelligence algorithms to detect color variations and material compositions. This automated approach eliminates tedious manual sorting tasks that consume significant time and labor resources. The sorting capability ensures material purity, which directly increases market value and buyer demand. Processing accuracy reaches 98 percent, significantly surpassing manual sorting performance. The waste bottle recycling machine's intelligent system learns from operational data, continuously improving sorting precision over time. Facilities achieve better material consistency, enabling partnerships with quality-conscious buyers. The technology handles mixed waste streams efficiently, requiring minimal pre-sorting by operators. Implementation of advanced sorting technology maximizes profitability while reducing quality complaints and customer dissatisfaction rates.
High-Volume Capacity with Space Efficiency

High-Volume Capacity with Space Efficiency

This waste bottle recycling machine delivers impressive processing capacity while maintaining a compact footprint suitable for diverse facility layouts. Models process between 500 and 5,000 kilograms per hour, accommodating small operations through large industrial facilities. The waste bottle recycling machine achieves this efficiency through innovative compression technology that reduces bottle volume by up to 90 percent. Vertical design configurations minimize floor space requirements while maximizing throughput capabilities. The waste bottle recycling machine's modular construction allows facilities to adjust production capacity without requiring facility renovations. Compressed output reduces storage area needs, lowering facility operational costs considerably. High-capacity performance enables facilities to process daily waste volumes efficiently, preventing bottlenecks during peak seasons. The waste bottle recycling machine consistently maintains quality standards regardless of input volume fluctuations. Integration into existing workflows requires minimal space modifications. Equipment dimensions range from compact models at 2x2 meters to industrial units at 5x3 meters, providing flexibility for various facility configurations.
Sustainable Environmental Impact and Cost Reduction

Sustainable Environmental Impact and Cost Reduction

Operating a waste bottle recycling machine generates substantial environmental and economic benefits for progressive organizations. Each machine diverts 5,000 to 10,000 tons of waste annually from landfills, reducing environmental burden significantly. The waste bottle recycling machine reduces carbon emissions associated with landfill operations and virgin material production. Processed materials become valuable secondary resources, supporting circular economy principles and sustainability goals. Cost reduction occurs through decreased labor expenses, reduced transportation requirements, and minimized landfill disposal fees. The waste bottle recycling machine helps facilities achieve environmental certifications and corporate sustainability targets. Revenue generation increases as recycled materials command premium prices in secondary markets. Energy consumption remains relatively low compared to virgin material production processes. The waste bottle recycling machine supports regulatory compliance with environmental protection standards and waste management regulations. Companies operating this equipment enhance brand reputation among environmentally conscious consumers and business partners. Investment in a waste bottle recycling machine demonstrates commitment to sustainable business practices.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy