 EN
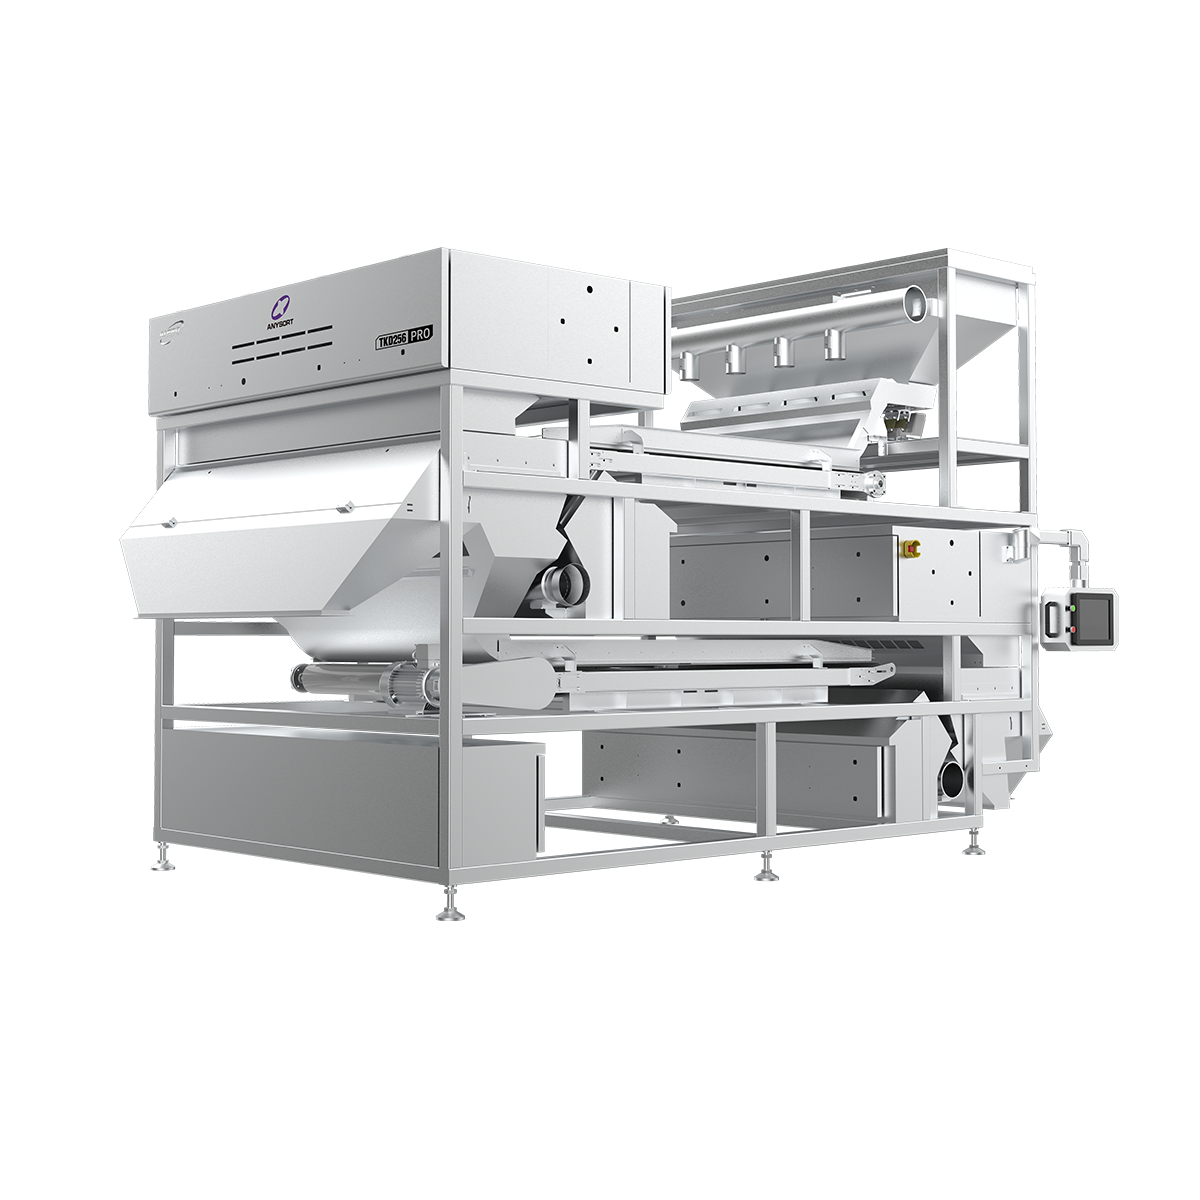
The global demand for advanced sorting technology has positioned China as a hub for innovation in grain and material processing equipment. A color sorter machine manufacturer in China represents a critical investment for agricultural operations, food processors, and industrial facilities seeking precision sorting solutions. The color sorter machine manufacturer sector has evolved dramatically over the past decade, driven by artificial intelligence integration, improved optical sensors, and customer demand for higher throughput and accuracy. Understanding the landscape of leading color sorter machine manufacturer operations helps procurement teams, distributors, and end-users make informed decisions about equipment selection and partnership opportunities.
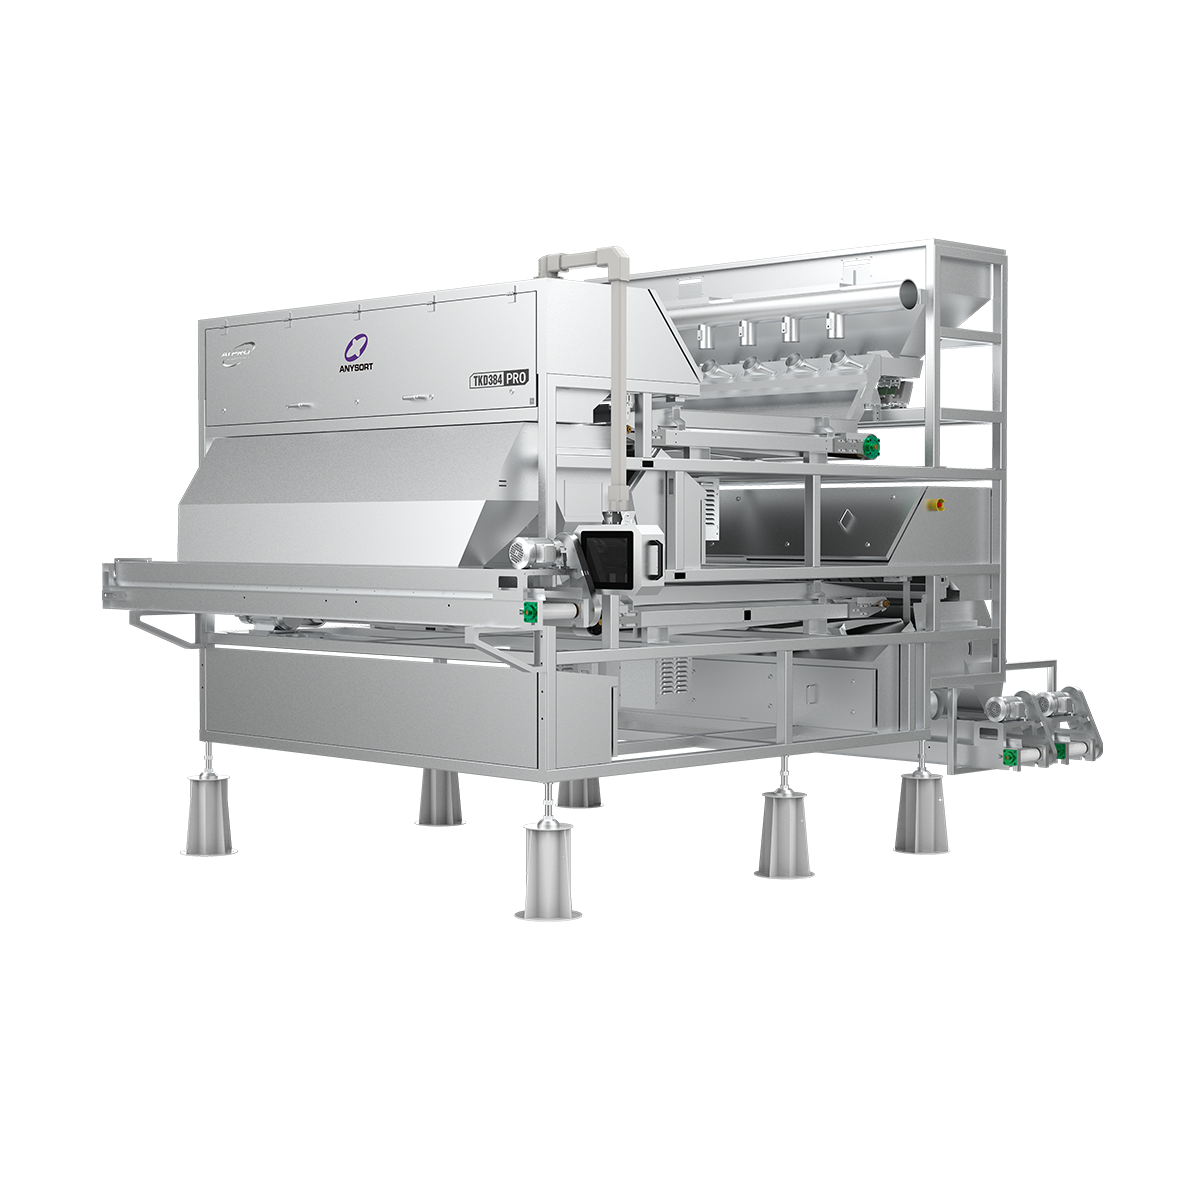
The competitive advantages of a leading color sorter machine manufacturer in China stem from decades of manufacturing expertise, access to component suppliers, and continuous research into artificial intelligence applications. Modern color sorter machine manufacturer operations combine precision engineering with cloud-based analytics, enabling real-time quality monitoring and predictive maintenance. As a color sorter machine manufacturer continues to refine sorting algorithms and hardware capabilities, the value proposition extends beyond simple mechanical sorting to intelligent processing ecosystems that integrate seamlessly with production facilities worldwide.
Key Characteristics of Established Color Sorter Machine Manufacturer Operations
Manufacturing Scale and Production Capacity
A professional color sorter machine manufacturer operates multiple production facilities equipped with advanced testing laboratories and quality assurance departments. The scale of a color sorter machine manufacturer determines its ability to fulfill large international orders, maintain consistent quality standards, and invest in research and development initiatives. Leading manufacturers operate state-of-the-art facilities where each color sorter machine manufacturer unit undergoes rigorous inspection before shipment. Production capacity varies significantly among players, with some color sorter machine manufacturer companies producing hundreds of units monthly while maintaining customization options for specialized applications.
Technological Innovation and AI Integration
The most competitive color sorter machine manufacturer enterprises have embedded artificial intelligence deep into their sorting algorithms, allowing machines to identify defects, color variations, and foreign materials with unprecedented accuracy. A modern color sorter machine manufacturer incorporates multi-spectral imaging, neural networks, and machine learning models to continuously improve sorting performance. The color sorter machine manufacturer that invests in AI capabilities delivers machines capable of handling diverse material types, from rice and wheat to specialty crops and industrial minerals. Innovation in a color sorter machine manufacturer's operations directly translates to customer productivity gains and reduced material waste, making technology advancement a key competitive differentiator.
Quality Standards and Certification Frameworks
International Compliance and Regulatory Alignment
A reputable color sorter machine manufacturer adheres to international quality standards including ISO 9001, CE certification, and industry-specific compliance requirements. The color sorter machine manufacturer must demonstrate product reliability through comprehensive testing protocols and transparent documentation of performance metrics. Quality-focused color sorter machine manufacturer companies implement traceability systems, spare parts management, and technical support networks that span global markets. Customers working with a color sorter machine manufacturer carrying robust certifications gain confidence in equipment durability, safety compliance, and long-term technical support availability.
Performance Metrics and Testing Procedures
Every legitimate color sorter machine manufacturer establishes objective performance benchmarks covering sorting accuracy, throughput capacity, and defect detection rates. A color sorter machine manufacturer evaluates machines using standardized test materials, documenting performance across different grain types and contamination scenarios. The most transparent color sorter machine manufacturer operations provide detailed specifications, video demonstrations, and trial period arrangements allowing customers to validate equipment performance in their own facilities. Testing procedures established by a color sorter machine manufacturer typically include environmental stress tests, sensor calibration verification, and long-term reliability assessments.
Selecting the Right Color Sorter Machine Manufacturer Partner
Assessing Manufacturer Capabilities and Support Infrastructure
Effective partnership with a color sorter machine manufacturer begins with comprehensive evaluation of their technical support, training programs, and spare parts availability. A dedicated color sorter machine manufacturer should offer remote monitoring capabilities, allowing technicians to diagnose issues and optimize machine performance without on-site visits. The color sorter machine manufacturer you choose must provide comprehensive operator training, documentation in your language, and responsive customer service across multiple time zones. Long-term success depends on selecting a color sorter machine manufacturer with established distribution networks, local service centers, and proven track records supporting similar applications in your industry.
Customization Options and Application-Specific Solutions
Leading color sorter machine manufacturer companies recognize that different materials and industries require tailored solutions rather than one-size-fits-all equipment. A sophisticated color sorter machine manufacturer offers modular designs, adjustable sorting parameters, and specialized sensor configurations to match your specific material properties and production goals. The color sorter machine manufacturer capable of delivering customized solutions can address unique challenges like high moisture content, similar color defects, or specialized material grades that standard machines cannot effectively process. Partnering with a flexible color sorter machine manufacturer enables you to optimize sorting performance for your exact application, maximizing return on investment and operational efficiency.
FAQ
What distinguishes a top color sorter machine manufacturer from competitors?
Leading color sorter machine manufacturer operations differentiate through advanced artificial intelligence integration, comprehensive quality certifications, reliable technical support networks, and proven performance in diverse applications. A top color sorter machine manufacturer invests continuously in research and development, maintains rigorous quality control standards, and builds strong relationships with customers through responsive service and transparent communication. The best color sorter machine manufacturer companies combine engineering excellence with customer-focused innovation, ensuring equipment delivers superior sorting accuracy and long-term operational value.
How does a color sorter machine manufacturer incorporate AI technology into sorting equipment?
Modern color sorter machine manufacturer equipment uses machine learning algorithms trained on millions of images to identify defects, color variations, and contamination with exceptional precision. The color sorter machine manufacturer integrates multi-spectral imaging sensors, processing units running sophisticated neural networks, and cloud-based analytics platforms that enable continuous algorithm improvement. A forward-thinking color sorter machine manufacturer implements adaptive learning systems allowing machines to improve sorting performance over time while maintaining detailed quality records for traceability and compliance purposes.
What factors should guide color sorter machine manufacturer selection for specific production needs?
When evaluating a color sorter machine manufacturer, prioritize technical specifications matching your material type, required throughput capacity, and sorting accuracy standards. Assess the color sorter machine manufacturer's customization capabilities, local support infrastructure, training programs, and spare parts availability to ensure long-term operational success. Request product demonstrations, compare warranty terms, verify international certifications, and consult references from existing customers to confirm the color sorter machine manufacturer can reliably support your production requirements and business objectives.